트윈 스크류 압출기 요소 제조업체: 완벽한 B2B 거래 분석 및 글로벌 소싱 가이드
트윈 스크류 압출기 부품의 세계 시장은 미국 간의 B2B 무역으로 인해 상당한 변화를 겪고 있습니다., 유럽연합, 아시아 태평양 제조 허브 강화. 트윈 스크류 압출기 요소 — 나사 세그먼트 포함, 반죽 블록, 배럴 라이너, 및 혼합 요소 — 플라스틱 합성에 중요한 구성 요소입니다., 식품 가공, 의약품 제조, 화학 공학. 고성능 고분자 화합물 및 첨단 소재에 대한 수요가 증가함에 따라, 오른쪽에서 소싱 트윈 스크류 압출기 요소 제조업체 전 세계 프로세서의 전략적 우선순위가 되었습니다.. 이 기사에서는 현재 무역 환경에 대한 심층 분석을 제공합니다., 공급업체 생태계, 시장 기회, 신뢰성을 추구하는 B2B 구매자를 위한 실질적인 지침과 트윈 스크류 압출기 요소 공급 업체 그리고 공장.
트윈 스크류 압출기 부품 산업 현황
트윈 스크류 압출기 시장의 가치는 약 USD 수준입니다. 1.2 10억 2024 USD에 도달할 것으로 예상됩니다. 1.7 10억 단위로 2030, 약 CAGR로 성장 5.8%, Grand View Research와 MarketsandMarkets가 발표한 데이터에 따르면 2024 업계 보고서. 교체 부품 및 요소 세그먼트 — 커버 나사 요소, 배럴, 샤프트, 및 내마모성 부품 — 애프터마켓 수익의 상당 부분을 차지합니다., 30으로 추정–40% 총 압출기 수명주기 지출 대비.
주요 동인에는 다음이 포함됩니다.:
- 자동차 경량화 및 EV 배터리 분리막 생산에서 엔지니어링 플라스틱 및 고분자 화합물에 대한 수요 증가
- 동남아시아 및 동유럽 전역의 마스터배치 및 농축 색상 제조 성장
- 제약 핫멜트 압출 분야에서 트윈 스크류 압출 채택 증가 (HME) 애플리케이션
- 지속 가능성은 재활용업체가 소비 후 수지를 위한 트윈 스크류 시스템을 향해 나아가도록 요구합니다. (PCR) 합성
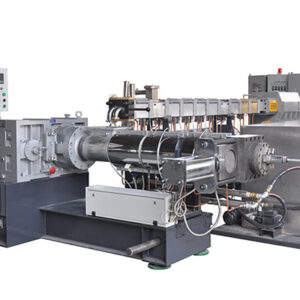
주요 OEM 압출기 브랜드 — 코페리온 (독일), 크라우스마파이 (독일), 라이스트리츠 (독일), JSW (일본), 난징에 본사를 둔 중국 제조업체 — 모두 정밀하게 설계된 나사 요소에 의존합니다.. 하지만, 애프터마켓 및 제3자 트윈 스크류 압출기 요소 제조업체 세그먼트가 빠르게 성장했습니다., 비슷한 야금 및 공차를 갖춘 비용 효율적인 대안 제공. 원천: 그랜드뷰리서치, 2024; 시장과 시장, 2024. 평행 이축 압출기
트윈 스크류 압출기 요소 생산을 대표하는 정밀 금속 부품을 갖춘 산업 제조 시설
산업 부품에 영향을 미치는 무역 정책 환경
The transatlantic trade relationship between the United States and the European Union remains the world's largest bilateral commercial partnership, 총 상품 및 서비스 거래가 USD를 초과하는 경우 1.3 미국 보고에 따르면 연간 1조 달러. 인구조사국과 Eurostat는 초기에. 트윈 스크류 압출기 부품과 같은 산업 기계 부품용, several policy developments in the past two months are particularly relevant:
관세환경 (4월–6월 ): 미국. administration's tariff actions in early have created significant uncertainty for industrial component trade. 부분 301 tariffs on Chinese-origin goods remain in effect, with machinery components facing duties of 25%. The EU's Carbon Border Adjustment Mechanism (CBAM) transitional phase continues to require importers to report embedded emissions in certain goods, though most extruder components fall outside the current CBAM scope (which covers steel, 알류미늄, 시멘트, 비료, 전기, 그리고 수소). 하지만, raw material inputs — particularly tool steel and tungsten carbide used in screw element manufacturing — are indirectly affected. 원천: 국제무역청 (ITA), .
EU 무역 방어 수단: The European Commission's Directorate-General for Trade has maintained anti-dumping duties on certain steel products from China, 이는 EU 시장에 진출하는 중국산 압출기 부품의 비용 구조에 영향을 미칩니다.. 이는 인도 제조업체에 기회를 창출합니다., 칠면조, 국내 EU 생산자. 원천: EU 무역DG, .
무역기술협의회 (TTC): TTC는 주로 반도체와 AI에 중점을 두었지만, 공급망 탄력성 작업 흐름은 중요한 산업 장비 소싱에 영향을 미칩니다., 단일 소스 의존성에서 벗어나 다양화 장려.
글로벌 공급업체 생태계: 트윈 스크류 압출기 부품이 제조되는 곳
트윈 스크류 압출기 요소 공장 환경은 지리적으로 여러 주요 지역에 집중되어 있습니다.:
중국 (난징, 장자강, 쿤산 클러스터)
중국은 애프터마켓 트윈 스크류 압출기 부품의 전 세계 생산량을 장악하고 있습니다.. 난징 클러스터만 단독으로 호스팅 50 스크류 요소 전문 제조업체, 배럴, 완벽한 나사 구성. 주요 이점에는 경쟁력 있는 가격이 포함됩니다. (일반적으로 40–60% 유럽 OEM 가격보다 낮음), 신속한 프로토타이핑 기능, 질화강을 포함한 광범위한 재료 옵션, 바이메탈 합금, PM-HIP (분말 야금 열간 등압 성형) 재료, 및 텅스텐 카바이드 코팅. 주목할만한 제조업체로는 Nanjing Kerke Extrusion Equipment가 있습니다., 난징 하이시 압출 장비, 장쑤 Xinda 기술. 중국 제조업체는 CNC 연삭에 막대한 투자를 해왔습니다., 좌표 측정기 (CMM), 유럽과 미국의 품질 표준을 충족하는 야금 테스트.
독일과 서유럽
독일은 여전히 기술 리더다., 코페리온 같은 회사와, 라이스트리츠, 공차가 엄격한 프리미엄급 부품을 제공하는 전문 요소 생산업체 (일반적으로 ±0.01mm) 고급 야금술. 유럽 제조업체는 추적성을 강조합니다., 재료 인증 (안에 10204 3.1 인증서), 장기적인 치수 안정성. 가격은 프리미엄 수준입니다, 그러나 마모가 심한 응용 분야에서는 총 소유 비용이 경쟁력이 있을 수 있습니다..
인도와 터키 (신흥 공급업체)
India's twin screw extruder elements manufacturing sector is growing, Ahmedabad 및 Pune의 회사는 품질 개선과 함께 중간급 가격을 제공합니다.. 터키는 서유럽보다 저렴한 비용으로 중국보다 짧은 리드 타임을 원하는 EU 구매자에게 근거리 옵션으로 부상했습니다..
산업 부품에 대한 국제 B2B 무역 물류를 대표하는 컨테이너 선박이 있는 글로벌 해운항
트윈 스크류 압출기 부품 시장의 B2B 거래 기회
B2B 구매자의 경우 — 플라스틱 배합기를 포함하여, 푸드 프로세서, 제약 제조업체, 및 압출기 OEM — 몇 가지 중요한 기회가 나타났습니다.:
1. 공급망 다각화: The ongoing US-China trade tensions and tariff uncertainties have accelerated "China+1" 소싱 전략. B2B 구매자는 대체 지역에서 자격을 갖춘 트윈 스크류 압출기 부품 공급업체를 적극적으로 찾고 있습니다.. 이는 인도 제조업체에 기회를 창출합니다., 베트남, 시장 점유율을 확보하기 위한 터키, 기존 중국 제조업체는 더 빠른 배송으로 현지 재고를 제공하기 위해 미국과 EU에 창고를 설립함으로써 대응하고 있습니다..
2. 애프터마켓 성장: 트윈 스크류 압출기의 설치 기반이 전 세계적으로 증가함에 따라 — 이상으로 추정 50,000 전세계 활성 기계 — 교체 요소에 대한 수요, 부품을 착용하다, 업그레이드 키트는 계속해서 확장되고 있습니다.. 30에서 OEM과 동등한 품질을 제공하는 타사 제조업체–50% 저렴한 가격이 좋은 위치에 있습니다.. Alibaba와 같은 B2B 전자상거래 플랫폼, 메이드 인 차이나, GlobalSources를 통해 구매자는 트윈 스크류 압출기 부품 도매 공급업체를 더욱 쉽게 식별하고 자격을 얻을 수 있습니다..
3. 소재 혁신: 고급 야금술은 차별화 기회를 창출하고 있습니다.. PM-HIP (분말 야금 열간 등압 성형) 나사 요소 제공 3–5x 기존 제품에 비해 수명이 길어졌습니다. 2단 압출기 연마용 질화강 (유리 섬유, 미네랄 필러). 이러한 기술에 투자하는 제조업체는 프리미엄 가격을 책정하는 동시에 구매자에게 더 낮은 총 소유 비용을 제공할 수 있습니다.. 압출기 제조업체
4. 맞춤화 및 엔지니어링 지원: B2B 구매자는 점점 더 부품뿐만 아니라 나사 구성 설계 지원도 필요로 합니다.. 시뮬레이션 기반 나사 설계 서비스를 제공하는 제조업체 (Ludovic 또는 독점 소프트웨어와 같은 도구 사용) 요소 제조와 함께 더 높은 가치의 주문을 확보하고 있습니다..
B2B 구매자와 제조업체가 직면한 과제
기회에도 불구하고, 트윈 스크류 압출기 부품 무역에는 몇 가지 문제가 지속됩니다.:
품질 검증: 주장된 품질과 실제 야금 품질 사이의 격차는 여전히 중요한 문제로 남아 있습니다., 특히 새로운 공급업체로부터 소싱할 때. 구매자가 일관성 없는 경도 문제를 보고합니다. (사양을 초과하는 HRC 변형), 스플라인 프로파일의 표면 마감 불량, 조기 마모 또는 가공 불안정을 유발하는 치수 편차. 완화 전략에는 제3자 검사 요구가 포함됩니다. (SGS, 뷰로베리타스), 재료 테스트 인증서 요청, 대량 구매를 시작하기 전에 평가판 수량을 주문합니다..
지적재산권 문제: OEM 압출기 제조업체는 특허로 보호되는 독점 스크류 요소 형상을 보유하고 있습니다.. 타사 제조업체는 IP 경계를 신중하게 탐색해야 합니다., 호환 가능하지만 침해하지 않는 디자인 제공. 이는 특히 자체 닦이는 프로파일 형상 및 특수 혼합 요소 설계와 관련이 있습니다..
물류 및 리드타임: 중국에서 미국 서부 해안까지의 해상 운송에는 14가 소요됩니다.–21 날, 추가 내륙 교통. 수에즈 운하 경로를 통한 EU행 배송에는 28일이 소요됩니다.–35 날. 긴급 주문에는 항공 화물을 이용할 수 있지만 비용이 5만큼 증가합니다.–8엑스. 홍해 해상 운송 중단 2024 아시아-유럽 노선의 조기 지연 및 비용 증가 초래, 일부 구매자를 유럽 또는 터키 공급업체로 유도. 원천: 상업저널, .
통화 및 결제 위험: 이 부문의 B2B 거래에는 일반적으로 전신 송금이 포함됩니다. (티/티) ~와 함께 30% 보증금과 70% 대량 주문의 경우 선적 서류 또는 L/C와의 잔액. USD 간 환율 변동, EUR, CNY는 도착 비용에 3만큼 영향을 줄 수 있습니다.–8% 조달주기에 걸쳐.
트윈 스크류 압출기 요소 제조 공정과 유사한 금속 부품을 생산하는 정밀 CNC 머시닝 센터
무역의 지리적, 정책적 이점
무역 통로는 산업 부품의 B2B 구매자에게 뚜렷한 이점을 제공합니다.:
규제 조정: 미국과 EU 모두 산업 장비 안전 및 재료 규정 준수에 대한 높은 표준을 유지합니다.. EU 표준에 따라 제조된 부품 (CE마킹, 폭발성 환경을 위한 ATEX) 최소한의 추가 인증만으로 미국 시장에서 일반적으로 허용됩니다.. 이러한 규정 호환성은 두 시장 모두에 서비스를 제공하는 제조업체의 규정 준수 비용을 줄여줍니다..
항만 인프라: 로테르담을 포함한 주요 항구 (Europe's largest), 함부르크, 앤트워프-브뤼헤, 로스앤젤레스/롱비치, Savannah는 컨테이너화된 산업용 부품을 효율적으로 처리합니다.. Rotterdam's Europoort complex handles over 14 million TEUs annually and offers direct connections to Europe's inland waterway network, 독일의 제조 클러스터에 비용 효율적으로 배포 가능, 벨기에, 그리고 네덜란드. 원천: 로테르담 항만청, 2024.
자유무역지역 및 보세창고: 미국 둘 다 (대외 무역 지역) 그리고 나 (자유지역) 압출기 부품 수입업자에게 혜택을 주는 관세 연기 및 감소 메커니즘 제공. 주요 시장에 보세 창고를 설립하는 제조업체는 관세 지불을 최적화하는 동시에 현지 재고 가용성을 제공할 수 있습니다..
무역금융 인프라: 미국과 EU의 성숙한 은행 시스템은 신용장을 포함한 신뢰할 수 있는 무역 금융 수단을 제공합니다., 수출신용보험 (오일러 헤르메스 같은 에이전시를 통해, 수출입은행), 구매자와 판매자 모두의 지불 위험을 줄이는 공급망 금융 프로그램.
압출기 요소 시장의 사례 연구 성공
사례 연구 1: EU 유통을 설립하는 중국 제조업체
난징에 본사를 둔 이축 압출기 부품 제조업체로 연간 매출이 약 USD입니다. 15 백만 명은 유럽 바이어들이 긴 리드 타임과 품질 문제로 인해 중국에서 직접 주문하는 것을 주저하고 있다는 사실을 인식했습니다.. ~ 안에 2023, 회사는 뒤스부르크에 창고를 설립했습니다., 독일 — Europe's largest inland port and a key logistics hub on the Belt and Road rail corridor. 재고를 유지함으로써 200+ 공통 나사 요소 펠릿화 공장 명세서 (코페리온 ZSK용, 라이스트리츠 ZSE, and KraussMaffei ZE series compatibility), they reduced delivery time from 35–45 days to 3–5 business days for EU customers. The company invested in EN 10204 3.1 material certification for all stocked items and hired a German-speaking technical sales engineer. Result: EU revenue grew 180% ~에 18 개월, with key accounts including compounders in Germany, 이탈리아, and Poland.
사례 연구 2: US Compounder Implementing Dual-Source Strategy
A mid-size plastics compounder in Texas operating 12 트윈 스크류 압출기 라인 (mix of Coperion and Leistritz machines) was spending approximately USD 400,000 annually on OEM replacement elements. After qualifying two alternative suppliers — one in Nanjing, 중국, and one in Ahmedabad, 인도 — the company reduced its annual spend to USD 220,000 while maintaining processing quality. The qualification process involved: Plastic Pellets Extruder (1) requesting sample elements with full material certificates, (2) conducting independent hardness and dimensional testing at a local metallurgical lab, (3) running 500-hour production trials on non-critical lines, 그리고 (4) gradually expanding to all lines over 6 개월. The dual-source approach also provided supply chain resilience when the Chinese supplier experienced a 3-week shipping delay due to port congestion.
사례 연구 3: European OEM Partnering with Specialized Element Manufacturer
A mid-tier European extruder OEM based in Italy, producing approximately 80 twin screw extruder lines annually, transitioned from in-house screw element production to a partnership model with a specialized manufacturer. By outsourcing element production to a dedicated facility with advanced CNC grinding capabilities and PM-HIP material processing, the OEM reduced its manufacturing footprint, improved element quality consistency, and shortened delivery times for custom screw configurations. The partnership model allowed the OEM to focus on machine design, 집회, and customer application engineering while the element manufacturer handled the metallurgy-intensive production. This approach is increasingly common in the industry, as reported by 오늘날의 플라스틱, 2024.
Business professionals in a B2B trade negotiation meeting discussing industrial component sourcing strategies
Trade Show and Industry Event Landscape
B2B buyers and manufacturers of twin screw extruder elements connect at several key industry events:
- K 무역 박람회 (뒤셀도르프, 독일): The world's largest plastics trade show, 3년마다 개최 (다음 판: 십월 ). All major extruder OEMs and many element manufacturers exhibit. Essential for supplier discovery and technology benchmarking.
- 이름 (올랜도, USA): North America's largest plastics show, 3년마다 개최. 그만큼 2024 edition attracted over 50,000 방문객을 맞이하고 광범위한 압출 기술 전시회를 선보였습니다..
- 차이나플라스 (심천/상하이, 교대로): Asia's largest plastics show, 중국 압출기 요소 제조업체의 강력한 대표력. 심천 에디션이 특집으로 소개되었습니다. 4,000 전시업체.
- 파쿠마 (프리드리히스하펜, 독일): 강력한 압출 기술에 초점을 맞춘 연례 유럽 플라스틱 전시회, 10월 예정.
이러한 이벤트는 직접 품질 평가를 위한 기회를 제공합니다., 대면 협상, B2B 산업부품 무역에 있어서 중요한 관계 구축 및 관계 구축. 원천: 메세 뒤셀도르프, .
구매자를 위한 재료 과학 및 기술 고려 사항
올바른 트윈 스크류 압출기 요소 제조업체를 선택하려면 성능과 수명에 영향을 미치는 기술 사양을 이해해야 합니다.:
나사 요소의 일반적인 야금학
- 질화강 (예를 들어, 1.8550 / 34CrAlNi7): 범용 컴파운딩의 표준재료. 표면 경도 900–1100 HV, 질화 깊이 0.3–0.7mm. 연마 응용 분야에서는 비용 효율적이지만 마모 수명이 제한적입니다..
- 경화 공구강 (예를 들어, D2, CPM-9V): 더 높은 벌크 경도 (58–62 HRC) 유리 섬유 및 미네랄 필러의 마모에 대한 저항력이 향상되었습니다..
- PM-HIP 소재 (예를 들어, CPM-10V, 반크론 40): 열간 등압 성형으로 가공된 분말 야금강은 탁월한 내마모성을 제공합니다. (3–5x 질화강) 좋은 인성을 가지고. 고충진 컴파운드 및 재활용 응용 분야에 대한 지정이 점점 늘어나고 있습니다..
- 텅스텐 카바이드 (화장실/공동): 마모가 매우 심한 응용 분야를 위한 최고의 내마모성 옵션. 일반적으로 코팅으로 적용되거나 특정 요소 유형에 대해 고체 형태로 사용됩니다.. 비용은 5–10x 질화강.
- Stellite 및 Colmonoy 코팅: 화학 및 제약 공정의 내식성 응용 분야를 위해 용접 또는 열 분사로 적용되는 코발트 기반 및 니켈 기반 표면 경화 합금.
구매자는 재료 테스트 인증서를 요청해야 합니다. (화학 성분, 경도 프로파일, microstructure 이미지) 구매 주문서에 승인 기준을 명시합니다.. 평판이 좋은 제조업체는 품질에 대한 헌신을 보여주기 때문에 이러한 요구 사항을 환영합니다..
산업용 부품의 정밀 제조에 사용되는 고급 야금 테스트 및 품질 관리 장비
직장 안전: 압출 제조 환경에서 작업자 보호
트윈 스크류 압출 산업은 B2B 운영자가 해결해야 하는 중요한 작업장 안전 문제를 제시합니다.. 압출 설비에는 중장비가 포함됩니다., 고온 (배럴 온도는 일반적으로 150~150도 범위입니다.°C~350°기음), 회전 장비, 연마재, 화학첨가제 등의 원료 취급 및 취급. 작업자 안전 — 특히 발 보호 — 중요한 운영 요구 사항입니다..
압출 공장에서 안전 신발이 필수적인 이유
압출 제조 환경은 작업자를 다양한 발 부상 위험에 노출시킵니다.:
- 무거운 물체에 충격을 가함: 트윈 스크류 압출기 요소 — 개별 나사 세그먼트, 배럴 섹션, 그리고 다이 플레이트 — 무게를 달 수 있다 2 kg 이상 50 kg. 나사 요소 또는 배럴 부분이 떨어지면 보호되지 않은 발에 심각한 압쇄 부상이 발생할 수 있습니다.. OSHA는 발 부상이 대략적으로 발생한다고 보고합니다. 60,000 미국 제조업에서 매년 직장 부상, 평균으로 7 사고당 근무일 손실. 원천: OSHA, 2024.
- 압축 위험: 압출기 조립 및 유지보수 중, 작업자는 오버헤드 크레인과 호이스트를 사용하여 무거운 구성품을 배치합니다.. 잘못된 정렬이나 장비 고장으로 인해 조립 영역 근처에 있는 발에 압박 부상이 발생할 수 있습니다..
- 펑크 위험: 압출 설비에는 금속 부스러기가 있는 경우가 많습니다., 부러진 나사 요소 조각, 철사, 바닥에 고정 장치도 있고. 표준 신발은 이러한 날카로운 물체로 인한 자상을 방지할 수 없습니다..
- 열적 위험: 용융 폴리머 드립, 핫 퍼지 재료, 가열된 배럴 표면과 접촉하면 심각한 화상을 입을 수 있습니다.. 압출 다이 및 다운스트림 장비 근처에서 작업하는 작업자에게는 적절한 밑창 등급을 갖춘 내열성 안전 신발이 필수적입니다..
- 미끄러짐 위험: 폴리머 펠릿, 가공유, and cleaning solvents create slippery floor conditions. Anti-slip safety footwear with SRC-rated soles (tested on both ceramic tile with sodium lauryl sulfate and steel with glycerol) significantly reduces slip-and-fall incidents.
- 전기적 위험: Extruder drive motors, 히터 밴드, and control systems present electrical shock risks. ESD (정전기 분산) or EH (전기적 위험) rated safety footwear provides an additional layer of protection.
Safety Footwear Standards and Certifications
B2B buyers sourcing safety footwear for extrusion plant workers should understand the applicable standards:
- ISO에서 20345 (EU 표준): Defines safety footwear with toe protection capable of withstanding 200J impact and 15kN compression. Classes include S1 (정전기 방지, energy absorption at heel), S1P (adds puncture resistance), S3 (adds water resistance and profiled outsole), and the newer S5 (waterproof boot with puncture resistance).
- ASTM F2413 (미국 표준): 충격 저항성을 포함한 보호 신발의 성능 요구 사항을 지정합니다. (I/75 = 75 ft-lbs), 압축 저항 (C/75 = 2,500 파운드), 중족골 보호 (산/75), and electrical hazard protection (뭐라고).
- 복합 대. Steel Toe Caps: 현대 안전 신발은 점점 더 복합재를 사용합니다. (유리섬유, 탄소섬유, 또는 케블라) 강철 대신 발가락 캡. 합성 발가락이 더 가볍습니다. (30–40% 체중 감소), 비금속 (콜드 트랜스퍼 불가, 공항 친화적), 동일한 충격/압축 표준을 충족합니다.. 8인이 근무하는 압출공장 환경에 적합–12 시간 교대, 무게 감소로 편안함이 크게 향상되고 피로가 줄어듭니다..
산업 운영을 위한 안전화 B2B 소싱
압출설비를 관리하는 B2B 사업자를 위한, 안전화 조달은 전략적으로 접근해야 합니다:
대량 구매: 시설 50+ 근로자는 상당한 수량 할인을 협상할 수 있습니다. (일반적으로 15–30% 소매 아래) 안전 신발 제조업체 또는 공인 대리점과 직접 협력하여. 연간 교체 프로그램을 통해 작업자는 항상 신발 상태를 양호하게 유지할 수 있습니다..
애플리케이션별 선택: 압출 공장 내 다양한 역할에는 다양한 보호 수준이 필요합니다.. 압출기 배럴 근처에서 작업하는 기계 작업자에게는 내열성 밑창이 필요합니다. (HRO 등급 300°C 접촉열). 유지보수 기술자는 중족골 보호 및 펑크 방지가 필요합니다.. 원자재 및 완제품을 취급하는 창고 직원에게는 충격 방지 및 미끄럼 방지 밑창이 필요합니다.. 계층형 사양 접근 방식은 보호와 비용을 모두 최적화합니다..
편안함과 규정 준수: 가장 보호력이 뛰어난 안전화도 작업자가 착용을 거부하면 쓸모가 없습니다.. Uvex와 같은 제조업체의 최신 안전 신발, 푸마 안전, 팀버랜드 프로, 레드윙, KEEN 유틸리티는 EVA 미드솔을 포함한 운동화의 편안함 기능과 보호 기능을 결합합니다., 수분 흡수 안감, 그리고 인체공학적인 풋베드. 편안한 안전화에 투자하면 일반적인 70%에서 규정 준수율이 향상됩니다.–80% 이상으로 95%, 부상 사고를 직접적으로 감소.
총 소유 비용: Premium safety footwear costing USD 120–180 per pair with a 12-month service life is more cost-effective than budget options at USD 40–60 that require replacement every 4–6 개월. The total cost including procurement, fitting, and disposal favors quality products. 추가적으로, each prevented foot injury saves an estimated USD 9,000–15,000 in direct medical costs and lost productivity, according to the National Safety Council. 원천: 국가안전협의회, 2024.
Complete Extrusion Systems Factory Industrial safety boots with steel toe protection used in manufacturing and extrusion plant environments Amazon Extruder Screw
Future Trade Trends: What to Expect in the Next 1-2 개월 (칠월–팔월 )
현재 시장 지표를 기준으로, 정책 개발, 업계 신호, several trends are likely to shape the twin screw extruder elements trade in the near term:
1. 관세 불확실성으로 인해 재고 축적이 촉진될 것: With ongoing US tariff policy volatility, B2B buyers are expected to increase safety stock levels of critical extruder components. Manufacturers with US and EU warehouse capabilities will see increased demand. Chinese manufacturers offering DDP (관세 지불 인도됨) pricing to US destinations will gain competitive advantage by absorbing tariff complexity for buyers.
2. Sustainability Requirements Will Intensify: EU buyers are increasingly requesting carbon footprint data for purchased components. The CBAM reporting requirements, while not yet directly covering machinery components, are creating a culture of emissions transparency that extends through supply chains. Manufacturers providing EPD (Environmental Product Declarations) or carbon footprint calculations for their products will differentiate themselves. The recycling sector's growth — driven by EU packaging regulations mandating 30% recycled content by 2030 — will increase demand for wear-resistant screw elements optimized for processing contaminated post-consumer waste streams.
3D Extruder Radiator 3. Digital Procurement Will Accelerate: B2B platforms are becoming more sophisticated in handling technical industrial components. Expect to see more twin screw extruder element manufacturers offering online configurators where buyers can select element type, 크기, 재료, and quantity with instant pricing. This reduces the traditional quote-negotiate-order cycle from 1–2 weeks to minutes, particularly for standard specifications.
4. Nearshoring Momentum in Europe: The combination of Red Sea shipping disruptions, rising Chinese labor costs, and EU supply chain due diligence regulations (the Corporate Sustainability Due Diligence Directive, effective 2026) will continue to push European buyers toward Turkish, Eastern European, 그리고 인도 공급업체. Turkey's proximity to EU markets (3–5 day shipping to major EU ports) and its customs union with the EU make it particularly attractive. Power Heater Extruder
5. Consolidation Among Manufacturers: The twin screw extruder elements manufacturing sector remains fragmented, 특히 중국에서는. Expect continued consolidation as larger manufacturers acquire smaller competitors to gain capacity, 기술, and customer relationships. This consolidation will ultimately benefit B2B buyers through improved quality consistency and financial stability of suppliers.
Aluminum Extruders Tennessee 6. Advanced Coating Technologies: PVD (Physical Vapor Deposition) and CVD (Chemical Vapor Deposition) coatings for screw elements are moving from laboratory to commercial availability. These coatings — including TiAlN, CrN, and DLC (Diamond-Like Carbon) — can extend element life by 2–4엑스 Tornado Extruder Kit in specific applications. Manufacturers investing in coating capabilities will capture premium market segments. 원천: 오늘날의 플라스틱, ; ITA Market Intelligence, .

Modern warehouse and logistics facility for B2B industrial component distribution and wholesale operations
Practical Sourcing Guide: How to Select a Twin Screw Extruder Elements Manufacturer
Underwater Pelletizer Supplier For B2B buyers evaluating potential suppliers, the following framework provides a structured approach:
단계 1: Define Technical Requirements
Document your extruder model, element specifications (OD, ID, length, profile type), material requirements, quantity, and delivery schedule. Include tolerance requirements and surface finish specifications. The more precise your specification, the more accurate and comparable the quotes you receive.
단계 2: Identify Potential Suppliers
Use multiple channels platforms (알리바바, 메이드 인 차이나, ThomasNet for US suppliers, Europages for EU suppliers), 무역 박람회 참가업체 목록 (케이쇼, 차이나플라스, 이름), industry referrals, and direct Google searches for "twin screw extruder elements factory" with geographic qualifiers.
단계 3: Initial Qualification
Request company profiles, production capability presentations, customer reference lists, and quality certifications (ISO 9001 최저한의, ISO 14001 preferred). Evaluate response time and communication quality as indicators of service capability.
단계 4: Sample and Test
Order sample elements (typically 2–5 조각) with full material certificates. Conduct independent testing: 치수검사 (CMM 측정), 경도 테스트 (surface and cross-section), 그리고 가능하다면, metallographic examination. Compare results against specifications and OEM benchmarks.
단계 5: Trial Production Run
Install qualified sample elements on a non-critical extruder line and run for a defined period (typically 500–1000 시간). Monitor processing parameters, 제품 품질, and element wear. Document results for comparison with incumbent supplier performance.
단계 6: Negotiate and Formalize
Based on successful trials, negotiate pricing (consider volume tiers, annual contracts, and consignment stock arrangements), 지불 조건, warranty conditions, and quality assurance protocols. Formalize the relationship with a supply agreement that includes quality specifications, delivery requirements, 분쟁 해결 메커니즘.
자주 묻는 질문 (FAQ)
- What materials are commonly used for twin screw extruder elements?
- The most common materials include nitrided steel (34CrAlNi7/1.8550), through-hardened tool steels (D2, CPM-9V), powder metallurgy HIP materials (CPM-10V, 반크론 40), and tungsten carbide for extreme wear applications. Material selection depends on the processed material's abrasiveness, corrosiveness, and processing temperature. A qualified manufacturer will recommend the optimal metallurgy based on your specific application.
- What is the typical lead time for custom twin screw extruder elements?
- Lead times vary by manufacturer and order complexity. Chinese manufacturers typically quote 3–5 weeks for standard specifications and 5–8 weeks for custom or PM-HIP materials. European manufacturers quote 4–8 weeks for standard and 8–12 weeks for specialized materials. Manufacturers maintaining warehouse stock of common sizes can ship within 1–5