

Twin vis extruder eleman faktori: Gid Komès B2B definitif pou manifaktirè yo, Founisè yo & Achtè an gwo nan
Mache mondyal eleman extruder vis jimo a ap fè eksperyans momantòm enpòtan kòm konpoze plastik, pwosesis manje, pharmaceutique, ak endistri chimik yo elaji atravè Amerik di Nò ak Ewòp. Pou achtè B2B k ap chèche yon serye jimo vis extruder eleman faktori, konprann peyizaj fabrikasyon an, politik komès, koridò lojistik yo, ak apwovizyone pi bon pratik esansyèl. Gid sa a bay yon analiz apwofondi de ekosistèm faktori eleman extruder vis jimo—kouvri dirijan manifaktirè yo, wholesale evalyasyon founisè, dinamik komès, konsiderasyon tarif yo, ak previzyon aksyon pou Q3–Q4. Kit ou se yon konpoze nan Almay, yon processeur plastik nan Ohio, oswa yon konpayi komès apwovizyone eleman vis nan echèl, resous sa a ekipe w ak entèlijans pou pran desizyon akizisyon konfyans.
Konprann eleman Twin Screw Extruder: Eleman debaz ak aplikasyon endistriyèl
Twin vis extruder eleman yo se blòk bilding modilè yo mete sou arbr yo nan ko-wotasyon oswa kont-wotasyon ekstride vis jimo.. Eleman sa yo—ki gen ladan eleman transmèt, mase blòk, eleman melanje, ak eleman vol inverse—detèmine sizayman an, tan rezidans, ak karakteristik debi nan pwosesis la extrusion. Yon espesyalize jimo vis extruder eleman faktori pwodui eleman sa yo soti nan asye zouti (pa egzanp, W6Mo5Cr4V2, 38CrMoAlA) oswa alyaj poud metaliji ak tolerans sere, tipikman ±0.01 mm sou pwofil la involute.
Sektè aplikasyon kle kondwi demann yo enkli:
- Konpozisyon plastik: Pwodiksyon Masterbatch, polymère melanje, konpoze plen ak ranfòse (fib vè, fib kabòn, file mineral).
- Pwosesis manje: Ekstrisyon goute, manje bèt kay, pwoteyin legim teksti (TVP), ak pwodiksyon sereyal.
- Famasetik: Ekstrisyon cho-fonn pou sistèm livrezon dwòg—yon segman k ap grandi byen vit nan Inyon Ewopeyen an ak Etazini.
- Pwosesis chimik: Ekstrisyon reyaktif, devolatilizasyon, ak melanje kontinyèl nan adezif, sele, ak kouch.
- Resiklaj: Resiklaj mekanik nan plastik pòs-konsomatè, a sector boosted by EU Circular Economy regulations and US EPA initiatives.
Double-Screw Extruder Dapre done ki soti nan Rechèch Grand View (2024), mache mondyal extruder jimo a te valè apeprè USD 1.2 billion and is projected to grow at a CAGR of 5.2% atravè 2030. The replacement and upgrade cycle for screw elements—which are wear parts—generates a recurring aftermarket estimated at 30–40% of the total extruder market value, making the twin screw extruder elements factory segment a critical supply chain node. Mixing Equipment Supplier

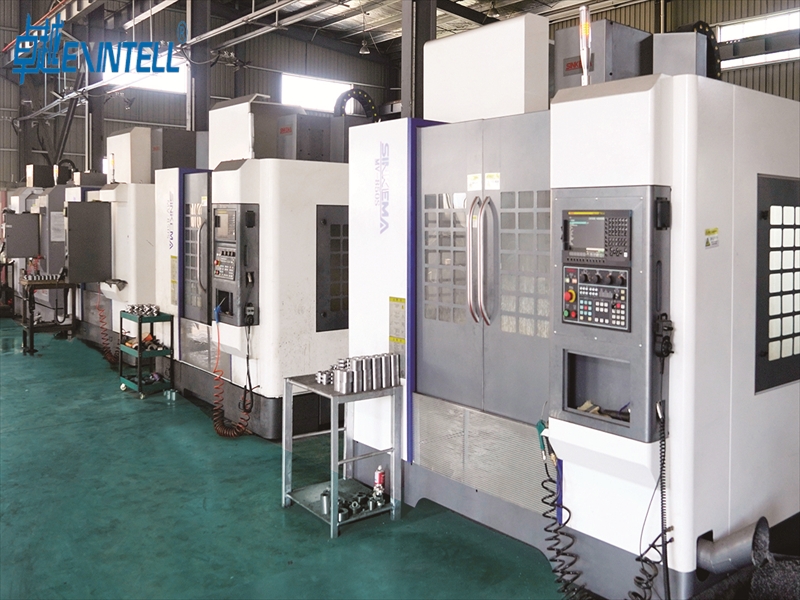
Industrial manufacturing facility with CNC machinery producing precision metal components for extrusion equipment
The Global Twin Screw Extruder Elements Factory Landscape: Who Makes What and Where
The manufacturing base for twin screw extruder elements is concentrated in several key regions, yo chak ak avantaj konpetitif diferan:
Lachin: The Volume Leader
China hosts the largest number of twin screw extruder elements factories, prensipalman gwoupe nan Nanjing (Pwovens Jiangsu), which is often called the "Extruder Capital" nan mond lan. Faktori ki baze nan Nanjing tankou Nanjing Jieya Extrusion Equipment Co., Nanjing Haisi Extrusion Ekipman Co., ak Nanjing Kerke Extrusion Equipment Co. bay eleman vis globalman. Faktori Chinwa yo ofri pri konpetitif—souvan 40–60% anba a ekivalan OEM Ewopeyen an—pandan y ap de pli zan pli matche kalite atravè envèstisman nan sant fanm k'ap pile CNC (pa egzanp, Pandri nan Niles, Reishauer) ak laboratwa tès métallurgique. Pou achtè an gwo, Lachin rete orijin prensipal apwovizyone pou pri-la efikas, gwo volim lòd.
Almay: Precision Benchmark la
Pince yon extruder Almay se lakay yo nan orijinal jimo vis extruder OEM yo—Coperion (Stuttgart), KraussMaffei Ekstrisyon (Hannover), ak Leistritz (Nuremberg). Konpayi sa yo fabrike eleman vis propriétaires ak tolerans ki pi sere ak metaliji prim. Eleman ki fèt Alman yo kòmande pri prim nan 2–4× sou ekivalan Chinwa men yo pi pito pou aplikasyon kritik nan edikaman, polymère pèfòmans-wo, ak manje-kontak extrusion kote trasabilite ak sètifikasyon (FDA, Inyon Ewopeyen 1935/2004) yo obligatwa.
Etazini: Kapasite Domestik k ap grandi
Manifaktirè ki baze nan Etazini tankou Entek (Liban, Oregon), Ekstrisyon Syèk (Traverse City, Michigan), ak CPM Extrusion Group bay tou de eleman vis OEM ak apre mache. Tandans nan reshoring, anplifye pa Seksyon 301 tariffs on Chinese machinery components and the CHIPS and Science Act's broader manufacturing incentives, ap ankouraje ekspansyon kapasite domestik. Sepandan, Faktori US toujou reprezante yon ti fraksyon nan pwodiksyon mondyal la.
Browse katalòg konplè nou an jimo vis extruder eleman Enjenieri pou Coperion, Leistritz, JSW, ak pwofil arbr Berstorff. Twin Screw Extruder machin manifakti
Politik Komèsyal ak enpak li sou Twin Screw Extruder Eleman Sourcing
The transatlantic trade relationship between the United States and the European Union is the world's largest bilateral commercial partnership, ak machandiz ak sèvis komès depase USD 1.3 billions chak ane selon la Biwo Reprezantan Komès Etazini (USTR) (2024 done). Pou achtè B2B nan eleman extruder vis jimo, plizyè dimansyon politik yo dirèkteman enpòtan:
Estrikti Tarif yo
Twin vis extruder eleman tipikman tonbe anba Kòd HS 8477.90 (pati nan machin pou travay kawotchou oswa plastik). MFN Ameriken an (Nasyon ki pi favorize) tarif tarif yo pou HS 8477.90 se 3.1% pou enpòtasyon ki soti nan eta manm Inyon Ewopeyen yo. Inyon Ewopeyen enpòtasyon soti nan peyi Etazini an fè fas a yon pousantaj konparab nan 2.7% anba Tarif Ladwàn Komen Inyon Ewopeyen an. Pousantaj tarif yo relativman ba sa yo fasilite komès bilateral nan eleman extruder.
Sepandan, lè apwovizyone soti nan Lachin, Enpòtatè Ameriken yo fè fas a yon lòt 25% Seksyon 301 tarif sou HS 8477.90 machandiz, enpoze depi 2018 epi kenbe atravè. Diferans tarif sa a te refòme estrateji apwovizyone yo: kèk Extruder Wholesale US konpoze kounye a sous eleman vis nan faktori Inyon Ewopeyen yo (patikilyèman Almay ak Itali) pou evite tarif Lachin nan, pandan ke lòt moun absòbe pri a akòz siyifikatif avantaj pri baz eleman Chinwa yo. Wholesale Lab extruders
Mekanis Ajisteman Fwontyè Inyon Ewopeyen Kabòn (CBAM)
The EU's CBAM, ki te antre nan faz tranzisyon li nan mwa Oktòb 2023 epi yo pral vin konplètman operasyonèl pa 2026, aplike nan enpòtasyon asye ak aliminyòm—matyè premyè kle pou pwodiksyon eleman vis. Yon faktori eleman extruder vis jimo ekspòte nan Inyon Ewopeyen an ap bezwen rapòte emisyon kabòn entegre, epi evantyèlman achte sètifika CBAM. Règleman sa a, dokimante pa la Komisyon Ewopeyen an – Taksasyon ak Inyon Ladwàn, ajoute konpleksite konfòmite ak pri potansyèl pou manifaktirè ki pa Inyon Ewopeyen, patikilyèman sa yo ki nan rejyon ki gen kabòn-entansif pwodiksyon asye.
Konsèy Komès ak Teknoloji (TTC)
TTC a, etabli nan 2021, gen gwoup k ap travay sou detèminasyon chèn ekipman ak aliyman estanda. Pou konpozan machin endistriyèl tankou eleman vis, the TTC's efforts to harmonize technical standards (pa egzanp, sètifikasyon materyèl, tolerans dimansyon) ta ka diminye baryè ki pa tarif yo epi fasilite akizisyon transfontyè. La Administrasyon Komès Entènasyonal (ITA) bay mizajou regilye sou pwogrè TTC.

View ayeryen nan yon gwo pò Ewopeyen an ak bato kontenè ak enfrastrikti lojistik sipòte komès entènasyonal B2B
Opòtinite komès B2B pou eleman Twin Screw extruder nan mache US ak Inyon Ewopeyen
Konvèjans plizyè tandans macro ap kreye gwo opòtinite B2B pou faktori eleman extruder vis jimo k ap sèvi Etazini ak Inyon Ewopeyen an.:
Opòtinite 1: Manda pou resiklaj plastik
Dispermat Mixer The EU's Packaging and Packaging Waste Regulation (PPWR), adopte nan 2024, mande minimòm kontni resikle nan anbalaj plastik—30% pa 2030 epi 65% pa 2040. Nan peyi Etazini, eta tankou Kalifòni (SB 54), New Jersey, ak Oregon te adopte responsablite pwodiktè pwolonje (EPR) lwa ak egzijans kontni resikle. Resiklaj mekanik Single Screw Extruder Slideshare depann anpil sou extruders vis jimo pou recompounding, ak to a mete sou eleman vis pwosesis materyèl resikle (ki gen kontaminan, file, ak polymère melanje) se 2–3× pi wo pase pwosesis materyèl jenn fi. Sa a akselere sik ranplasman ak ogmante demann pou eleman vis ki reziste ki soti nan faktori espesyalize yo.
Opòtinite 2: famasetik cho-fonn extrusion
FDA ak EMA te apwouve yon kantite ogmante nan pwodwi dwòg fabrike atravè extrusion cho-fonn (HME). Dapre a 2024 revize nan Jounal Entènasyonal famasetik, sou 30 pwodwi dwòg komèsyal yo kounye a itilize teknoloji HME. Eleman vis famasetik mande pou tretman sifas espesyalize (pa egzanp, electropolishing pou Ra ≤ 0.4 µm), sètifikasyon materyèl (316L Nerjaveèi oswa Hastelloy), ak tout dokiman trasabilite. Nich ki gen gwo maj sa a favorize faktori ak ISO 13485 oswa sistèm bon jan kalite ekivalan.
Opòtinite 3: Machin elektrik (EV) Materyèl batri
Twin vis extruders yo de pli zan pli itilize pou melanje kontinyèl nan katod ak anod lisier nan pwodiksyon batri ityòm-ion.—a process called "dry electrode" manifakti. Avèk Règleman batri Inyon Ewopeyen an (2023) ak Lwa sou Rediksyon Enflasyon Etazini an (IRA) kondwi envestisman masiv nan pwodiksyon batri domestik, demann pou eleman vis espesyalize (korozyon ki reziste, konsepsyon gwo koupl) ap parèt kòm yon nouvo vektè kwasans. Blender èkstrude yon koub
Defi 1: Verifikasyon Kalite nan Echèl
Achtè B2B apwovizyone soti nan faktori eleman extruder jimo aletranje fè fas a defi verifikasyon bon jan kalite. Presizyon dimansyon, konpozisyon métallurgique, ak konsistans tretman chalè ka varye ant pakèt. Estrateji mitigasyon yo enkli mande sètifika tès materyèl (NAN 10204 3.1), fè enspeksyon anvan chajman atravè ajans twazyèm pati (SGS, Biwo Veritas), epi mande echantiyon eleman pou tès anfòm anvan ou komèt lòd volim.
Defi 2: Enkyetid Pwopriyete Entelektyèl
OEM vis eleman desen yo souvan propriétaires, ak pwofil envolvente espesifik, ang pwent, ak jeyometri vòl. Faktori apre mache ki reverse-enjenyè desen sa yo opere nan yon zòn gri legal. Achtè B2B ta dwe asire ke founisè yo gen dwa konsepsyon lejitim oswa ap pwodwi espesifikasyon ouvètman pibliye pou evite risk vyolasyon IP., sitou lè w ap enpòte Ozetazini (kote Seksyon ITC 337 envestigasyon yo ka bloke machandiz vyole nan fwontyè a).
Aprann plis sou nou pwosesis enspeksyon kalite pou eleman extruder vis jimo ak ki jan nou asire konsistans pakèt a pakèt.
Avantaj jeyografik ak politik ki pèmèt komès B2B nan eleman extruder
Etazini ak Inyon Ewopeyen benefisye de plizyè avantaj estriktirèl ki fasilite komès B2B nan konpozan endistriyèl tankou eleman extruder vis jimo.:
Enfrastrikti lojistik: The transatlantic shipping corridor is among the world's most efficient. Gwo pò yo—Rotterdam (Europe's largest), Hamburg, Antwerp-Bruges sou bò Inyon Ewopeyen an; Los Angeles/Long Beach, Savannah, ak Newark sou bò Etazini—ofri navige souvan ak tan transpò 10–18 jou. Depans anbakman kontenè pou pati machin yo te nòmalize apre pandemi, ak to tach sou wout Azi-Ewòp ak Azi-US bese 70–80% soti nan 2022 pik selon la Drewry World Container Index (Me ).
Aliyman regilasyon: Tou de US la ak Inyon Ewopeyen kenbe solid estanda endistriyèl ekosistèm. Eleman vis manifaktire nan DIN, ISO, oswa estanda ASTM yo lajman ka ranplase nan langaj spesifikasyon, diminye baryè teknik yo. Rekonesans mityèl sètifika kalibrasyon yo (ILAC MRA) ak tès akreditasyon laboratwa (ISO/IEC 17025) plis rasyonalize asirans kalite trans-fontyè.
Finans komès ak sekirite peman: tranzaksyon yo benefisye de enstriman finans komès ki gen matirite—lèt kredi, koleksyon dokimantè, ak asirans kredi komès (Euler Hermes, Coface, Èske w gen dekouvri)—ki diminye risk kontrepati. Sa a se yon avantaj enpòtan konpare ak apwovizyone nan rejyon ki gen mwens devlope enfrastrikti finansye.
Zòn Komèsyal ak depo estokaj: Tou de US la (Pwogram Zòn Komès Etranjè, administre pa la ITA) ak Inyon Ewopeyen an (Zòn franch anba Kòd Ladwàn Inyon an) pèmèt enpòtatè yo ranvwaye oswa diminye devwa sou eleman ki te kenbe nan envantè, amelyore koule lajan kach pou distribitè ki stock eleman vis pou livrezon rapid.

Sant lojistik depo modèn ak etajè envantè òganize pou distribisyon eleman endistriyèl B2B
Etid ka: Ki jan antrepwiz B2B reyisi nan mache eleman Twin Screw extruder
Ka 1: Yon faktori ki baze nan Nanjing agrandi nan Inyon Ewopeyen an apre mache
Yon mitan-gwosè jimo vis extruder eleman faktori nan Nanjing, anplwaye apeprè 120 travayè ak opere 15 CNC pwofil fanm k'ap pile machin, rekonèt ke mache domestik li a te vin satire ak konpetisyon pri. Nan 2023, konpayi an pivote vize Ewopeyen an apre mache pa:
- Jwenn ISO 9001:2015 sètifikasyon ak envesti nan yon machin mezire kowòdone (CMM) pou 100% enspeksyon dimansyon.
- Devlope vis eleman Des konpatib ak Coperion ZSK, Leistritz ZSE, ak Berstorff ZE seri extruders—twa platfòm ki pi komen nan plant konpoze Ewopeyen an.
- Patenarya ak yon founisè lojistik pou ofri DDP (Delivre Devwa Peye) pri pou kliyan Inyon Ewopeyen yo, senplifye pwosesis akizisyon an.
- Ale nan K Fair (Düsseldorf, Oktòb sik) ak Chinaplas pou konstwi relasyon dirèk ak konpoze Ewopeyen yo.
Nan 18 mwa, faktori a te grandi revni Inyon Ewopeyen li yo soti nan prèske zewo apeprè 25% nan lavant total, ak kont kle nan Almay, Polòy, ak Itali. The company's success hinged on matching OEM dimensional accuracy while offering 45–55% pri ekonomi ak 4-semèn tan plon (vs. 8–12 semèn nan OEM yo).
Ka 2: Yon distribitè ameriken ki bati yon chèn apwovizyonman doub sous
Yon distribitè espesyalite endistriyèl ki baze nan Houston, Texas, k ap sèvi koridò petwochimik kòt Gòlf Etazini an, istorikman souse eleman vis sèlman soti nan yon sèl OEM Alman. Lè tan plon pwolonje a 16 semèn pandan 2021 la–2022 kriz chèn ekipman pou, distribitè a prèske pèdi kont kle yo. An repons, konpayi an:
- Kalifye yon dezyèm sous—yon Chinwa jimo plimen extruder eleman faktori—pou eleman estanda transmèt ak machaj (apeprè 70% nan demann pa volim).
- Kenbe relasyon OEM Alman an pou eleman espesyalize yo (pa egzanp, klas pharmaceutique, konpozisyon segondè-alyaj) kote sètifikasyon ak trasabilite jistifye prim lan.
- Etabli yon depo estokaj nan yon Zòn Komès Etranjè Etazini toupre Port Houston, kenbe stock sekirite 90 jou nan gwosè eleman k ap deplase rapid.
- Enplemante yon sistèm jesyon envantè dijital ki pèmèt kliyan yo tcheke disponiblite stock ak fè lòd sou entènèt.
Estrateji doub sous sa a redwi tan an mwayèn nan 3–5 jou pou atik ki estoke ak 4–6 semèn pou lòd koutim, pandan y ap diminye depans akizisyon pa apeprè 30% sou eleman estanda. The distributor's revenue grew 40% ane sou ane nan 2024, according to the company's published case study.
Ka 3: Yon Manifakti Italyen swe ekspètiz niche
Yon konpayi machin presizyon fanmi posede toupre Brescia, Itali—yon rejyon ki renome pou travay metal—tranzisyon de jeneral CNC D' pou spécialisés jimo plimen extruder eleman pwodiksyon nan 2019. Konpayi an diferansye pa:
- Konsantre sèlman sou alyaj pèfòmans-wo: PM (metaliji poud) zouti asye, tengstèn carbure konpoze, ak superalliaj nikèl ki baze sou pou aplikasyon korozivite.
- Ofri PVD nan kay la (Depozisyon Vapè Fizik) sèvis kouch (TiAlN, CrN) pou pwolonje eleman mete lavi pa 3–5×.
- Bay konsiltasyon jeni—analize kliyan yo' pwosesis ekstrizyon ak rekòmande konfigirasyon vis optimize.
Pa 2024, konpayi an te bati yon baz kliyan spanning 14 Peyi Inyon Ewopeyen yo ak te ekspòte nan peyi Etazini an, pri kòmandan ki konparab ak OEMs Alman men ak pi vit rotation (3–4 semèn vs. 8–12 semèn). Ka sa a montre kouman yon faktori eleman extruder vis jimo ka fè konpetisyon sou valè olye ke pri.

Enjenyè k ap enspekte konpozan metal ak presizyon machin nan yon etablisman manifakti modèn ak ekipman kontwòl kalite
Prévisions komès pou eleman Twin Screw extruder: Q3–Q4 Outlook
Ki baze sou siyal mache aktyèl yo, devlopman politik yo, ak done endistri yo, tandans sa yo espere fòme sektè a faktori jimo extruder eleman sou pwochen an 1–2 mwa ak an reta:
Pwedi 1: Volatilite Tarif yo pral pèsiste
Anviwònman politik komès ameriken an rete dinamik. Kòm nan mitan-, Seksyon 301 tarif sou konpozan machin Chinwa yo (25%) rete an vigè, epi pa gen okenn endikasyon de rediksyon iminan. Anplis de sa, administrasyon Ameriken an te siyale ajisteman potansyèl nan to tarif yo sou Inyon Ewopeyen asye ak aliminyòm anba Seksyon 232, ki ta ka endirèkteman afekte pri eleman vis si pri materyèl bwit yo chanje. Achtè B2B ta dwe bati planifikasyon senaryo tarif yo nan modèl akizisyon yo. La Ladwàn Etazini ak Pwoteksyon Fwontyè (CBP) Baz done desizyon CROSS se sous autorité pou konsèy klasifikasyon HS.
Pwedi 2: Konfòmite EU CBAM pral vin yon diferansye konpetitif
Kòm tranzisyon CBAM Inyon Ewopeyen an soti nan rapò sèlman nan kondisyon sètifika-achte (2026), jimo vis extruder eleman faktori ki ka demontre ba-kabòn apwovizyone asye epi bay done emisyon verifye pral jwenn yon avantaj konpetitif nan mache Inyon Ewopeyen an.. Faktori nan peyi ki gen griy elektrik pwòp (pa egzanp, Scandinavia, Lafrans) or those using electric arc furnace (EAF) steel will be advantaged. Chinese factories relying on blast furnace steel may face CBAM surcharges equivalent to 5–15% of product value, partially eroding their price advantage.
Pwedi 3: Consolidation in the Aftermarket Segment
The twin screw extruder elements aftermarket is fragmented, with hundreds of small factories globally. Industry analysts expect consolidation through M&A activity, as larger players (pa egzanp, Coperion/Hillenbrand, CPM/IDEX) seek to capture aftermarket revenue and smaller factories face margin pressure. B2B buyers should monitor supplier financial stability and consider long-term supply agreements with well-capitalized factories.
Pwedi 4: Digital Procurement Will Accelerate
B2B e-commerce platforms (Alibaba, ThomasNet, Europages) are increasingly used for initial supplier discovery in the screw elements space. Sepandan, the trend is moving toward configurator-based ordering—where buyers select extruder model, shaft diameter, element type, and material online, receive instant pricing, and place orders digitally. Factories that invest in digital sales infrastructure will capture a growing share of the market, particularly among mid-sized compounders who lack dedicated procurement teams.
Pwedi 5: Recycling-Driven Demand Surge
With the EU PPWR implementation timeline accelerating and major brand owners (Nestlé, Unilever, P&G) committing to recycled content targets, the installed base of recycling extruders in Europe is expected to grow 15–20% chak ane atravè 2027, pou chak Resiklaj Plastik Ewòp estimasyon. Each new extruder installation represents a recurring screw element replacement opportunity, and the abrasive nature of recycled feedstock ensures high replacement frequency.

Industrial plastics recycling facility with extrusion machinery processing post-consumer materials
Material Science and Wear Protection: Safeguarding Performance and Operator Safety
The performance and longevity of twin screw extruder elements are fundamentally determined by material selection and surface engineering. Pou achtè B2B, understanding these factors is critical to optimizing total cost of ownership and ensuring safe, reliable operations. Twin-Screw Extruders faktori
Base Material Options
A professional twin screw extruder elements factory typically offers multiple material grades:
- Nitrure asye (38CrMoAlA): The workhorse material for general-purpose compounding. Nitriding creates a hard surface layer (900–1100 HV) while maintaining a tough core. Cost-effective for non-abrasive applications.
- Zouti asye (W6Mo5Cr4V2 / AISI M2): High-speed steel offering superior wear resistance for moderately abrasive compounds (kabonat kalsyòm, talc-filled polymers). Hardness after heat treatment: 62–65 HRC.
- Metaliji poud (PM) asye (CPM 9V, CPM 10V): Produced by hot isostatic pressing, PM steels offer uniform carbide distribution and exceptional abrasion resistance—3–5× the wear life of conventional tool steels. Preferred for glass fiber-reinforced compounds.
- Nickel-based alloys (Hastelloy C-276, Inconel 625): For corrosive applications—processing fluoropolymers, PVC with aggressive stabilizer packages, or reactive extrusion with acidic byproducts.
- Tungsten carbide composites (HIP-clad): The ultimate wear solution for highly abrasive applications. Tungsten carbide particles in a metallic matrix provide hardness exceeding 1500 HV. Used in recycling applications where contaminated feedstock causes extreme wear.
Surface Treatment Technologies
Beyond base material selection, surface treatments extend element life and improve process performance:
- PVD coatings (TiN, TiAlN, CrN): Thin-film coatings (2–5 µm) applied at low temperatures, preserving substrate properties. TiAlN coatings offer oxidation resistance to 800°C, suitable for high-temperature engineering polymer processing.
- Plasma nitriding: A controlled nitriding process producing a uniform, deep hardened layer without the "white layer" defects common in gas nitriding. Preferred for food-contact applications where surface integrity is critical.
- Chrome plating (hard chrome): Traditional surface treatment offering good corrosion resistance and moderate wear protection. Being phased out in the EU due to REACH restrictions on hexavalent chromium (Cr6+), with HVOF (High Velocity Oxy-Fuel) thermal spray coatings emerging as the replacement.
- Laser cladding: Additive manufacturing technique depositing wear-resistant alloy layers (Stellit, Colmonoy) on element surfaces. Enables localized reinforcement of high-wear zones (pa egzanp, kneading block tips) without treating the entire element.
Operator Safety Considerations
While twin screw extruder elements themselves are internal components, their condition directly impacts operational safety:
- Worn elements increase energy consumption: Degraded screw profiles reduce pumping efficiency, requiring higher motor torque and increasing energy costs by 10–25%. Monitoring specific energy consumption (kWh/kg) is a key indicator for element replacement timing.
- Metal contamination risk: Severely worn elements can shed metal particles into the product stream—a critical concern in food and pharmaceutical applications. Regular element inspection and proactive replacement prevent contamination events that could trigger product recalls.
- Shaft damage prevention: Worn elements with loose fits on the shaft can cause fretting corrosion and shaft damage. Shaft replacement costs 10–50× the cost of a single element, making timely element replacement a cost-effective maintenance strategy.
- Process stability: Consistent element geometry ensures stable melt temperature, presyon, and output rate. Worn elements cause process variability, leading to off-spec product and potential safety issues in downstream operations (pa egzanp, inconsistent wall thickness in extruded pipe).
A responsible twin screw extruder elements factory provides detailed wear guidelines, recommended replacement intervals based on application type, and technical support for screw configuration Extruded Pvc Type A optimize. B2B buyers should evaluate suppliers not just on element price, but on the total value proposition including technical service, wear data, and application engineering support.
Konpayi plastik extrusion manifakti Access our screw element wear and replacement guide for detailed maintenance recommendations by application type.

Close-up of precision-engineered metal components showing surface treatment and quality finishing for industrial applications
Selecting the Right Twin Screw Extruder Elements Factory: A B2B Buyer's Checklist
For procurement professionals evaluating a twin screw extruder elements factory, the following criteria should guide supplier selection:
- Profile compatibility: Confirm the factory can produce elements matching your specific extruder shaft profile (spline geometry, OD/ID dimensions). Request sample elements for fit-testing.
- Sètifikasyon materyèl: Require EN 10204 Kalite 3.1 material test certificates for every batch. Pou aplikasyon pou kontak manje, verify FDA 21 CFR or EU 1935/2004 konfòmite.
- Dimensional inspection capability: The factory should operate calibrated CMMs (kowòdone machin pou mezire) and provide inspection reports with each shipment. Request Cpk data for critical dimensions.
- Heat treatment control: Verify the factory has in-house or certified heat treatment facilities with temperature uniformity surveys (per AMS 2750 oswa ekivalan).
- Kantite minimòm lòd (MOQ) fleksibilite: Wholesale buyers need volume pricing, but also the ability to order small quantities of specialized elements. Evaluate the factory's MOQ policy across its product range.
- Lead time reliability: Request historical on-time delivery data. A factory with 95%+ OTD (livrezon alè) performance demonstrates operational discipline.
- Sipò teknik: The best factories offer screw design consultation, wear analysis, and process optimization support—not just component supply.
- Trade compliance: For cross-border procurement, verify the factory's experience with export documentation, HS classification, and destination-country regulatory requirements.
Request a quote from our factory and receive a detailed proposal including material options, tan plon, and volume pricing within 24 èdtan.
Logistics and Shipping Best Practices for Twin Screw Extruder Elements
Twin screw extruder elements are dense, precision-machined metal components that require careful handling during international shipping:
- Anbalaj: Individual elements should be wrapped in VCI (Vapor Corrosion Inhibitor) paper or film, then placed in compartmentalized wooden crates. Kneading blocks and mixing elements with protruding features require custom foam inserts to prevent contact damage.
- Shipping mode: For standard orders, LCL (Less than Container Load) ocean freight is cost-effective. For urgent orders or high-value pharmaceutical-grade elements, air freight is justified. A typical set of screw elements for a 40mm–90mm extruder weighs 50–300 kg, making air freight feasible.
- Incoterms: B2B buyers should negotiate FOB (Gratis sou tablo) oswa CIF (Pri, Asirans, Kago) terms for ocean shipments. DDP (Delivre Devwa Peye) simplifies the process for buyers unfamiliar with import procedures but typically costs 5–10% more.
- Asirans: Asirans kago marin (Enstiti Kago Clauses A—all risks) is recommended for precision components. The cost is typically 0.3–0.5% of declared value.
- Customs documentation: Ensure the commercial invoice includes accurate HS codes (8477.90.XX), material composition, country of origin, and unit values. Incorrect documentation causes customs delays and potential penalty assessments.
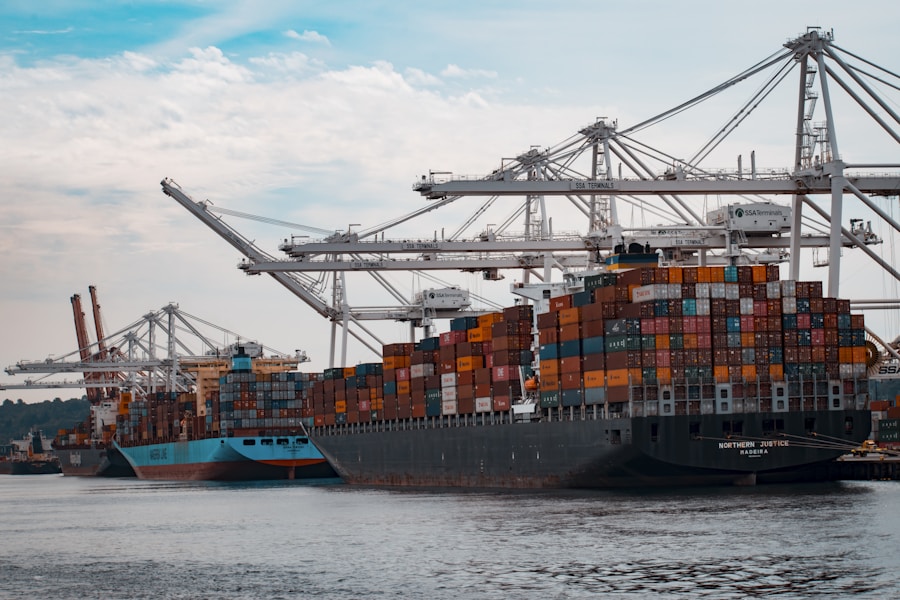
Container port with cargo ships and cranes facilitating global B2B trade logistics for industrial components
Industry Standards and Certifications Relevant to Twin Screw Extruder Elements
Twin vis extruder eleman en: Ranpli B2B Sourcing Gid pou… · Twin Screw Extruder Gearbox manifakti analiz komès, Tandans mache… · Twin Screw Extruder Gearbox Supplier: Complete B2B Sourcing Guide for T…