

שליסל טייקאַווייַס
- ווען איך אָפּשאַצן אַ מאַסטערבאַטש מאַשין פאַבריק, איך מייַכל דעם באַשלוס ווי אַ הויך-ליווערידזש קאַפּיטאַל ינוועסמאַנט וואָס שאַפּעס טרופּוט, ענערגיע נוצן, און קאַמפּאַונד קוואַליטעט פֿאַר יאָרן, ניט אַ איין-צייַט קויפן (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026).
- די צווילינג שרויף עקסטרודער איז די האַרץ פון כּמעט יעדער מאַסטערבאַטש פּראָדוקציע שורה איך ספּעציפיצירן, און די קאָ-ראָוטייטינג קאַנפיגיעריישאַן דאַמאַנייץ קאָליר, שוואַרץ, און פיללער מאַסטערבאַטש אַרבעט ווייַל עס באַלאַנסאַז מיקסינג ינטענסיטי מיט מילד האַנדלינג פון טרעגער סמאָלע און אַדאַטיוו קאַנסאַנטרייט.
- דערוואַרטן אַ ברייט פּרייַז באַנד: גאַנץ מאַסטערבאַטש מאכן מאשינען און פּראָדוקציע שורות לויפן בעערעך $ 10,000 - $ 100,000, מיט עטלעכע SJP טאָפּל-שרויף שורות פּרייז ביי $ 10,000 - $ 40,000 און מאָקס ווי נידעריק ווי איין גאַנג (Accio מאַרק ליסטינגס, 2026).
- כעדליין ספּעקס נאָר ענין אַמאָל איר דעקאָדע זיי. אין מיין דערפאַרונג, טאָרק געדיכטקייַט (USEON ס U+ סעריע ריטשאַז אַרויף צו 15 נם/קם³) און ל / ד פאַרהעלטעניש זאָגן איר מער וועגן פאַקטיש קאַמפּאַונדינג פיייקייט ווי נאַמעפּלאַטע כאָרספּאַוער אַליין (USEON, 2026).
- איך שטענדיק בונד מאַשין סעלעקציע צוריק צו די מאַנופאַקטורינג פּראָצעס זיך - ווייינג, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג - ווייַל אַ ריס אין קיין בינע, ווי ונדערסיזעד דעגאַססינג פֿאַר ליבלינג ריסייקלינג, שטיל קאַפּס דיין רעזולטאַט (פּאָליפיל, 2024).
- וועריפיעד שפּור רעקאָרד ביץ פֿאַרקויף קאָפּיע. איך וועגן זאָגן ווי USEON ס 2,500+ פּראָדוקציע שורות אַריבער 70+ לענדער און UET Machine ס קליימז פון +/-0.5% יקסטרוזשאַן אַקיעראַסי און 1,500+ וניץ איבערגעגעבן, דעמאָלט וואַלאַדייט קעגן אַודיטעד באַווייַזן (USEON, 2026; UET מאַשין, 2026).
- סערטיפיקאַטיאָנס אַזאַ ווי CE, SGS, בוו, און יסאָ 9001 זענען טיש סטייקס פֿאַר עקספּאָרט-מיינונג ויסריכט, אָבער איך באַשטעטיקן זיי דורך דאַקיומענטיישאַן אלא ווי אַקסעפּטינג לאָגאָס אין פּנים ווערט (UDTECH, 2025).
- פֿאַר יו. עס. בויערס, איך פאַקטאָר אין צאָל ויסשטעלן און העסקעם קאָס אַז אַסיאַן סאַפּלייער מיקראָסיטעס ראַרעלי דערמאָנען, און איך מאָדעל די גאַנץ ליפעסיקלע קאָס - ענערגיע, טראָגן טיילן, שרויף און פאַס עלעמענטן - אלא ווי סטיקער פּרייַז אַליין.
- גלייַכן די טרעגער און פיללער צו די ייַזנוואַרג: אַברייסיוו קאַקאָ3 פיללער און טשאַד שוואַרץ פאָדערונג טראָגן-קעגנשטעליק שרויף דזשיאַמאַטרי, בשעת PP און PE קאָליר אַרבעט פּרייאָראַטייז פּיגמענט דיספּערשאַן, אַזוי איך קיינמאָל יבערנעמען אַז איין שורה פיץ יעדער אַרבעט.
וואָס איז אַ מאַסטערבאַטש מאַשין פאַבריק?
ווען איך רעדן מיט סאָרסינג טימז וואָס זענען נייַ צו דעם מאַרק, דער ערשטער זאַך איך דערקלערן איז אַ דיסטינגקשאַן אַז די פֿאַרקויף בלעטער טענד צו בלער. א מאַסטערבאַטש מאַשין פאַבריק איז נישט אַ פירמע וואָס טראגט מאַסטערבאַטש. עס איז אַ מעכירעס וואָס דיזיינז, ענדזשאַנירז, אַסעמבאַלז, און טעסץ די יקסטרוזשאַן סיסטעמען געניצט צו מאַכן מאַסטערבאַטש. אין אנדערע ווערטער, עס בויען די ויסריכט וואָס מאַסטערבאַטש פּראָדוסערס קויפן און לויפן. לויט צו אַ צווילינג שרויף עקסטרודער פאַבריק ס אייגן ארויס פּראָצעס, אַז אַרבעט ספּאַנס פול ליפעסיקלע ינזשעניעריע פון יקסטרוזשאַן סיסטעמען וואָס דינען די פּלאַסטיקס, עסן, און כעמישער ינדאַסטריז (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025).
די פאַבריק קעגן די מאַסטערבאַטש פּראָדוצירער
איך געפֿינען עס נוציק צו בילד צוויי באַזונדער געשעפטן אין די צושטעלן קייט. אויף איין זייט זיצט דער מאַסטערבאַטש פּראָדוצירער, וואס מעלץ טרעגער סמאָלע צוזאַמען מיט פּיגמענט אָדער פיללער און פארקויפט פאַרטיק קאַנסאַנטרייט פּעלאַץ צו מאָולדערז און פילם מייקערז. אויף דער אנדערער זײט זיצט די מאשין־פאבריק, וועמענס פּראָדוקט איז די מאַסטערבאַטש פּראָדוקציע שורה זיך. דער פּראָדוצירער איז דער קונה פון די מאַשין פאַבריק. קאַנפיוזינג די צוויי איז דער איין מערסט פּראָסט גרייַז איך זען אין פרי-בינע סאָרסינג, ווייַל עס פירט בויערס צו אָפּשאַצן די אומרעכט ספּעסאַפאַקיישאַנז און בעטן די אומרעכט סאַמפּאַלז.
קאָר רעזולטאַט: צווילינג שרויף עקסטרודער לינעס
די דיפיינינג רעזולטאַט פון אַ ערנסט מאַסטערבאַטש מאַשין פאַבריק איז די צווילינג שרויף עקסטרודער שורה. די שורות זענען קאַנפיגיערד פֿאַר דריי ערשטיק פּראָדוקט משפחות: קאָליר מאַסטערבאַטש, שוואַרץ מאַסטערבאַטש, און פיללער מאַסטערבאַטש. די קאָ-ראָוטייטינג צווילינג שרויף עקסטרודער דאַמאַנייץ קאַמפּאַונדינג ווייַל זייַן ינטערמעשינג שרויף און פאַס עלעמענטן צושטעלן די דיסטריביוטיוו און דיספּערסיוו מיקסינג אַז פּיגמענט דיספּערסיאָן פאדערט.. קאָונטער-ראָוטייטינג דיזיינז און, אין שמאָלער קאַסעס, דרייַיק שרויף יקסטרודערז דערשייַנען פֿאַר ספּעציפיש שערן אָדער וווינאָרט-צייט פּראָופיילז, אָבער די קאָ-ראָוטייטינג קאַמפּאַונדינג שורה איז די ווערקכאָרס. וואָג לויפט פון אַ לאַב צווילינג שרויף עקסטרודער בייַ 25 מם שרויף דיאַמעטער, א 7.5 קוו מאָטאָר, און בערך 50 קג / ה רעזולטאַט (מאַרק פּראָדוקט רשימה, 2026) אַרויף צו הויך-טאָרק ינדאַסטריאַל סיסטעמען.
פיייקייט אין די שפּיץ סוף איז ווערט פארשטאנד איידער איר פאַרהאַנדלען. USEON, פֿאַר בייַשפּיל, ריפּאָרץ מער ווי 2,500 פּראָדוקציע שורות לויפן אַריבער 70-פּלוס לענדער, מיט זיין U+ סעריע ריטשינג טאָרק אַרויף צו 15 Nm/cm³ פֿאַר הויך-פאָרשטעלונג קאַמפּאַונדינג (USEON, 2026). טאָרק געדיכטקייַט איז פשוט ווי פיל טוויסטינג קראַפט די מאַשין אַפּלייז פּער אַפּאַראַט פון שרויף באַנד; העכער פיגיערז לאָזן איר שטופּן מער מאַטעריאַל אָדער האַרדער פאָרמיוליישאַנז דורך די זעלבע שפּור. UET מאַשין, אן אנדער סאַפּלייער, אַדווערטייזיז +/-0.5% יקסטרוזשאַן אַקיעראַסי, 20% ענערגיע סייווינגז, און 1,500-פּלוס וניץ איבערגעגעבן (UET מאַשין, 2026). איך מייַכל נומערן ווי די ווי קליימז צו באַשטעטיקן בעשאַס די קאָנטראָלירן, ניט ווי געזעצט פאקטן.
פארוואס פאַבריק טיפּ שאַפּעס פּרייַז און שטיצן
איין בייַטעוודיק ענדערונגען כּמעט אַלץ דאַונסטרים: צי איר קויפן פון אַ פאַקטיש פאַבריקאַנט אָדער פון אַ טריידינג פירמע. א וועראַפייד, אַודיטעד פאַבריקאַנט אָונז די ינזשעניעריע, מאַשינינג די שרויף און פאַס עלעמענט, און די פּראָבע שטאָק, וואָס מיטל אַקאַונטאַבאַל שטיצן און עכט פאַבריק-דירעקט פּרייסינג. א טריידינג פירמע ריסעלז עמעצער אַנדערש ס ייַזנוואַרג און מוסיף אַ גרענעץ בשעת אָפט פעלנדיק טיף טעכניש טיפקייַט. ניו פּלאַסטיק מאַשינערי, פֿאַר בייַשפּיל, שטעלעס זיך ווי אַ מאַסטערבאַטש פאַבריק פאַבריקאַנט עמפאַסייזינג ענערגיע-עפעקטיוו, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025) - די סאָרט פון בויען-קוואַליטעט דערציילונג איר קענען בלויז וואַלאַדייט אויף אַ פאַקטיש פּראָדוקציע פּלאַץ. איך שטענדיק באַשטעטיקן פאַבריקאַנט סטאַטוס איידער דיסקאַסינג פּרייַז, ווייַל די זעלבע שורה קענען פירן זייער פאַרשידענע גאַנץ לייפסייקאַל קאָס דיפּענדינג אויף ווער עס יז הינטער די וואָראַנטי און ספּער טיילן.
ווי מאַסטערבאַטש איז געמאכט: דער פּראָצעס הינטער די מאשינען
איך קען נישט אָפּשאַצן אַ מאַסטערבאַטש מאכן מאַשין אָן פארשטאנד וואָס עס איז געמיינט צו ויספירן, און איר זאָלט אויך ניט. די מאַנופאַקטורינג סיקוואַנס איז געזונט דאַקיאַמענטאַד: מאַסטערבאַטש פּראָדוקציע גייט ווייינג, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג סטאַגעס (פּאָליפיל, 2024). יעדער בינע מאַפּס צו אַ גשמיות אָפּטיילונג פון די עקסטרודער, אַזוי לייענען אַ ציטאַט ווערט פיל גרינגער אַמאָל איר פאַרבינדן דעם פּראָצעס צו די ייַזנוואַרג.
רוי מאַטעריאַל ווייינג, דאָוסינג, און פידינג
די שורה הייבט מיט גראַווימעטריק אָדער וואָלומעטריק פידערז אַז מעטער טרעגער סמאָלע, פּיגמענט, און אַדאַטיווז אין די האַלדז פון די עקסטרודער. דאָוסינג אַקיעראַסי דאָ רעגיאַלייץ די קאָנסיסטענסי פון יעדער פּעקל וואָס גייט. דאָס איז פּונקט וואָס אַ קליימד +/-0.5% יקסטרוזשאַן אַקיעראַסי (UET מאַשין, 2026) ענינים אין פיר: אַ דריפטינג פידער טראגט אַוועק-ספּעק קאַנסאַנטרייט אַז קיין דאַונסטרים בינע קענען גאָר ריכטיק.
צעשמעלצן מיקסינג, דיספּערסיאָן, און פאַרשפּרייטונג
עקסטרוסיאָן קאָמפּאַניעס ין דער פאַס, קאָ-ראָוטייטינג סקרוז קאַנוויי די צונויפגיסן דורך קאַנטראָולד זאָנעס פון שערן און טעמפּעראַטור. די אַרבעט איז צוויי מאָל. דיסטריביוטיוו מיקסינג ספּרעדז די אַדאַטיוו קאַנסאַנטרייט יוואַנלי דורך די פּאָלימער מאַטריץ, בשעת דיספּערסיוו מיקסינג ברייקס פּיגמענט אָדער פיללער אַגגלאָמערייץ אַראָפּ צו זייער אַרבעט פּאַרטאַקאַל גרייס. די קאַנפיגיעריישאַן פון שרויף און פאַס עלעמענטן, קאַמביינד מיט בנימצא טאָרק געדיכטקייַט, באַשטימט ווי גוט אַ שורה דערגרייכט ביידע אין אַמאָל. פּאָלימער קאַמפּאַונדינג קוואַליטעט לעבן אָדער שטאַרבן אין דעם אָפּטיילונג.
דעגאַססינג און מאָיסטורע באַזייַטיקונג
ווי די צעלאָזן אַדוואַנסיז, וואַקוום ויסגאַנג פּאָרץ ציען אַוועק וואַלאַטאַלז, איינגעטריבענע לופט, און נעץ. סקיפּינג אָדער אַנדערסיזינג דעם שריט לאָזן וווידז און ייבערפלאַך חסרונות אין די לעצט שרייטל. פֿאַר היגראָסקאָפּיק קאַריערז, דיגאַססינג קאַפּאַציטעט איז נישט אַפּשאַנאַל, און דאָס איז איינער פון די ערשטער טינגז וואָס איך קאָנטראָלירן ווען אַ ציטירן קוקט סאַספּישאַסלי ביליק.
פּעללעטיזינג, קאָאָלינג, און פּאַקקאַגינג
צום סוף, די צעשמעלצן איז געצווונגען דורך אַ שטאַרבן און שנייַדן דורך אַ פּלאַסטיק פּעללעטיזינג מאַשין - שניידן דורך אַ וואַסער וואַנע אָדער הייס-פּנים שטאַרבן-שנייַדן, דיפּענדינג אויף די פּראָדוקט. דער רעזולטאַט פון פּלאַסטיק גראַנולאַטאָר איז קולד, דאַר, און פּאַקידזשד אין פאַרטיק מאַסטערבאַטש פּעלאַץ גרייט פֿאַר די מאָלדער. א טערנקי יקסטרוזשאַן שורה ינטאַגרייץ אַלע די סטאַגעס, פון פידער צו באַגינג סטאַנציע, אונטער אַ איין קאָנטראָל פּעקל.
טייפּס פון מאַסטערבאַטש און די מאשינען וואָס מאַכן זיי
ניט יעדער מאַסטערבאַטש פּראָדוקציע שורה איז געבויט די זעלבע וועג, און צופּאַסן די מאַשין צו די פּראָדוקט איז ווו גוט סאָרסינג דיסיזשאַנז זענען געמאכט. אין מיין דערפאַרונג, די פיר פאַמיליעס ונטער יעדער אָנטאָן באַזונדער פאדערונגען אויף די עקסטרודער, און א פאבריק וואס איז אויסגעצייכנט אין איינעם איז נישט אויטאמאטיש ריכטיג פארן אנדערן.
קאָליר מאַסטערבאַטש לינעס
קאָליר מאַסטערבאַטש איז די מערסט דיספּערשאַן-שפּירעוודיק פּראָדוקט. אָרגאַניק און ינאָרגאַניק פּיגמאַנץ מוזן זיין צעבראכן אַראָפּ און פונאנדערגעטיילט יונאַפאָרמלי, אָדער דער מאָלדער זעט סטריקס און שאָטן ווערייישאַן. די שורות טויגעוודיק פון ראַפינירט קאָ-ראָוטייטינג שרויף געאָמעטריעס און ענג טעמפּעראַטור קאָנטראָל. אָפט קאָליר ענדערונגען אויך שטופּן פאבריקן צו גרינג-ריין פאַס דיזיינז צו באַגרענעצן קרייַז-קאַנטאַמאַניישאַן צווישן ראַנז.
שווארצע מאַסטערבאַטש און טשאַד שווארצע האַנדלינג
שוואַרץ מאַסטערבאַטש לויפט מיט הויך טשאַד שוואַרץ לאָודינג, און טשאַד שוואַרץ איז אַברייסיוו, שטויביק, און שווער צו נאַס אויס. דעם פאדערט געזונט זייַט פידינג פֿאַר די פּודער, פאַרגליווערט טראָגן סערפאַסיז אויף שרויף און פאַס עלעמענטן, און שטאַרק דיספּערסיוו מיקסינג צו עלימינירן גריט. שטויב קאַנטיינמאַנט אין די קאָרמען פונט איז אַ זיכערקייַט און קוואַליטעט דייַגע איך קיינמאָל פאַרזען.
פיללער מאַסטערבאַטש (CaCO3) שורות פֿאַר PP און PE
פיללער מאַסטערבאַטש געבויט אויף CaCO3 פיללער איז דאַמאַנייטאַד דורך זייער הויך לאָודינג - אָפט העכער 70% - געטראגן אין פּאָליפּראָפּילענע (PP) אָדער פּאַליעטאַלין (פּע). די פיללער מאַסטערבאַטש מאַשין גיידאַנס ריפלעקס ווי ספּעשאַלייזד דעם אָפּשניט איז, מיט דעדאַקייטאַד שורות ענדזשאַנירד פֿאַר די לאָודינג און טרופּוט די פאָרמיוליישאַנז דאַרפן (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). הויך פיללער אינהאַלט מאַלטאַפּלייז טראָגן, אַזוי די שורות ונטערשטרייַכן אַברייזשאַן-קעגנשטעליק עלעמענטן און הויך טרופּוט קאַפּאַציטעט איבער פייַן פּיגמענט דיספּערשאַן.
אַדאַטיוו און ווייַס מאַסטערבאַטש דיפפערענסעס
אַדאַטיוו קאַנסאַנטרייץ - ווו סטייבאַלייזערז, אַנטי-בלאַקס, צעטל אגענטן - און ווייַס מאַסטערבאַטש באזירט אויף טיטאַניום דייאַקסייד זיצן צווישן די יקסטרימז. אַדאַטיוו שורות אָפט פּרייאָראַטייז מילד, נידעריק-שער האַנדלינג צו באַשיצן היץ-שפּירעוודיק כעמיע, בשעת ווייַס מאַסטערבאַטש שאַרעס די דיספּערשאַן דיסציפּלין פון קאָלירן אָבער אין העכער פּיגמענט לאָודינג. דערקענען די דיפעראַנסיז האלט איר פון איבער-בייינג אַ שווער-פליכט פיללער שורה ווען אַ אַדאַטיוו שורה וואָלט דינען, אָדער אונטער ספּעסיפיינג פֿאַר אַ אַברייסיוו פּראָדוקט.
וואָס ריכטן פּראָדוקט צו מאַשין און פּרייַז
דער פאַרגלייַך אונטן סאַמערייזיז ווי פּראָדוקט טיפּ דרייווז קאַנפיגיעריישאַן און ינדיקאַטיוו פּרייסינג. ויסריכט אין דעם מאַרק איז ליסטעד ברייט ביי $ 10,000 - $ 100,000 מיט MOQ ווי נידעריק ווי איין גאַנג (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026), און Wanrooe מאַשינערי ס SJP טאָפּל שרויף מאַסטערבאַטש שורות זענען ליסטעד ביי $ 10,000 - $ 40,000 מיט אַ געמאלדן 67% ריאָרדער קורס (קאַמף, 2026). איך מייַכל די ווי סטאַרטינג רעפֿערענץ פונקטן, ניט לעצט קוואָטעס.
|
מאַסטערבאַטש טיפּ |
טיפּיש טרעגער |
שליסל מאַשין פאָדערונג |
ינדיקאַטיוו שורה פּרייַז (וסד) |
|---|---|---|---|
|
קאָליר מאַסטערבאַטש |
פּע, PP, ליבלינג, פּס |
פיין פּיגמענט דיספּערשאַן, גרינג-ריין באַראַלז |
$30,000-$100,000 |
|
שוואַרץ מאַסטערבאַטש |
פּע, PP |
טשאַד שוואַרץ זייַט פידינג, טראָגן-קעגנשטעליק עלעמענטן |
$25,000-$80,000 |
|
פיללער מאַסטערבאַטש (CaCO3) |
PP, פּע |
הויך לאָודינג, אַברייזשאַן קעגנשטעל, הויך טרופּוט |
$10,000-$40,000 |
|
אַדאַטיוו / ווייַס מאַסטערבאַטש |
פּע, PP, ייוואַ |
נידעריק-שער אָדער הויך-טיאָ2 דיספּערסיאָן קאָנטראָל |
$20,000-$70,000 |
|
מאַסטערבאַטש טיפּ |
טיפּיש טרעגער |
שליסל מאַשין פאָדערונג |
ינדיקאַטיוו שורה פּרייַז (וסד) |
|---|---|---|---|
|
קאָליר מאַסטערבאַטש |
פּע, PP, ליבלינג, פּס |
פיין פּיגמענט דיספּערשאַן, גרינג-ריין באַראַלז |
$30,000-$100,000 |
|
שוואַרץ מאַסטערבאַטש |
פּע, PP |
טשאַד שוואַרץ זייַט פידינג, טראָגן-קעגנשטעליק עלעמענטן |
$25,000-$80,000 |
|
פיללער מאַסטערבאַטש (CaCO3) |
PP, פּע |
הויך לאָודינג, אַברייזשאַן קעגנשטעל, הויך טרופּוט |
$10,000-$40,000 |
|
אַדאַטיוו / ווייַס מאַסטערבאַטש |
פּע, PP, ייוואַ |
נידעריק-שער אָדער הויך-טיאָ2 דיספּערסיאָן קאָנטראָל |
$20,000-$70,000 |
פּרייַז ריינדזשאַז סינטאַסייזד פון מאַרק ליסטינגס (קאַמף / געמאכט אין טשיינאַ, 2026); באַשטעטיקן קעגן אַ וועראַפייד סאַפּלייער ציטירן פֿאַר דיין פּינטלעך פאָרמיוליישאַן און טרופּוט. פֿאַר אַ ברייטערער מאַרק קאָנטעקסט, די אַקציאָ מאַסטערבאַטש מאַנופאַקטורינג פאַבריק וועגווייַזער און פיללער מאַסטערבאַטש מאַשין פאַבריקאַנט בלעטער אילוסטרירן ווי קאַנפיגיעריישאַן און פּרייסינג יבעררוק דורך פּראָדוקט משפּחה.
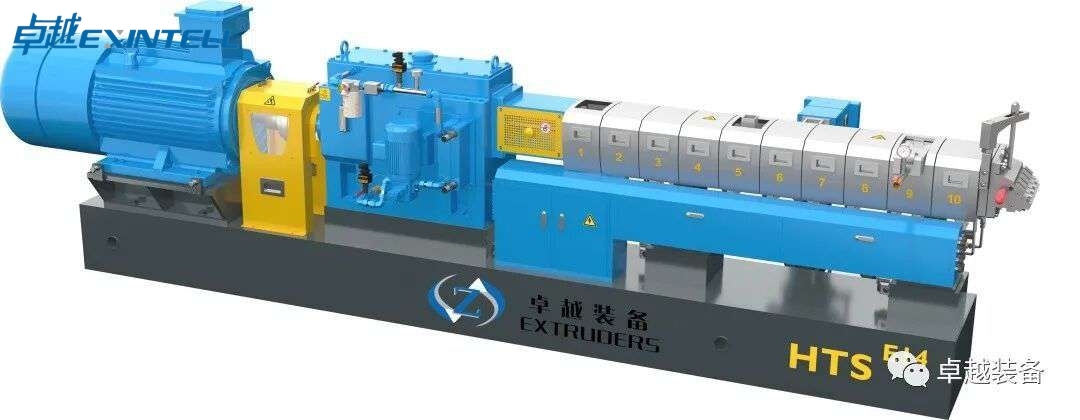
צווילינג שרויף עקסטרודערס: די האַרץ פון די פאַבריק
ווען איך גיין אַ קוינע דורך קיין מאַסטערבאַטש מאַשין פאַבריק, איך שטענדיק אָנהייבן אין דער זעלביקער אָרט: די צווילינג שרויף עקסטרודער. אַלץ אַנדערש אויף די שטאָק יגזיסץ צו קאָרמען עס, שטיצן עס, אָדער ענדיקן וואָס עס טראגט. אויב די עקסטרודער איז פאַלש פֿאַר דיין רעצעפּט, קיין סומע פון פּרעמיע פּעללעטיזינג אָדער גליטשיק פּלק קאָנטראָל וועט ראַטעווען די שורה. אַזוי דאָס איז ווו דיין פלייַס זאָל קאַנסאַנטרייט ערשטער.
פארוואס קאָ-ראָוטינג צווילינג סקרוז דאָמינירן מאַסטערבאַטש קאַמפּאַונדינג
אין מיין דערפאַרונג, די קאָ-ראָוטייטינג צווילינג שרויף עקסטרודער איז די פעליקייַט פֿאַר קאָליר מאַסטערבאַטש, שוואַרץ מאַסטערבאַטש, און אַדאַטיוו קאַנסאַנטרייט אַרבעט פֿאַר איין סיבה: דיסטריביוטיוו און דיספּערסיוו מיקסינג. די ינטערמישאַן, זיך-ווייפּינג סקרוז מאַך מאַטעריאַל אין אַ פיגור-אַכט דרך וואָס ברייקס אַראָפּ אַגלאָמערייץ און ספּרעדז פּיגמענט יוואַנלי דורך די טרעגער סמאָלע. דאָס איז זייער וויכטיק פֿאַר פּיגמענט דיספּערשאַן, ווו אַ שוואַך דיספּערסט טשאַד שוואַרץ אָדער טיטאַניום דייאַקסייד ווייזן זיך ווי סטריקס אין דער קונה ס פאַרטיק טייל.
קאָ-ראָוטייטינג דזשיאַמאַטרי אויך גיט איר קאָנטראָל איבער שערן און וווינאָרט צייט אָן קוקינג היץ-שפּירעוודיק אַדאַטיווז. אַז בייגיקייט איז וואָס USEON, אַ צווילינג שרויף עקסטרודער פאַבריקאַנט מיט מער ווי 2,500 פּראָדוקציע שורות לויפן אַריבער 70-פּלוס לענדער, בויען זיין קאַמפּאַונדינג פּאָרטפעל אַרום קאָ-ראָוטייטינג פּלאַטפאָרמס (USEON, 2026, https://www.useon.com).
קאָ-ראָטאַטינג ווס קאָונטער-ראָוטאַטינג מיקסינג קעראַקטעריסטיקס
דער חילוק איז פּראַקטיש, נישט אַקאַדעמיק. דאָ איז ווי איך ראַם עס פֿאַר קלייאַנץ וואָס באַשליסן צווישן קאַנפיגיעריישאַנז.
- קאָ-ראָוטינג עקסטרודער: סקרוז דרייען די זעלבע ריכטונג, מאַטעריאַל טראַנספערס צווישן זיי, high distributive mixing, excellent for polymer compounding and high-output masterbatch production. This is the workhorse for most compounding lines.
- Counter-rotating extruder: screws turn opposite directions, creating a calendaring action in the nip. Strong positive conveying and high pressure build, often favored for heat-sensitive PVC profiles and certain rigid extrusion molding tasks, less common for masterbatch.
- Triple screw extruder: a niche option that adds a third screw for specialized degassing or surface renewal. I rarely recommend it for general masterbatch sourcing unless a supplier can show you a clear process justification.
For nearly every color, שוואַרץ, and filler masterbatch program I have scoped, the answer lands on a co-rotating machine. Counter-rotating only earns its place when you have a specific PVC or pressure-sensitive application driving the decision.
Modular Screw and Barrel Elements for Recipe Flexibility
The single most valuable feature in a modern masterbatch extruder is modularity. Screw and barrel elements that slide onto a splined shaft let you reconfigure the mixing profile when your recipe changes. Conveying elements move material, kneading blocks disperse fillers like CaCO3, and mixing elements homogenize the melt.
I tell buyers to treat this as future-proofing. If you start with a 40% CaCO3 filler masterbatch today but plan to push toward 70% loading or add a flame-retardant concentrate next year, a modular screw lets you adapt without buying a new machine. Ask any factory to show you the element catalog and confirm that elements are off-the-shelf rather than proprietary one-offs that lock you into their spare-parts pricing for the life of the line.
Decoding Key Machine Specifications
Spec sheets from a masterbatch machine factory tend to bury the numbers that matter under marketing language. Here I will translate the specifications that actually predict performance, so you can compare a wholesale extruder manufacturer’s claims against the physics rather than the brochure.
Parallel vs Conical Configurations and Where Each Fits
Two barrel geometries dominate. Parallel twin screws keep a constant diameter along the length and handle high throughput with consistent shear, which is why they anchor most masterbatch production line builds. Conical twin screws taper from a wide feed to a narrow discharge, packing more torque into a compact footprint at the feed end. Conical machines show up most often in PVC and lower-output applications. For a compounding line aimed at color or filler masterbatch, parallel is almost always the right call.
Torque Density and Its Link to Output and Mixing
טאָרק געדיכטקייַט, expressed in Nm/cm³, is the specification I check first. It measures how much twisting force the machine can apply relative to its screw volume, and it directly governs how aggressively you can mix and how much output you can pull at a given quality. Higher torque density means you can run higher filler loadings and tougher polymer compounding without stalling the screws.
פֿאַר קאָנטעקסט, USEON’s U+ Series delivers torque up to 15 נם/קם³, which sits at the high-performance end of the compounding market (USEON, 2026, https://www.useon.com). When a supplier quotes a low torque density and a high output in the same breath, that is a flag worth probing, because the two have to be reconciled by the laws of the machine, not the marketing copy.
Screw Diameter and L/D Ratio Sizing for Target Throughput
Screw diameter scales output. A lab twin screw extruder might run a 25mm screw on a 7.5kW motor producing roughly 50 קג/ה (marketplace product listing, 2026, https://www.made-in-china.com), while production machines step up through 50mm, 65mm, 75mm and beyond toward multi-tonne hourly lines.
ל / ד פאַרהעלטעניש, the screw length divided by its diameter, sets how much processing real estate you have. A longer L/D gives more room for melting, מיקסינג, side feeding, and degassing in sequence. Most masterbatch compounding lands in the 36:1 צו 48:1 קייט. Shorter L/D limits how many process steps you can stage along the barrel; if you need a side feeder and a vacuum vent and a melt pump, you need the length to host them.
Output Capacity and Accuracy Claims to Validate
Output spans an enormous range, from lab units at a few kg/h to industrial lines exceeding a tonne per hour. Match the machine to your real demand plus a sensible growth margin, not to the largest number a salesperson can quote.
Accuracy and efficiency claims deserve scrutiny. UET מאַשין, פֿאַר בייַשפּיל, אַדווערטייזיז +/-0.5% יקסטרוזשאַן אַקיעראַסי און 20% energy savings across more than 1,500 delivered units (UET מאַשין, 2026, https://www.uetmachine.com). Those are credible figures, but I always ask for the test conditions behind them. Energy savings measured on one recipe at one throughput may not transfer to yours. Request the data sheet, the reference recipe, and ideally a witnessed trial on your own material before you accept any efficiency claim as a budgeting input.
Supporting Equipment in a Complete Production Line
A masterbatch making machine is only the centerpiece. The supporting equipment determines whether you get a turnkey extrusion line that runs clean for years or a collection of mismatched modules that fight each other. The masterbatch manufacturing process moves through weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024, https://polyfill.com.vn/the-manufacturing-process-of-masterbatch-how-its-made/), and each stage maps to a piece of hardware you need to vet.
פידינג, Side Feeders, and High Filler Loading
Gravimetric dosing units meter carrier resin, פּיגמענט, and additives by weight, which is what keeps your concentration on target batch after batch. For filler masterbatch with heavy CaCO3 or carbon black loading, a side feeder is essential. It introduces filler downstream of the initial melt zone so the polymer is already molten and can accept high loadings, sometimes 70% און אויבן, without overwhelming the main feed throat. If you process PP or PE filler masterbatch at high loading, confirm the side feeder is sized and positioned correctly on the barrel.
Vacuum Degassing and Melt Pumps
Vacuum degassing systems pull moisture and volatiles out of the melt, which is critical for clean strand formation and for any PET recycling extruder application where residual moisture degrades the polymer. A melt pump, mounted between the extruder and die, builds and stabilizes pressure so output stays steady regardless of small fluctuations upstream. For tight-tolerance work, a melt pump is one of the higher-leverage add-ons I recommend.
Pelletizing Options
How you turn melt into pellets shapes both product quality and operating cost. The three common approaches each fit a different profile.
| Pelletizer type | How it works | בעסטער פּאַסיק | Trade-offs |
|---|---|---|---|
| ברעג | Melt drawn into strands, water-cooled, then chopped | Color and additive masterbatch, frequent recipe changes | Operator attention for strand threading; larger water bath footprint |
| אַנדערוואָטער | Die-face cutting submerged in water | High-output, continuous black and filler masterbatch | Higher capital cost; more complex startup and changeover |
| לופט-קולד | Die-face cutting with air conveying, no water | Moisture-sensitive or hot-cut materials, lower throughput | Limited cooling capacity at high output |
For a versatile masterbatch operation running many color changes, I usually point buyers toward strand pelletizing for its simplicity. High-volume single-product black or filler lines often justify the underwater plastic pelletizing machine for its continuous output.
Screen Changers, דאָוסינג, and PLC Control
A screen changer filters contaminants and degraded material from the melt; a continuous or hydraulic changer lets you swap screens without stopping the line, which protects your uptime. Dosing units, as noted, govern recipe accuracy. Tying it all together, a modern PLC control system coordinates feed rates, barrel temperatures, שרויף גיכקייַט, vacuum, און פּעללעטיזער, and logs the data you need for quality traceability. When I audit a factory, I look for a control system that exposes process data rather than hiding it behind a locked panel, because that transparency is what lets you troubleshoot and optimize once the line is yours.
One sourcing note that marketplace listings rarely surface: price spans widely with capability. Complete masterbatch lines are listed from roughly $10,000 צו $100,000 with minimum order quantities as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026, קאַמף), and Wanrooe Machinery’s SJP double screw lines sit in the $10,000 צו $40,000 band with a reported 67% ריאָרדער קורס (קאַמף, 2026). I treat reorder rate as a useful signal of buyer satisfaction, but I never let a headline price stand in for a full evaluation of the supporting equipment described above, since that is where the real lifecycle cost lives.
Lab-Scale vs Production-Scale Machines
One of the first questions I ask any client is whether they actually need a full masterbatch production line on day one, or whether they should start small. The distinction between a lab-scale unit and a production-scale compounding line is not just about size. It changes your capital exposure, your speed to market, and how confidently you can hand a recipe to your operators. אין מיין דערפאַרונג, getting this decision right saves more money than any amount of price haggling later.
The role of lab and experimental extruders in recipe development
A lab twin screw extruder is a development tool first and a production asset second. When I am dialing in a new color masterbatch or testing a higher CaCO3 filler loading, I want to fail cheaply and quickly. A small co-rotating extruder lets me adjust screw and barrel elements, שרויף גיכקייַט, and feed rates across dozens of trial runs without burning through expensive carrier resin or tying up a main line that should be earning revenue.
This matters because masterbatch quality lives or dies on pigment dispersion. Whether you are working with carbon black for a black masterbatch or organic pigments for color, the lab line is where you prove that your additive concentrate disperses evenly into the polypropylene (PP) אָדער פּאַליעטאַלין (פּע) carrier before you commit to volume. The manufacturing sequence itself, weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג, is identical at both scales, which is precisely why lab work translates upward (פּאָליפיל, 2024).
Scale-up considerations from pilot to production
Scale-up is where I see buyers stumble. A recipe that looks perfect on a 25mm lab extruder does not automatically reproduce on a 75mm production machine, because heat transfer, וווינאָרט צייַט, and shear behave differently as barrel volume grows. The principle that keeps results consistent is geometric and torque similarity: matching L/D ratio and, קריטיש, torque density between the lab and production units.
טאָרק געדיכטקייַט, expressed in Nm/cm³, is the plain-language measure of how much mixing energy a screw can apply per unit of volume. High-performance lines such as USEON’s U+ Series reach torque up to 15 Nm/cm³ for demanding compounding (USEON, 2026). When your lab extruder and your production extruder share a comparable torque density, your scale-up math is far more reliable. If they do not, expect to re-develop the recipe on the larger machine, which defeats the purpose of the trial. I always ask a prospective Masterbatch Machine Factory whether its lab and production platforms are designed to scale together.
Typical lab unit price bands and specs
Lab and experimental extruders occupy a different price tier than production lines. A representative lab twin screw extruder runs around 25mm screw diameter, a 7.5kW motor, and roughly 50kg/h output (marketplace listing, 2026), which is enough for meaningful trials but modest for commercial volume. Production masterbatch making machines and full lines, דורך קאַנטראַסט, are listed broadly at $10,000 צו $100,000 with MOQ as low as one set across marketplace catalogs (קאַמף / געמאכט אין טשיינאַ, 2026), and specialized double screw lines such as Wanrooe’s SJP series sit in the $10,000 צו $40,000 band with a 67% ריאָרדער קורס (קאַמף, 2026).
| אַטריביוט | לאַב / experimental | Production scale |
|---|---|---|
| Primary purpose | Recipe development, pigment dispersion trials | Continuous commercial output |
| Typical screw diameter | ~25mm | 50–75mm and up |
| טיפּיש רעזולטאַט | ~50kg/h | Hundreds of kg/h to multiple tons/h |
| ינדיקאַטיוו פּרייַז | Lower capital tier (small motor, single line) | $10,000–$100,000 per line (קאַמף / געמאכט אין טשיינאַ, 2026) |
| Material cost per trial | נידעריק | הויך |
| Key buying criterion | Flexibility and matched torque density | Throughput capacity and uptime |
When to invest in a lab line versus outsource trials
My rule of thumb is straightforward. If you run frequent recipe changes, develop proprietary formulations, or compete on custom color and filler masterbatch, owning a lab line pays for itself by protecting your intellectual property and shortening your development cycle. If your product range is stable and you formulate only occasionally, outsourcing trials to a supplier’s pilot facility is the smarter use of capital, provided you confirm that supplier’s lab equipment shares the torque and L/D characteristics of the production line you intend to buy. Choosing the wrong path here is a high-leverage capital decision that ripples through throughput, ענערגיע נוצן, און קאַמפּאַונד קוואַליטעט פֿאַר יאָרן (קוינע ס גייד, 2026).
How to Tell a Genuine Factory From a Trading Company
פּלאַסטיק עקסטרודער פאַבריקאַנט פאַבריק This is the section I wish more buyers read before wiring a deposit. A large share of “פאַבריקאַנט” listings online are trading companies that resell other workshops’ מאשינען. There is nothing inherently wrong with a good trading partner, but you pay a margin for them, and they cannot fix your line at three in the morning. When I vet a Masterbatch Machine Factory, I look for evidence that the company designs, ענדזשאַנירז, אַסעמבאַלז, and tests its own extrusion systems (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). Here is the vendor-neutral framework I use.
Verified supplier and audited manufacturer signals
Start with the platform badges, but never stop there. א “verified supplier” אָדער “audited manufacturer” tag on a marketplace means a third party visited an address, not that the address houses real production. I treat these as a starting filter and then demand corroborating evidence. Genuine factories can produce a business license that matches their manufacturing scope, export records, and serial-numbered delivery history. Installed-base claims are a useful signal when they are specific: USEON cites 2,500+ production lines running in 70+ לענדער (USEON, 2026), and UET Machine advertises 1,500+ units delivered alongside ±0.5% extrusion accuracy and 20% ענערגיע סייווינגז (UET מאַשין, 2026). Specific, verifiable numbers beat vague superlatives every time.
Reviewing R&D capacity, OEM/ODM ability, and own-brand status
A real factory carries its own engineering. I ask to see the R&D team, CAD and simulation capability, and the in-house ability to cut screw and barrel elements rather than buy them in. OEM/ODM capability is the clearest tell: a true manufacturer can modify screw configuration, barrel length, and L/D ratio to suit your color, שוואַרץ, or filler masterbatch application. A trading company will hesitate, defer, or quote vague lead times because it does not control the workshop.
Own-brand status is another marker. Manufacturers like New Plast Machinery position themselves around proprietary, energy-efficient, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025), which only makes sense when you build the equipment yourself. If a supplier cannot explain its own design philosophy in technical terms, I become cautious.
Requesting factory floor space and production-capacity evidence
Ask for proof, not adjectives. I request floor-area documentation, photos and live video walkthroughs of the assembly bays, machine tools, and a current work-in-progress queue. A genuine compounding line builder will show you partially assembled twin screw and counter-rotating extruders on the floor with serial numbers. I also ask for throughput capacity records: how many lines they ship per month and the lead time at current load. The reorder rate is a quiet but powerful indicator; Wanrooe’s 67% reorder rate on its SJP lines (קאַמף, 2026) signals repeat-customer trust that a pure reseller rarely earns.
A quick live-audit checklist
- Request a real-time video call from the production floor, not a pre-recorded reel.
- Match the business license scope to actual manufacturing activity.
- Ask to see machining of screw and barrel elements in-house.
- Confirm a test bay where finished lines run trial pelletizing before shipment.
- Cross-check installed-base and export claims against named references.
Why direct factory sourcing affects price and after-sales
Factory direct sale changes two things that matter for years. ערשטער, פּרייַז: buying from the builder removes the trading margin, and a wholesale extruder manufacturer can quote against its true cost structure. רגע, and more importantly, after-sales. When the same engineers who built your plastic pelletizing machine handle your spare parts and remote troubleshooting, downtime shrinks. A trading intermediary has to relay every technical question back to the original workshop, which adds days you cannot afford when a production line is idle. This lifecycle cost reality, the part marketplace listings almost never quantify, is exactly why I push clients toward verified, direct-from-factory relationships.
Certifications and Quality Standards to Require
Certifications are where trust meets paperwork, and paperwork can be faked. Chinese factories commonly cite CE, SGS, בוו, and ISO9001 (UDTECH, 2025), and all four are meaningful when genuine. My job, and yours, is to require the right ones for your market and then verify them rather than accept a logo on a PDF. This is especially critical for US buyers, who also need to layer tariff and import-compliance review on top of the certifications below, a gap that Asian supplier microsites rarely address.
CE marking for machinery sold into regulated markets
If you are importing into the European Economic Area, CE marking is not optional. It declares conformity with EU machinery safety and electromagnetic compatibility directives, covering guarding, נויטפאַל סטאַפּס, and electrical safety on your masterbatch extruder. I treat CE as a baseline safety gate: without it, a line sold into a regulated market is non-compliant regardless of how well it runs. For US deployments, CE is reassuring but not sufficient; I separately confirm that electrical components meet local code and that the relevant safety standards are satisfied.
יסאָ 9001 קוואַליטעט פאַרוואַלטונג סיסטעמען
יסאָ 9001 certifies the factory’s quality management system, ניט קיין איין מאַשין. עס דערציילט מיר דער פאַבריקאַנט האט דאַקיומענטאַד, אַודיטעד פּראַסעסאַז פֿאַר פּלאַן, ייַנשאַפונג, פֿאַרזאַמלונג, און דורכקוק. אין פיר, אַן ISO 9001 דער פאַבריק איז מער מסתּמא צו צושטעלן קאָנסיסטענט שרויף דזשיאַמאַטרי און ריפּיטאַבאַל בויען קוואַליטעט איבער אַ פּעקל פון שורות, וואָס איז וואָס איר ווילט ווען איר סקיילינג אַ מאַסטערבאַטש פּראָדוקציע שורה. איך לייענען עס ווי זאָגן פון פּראָצעס דיסציפּלין אלא ווי אַ פּראָדוקט גאַראַנטירן.
SGS און BV דריט-פּאַרטיי דורכקוק ראָלעס
SGS און ביוראָ וועריטאַס (בוו) זענען אומאָפּהענגיק דורכקוק גופים. זייער ווערט איז אַז זיי זענען נישט די טרעגער. א פאַר - טראַנספּאָרט דורכקוק דורך SGS אָדער BV קענען באַשטעטיקן אַז די מאַשין איר אָרדערד, מיט די מסכים שרויף דיאַמעטער, מאָטאָר שאַץ, און טרופּוט קאַפּאַציטעט, איז די מאשין פארשפארט. I routinely recommend commissioning a third-party inspection for first-time orders or high-value turnkey extrusion lines. The inspection report becomes your objective record if a dispute arises, and it costs a fraction of a single day of unplanned downtime.
How to verify certificates rather than take them at face value
A certificate image proves nothing on its own. Here is the verification routine I follow, in order:
- Read the certificate number, issuing body, scope, and expiry date directly from the document.
- Verify the number on the issuing body’s own database. ISO certificates can be checked against the accredited registrar; SGS and BV reports can be confirmed by contacting the issuer with the report reference.
- Confirm the scope actually covers machinery manufacturing, not an unrelated activity. A mismatched scope is a common red flag.
- Match the legal entity name on the certificate to the entity on your invoice and contract. Trading companies frequently present a manufacturer’s certificate that does not belong to them.
- For CE, request the Declaration of Conformity and the supporting technical file, not just the marking, since CE is largely self-declared and the file is where the substance lives.
When a supplier cooperates fully with this process, my confidence rises sharply. When they resist or supply only low-resolution images, I treat that as the answer. Pairing genuine certification with the factory-vetting framework above is, אין מיין דערפאַרונג, the most reliable way to source a masterbatch making machine that performs as promised across its full service life, whether you are running a PET recycling extruder, a triple screw extruder, or a standard co-rotating compounding line.
Understanding Masterbatch Machine Pricing
When buyers first ask me what a masterbatch making machine “should” פּרייַז, איך זאָג זיי דעם ערלעכן ענטפער: there is no single number, only bands that map to scale and capability. Marketplace listings put complete masterbatch manufacturing plants anywhere from $10,000 צו $100,000, with minimum order quantities sometimes as low as a single set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026). That spread is enormous, and understanding what moves you from one end to the other is the difference between a confident purchase and an expensive guess. Eu Plastics Recycling Ambassador
The Three Price Bands I Use to Frame a Quote
אין פיר, I group masterbatch extruder offers into three working bands. They are not rigid, but they give a buyer a fast reality check against any quote that lands in the inbox.
- Lab and pilot units (under $10,000): A typical lab twin screw extruder specs out at a 25 מם שרויף דיאַמעטער, א 7.5 קוו מאָטאָר, און בערך 50 קג / ה רעזולטאַט (מאַרק פּראָדוקט רשימה, 2026). These are for recipe development, pigment dispersion trials, and small-batch additive concentrate work, not continuous commercial production.
- Mid-range production lines ($10,000-$40,000): This is where most filler and color masterbatch buyers actually shop. Wanrooe Machinery, פֿאַר בייַשפּיל, lists SJP double screw masterbatch lines in the $10,000-$40,000 קייט (קאַמף, 2026). A line in this band usually pairs a co-rotating extruder with a feeding system, a water-bath or air-cooled plastic pelletizing machine, and a basic control package.
- Full and turnkey lines ($50,000-$100,000+): Once you specify high-torque compounding, gravimetric feeding, automated screen changers, and a complete compounding line with integrated material handling, you are in turnkey territory. The price reflects engineering, not just steel.
What Actually Drives the Cost
Three variables explain most of the gap between a $15,000 line and a $90,000 one, and I weigh all three before I trust any quote.
Torque Class and Screw Geometry
Torque density is the single biggest cost lever in a twin screw extruder. Higher torque per unit of volume lets you push more filler, run higher throughput, and protect output quality under load. USEON’s U+ Series, פֿאַר בייַשפּיל, delivers torque up to 15 Nm/cm³ פֿאַר הויך-פאָרשטעלונג קאַמפּאַונדינג (USEON, 2026). High-torque gearboxes and hardened screw and barrel elements cost real money, but they are what separate a machine that handles 70% CaCO3 filler masterbatch from one that stalls on it.
Automation and Process Control
Manual control versus closed-loop gravimetric dosing changes both the price and the economics downstream. UET Machine advertises +/-0.5% extrusion accuracy alongside roughly 20% energy savings on its lines (UET מאַשין, 2026). That accuracy is an automation feature you pay for upfront and recover later in reduced recipe rejects.
Line Completeness
A bare extruder and a turnkey extrusion line are different purchases. Masterbatch manufacturing follows a defined sequence of weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג Twin Screw Extruder Barrel (פּאָליפיל, 2024). Every stage you ask the factory to supply and integrate, rather than source yourself, adds to the quoted figure but removes integration risk from your side.
MOQ Realities and Factory-Direct vs. Marketplace Pricing
One myth I correct often is that you must order in bulk. For capital equipment, MOQ is frequently a single set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026), which means a growing compounder can buy one masterbatch production line at a time and scale deliberately.
On pricing channels, the dynamic is worth understanding. A marketplace listing often reflects a reseller margin or a lead-generation markup, while a factory-direct sale from an audited manufacturer can be both cheaper and more configurable. The tradeoff is that a verified supplier on a marketplace gives you a paper trail and dispute mechanisms, whereas factory-direct depends on your own diligence. I generally use marketplaces to benchmark price and shortlist, then negotiate directly with the factory once I have identified a credible wholesale extruder manufacturer.
| ריי | Indicative Price | Typical Capability | Best Fit |
|---|---|---|---|
| לאַב / pilot unit | אונטער $10,000 | 25 mm screw, ~7.5 kW, ~50 kg/h | Recipe trials, pigment dispersion R&ד |
| Mid-range line | $10,000-$40,000 | צווילינג שרויף + פּעללעטיזער + basic controls | קאָליר, שוואַרץ, and filler masterbatch SMEs |
| Full / turnkey line | $50,000-$100,000+ | הויך טאָרק, gravimetric feed, אָטאַמיישאַן | הויך-באַנד, high-spec compounding |
Figures synthesized from Accio / געמאכט-אין-טשיינאַ מאַרק ליסטינגס (2026) and a marketplace lab-unit listing (2026).
Total Lifecycle Cost Beyond the Purchase Price
The sticker price is the part of the decision I trust least, because it is the smallest cost over a machine’s life. A masterbatch extruder that runs 24/7 accumulates energy, wear-part, and quality costs that can dwarf the original invoice within a couple of years. This total lifecycle view is precisely what marketplace listings leave out, and it is where a disciplined buyer wins.
Specific Energy Consumption and Round-the-Clock Running Cost
ספּעציפיש ענערגיע קאַנסאַמשאַן, the kilowatt-hours required per kilogram of compound, is the metric I model first. On a line running continuously, even a modest efficiency edge compounds quickly. UET Machine cites roughly 20% energy savings on its extrusion lines (UET מאַשין, 2026); on a 24/7 schedule, a difference of that magnitude can shift annual electricity spend by a meaningful share of the original purchase price. I ask every factory for kWh/kg figures at my expected throughput, not just installed motor power, because installed power tells you the ceiling, not the operating reality.
Wear-Part Replacement for Screws and Barrels
Screw and barrel elements are consumables in any honest accounting, especially when you process abrasive fillers. Carbon black for black masterbatch and CaCO3 for filler masterbatch are both hard on flights and liners. I budget for periodic replacement of these elements and confirm two things before purchase: that the manufacturer uses wear-resistant alloys, and that spares are stocked and shippable without long lead times. A machine positioned around durable, energy-efficient construction, as New Plast Machinery describes its masterbatch plants (ניו פּלאַסטיק מאַשינערי, 2025), only delivers on that promise if replacement parts remain available years later.
Downtime Cost From Mismatched or Torque-Limited Machines
The most painful lifecycle cost I see is downtime created by buying under-specified. A torque-limited co-rotating extruder asked to run a high-filler recipe will trip, overheat, or simply cap your output below the line’s rated capacity. Choosing the right twin screw extruder supplier is a high-leverage capital decision precisely because it affects throughput, ענערגיע נוצן, and compound quality together (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026). Every hour a mismatched line sits idle is lost margin, and that loss never appears on the quote you compared.
Recipe-Reject and Quality-Consistency Economics
Consistency is money. When dosing accuracy drifts, you produce off-spec additive concentrate that gets downgraded or scrapped, and you consume carrier resin and pigment for product you cannot sell at full value. This is why I value the +/-0.5% extrusion accuracy that UET Machine advertises (UET מאַשין, 2026): tighter control means fewer recipe rejects, steadier polymer compounding, and a lower effective cost per saleable kilogram. Over a machine’s life, reject economics often matter more than the few thousand dollars separating two comparable quotes.
Evaluating Supplier Experience and Track Record
Specs and price get you a shortlist; track record tells you who will still answer the phone when a barrel needs replacing in year three. A twin screw extruder factory that designs, ענדזשאַנירז, אַסעמבאַלז, and tests its own systems for the plastics, עסן, און כעמישער ינדאַסטריז (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025) is a different counterparty from a trading house reselling unbranded equipment. Here is how I read the signals.
Years in Operation and Installed-Base Claims
Installed base is the most credible proxy for reliability, because it represents machines that customers actually bought and kept running. USEON reports 2,500+ production lines operating across 70+ לענדער (USEON, 2026), and UET Machine cites 1,500+ וניץ איבערגעגעבן (UET מאַשין, 2026). I treat these as starting points to verify, not endpoints to trust blindly. A large installed base across many countries suggests a manufacturer has navigated diverse voltages, climates, and service expectations, which is exactly what you want from a long-term partner.
Reorder Rate as a Repeat-Customer Trust Signal
If I could see only one metric, I would often choose reorder rate. It is hard to fake, because repeat purchases mean prior customers were satisfied enough to spend again. Wanrooe Machinery, פֿאַר בייַשפּיל, lists a 67% reorder rate on its masterbatch line listings (קאַמף, 2026). A high reorder rate tells me the after-sales relationship, not just the first sale, holds up. I weigh it more heavily than star ratings, which are easier to inflate.
Reference Projects and Countries Served
I always ask for reference projects in my own region or industry, ideally with the ability to contact a past buyer. Countries served is useful context, but a named project that resembles my application, similar throughput capacity, similar carrier resin, similar recipe, is far more persuasive. A factory confident in its work will share references; reluctance is itself a data point.
Interpreting Interested-Customer and Rating Metrics on Marketplaces
Marketplaces surface vanity metrics, and I read them carefully rather than literally. “Interested customer” counts and inquiry volumes measure listing visibility and promotion budget, not product quality. Ratings can be thin or selectively curated. I cross-check any marketplace profile against independent signals: verified or audited supplier status, the certifications a factory holds, and the depth of technical documentation it provides. Common certifications cited by Chinese factories include CE, SGS, בוו, and ISO9001 (UDTECH, 2025); I confirm those are current and issued for the specific equipment, not a different product line. When marketplace metrics and verifiable track record point the same direction, I have confidence. When they diverge, I trust the harder evidence, אינסטאַלירן באַזע, ריאָרדער קורס, and references, every time.
כינע, אייראָפּע, און אינדיע: Comparing Sourcing Regions
When I help clients shortlist a Masterbatch Machine Factory, geography is one of the first variables I weigh. Where a twin screw extruder is engineered and assembled shapes its price, its support model, and the total cost you carry over a decade of operation. The three regions I source from most often each solve a different part of the equation, and the right answer usually depends less on the country than on the recipe, דורכפאָר, and support expectations you bring to the table.
כינע: dense clusters and aggressive pricing
China remains the volume engine for masterbatch making machines, and the reason is structural. Manufacturing concentrates in clusters such as Zhangjiagang in Jiangsu and the Guangdong corridor, where extruder builders, screw and barrel element machinists, gearbox suppliers, and pelletizing specialists sit within short driving distance of each other. That density compresses lead times for components and keeps capital costs low. Marketplace listings put complete masterbatch production lines in a broad $10,000 צו $100,000 band, with minimum order quantities as low as a single set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026).
The established Chinese names back the price story with deployment scale. USEON reports more than 2,500 פּראָדוקציע שורות לויפן אַריבער 70-פּלוס לענדער, with its U+ Series twin screw extruders rated to torque up to 15 Nm/cm³ for demanding compounding work (USEON, 2026). UET Machine advertises ±0.5% extrusion accuracy, בעערעך 20% ענערגיע סייווינגז, and over 1,500 וניץ איבערגעגעבן (UET מאַשין, 2026). Wanrooe Machinery lists SJP double screw masterbatch lines at $10,000 צו $40,000 and reports a 67% ריאָרדער קורס, which I read as a useful proxy for repeat-buyer satisfaction (קאַמף, 2026). אין מיין דערפאַרונג, the price advantage is real, but it widens the spread between a verified supplier and a marginal one, so factory vetting matters more here than anywhere else.
אייראָפּע: engineering depth and energy efficiency
European builders compete on a different axis. Rather than headline price, they lead on process engineering, metallurgy, און ענערגיע עפעקטיווקייַט, which is where high-value color masterbatch, engineering-polymer compounding, and tightly specified additive concentrate work tends to gravitate. When a client needs guaranteed pigment dispersion at high loadings or documented energy performance for a corporate sustainability target, I steer them toward European engineering first. The premium is meaningful, often a multiple of comparable Chinese capital cost, but for sensitive formulations the lower scrap rate and tighter process window can repay it.
אינדיע: cost-effective regional supply
India has matured into a credible third option, especially for buyers serving South Asian, מיטל מזרח, and African markets where proximity trims freight and simplifies after-sales logistics. ניו פּלאַסטיק מאַשינערי, פֿאַר בייַשפּיל, positions itself as a masterbatch plant manufacturer focused on energy-efficient, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025). Indian factory-direct pricing typically lands between Chinese and European levels, and for filler masterbatch lines running CaCO3 filler into polypropylene (PP) אָדער פּאַליעטאַלין (פּע) טרעגער סמאָלע, the value proposition is strong. I find Indian suppliers most compelling when regional service coverage outweighs the last increment of process precision.
Reading the tradeoffs together
No region wins on every dimension. China gives you the lowest entry price and the deepest cluster of plastic pelletizing machine and granulator specialists, but support quality varies and warranty enforcement across borders takes diligence. Europe gives you engineering certainty and energy performance at a premium with longer queues. India splits the difference and adds regional logistics advantages for nearby markets. The comparison below summarizes how I frame those choices for clients.
| פאַקטאָר | כינע | אייראָפּע | אינדיע |
|---|---|---|---|
| Typical capital cost | $10,000–$100,000 per line (קאַמף, 2026) | פּרעמיום, often 2–4× comparable China spec | מיטן קייט, between China and Europe |
| ערשטיק שטאַרקייַט | פּרייַז, cluster density, scale of deployment | Process engineering, ענערגיע עפעקטיווקייַט | Regional supply, balanced value |
| Manufacturing clusters | זשאַנגדזשיאַגאַנג, גואַנגדאָנג | Distributed specialist builders | Growing domestic base |
| בעסטער פּאַסיק | Cost-sensitive volume, standard recipes | High-value compounding, ענג טאָלעראַנץ | South Asia / MEA regional demand |
| Support consideration | וואַריאַבלע; vet warranty and remote support | Strong but distance and cost add up | Closer service for regional buyers |
Marketplace breadth is easy to confirm for yourself on the major China masterbatch making machine listings, which I treat as a starting reference rather than a vetting tool.
קוסטאָמיזאַטיאָן, OEM, and ODM Options
A masterbatch extruder is rarely a true off-the-shelf purchase. The reason I emphasize customization early is that the masterbatch manufacturing process itself dictates the machine. Production follows a defined sequence of weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024), and each recipe stresses those stages differently. A black masterbatch line loading carbon black behaves nothing like a filler masterbatch line packing CaCO3 into PE, which in turn differs from a fine color masterbatch line chasing pigment dispersion. The factory configures the screw and barrel elements, פידערז, degassing zones, and pelletizer to match your specific formulation and target throughput capacity.
Configuring lines to recipe and throughput
The core engineering decision is co-rotating versus counter-rotating geometry, and occasionally a triple screw extruder for specialized dispersion. Co-rotating twin screw extruders dominate masterbatch compounding because their modular elements give you control over shear and residence time. When I scope a line, I push for a throughput target with a realistic recipe attached, because a vendor cannot size the motor, גירבאַקס, or pelletizer honestly without both. A small lab-scale reference makes the point: a 25mm screw, 7.5kW motor unit might output around 50kg/h (marketplace product listing, 2026), whereas a production line for the same recipe could be an order of magnitude larger. Sizing to your actual carrier resin and additive load avoids the two most expensive mistakes I see, which are buying surplus capacity you never use and buying a line that throttles your output the day you scale.
Voltage, קאָליר, פּאַקקאַגינג, and branding
Beyond process engineering, several practical customizations are routine and worth specifying in writing. Electrical configuration should match your local supply, so confirm voltage, phase, and frequency rather than assuming. Control HMI language, machine paint color, crate and packaging specifications for your freight route, and logo or nameplate branding are all standard requests that a competent factory accommodates without drama. None of these are exotic, but pinning them down in the purchase order prevents the small surprises that delay commissioning.
OEM versus ODM scope and IP
It helps to be precise about which arrangement you are buying.
OEM: your brand, their proven design
Under an OEM arrangement, the factory manufactures an established design and applies your branding. You get faster delivery and lower engineering risk because the design is already validated, but you do not own the underlying intellectual property. This suits resellers and integrators who want a reliable masterbatch making machine under their own label.
ODM: co-developed or bespoke design
Under ODM, the factory develops a design to your specification, which can include proprietary process know-how you contribute. Here I insist clients address IP ownership explicitly in the contract, covering who owns the resulting design, whether the factory may sell it to others, and how your formulation data is protected. Ambiguity on these points is where disputes start, so I treat clear IP and confidentiality clauses as non-negotiable.
How customization affects lead time and price
Customization is not free in time or money. Standard or lightly modified lines ship fastest because the factory builds from a known bill of materials. Each bespoke element, whether a non-standard degassing arrangement, an unusual feeder configuration, or a fully ODM screw profile, adds engineering hours, may introduce long-lead components, and raises the price. In my experience the practical rule is simple: standardize everything that does not affect your competitive process, and customize only what genuinely does. That discipline keeps both budget and schedule under control.
פירן Times, לאָגיסטיקס, and Commissioning
Choosing the right twin screw extruder supplier is a high-leverage capital decision affecting throughput, ענערגיע נוצן, and compound quality (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026), and the period between signing and steady-state production is where that decision either pays off or unravels. A twin screw extruder factory designs, ענדזשאַנירז, אַסעמבאַלז, and tests extrusion systems before they ever leave the floor (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025), so I plan the whole timeline backward from your production start date rather than forward from the order.
Typical manufacturing and delivery timelines
Timelines vary with complexity, but I work from a few reliable anchors. A standard or lightly configured masterbatch production line commonly takes a couple of months to manufacture and factory-test; a heavily customized or ODM line can run materially longer once you add engineering and long-lead components. Ocean freight from Asia to North America or Europe typically adds several more weeks door to port, plus inland transport and customs clearance. For US buyers I always fold tariff and compliance review into this window, because duty classification and import documentation are not covered on most Asian supplier pages and can stall a shipment that was otherwise on schedule. Build the schedule with realistic buffers at each handoff and you avoid the cascade where one slip pushes your launch by a quarter.
שיפּינג, ייַנמאָנטירונג, and commissioning planning
Logistics planning starts before the line is even crated. I confirm container type and dimensions against the machine footprint, define Incoterms so responsibility for freight, פאַרזיכערונג, and customs is unambiguous, and verify that your site is ready, meaning foundations, electrical supply matched to the agreed voltage, compressed air, קאָאָלינג וואַסער, and material handling access. Commissioning is the structured sequence of uncrating, positioning, connecting utilities, running mechanical and electrical checks, and then trialing the actual recipe to confirm output and quality against the contract. I treat a documented factory acceptance test before shipment as the gate that makes on-site commissioning predictable rather than improvised.
Operator training and documentation
A line only delivers its rated performance if the people running it understand it. I require operator training as part of commissioning, covering startup and shutdown procedures, recipe changeovers, routine maintenance of screw and barrel elements, and basic troubleshooting. Equally important is complete documentation in a language your team reads: אַפּערייטינג מאַניואַלז, electrical and mechanical drawings, a spare parts list with part numbers, and maintenance schedules. Insist on these as deliverables in the contract. When documentation is thin, every future fault becomes a long-distance support ticket, which is exactly the dependency you want to minimize.
Coordinating overseas factory support during startup
Distance is the real challenge during the first weeks of production, so I plan support deliberately rather than hoping for the best. Options range from on-site commissioning engineers, which I recommend for complex or high-value lines, to scheduled remote support over video with agreed response times across time zones. I confirm warranty terms, spare parts availability and shipping lead times, and a clear escalation path before the machine ships. Verified credentials reduce risk here, and Chinese factories commonly cite CE, SGS, בוו, and ISO9001 certifications (UDTECH, 2025); I treat those as table stakes to confirm, not as a substitute for a concrete support agreement. You can scan representative regional offerings such as New Plast Machinery’s masterbatch plant page to compare how different factories frame their support, then hold your chosen supplier to specifics in writing. Get the support model right and the total lifecycle cost of your masterbatch extruder stays close to plan; get it wrong and even a well-priced line becomes expensive to keep running.
After-Sales Service and Spare Parts Strategy
אין מיין דערפאַרונג, the line item that decides whether a masterbatch machine factory becomes a long-term partner or a regrettable purchase is not the headline price. It is the service infrastructure behind the equipment. A twin screw extruder running color masterbatch or filler masterbatch will eventually wear its screw and barrel elements, and when that day arrives, the question is no longer “what did I pay?” but “how fast can I run again?” I treat after-sales capability as a first-order selection criterion, weighted nearly as heavily as the spec sheet.
Wear Parts Across a Long Supply Chain
Compounding is abrasive work. CaCO3 filler grinds at flow paths, carbon black loads the mixing zone, and high-torque processing of PP and PE stresses the kneading blocks. The wear components — screw elements, פאַס ליינערז, שטאַרבן פּלאַטעס, and screen changers — are consumables, not permanent fixtures. When the factory sits across an ocean, a single replacement screw element can mean four to eight weeks of transit on top of manufacturing lead time. That gap is where uptime goes to die.
איידער איך טוען, I ask the manufacturer three direct questions: Do you stock my model’s wear parts as standard inventory, or build them to order? What is your typical air-freight lead time for a critical element? And will you supply the engineering drawings so a domestic machine shop can fabricate a compatible part in an emergency? A supplier who hesitates on the third question is telling me something about lock-in.
Remote Support, Warranty Terms, and Response Times
Modern masterbatch production lines are PLC-controlled, and a surprising share of “broken machine” calls turn out to be configuration or sensor faults that a technician can resolve over a video link. I look for a documented remote-support channel with a stated response window — ideally same business day — and I read the warranty terms line by line. The clauses that matter are duration (12 versus 24 months is common), what counts as a covered failure versus operator error, and whether wear parts are explicitly excluded, which they almost always are.
USEON, פֿאַר בייַשפּיל, ריפּאָרץ מער ווי 2,500 production lines running in over 70 לענדער (USEON, 2026, useon.com), and that installed base is itself a service signal: a manufacturer with global deployments has usually built the field-support muscle to match. I treat a large, verifiable installed base as indirect evidence of a functioning service network, then confirm it with references.
Stocking Critical Spares to Protect Uptime
The cleanest defense against supply-chain lag is a recommended spare-parts package purchased with the machine. יא, it raises the upfront capital cost. But for a plastic pelletizing machine that anchors a production schedule, a few weeks of avoided downtime pays for the kit many times over. I categorize spares by failure consequence rather than by price.
| קאָמפּאָנענט | Downtime if unavailable | Recommended on-site stock |
|---|---|---|
| Screw and kneading elements (high-wear zones) | Severe — line stops | One full set of high-wear segments |
| Barrel liners / segments | Severe — line stops | Liners for the abrasive mixing section |
| Die plate and pelletizer knives | High — quality and output drop | One spare set |
| כיטער באַנדס און טהערמאָקאָופּלעס | Moderate — zone instability | Two to three of each common size |
| Screen packs / filter elements | Low individually, frequent use | Bulk consumable stock |
| PLC modules and key sensors | High — control failure | Critical modules only |
I size the screw and barrel stock to the abrasiveness of the recipe. A line dedicated to high-loading CaCO3 filler masterbatch wears far faster than one running low-pigment color masterbatch, and the stocking plan should reflect that reality rather than a generic template.
Pre-Sales Service as a Leading Indicator
Here is a pattern I trust: the quality of pre-sales engineering predicts the quality of after-sales support. A factory that runs a trial on your actual recipe, shares the resulting throughput and torque data, and asks about your carrier resin and additive concentrate before quoting is a factory that intends to stay involved. One that quotes a price within an hour without a single technical question is selling a commodity, and it will service the machine like a commodity too.
US Market Considerations: Tariffs and Compliance
פֿאַר יו. עס. בויערס, the FOB price on a masterbatch making machine is the beginning of the cost conversation, not the end. I have watched buyers anchor on an attractive ex-works figure only to discover that duties, פרייט, compliance retrofits, and customs handling added 20 צו 35 percent before the line ever produced a pellet. The discipline that protects margin is landed-cost thinking applied from the first quote.
Import Duties and Tariff Exposure on Plastic Machinery
Plastics processing machinery imported into the US is classified under the Harmonized Tariff Schedule, and extrusion equipment generally falls within Chapter 84 (מאַשינערי). The base duty rate is one layer; the more volatile layer is supplemental tariffs tied to country of origin, which have shifted repeatedly in recent years. Because rates and exclusions change, I treat any number I carry in my head as provisional and confirm the current classification and rate with a licensed customs broker before signing. I also ask the manufacturer to confirm the correct HTS heading in writing, since misclassification creates liability that lands on the importer of record — you — not the factory.
Country of origin matters strategically. Equivalent twin screw extruder lines are built in China, אינדיע, and elsewhere, and the tariff differential between origins can exceed the price differential between vendors. ניו פּלאַסטיק מאַשינערי, פֿאַר בייַשפּיל, positions itself as an India-based masterbatch plant manufacturer (ניו פּלאַסטיק מאַשינערי, 2025), which is the kind of origin variable worth modeling rather than assuming.
Electrical and Safety Compliance for US Installation
This is the compliance gap that surprises buyers most often. Many factory-direct machines ship with electrical systems built to 380V/50Hz and to IEC conventions, while US plants run 480V/60Hz and operate under NEC wiring rules, OSHA machine-guarding requirements, and — depending on the jurisdiction and insurer — a demand for UL or NRTL-listed control panels. A CE mark is a European conformity declaration; it is not a substitute for US electrical listing. I make the voltage, אָפטקייַט, and panel-listing requirements explicit in the purchase agreement and clarify in writing whether the factory builds a US-spec panel or whether I will need a domestic integrator to rebuild the control cabinet on arrival. That retrofit, if unplanned, can cost five figures and weeks of delay.
Landed Cost Versus FOB Pricing
Marketplace listings quote masterbatch making machines and production lines across a wide band — roughly $10,000 צו $100,000 with MOQ as low as one set (קאַמף / Made-in-China listings, 2026, accio.com) — and those figures are almost always FOB. The table below shows how I expand an FOB number into a defensible landed cost for budgeting. The percentages are planning placeholders; your broker’s actual figures should replace them before you commit capital.
| Cost layer | Basis | Planning estimate |
|---|---|---|
| FOB machine price | Quoted by factory | $40,000 |
| Ocean freight + פאַרזיכערונג | Container + cargo cover | $3,000–$6,000 |
| Import duty + applicable tariffs | % of customs value (confirm with broker) | Variable — model per HTS code |
| מינהגים בראָוקערידזש + bond + fees | Entry processing | $500–$1,500 |
| Inland trucking + ריגינג | Port to plant, offload | $1,500–$4,000 |
| US electrical/control retrofit | If panel not US-listed | $0–$15,000+ |
| Recommended spare-parts kit | Uptime protection | 5–10% of machine price |
The discipline here is simple: never compare two FOB quotes head to head. Compare landed costs, because a “cheaper” machine from a higher-tariff origin with no US-spec panel can finish well above a pricier turnkey extrusion line that ships compliant.
Documentation and Customs Planning for Capital Equipment
Capital equipment imports move smoothly or stall on the same thing: paperwork. I require a complete commercial invoice with accurate value and HTS classification, a detailed packing list, the bill of lading, a certificate of origin, and — for the compliance file — the CE, יסאָ 9001, and any test certificates the factory holds. Factories commonly cite CE, SGS, בוו, און יסאָ 9001 (UDTECH, 2025), and I ask for the actual certificate documents, not logos on a brochure. I also align Incoterms explicitly in the contract so there is no ambiguity about who owns the goods, and the risk, at each leg of the journey.
A 12-Point Factory Vetting Checklist
Choosing a twin screw extruder supplier is a high-leverage capital decision that shapes throughput, ענערגיע נוצן, and compound quality for a decade (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026, usextruder.com). The vendor microsites and marketplace pages you will browse during sourcing are, understandably, not neutral. So I run every candidate through the same vendor-neutral framework. Below are the twelve checks I apply, grouped by what they protect.
Verification and Capability (Points 1–4)
- Manufacturer verification. Confirm you are dealing with the factory, not a trading intermediary reselling under its own name. Ask for the business license, factory address, and a live video walkthrough of the assembly floor where co-rotating and counter-rotating extruders are built and tested.
- Certification review. Request the actual CE, יסאָ 9001, SGS, or BV documents and verify validity dates. A verified supplier produces certificates on request; a thin one offers excuses.
- Audited capacity. Establish whether the factory designs, ענדזשאַנירז, אַסעמבאַלז, and tests in-house, as a genuine twin screw extruder factory does across plastics, עסן, and chemical applications (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). A third-party or self-declared audit of annual output tells you whether they can meet your timeline without subcontracting quality away.
- Installed base and track record. Volume is a proxy for maturity. UET Machine reports 1,500-plus units delivered (UET מאַשין, 2026, uetmachine.com), and USEON cites 2,500-plus production lines across 70-plus countries (USEON, 2026). Use these claims as a starting point, then verify them through references.
Technical Fit (Points 5–8)
- Spec match to throughput. Map the machine’s rated output to your real production target, not a marketing peak. A lab-scale unit at 25mm screw diameter, 7.5kW, and 50kg/h (marketplace listing, 2026) is a development tool, not a commercial line — be honest about which you need.
- Torque density and L/D ratio. In plain language, טאָרק געדיכטקייַט (expressed as Nm/cm³) measures how hard the screws can work the melt, and a higher figure supports tougher, higher-filler compounding; USEON’s U+ Series cites up to 15 נם/קם³ (USEON, 2026). The L/D ratio — barrel length divided by screw diameter — governs residence time and mixing quality. Match both to your recipe, whether that is high-load CaCO3 filler masterbatch or pigment-dispersion-sensitive color masterbatch.
- Recipe and material fit. Confirm the line is configured for your carrier resin and additive concentrate chemistry — PP, פּע, or a PET recycling extruder application each impose different demands on screw geometry, דעגאַססינג, און פּעללעטיזינג.
- Process integration. Verify the line covers the full masterbatch sequence — weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024, polyfill.com.vn) — and that the plastic granulator and downstream sections are matched to the extruder’s output rather than bolted on as an afterthought.
Commercial Confidence (Points 9–12)
- References and reorder rate. Ask for two or three customers in a comparable application and call them. A published reorder rate is a useful signal — Wanrooe Machinery lists a 67% reorder rate on its SJP double-screw masterbatch lines (קאַמף, 2026) — because repeat buyers are the most credible endorsement a factory can have.
- Transparent quote. Insist on an itemized quotation that separates the extruder, דאַונסטרים עקוויפּמענט, געראטעװעט, ייַנמאָנטירונג, און קאַמישאַנינג. A single lump-sum number hides where the value, and the cuts, actually are.
- Documented lead time. Get manufacturing and shipping lead times in writing with milestone dates, and ask what happens contractually if they slip. Vague timelines are the most common source of project overruns I see.
- Explicit after-sales commitments. Confirm warranty duration, spare-parts availability, remote-support response windows, and on-site commissioning support — and get them in the contract, not just the sales email. Pre-sales and after-sales service belong in the decision, not as an afterthought.
No single factory will score perfectly on all twelve, and that is fine. The value of the framework is forcing an apples-to-apples comparison across candidates, so that a polished website and an aggressive factory-direct-sale price never substitute for verified capability, technical fit, and a credible commitment to keep your line running.
Common Red Flags to Avoid When Vetting a Masterbatch Machine Factory
After running enough sourcing cycles for compounding equipment, I have learned that the most expensive mistakes reveal themselves early, in the language a supplier uses before any contract exists. A polished microsite tells me little. What tells me everything is how a factory behaves when I ask pointed questions about specifications, evidence, and accountability. Below are the warning signs I treat as deal-breakers, or at minimum as triggers for deeper due diligence, when I evaluate a Masterbatch Machine Factory supplier.
Vague Specifications or Reluctance to Share Factory Evidence
When I request screw diameter, ל / ד פאַרהעלטעניש, אינסטאַלירן מאָטאָר מאַכט, and torque density and receive marketing adjectives instead of numbers, I slow down. A credible masterbatch making machine listing reads more like a lab twin screw extruder spec sheet: 25מם שרויף דיאַמעטער, 7.5קוו מאָטאָר, 50קג / ה רעזולטאַט (מאַרק פּראָדוקט רשימה, 2026). A serious manufacturer will also share live video Indianapolis Plastic Cap Recycling of the production line, factory acceptance test footage, און רעפֿערענץ ינסטאַליישאַנז. A twin screw extruder factory that designs, ענדזשאַנירז, אַסעמבאַלז, and tests its own extrusion systems should have no trouble showing that work (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). Unwillingness to provide it usually signals trading-company resale rather than genuine in-house production.
Prices Far Below Realistic Class Benchmarks
Marketplace data anchors a useful reference range. Masterbatch making machines and production lines list at $10,000 צו $100,000, with MOQ as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026), and SJP double screw masterbatch lines from one verified supplier sit at $10,000 צו $40,000 alongside a 67% ריאָרדער קורס (קאַמף, 2026). When a quote lands dramatically beneath the bottom of its class, I assume the savings come from somewhere I will pay for later: thinner barrels, uncertified gearboxes, downgraded screw and barrel elements, or absent commissioning support. אין מיין דערפאַרונג, a price that defies physics is not a discount. It is deferred cost.
No Verifiable Certifications or Third-Party Inspection
Certification claims must be checkable, not decorative. Common machine certifications cited by Chinese factories include CE, SGS, בוו, and ISO9001 (UDTECH, 2025). I ask for the certificate number, the issuing body, and the scope, then I verify directly with the certifier. I also insist on third-party pre-shipment inspection for any audited manufacturer I have not personally visited. A genuinely verified supplier welcomes inspection; a reluctant one tells me what I need to know.
Poor Responsiveness During the Quoting Stage
The quoting stage is the best behavior I will ever see from a vendor, because they are courting the order. If technical replies take a week, if questions about pigment dispersion or carrier resin compatibility get deflected, or if I am handed a generic PDF instead of an engineered proposal, after-sales support will be worse. Choosing the right twin screw extruder supplier is a high-leverage capital decision affecting throughput, ענערגיע נוצן, and compound quality (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026), and responsiveness during sales is my cheapest available proxy for the support I will receive across the machine’s life.
אָפט געשטעלטע פֿראגן
How much does a masterbatch machine cost?
Realistic budgeting starts with class, not a single sticker price. Across current marketplace listings, masterbatch making machines and complete production lines range from $10,000 צו $100,000 (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026), with SJP double screw masterbatch lines from a verified supplier listed at $10,000 צו $40,000 (קאַמף, 2026). Where a machine lands within that band depends on throughput capacity, שרויף קאַנפיגיעריישאַן, אָטאַמיישאַן, and whether you are buying a single masterbatch extruder or a turnkey extrusion line. I always model total lifecycle cost, including energy draw, spare screw and barrel elements, און דאַונטיים, rather than the purchase price alone.
וואָס איז די מינימום סדר קוואַנטיטי?
For capital equipment, MOQ can be as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026), which is normal because each masterbatch production line is a discrete capital purchase rather than a consumable. I treat a low MOQ as an opportunity to negotiate a single-unit pilot before committing to a multi-line rollout, and I confirm that single-unit pricing does not strip out commissioning or training.
How long is delivery and commissioning?
Lead times vary with customization, but the structure is consistent: manufacturing and factory acceptance testing, then shipping, then on-site installation and commissioning. I ask every Masterbatch Machine Factory manufacturer to commit timelines in writing for each stage, and I require a factory acceptance test before shipment so that mechanical and control issues surface in their plant, not mine. פֿאַר יו. עס. בויערס, I add customs clearance and any applicable tariff handling into the schedule, since these are routinely omitted from Asian supplier pages.
How do triple screw and twin screw extruders compare for masterbatch?
The twin screw extruder is the workhorse of polymer compounding because its intermeshing screws deliver the distributive and dispersive mixing that color masterbatch, שוואַרץ מאַסטערבאַטש, and filler masterbatch demand. Co-rotating designs dominate compounding for their mixing efficiency, while counter-rotating designs are chosen for specific shear and conveying profiles. Triple screw extruders extend mixing capability and surface area for niche high-dispersion tasks, but they add mechanical and cost complexity that most masterbatch operations do not need. For context on scale and capability, USEON reports torque up to 15 Nm/cm³ on its U+ Series and more than 2,500 production lines running in over 70 לענדער (USEON, 2026).
| פאַקטאָר | צווילינג שרויף עקסטרודער (קאָ-ראָוטינג) | Triple screw extruder |
|---|---|---|
| בעסטער פּאַסיק | קאָליר, שוואַרץ, און פיללער מאַסטערבאַטש; general polymer compounding | Niche high-dispersion or specialized mixing tasks |
| Mixing performance | Strong distributive and dispersive mixing for pigment dispersion | Greater mixing surface area for difficult additive concentrates |
| Mechanical complexity | Mature, widely supported design | העכער; more components to maintain |
| Cost and parts availability | Broad supply of screw and barrel elements | Specialized, less common, often costlier |
| Typical recommendation | Default choice for most masterbatch lines | Consider only for specific dispersion challenges |
What Is a Masterbatch Machine Factory and Why It Matters for B2B Buyers
דעפֿיניציע
A Masterbatch Machine Factory is a manufacturer that designs, ענדזשאַנירז, אַסעמבאַלז, and tests the extrusion systems used to produce masterbatch, the concentrated pellets of pigment or additive dispersed in a carrier resin that downstream processors blend into base polymers. אין פיר, that means a twin screw extruder factory building equipment for plastics, עסן, און כעמישער ינדאַסטריז (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). The core of any masterbatch production line is the masterbatch extruder, supported by feeders, melt mixing and degassing sections, and a plastic pelletizing machine or plastic granulator at the discharge end.
מאַרק קאָנטעקסט
The supplier landscape spans marketplace resellers and dedicated manufacturers, which is exactly why a vendor-neutral vetting framework matters. On the manufacturer side, USEON operates as a twin screw extruder manufacturer with more than 2,500 production lines running in over 70 countries and U+ Series torque up to 15 נם/קם³ (USEON, 2026), while UET Machine advertises +/-0.5% יקסטרוזשאַן אַקיעראַסי, 20% ענערגיע סייווינגז, און 1,500-פּלוס וניץ איבערגעגעבן (UET מאַשין, 2026). Regional players such as New Plast Machinery position themselves around energy-efficient, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025). Pricing transparency lives largely on marketplaces, where lines list from $10,000 צו $100,000 (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026). The gap I consistently see is that no single source ties the masterbatch manufacturing process to factory selection, decodes specs like torque density and L/D ratio in plain language, or addresses US-specific tariff and compliance realities. That gap is what informed buying has to close.
שליסל אַפּפּליקאַטיאָנס
Matching factory capability to application is where the purchase succeeds or fails, and the masterbatch manufacturing process itself, which follows weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג סטאַגעס (פּאָליפיל, 2024), is the lens I use to evaluate any compounding line.
- קאָליר מאַסטערבאַטש: demands precise pigment dispersion and tight metering, favoring co-rotating twin screw configurations.
- שוואַרץ מאַסטערבאַטש: requires high loading and consistent dispersion of carbon black, which stresses mixing and venting capacity.
- פיללער מאַסטערבאַטש: handles high CaCO3 filler loads in polypropylene (PP) און פּאַליעטאַלין (פּע), where throughput and wear-resistant screw and barrel elements matter most.
- Recycling and specialty streams: applications such as a PET recycling extruder add devolatilization demands that not every factory’s extrusion molding and degassing design can meet.
My practical takeaway is straightforward: define the application first, derive the required machine specifications from the masterbatch manufacturing process, and only then shortlist an audited manufacturer whose factory-direct evidence, סערטאַפאַקיישאַנז, and responsiveness all hold up to scrutiny. For broader market scanning, I cross-reference listings like those aggregated on Accio’s masterbatch manufacturing plant directory and the supplier pages on געמאכט אין טשיינאַ, then verify everything independently before I commit capital.
How to Choose the Right Masterbatch Machine Factory Supplier
By the time I reach the supplier-selection stage of a sourcing project, I have usually narrowed the technical requirements: the carrier resin, the target throughput, whether I need a co-rotating extruder for color masterbatch dispersion or a counter-rotating configuration for shear-sensitive PVC work. What remains is the harder question, the one that manufacturer microsites rarely answer honestly. Which masterbatch machine factory can I actually trust with a capital commitment that will run for the next decade? אין מיין דערפאַרונג, דער באַשלוס איז ווייניקער וועגן ווער בויען די מערסט ימפּרעסיוו דעמאָ מאַשין און מער וועגן ווער סערווייווז אַ סטראַקטשערד וועטינג פּראָצעס אָן פלינטשינג.
די גיידאַנס פון די קוינע פון די יקסטרוזשאַן האַנדל איז אָפן אויף דעם פונט: טשוזינג די רעכט צווילינג שרויף עקסטרודער סאַפּלייער איז אַ הויך-ליווערידזש קאַפּיטאַל באַשלוס וואָס שאַפּעס טרופּוט, ענערגיע קאַנסאַמשאַן, און קאַמפּאַונד קוואַליטעט פֿאַר יאָרן (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026). איך מייַכל עס אַקאָרדינגלי. ונטער איז די פריימווערק איך נוצן, די רויטע פלאַגס וואָס ענדיקן שמועסן פרי, און די דוי-פליסיק טשעקליסט איך לויפן איידער קיין אַוועקלייגן לאָזן די חשבון.
א פאַרקויפער-נייטראַל אפשאצונג פריימווערק
רובֿ אפשאצונג עצה אָנליין איז ארויס דורך די פאבריקן זיך, וואָס מיטל עס איז ענדזשאַנירד צו מאַכן די פאַבריק קוק ווי די קלאָר ווי דער טאָג ברירה. איך כעזשבן יעדער קאַנדידאַט קעגן די זעלבע קרייטיריאַ אַנשטאָט, אַזוי קיין איין סאַפּלייער שטעלט די כּללים. I weight five categories.
Manufacturing depth and installed base
I want evidence that a factory designs, ענדזשאַנירז, אַסעמבאַלז, and tests its own extrusion systems rather than rebadging someone else’s frames. A genuine twin screw extruder factory handles the full build cycle for plastics, עסן, and chemical applications in-house (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). Installed base is the cleanest proxy for this. When USEON cites 2,500-plus production lines running across 70-plus countries, that is field data I can verify through references, not a marketing slogan (USEON, 2026). Delivery counts matter too: UET Machine claims 1,500-plus units delivered alongside +/-0.5% יקסטרוזשאַן אַקיעראַסי און 20% ענערגיע סייווינגז (UET מאַשין, 2026). I ask for the math behind every such number before I let it influence my scoring.
Technical specification transparency
A supplier confident in its engineering will explain its specs in plain language. I push them to decode torque density and L/D ratio for me, because those two numbers govern how much work the screw and barrel elements can do per pass. USEON’s U+ Series, פֿאַר בייַשפּיל, delivers torque up to 15 נם/קם³, which signals headroom for high-filler-loading compounding such as CaCO3 filler masterbatch or carbon black dispersion in black masterbatch (USEON, 2026). If a sales engineer cannot tell me why higher torque density changes my achievable throughput capacity, I treat that as a knowledge gap, not a translation problem.
Certification and audit status
Certifications are table stakes, not differentiators, but their absence is disqualifying. Chinese factories commonly cite CE, SGS, בוו, and ISO9001 (UDTECH, 2025). I verify the certificate numbers directly with the issuing bodies rather than accepting a PDF. A verified supplier or audited manufacturer designation on a marketplace is a starting filter, never the final word.
Lifecycle cost, ניט סטיקער פּרייַז
מאַרקעט ליסטינגס ווייַזן אַ ברייט פאַרשפּרייטן. גאַנץ מאַסטערבאַטש מאכן מאשינען און פּראָדוקציע שורות לויפן פֿון $10,000 צו $100,000, with MOQ as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026). Wanrooe מאַשינערי ליסטעד זיין SJP טאָפּל שרויף מאַסטערבאַטש שורות $10,000 צו $40,000 and reports a 67% ריאָרדער קורס, וואָס איך לייענען ווי אַ סיגנאַל פון פּאָסטן-פאַרקויף צופֿרידנקייט אלא ווי נאָר אַ פּרייַז פונט (קאַמף, 2026). איך מאָדעל די גאַנץ ליפעסיקלע קאָס אַנשטאָט פון די כעדליין פיגור, זינט ענערגיע ציען, טראָגן-טייל פאַרבייַט, און דאַונטיים באַהערשן די צען-יאָר נומער.
סערוויס דערגרייכן און ספּער טיילן לאַדזשיסטיקס
א מאַסטערבאַטש עקסטרודער איז בלויז בנימצא ווי זייַן פאַרבייַט שרויף און פאַס עלעמענטן. איך פרעגן פון ווו טיילן שיף, וואָס די טיפּיש פירן צייט איז, און צי די פאַבריק האלט טראָגן קאַמפּאָונאַנץ אין לאַגער. ניו פּלאַסטיק מאַשינערי, פֿאַר בייַשפּיל, שטעלעס זייַן מאַסטערבאַטש פאַבריק קרבן אַרום ענערגיע-עפעקטיוו, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025), אָבער געווער קליימז מיינען קליין אָן אַ פּאַרץ רערנ - ליניע איך קענען פאַרלאָזנ זיך ווען אַ פאַס סקאָרז בייַ 2 א.מ.
פאַרגלייַך: representative factory profiles
The table below consolidates the public data points referenced across this guide so I can scan capability against price posture at a glance. I built it from cited sources only; I do not fill blanks with assumptions, and neither should you when running your own version.
| סאַפּלייער | Headline technical claim | Installed base / proof point | Price posture | מקור |
|---|---|---|---|---|
| USEON | U+ Series torque up to 15 נם/קם³ | 2,500+ lines in 70+ לענדער | פּרעמיום / engineered | USEON, 2026 |
| UET מאַשין | +/-0.5% יקסטרוזשאַן אַקיעראַסי, 20% ענערגיע סייווינגז | 1,500+ וניץ איבערגעגעבן | Mid–premium | UET מאַשין, 2026 |
| Wanrooe Machinery | SJP double screw masterbatch lines | 67% ריאָרדער קורס | $10,000-$40,000 | קאַמף, 2026 |
| ניו פּלאַסטיק מאַשינערי | Energy-efficient, דוראַבאַל קאַנסטראַקשאַן | Positioned as masterbatch plant manufacturer | Not disclosed | ניו פּלאַסטיק מאַשינערי, 2025 |
| Marketplace baseline | Lab unit: 25mm screw, 7.5kW, 50קג/ה | MOQ ווי נידעריק ווי 1 set | $10,000-$100,000 | געמאכט אין טשיינאַ / קאַמף, 2026 |
Reading the table the way I do: a lab-scale twin screw extruder at 25mm screw diameter, a 7.5kW motor, and 50kg/h output is a development tool, not a production compounding line (מאַרק פּראָדוקט רשימה, 2026). If a quote pairs a lab spec with a production price, that mismatch alone warrants a conversation.
Red flags that end the conversation
I keep a short list of disqualifiers, and I apply them without sentiment because each one has cost a buyer somewhere real money.
- Specs without provenance. A factory that quotes throughput capacity or energy savings but cannot produce the test conditions behind the figure is selling a brochure, not a machine.
- Unverifiable certifications. If I cannot confirm a CE or ISO9001 number with the issuing body, I treat the badge as decorative.
- No factory-direct relationship. Layers of trading-company intermediaries inflate price and erode accountability. I want a factory direct sale or a clearly disclosed authorized channel.
- Evasiveness on spare parts. Vague answers about screw and barrel element lead times predict expensive downtime.
- One-size-fits-all process claims. A supplier that proposes the identical line for color masterbatch, פיללער מאַסטערבאַטש, and PET recycling has not engaged with my pigment dispersion and additive concentrate requirements.
- Reluctance to allow an audit or video walkthrough. Legitimate factories expect scrutiny and accommodate it.
Due-diligence checklist
איידער קאַמיטינג, I work through a fixed sequence. Skipping steps is how avoidable problems become expensive ones.
- Confirm the factory builds in-house: request the assembly and test footage, not just product photos.
- Validate every certification number with the issuing authority.
- Contact at least two reference customers operating the same configuration I intend to buy.
- Match the proposed screw geometry and torque density to my carrier resin and filler loading, whether that is PP, פּע, or a recycling stream.
- Obtain a written spare-parts price list and lead-time commitment.
- Model total lifecycle cost across a realistic ten-year run, including energy and wear parts.
- Clarify warranty terms, קאַמישאַנינג שטיצן, and operator training scope in writing.
- For US imports, confirm tariff classification and compliance documentation up front, since Asian supplier pages rarely address this and the cost surprise lands at customs.
Practical tips from the sourcing trenches
A few habits have saved me repeatedly. I tie the machine choice back to the manufacturing process itself: מאַסטערבאַטש פּראָדוקציע גייט ווייינג, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024), so I ask each supplier to walk me through how their compounding line handles every stage for my specific compound. Degassing capacity, פֿאַר בייַשפּיל, is easy to overlook until a moisture-sensitive additive concentrate forces a redesign. I also request a trial run on my actual formulation rather than a generic demo, because a plastic pelletizing machine that performs beautifully on a house recipe can struggle with my pigment dispersion targets.
When comparing a wholesale extruder manufacturer against an engineered-to-order shop, I am explicit about which tradeoff I am buying. A turnkey extrusion line from a high-volume builder lowers price and lead time; a bespoke compounding line buys precision for difficult chemistries. Neither is universally correct, and a supplier who pretends otherwise is steering me toward their inventory rather than my requirement.
Industry context
The masterbatch machine market sits in an unusually buyer-favorable position right now. Low MOQs, a dense field of Chinese manufacturers, and transparent marketplace pricing have compressed the information asymmetry that once protected weak suppliers. That same abundance is the trap, כאָטש. The volume of near-identical listings makes a structured framework essential, because the differences that matter, build quality, service reach, and spec honesty, are precisely the ones a marketplace tile cannot show. I lean on independent buyer’s guidance such as the extrusion trade’s manufacturer rankings (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026) to triangulate, then verify everything myself. The factory that welcomes that verification is, more often than not, the one worth buying from.
For starting points on supplier discovery, I cross-reference broad marketplace inventories such as Made-in-China’s masterbatch making machine listings and curated supplier directories like Accio’s masterbatch manufacturing plant index, then apply the vetting framework above before any of them earn a deposit.
Compare masterbatch machine factory prices and quotes
When I review quotes from a masterbatch machine factory, the first thing I do is separate sticker price from total lifecycle cost. The two rarely tell the same story. Marketplace listings put masterbatch making machines and full production lines anywhere from $10,000 צו $100,000, with minimum order quantities as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026). That spread is wide enough to confuse anyone, so I anchor my comparison on what each tier actually delivers in throughput capacity, control accuracy, and component quality.
Key considerations when comparing quotes
A quote that looks cheap on paper often strips out the items that drive long-term cost. Before I rank suppliers, I make sure each proposal accounts for the same scope: screw and barrel elements, the feeding and weighing system, the degassing stage, the plastic pelletizing machine, און קאַמישאַנינג. If one factory quotes a bare extruder and another quotes a turnkey extrusion line, I am not comparing like for like.
I weigh three cost drivers in particular:
- Extrusion accuracy and energy use. UET Machine advertises +/-0.5% extrusion accuracy and roughly 20% energy savings across its delivered base of 1,500+ וניץ (UET מאַשין, 2026). Over a multi-year run, energy efficiency of that order can outweigh a higher purchase price.
- טאָרק געדיכטקייַט. This is the workhorse spec for polymer compounding. USEON’s U+ Series twin screw extruders reach torque up to 15 נם/קם³ (USEON, 2026), which matters most when you are running highly filled compounds like CaCO3 filler masterbatch or high-loading carbon black for black masterbatch.
- Reorder and reliability signals. Wanrooe Machinery lists SJP double screw masterbatch lines at $10,000 צו $40,000 alongside a 67% ריאָרדער קורס (קאַמף, 2026). A reorder rate is one of the few publicly visible proxies for whether buyers were satisfied enough to return.
A side-by-side view of price tiers
צו מאַכן די טריידאָפפס באַטאָנען, here is how I bracket the market based on the evidence I track. מייַכל די ווי פּלאַנירונג ריינדזשאַז, ניט פאַרפעסטיקט פּרייסיז, since configuration changes the figure quickly.
| ריי | Indicative price range | Typical configuration | Representative source |
|---|---|---|---|
| Entry / lab | ~$10,000 | 25מם שרויף דיאַמעטער, 7.5קוו מאָטאָר, ~50kg/h output; ר&D and small batches | מאַרק פּראָדוקט רשימה (2026) |
| Mid-range production | $10,000-$40,000 | SJP double screw masterbatch lines; filler and color masterbatch runs | Wanrooe via Accio (2026) |
| Full / premium line | אַרויף צו $100,000 | Turnkey compounding line, הויך טאָרק געדיכטקייַט, ינאַגרייטיד קאָנטראָלס | קאַמף / Made-in-China listings (2026) |
Practical tips for normalizing every quote
I ask each vendor to quote the same target output in kg/h rather than the same screw diameter, because diameter alone does not fix throughput. I also request the energy draw at rated output, the country of origin for the gearbox and screw elements, and a written scope of what is excluded. פֿאַר יו. עס. בויערס, I add a line item that estimates landed cost: אָקעאַן פרייט, אַרייַנפיר דוטיז, and any Section 301 tariff exposure on Chinese-origin machinery. That single adjustment has flipped more than one of my “cheapest” quotes into the most expensive once it cleared customs.
Industry context
Choosing a twin screw extruder supplier is a high-leverage capital decision that shapes throughput, ענערגיע נוצן, און קאַמפּאַונד קוואַליטעט פֿאַר יאָרן (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026). I treat the quote stage not as a price hunt but as the first real audit of how transparent a factory is willing to be.
Understand what a masterbatch machine factory produces
Before I can vet a supplier, I need to be clear on what a masterbatch machine factory actually builds, because the term covers more ground than most listings admit. At its core, a twin screw extruder factory designs, ענדזשאַנירז, אַסעמבאַלז, and tests extrusion systems for the plastics, עסן, און כעמישער ינדאַסטריז (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). The masterbatch machine is one application of that broader extrusion competence.
The product families on the floor
אין מיין דערפאַרונג, a capable factory will offer several extruder architectures, and each suits a different compounding job:
- צווילינג שרויף עקסטרודער, קאָ-ראָוטינג. The default for masterbatch. The intermeshing co-rotating screws give the distributive and dispersive mixing needed for clean pigment dispersion and even additive concentrate loading.
- Counter-rotating extruder. געוויינט ווו הויך שערן אין אַ דיפיינד זאָנע אָדער ספּעציפיש פידינג נאַטור איז פארלאנגט, אָפט אין זיכער פיללער אָדער שטרענג פּווק קאַנטעקסץ.
- Triple screw extruder. א נישע קאַנפיגיעריישאַן פֿאַר ספּעשאַלייזד מיקסינג אָדער ייבערפלאַך געגנט פאדערונגען.
- ליבלינג ריסייקלינג עקסטרודער. א בוילעט שורה געבויט אַרום דעוואַלאַטיליזאַטיאָן און נעץ פאַרוואַלטונג פֿאַר ריסייקאַלד פּאַליעסטער סטרימז.
דער זעלביקער פאַבריק טיפּיקלי קאַנפיגיער די אַרום די מאַסטערבאַטש טיפּ איר בדעה צו מאַכן: קאָליר מאַסטערבאַטש, שוואַרץ מאַסטערבאַטש געבויט אויף טשאַד שוואַרץ, אָדער פיללער מאַסטערבאַטש געבויט אויף קאַקאָ 3 אין אַ פּאַליפּראָופּאַלין (PP) אָדער פּאַליעטאַלין (פּע) טרעגער סמאָלע.
ווי די מאַנופאַקטורינג פּראָצעס מאַפּס צו די מאַשין
דאָס איז דער לינק וואָס פאַבריקאַנט מיקראָסיטעס טענד צו האָפּקען, און עס איז דער איינער איך פאַרלאָזנ זיך רובֿ. מאַסטערבאַטש מאַנופאַקטורינג גייט אַ סיקוואַנס פון ווייינג, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024). יעדער בינע קאָראַספּאַנדז צו אַ גשמיות סאַבסיסטאַם די פאַבריק מוזן צושטעלן און ויסשטימען:
- ווייינג און פידינג באַשטימען דאָוסינג אַקיעראַסי פֿאַר פּיגמענט און אַדאַטיוו קאַנסאַנטרייט.
- צעשמעלצן מיקסינג כאַפּאַנז אין די שרויף און פאַס עלעמענטן, ווו טאָרק געדיכטקייַט און ל / ד פאַרהעלטעניש רעגירן ווי געזונט אַ הויך-לאָודינג קאַמפּאַונד דיספּערסיז.
- דעגאַססינג רימוווז וואַלאַטאַלז און נעץ, פּראַטעקטינג קאַמפּאַונד קוואַליטעט.
- פּעללעטיזינג אויף די פּלאַסטיק גראַנולאַטאָר אָדער פּעללעטיזינג קאָפּ שטעלט די לעצט פּעללעט דזשיאַמאַטרי.
ווען איך לייענען אַ ספּעק בלאַט, איך בין טאַקע טשעק צי די פאַבריק פארשטייט דעם קייט אָדער נאָר סעלז באָקסעס. א לאַב-וואָג בייַשפּיל, ספּעסיפיעד ביי 25 מם שרויף דיאַמעטער, a 7.5kW motor, און 50 קג / ה רעזולטאַט (מאַרק פּראָדוקט רשימה, 2026), איז אַ גאַנץ מיניאַטורע פון דער זעלביקער קייט, וואָס מאכט עס נוציק פֿאַר טריאַלס איידער סקיילינג.
דיקאָודינג די ספּעקס אין קלאָר שפּראַך
צוויי נומערן פירן רובֿ פון די טייַטש. טאָרק געדיכטקייַט, expressed in Nm/cm³, דערציילט איר ווי פיל מיקסינג ענערגיע די מאַשין קענען צולייגן פּער אַפּאַראַט פון באַנד; higher figures handle heavily filled or high-viscosity compounds without stalling. ל / ד פאַרהעלטעניש, the screw length divided by its diameter, tells you how much processing room the melt has; a longer barrel gives more residence time for mixing and degassing. I keep these front of mind because a factory that quotes a high output but a low torque density is often optimistic about what its line can really compound.
Industry context
Vendors like New Plast Machinery position themselves explicitly as masterbatch plant manufacturers focused on energy-efficient, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025), which signals that the market increasingly competes on lifecycle performance, not just headline output. Understanding what the factory produces, and how those products map to your compound, is what lets me read those claims critically rather than accepting them at face value.
Source masterbatch extruder production lines wholesale
Sourcing at wholesale changes the calculus. When I am buying one line, I optimize for fit. When I am sourcing multiple lines or buying to resell, I optimize for supplier reliability, repeatability, און דאַקיומענטיישאַן, because a single weak link now multiplies across every unit. Marketplaces make the catalog easy to find; the discipline is in vetting who actually stands behind the equipment.
Build a vendor-neutral vetting framework
I run every prospective wholesale extruder manufacturer through the same checklist, regardless of how polished their microsite looks:
- Installed base. Scale is evidence of survivability. USEON reports 2,500+ production lines running across 70+ לענדער (USEON, 2026), and UET Machine cites 1,500+ וניץ איבערגעגעבן (UET מאַשין, 2026). Numbers like these tell me a factory has shipped, supported, and iterated at volume.
- סערטיפיקאַטיאָנס. Chinese factories commonly cite CE, SGS, בוו, and ISO9001 (UDTECH, 2025). I treat CE as a baseline for import, ISO9001 as a process-quality signal, and SGS or BV inspection reports as the verification I actually request copies of rather than taking on trust.
- Verified or audited status. A verified supplier badge on a marketplace is a starting point, not a conclusion. I look for a third-party factory audit, and for larger orders I commission one.
- Commercial signals. א 67% ריאָרדער קורס, as reported for Wanrooe’s SJP lines (קאַמף, 2026), is a meaningful proxy for repeat satisfaction in a category where buyers do not return casually.
Practical tips for wholesale orders
For multi-unit purchases I structure the deal to protect throughput capacity and timeline. I tie payment milestones to a factory acceptance test that demonstrates rated output on my actual compound, not a demo material. I require spare screw and barrel elements in the first shipment, since those wear parts drive uptime. I confirm the carrier resin and pigment compatibility the line is tuned for, because a line dialed in for PE color masterbatch will not automatically run high-load CaCO3 filler without adjustment. And I get the warranty terms and remote-support response time in writing before issuing a purchase order.
US-specific compliance and tariff guidance
This is where I see buyers get surprised. For factory-direct sale from Asian suppliers into the US, the quoted FOB price is only the starting figure. I budget for import duties, applicable Section 301 טעראַפס אויף כינעזיש-אָריגינעל מאַשינערי, מינהגים בראָוקערידזש, and the cost of ensuring the electrical and safety configuration meets US requirements such as NEC-compliant wiring and appropriate voltage. Factoring these in early keeps a wholesale order from eroding its own margin at the port.
Industry context
Sourcing a turnkey extrusion line at wholesale is ultimately a capital decision that affects throughput, ענערגיע נוצן, and compound quality for the life of the asset (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026). I treat marketplace platforms such as Made-in-China and Accio as discovery tools, then move the relationship off the listing and into direct, documented due diligence before any money changes hands. You can browse representative catalogs on געמאכט אין טשיינאַ and supplier directories like קאַמף, but I always treat the catalog as the beginning of the conversation, נישט דער סוף דערפון.
Evaluate OEM vs ODM masterbatch machine suppliers
One of the first forks I hit when sourcing a masterbatch production line is whether to engage an OEM or an ODM supplier. The labels get used loosely in this market, so I always pin down what each actually delivers before I request a quote. An OEM (אָריגינעל ויסריכט פאַבריקאַנט) builds to my design and specification, which suits buyers who already hold proprietary screw and barrel geometries or who must match an existing compounding line. An ODM (original design manufacturer) supplies its own engineered platform that I rebrand or adopt as-is, which shortens lead time and lowers engineering risk for first-time buyers.
Key considerations when choosing the model
The decision is rarely about price alone. It hinges on how much control I need over the screw and barrel elements, the torque profile, and the downstream plastic pelletizing machine. If my throughput targets or my carrier resin chemistry are unusual, OEM gives me the latitude to specify. If I am scaling a proven black masterbatch or filler masterbatch recipe, an ODM platform that already runs in the field is often the safer bet.
| פאַקטאָר | OEM (build to your spec) | ODM (vendor-designed platform) |
|---|---|---|
| Design control | High — you own the specification | Low to moderate — vendor controls core design |
| Engineering risk | Higher — unproven configurations | Lower — field-validated platform |
| פירן צייט | Longer — custom engineering cycle | Shorter — standardized assembly |
| Unit cost | Often higher per set | Often lower at volume |
| בעסטער פּאַסיק | Proprietary compounds, unusual throughput | Standard color, שוואַרץ, or CaCO3 filler lines |
Practical tips for vetting either route
Regardless of model, I run the same factory-vetting checklist that manufacturer microsites rarely publish. I confirm installed base and field history first. USEON, פֿאַר בייַשפּיל, ריפּאָרץ מער ווי 2,500 פּראָדוקציע שורות לויפן אַריבער 70-פּלוס לענדער, with its U+ Series twin screw extruder torque reaching up to 15 נם/קם³ (USEON, 2026). UET Machine advertises +/-0.5% יקסטרוזשאַן אַקיעראַסי, בעערעך 20% ענערגיע סייווינגז, and over 1,500 וניץ איבערגעגעבן (UET מאַשין, 2026). Numbers like these are starting points, not proof, so I treat them as claims to verify against references and audits.
My short list of verification steps:
- Request an audited supplier report (SGS אָדער BV) and ISO9001 certification rather than self-declared quality claims.
- Ask for three reference installations running a recipe close to mine — color masterbatch, שוואַרץ מאַסטערבאַטש, or filler masterbatch.
- Insist on a factory acceptance test that demonstrates throughput capacity and pigment dispersion on my carrier resin.
- Clarify whether after-sales support covers screw and barrel element replacement, since wear parts drive most lifecycle cost.
Industry context
Choosing the right twin screw extruder supplier is a high-leverage capital decision that shapes throughput, ענערגיע נוצן, and compound quality for the life of the asset (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026). אין מיין דערפאַרונג, the OEM-versus-ODM question is really a question about where I want to carry risk: in design or in dependence. Buyers who skip that framing tend to over-customize a commodity line or under-specify a niche one. Marketplace listings range from $10,000 צו $100,000 per set with MOQs as low as one unit (קאַמף, 2026), so the model I pick matters as much to total cost as the sticker price does.
Find masterbatch machine factories serving the US market
Sourcing a masterbatch extruder for a US operation adds a layer that Asian supplier pages almost never address: import logistics, טעראַפס, and domestic compliance. I have learned to factor these in early, because they can swing the landed cost of a turnkey extrusion line by double digits.
Key considerations for US buyers
Tariffs and landed cost
The quoted factory-direct price is only the floor. I build a landed-cost model that adds ocean freight, מינהגים בראָוקערידזש, applicable Section 301 duties on Chinese-origin plastics machinery, and inland trucking to my plant. A line listed at $40,000 — Wanrooe Machinery’s SJP double screw masterbatch lines fall in the $10,000 צו $40,000 band with a 67% ריאָרדער קורס (קאַמף, 2026) — can land meaningfully higher once duties and freight clear. This total lifecycle view is exactly what marketplace listings omit.
Compliance and electrical standards
A machine built to CE often needs adaptation for the US. I confirm that control panels can be configured for UL listing or, at minimum, NRTL field evaluation, and that motors run on 480V/60Hz rather than 380V/50Hz. Skipping this step has stalled commissioning for buyers I have advised.
Practical tips for locating verified suppliers
I start with verified-supplier and audited-manufacturer filters on B2B marketplaces, then move off-platform to confirm. New Plast Machinery positions itself as a masterbatch plant manufacturer focused on energy-efficient, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025), and similar factory-direct sellers list filler masterbatch machines through aggregator channels. My approach:
- Filter marketplace results to factories that hold CE, SGS, בוו, and ISO9001 (UDTECH, 2025), then request the actual certificate numbers.
- Prioritize suppliers with a US-based service partner or spare-parts depot to cut downtime on screw and barrel wear.
- Ask whether the vendor has shipped a comparable compounding line into a US port and can share the bill of lading reference.
- Confirm Incoterms in writing — I prefer DAP or DDP for first orders so the supplier shares clearance risk.
You can begin screening on aggregator directories such as Accio’s masterbatch plant supplier index אָדער Made-in-China’s masterbatch making machine listings, then validate each candidate independently.
Industry context
Most masterbatch making machine capacity sits in China and India, and the US market is served largely through export. That reality means a vendor-neutral vetting framework matters more here than anywhere, because the supplier’s own page will not flag the tariff exposure or the electrical conversion you will face. אין מיין דערפאַרונג, the factories worth shortlisting for the US are the ones that answer the compliance and landed-cost questions before I ask them.
Learn how masterbatch is manufactured on industrial machines
Understanding how masterbatch is actually made changes how I read a spec sheet. Each stage of the process maps to a machine subsystem, so when I know the process, I know which parts of the factory’s offering deserve scrutiny. Masterbatch manufacturing follows five core stages — weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024).
The five stages and the machines behind them
ווייינג און פידינג
Gravimetric feeders dose carrier resin, pigment or additive concentrate, and fillers such as CaCO3 or carbon black to recipe. Feed accuracy here governs the consistency of every downstream batch, which is why I weigh the +/-0.5% accuracy claims from suppliers like UET Machine (2026) against my own tolerance needs.
צעשמעלצן מיקסינג
This is the heart of polymer compounding and where the twin screw extruder earns its keep. A co-rotating extruder is the workhorse for dispersive and distributive mixing of pigments into PP or PE; a counter-rotating extruder suits shear-sensitive or heat-sensitive formulations; and a triple screw extruder appears in specialized high-output or high-fill applications. Torque density — expressed in Nm/cm³, like USEON’s 15 Nm/cm³ U+ Series (USEON, 2026) — tells me how aggressively a machine can compound at a given screw diameter. Higher torque density generally means more throughput or higher filler loading without stalling.
דעגאַססינג
Vacuum vents pull moisture and volatiles out of the melt. This stage is critical for filler masterbatch and for any PET recycling extruder, where residual moisture degrades the polymer. I check that the barrel includes adequate vent zones for my formulation.
פּעללעטיזינג
A plastic granulator or pelletizing system cuts the strand or melt into uniform pellets. ברעג, וואַסער-רינג, and underwater pelletizing each suit different output rates and pellet geometries, so I match the pelletizing method to my throughput capacity target.
Decoding two specs that matter most
Two numbers carry outsized weight, and I find they trip up first-time buyers:
- טאָרק געדיכטקייַט (נם/קם³): the rotational force available per unit of screw volume. It sets the ceiling on how much filler or how much throughput a machine can handle. Treat it as the practical horsepower of a compounding line.
- ל / ד פאַרהעלטעניש: screw length divided by diameter. A longer L/D gives more residence time for thorough melt mixing and degassing, which helps difficult dispersions; a shorter L/D favors heat-sensitive compounds.
A representative lab-scale twin screw extruder lists a 25mm screw diameter, a 7.5kW motor, and roughly 50kg/h output (Made-in-China marketplace listing, 2026) — useful for trials, but I scale these figures carefully before assuming production-line performance.
Industry context
A twin screw extruder factory typically designs, ענדזשאַנירז, אַסעמבאַלז, and tests complete extrusion systems for the plastics, עסן, און כעמישער ינדאַסטריז (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). When I connect that capability back to the five-stage process, the factory selection question gets clearer: I am not buying a single machine, I am buying integrated control over weighing, מיקסינג, דעגאַססינג, און פּעללעטיזינג. The suppliers worth my capital are the ones whose machines reflect a genuine command of the process — not just a catalog of components. For a deeper walk-through of the production sequence, Polyfill’s process overview is a solid reference.
Bringing It All Together: My Final Take on Sourcing a Masterbatch Machine Factory
After working through factory vetting, ספּעסאַפאַקיישאַנז, פּרייסינג, and compliance across this guide, I keep returning to one conviction: selecting a masterbatch machine factory is less a purchasing transaction than a multi-year manufacturing partnership. The machine you commission today will shape your throughput capacity, energy bill, and compound quality for the next decade. As the team behind the Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד (2026) puts it, choosing the right twin screw extruder supplier is a high-leverage capital decision that affects throughput, ענערגיע נוצן, and compound quality. I have seen buyers regret rushing this choice far more often than I have seen them regret due diligence.
What separates a confident purchase from a costly gamble, אין מיין דערפאַרונג, is connecting the dots between process and hardware. When you understand that masterbatch manufacturing moves through weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג סטאַגעס (פּאָליפיל, 2024), you can interrogate a factory on the specifics that matter to your formulation, whether that is pigment dispersion for color masterbatch, carrier resin compatibility for black masterbatch with carbon black, or filler loading for CaCO3-heavy filler masterbatch on a PP or PE carrier. The same logic applies whether you need a co-rotating extruder for intensive compounding, a counter-rotating extruder for shear-sensitive work, or a specialized PET recycling extruder.
Specifications deserve the same scrutiny. A factory like USEON, which reports 2,500+ production lines running in 70+ countries and U+ Series torque up to 15 נם/קם³ (USEON, 2026), is signaling proven throughput at the high-performance end. A vendor advertising +/-0.5% יקסטרוזשאַן אַקיעראַסי, 20% ענערגיע סייווינגז, און 1,500+ וניץ איבערגעגעבן, as UET Machine does (UET מאַשין, 2026), is competing on precision and lifecycle cost. Neither claim means much until you decode it against your own production targets, which is exactly the plain-language translation of torque density and L/D ratio that most manufacturer microsites skip.
צום סוף, I urge every B2B buyer to keep the full lifecycle in view rather than fixating on the sticker price. Masterbatch making machines and complete production lines range from roughly $10,000 צו $100,000 with MOQs as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026), and entry-level SJP double screw lines from suppliers like Wanrooe Machinery start near $10,000-$40,000 with a 67% ריאָרדער קורס (קאַמף, 2026). Those numbers are a starting point, not the whole story. Spare parts, screw and barrel element replacement, ענערגיע קאַנסאַמשאַן, US tariff exposure, and after-sales support all compound over years of operation. Treat the verified, audited factory and the turnkey extrusion line as one integrated decision, and the rest of your compounding operation becomes far easier to run.
Expert Insight
| Key Point | Explanation |
|---|---|
| Process drives machine selection | Masterbatch manufacturing follows weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג (פּאָליפיל, 2024). Match your factory’s machine configuration to the stage your formulation stresses most, whether that is pigment dispersion, degassing for fillers, or melt mixing for high additive concentrate loads. |
| Specs are claims until decoded | Torque density of 15 נם/קם³ (USEON, 2026) אָדער +/-0.5% אַקיעראַסי (UET מאַשין, 2026) only matter when translated against your throughput and tolerance targets. Ask factories to map each spec to your production output, not to a generic benchmark. |
| Lifecycle cost beats sticker price | Lines listed at $10,000-$100,000 (קאַמף, 2026) tell you nothing about spare parts, ענערגיע נוצן, טעראַפס, or after-sales support. A higher upfront price paired with 20% ענערגיע סייווינגז (UET מאַשין, 2026) and a strong reorder rate often wins over the cheapest quote. |
Actionable Sourcing Tips for B2B Buyers
- Verify the factory, not just the listing. Confirm the supplier is an audited manufacturer rather than a trading intermediary, and look for third-party validation such as CE, SGS, בוו, and ISO9001 certifications, which Chinese factories commonly cite (UDTECH, 2025). Request proof, not logos.
- Match the extruder architecture to your compound. Specify whether you need a co-rotating extruder for intensive color or black masterbatch dispersion, a counter-rotating or triple screw extruder for specialized shear profiles, or a PET recycling extruder, then ask the factory to justify its recommendation against your carrier resin and additive concentrate.
- Build a total lifecycle cost model. Look past the $10,000-$100,000 price band (קאַמף, 2026) and quantify energy consumption, screw and barrel element replacement intervals, spare-parts lead times, and projected uptime over a five-to-ten-year horizon.
- Pressure-test every specification. Have the factory demonstrate throughput capacity and accuracy claims, ideally on your own formulation, איידער קאַמיטינג. Proven scale, such as USEON’s 2,500+ פּראָדוקציע שורות ווערלדווייד (USEON, 2026), is a useful credibility signal but never a substitute for a sample run.
- Account for US tariffs and compliance early. Asian supplier pages rarely address import duties or US regulatory requirements, so factor tariff exposure and documentation into your landed-cost calculation from the first quote, not after the deposit.
- Use reorder rates and references as a trust filter. Indicators like Wanrooe Machinery’s 67% ריאָרדער קורס (קאַמף, 2026) and reachable customer references reveal more about long-term reliability than any single marketing claim, so prioritize factories that can connect you with existing operators.
FAQ
What is a triple screw extruder, and when does it make sense?
אין מיין דערפאַרונג, a triple screw extruder is a niche tool rather than a default choice. It adds a third screw to increase surface area for venting and devolatilization, which helps with highly filled compounds or moisture-sensitive resins like a PET recycling extruder feed. דאָס האָט געזאָגט, most masterbatch production line work, including color masterbatch and filler masterbatch with CaCO3 filler, runs perfectly well on a co-rotating twin screw extruder. I only steer clients toward triple screw configurations when degassing demands or specialized pigment dispersion targets justify the added mechanical complexity and maintenance load.
Do I need a lab-scale twin screw extruder before buying a full line?
If you are developing new additive concentrate formulations or qualifying a new carrier resin, yes. A lab-scale twin screw extruder lets you validate screw and barrel elements and throughput behavior before committing to a turnkey extrusion line. A representative lab unit specs at roughly 25 מם שרויף דיאַמעטער, א 7.5 קוו מאָטאָר, און 50 קג / ה רעזולטאַט (מאַרק פּראָדוקט רשימה, 2026), which is enough to prove a recipe while keeping material waste low. I treat the lab machine as insurance: the cost is trivial next to scrapping a mis-specified compounding line.
How do I choose a reliable masterbatch machine supplier?
I vet on four axes: אינסטאַלירן באַזע, engineering depth, verifiable certifications, and after-sales reach. A credible audited manufacturer should design, ינזשעניר, assemble, and test its extrusion systems in-house rather than reselling (פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד, 2025). Track record matters too. USEON, פֿאַר בייַשפּיל, cites 2,500+ production lines running in 70+ לענדער (USEON, 2026), and UET Machine claims 1,500+ וניץ איבערגעגעבן (UET מאַשין, 2026). Choosing the right twin screw extruder supplier is a high-leverage capital decision that affects throughput, ענערגיע נוצן, און קאַמפּאַונד קוואַליטעט פֿאַר יאָרן (Top 15 צווילינג שרויף עקסטרודער מאַניאַפאַקטשערערז בויער ס גייד, 2026), so I always request references in my own polymer and region before signing.
What is the cost vs quality tradeoff in masterbatch machinery?
The honest answer is that the cheapest masterbatch extruder rarely wins on total lifecycle cost. Low-bid machines often skimp on screw and barrel metallurgy, drive torque density, and process control, which shows up as inconsistent pigment dispersion and higher energy bills. UET מאַשין, דורך קאַנטראַסט, אַדווערטייזיז +/-0.5% יקסטרוזשאַן אַקיעראַסי און 20% ענערגיע סייווינגז (UET מאַשין, 2026), and higher torque density (USEON ס U+ סעריע ריטשאַז אַרויף צו 15 נם/קם³, USEON 2026) lets you push output without overdriving the motor. My rule: weigh purchase price against energy draw, wear-part replacement intervals, and uptime over a five-year horizon, not the quote alone.
How much does a masterbatch production line cost?
Pricing spans a wide range depending on capacity and automation. Marketplace listings put masterbatch making machines and full production lines at roughly $10,000 צו $100,000, sometimes with a minimum order as low as one set (קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס, 2026). At the entry end, Wanrooe Machinery lists SJP double screw masterbatch lines at $10,000 צו $40,000 (קאַמף, 2026). For a true factory-direct-sale turnkey extrusion line with feeders, plastic granulator, און פּעללעטיזינג, I budget toward the upper half of that band, then add installation, געראטעװעט, און קאַמישאַנינג.
What is the difference between twin screw and triple screw extruders?
A twin screw extruder uses two intermeshing screws, most commonly in a co-rotating extruder layout for strong distributive mixing, with counter-rotating extruder designs reserved for high-shear or specific dispersive needs. It handles the bulk of polymer compounding for color masterbatch, black masterbatch with carbon black, and filler grades in PP and PE. A triple screw extruder adds a third screw mainly to expand venting and devolatilization capacity. In practical terms, twin screw is the workhorse for most masterbatch making machines, while triple screw addresses edge cases where degassing throughput is the bottleneck.
What certifications should a masterbatch machine factory have?
אין מינימום, איך קוק פֿאַר ISO 9001 quality management plus CE marking for any line destined for regulated markets. Common certifications cited by established factories include CE, SGS, בוו, און יסאָ 9001 (UDTECH, 2025). I treat third-party audit marks like SGS or BV as confirmation that a verified supplier’s claims have been independently checked rather than self-asserted. פֿאַר יו. עס. בויערס, I also confirm electrical and safety compliance against local standards early, since retrofitting controls after delivery is costly and slow.
Should I buy from China, אייראָפּע, or India?
Each region trades off price, פירן צייַט, and support differently. Chinese factories like USEON dominate on installed base and value (USEON, 2026); Indian builders such as New Plast Machinery position around energy-efficient, דוראַבאַל קאַנסטראַקשאַן (ניו פּלאַסטיק מאַשינערי, 2025); and European suppliers typically command a premium for process control and proximity-based service. פֿאַר יו. עס. בויערס, the decision is not just sticker price. I factor in tariffs, compliance documentation, and the realistic cost of getting an engineer on-site, which can erode the savings on a lower headline quote. Delivery and commissioning of a full masterbatch production line typically runs from several weeks for stock configurations to three or more months for custom turnkey lines, so I confirm lead times in writing before ordering. You can cross-check current listings on געמאכט אין טשיינאַ און Accio’s supplier directory to benchmark price and MOQ before committing.
רעפערענצן
- USEON is a twin screw extruder manufacturer with 2,500+ production lines running in 70+ countries and U+ Series torque up to 15 Nm/cm3 — USEON (2026)
- UET Machine advertises +/-0.5% יקסטרוזשאַן אַקיעראַסי, 20% ענערגיע סייווינגז, און 1,500+ וניץ איבערגעגעבן — UET מאַשין (2026)
- Masterbatch making machines and production lines are listed at $10,000-$100,000 with MOQ as low as 1 set — קאַמף / געמאכט-אין-טשיינאַ מאַרק ליסטינגס (2026)
- Masterbatch manufacturing follows weighing, פידינג, צעשמעלצן מיקסינג, דעגאַססינג, און פּעללעטיזינג סטאַגעס — פּאָליפיל (2024)
- A twin screw extruder factory designs, ענדזשאַנירז, אַסעמבאַלז, and tests extrusion systems for plastics, עסן, און כעמישער ינדאַסטריז — פּלאַסטיק עקסטרודער סאַפּלייער B2B גייד (2025)
- Choosing the right twin screw extruder supplier is a high-leverage capital decision affecting throughput, ענערגיע נוצן, and compound quality — Top 15 Twin Screw Extruder Manufacturers Buyer's Guide (2026)
- Wanrooe Machinery lists SJP double screw masterbatch lines at $10,000-$40,000 with a 67% ריאָרדער קורס — קאַמף (2026)
- Common machine certifications cited by Chinese factories include CE, SGS, בוו, and ISO9001 — UDTECH (2025)
- New Plast Machinery positions itself as a masterbatch plant manufacturer focused on energy-efficient, דוראַבאַל קאַנסטראַקשאַן — ניו פּלאַסטיק מאַשינערי (2025)
- A lab twin screw extruder example specs at 25mm screw diameter, 7.5קוו מאָטאָר, און 50 קג / ה רעזולטאַט — מאַרק פּראָדוקט רשימה (2026)