

Роҳҳои асосӣ
- Экструзияи пластикӣ қатрони хомро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад., ки он ба дарозо мувофик аст, истехсоли махсулоти зиёд ба рох монда шудааст (Пластикҳои SeaGate, 2024).
- Вақте ки ман як истеҳсолкунандаи профили пластикиро арзёбӣ мекунам, ҷудо мекунам экструзияи фармоишӣ, ки маблаги якдафъаина ва асбобсозиро ичро мекунад, аз шаклҳои истихроҷи саҳҳомӣ, ки арзиши пешакиро сарфи назар мекунанд (Роҳнамои таъминкунандаи Thomasnet, 2024).
- Интихоби мавод ҳама чизро ба поён мебарад: Ман барномаро ба полимери дуруст мувофиқат мекунам, ки оё он барои қубур ва профилҳо PVC аст, ABS ё поликарбонат барои қувваи таъсир, HDPE ва LDPE барои муқовимати кимиёвӣ, полипропилен барои болгахои зинда, акрилӣ (PMMA) барои равшанӣ, ё нейлони дараҷаи муҳандисӣ (ПА) ва PEEK барои қисмҳои серталаб.
- PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, умумӣ дар саросари профилҳои, қубур, ва қубур, Аз ин рӯ, бисёр таъминкунандагон онро ҳамчун қобилияти пешфарз номбар мекунанд (Ассотсиатсияи саноати пластикӣ, 2023).
- Таҳаммулпазирии экструзия нисбат ба қолаби тазриқӣ аз сабаби коҳишёбии мавод ва ташаккули доимӣ сусттар аст., аз ин рӯ, ман таҳаммулпазириро барвақттар ба нақша гирифтам, на ба он ки дақиқии қисмҳои қолабӣ (Протолабҳо, 2023).
- Ман ба ISO муносибат мекунам 9001 ҳамчун сигнали ибтидоии системаи баркамол идоракунии сифат, кафолат нест, ва онро бо рӯйхати мушаххаси санҷиши иқтидори фарогиранда ҷуфт кунед, қобилияти коэкструзия, ва вақти роҳбарӣ (ISO, 2015).
- Барои мақсади ҷойгиршавӣ, аз истеҳсолкунандаи пластикии ватанӣ харидорӣ карда метавонад, арзиши умумии заминро тавассути кам кардани бор кам кунад, вазифадор, ва хароҷоти интиқоли захираҳо, як нуқтае, ки танҳо нисбат ба нархи воҳид баркашидан лозим аст (Ташаббуси барқарорсозӣ, 2023).
- Термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад, ки ман ҳам ба гуфтугӯҳои арзиш ва ҳам устуворӣ омил мекунам (ИМА EPA, 2023).
- Даъвоҳо ба монанди “калонтарин” ё “беҳтарин” фабрика бе контекст кам маъно дорад, бинобар ин ман таъминкунандагонро дар арзиши асбобҳо муқоиса мекунам, MOQ, истехсо-ли зудтаъмиршаванда, ва дастгирии исботшудаи прототип ба истеҳсол ба ҷои он.
Ширкатҳо ва заводҳои экструзияи пластикӣ воқеан чӣ кор мекунанд
Вақте ки ман як молрасонро барои муштарӣ арзёбӣ мекунам, Ман бо равшан кардани он, ки калима чӣ гуна аст “экструзия” аслан дар ошёнаи цех тасвир мекунад. Экструзияи пластикӣ ашёи хоми пластикиро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад (Пластикҳои SeaGate, 2024). Ин як ҷумлаи ягона вазнҳои зиёде дорад: процесс на тирандозй давом дорад, ва геометрия бо як буриши дученака муайян карда мешавад, ки дарозии пурраи қисмро иҷро мекунад. Аз ин рӯ, он барои истеҳсоли дарозмуддат ва истеҳсоли ҳаҷм хеле хуб мувофиқ аст, ва он як фанни воқеан аз қолаби сӯзандору ё коркарди мошинсозӣ фарқ мекунад.
Дар амал, “экструзияи қатрон” муҳаррикест, ки дар паси се оилаи васеи истеҳсолот ман мебинам, ки аксар вақт дархост карда мешаванд:
- Профилҳо — профилҳои пластикии фармоишӣ бо буриши муайян, аз каналҳои оддӣ ва ороишҳои канорӣ то шаклҳои мураккаби бисёр-люмен. Дар ин ҷо экструзияи профил ва коэкструзия воқеан дурахшон аст.
- Қубур — мудаввар, байзавии, ва найчаи бисёр-люменӣ, ки дар тиб истифода мешаванд, коркарди моеъ, ва барномаҳои пневматикӣ, аз таъминкунандаи махсуси қубурҳои пластикӣ гирифта шудааст.
- Варақ — экструзияи пластмасса барои панельхо, лайнерҳо, ва захираи термоформинг, ба воситаи матрит ва рол ҳамвор истеҳсол.
Истеҳсолкунандагон, Заводхо, ва дистрибюторҳо якхела нестанд
Харидорон аксар вақт ин истилоҳҳоро ба ҷои ҳамдигар истифода мебаранд, ва ин ба онҳо вақт сарф мекунад. Ин аст, ки чӣ тавр ман онҳоро ҷудо мекунам:
- А истеҳсолкунанда ё фабрика сохиби хатхои экструзия мебошад, мурдаи худро мебурад, ва равандро аз қатрон то қисми тайёр назорат мекунад. Ин аст он касе, ки шумо барои асбобҳои фармоишӣ мехоҳед, назорати қатъии раванд, ё пластмассаи инженерй.
- А дистрибютор ё фурӯшанда шаклҳои стандартиро захира мекунад ва мефиристад, аммо одатан хатро иҷро намекунад. Барои шаклҳои экструдсионии саҳҳомӣ ва фармоишҳои зуд, камтар барои кори фармоишӣ.
- А истеҳсолкунанда профилҳои саҳҳомӣ ва мошинро харида метавонанд, кафшер кардан, ё онҳоро ба хизматрасониҳои тайёри истеҳсоли пластикӣ ҷамъ кунед.
Вақте ки ман Thomasnet-ро ҷустуҷӯ мекунам, Ман дидаву дониста филтр мекунам, зеро ин феҳристҳо истеҳсолкунандагони экструзияи пластикии амрикоиро аз рӯи қобилият ва минтақа номбар ва гурӯҳбандӣ мекунанд (Томаснет, 2024). Ин филтри қобилият он чизест, ки ба шумо мегӯяд, ки оё шумо бо як истеҳсолкунандаи профили пластикӣ ё миёнарав сӯҳбат мекунед.
Чаро харидорон ҷустуҷӯ мекунанд “Завод” Ба ҷои “Таъминкунанда”
Дар таҷрибаи ман, гузариш ба сӯи “завод” сигналҳои забон ният. Харидороне, ки онро менависанд, мехоҳанд сарчашмае дошта бошанд, ки назорати дохилии тарроҳӣ ва асбобҳоро дар дохили хона назорат кунанд, сӯҳбатҳои шаффоф MOQ, ва қобилияти васеъ кардани миқёс аз прототип ба истеҳсолот. Он инчунин фишори барқароркуниро инъикос мекунад: таъминоти дохилӣ метавонад арзиши умумии заминро тавассути кам кардани бор кам кунад, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023), ва саноати пластикии ИМА саҳми асосии интиқоли истеҳсоли ватанӣ ва шуғл боқӣ мемонад (Ассотсиатсияи саноати пластикӣ, 2023). Ҷустуҷӯи истеҳсолкунандаи пластикии ватанӣ, на як таъминкунандаи умумӣ, аксар вақт як қарори дидаю дониста хавф ва хароҷот аст.
Чӣ тавр раванди экструзияи пластикӣ кор мекунад, Қадам ба қадам

Фаҳмидани механика ба шумо кӯмак мекунад, ки саволҳои беҳтар диҳед ва иқтибосро дақиқ хонед. Истеҳсолкунандагони Экизак винт Extruder Истеҳсолкунанда Ман мизоҷонро тавассути панҷ марҳилаи раванди экструзияи пайваста мегузарам.
1. Гирифтани ашьёи хом ва гудохтан дар бочка
Пелетҳои термопластикӣ - одатан PVC, ABS, HDPE, LDPE, ё полипропилен — ба бункер дохил шуда, ба бочкаи тафсон бо винти даврзананда афтед. Маҷмӯи гармкунакҳои баррел ва буриш қатронро ба ҷараёни якхелаи гудохта гудохта мекунад. Интихоби мавод дар ин ҷо муҳим аст: PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, одатан дар профилҳо истифода мешаванд, қубур, ва қубур (Ассотсиатсияи саноати пластикӣ), дар ҳоле ки поликарбонат, акрилӣ (PMMA), нейлон (ПА), ва PEEK бештар серталаб хизмат мекунанд, барномаҳои дараҷаи муҳандисӣ. Аз нав коркардшуда аксар вақт метавонад дубора омехта карда шавад, ва термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, аз ин рӯ, истифодаи дубораи дубора самаранокии маводро беҳтар мекунад (ИМА EPA, 2023).
2. Маҷбур кардани пластикии гудохта тавассути як қолаби фармоишӣ
Гудохта ба воситаи қолаб тела дода мешавад, ки буридани профилро муайян мекунад. Ин дили раванд аст ва сабаби кори фармоишӣ арзиши асбобро дорад. Танзими муштараки экструзия зиёда аз як экструдерро истифода мебарад, ки як штампро ғизо медиҳад, ба шумо имкон медиҳад, ки маводҳоро якҷоя кунед - субстрати сахт бо лаби мӯҳри мулоими TPE/TPU, барои намуна, ё қабати сарпӯши ранга бар ядрои арзонтар.
3. Хунуккунӣ, Андоза, ва Парвози муттасил
Тарки марг, профили нарм аз системаи хунуккунӣ ва андозагирӣ мегузарад - одатан ваннаи об ё зарфи вакуумӣ - ки андозаҳоро қуфл мекунад. Парвоз (кашанда) профилро бо суръати идорашаванда мекашад. Зеро кисм пай дар пай ташаккул меёбад ва масолех хангоми хунук шуданаш хурд мешавад, таҳаммулпазирии экструзия одатан нисбат ба қолаби тазриқӣ сусттар аст (Протолабҳо, 2023). Ман ин интизориро барвақт муқаррар кардам, то муштариён таҳаммулпазирии воқеиро муайян кунанд, ба ҷои пардохти дақиқи раванд, ки онро аз ҷиҳати иқтисодӣ нигоҳ дошта наметавонад.
4. Буридани дарозӣ ва истеҳсоли дуввум
Арра ё корди дарунсохт ҳосили доимиро ба дарозии кӯтоҳ мекунад. Аз он чо, корхои дуюмдарача — пармакунй, мушт задан, кандакорӣ кардан, чоп кардан, ё васлкунӣ — қисмҳои пластикии истихроҷшударо ба ҷузъҳои тайёр табдил диҳед. Ин пули байни профили хом ва дастрасии қобили истифода аст, ва дар он ҷо истеҳсоли зудтаъминкунӣ ё бурд мекунад ё аз даст меравад.
Фармоишгар против Extrusions пластикӣ саҳҳомӣ: Кадом ба шумо лозим аст?
Ин қарорест, ки аз ман бештар пурсида мешавад, ва ҷавоби ростқавл аст: ба хачм вобаста аст, геометрия, ва ҷадвали вақт. Биёед ман ҳар як роҳро вайрон кунам.
Вақте ки профилҳои саҳҳомии берун аз раф интихоби дуруст мебошанд
Шаклҳои исканҷашуда саҳҳомӣ - асои стандартӣ, найча, канал, кунҷ, ва варақ — хароҷоти асбобро комилан пешгирӣ кунед ва зуд интиқол диҳед. Агар профили каталог аризаи шумо дар доираи таҳаммулпазирии мувофиқ мувофиқ бошад, хариди саҳмияҳо қариб ҳамеша арзонтар аст, масири тезтар. Ман мизоҷонро дар ин ҷо барои прототипҳо роҳнамоӣ мекунам, ҳаҷми паст, ва ҳар қисме, ки дар он як порчаи стандартӣ кор мекунад.
Вақте ки асбобҳо ва профилҳои фармоишӣ асоснок карда мешаванд
Экструзияи фармоишӣ маъмулан як василаи якдафъаина ва сармоягузориро талаб мекунад, дар ҳоле ки профилҳои саҳҳомӣ аз ин хароҷот канорагирӣ мекунанд (роҳнамоии манбаи саноат). Вақте ки геометрияи шумо моликияти шумост, ин хароҷот асоснок карда мешавад, вақте ки салиб-фасли фармоишӣ василаи поёнобро нест мекунад, ё вакте ки хачми солона барои амортизацияи асбоб ба кадри кифоя зиёд аст. Аз андозаи муайяни давидан, сарфаи дар як фои-да барои максади сохташуда аз харочоти пешакй зиёд аст.
Равиши гибридӣ: Профилҳои стандартӣ, Қисмҳои фармоишӣ
Роҳи миёнаи дӯстдоштаи ман аксар вақт нодида гирифта мешавад. Профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд (Пластикҳои SeaGate, 2024). Шумо сармоягузории маргро гузаред, баъд буриданро истифода баред, коркард, ва васлкунӣ барои расидан ба як таҳвили фармоишӣ. Барои бисёр барномаҳои миёнаҳаҷм, ин гибрид ҳам захираи пок ва ҳам фармоишгари пурраро аз рӯи арзиши умумӣ мезанад.
Муқоисаи арзиш ва вақти кор
Ин аст, ки чӣ гуна се равишро умуман муқоиса мекунанд. Инҳоро ҳамчун доираи банақшагирии самтбахш баррасӣ кунед, на иқтибосҳо - рақамҳои воқеӣ аз мавод вобастаанд, геометрия, ва ҳаҷм.
|
Омил |
Профилҳои саҳҳомӣ |
Гибрид (Стандарти сохташуда) |
Экструзияи пурраи фармоишӣ |
|---|---|---|---|
|
Арзиши асбобҳои пешакӣ |
Ҳеҷ |
Ҳеҷ ба паст (танҳо асбобҳо) |
Сармоягузории яквақта |
|
Вақти маъмулии интиқол |
Кӯтоҳтарин (аксар вақт дар анбор) |
Кӯтоҳ то миёна |
Дарозитарин (месозанд + мақолаи аввал) |
|
Тартиби ҳадди ақал (MOQ) |
Кам |
Кам то миёна |
Баландтар (амортизация кардани асбобу анчом) |
|
Фасли геометрия |
Танҳо шаклҳои каталог |
Шакли стандартӣ + коркард |
Қисмати пурраи фармоишӣ |
|
Беҳтарин мувофиқ |
Прототипҳо, ҳаҷми паст |
Ҳаҷми миёна, мутобиқсозии ҳалим |
Ҳаҷми баланд, профилҳои хусусӣ |
|
Омил |
Профилҳои саҳҳомӣ |
Гибрид (Стандарти сохташуда) |
Экструзияи пурраи фармоишӣ |
|---|---|---|---|
|
Арзиши асбобҳои пешакӣ |
Ҳеҷ |
Ҳеҷ ба паст (танҳо асбобҳо) |
Сармоягузории яквақта |
|
Вақти маъмулии интиқол |
Кӯтоҳтарин (аксар вақт дар анбор) |
Кӯтоҳ то миёна |
Дарозитарин (месозанд + мақолаи аввал) |
|
Тартиби ҳадди ақал (MOQ) |
Кам |
Кам то миёна |
Баландтар (амортизация кардани асбобу анчом) |
|
Фасли геометрия |
Танҳо шаклҳои каталог |
Шакли стандартӣ + коркард |
Қисмати пурраи фармоишӣ |
|
Беҳтарин мувофиқ |
Прототипҳо, ҳаҷми паст |
Ҳаҷми миёна, мутобиқсозии ҳалим |
Ҳаҷми баланд, профилҳои хусусӣ |
Кадом роҳро интихоб кунед, Ман тавсия медиҳам, ки дар мағоза системаи ҳуҷҷатшудаи сифат - ISO кор мекунад 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад (ISO, 2015) ва ҳамчун меъёри васеъ қабулшуда дар бахши пластикӣ боқӣ мемонад. Барои дидани амалии он, ки чӣ гуна саҳмияҳо ва пешниҳодҳои фармоишӣ паҳлӯ ба паҳлӯ менишинанд, меёбам Пластикҳои SeaGate’ Шарҳи экструзияи фармоишӣ нуқтаи истинод муфид.
Намудҳои профилҳои пластикии экструзия ва маҳсулоти

Вақте ки ман лоиҳаро барои экструзия арзёбӣ мекунам, Ман аз порча оғоз мекунам, зеро геометрияи кисми тайёр кариб хама чизро дар поёноб дикта мекунад: тарҳрезии матоъ, интихоби моддӣ, ва дар ниҳоят нархе, ки шумо пардохт мекунед. Экструзияи пластикӣ қатрони хомро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад. (Пластикҳои SeaGate, 2024). Ин як принсипи ягона феҳристи ҳайратангези васеи шаклҳоро ба вуҷуд меорад, бинобар ин барои гурӯҳбандӣ кардани онҳо аз рӯи мураккабӣ ва функсия кӯмак мекунад.
Профилҳои сахт, Профилҳои холӣ, ва геометрияҳои мураккаб
Solid profiles are the workhorses of the industry: чубхо, bars, канори, and trim with no internal voids. They are the easiest to tool and the most forgiving on tolerance, which is why I recommend them for first-time buyers testing a design. Hollow profiles introduce internal channels, and they demand more sophisticated dies with mandrels or pins to hold the cavity open as the melt cools. Complex geometries combine multiple walls, зербурҳо, and thin-to-thick transitions in a single cross-section, and this is where die design and tooling expertise separates a capable plastic profile manufacturer from an average one. Дар таҷрибаи ман, uneven wall thickness is the most common cause of warping, so I press suppliers early on how they plan to balance material flow across the profile.
Tubing and Multi-Lumen Extrusions
Tubing зер маҷмӯи махсуси экструзияи холӣ мебошад, ва он ҳама чизро аз қубурҳои оддии як сӯрохӣ то тарҳҳои бисёр-люменӣ бо якчанд каналҳои параллелӣ, ки дар дарозии қисм кор мекунанд, фаро мегирад.. Харидорони таҷҳизоти тиббӣ ва асбобҳои аналитикӣ барои интиқоли моеъҳо ба экструзияҳои бисёр-люмен такя мекунанд, симхо, ва сенсорҳо тавассути як профили паймон. Таъминкунандаи боэътимоди қубурҳои пластикӣ таҳаммулпазирии зич ва диаметри дохилиро нигоҳ медорад, гарчанде ки ман ҳамеша ба мизоҷон хотиррасон мекунам, ки таҳаммулпазирии экструзия одатан нисбат ба қолаби тазриќӣ аз сабаби камшавии мавод ва ташаккули доимӣ сусттар аст. (Захираҳои тарроҳии Protolabs, 2023). Ба ҷои он ки бо он мубориза баред, мувофиқат ва равшании худро дар атрофи он воқеият ба нақша гиред.
Ко-экструзия ва профилҳои бисёрсоҳавӣ
Ко-экструзия ду ё зиёда қатронро тавассути қолаби муштарак мегузаронад, то профили ягона бо минтақаҳои гуногуни моддӣ истеҳсол карда шавад.. Ман онро истифода мебарам, вақте ки як қисм якбора хосиятҳои ба ҳам мухолиф лозим аст, ба монанди як мақоми сохтории PVC сахт бо лаби gasket мулоим TPE / TPU, ё қабати сарпӯши обу ҳаво дар болои субстрати арзонтар. Он қадамҳои дуюмдараҷаи васлкунӣ ва пайвасткуниро нест мекунад, ки дар хачм сарфаи пурмазмуни харочот мебошад. Мубодила мураккабии асбобҳост, аз ин рӯ, ман экструзияи муштаракро барои тарҳҳое нигоҳ медорам, ки фоидаи бисёрсоҳавӣ сармоягузории иловагиро ба таври возеҳ асоснок мекунад.
Барномаҳои умумии саноат барои ҳар як намуд
Геометрияҳои гуногун ба бахшҳои гуногун ҷалб карда мешаванд, ва мувофиқ кардани онҳо барвақттар сӯҳбатҳоро дар маркази диққат медиҳад.
- Профилҳои сахт: канори рафи чакана, ороиши мебел, мӯҳрҳо, ва ҷузъҳои девор.
- Профилҳои холӣ: чорчубахои дару тиреза, Каналҳои равшании LED, ва пӯшиши сохторӣ.
- Қубур ва бисёр-люмен: катетерҳои тиббӣ, хатҳои интиқоли моеъ, ва қубурҳои пневматикӣ.
- Профилҳои якҷояшуда: обу ҳаво, қубурҳои яхдон, ва дастаки ду-дурометр.
- Экструзияи варақ: нишона, захираи термоформинг, ва панелҳои муҳофизатӣ.
Зеро экструзияи пластикӣ пайваста аст, раванди ҳаҷми баланд, он барои истеҳсоли дарозмуддат мувофиқ аст, махсусан хуб, ва профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд (Пластикҳои SeaGate, 2024). Агар талаботи солонаи шумо устувор бошад ва дар даҳҳо ҳазор фут чен карда шавад, иқтисоди extrusion сахт ба манфиати шумо кор.
Маводҳои маъмуле, ки дар экструзияи пластикӣ истифода мешаванд
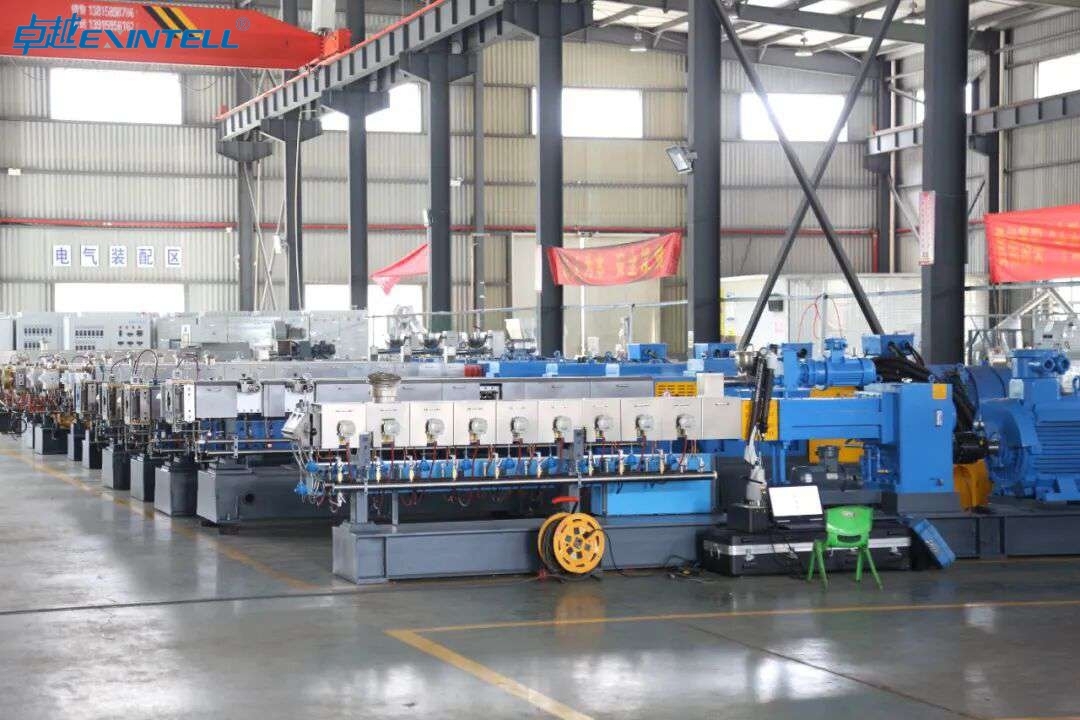
Интихоби мавод ин қарорест, ки ман мебинам, ки харидорон аксар вақт нодида мегиранд. Қатрон қувваи механикиро идора мекунад, муқовимати химиявӣ, диапазони ҳарорат, арзиш, ва ҳатто то чӣ андоза сахт таҳаммулпазирии экструдер метавонад ба таври воқеӣ нигоҳ дошта шавад. Ман қатронҳои экструзияро ба се зина гурӯҳбандӣ мекунам, пас бо муштариён кор кунед, то танҳо он ҷое, ки барнома воқеан талаб мекунад, боло равед.
Қатронҳои молӣ: PVC, Полиэтилен, ва полипропилен
Қатронҳои молӣ қисми зиёди ҳаҷми истихроҷшударо фаро мегиранд, ва бо сабаби хуб. PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, Дар профилҳо маъмуланд, қубур, ва қубур (Ассотсиатсияи саноати пластикӣ). Он устувориро пешниҳод мекунад, тобовар будани обу ҳаво, ва арзиши паст, ва он ранг ва рангро хуб мегирад. Полиэтилен дар ду навъи шинос пайдо мешавад: HDPE барои сахт, профилҳои ба кимиёвӣ тобовар ва LDPE, ки чандирӣ муҳим аст. Полипропилен муқовимати кимиёвиро бо таносуби хуби қувват ба вазн ва иҷрои ҳалқаи зинда мувозинат мекунад. Вақте ки муштарӣ дар бораи экструзияи қатрон барои ҳаҷми баланд мепурсад, қисми ҳассос ба хароҷот, ин қариб ҳамеша аз он ҷое ки ман оғоз мекунам.
Қатронҳои муҳандисӣ: ABS, Поликарбонат, Нейлон, ва акрилӣ
Пластмассаҳои дараҷаи муҳандисӣ дар иҷрои механикӣ ва гармӣ баланд мешаванд. ABS барои қисмҳои истеъмолкунанда ва иҳота қувваи таъсир ва ороиши тоза медиҳад. Polycarbonate brings high impact resistance and optical clarity, which makes it a staple for lighting lenses and safety glazing. Нейлон (ПА) offers wear resistance and toughness for mechanical components and cable management. Акрилӣ (PMMA) provides excellent clarity and UV stability for display and signage profiles. I move buyers into this tier when commodity resins cannot meet load, гармй, or clarity requirements, and I make sure they price the resin premium against the performance gain before committing.
High-Performance Materials Like PEEK
At the top sits a small group of high-performance polymers, with PEEK as the reference point. PEEK withstands continuous high temperatures, кимиёвии хашмгин, and demanding mechanical loads, ки чаро он дар кайхонй зохир мегардад, тиббй, and semiconductor applications. The material cost is substantial, бинобар ин ман онро танҳо вақте муайян мекунам, ки муҳити корӣ имкони арзонтаре надошта бошад. На ҳар як истеҳсолкунандаи профили пластикӣ PEEK-ро коркард мекунад, бинобар ин скрининги қобилият дар ин сатҳ муҳимтар аст.
Мутобиқати хосиятҳои моддӣ ба талаботи дархост
Чаҳорчӯбаи интихоби ман дидаву дониста оддӣ аст: аввал талаботи гайримукаррариро муайян кунед, он гоҳ қатрони арзонтаринро интихоб кунед, ки онро тоза мекунад. Ҷадвали дар поён овардашуда ҷамъбаст мекунад, ки чӣ гуна ман вариантҳои маъмулии қисмҳои пластикии истихроҷшударо баркашам.
| Материал | Сатҳи | Тарафҳои асосӣ | Арзиши нисбӣ | Барномаҳои маъмулӣ |
|---|---|---|---|---|
| PVC | Мол | Сахт, тобовар, камхарҷ | $ | Профилҳо, қубур, тарм |
| HDPE / LDPE | Мол | Муқовимати кимиёвӣ; сахт ё чандир | $ | Қубур, лайнерҳо, канализатсия |
| Полипропилен | Мол | Муқовимати кимиёвӣ, ҳалқаҳои зинда | $ | Муносибати моеъ, болгаҳо |
| ABS | Муҳандисӣ | Қувваи таъсир, анҷоми тоза | $$ | Заводҳо, қисмҳои истеъмолӣ |
| Поликарбонат | Муҳандисӣ | Муқовимат ба таъсир, равшанӣ | $$ | Линзаҳо, шишабандии бехатарӣ |
| Нейлон (ПА) | Муҳандисӣ | Муқовимат ба пӯшидан, сахтгирй | $$ | Механикӣ, дастурҳои кабелӣ |
| Акрилӣ (PMMA) | Муҳандисӣ | Возеіият, Устувории ултрабунафш | $$ | Нишон, намоиш медихад |
| PEEK | Самаранокии баланд | Гарм, химиявй, ва муқовимати сарборӣ | $$$$ | Аэрокоинот, тиббй, нимноқил |
Як нуқтаи самаранокиро бо ҳама таъминкунанда баланд кардан лозим аст: термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад (Агентии ИМА оид ба ҳифзи муҳити зист, 2023). Asking how a factory handles regrind tells me something about both their cost discipline and their sustainability practices.
Plastic Extrusion Manufacturers in the USA
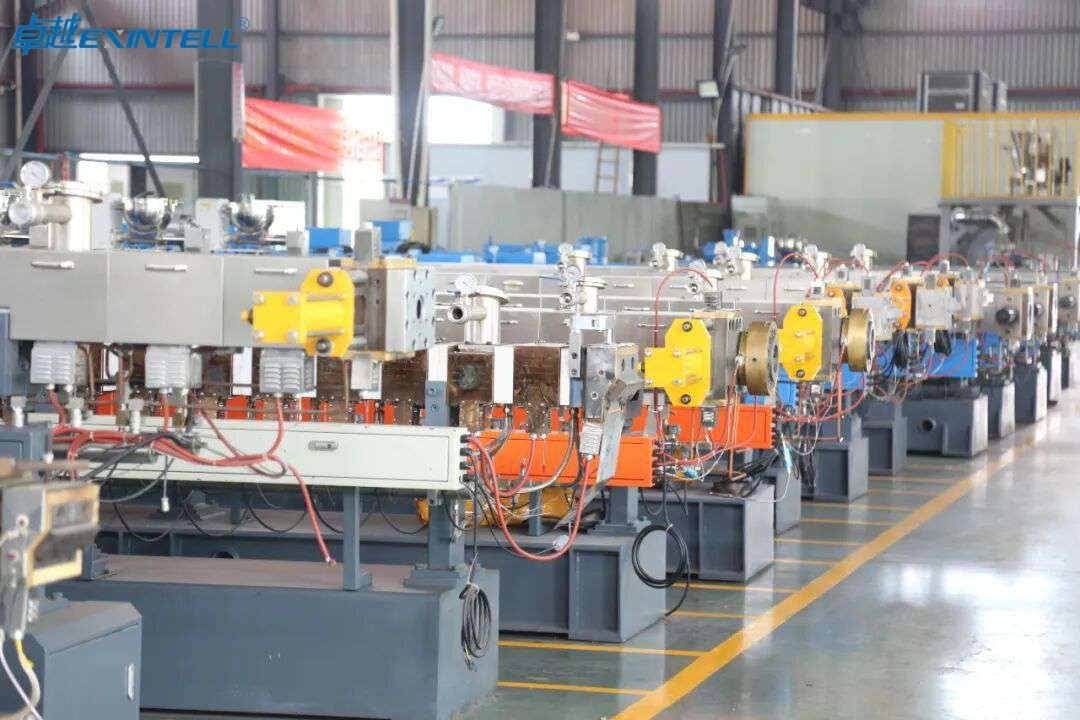
For many of the buyers I advise, the sourcing question is not only “who can extrude this profile” аммо “who can extrude it here.” Domestic sourcing has moved from a preference to a strategic decision, and it deserves a clear-eyed look rather than reflexive patriotism.
Why US-Based Sourcing Matters for Many Buyers
The financial case is stronger than it first appears. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023). When I run a total-cost comparison rather than a unit-price comparison, offshore savings often shrink once I add ocean freight, тарифхо, захираи бехатарӣ, ва сармояи кории дар муддати тӯлонии транзит басташуда. Барои як истеҳсолкунандаи пластикии ватанӣ, ки ба муштарии ИМА хизмат мерасонад, мӯҳлатҳои иҷроиш, ки бо ҳафтаҳо, на моҳҳо чен карда мешаванд, инчунин хавфи камтарро дорад, агар тарроҳӣ дар миёнаи барнома тағир ёбад.
Марказҳои истеҳсолии минтақавӣ дар саросари кишвар
Иқтидори экструзияи ИМА баробар тақсим карда нашудааст, ва донистани харита сарчашмаҳоро суръат мебахшад. Кӯлҳои Бузург ва Миёнаи Ғарби Боло профили таъиноти умумӣ ва экструдерҳои қубурро дар наздикии талаботи автомобилӣ ва саноатӣ мутамарказ мекунанд. Дар шимолу шарқ як кластери зиччи мутахассисони соҳаи тиб ва найҳои дақиқ мавҷуд аст. Ҷанубу Шарқ дар атрофи маҳсулоти сохтмонӣ ва бастабандӣ зуд афзоиш ёфтааст. Соҳили Ғарбӣ ва Ҷанубу Ғарб ба электроника хизмат мекунанд, кайхонй, ва бозорхои истеъмолй. Supplier directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Томаснет, 2024), which is where I usually build a first shortlist before making calls.
Domestic Quality, Муошират, and IP Advantages
Beyond cost, three practical advantages keep drawing buyers home. Аввал, quality systems are easier to verify in person; ISO 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад (Ташкилоти байналхалқии стандартизатсия, 2015), and I can audit a domestic supplier’s implementation without an international trip. Дуюм, time-zone-aligned communication shortens the feedback loop from prototype to production, which matters when a die needs a mid-run adjustment. Сеюм, intellectual property protection is more enforceable under US jurisdiction, a real concern when a custom profile is a competitive differentiator. I treat these as the differences that a spreadsheet alone will miss.
How US Factories Serve Diverse Industries
American extruders span the full range of contract manufacturing, from stock extruded shapes shipped from inventory to fully custom die programs. Custom extrusion typically requires a one-time tooling or die investment, while stock profiles avoid that cost, so I match the sourcing path to how unique the geometry really needs to be. The US plastics industry remains a major contributor to domestic manufacturing shipments and employment (Ассотсиатсияи саноати пластикӣ, 2023), and that depth means a buyer can usually find a plastic fabrication services partner suited to their volume, from prototype to production. For a broad view of custom capabilities, I often point clients to overviews such as custom plastic extrusion manufacturers to calibrate expectations before requesting quotes.
How to Find Plastic Extrusion Companies Near You
When I begin a sourcing project, geography is one of the first variables I weigh. Location shapes freight cost, communication cadence, and how quickly I can iterate from prototype to production. Гуфт, proximity is only valuable when the nearby supplier can actually do the work. Дар таҷрибаи ман, the smartest approach treats “дар наздикии ман” as a filter, not a decision.
Why Local Sourcing Often Pays Off
A domestic plastics manufacturer close to your facility gives you three concrete advantages. Аввал, shorter shipping distances lower freight and lead-time risk, which matters for bulky extruded plastic parts and long profiles that ship as oversized freight. Дуюм, local partners make on-site visits practical, and I have caught more process issues in a two-hour plant walkthrough than in weeks of email. Сеюм, proximity accelerates iteration: when a die needs a tweak, a supplier a few hours away can turn samples faster than one across an ocean.
The financial case reaches beyond the unit price. According to the Reshoring Initiative (2023), таъминоти дохилӣ метавонад арзиши умумии заминро тавассути кам кардани бор кам кунад, вазифадор, ва хароҷоти интиқоли захираҳо. The domestic base is substantial, низ; иттиходияи саноати пластмасса (2023) reports that the US plastics industry is a major contributor to domestic manufacturing shipments and employment, which means qualified capacity for resin extrusion is usually within reach.
Where I Look: Directories, Associations, ва муроҷиатҳо
To build an initial list of candidates, I use three complementary channels:
- Supplier directories. Томаснет (2024) lists and categorizes US plastic extrusion manufacturers by capability and region, which makes it straightforward to filter by material, раванд, and location.
- Trade associations. Membership in bodies like the Plastics Industry Association signals a firm that invests in standards and industry engagement.
- Referrals. A recommendation from an engineer who has run production with a plastic profile manufacturer carries more weight than any marketing page, because it reflects delivered performance.
I treat the directory as a starting point for a plastic tubing supplier or profile shop, then validate each name against real references before it earns a spot on my shortlist.
Balancing Proximity Against Capability and Price
Distance is a tiebreaker, not a trump card. If a nearby shop cannot hold your tolerances, run your resin, or meet your volume, the convenience is worthless. I rank capability and quality first, баъд нарх, then location. A plastic extrusion companies factory supplier two states away with the right co-extrusion line and a proven ISO 9001 system will usually serve me better than a closer shop lacking those capabilities.
When Local Is Not the Best Option
Sometimes the right partner is not nearby. Specialized work in engineering-grade plastics such as PEEK, поликарбонат, ё нейлон (ПА) may only be done well by a handful of shops nationally. High-volume manufacturing programs can justify shipping economics that favor a distant, more automated plant. And when you need capabilities like plastic sheet extrusion combined with in-line fabrication, the fit of the process matters more than the mileage. In those cases I widen the search radius and lean on video plant tours and third-party audits to close the distance gap.
Understanding the Largest Plastic Extrusion Companies
Buyers often gravitate toward the biggest names, assuming scale guarantees a better outcome. Scale does deliver real advantages, but it also carries tradeoffs. Understanding what “калонтарин” actually means helps me match a supplier’s footprint to my program rather than to a reputation.
What Scale Means for Capacity and Reliability
Экструзия давомнок аст, high-volume process well suited to long production runs, and large factories are built around that reality. More extrusion lines mean higher throughput, redundancy if one line goes down, and the ability to absorb demand spikes. Scale usually correlates with mature quality systems as well; ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (Ташкилоти байналхалқии стандартизатсия, 2015), is almost table stakes among large plants. That maturity translates into more consistent extruded plastic parts across long runs.
The Tradeoffs of Large Factories vs. Specialized Shops
Bigger is not automatically better. Large plants optimize for volume, which can mean higher minimum order quantities, less flexibility on small custom runs, and slower responsiveness on prototype work. A specialized shop may excel at tight-tolerance custom plastic profiles, unusual resins, or quick-turnaround production that a high-volume plant treats as a nuisance. The table below summarizes how I weigh the two.
| Омил | Large-Scale Factory | Specialized Shop |
|---|---|---|
| Иқтидор | Баланд; multiple lines, redundancy | Маҳдуд; fewer lines |
| Миқдори ҳадди ақали фармоиш | Often high | Usually flexible |
| Prototype speed | Оҳистатар; volume-focused scheduling | Тезтар; agile setup |
| Material range | Broad commodity resins (PVC, HDPE, LDPE, PP) | Often engineering-grade (PEEK, Компютер, ПА) |
| Price per unit at volume | Поёнтар | Баландтар |
| Беҳтарин мувофиқ | Long production runs | Фармоишгар, low-to-mid volume, complex profiles |
When High-Volume Capability Is Essential
There are programs where I will not compromise on scale. Пайваста, long-run demand for standardized profiles, қубур, or tubing in commodity resins is the natural home of a large factory. PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, одатан дар профилҳо истифода мешаванд, қубур, ва қубур, and sourcing it at volume rewards the economies a big plant provides. If your forecast calls for millions of feet of a stable profile cross-section, high-volume capability moves from nice-to-have to essential.
How to Verify Claimed Scale and Capacity
Claims on a website are not evidence. Before I accept a “калонтарин” ё “highest capacity” claim, I verify it with concrete questions:
- How many extrusion lines are operational, and what is the die diameter range on each?
- What is current utilization, and how much spare capacity exists for my program?
- Can you share throughput figures (lbs/hour or feet/day) for a comparable profile?
- What redundancy exists if a line fails mid-run?
- Which certifications, ба монанди ISO 9001, are current, and may I see the certificate?
I pair those answers with a plant tour or audit. Physical evidence of running lines, staffing, and inventory tells me far more than any capacity figure quoted in a brochure.
How to Identify the Best Plastic Extrusion Factory for Your Project
“Best” is one of the most misused words in supplier marketing. Дар амал, the best plastic extrusion companies factory manufacturer is the one that best fits your specific requirements, not the one with the loudest claim. I define the term relative to my project, then score candidates against that definition.
Defining “Best” Relative to Your Specific Needs
Before comparing suppliers, I document what my project actually demands: the resin (гуфтан, ABS for impact resistance, акрилӣ (PMMA) барои равшании оптикӣ, or TPE/TPU for flexibility), the tolerance band, the volume, the timeline, and the level of engineering support I need for die design and tooling. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Захираҳои тарроҳии Protolabs, 2023), so I confirm early that a candidate can meet my dimensional requirements rather than assuming it can. A shop that is ideal for a high-volume HDPE pipe run may be the wrong choice for a tight-tolerance polycarbonate profile.
Weighing Quality, Арзиш, Суръат, and Support
Every sourcing decision balances four levers, and improving one often pressures another:
- Сифат. Documented quality systems, in-process inspection, and material traceability. ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics.
- Арзиш. Not just unit price. Экструзияи фармоишӣ маъмулан як василаи якдафъаина ва сармоягузориро талаб мекунад, while stock extruded shapes avoid that cost, so I model total cost including tooling and MOQ.
- Суръат. Профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд (Пластикҳои SeaGate, 2024), but lead times vary widely between shops.
- Дастгирӣ. Engineering input on profile cross-section and material selection can prevent costly redesigns as you move from prototype to production.
Sustainability increasingly enters the equation as well. Термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад (Агентии ИМА оид ба ҳифзи муҳити зист, 2023), which can reduce both cost and waste when a supplier manages it responsibly.
Reading Past “Best” Marketing Claims
Superlatives are easy to print and hard to prove. When I see “беҳтарин,” “рохбарй мекунад,” ё “premier,” I translate the claim into a testable question. Instead of accepting “best quality,” I ask for defect rates and inspection records. Ба ҷои “fastest,” I ask for typical lead times on my specific part. Ба ҷои “most experienced,” I ask for references in my industry. Marketing language that cannot survive a follow-up question does not influence my shortlist.
Building a Shortlist Scoring Method
To keep the comparison objective, I use a weighted scoring model. I list my criteria, assign each a weight that reflects its importance to the project, score every candidate from 1 ба 5, and multiply. The weights shift by project; a prototype program might weight speed and engineering support heavily, while a mature production program weights cost and capacity.
- List criteria: системаҳои сифат, material capability, таҳаммулпазирӣ, иктидор, вақти иҷрошуда, tooling cost, дастгирии муҳандисӣ, and location.
- Assign weights that total 100 percent, reflecting your priorities.
- Score each supplier 1 ба 5 on every criterion, using verified evidence rather than marketing claims.
- Calculate weighted totals and rank the candidates.
- Validate the top two with reference calls and, идеалӣ, a plant visit before committing.
This structured method has consistently steered me toward the partner that fits the work, whether that turns out to be a large plant, a nimble specialist, or a domestic shop just down the road. For a deeper look at how custom extrusion capabilities map to applications, resources such as Пластикҳои SeaGate’ Шарҳи экструзияи фармоишӣ are a useful reference as you refine your own criteria.
Key Capabilities to Evaluate in a Plastic Extrusion Company
When I vet a plastic profile manufacturer, I look
Tolerances and Precision in Extruded Parts
Вақте ки ман як истеҳсолкунандаи профили пластикиро арзёбӣ мекунам, tolerances are the first place I look for a reality check. Extrusion is a continuous forming process, so it behaves differently from molding. As Protolabs notes, extrusion tolerances are generally looser than injection molding because material shrinkage and continuous forming introduce variability that a closed mold does not (Захираҳои тарроҳии Protolabs, 2023). Setting expectations here early saves both money and rework later.
Typical Achievable Tolerances by Material and Profile
Дар таҷрибаи ман, achievable precision depends heavily on the resin and the geometry of the profile cross-section. Rigid engineering-grade plastics hold tighter dimensions than soft or semi-crystalline materials, and simple shapes hold tighter than complex hollow profiles. The ranges below reflect commonly quoted commercial extrusion capabilities for custom plastic profiles; always confirm against your supplier’s published standards for your specific part.
| Материал | Устувории андоза | Typical tolerance tendency | Notes for specifying |
|---|---|---|---|
| PVC сахт | Баланд | Tighter, well-controlled | Widely extruded; predictable in profiles and tubing |
| ABS | Баланд | Tight on rigid profiles | Good for structural extruded plastic parts |
| Поликарбонат | Баланд | Сахт, low shrink | Optical and impact-rated applications |
| Акрилӣ (PMMA) | Баланд | Сахт, but brittle at thin walls | Sheet and clear profiles |
| Нейлон (ПА) | Муътадил | Looser; moisture-sensitive | Account for post-extrusion moisture uptake |
| HDPE / LDPE | Moderate to low | Looser; higher shrink | Expect wider bands on wall and OD |
| Полипропилен | Муътадил | Looser; semi-crystalline shrink | Allow generous tolerance on critical dims |
| PEEK | Баланд | Сахт, but specialized | High-temp engineering runs; higher cost |
| TPE / TPU | Кам | Loosest; flexible recovery | Soft profiles deform under measurement |
Factors That Affect Dimensional Stability
Several variables move a part inside or outside its tolerance band. Wall thickness uniformity matters most: thick and thin sections in the same profile cool at different rates and warp. Semi-crystalline resins like polypropylene and HDPE shrink more than amorphous ones like polycarbonate and acrylic, so the die must be cut to compensate. I also watch for haul-off speed, melt temperature, and cooling-bath control, since drift in any of these shows up as dimensional variation over a long run. For hygroscopic materials such as nylon, moisture absorbed after extrusion can change dimensions days later, which is why I ask how a supplier conditions and stores finished stock.
Specifying Tolerances in Your Drawings
The cleanest way to control cost is to tolerance only what functionally matters. I call out critical dimensions explicitly, apply a reasonable general tolerance block to everything else, and reference the datum features that mate with other components. Where a flexible TPE or TPU profile is involved, I specify the measurement method and fixture, because a soft part measures differently under light pressure than at rest. Being specific about which surfaces are cosmetic versus functional lets a plastic fabrication services partner set up the line intelligently instead of overbuilding to a blanket precision requirement.
Balancing Precision Against Cost
Tighter tolerances raise cost through slower line speeds, more scrap, added inspection, and sometimes secondary sizing or machining. Дар амал, I treat precision as a dial rather than a switch: I hold the two or three dimensions that drive fit and function tightly and relax the rest. That approach keeps resin extrusion economical while still delivering parts that assemble correctly. When a design genuinely needs molding-level precision on every feature, that is a signal the part may not be a good extrusion candidate, and I revisit the process choice before committing to tooling.
Minimum Order Quantities and Lead Times
MOQs and lead times are where the difference between stock extruded shapes and true custom work becomes concrete. Custom extrusion typically requires a one-time tooling investment in a die, while stock profiles avoid that cost entirely, per common industry sourcing guidance. That single fact drives most of the ordering economics, so I plan around it from the start.
Typical MOQ Ranges for Stock vs Custom
Stock profiles and tubing can often be bought in small quantities, sometimes by the foot or in single boxes, because the supplier already runs them. As SeaGate Plastics points out, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround, which is a practical advantage when volumes are modest (Пластикҳои SeaGate, 2024). Custom profiles are different. Because the line has to be set up, purged, and stabilized before good parts come off, suppliers set a minimum run to amortize that setup. I commonly see custom MOQs expressed in pounds of resin or in linear footage rather than piece count, and the threshold rises with more exotic engineering-grade plastics.
How Lead Times Vary With Tooling and Volume
For a new custom profile, the die is the pacing item. Tooling design, буридан, and first-article trials typically dominate the initial schedule, and I budget several weeks for die design and tooling before any production parts exist. Once the die is proven, repeat orders move quickly because the tooling is on the shelf. Higher volumes actually help here: extrusion is a continuous, high-volume process well suited to long production runs, so once a line is dialed in, adding footage is efficient rather than disruptive.
Quick-Turnaround Options and Expedited Runs
When a timeline is tight, I look at three levers. Аввал, use stock profiles or standard tubing that can ship from inventory and be cut or fabricated to length. Дуюм, ask whether an existing die is close enough to modify rather than cutting a new one. Сеюм, request an expedited slot, which many suppliers offer for a premium by prioritizing line time. Quick-turnaround production is realistic for standard shapes; for genuinely new custom geometry, the tooling step still sets the floor on how fast you can go.
Planning Your Project Timeline
I work backward from the required delivery date and add explicit buffers for die design, first-article approval, and any secondary operations. Moving from prototype to production is smoother when I lock the profile cross-section early, because late geometry changes mean recutting the die and resetting the clock. Aligning MOQ with real annual demand also matters: ordering an efficient run size once beats paying repeated setup charges on small, frequent custom orders.
Cost Drivers in Plastic Extrusion Pricing
Understanding what actually drives a quote lets me negotiate from evidence rather than instinct. Extrusion pricing breaks down into a handful of levers, and knowing which one dominates for a given part tells me where the savings live.
Material Selection and Resin Pricing
Resin is usually the largest recurring cost, and it varies widely by grade. Commodity materials like PVC, полипропилен, HDPE, and LDPE sit at the low end; PVC in particular is among the most widely extruded plastics globally and is well supported across suppliers. Engineering-grade plastics such as polycarbonate, нейлон, and especially PEEK command higher prices and can require specialized processing. One efficiency I always ask about is regrind: термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад, which can lower material cost on non-critical parts (Агентии ИМА оид ба ҳифзи муҳити зист, 2023). Choosing the least expensive resin that meets the application requirement is the single highest-leverage decision in material selection.
Асбобсозӣ, Setup, and Run Volume
Custom work carries a one-time die cost that stock profiles avoid. That tooling charge is fixed, so it amortizes across the run: the more footage I order, the lower the per-part tooling burden. Setup time and line stabilization add cost to every job regardless of size, which is exactly why small custom orders feel expensive per piece. Ко-экструзия, which combines two materials in one profile, adds tooling and process complexity and therefore cost, but it can eliminate secondary assembly, so I weigh the tradeoff on total value rather than tooling alone.
Secondary Operations and Finishing
Anything that happens after the profile leaves the die adds cost: cutting to length, пармакунй, кандакорӣ кардан, чоп кардан, hole punching, tight-tolerance sizing, ва бастабандӣ. Individually these are minor, but they stack quickly on high piece counts. I decide deliberately which operations belong in-line with the extrusion and which are genuinely needed, because each added step also adds handling and inspection. Where a feature can be designed into the profile cross-section instead of machined afterward, I do that, since forming a feature is nearly free compared with a downstream operation.
Domestic vs Offshore Cost Comparisons
Headline piece price often favors offshore, but I evaluate total landed cost. The Reshoring Initiative notes that domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023), and those factors are easy to underestimate when comparing unit prices alone. Working with a domestic plastics manufacturer also shortens lead times, simplifies communication, and reduces the inventory buffer I have to hold against long ocean transit. The US plastics industry is a substantial contributor to domestic manufacturing shipments and employment (Ассотсиатсияи саноати пластикӣ, 2023), so the domestic supplier base for both stock and custom profiles is deep. Қоидаи ман: барои ҳаҷми баланд, low-mix commodity profiles, offshore can win on price; for responsive, higher-mix, or engineering-grade work, domestic contract manufacturing usually wins on total cost and risk. For a fuller look at custom capabilities, I point buyers to custom plastic extrusion manufacturers such as SeaGate Plastics as a reference point for scope and services.
Questions to Ask Before Choosing a Factory
When I vet a plastic profile manufacturer, I treat the first conversation as a structured interview rather than a sales call. The goal is to separate shops that can genuinely deliver my part from those that simply want the order. Over years of sourcing extruded plastic parts, I have found that a handful of pointed questions surface most of the risk before a single dollar changes hands. Below is the checklist I actually use.
Иқтидор, Сертификатсияҳо, and Material Expertise
I start by asking what the factory runs today, not what it claims it can run. Continuous extrusion is a high-volume manufacturing process, so I want to know line count, typical run lengths, and whether they have headroom for my volume without displacing existing customers. On the quality side, I ask directly about certification. ISO 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад (Ташкилоти байналхалқии стандартизатсия, 2015), and while certification is not a guarantee of good parts, its absence tells me the shop may lack documented process controls.
Material expertise is the third leg. A capable resin extrusion supplier should speak fluently about the polymers relevant to my application, whether that is PVC and HDPE for construction profiles, ABS and polycarbonate for enclosures, polypropylene and LDPE for packaging and tubing, or engineering-grade plastics like nylon (ПА) and PEEK for demanding environments. PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, одатан дар профилҳо истифода мешаванд, қубур, ва қубур (Ассотсиатсияи саноати пластикӣ). If I need flexible sections, I confirm experience with TPE/TPU, and if my part demands a rigid core with a soft-touch or weather-resistant skin, I ask whether they offer co-extrusion. Лабораторияи экструдер яклухт
Prototyping and Design Support Availability
I ask whether the factory offers design consultation before tooling is cut. The best plastic fabrication services partners will review my cross-section for extrudability, flag thin walls or sharp corners that trap stress, and suggest material substitutions that lower cost without hurting performance. I also confirm they can produce a representative prototype rather than pointing me straight to a production die.
Вақтҳои пешбарӣ, MOQs, and Delivery Track Record
Here I get specific. I ask for standard lead times on both tooling and production, the minimum order quantity, and how MOQ scales with material and profile complexity. Custom extrusion typically requires a one-time tooling investment for the die, while stock extruded shapes avoid that cost entirely (роҳнамоии манбаи саноат). If my volumes are modest, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (Пластикҳои SeaGate, 2024), so I always ask what stock profiles they carry. On delivery, I want on-time performance data, not adjectives.
References and Industry Experience
Дар охир, I ask for references in my industry. A shop that regularly serves medical, мошинсозй, or building-products customers has already navigated the tolerances and documentation those sectors demand. I call the references and ask two questions: did the parts meet spec on the first production run, and how did the supplier handle the problem when something went wrong?
From Prototype to Production: How the Process Unfolds
Once I have chosen a supplier, the path from a drawing to shippable extruded plastic parts follows a predictable sequence. Understanding each stage helps me set realistic timelines internally and catch problems while they are still cheap to fix.
Submitting Drawings and Design Consultation
I begin by sending a dimensioned drawing of the profile cross-section, along with the target material, ранг, tolerance requirements, and end-use environment. This is where design-for-manufacturing consultation earns its keep. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Захираҳои тарроҳии Protolabs, 2023), a good engineer will help me place critical dimensions where the process can reliably hold them and relax the ones that do not matter.
Sample and Prototype Validation
Next comes a sample or prototype. Depending on the shop, this may be pulled from a soft or temporary die, or matched from existing stock extruded shapes. I use this stage to validate fit, чандирӣ, анҷом додани сатҳи, and material behavior in my actual assembly. Catching a wall-thickness issue on a prototype costs me a revision; catching it after the production die is cut costs me the tooling.
Tooling Approval and First-Article Inspection
Extruder Twin Screw After I approve the design, the factory cuts the production die. The die design and tooling step is the largest one-time cost in custom extrusion, so I review the tooling drawing carefully before signing off. Once the die runs, I require a first-article inspection: a documented measurement of the initial output against my drawing. I do not release full production until the first article passes.
Ramping to Full Production
With the first article approved, the line ramps to full production. Plastic extrusion is a continuous, high-volume process well suited to long production runs (SPI/Plastics Industry Association overview), so unit costs typically drop as volume climbs. I confirm the quality plan for ongoing runs, including sampling frequency and the criteria for holding or scrapping out-of-spec material. Термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад (Агентии ИМА оид ба ҳифзи муҳити зист, 2023), so I also clarify the shop’s regrind policy when appearance or mechanical properties are critical.
Domestic vs Overseas Extrusion Sourcing
One of the most consequential decisions I make is where to source. The instinct is to compare unit price, but in my experience that number alone is misleading. What matters is total landed cost and the operational realities that price hides.
Cost vs Total Landed Cost Considerations
Overseas suppliers often quote a lower piece price, but I add freight, вазифахо, customs handling, and the inventory carrying cost of larger safety stock and longer transit. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023). Once I build a full landed-cost model, the gap between a domestic plastics manufacturer and an overseas one usually narrows, and sometimes reverses.
Lead Time, Фиристодан, and Communication Factors
Domestic sourcing shortens my supply chain and simplifies communication across time zones and languages, which matters most when I need quick-turnaround production or fast design changes. Overseas sourcing can suit stable, high-volume programs where the design is frozen and lead time is not a constraint.
Quality Control and IP Protection
Proximity makes on-site audits and first-article reviews far easier, and domestic contracts generally offer stronger, more enforceable intellectual property protection for a proprietary die design. When my profile represents real design investment, that protection weighs heavily.
When Each Option Makes Sense
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (Ассотсиатсияи саноати пластикӣ, 2023), and directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Томаснет, 2024), which makes local sourcing practical to research. The table below summarizes how I weigh the two paths.
| Омил | Domestic Sourcing | Overseas Sourcing |
|---|---|---|
| Unit price | Higher piece price | Often lower piece price |
| Арзиши умумии замин | Lower freight, вазифадор, and carrying cost | Added freight, вазифадор, and inventory cost |
| Lead time | Кӯтоҳтар, more responsive | Дарозтар, transit-dependent |
| Муошират | Same time zone and language | Time-zone and language gaps |
| Quality audits | On-site visits practical | Remote or costly to audit |
| Муҳофизати IP | Қавитар, more enforceable | Variable enforcement |
| Беҳтарин мувофиқ | Профилҳои фармоишӣ, fast changes, proprietary tooling | Frozen designs, very high volume, price-driven programs |
Дар амал, I lean domestic for custom plastic profiles that involve proprietary tooling, evolving designs, or short lead times, and I consider overseas contract manufacturing only for mature, устувор, high-volume parts where the landed-cost math clearly favors it. For a starting point on capabilities and stock offerings, resources like Пластикҳои SeaGate are a useful reference when scoping a domestic partner.
Sustainability and Recyclability in Extrusion
When I evaluate a plastic extrusion companies factory today, sustainability is no longer a soft preference tucked into the back of a proposal. It sits alongside price, вақти иҷрошуда, and quality as a core selection criterion. The good news is that extrusion is inherently well suited to responsible material use, and the suppliers I trust have built that advantage into their operations rather than treating it as an afterthought.
Recyclable Thermoplastics and Scrap Reuse
Most of the polymers I specify for extruded plastic parts are thermoplastics, which means they can be remelted and reformed multiple times without a complete loss of properties. According to the US Environmental Protection Agency (2023), термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад. That single characteristic separates them from thermosets and gives buyers real leverage on both cost and environmental footprint.
Дар амал, this recyclability spans the common resins you will encounter across quotes. PVC, HDPE, LDPE, and Polypropylene are among the workhorses of profile extrusion and plastic tubing, and each reclaims well when handled correctly. Engineering-grade plastics such as ABS, Поликарбонат, Нейлон (ПА), ва акрилӣ (PMMA) also tolerate controlled regrind, though I hold them to tighter blend ratios because their properties matter more in demanding applications. High-performance materials like PEEK and flexible TPE/TPU sit at the specialized end, where reuse requires more careful process control.
Regrind and Material Efficiency Practices
The continuous extrusion process generates predictable scrap: startup purge, trim from profile cross-section adjustments, and off-spec runs during die changeovers. A capable plastic profile manufacturer captures this material, granulates it into regrind, and reintroduces it at a defined percentage back into virgin resin. I always ask for the specifics because the details reveal how disciplined an operation really is.
- What regrind percentage do you blend into standard production, and does it change for cosmetic versus structural parts?
- How do you segregate resin types to prevent cross-contamination during resin extrusion?
- Can you document material traceability from raw resin through finished profile?
- Do you offer post-industrial recycled content options when my application allows it?
Co-extrusion deserves a mention here. By combining a virgin outer layer with a regrind or recycled core, some suppliers deliver the surface quality I need while lowering virgin material consumption. It is a practical way to reconcile appearance requirements with sustainability goals on the same part.
Choosing Environmentally Responsible Suppliers
Дар таҷрибаи ман, a domestic plastics manufacturer often carries a sustainability advantage that has nothing to do with marketing. The Reshoring Initiative (2023) notes that domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо, and shorter supply chains also mean lower transport emissions. When I compare a nearby US factory against overseas alternatives, the environmental and logistical benefits frequently reinforce each other.
Beyond geography, I look for suppliers whose quality systems formalize waste reduction. ISO 9001, described by the International Organization for Standardization (2015) as the internationally recognized standard for quality management systems, does not mandate sustainability by itself, but shops that maintain it tend to run tighter processes with less scrap and better material accountability.
Regulatory and Buyer Sustainability Expectations
My downstream customers increasingly ask about recycled content, chemical compliance, and end-of-life recyclability before they will approve a part. That pressure flows straight back to how I write specifications. Ҳоло ман ба ҳуҷҷатҳои устуворӣ ҳамчун як қисми натиҷаҳо муносибат мекунам, бонус нест. Вақте ки таъминкунанда метавонад ба ман шаҳодатномаҳои моддӣ диҳад, сиёсати аз нав баркарор кардан, ва маълумоти такрорӣ бидуни дудилагӣ, он нишон медиҳад, ки шарике омода аст, ки бозор ба куҷо меравад, на ба куҷое ки буд.
Қабули қарори ниҳоии худ ва дархости иқтибос
Вақте ки ман номзадҳоро ба рӯйхат гирифтам, Қарор ба мувофиқат кардани қобилиятҳои воқеии ҳар як таъминкунанда бар зидди ғайримуҷозоти лоиҳаи ман меояд. Бозори экструзия ихтисосро мукофот медиҳад, пас максад дарьёфт кардани корхонаи калонтарин ё зинат-ноктарин нест, балки онест, ки кувваи он бо хиссаи ман мувофик аст, ҷилди ман, ва ҷадвали ман.
Якҷоя кардани меъёрҳои арзёбии шумо
I bring my findings together into a single scorecard so I am comparing suppliers on the same terms. Даъвоҳо ба монанди “калонтарин” ё “беҳтарин” mean little in isolation; a large plastic extrusion companies factory tuned for high-volume commodity profiles may be the wrong fit for a low-volume, tight-tolerance engineering part, ва баръакс. The table below shows the weighting I typically apply, though I adjust it to the priorities of each program.
| Evaluation Criterion | Он чизе ки ман меҷӯям | Typical Weight |
|---|---|---|
| Material capability | Experience with my resin (PVC, HDPE, Поликарбонат, ва ғайра.) and co-extrusion if needed | Баланд |
| Тарҳрезии асбобҳо ва қолабҳо | In-house die design, tooling lead time, revision support | Баланд |
| Quality system | ISO 9001 certification and documented process controls | Баланд |
| Volume fit | Alignment of MOQ and capacity with my annual demand | Миёна |
| Lead time | Realistic tooling plus production schedule, quick-turnaround options | Миёна |
| Ҷойгиршавӣ | Domestic sourcing benefits, боркашонй, and responsiveness | Миёна |
| Устуворӣ | Regrind practices, мундариҷаи такрорӣ, пайгирии моддӣ | Rising |
Preparing a Clear RFQ Package
The quality of the quotes I receive is directly proportional to the quality of the request I send. A vague inquiry produces padded, cautious pricing; a complete RFQ produces sharp, comparable numbers. Extrusion carries specific cost drivers a supplier needs to see up front, chiefly the one-time tooling investment for custom profiles, which industry sourcing guidance confirms is avoided only when you use stock extruded shapes.
What Information to Include for Accurate Quotes
I make sure every RFQ package answers the questions a plastic fabrication services provider will otherwise have to ask, because each back-and-forth adds days to the timeline.
- A dimensioned drawing of the profile cross-section with tolerances. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming, per Protolabs (2023), I flag which dimensions are critical and which can float.
- Material specification, including resin type, grade, ранг, and any UV, flame, or food-contact requirements.
- Annual volume and order frequency, plus expected part length and cut tolerances.
- Whether I need custom tooling or can use a stock profile, and whether secondary operations such as cutting, мушт задан, or printing apply.
- Target price, required delivery date, and destination for landed-cost accuracy.
- Application and industry context, which helps the supplier recommend the right material and process.
Next Steps to Start Your Project
With the scorecard filled in and the RFQ ready, I send it to two or three well-matched suppliers rather than blasting a dozen. I ask for a sample or first-article inspection before committing to full production, and I confirm the tooling ownership terms in writing. Гузариш аз прототип ба истеҳсолот, ин дидаву дониста маро аз сюрпризҳои гаронбаҳо наҷот дод. Директорияҳо ба монанди Thomasnet (2024), ки истеҳсолкунандагони экструзияи пластикии ИМА-ро аз рӯи қобилият ва минтақа номбар ва гурӯҳбандӣ мекунанд, вақте ки ман бояд майдонро васеъ кунам, нуқтаи ибтидоии муфид боқӣ мемонад, ва экструдерҳои махсуси фармоишӣ ба монанди Пластикҳои SeaGate нишон диҳед, ки чӣ гуна профилҳои саҳҳомӣ ва қубурҳоро ба қисмҳои фармоишии камхарҷ сохтан мумкин аст.
Саволҳои зуд-зуд додашаванда
Инҳо саволҳое мебошанд, ки харидорон аксар вақт ҳангоми дарёфти шарики экструзия ба ман мепурсанд. Ман ҷавобҳоро мухтасар ва амалӣ нигоҳ доштам, то шумо метавонед ба онҳо зуд амал кунед.
Чӣ гуна метавонам як корхонаи ширкатҳои экструзияи пластикиро дар наздикии ман ё дар ИМА пайдо кунам?
Бо қобилият оғоз кунед, баъд аз рӯи ҷуғрофиё филтр кунед. I search supplier directories such as Thomasnet (2024) that categorize US plastic extrusion manufacturers by region and process, then cross-check each candidate’s material and volume fit. Choosing a domestic plastics manufacturer often pays off beyond convenience: the Reshoring Initiative (2023) reports that domestic sourcing can lower freight, вазифадор, ва хароҷоти интиқоли захираҳо, reducing total landed cost.
How much does custom plastic extrusion cost?
There are two cost layers. Custom profiles require a one-time tooling and die investment, after which per-part pricing depends on resin, ғафсии девор, output rate, ва ҳаҷм. Stock extruded shapes skip the tooling charge entirely, which is why I default to them when a standard profile meets the requirement. Зеро экструзия давомнок аст, раванди ҳаҷми баланд, unit costs typically fall as run length increases.
What is the difference between custom and stock extruded profiles?
Stock profiles are standard cross-sections a plastic profile manufacturer already produces, so they carry no tooling cost and short lead times, though the shape is fixed. Custom extrusion gives me a die designed to my exact profile cross-section, which is worth the tooling investment when the geometry, функсия, or branding demands it. Пластикҳои SeaGate (2024) also notes that standard profiles and tubes can be fabricated into cost-effective custom parts, a useful middle path when a full custom die is not justified.
How do I choose the right material for my extruded part?
I match the resin to the application. PVC is among the most widely extruded plastics for profiles, қубур, ва қубур. HDPE, LDPE, and Polypropylene serve well in chemical-resistant and flexible applications. When I need clarity, қувваи таъсир, or heat resistance, I move to engineering-grade plastics such as Polycarbonate, ABS, Акрилӣ (PMMA), or Nylon (ПА), and I reserve PEEK for extreme thermal and mechanical demands. Sharing your application and environment with the supplier is the fastest route to the right recommendation.
What certifications should a quality extrusion supplier hold?
ISO 9001 асоси ман аст. The International Organization for Standardization (2015) describes it as the internationally recognized standard for quality management systems used across manufacturing, and it is the most widely adopted quality standard in the plastics sector. Depending on your industry, you may also require food-contact, тиббй, or flame-rating compliance, so confirm those specifics against your application.
What mistakes should I avoid when sourcing an extrusion partner?
The most common ones I see are chasing “калонтарин” ё “беҳтарин” claims without checking fit, sending incomplete drawings that produce inflated quotes, and underestimating tooling lead time. I also caution against ignoring MOQ alignment; a factory built for high-volume manufacturing may not welcome low-volume work, and a small shop may struggle with your scale. Match the supplier to the job rather than the reputation.
What are the next steps once I have chosen a supplier?
Send a complete RFQ, request a sample or first-article inspection, confirm tooling ownership in writing, and agree on a realistic schedule that separates tooling time from production time. Validating the part before full production is the single most reliable way I have found to move from prototype to production without expensive rework.
What Is a Plastic Extrusion Companies Factory and Why It Matters for B2B Buyers
When I evaluate a plastic extrusion companies factory for a client, Ман аз худи раванд оғоз мекунам, because the process defines what a supplier can and cannot do for you. Экструзияи пластикӣ ашёи хоми пластикиро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад (Пластикҳои SeaGate, 2024). That single sentence carries more purchasing implications than most buyers realize: ба “fixed cross-section” is why extrusion excels at long, uniform shapes like tubing, тарм, ва каналҳо, and it is also why you cannot expect the same complex three-dimensional geometry you would get from molding.
Таъриф: What You Are Actually Buying
Дар шароити амалӣ, a plastic extrusion factory pushes softened resin through a shaped die to produce items such as custom plastic profiles, қубурҳои пластикӣ, and plastic sheet. Because this is a continuous extrusion process, it runs well for high-volume manufacturing and long production runs rather than one-off complex parts. The two categories I ask buyers to distinguish early Таъминкунандаи истеҳсоли пластикии Extrusion are stock extruded shapes, which are ready-made and avoid tooling, and custom extruded plastic parts, which require a die designed to your cross-section. Standard extruded profiles and tubes can also be fabricated into cost-effective custom parts with quick-turnaround production (Пластикҳои SeaGate, 2024), which is a useful middle path when a full custom die is not justified.
Market Context
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (Ассотсиатсияи саноати пластикӣ, 2023), so you are not sourcing from a niche trade. That scale matters for buyers: it means real competition among suppliers, redundancy if one plastic profile manufacturer cannot meet lead time, and a mature base of contract manufacturing and plastic fabrication services. It also means claims of being the “калонтарин” ё “беҳтарин” factory are marketing shorthand, not verified rankings. I treat those labels as prompts to ask about actual line capacity, сертификатсияҳо, and reference customers rather than as evidence.
Key Applications and Materials
Material selection drives most of the outcome, so I map the resin to the application before shortlisting any supplier. Common choices I see across projects include:
- PVC — among the most widely extruded plastics globally, Дар профилҳо маъмуланд, қубур, ва қубур (Ассотсиатсияи саноати пластикӣ).
- HDPE and LDPE — durable, chemically resistant polyethylenes used for tubing, лайнерҳо, and industrial profiles.
- Полипропилен — lightweight and fatigue-resistant, frequently chosen for living hinges and chemical handling.
- ABS and Polycarbonate — impact-resistant options for structural trim and enclosures; polycarbonate adds optical clarity and heat resistance.
- Акрилӣ (PMMA) — clarity and weatherability for lenses, намоиш медихад, and lighting profiles.
- Нейлон (ПА) ва PEEK — engineering-grade plastics for wear, ҳарорат, and mechanical demands; PEEK is the high-performance choice for aerospace and medical.
- TPE/TPU — flexible elastomers for seals, қубурҳо, and grips, often produced through co-extrusion with a rigid substrate.
Co-extrusion deserves special attention because it lets a factory combine two materials in one profile, for example a rigid PVC body with a soft TPE sealing lip. If your part needs both stiffness and flexibility, confirm the supplier runs true co-extrusion rather than secondary assembly.
Why This Matters for B2B Buyers
Understanding the process changes how you write a request for quote. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Протолабҳо, 2023), so specifying injection-molding-tight tolerances on an extruded profile will either inflate your price or trigger a round of clarifying questions that delays the quote. On sustainability, термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад (ИМА EPA, 2023), which gives you a legitimate lever for both cost and environmental goals when you discuss regrind percentages with a supplier.
How to Choose the Right Plastic Extrusion Companies Factory Supplier
Choosing a supplier is where I see the most avoidable mistakes, usually because buyers compare on unit price alone and ignore the cost drivers hiding behind that number. Below is the framework I use, built around evaluation criteria, red flags, and a due diligence checklist you can lift directly into your sourcing process.
Vendor Evaluation Criteria
I score candidates against five dimensions rather than a single quote:
- Capability match. Does the factory routinely run your resin and profile size? A plastic tubing supplier optimized for small-diameter medical tubing is not the same shop as one running large architectural profile extrusion.
- Quality systems. ISO 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад (ISO, 2015) and remains the most widely adopted quality standard in the plastics sector. Certification is not a guarantee of good parts, but its absence tells me to dig deeper into inspection practices.
- Тарҳрезии асбобҳо ва қолабҳо. Ask who owns the die, how long die design and tooling take, and what happens to the tool if you leave. Ownership terms are frequently buried in fine print.
- Lead time and capacity. Confirm whether quoted lead times reflect current backlog or ideal conditions. Quick-turnaround production claims should be tied to a specific committed date.
- Financial and operational stability. A supplier that becomes your sole source for a critical profile is a risk if it is financially fragile.
Understanding the Cost Drivers
Transparency on cost structure separates a strong plastic profile manufacturer from an opaque one. Three drivers determine your total price, and I ask suppliers to break them out explicitly:
| Cost driver | Stock extruded shapes | Custom extruded profiles |
|---|---|---|
| Асбобсозӣ / die investment | None — profile already exists | One-time die cost required before first run (роҳнамоии манбаи саноат, Thomasnet supplier guides) |
| Миқдори ҳадди ақали фармоиш (MOQ) | Кам; buy by the length | Баландтар; tied to setup and material changeover |
| Lead time | Short — often shelf stock | Дарозтар; includes die fabrication and first-article approval |
| Per-unit price at volume | Fixed by catalog | Lower at high volume once tooling is amortized |
| Беҳтарин мувофиқ | Prototyping, ҳаҷми паст, standard cross-sections | Proprietary geometry, high-volume manufacturing, prototype to production scale-up |
Custom extrusion typically requires a one-time tooling investment, дар ҳоле ки профилҳои саҳҳомӣ аз ин хароҷот канорагирӣ мекунанд (роҳнамоии манбаи саноат). Дар таҷрибаи ман, buyers who plan to scale from prototype to production should quote the custom die early even if they start with stock shapes, so the amortized per-unit price is visible before volumes ramp.
Red Flags I Watch For
- Refusal to share ISO or equivalent quality documentation, or vague answers about inspection frequency.
- Quotes with no tooling line item, which usually means the cost reappears later or the die is undersized.
- Unwillingness to provide references in your industry or sample parts.
- Tolerances promised on paper that are tighter than what continuous extrusion realistically holds — a sign the supplier may be overselling.
- “Largest” ё “беҳтарин” claims with no capacity data, сертификатсияҳо, or customer evidence behind them.
Due Diligence Checklist
Before I commit to a Plastic Extrusion Companies Factory supplier, I confirm every item below in writing:
- Do you hold ISO 9001 or an equivalent, and can I see the certificate and scope?
- Which resins do you run in production, and can you handle my material — PVC, ABS, поликарбонат, HDPE, LDPE, полипропилен, or an engineering grade?
- What tolerances do you guarantee for this profile cross-section, and how are they measured?
- What is the tooling cost, вақти иҷрошуда, and MOQ, and who owns the die?
- Do you offer co-extrusion and secondary fabrication in-house?
- What percentage of regrind is used, and how does that affect certification and appearance?
- Can you provide first-article inspection reports and material certifications?
- What is your realistic committed lead time given current backlog?
Find Plastic Extrusion Companies and Factories in the United States
Buyers frequently search for a plastic extrusion factory “дар наздикии ман” ё “in the USA,” and the location question is more strategic than it first appears. Domestic sourcing is not only about proximity; it changes your total landed cost and your supply-chain risk profile.
Where to Start Your Search
Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Томаснет, 2024), which makes them a practical first filter when you want to build a shortlist by material, раванд, or state. I pair directory research with capability-specific sources such as custom plastic extrusion manufacturer references to understand what a given shop actually produces before I reach out. The goal at this stage is a shortlist of five to eight candidates whose capabilities genuinely match your resin and profile, not a long list of names. Ширкатҳои экструзияи пластикӣ
Key Considerations for Domestic Sourcing
Reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023). For extruded parts, which are often bulky and low in value density, freight is a meaningful line item, so a domestic plastics manufacturer closer to your assembly point can offset a higher unit price. I weigh three factors:
- Арзиши умумии замин, на нархи воҳид. Add freight, вазифадор, and the carrying cost of the safety stock you need to cover long overseas transit.
- Communication and design iteration. Domestic time-zone alignment speeds up die design and tooling revisions during the prototype-to-production phase.
- Supply resilience. Shorter lines reduce exposure to port delays and long lead-time shocks.
Interpreting “Largest” ва “Best” Factory Claims
Location searches often surface superlatives, and I treat them skeptically. “Largest” tells you nothing about whether a factory runs your material or holds your tolerances. Ба ҷои ин, I convert vague claims into verifiable questions: How many extrusion lines run my resin family? What is your on-time delivery rate? Which certifications do you hold? A smaller shop that specializes in your profile is frequently a better partner than a large one for which your job is an afterthought.
Practical Tips and Industry Context
A few habits have consistently saved my clients time and money. Аввал, request stock extruded shapes for early validation before investing in a custom die — it lets you test fit and function cheaply. Дуюм, share a dimensioned drawing with realistic extrusion tolerances up front so quotes are comparable. Сеюм, confirm the supplier’s regrind policy, since recyclable thermoplastics and regrind reuse improve material efficiency (ИМА EPA, 2023) but can affect appearance on cosmetic parts. Дар охир, remember that plastic extrusion is a continuous, high-volume process well suited to long production runs, so it rewards buyers who can consolidate demand and forecast accurately. Within the mature US plastics manufacturing base (Ассотсиатсияи саноати пластикӣ, 2023), you have room to be selective — use it, and let a structured checklist rather than a headline claim decide your Plastic Extrusion Companies Factory supplier.
Locate a plastic extrusion factory near my location
When buyers ask me how to find a plastic extrusion factory nearby, I remind them that “дар наздикии ман” is really shorthand for two goals: shorter freight lanes and easier communication. Extrusion melts raw plastic material and forms it into a continuous profile with a fixed cross-section (Пластикҳои SeaGate, 2024), and because that continuous extrusion process runs at high volume, the finished product is often bulky and freight-sensitive. Дар таҷрибаи ман, the cost of moving extruded plastic parts across the country can quietly erode the price advantage of a distant supplier, so location genuinely matters.
Key considerations for local sourcing
I start every local search by matching capability to geography rather than proximity alone. A plastic profile manufacturer two states away with the right die design and tooling almost always beats a closer shop that cannot hold your profile cross-section. I evaluate three things in order: the materials they run (PVC, ABS, поликарбонат, HDPE, LDPE, полипропилен, акрилӣ, and engineering-grade resins such as nylon or PEEK), the processes they offer (экструзияи профил, экструзияи варақи пластикӣ, қубур, ва коэкструзия), and their quality systems. ISO 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад (ISO, 2015), so I treat certification as a baseline filter, бонус нест.
Practical tips to find and vet a factory
Thomasnet supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Томаснет, 2024), which makes them a reliable starting point for a location-based shortlist. Аз он чо, I qualify each candidate with a consistent set of questions before I ever request a quote.
My local supplier vetting checklist
- Which resins do you extrude in-house, and can you run regrind for material efficiency?
- Do you offer co-extrusion or dual-durometer profiles if my part needs a soft-touch or barrier layer?
- What tolerances can you hold, and how do you document them?
- Are you ISO 9001 тасдиқ карда шудааст, and can you share a recent audit summary?
- What is your typical lead time from approved die to first article?
- Do you provide plastic fabrication services (буридан, мушт задан, пармакунй) so I receive finished parts, not just stock lengths?
Industry context
Domestic proximity is more strategic than it looks. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023). Because the US plastics industry is a major contributor to domestic manufacturing shipments and employment (Ассотсиатсияи саноати пластикӣ, 2023), most regions have a viable domestic plastics manufacturer within a reasonable freight radius. I tell buyers that “дар наздикии ман” should mean near enough to control landed cost and lead time, which is often a regional rather than a strictly local decision.
Identify the largest plastic extrusion companies in the US
Buyers frequently ask me to point them to the “калонтарин” ширкатҳои экструзияи пластикӣ, and my first move is always to define what “калонтарин” means for their project. Size can describe revenue, plant footprint, number of extrusion lines, or annual resin throughput, and those metrics do not always move together. A plastic extrusion companies factory supplier with enormous pipe capacity may be the wrong fit for a low-volume acrylic profile, so I interpret scale through the lens of the specific job.
Key considerations when “калонтарин” муҳим аст
Scale earns its keep on long production runs. Plastic extrusion is a continuous, high-volume process well suited to long production runs, so the largest producers shine when you need millions of feet of PVC profile or HDPE pipe on a predictable schedule. PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, одатан дар профилҳо истифода мешаванд, қубур, ва қубур, which is why the biggest players tend to concentrate capacity there. If your program is high-volume and standardized, a large plastic profile manufacturer offers redundancy, buffer inventory, and pricing leverage. If your program is small or highly custom, that same scale can translate into higher minimums and less flexibility.
Practical tips for evaluating scale claims
I never take a marketing claim of “калонтарин” at face value. Ба ҷои ин, I ask for concrete indicators: number of extrusion lines by size class, resins run at volume, and the split between stock extruded shapes and custom work. A large firm quoting a wholesale program should be able to show quick-turnaround production capacity, secondary plastic fabrication services, and a documented MOQ structure. The table below summarizes how I weigh large versus specialized suppliers.
Large versus specialized extrusion suppliers
| Омил | Largest producers | Specialized suppliers |
|---|---|---|
| Беҳтарин мувофиқ | Ҳаҷми баланд, standardized runs (қубур, Профили PVC) | Custom plastic profiles, engineering-grade resins |
| Миқдори ҳадди ақали фармоиш | Higher MOQ to justify line time | Lower MOQ, more flexible |
| Арзиши асбобҳо | Amortized across large volumes | One-time die cost more visible per unit |
| Lead time | Predictable, buffered by capacity | Тағйирёбанда, project-dependent |
| Material range | Commodity resins (PVC, HDPE, LDPE, PP) | Specialty resins (Компютер, PMMA, ПА, PEEK, TPE/TPU) |
| Ко-экструзия | Common on standard lines | Often available for niche multi-layer parts |
Industry context
The largest US extruders are anchored in commodity, freight-heavy products where continuous, high-volume manufacturing rewards efficiency. Custom extrusion typically requires a one-time tooling or die investment, дар ҳоле ки профилҳои саҳҳомӣ аз ин хароҷот канорагирӣ мекунанд, so large producers often lead with catalogs of stock extruded shapes. I remind buyers that “калонтарин” is a useful signal for reliability and capacity, but it is not a proxy for quality or fit. The right size is the one that matches your volume, материал, and tolerance needs.
Discover the best-rated plastic extrusion manufacturers
“Best-rated” is the claim I scrutinize most, because ratings can reflect genuine performance or simply strong marketing. Дар таҷрибаи ман, the manufacturers worth shortlisting are the ones that make their quality measurable. I look past star counts and testimonials for evidence I can verify: сертификатсияҳо, documented tolerances, пайгирии моддӣ, and a track record of moving projects from prototype to production without surprises.
Key considerations for judging quality
Quality management is the foundation. ISO 9001 is the most widely adopted quality management standard, used across manufacturing sectors including plastics, so I treat it as table stakes for a best-rated plastic extrusion companies factory manufacturer. Beyond certification, I assess how a supplier handles tolerances. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Протолабҳо, 2023), and the best manufacturers explain that reality up front rather than overpromising. A shop that gives me realistic tolerance ranges and a clear inspection plan earns more trust than one quoting numbers it cannot hold.
Practical tips for choosing the best-rated supplier
I use a material selection framework tied to the application. The resin drives the manufacturer, not the other way around.
- PVC — profiles, қубур, and tubing where cost and rigidity matter.
- ABS and polycarbonate — impact-resistant parts; polycarbonate adds clarity and heat tolerance.
- HDPE and LDPE — chemical resistance and flexibility for tubing and liners.
- Полипропилен — lightweight parts needing fatigue and chemical resistance.
- Акрилӣ (PMMA) — optical clarity for lighting and display profiles.
- Нейлон (ПА) ва PEEK — engineering-grade parts under mechanical or thermal stress.
- TPE/TPU — flexible seals and gaskets, often via co-extrusion.
Once the material is set, I confirm the supplier offers the matching process, whether that is profile extrusion, экструзияи варақи пластикӣ, or resin extrusion with co-extrusion for multi-layer parts. Профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд (Пластикҳои SeaGate, 2024), so I favor manufacturers that pair extrusion with in-house fabrication and prototype-to-production support. For a working example of custom capability and stock profile options, I point buyers to references such as Пластикҳои SeaGate.
Industry context
The best-rated manufacturers increasingly compete on sustainability alongside quality. Термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад (ИМА EPA, 2023), so I ask top candidates how they manage scrap and regrind. A manufacturer that documents its quality system, states honest tolerances, and runs an efficient material loop tends to be “best-rated” for reasons that hold up under a plant visit. That is the standard I apply, and it is the one I recommend every buyer use before committing to a contract manufacturing partner.
Understand how the plastic extrusion manufacturing process works
Вақте ки ман як истеҳсолкунандаи профили пластикиро арзёбӣ мекунам, I start by making sure the buyer understands what actually happens on the shop floor. Экструзияи пластикӣ ашёи хоми пластикиро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад (Пластикҳои SeaGate, 2024). That single sentence carries most of what you need to know: the process is continuous, the cross-section is constant along the length, and the shape is defined by tooling rather than by a closed mold.
The core stages of the continuous extrusion process
Дар амал, I describe the workflow in five stages. Аввал, resin pellets are fed into a hopper. Дуюм, a heated barrel with a rotating screw melts and pressurizes the material, which is why practitioners often call it resin extrusion. Сеюм, the molten polymer is forced through a die that establishes the profile cross-section. Чорум, the extrudate is cooled in a water bath or air rack so it holds its geometry. Панҷум, pullers draw the part at a steady rate before a saw or cutter sizes it. Because nothing stops between stages, the method is genuinely a continuous extrusion process rather than a cycle-by-cycle one.
Why tolerances differ from injection molding
One point I raise early with engineering teams: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Захираҳои тарроҳии Protolabs, 2023). This is not a defect. It reflects the physics of pulling a hot polymer through open tooling and cooling it under tension. If your extruded plastic parts need tight dimensional control on a specific feature, plan for secondary machining or specify that feature as a fabrication step rather than expecting the die alone to hold it.
Co-extrusion and profile extrusion variants
Profile extrusion covers the custom cross-sections most buyers picture: каналхо, қубурҳо, ороишҳо, ва шаклҳои сохторӣ. Co-extrusion runs two or more materials through the die at once, which lets you combine, барои намуна, a rigid PVC body with a flexible TPE/TPU sealing lip in a single pass. I find co-extrusion is where a capable factory earns its rate, because it removes a downstream assembly step and improves seal performance. Plastic sheet extrusion and tubing use the same fundamentals with different die and downstream setups.
Industry context and material efficiency
Extrusion suits high-volume manufacturing because it is inherently a continuous, high-volume process well suited to long production runs. Once a die is dialed in, output scales with line speed and run time. It also has a reasonable sustainability story: термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад (ИМА EPA, 2023). Дар таҷрибаи ман, asking a supplier how they handle regrind tells you a lot about both their cost discipline and their process control.
Compare custom vs stock plastic extrusion suppliers
The most consequential sourcing decision I help buyers make is custom versus stock. It drives your tooling cost, миқдори ҳадди ақали фармоиш, and lead time all at once. The right answer depends on how closely a standard shape fits your application and how much volume you expect to run.
What separates the two paths
Экструзияи фармоишӣ маъмулан як василаи якдафъаина ва сармоягузориро талаб мекунад, дар ҳоле ки профилҳои саҳҳомӣ аз ин хароҷот канорагирӣ мекунанд. Профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд (Пластикҳои SeaGate, 2024). So there is a middle path many buyers miss: start from a stock extruded shape and fabricate it, capturing part of the customization benefit without paying for a new die.
Cost drivers to model before you request a quote
When I build a sourcing model, I separate three drivers so the numbers stay honest:
- Die design and tooling: a one-time cost on custom work, typically amortized across your first order or two.
- MOQ: custom lines carry higher minimums to justify setup and purge material; stock shapes can ship in small quantities.
- Lead time: stock ships quickly; custom adds die fabrication and first-article approval before production begins.
Ҷадвали муқоиса: custom vs stock extrusion
| Омил | Custom profile extrusion | Stock extruded shapes |
|---|---|---|
| Арзиши асбобҳо | One-time die investment required | Ҳеҷ |
| Миқдори ҳадди ақали фармоиш | Баландтар, to amortize setup | Кам, often cut-to-length |
| Lead time | Дарозтар (месозанд + мақолаи аввал) | Quick-turnaround production |
| Dimensional fit | Exact cross-section to spec | Nearest standard, plus fabrication |
| Беҳтарин барои | Sustained volume, unique geometry | Прототипҳо, ҳаҷми паст, near-fit needs |
| Unit price at scale | Пас аз амортизатсияи асбобҳо пасттар мешавад | Higher per unit for heavy customization |
A vetting checklist for either path
Whether you pursue a custom plastic profile manufacturer or a stock plastic tubing supplier, I ask the same core questions. Is the shop certified to ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015)? ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics, so its absence is worth a direct conversation. Beyond certification, I ask:
- Which resins do you run in-house, and can you handle engineering-grade plastics like polycarbonate, нейлон (ПА), or PEEK?
- Do you offer co-extrusion and downstream plastic fabrication services?
- How do you document tolerances and first-article inspection?
- What is your true MOQ, and how is tooling amortized on the initial order?
- Can you support the move from prototype to production without re-tooling?
Location intent: near me and in the USA
Buyers frequently search for a Plastic Extrusion Companies Factory supplier “дар наздикии ман” or a domestic plastics manufacturer in the USA. Two resources help here. Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Томаснет, 2024), which is a practical starting point for shortlisting. And the case for domestic sourcing is more than convenience: reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023). I treat “калонтарин” ва “беҳтарин” factory claims with skepticism; capability fit for your specific resin, таҳаммулпазирӣ, and volume matters far more than a superlative on a homepage.
Learn what products can be made through plastic extrusion
Extrusion produces a broader range of products than most buyers expect, and the material you choose shapes both what is possible and what it costs. I organize my recommendations around a material selection framework tied to application and industry rather than a generic parts list.
Common extruded product categories
The workhorse outputs are custom plastic profiles, қубур, варақ, каналхо, ороишҳо, қубурҳо, ва шаклҳои сохторӣ. Anything with a consistent profile cross-section along its length is a candidate. PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, одатан дар профилҳо истифода мешаванд, қубур, ва қубур (Ассотсиатсияи саноати пластикӣ). That prevalence is why so many stock extruded shapes are available in PVC first.
Material selection framework
Here is how I match resins to needs across the polymers you will encounter most often:
- PVC: иқтисодӣ, rigid or flexible, strong for profiles, қубур, ва қубур.
- ABS: tough and impact-resistant, common in housings and trims.
- Поликарбонат: high impact strength and clarity for glazing and guards.
- HDPE and LDPE: полиолефинхои аз чихати химиявй тобовар барои трубахо, лайнерҳо, ва профилҳои камхарҷ; HDPE сахтии бештар меорад, LDPE чандирии бештар.
- Полипропилен: нур, ба химия тобовар, ва ба хастагӣ таҳаммулпазир барои ҳалқаҳо ва профилҳои зиндагӣ.
- Акрилӣ (PMMA): равшании оптикӣ барои профилҳои намоиш ва равшанӣ.
- Нейлон (ПА): муқовимат ва қувват барои қисмҳои механикӣ фарсуда.
- PEEK: ҳарорати баланд, пластикаи муҳандисии аз ҷиҳати кимиёвӣ мустаҳкам барои корҳои аэрокосмосӣ ва тиббӣ серталаб.
- TPE/TPU: эластомерҳои чандир барои мӯҳрҳо ва лабҳои ко-экструдсионии нарм мувофиқанд.
Барномаҳои саноатӣ
Сохтмон ба профилҳои PVC ва ABS барои чаҳорчӯбаи тиреза такя мекунад, ороишҳо, ва канор. Корҳои тиббӣ ва лабораторӣ акрилро истифода мебаранд, полипропилен, ва қубурҳо ва каналҳои PEEK. Электроника ва асбобҳо дар корпусҳои поликарбонат ва ABS истифода мешаванд. Хатҳои саноатӣ ва коркарди моеъ ба HDPE ва нейлон такя мекунанд. Харитасозии саноати худ ба ин қатронҳо барвақттар сӯҳбати иқтибосҳоро мутамарказ нигоҳ медорад ва аз нишон додани маводи аз ҳад зиёди муҳандисии ба шумо лозим нест..
Маслиҳатҳои амалӣ барои гузаштан аз консепсия ба истеҳсолот
Дар таҷрибаи ман, се одат лоиҳаҳои экструзияро дар ҷадвал нигоҳ медоранд. Аввал, прототип аз шаклҳои саҳҳомӣ, ки геометрия имкон медиҳад, пас танҳо пас аз тасдиқи тарҳ ба асбобҳои фармоишӣ итоат кунед, ки сармоягузории марги шуморо муҳофизат мекунад. Дуюм, Муайян кардани таҳаммулпазирӣ аз рӯи хусусият, на кӯрпаро пурзӯр кардани тамоми профил, зеро ин равандро эҳтиром мекунад ва хароҷотро назорат мекунад. Сеюм, тасдиқ кунед, ки таъминкунандаи шумо метавонад қисмро аз прототип ба истеҳсол дар як хат интиқол диҳад, аз ин рӯ, миқёси боло иқтибосро маҷбур намекунад. Ин тавр рафтор кард, экструзия қисмҳои фармоиширо аз ҷиҳати иқтисодӣ таъмин мекунад, бо гардиши зуд, ки ин равандро дар ҷои аввал ҷолиб мегардонад.
For a deeper look at fabricating cost-effective custom parts from standard and custom profiles, I point buyers to Пластикҳои SeaGate’ extrusion overview.
Bringing Your Extrusion Sourcing Strategy Together
After walking through capabilities, масолех, and vetting criteria, the through-line I keep returning to is this: choosing among plastic extrusion companies and factories is less about finding the “калонтарин” ё “беҳтарин” name and more about matching a supplier’s real strengths to your specific part, ҳаҷми, ва ҷадвали вақт. A continuous, high-volume manufacturing process rewards long production runs, but the same shop that excels at a million linear feet of PVC profile may not be the partner I want for a low-volume PEEK prototype. Дар таҷрибаи ман, buyers who define the problem precisely before they request quotes get sharper pricing and fewer surprises downstream.
Material selection sits at the center of every good decision. Whether the application calls for rigid PVC or ABS in structural profiles, polycarbonate or acrylic (PMMA) барои равшании оптикӣ, HDPE ва LDPE барои муқовимати кимиёвӣ, полипропилен барои болгахои зинда, нейлон (ПА) for wear surfaces, or TPE/TPU for flexible seals, the resin drives tooling, таҳаммулпазирӣ, ва арзиш. Extrusion melts raw plastic and forms it into a continuous profile with a fixed cross-section (Пластикҳои SeaGate, 2024), ва профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд (Пластикҳои SeaGate, 2024). That combination of stock shapes and custom profile extrusion, sometimes paired with co-extrusion for multi-material geometry, is what makes the process so versatile from prototype to production.
On the commercial side, I always separate one-time and recurring costs. Custom extrusion typically carries a one-time tooling and die investment, while stock profiles avoid it, so the die design and tooling decision shapes the whole business case. Domestic sourcing deserves a second look too: reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023), which often narrows the gap that offshore unit pricing appears to open. And because thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (ШМА. EPA, 2023), a quality-focused domestic plastics manufacturer can support both cost and sustainability goals at once.
Quality systems are the final filter I apply. ISO 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад (ISO, 2015), and it remains the most widely adopted benchmark I look for when comparing a custom plastic extrusion manufacturer against its peers. Pair that with realistic expectations on precision, since extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Протолабҳо, 2023), and you have a grounded framework for evaluating any plastic profile manufacturer or plastic tubing supplier.
Мутахассиси фаҳмиш
| Нуқтаи асосӣ | Шарҳ |
|---|---|
| Match process to volume, not to reputation | Continuous extrusion is a high-volume process best suited to long production runs, so I weigh a factory’s real strengths against my order size rather than chasing “калонтарин” ё “беҳтарин” claims. |
| Separate tooling from unit price | Custom profiles require a one-time die investment while stock extruded shapes avoid it; understanding this split keeps the true cost of custom plastic profiles from hiding inside a quoted per-foot rate. |
| Verify quality before precision expectations | ISO 9001 сертификатсия (ISO, 2015) signals a managed process, and I set tolerance expectations knowing extrusion runs looser than injection molding (Протолабҳо, 2023). |
Маслиҳатҳо оид ба таъминоти амалӣ барои харидорони B2B
- Define the part before you shop. Document the profile cross-section, қатрон (PVC, ABS, поликарбонат, HDPE, полипропилен, or an engineering-grade plastic), ҳаҷми солона, and target tolerance so every plastic extrusion companies factory supplier quotes against the same brief.
- Ask for tooling, MOQ, and lead-time numbers separately. Request the die cost, миқдори ҳадди ақали фармоиш, and quoted lead time as distinct line items to compare custom extrusion and stock profiles on equal footing.
- Confirm the quality system in writing. Ask for a current ISO 9001 certificate and the inspection points used on extruded plastic parts, rather than accepting a general quality claim.
- Weigh domestic sourcing on total landed cost. Compare a domestic plastics manufacturer against offshore options using freight, вазифадор, ва хароҷоти интиқоли захираҳо, на танҳо нархи воҳид (Ташаббуси барқарорсозӣ, 2023).
- Test the relationship with a small run. Move from prototype to production in stages so you validate quick-turnaround performance and communication before committing to high-volume manufacturing.
- Use supplier directories as a starting list, рӯйхати кӯтоҳ нест. Директорияҳо ба монанди Thomasnet (2024) help you locate regional plastic fabrication services, but I still vet capability, масолех, and certification directly with each shop.
Саволҳои зиёд такрормешуда
How do I find plastic extrusion companies or a factory near me?
When I evaluate location intent, I start by mapping suppliers against my shipping lanes rather than pure geographic proximity. A plastic profile manufacturer two states away with the right die design and tooling capability often beats a closer shop that lacks my resin. I use supplier directories that list and categorize US plastic extrusion manufacturers by capability and region to build a shortlist, then verify with a plant visit or video walkthrough. Thomas directories are a practical starting point for this (Томаснет, 2024, thomasnet.com). Дар таҷрибаи ман, “дар наздикии ман” should mean short, predictable lead times and low freight, not just a nearby ZIP code.
What should I look for in plastic extrusion manufacturers in the USA?
For domestic sourcing, I weigh three things: certified quality, material breadth, and total landed cost. A domestic plastics manufacturer can reduce total landed cost by lowering freight, вазифадор, ва хароҷоти интиқоли захираҳо (Ташаббуси барқарорсозӣ, 2023, reshorenow.org), which often narrows the gap with offshore quotes once you account for the full picture. The US plastics industry is also a major contributor to domestic manufacturing shipments and employment (Ассотсиатсияи саноати пластикӣ, 2023), so the supplier base is deep. I confirm they run the resins I need, from commodity grades like PVC, HDPE, LDPE, and polypropylene to engineering-grade plastics such as polycarbonate, нейлон (ПА), ва PEEK.
How do I choose the right plastic extrusion supplier for my project?
I treat supplier selection as a vetting checklist, not a gut call. The concrete questions I ask every candidate:
- Do you hold ISO 9001 сертификатсия, the internationally recognized standard for quality management systems (ISO, 2015)?
- Which resins and profiles do you run in production, and do you offer co-extrusion?
- What are your tolerances, and how do you handle profile cross-section validation?
- What is your minimum order quantity (MOQ), tooling lead time, and production lead time?
- Can you support the full path from prototype to production and quick-turnaround production for reorders?
Industrial Plastic Extrusion Parts The biggest mistake I see buyers make is choosing on unit price alone and ignoring tooling cost, MOQ, and lead-time risk. Those drivers usually decide whether a program is actually profitable.
What is the difference between custom and stock plastic extrusions?
Stock extruded shapes are standard profiles and tubes a supplier already produces, so you skip tooling and buy off the shelf. Custom extrusion requires a one-time tooling and die investment to create your unique profile cross-section. Мубодила рост аст: stock plastic extrusions minimize upfront cost and lead time, while custom plastic profiles fit your exact geometry. Махсусан, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (Пластикҳои SeaGate, 2024, seagateplastics.com), so I often prototype with stock shapes before committing to a die.
How should I read “калонтарин” ва “беҳтарин” plastic extrusion factory claims?
I read those labels with healthy skepticism. “Largest” usually reflects capacity or revenue, which matters for high-volume manufacturing but tells me nothing about fit for a low-volume, tight-tolerance job. “Best” is subjective marketing unless it is backed by certifications, маълумотномаҳо, and capability data. Қоидаи ман: rank suppliers against my own requirements, not against a generic superlative. The largest plastic extrusion company on a list may be the wrong contract manufacturing partner for a specialty acrylic (PMMA) or TPE/TPU part, while a mid-size specialist nails it.
What are plastic extrusion profiles, and how are they made?
A profile is a continuous shape with a fixed cross-section. Экструзияи пластикӣ ашёи хоми пластикиро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад (Пластикҳои SeaGate, 2024). Because it is a continuous forming process, resin extrusion is well suited to long production runs and high-volume manufacturing. It also supports plastic sheet extrusion and tubing. One thing I always plan around: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Захираҳои тарроҳии Protolabs, 2023), so I set tolerance expectations early with the plastic tubing supplier or profile shop.
Which plastic material should I choose for my extruded parts?
I anchor material selection to the application, not habit. PVC is among the most widely extruded plastics globally and is common in profiles, қубур, ва қубур. For impact and appearance, I look at ABS or polycarbonate; for chemical resistance and living hinges, полипропилен; for outdoor and clarity, акрилӣ (PMMA); and for demanding thermal or wear conditions, нейлон (ПА) or PEEK. I also confirm recyclability up front, since thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (ИМА EPA, 2023). Matching resin to service environment prevents the costly redesigns I have watched derail otherwise solid programs.
What drives the cost of extruded plastic parts?
Three levers move price more than anything else. Аввал, асбобсозй: a custom die is a one-time investment that stock profiles avoid entirely. Дуюм, MOQ and run length, since extrusion rewards volume and unit cost drops as quantities rise. Сеюм, material grade, where engineering-grade plastics and specialty resins cost well above commodity options. When I request a quote, I ask suppliers to break out tooling, per-unit price, and secondary plastic fabrication services separately so I can compare offers on equal terms and identify where the real cost lives.
Иқтибосҳо
- Экструзияи пластикӣ ашёи хоми пластикиро гудохта, онро ба профили доимӣ бо буриши собит ташкил медиҳад. — Пластикҳои SeaGate (2024)
- Профилҳо ва қубурҳои стандартии истихроҷшуда метавонанд ба қисмҳои фармоишии камхарҷ бо гардиши зуд сохта шаванд. — Пластикҳои SeaGate (2024)
- ISO 9001 стандарти дар сатҳи байналмилалӣ эътирофшуда барои системаҳои идоракунии сифат дар истеҳсолот истифода мешавад. — Ташкилоти байналхалқии стандартизатсия (2015)
- The US plastics industry is a major contributor to domestic manufacturing shipments and employment. — Ассотсиатсияи саноати пластикӣ (2023)
- Reshoring and domestic sourcing can reduce total landed cost by lowering freight, вазифадор, and inventory carying costs. — Ташаббуси барқарорсозӣ (2023)
- Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming. — Захираҳои тарроҳии Protolabs (2023)
- Термопластикае, ки дар экструзия истифода мешаванд, такроран истифода мешаванд, ва аз нав истифода бурдани дубора самаранокии моддиро беҳтар мекунад. — Агентии ИМА оид ба ҳифзи муҳити зист (2023)
- Thomas suplier directories list and categorize US plastic extrusion manufacturers by capability and region. — Томаснет (2024)
- Plastic extrusion is a continuous, high-volume process well suited to long production runs, per general industry manufacturing references (SPI/Plastics Industry Association overview). — Planning analysis
- PVC яке аз пластикҳои аз ҳама васеъ экструдсияшуда дар саросари ҷаҳон мебошад, одатан дар профилҳо истифода мешаванд, қубур, ва қубур (Ассотсиатсияи саноати пластикӣ). — Planning analysis