

Viktiga takeaways
- Enligt min erfarenhet, de smartaste grossistbesluten börjar med att matcha maskinklass med råvara: extruders med enkel skruv hanterar enkel PVC, HDPE, och polypropenprofiler, tvillingskruvextrudrar passar sammansatta och krävande polymerer, och dedikerade plaståtervinningsextrudrar finns som en distinkt klass för återvunna plastflingor (källa: ThoYu, 2024).
- Jag utvärderar alltid specifikationer före pris. Kärnnummer som L/D-förhållandet, antal fatzoner, växellådans reduktionsförhållande, servicefaktor, och motorhästkrafter berättar mycket mer om verklig kapacitet än en total effektsiffra. För referens, en begagnad Davis Standard 9-tums extruder par a 32:1 L/D-förhållande och 7-zoners pipa med en 900 HP DC-motor (källa: Aaron Utrustningslista).
- Fabriksdirekta priser från Kina-baserade tillverkare är verkligen konkurrenskraftiga för ny utrustning (källa: ThoYu, 2024), men jag väger det mot en total total ägandekostnadsbild som inkluderar importtullar, sjöfrakt, tackling, installation, och tillgång till eftermarknadssupport.
- Jag behandlar nya, begagnad, och importeras som tre separata upphandlingsspår, var och en med sina egna avvägningar. Begagnatmarknaden har mognat, varumärkesspecifika listor för extruders med en skruv (källa: Aaron utrustning), vilket gör det till en gångbar väg när jag kan verifiera skick och slitage.
- Leverantörskontroll och betalningsskydd har lika stor betydelse som specifikationsbladet. Innan du begår, Jag bekräftar minsta beställningskvantitet, ledtider, garantivillkor, och tillgång till reservdelar, och jag strukturerar betalningar för att skydda mot utebliven leverans.
- Processgrunderna styr mina kontroller: råvaran kommer in genom en trattmatare i pulver, pellets, eller granulatform, smälts av elektriska värmerör, och homogeniseras genom skruvskjuvning innan extruderingsformen formar en kontinuerlig tvärsektionsprofil (källor: ThoYu; Amade-Tech).
- Jag bekräftar värmehanteringen i förväg. Flerzonsfat kombinerar vanligtvis elektrisk uppvärmning med vattenkylning med sluten krets (källa: Aaron Utrustnings spec), och tillförlitlig smälttemperaturkontroll är det som håller produktionen dimensionellt konsekvent över rören, rör, filmer, brädor, och flaskor.
- Skruvkonfiguration och anpassade verktygsverktyg definierar vad en linje faktiskt kan göra, så jag tar upp dem mot min produktmix snarare än att köpa generisk kapacitet. För R&D eller små körningar, en extruder i labbskala byggd för kontinuerlig enhetlig tvärsnittsproduktion är ofta rätt ingångspunkt (källa: Amade-Tech).
Vad är en plastextruderingsmaskin och hur fungerar den?
När jag utvärderar vilken polymerbearbetningsmaskin som helst, Jag börjar med samma mentala modell: en extruder är ett kontrollerat smält- och formningssystem. Solid plast går i ena änden, och en kontinuerlig, enhetlig tvärsnittsprofil kommer ut den andra. Allt mellan dessa två punkter handlar om att applicera värme och mekanisk skjuvning i rätt takt. Att förstå det flödet är det som skiljer en säker köpare från någon som gissar på specifikationer, och det formar direkt hur jag närmar mig en Plast extrudering Machine grossist köpa.
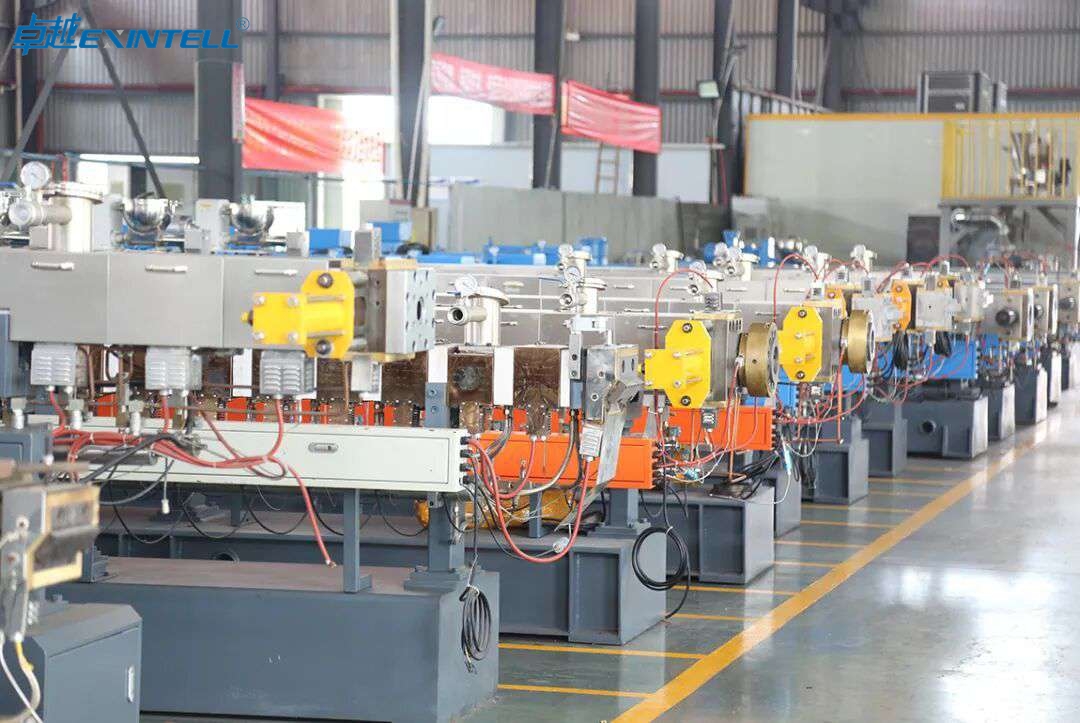
Kärnsmältningsprocessen
Inuti maskinen, solid plast transporteras framåt med en roterande skruv medan elektriska värmerör sveper in trumman i flera zoner. Plasten smälter genom en kombination av den externa värmen och den inre skjuvningen som genereras när skruven tvingar materialet mot cylinderväggen. Enligt ThoYu, plast i en extruder smälts av elektriska värmerör och omvandlas till en enhetlig smälta genom skruvextrudering och skjuvning (ThoYu, 2024). Den där dubbla mekanismen, ledande värme plus mekanisk friktion, Det är därför skruvgeometrin spelar lika stor roll som fattemperaturen.
Smälttemperaturkontroll är den del jag granskar mest i alla citat. Flerzonsfat parar vanligtvis elektrisk uppvärmning med sluten vattenkylning för att hålla varje zon inom ett smalt band (Aaron Utrustningsspecifikation). Om en tunna inte kan svalna lika exakt som den värms, du förlorar förmågan att köra värmekänsliga hartser rent.
Råmaterialformulär du kan köra
Materialet du matar formar maskinen du köper. I praktiken ser jag fyra vanliga råvaruformer:
- Pellets — standard för nyharts, lätt att mäta och smälta
- Granulat — något grövre, vanligt i sammansättningslinjer
- Pulver — Typiskt för torrblandningar av PVC och arbete i laboratorieskala
- Återvunnen flinga — återvunnet material med variabel bulkdensitet
Amade-Tech noterar att strängpressningsmaskiner för laboratorier bearbetar råmaterial i pulver, pellets, eller granulform för att producera kontinuerliga polymerprodukter med enhetligt tvärsnitt (Amade-Tech, 2024). En trattmonterad matarskruv levererar sedan råvaran jämnt in i fatet (ThoYu, 2024). Även utfodring är ingen liten detalj; inkonsekvent trattleverans visar sig som överspänningslinjer och dimensionell drift i den färdiga profilen.
Hur formen formar resultatet
Extruderingsmunstycket är det sista verktyget som smältan passerar genom, och den definierar produktens tvärsnitt. Rör, rör, filmer, brädor, och alla flaskor kommer från samma fat med olika formar (Amade-Tech, 2024). Eftersom formen ger en kontinuerlig tvärsektionsprofil, en maskin kan betjäna flera produktlinjer om du investerar i anpassade formverktyg. Denna verktygsflexibilitet är en anledning till att jag behandlar matrisinventering som en del av det totala köpbeslutet snarare än en eftertanke.
Kärnkomponenter som jag inspekterar på varje maskin
Oavsett om jag recenserar en industriell extruder till salu eller en begagnad enhet, Jag går igenom samma komponentchecklista:
- Fat — den uppvärmda cylindern, helst flerzoner med sluten kylning
- Skruva — hjärtat av smältning och förmedling; skruvkonfigurationen avgör utskriftskvaliteten
- Motor — extrudermotorns hästkrafter sätter ditt genomströmningstak
- Växellåda — Reduktionsförhållandet och servicefaktorn definierar användbart vridmoment
- Kontroller — kontroll av smälttemperatur och zonhantering
- Dö — det profilbildande verktyget
Två specifikationer förankrar denna utvärdering. Första, L/D-förhållandet, piplängden dividerad med skruvdiametern, berättar hur mycket uppehållstid smältan får; en begagnad Davis Standard 9-tums extruder (Modell 80IN80HT) inbyggd 2001 par a 32:1 L/D-förhållande med en 7-zonspipa och en 900 HP DC-motor (Aaron Utrustningslista). Andra, växellådans reduktionsförhållande och servicefaktor definierar vridmomentleveransen; industriella enheter listar vanligtvis förhållanden som t.ex 10.15:1 med en servicefaktor på 1.5 (Aaron utrustning). Dessa siffror översätts direkt till hur hårt du kan trycka viskösa material som HDPE eller fyllda föreningar utan att stanna.
Varför köpa plastextruderingsmaskiner i grossistledet?
Grossistvägen är där inköpsstrategin tjänar sitt stöd. Enligt min erfarenhet, skillnaden mellan detaljhandel och fabriksdirekta inköp är sällan en liten procentandel; det omformar ekonomin för en hel extruderingslinje. Nedan delar jag upp de fyra anledningarna till att jag konsekvent rekommenderar att man köper bulkextruderingsutrustning via grossistkanaler.
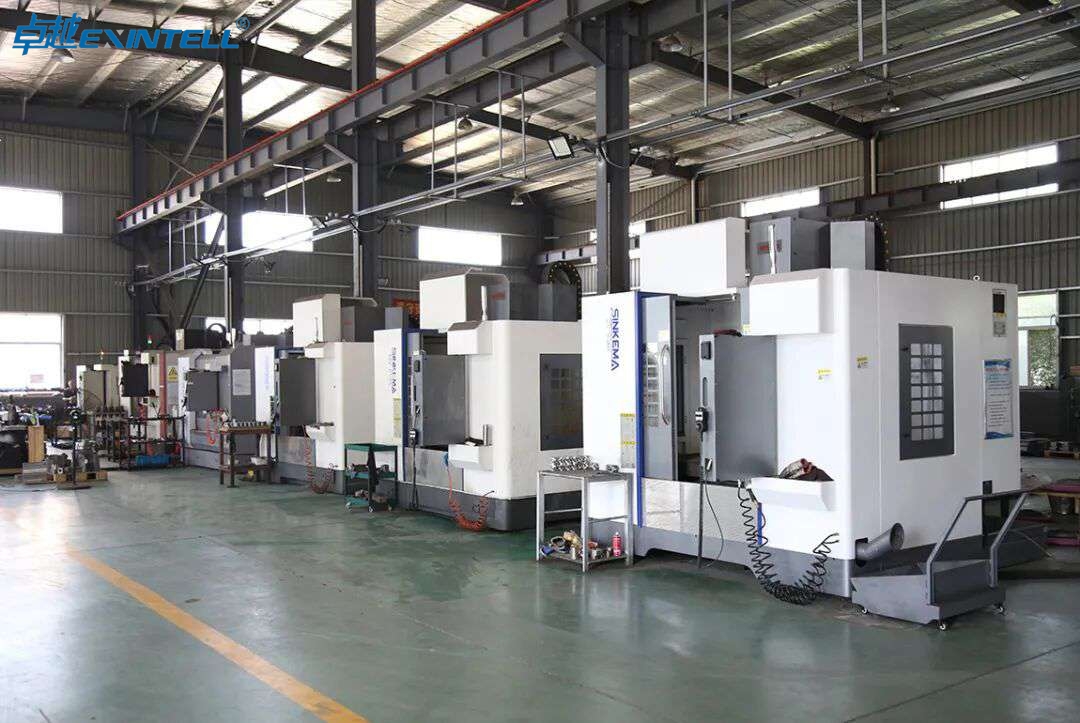
Kostnadsbesparingar på bulk- och fabriksdirekta beställningar
Fabriksdirekta prissättning tar bort lagren av distributörsmärkning som blåser upp priset för en plastextrudermaskin. Kina-baserade tillverkare, till exempel, erbjuda fabriksdirekta grossistpriser på plastextruders (ThoYu, 2024), vilket är anledningen till att så mycket prisrelaterade sökintentioner pekar mot utländska leverantörer. När jag jämför en enskild detaljhandelsenhet mot en bulkorder från en grossistmaskinleverantör, kostnaden per maskin sjunker vanligtvis tillräckligt för att ändra återbetalningsberäkningen för hela projektet. Som sagt, fabriksdirekt prissättning lönar sig bara när du tar hänsyn till den totala ägandekostnaden, en lucka jag tar upp senare i den här guiden.
Tillgång till OEM- och ODM-anpassning
Grossistrelationer öppnar dörren till OEM- och ODM-anpassning som detaljhandelskanaler sällan erbjuder. Istället för att acceptera en lagerkonfiguration, Jag kan specificera skruvlängden, fatzoner, kontrollpaket, och anpassade formverktyg som matchar min produkt. För alla som kör en specialiserad kontinuerlig tvärsnittsprofil, detta är det enskilt starkaste argumentet för att köpa direkt från en extruderingsmaskintillverkare snarare än en återförsäljare.
Bättre villkor för verktyg och reservdelar
Konversationen med tärningar och reservdelar är där grossistvillkor tyst sammanfogar till din fördel. Att förhandla om verktyg och ett reservdelspaket i den ursprungliga beställningen slår nästan alltid att köpa dem bitvis senare. Jag behandlar klädesplagg, skruvar, värmeband, och fatliners, som en del av det ursprungliga avtalet, och jag trycker på för skriftliga åtaganden om support efter försäljning. Starkt eftermarknadsstöd är det som håller en linje igång; utan det, en billig maskin blir en dyr flaskhals.
Skala produktionskapacitet effektivt
Slutligen, grossistinköp låter mig skala extruderns kapacitet utan att upprepa hela inköpscykeln varje gång. Standardisering på en leverantörs plattform innebär konsekventa reservdelar, bekanta kontroller, och repeterbar förarutbildning på flera maskiner. När efterfrågan växer, Att lägga till en andra eller tredje identisk enhet är mycket smidigare än att integrera felaktig utrustning från olika leverantörer.
Typer av plastextruders: Single Screw vs Twin Screw
Att välja mellan en enskruvsextruder och en dubbelskruvextruder är det mest följdriktiga tekniska beslutet vid ett grossistköp. Jag ramar in det enkelt: enskruvsmaskiner transporterar och smälter effektivt, medan dubbelskruvmaskiner blandar och sammansätter. Få den här matchningen rätt och resten av specifikationen faller på plats.
Enkelskruvextruders
Enkelskruvextrudern är arbetshästen för standardprofiler till en lägre kostnad. Det utmärker sig när det gäller att smälta jungfruharts och trycka det genom en form med jämn uteffekt, vilket gör den idealisk för rör, rör, och enkla kontinuerliga profiler. Det är också den vanligaste kategorin av begagnad utrustning, med varumärkesspecifika återförsäljningslistor allmänt tillgängliga (Aaron utrustning). Om din produktlinje kör konsekventa material som HDPE eller polypropen genom en fast form, en maskin med en enkel skruv ger vanligtvis det bästa värdet per enhet.
Tvillingskruvextruders
Den dubbelskruvade extrudern tjänar sin högre kostnad genom blandningsförmåga. Två sammangripande skruvar genererar den fördelande och dispersiva blandningen som behövs för blandningen, lägga till fyllmedel, färgämnen, och stabilisatorer, och för bearbetning av återvunnet material med varierande egenskaper. När jag arbetar med återvunnen plastflingor eller värmekänsliga tekniska polymerer som PEEK, tvillingskruvens överlägsna kontroll över skjuvning och uppehållstid är avgörande. Det är värt att notera att återvinningsextrudrar är en distinkt maskinklass byggd specifikt för återvunnet råmaterial (ThoYu, 2024), och många av dessa linjer förlitar sig på dubbla skruvdesigner av exakt denna anledning.
Utgångshastighet och materialkompatibilitet
De två typerna skiljer sig kraftigt åt i utgångsbeteende och materialpassning. Enskruvs utgång är till stor del en funktion av skruvhastighet och motorhästkrafter, vilket gör det förutsägbart för ett enda harts. Dubbelskruvsutgång är mer flexibel i olika formuleringar men är ofta optimerad för blandningskvalitet snarare än rå genomströmning. Material som PVC-torrblandningar och återvunna flingor drar nytta av dubbelskruvhantering, medan en ren singelharts går ekonomiskt på en enda skruv.
Single Screw vs Twin Screw: Jämförelsetabell
|
Faktor |
Enkelskruvsextruder |
Twin Screw Extruder |
|---|---|---|
|
Primär styrka |
Smältning och transport av standardprofiler |
Blandning, sammansättning, och devolatilisering |
|
Relativ kostnad |
Lägre |
Högre |
|
Bästa materialen |
HDPE, polypropen, enkla jungfruhartser |
PVC torrblandningar, återvunnen flinga, fyllda eller PEEK-föreningar |
|
Blandningskvalitet |
Begränsad |
Excellent (distributiv och dispersiv) |
|
Typiska produkter |
Rör, rör, enkla profiler |
Föreningar, masterbatch, återvunnen pellets |
|
Tillgänglighet på begagnatmarknaden |
Bred, varumärkesspecifika listor vanliga |
Smalare, mer specialiserad |
|
Idealisk köpare |
Fast produktlinje, kostnadsfokuserad |
Återvinning, anpassade formuleringar, R&D |
|
Faktor |
Enkelskruvsextruder |
Twin Screw Extruder |
|---|---|---|
|
Primär styrka |
Smältning och transport av standardprofiler |
Blandning, sammansättning, och devolatilisering |
|
Relativ kostnad |
Lägre |
Högre |
|
Bästa materialen |
HDPE, polypropen, enkla jungfruhartser |
PVC torrblandningar, återvunnen flinga, fyllda eller PEEK-föreningar |
|
Blandningskvalitet |
Begränsad |
Excellent (distributiv och dispersiv) |
|
Typiska produkter |
Rör, rör, enkla profiler |
Föreningar, masterbatch, återvunnen pellets |
|
Tillgänglighet på begagnatmarknaden |
Bred, varumärkesspecifika listor vanliga |
Smalare, mer specialiserad |
|
Idealisk köpare |
Fast produktlinje, kostnadsfokuserad |
Återvinning, anpassade formuleringar, R&D |
Matcha typen till din produktlinje
Min beslutsregel är okomplicerad. Om jag extruderar ett konsekvent material till en stabil profil, Jag väljer en maskin med en skruv och lägger besparingarna på anpassade verktyg och reservdelar. Om min process involverar sammansättning, färgförändringar, eller en plaståtervinningsextruder som hanterar återvunnet råmaterial, Jag anger en dubbelskruvsplattform och accepterar det högre priset som kostnaden för processkontroll. För köpare som väger en extruder i labbskala för produktutveckling, samma logik gäller vid mindre utgång: matcha skruvtyp till om du bevisar en formulering (tvilling) eller en profil (enda). Förankra skruvbeslutet till din faktiska produktlinje, snarare än enbart rubrikpris, är det som gör att ett grossistköp lönar sig under hela livslängden. Du kan granska verkliga konfigurationer på leverantörs- och återförsäljningslistor som t.ex Aaron Equipments begagnade enskruvsinventering och ThoYus grossistextrudersidor för att se hur dessa specifikationer ser ut i praktiken.
Hur mycket kostar en plastextruderingsmaskin?
När kunder ber mig om ett enda nummer, Jag säger det ärliga svaret till dem: en plastextruderingsmaskin kostar allt från några tusen dollar till långt över en miljon, och spridningen handlar helt och hållet om skala. Enligt min erfarenhet skaffar jag utrustning över tre nivåer, prisbanden bryts rent längs produktionskapaciteten, skruvkonfiguration, och nivån av automatisering du behöver. Innan du begär en offert, det hjälper att veta vilken nivå du faktiskt tillhör, eftersom en strängsprutmaskin i labbskala och en produktionslinje för industriell strängsprutning inte är samma köp med en annan prislapp. Det är olika maskiner. Lätt återvinningsbar plastförpackning
Prisklasser efter skala: Labb, Små, och industri
Jag grupperar köpare i tre praktiska kategorier. Extruders i laboratorieskala är kompakta, bänkskivor eller golvenheter byggda för R&D, sammansättningsförsök, och materialkaraktärisering. De bearbetar råmaterial i pulver, pellets, eller granulform för att framställa kontinuerliga polymerprodukter med ett enhetligt tvärsnitt (Amade-Tech). Små kommersiella enheter hanterar lågvolymproduktion, prototypkörningar, och nischprofilarbete. Industriella maskiner driver hela extruderade produktionslinjer för rör, filma, styrelse, och flaskutgång dygnet runt.
Här är hur siffrorna vanligtvis landar baserat på offerter jag har samlat in och offentliga listor. Behandla dessa som planeringsintervall, inte fasta priser, eftersom skruvkonfiguration och verktyg förändrar dem avsevärt.
| Tier | Typisk utgång | Skruvtyp | Ny prisklass (USD) | Begagnad prisklass (USD) |
|---|---|---|---|---|
| Extruder i labbskala | Upp till ~5 kg/timme | Enkel eller dubbelskruv | $8,000 – $45,000 | $4,000 – $25,000 |
| Liten reklamfilm | ~20 – 150 kg/h | Enkelskruvsextruder | $30,000 – $120,000 | $12,000 – $60,000 |
| Industriell linje | 300 kg/h och uppåt | Enkel- eller dubbelskruvextruder | $150,000 – $1,000,000+ | $50,000 – $400,000 |
Den övre änden av industribandet reflekterar kompletta linjer med nedströmsutrustning som avdrag, kyltankar, och upprullare, plus avancerad smälttemperaturkontroll. Ett rent extruderhuvud kostar mycket mindre än en nyckelfärdig linje, så bekräfta alltid vad offerten faktiskt innehåller innan du jämför leverantörer.
Vad sitter bakom klistermärkespriset
Fyra variabler flyttar talet mer än något annat. Kapaciteten är den självklara: genomströmningsvåg med pipdiameter och motorhästkrafter, och båda lägger till kostnad. Varumärket spelar roll, eftersom en maskin från en etablerad extruderingsmaskintillverkare har en premie kopplad till tillförlitlighet och reservdelstillgänglighet. Skick delar upp hela marknaden i nytt och begagnat, som jag tar upp i detalj nedan. Och verktyg är den tysta budget-buster. En anpassad form för en specifik kontinuerlig tvärsnittsprofil kan lägga till tiotusentals dollar, och det citeras ofta separat från själva maskinen.
Dolda kostnader bortom offerten
Köpeskillingen är sällan den totala ägandekostnaden, och det är här jag ser förstagångsköpare bli brända. Bortom maskinen, budget för dessa rader:
- Anpassad formverktyg för varje produktprofil du planerar att köra.
- Installation och riggning för tunga industrienheter, som ofta kräver kranservice och förstärkta golv.
- Uppgraderingar av el och energi för att leverera motorer med hög hästkraft och kylsystem med sluten krets.
- Frakt och, för import, arbetsuppgifter som jag bryter ner i logistikavsnittet i den här guiden.
- Reserv slitdelar såsom utbytesskruvar, fat, och värmeband.
- Driftsättning och operatörsutbildning, speciellt för automatiserade styrsystem.
Min tumregel: tillägga 15 till 30 procent till maskinpriset för att uppskatta det fullt installerade, produktionsfärdig kostnad. Att hoppa över den här matematiken är det enskilt vanligaste planeringsmisstaget jag stöter på.
Plast extruderingsmaskin grossistpris: Vad driver den?
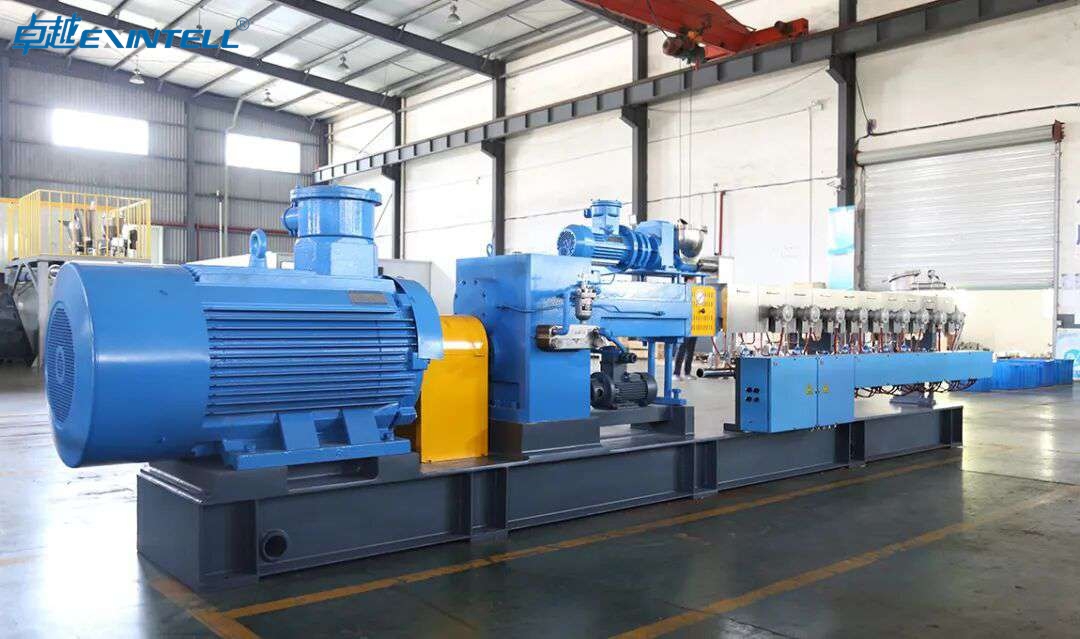
Grossistprissättning följer samma logik som detaljhandel, men med mer utrymme att förhandla och fler variabler att granska. När jag utvärderar ett fabriksdirekt extruderpris, antingen från en inhemsk återförsäljare eller en Kina-baserad leverantör som erbjuder grossistpriser (ThoYu), Jag arbetar igenom en konsekvent checklista med specifikationer. Var och en har en direkt kostnadslinje, och genom att förstå dem kan du jämföra citat på lika villkor istället för att gissa.
Specifikationer för skruv och fat
Skruven och pipan är hjärtat i maskinen, och de definierar både kapacitet och pris. Den viktigaste specen är L/D-förhållandet, skruvens förhållande mellan längd och diameter. Ett högre L/D-förhållande ger bättre blandning och smältenhet, vilket är viktigt för krävande polymerer. För referens, en begagnad Davis Standard 9-tums extruder (Modell 80IN80HT) kör a 32:1 L/D-förhållande med en 7-zoners pipa (Aaron Utrustningslista). Fler zoner innebär finare smälttemperaturkontroll, eftersom plast smälts av elektriska värmerör och omvandlas till en enhetlig smälta genom skruvklippning (ThoYu).
Skruvkonfigurationen avgör också maskinklassen. En enkelskruvextruder är arbetshästen för enkla profiler och är den vanligaste kategorin för begagnad utrustning (Aaron utrustning). En dubbelskruvsextruder kostar mer men utmärker sig vid blandning, blanda tillsatser, och bearbetning av återvunnen plastflingor. Om du kör PVC, HDPE, eller polypropen i volym, skruvgeometrin ska matcha hartset; PEEK och andra högpresterande polymerer driver dig mot specialiserade, högre kostnadskonfigurationer. Twin Screw Extruders Tillverkare
Motor och växellåda Hästkrafter
Extruder motor hästkrafter är en direkt proxy för genomströmning och, därför, pris. Samma Davis Standard-enhet parar sin pipa med en 900 HP DC-motor (Aaron Utrustningslista), som säger att den byggdes för tung industriproduktion. Växellådan översätter motorkraften till användbart vridmoment vid skruven. Reduktionskvoter som t.ex 10.15:1 kombinerat med en servicefaktor runt 1.5 definiera hur mycket vridmoment maskinen säkert kan leverera under belastning (Aaron utrustning). När jag jämför två liknande prissatta maskiner, en högre servicefaktor signalerar mer utrymme för hållbarhet, vilket är värt att betala för på utrustning du planerar att köra hårt.
Automation och styrsystem
Styrsystem skiljer en basmaskin från en modern. Manuella temperaturrattar och enkla reläer håller nere priset men kräver skickliga operatörer och producerar mer skrot. PLC-driven systems with closed-loop barrel cooling, receptförvaring, and data logging cost more upfront but pay back through consistency and lower waste. A hopper feeder with a hopper-mounted feeding screw that delivers raw material evenly into the barrel (ThoYu) is standard, but gravimetric feeding and automated blending add cost and precision. For high-volume operations, I consider automation a value driver rather than a luxury.
Certifications and Origin
Origin and certification shape both price and risk. Domestic and European machines command higher prices, partly for build quality and partly for support proximity. Fabriksdirekta priser från Kina-baserade tillverkare (ThoYu) kan sänka maskinkostnaden avsevärt, men du bör verifiera CE-märkningen, UL-överensstämmelse för den amerikanska marknaden, och dokumenterad elsäkerhet innan man begår. Jag ber alltid om certifieringshandlingar skriftligen, eftersom eftermontering av en ocertifierad maskin för att uppfylla amerikansk elkod raderar besparingarna som gjorde importen attraktiv i första hand.
New vs Used Plastic Extrusion Machines
This is the decision I get asked about most, and my answer is always the same: det beror på din risktolerans och din tidslinje. Använd extruderingsutrustning kan halvera kapitalkostnaderna eller mer, men besparingarna kommer med verklig exponering. Nya maskiner kostar mer och har ofta längre ledtider, men de kommer med garantier, nuvarande kontroller, och förutsägbar prestanda. Låt mig lägga ut båda sidor som jag skulle göra för en klient.
Kapitalbesparingar vs risk på begagnade andelar
Det ekonomiska argumentet för begagnad utrustning är starkt. Som pristabellen ovan visar, en begagnad industrienhet kan köras 40 till 60 procent under ny, frigöra kapital för verktyg och efterföljande utrustning. För en nystartad eller butik som testar en ny produktlinje, den skillnaden kan vara hela affärsfallet. Risken är att en polymerbearbetningsmaskin har slitagekomponenter, skruvar och fat försämras, värmeband misslyckas, och motorer tappar effektivitet, och de problemen är inte alltid synliga i ett listfoto. Besparingarna är verkliga, and so is the possibility of buying someone else’s problem.
Inspecting Condition, Hours, and Build Year
I never buy used equipment sight unseen, and I recommend you do not either. My inspection priorities, in order:
- Slitage på skruv och pipa: measure clearances if possible. Excessive clearance kills output and melt quality, and a replacement screw and barrel set is expensive.
- Build year and operating hours: a machine built in 2001, like the Davis Standard example, can still be excellent if maintained, but you need service records to judge.
- Heating and cooling systems: confirm all barrel zones heat correctly and that closed-loop water cooling holds temperature.
- Motor and gearbox condition: listen for bearing noise and check for oil leaks and gearbox play.
- Control panel function: verify every zone reads and controls accurately, since older controls may lack replacement parts.
When feasible, insist on a powered demonstration running actual Plastic Pellet Manufacturers material. A cold machine hides most of its problems.
Warranty and Support Gaps on Used Equipment
The support gap is the cost that does not show on the invoice. New machines from an extrusion machine manufacturer typically include warranty coverage, commissioning help, and access to after-sales support. Used units are usually sold as-is, so you own every failure from day one. Before I buy used, I confirm two things: that spare parts remain available for that model, and that a service technician familiar with the brand can be reached. A cheap machine with no parts pipeline is a liability, not a bargain.
Resale Value Considerations
Slutligen, think about the exit before you enter. Maskiner från erkända märken håller sitt värde mycket bättre på andrahandsmarknaden, vilket är exakt varför varumärkesspecifika återförsäljningslistor kräver en stadig efterfrågan (Aaron utrustning). If there is any chance you will resize or exit within a few years, buying a well-known single screw extruder, even at a premium, protects your capital on the way out. Enligt min erfarenhet, resale strength is the most overlooked factor in the new versus used debate, and it often tips a borderline decision toward the established brand.
My bottom line: buy new when uptime is critical, support matters, and you plan to run the machine for a decade. Buy used when capital is tight, you have the technical capacity to inspect and maintain the equipment, and you stick to reputable brands with living parts supply. Hur som helst, do the total cost of ownership math first, because the quote is only the beginning of the spend.
Källor: Aaron utrustning, Used Single Screw Extruders; ThoYu, Wholesale Price China Plastic Extruder; Amade-Tech, Lab Plastic Extrusion Machine.
Where to Find Used Plastic Extrusion Machines Wholesale
When I source equipment on a tight capital budget, the used market is usually my first stop. En välskött begagnad extruder kan leverera 80 till 90 procent av livslängden för en ny enhet till en bråkdel av kostnaden, provided you know how to read a listing and verify condition before wiring any funds. The challenge is not finding machines. It is separating a genuine bargain from a decommissioned liability.
Marketplaces and Dealers Worth Knowing
Most of my used purchases have come through established dealer networks rather than open classified listings. Specialized resellers such as Aaron Equipment maintain rotating inventories of single screw and twin screw extruders, and they photograph, tag, and often power-test each unit before listing it. That vetting matters. A dealer with a physical yard and a reputation to protect gives me recourse that an anonymous marketplace posting never will. I still cross-check auction houses and industry-specific listing boards, but I treat a reputable dealer as the baseline for used extrusion equipment.
Reading a Listing Like an Engineer
A used listing is a spec sheet in disguise, and three numbers tell me most of what I need to know before I ever call. Consider a real example: en begagnad Davis Standard 9-tums extruder (Modell 80IN80HT) inbyggd 2001, advertised with a 32:1 L/D-förhållande, a 7-zone barrel, och a 900 HP DC-motor (källa: Aaron Utrustningslista).
- L/D-förhållande. The barrel length-to-diameter ratio governs residence time and mixing. A 32:1 ratio suits demanding melt homogeneity work; shorter ratios around 24:1 handle simpler profiles. If your polymer needs thorough melting, do not buy short.
- Barrel zones. Seven independently controlled heating zones give me granular melt temperature control across the barrel length. More zones mean finer thermal tuning, which is critical for heat-sensitive resins.
- Motor horsepower. A 900 HP drive signals a high-throughput production machine, not a lab tool. Motor HP scales roughly with output capacity, so match it to your target line speed rather than buying more drive than your die can use.
Listings also disclose the gearbox reduction ratio and service factor, which together define usable torque. A 10.15:1 reduction with a 1.5 servicefaktor, till exempel, tells me the drivetrain has headroom for sustained duty (källa: Aaron utrustning). I read those figures as a durability signal, not a footnote.
Brands That Hold Value on the Resale Market
Brand reputation follows a machine into its second life. Davis Standard, in my experience, commands a premium on the resale market precisely because parts, skruvar, and service documentation remain available years after manufacture. That liquidity cuts both ways: I pay more up front, but I recover more when I resell, and I spend less time hunting for a replacement extruder screw configuration or barrel liner. When I compare two similar used units, a supported brand almost always wins on total cost of ownership even at a higher sticker price.
Verifying Condition Before You Commit
I never buy a used extruder on photographs alone. My pre-purchase checklist runs through the wear points that quietly drain performance:
- Slitage på skruv och pipa. Request bore measurements. Worn clearances degrade output and pressure stability, and reconditioning a barrel is expensive.
- Heater and thermocouple health. Confirm every zone reaches and holds setpoint. Dead zones on a multi-zone barrel are a red flag.
- Drive and gearbox. Listen for bearing noise and check for oil leaks. A failing gearbox can cost as much as the machine.
- Cooling system. Many industrial units use electric heating with closed-loop water cooling (källa: Aaron Utrustnings spec). Verify the cooling circuit is intact and free of scale.
- Run test. Whenever possible, I insist on a powered demonstration under load, not just a cold spin.
If a seller resists an inspection or a run test, I walk. The savings on a used polymer processing machine evaporate the moment you have to rebuild a drivetrain.
Small and Lab-Scale Plastic Extrusion Machines
Not every buyer needs a 900 HP monster. A large share of the search interest around this keyword points toward small and near-me machines, and that tracks with what I see in practice: R&D-lag, universitet, and startups need compact extruders that fit a lab bench and run on standard power. These machines trade throughput for flexibility, and for the right use case that is exactly the trade you want.
What Lab-Scale Machines Actually Do
A lab-scale extruder processes feedstock in powder, pellets, eller granulform för att framställa kontinuerliga polymerprodukter med ett enhetligt tvärsnitt (källa: Amade-Tech). The core physics is identical to production equipment: a hopper feeder delivers raw material evenly into the barrel, electric heating tubes melt the polymer, and the screw shears and homogenizes it into a uniform melt before the extrusion die shapes the output (källa: ThoYu). The difference is scale, not principle, which is what makes lab machines so useful for process development. What you learn at bench scale transfers to production.
Typical Products and Use Cases
Jag sträcker mig efter en enhet i labbskala i tre situationer:
- R&D och formulering. Testar nya hartsblandningar, tillsatser, eller återvunnen plastflinga utan att begå en produktionslinje.
- Prototypframställning. Producerar provfilmer, rör, och små profiler för kundgodkännande eller verktygsvalidering.
- Lågvolymproduktion. Betjänar nischmarknader där efterfrågan inte motiverar en fullständig extruderingslinje.
Dessa maskiner hanterar lätt vanliga termoplaster som PVC, HDPE, och polypropen, och högre specifikationer sträcker sig till tekniska polymerer som PEEK när cylindern och skruven är klassade för de förhöjda smälttemperaturerna.
Fotavtryck och strömkrav
Det praktiska med en labbextruder är att den bor i ett vanligt rum. Många bänkenheter drar enfas eller lätt trefaskraft och upptar ett fotavtryck mätt i några kvadratfot, versus the dedicated bay and heavy three-phase service a production extruder demands. Before buying, I confirm two things: the electrical service my facility can supply, and whether the cooling requirement is air or water. Getting the utilities wrong is the most common reason a small machine sits idle after delivery.
Knowing When to Upgrade to Production Scale
A lab machine has a ceiling, and recognizing it early saves money. I plan the jump to production scale when sustained order volume outpaces the machine’s extruder capacity output, when I am running multiple shifts just to keep up, or when per-unit cost on the small line exceeds what a production extruder would deliver. The signal is economic, not emotional: once the lab unit becomes the bottleneck rather than the tool, it is time to scale. I typically keep the lab machine anyway, redeployed for the R&D work it does best.
Lab-Scale vs Production Extruders at a Glance
| Attribut | Labb / Small-Scale Extruder | Production Extruder |
|---|---|---|
| Primary use | R&D, prototypframställning, low-volume runs | Continuous commercial production |
| Typical motor | Fractional to ~20 HP | 50 till 900+ HP (till exempel, 900 HP Davis Standard) |
| L/D-förhållande | ~20:1 till 25:1 | 24:1 till 32:1 |
| Barrel zones | 2 till 4 | 5 till 7+ |
| Power service | Single-phase / light 3-phase | Heavy 3-phase |
| Footprint | Benchtop to compact floor unit | Dedicated production bay |
| Produktion | Grams to low kg/hr | Hundreds of kg/hr |
Figures for the production column reflect the specification range seen in listings such as the Davis Standard 80IN80HT (källa: Aaron utrustning); lab-scale ranges reflect typical bench-unit configurations.
Buying Plastic Extrusion Machines Wholesale in the USA
Search intent around this keyword leans heavily toward USA and near-me queries, and that reflects a real procurement decision every US buyer faces: buy domestic or import. Factory-direct pricing from overseas manufacturers is genuinely attractive, and I have bought imported equipment when the numbers justified it. But the sticker price is only one line in the ledger. Here is how I weigh the domestic option.
The Case for Domestic Dealers
Buying from a US-based dealer or manufacturer gives me three advantages that rarely show up on a spec sheet but always show up in operations:
- Faster lead times. A machine in a domestic yard ships in days, not the weeks of ocean transit and customs clearance an import requires. When a line is down, that speed is worth real money.
- Easier service and parts. Domestic support means same-timezone technicians, stocked spare parts, and no international freight on a replacement gearbox or barrel. After-sales support is the single most underrated factor in extruder ownership.
- Standards compliance. US machines are typically built or certified to UL and NEC electrical requirements. That compliance simplifies installation, satisfies insurers, and passes inspection without the retrofit an uncertified import may need.
Compliance Is Not Optional
I want to be direct about this because it trips up first-time importers. An extruder that is not UL-listed or NEC-compliant can fail a facility electrical inspection, void insurance coverage, and create OSHA exposure. Retrofitting an imported machine to meet US standards, rewiring controls, replacing heaters, adding certified safety interlocks, can consume much of the money you saved on purchase price. Before I import, I confirm exactly what certification the unit carries and what it will cost to close any gap.
Cost Tradeoffs: Domestic vs Imported
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (källa: ThoYu), and for high-volume standardized equipment that pricing can be compelling. But the landed cost of an import includes freight, försäkring, importtullar, customs brokerage, och inlandstransporter, none of which appear in the quoted machine price. Layer on longer lead times, potential language and timezone friction on support, and any compliance retrofit, and the gap narrows considerably. Min tumregel: I model total cost of ownership over the first three years, not the purchase price, before deciding. On that basis, domestic often wins for equipment I need serviced quickly, while imports can win for planned capacity additions where lead time is not urgent.
How I Vet a Wholesale Supplier
Whether domestic or overseas, I run every wholesale machinery supplier through the same gate before committing capital. I confirm the minimum order quantity and whether it fits my actual need, request references from buyers running the same machine class, verify certifications in writing rather than taking a catalog claim at face value, and structure payment with protection, staged milestone payments or an escrow arrangement rather than a full wire against a promise. For imports specifically, I clarify Incoterms so I know exactly where the seller’s responsibility ends and mine begins. A supplier who answers these questions clearly is one I can build a relationship with; one who deflects is one I pass on.
Finding Wholesale Suppliers Near You
When I start a sourcing project for bulk extrusion equipment, I map suppliers in concentric circles: local, regional, then global. Proximity carries real value that rarely shows up on a quote, and I have learned to weigh it deliberately before chasing the lowest number.
Local vs Regional Sourcing Benefits
A supplier within a few hours’ drive lets me tour the floor, watch a machine run my resin, and shake hands with the service manager who will pick up the phone at 2 a.m. during a line-down event. Regional suppliers widen the pool of available inventory and specialization while keeping domestic warranty terms and familiar payment protections intact. Enligt min erfarenhet, the closer the vendor, the shorter the mean-time-to-repair, and for a single screw extruder running continuous cross-section profile work, downtime is the expense that quietly dwarfs the purchase price.
Installation and Service Proximity
Tackling, leveling, wiring a 900 HP DC drive, and commissioning a 7-zone barrel with closed-loop cooling all go smoother when the technician is local. A used Davis Standard 9-inch extruder (Modell 80IN80HT) med en 32:1 L/D ratio and 900 HP motor, inbyggd 2001, is a serious piece of iron to install and dial in (källa: Aaron Utrustningslista). I want the people who know that machine within reach for melt temperature control tuning and screw configuration adjustments during the first production weeks.
Trade Shows and Industry Directories
Two channels consistently surface credible vendors for me. Trade shows such as NPE: The Plastics Show and Fakuma put dozens of extrusion machine manufacturers in one hall, where I can compare a twin screw extruder against a single screw side by side and collect real spec sheets. For structured search, I lean on Thomasnet and the used-equipment marketplaces like Aaron Equipment, which maintains brand-specific resale listings for single screw extruders (källa: Aaron utrustning). Directories are a starting shortlist, inte en dom, so I always follow up with a plant visit or video walkthrough.
China vs US Suppliers: Weighing the Tradeoffs
The decision I face most often is factory-direct pricing from overseas versus the service density of a domestic partner. Neither wins outright. The right call depends on your volume, your in-house maintenance capability, and how much lead-time risk your production schedule can absorb.
Balansera lokalt pris med globala alternativ
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders, och det gapet kan vara betydande på jämförbara specifikationer (källa: ThoYu). amerikanska leverantörer, och begagnad hushållsutrustning, täppa till en del av det gapet när du räknar in frakt, arbetsuppgifter, och kostnaden för att samordna stöd över tidszoner. Jag behandlar klistermärkespriset som en insats i den totala ägandekostnaden, inte den avgörande siffran.
Ledtid och leveransöverväganden
Begagnad hushållsutrustning kan skickas på dagar; en ny utländsk extruderingslinje körs vanligtvis på en bygg-plus-hav-frakt-tidslinje mätt i månader. Havstransitering, hamnhantering, och inlandsdrayage lägger alla till veckor och variation. Om ditt projekt har ett svårt startdatum, den schemarisken förtjänar en linje i din modell vid sidan av prisfördelen.
Stöd, Delar, och språklogistik
Det är här jag har sett köpare underskatta friktionen. Time-zone offsets stretch troubleshooting cycles, spare gearbox and screw components may ship internationally, and technical documentation quality varies. Before committing overseas, I confirm English-language manuals, a named support contact, and a stocked or expedited parts channel for wear items like screws, fat, och värmeband.
China vs US Sourcing at a Glance
| Faktor | Utomlands (till exempel, Kina) factory-direct | US supplier / domestic used |
|---|---|---|
| Unit price | Lägst, factory-direct wholesale (källa: ThoYu) | Higher new; competitive on used inventory (källa: Aaron utrustning) |
| Ledtid | Build plus ocean freight, typically months | Days to weeks for in-stock units |
| Landad kostnad | Add freight, arbetsuppgifter, draage | Add domestic freight and rigging |
| Service proximity | Avlägsen, time-zone dependent | On-site or regional |
| Parts availability | International shipping, plan ahead | Domestic stock, snabbare vändning |
| Documentation & språk | Verify English manuals and support | Native-language support |
Min tumregel: high volume with a capable maintenance team favors overseas factory-direct; tight timelines or lean staffing favor domestic. Note that SERP demand for this keyword splits evenly across manufacturer, ecommerce, and informational content at roughly 33.3% varje (källa: SERP analysis, 2025), and buyer searches cluster around price, “near me,” “USA,” och “begagnad” intents (källa: SERP/PAA data, 2025) — a fair reflection of how mixed real purchasing behavior is.
How to Choose a Plastic Extrusion Machine Manufacturer
Once I have a shortlist, I run every candidate through the same vetting sequence. The goal is to separate a genuine polymer processing machine partner from a broker who will disappear after the wire transfer clears.
Quality Assurance and Factory Verification
I verify the factory before I verify the price. For overseas vendors that means a live video walkthrough or a third-party inspection of the production floor, weld quality on the extruder barrel, and evidence they actually build rather than resell. I ask to see a machine running feedstock in powder, pellets, or granule form to confirm they handle continuous polymer output the way their marketing claims (källa: Amade-Tech). Seeing the heating tubes and screw shearing melt real resin into a uniform stream tells me more than any brochure (källa: ThoYu).
Track Record and Reference Customers
I request three reference customers running similar materials, whether that is PVC pipe, HDPE-profil, polypropylene sheet, eller en krävande ingenjörspolymer som PEEK. A manufacturer with a documented history in your specific application has already solved the problems you are about to encounter. If a vendor cannot produce references, I treat that as a signal, not an oversight.
Customization and Application Expertise
The best manufacturers speak fluently about screw configuration, L/D ratio selection, and custom die tooling for your exact profile. Extruders produce a wide range of continuous products, including pipes, rör, filmer, brädor, och flaskor (källa: Amade-Tech), and each demands different tooling and thermal setup. I probe how they size the gearbox reduction ratio and service factor to my torque needs, drawing on published industrial examples such as a 10.15:1 ratio at a 1.5 servicefaktor (källa: Aaron utrustning). A vendor who can discuss whether a single screw or twin screw extruder fits my recycled plastic flake feedstock, and how the hopper feeder delivers material evenly, has earned a closer look.
After-Sales Support and Parts Availability
I put the support terms in writing before purchase: response-time commitments, commissioning assistance, operatörsutbildning, and guaranteed availability of wear parts like screws, fat, and heater elements. For a plastic recycling extruder or any line running abrasive reclaimed material, wear-part supply is not optional, it is the difference between a productive asset and expensive scrap. I confirm lead times on those parts specifically, since that is what governs real-world uptime.
Certifications and Quality Systems
Slutligen, I check the paperwork that signals a disciplined operation. ISO 9001 indicates a functioning quality management system, and CE marking matters if the equipment enters or transits European jurisdictions. For a US install I confirm the electrical build can meet UL and NFPA 79 expectations, since a 900 HP DC drive with multi-zone electric heating and closed-loop water cooling (källa: Aaron Utrustnings spec) has to satisfy my local inspector and my insurer. Certifications do not guarantee quality on their own, but their absence usually correlates with corners cut elsewhere.
Vetting sources I return to include ThoYu for factory-direct wholesale context (ThoYu wholesale listing) and Aaron Equipment for used single screw extruder benchmarks (Aaron Equipment used extruders).
Decoding Key Specifications Before You Buy
Every wholesale quote I review lists a wall of specifications, and most buyers I coach fixate on price before they understand what those numbers actually deliver. Enligt min erfarenhet, four figures tell you more about a machine’s real capability than the headline output rate does: L/D-förhållandet, the number of heating and cooling zones, the screw diameter, and the motor-to-gearbox pairing. Read those correctly and you can predict melt quality, energy draw, and output ceiling before the machine ever ships.
L/D Ratio and Its Impact on Melting and Mixing
The L/D ratio expresses the screw’s effective length divided by its diameter, and it governs how much residence time the polymer gets inside the barrel. A longer L/D gives the melt more distance to homogenize, which matters when you run temperature-sensitive or highly filled compounds. För referens, en begagnad Davis Standard 9-tums extruder (Modell 80IN80HT) I analyzed lists a 32:1 L/D-förhållande (källa: Aaron Utrustningslista), which sits at the higher end for single-screw machines and signals strong melting and mixing headroom.
As a rough guide, jag behandlar 24:1 till 26:1 as adequate for straightforward commodity resins, 28:1 till 32:1 as the sweet spot for consistent mixing and venting, and anything longer as specialty territory for demanding compounds. A single screw extruder built for basic profile work rarely needs the same length as one processing recycled plastic flake with variable bulk density. If a supplier can’t tell you the L/D ratio, that’s a signal the listing is thin on engineering detail.
Number of Heating and Cooling Zones
Multi-zone barrels let you stage the temperature profile from feed throat to die, and more zones mean finer control over melt temperature. The Davis Standard unit referenced above uses a 7-zone barrel (källa: Aaron Utrustnings spec), which gives an operator granular control across the length of the screw. Plastic in an extruder is melted by electric heating tubes and converted into a uniform melt through screw shearing (källa: ThoYu), so the zone count directly shapes how evenly that transition happens.
Cooling is the other half of the equation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (källa: Aaron Utrustnings spec), which pulls heat back out when shear or process feedback pushes a zone above setpoint. When I vet a machine, I confirm both the heating zone count and whether cooling is air or closed-loop water. Water cooling responds faster and holds tighter melt temperature control, which pays off on precision products.
Screw Diameter and Output Rate
Screw diameter is the single strongest predictor of throughput. Output scales roughly with the cube of the diameter, so a modest jump in screw size produces a large jump in kilograms per hour. That relationship is why a 9-inch machine like the Davis Standard example carries a 900 HP DC-motor (källa: Aaron Utrustningslista) — the mass of material moving through a large-diameter screw demands proportionally more drive power.
When comparing wholesale offers, always normalize output against diameter and resin type. A quoted output of, säga, 300 kg/hr means little without knowing whether it was measured on low-density film resin or a stiff PVC compound. I ask suppliers to state the resin, melt temperature, and screw speed used for their rated output, then compare like with like.
Motor HP and Gearbox Reduction Ratio
The motor and gearbox work as a matched pair. Motor horsepower sets the available power, while the gearbox reduction ratio converts high-speed, low-torque motor output into the low-speed, high-torque rotation the screw needs. Industrial extruders publish both the ratio and a service factor — for example, a 10.15:1 reduction with a 1.5 servicefaktor (källa: Aaron utrustning) — and that service factor tells you how much margin the drivetrain carries above nominal load.
I treat the service factor as a durability indicator. A gearbox rated 1.5 is designed to absorb shock loads and continuous duty without premature wear, which is exactly what you want on a machine running multiple shifts. A hopper-mounted feeding screw delivers raw material evenly into the barrel (källa: ThoYu), and that steady feed keeps torque demand predictable so the gearbox operates within its rated envelope.
Matching Machine Capacity to Your Production Volume
Specifications only matter once you tie them to your actual demand. The most expensive mistakes I see in wholesale procurement come from sizing decisions, not from picking a bad brand. Online Plastics Recycling Marketplace Buy too small and you’ll run the line flat out with no cushion for growth; buy too large and you’ll carry idle capital, higher energy bills, and startup scrap on every short run.
Estimating Throughput Needs
Start with your target finished-product volume, then work backward. I calculate required output in kilograms per hour by taking monthly demand, dividing by realistic operating hours, and adding an allowance for scrap and changeover. A useful sanity check: if you need 40,000 kg per month and run a single shift of about 160 productive hours, you need roughly 250 kg/hr of sustained output, and I’d size for 300 kg/hr to leave headroom.
Feedstock form affects this math too. Lab and production extruders process feedstock in powder, pellets, or granule form for continuous polymer products with uniform cross section (källa: Amade-Tech), and bulk density varies enough between those forms that the same screw can deliver noticeably different mass throughput. Confirm your rated output against the feedstock you’ll actually run.
Avoiding Under- and Over-Sizing
Undersizing forces the machine to run at maximum screw speed constantly, which raises melt temperature, accelerates wear, and leaves zero margin for demand spikes. Oversizing is subtler but real: an oversized extruder run at low speed can produce poor mixing and unstable output, and you pay for motor and heating capacity you never use. My rule is to target a machine that hits your peak demand at roughly 75 till 85 percent of its rated capacity, which keeps it in an efficient, controllable band.
Planning for Future Growth
Wholesale machinery is a multi-year commitment, so I plan sizing against a two-to-three-year demand forecast, not today’s orders. Som sagt, buying far ahead of demand ties up capital you could deploy elsewhere. A middle path I often recommend: size the extruder for near-term growth, but confirm the extrusion production line’s downstream equipment and the supplier’s screw and die options can scale, so you upgrade tooling rather than replacing the whole line.
Batch vs Continuous Production
Extrusion is inherently a continuous process — extruders produce continuous profiles including pipes, rör, filmer, brädor, och flaskor (källa: Amade-Tech) — so the batch-versus-continuous question is really about how your business schedules work. If you run long stable jobs, a larger continuous line maximizes efficiency. If you run many short jobs with frequent material and color changes, prioritize fast changeover and quick thermal response over raw size, because your losses will come from transitions, not from top-line speed.
| Production profile | Typical screw diameter | Indicative output | Suggested L/D | Bäst passform |
|---|---|---|---|---|
| Labb / R&D and small runs | 20–45 mm | Up to ~50 kg/hr | 24:1–28:1 | Sampling, small-batch, PEEK trials |
| Liten reklamfilm | 50–75 mm | ~80–250 kg/hr | 26:1–30:1 | Profiler, small pipe, specialty film |
| Mid-volume production | 90–120 mm | ~300–600 kg/hr | 28:1–32:1 | HDPE pipe, ark, continuous profile |
| Hög volym / heavy industrial | 150 mm and up | 600 kg/h och mer | 30:1–32:1+ | Large pipe lines, pallet, återvunnen flinga |
I treat these ranges as a starting frame for supplier conversations, not fixed rules. Actual output always depends on resin, melt temperature control, and screw configuration, so I verify each figure against a supplier’s tested data for my specific material.
Extruders for Specific Products: Pipe, Film, Ark, Pallet
The extruder is only the melt engine. What defines your finished product is the extrusion die and the downstream line built around it. When I evaluate a wholesale package, I look at the die and tooling as closely as the machine itself, because that’s where product quality and application fit are actually determined.
Pipe and Tube Extrusion Lines
Pipe and tube lines pair the extruder with an annular die, a vacuum calibration and cooling tank, a haul-off, and a cutter or coiler. For PVC and HDPE pipe, dimensional stability and wall concentricity are everything, so tight melt temperature control and steady output matter more than peak speed. I confirm the die is matched to my target diameter range and that the calibration tooling is included or clearly quoted, since retooling for a new pipe size is a recurring cost buyers often overlook.
Film and Sheet Die Configurations
Film and sheet share extrusion fundamentals but diverge at the die. Blown film uses an annular die with an air ring and tower; cast film and sheet use a flat T-die or coat-hanger die feeding a chill-roll or three-roll stack. Polypropylene and polyethylene dominate here, and die width plus lip adjustment set your thickness tolerance. When comparing offers, I ask specifically which die configuration is included and whether the lip is manually or automatically adjustable, because that determines how tightly you can hold gauge across the web.
Pallet and Profile Applications
Pallet and heavy-profile production is where large machines and recycled feedstock meet. Chinese manufacturers offer factory-direct wholesale pricing on plastic extruders built for pallet production (källa: ThoYu, ThoYu pallet extruder), and these lines frequently run reclaimed material. Recycling extruders are a distinct machine class designed for reclaimed plastic feedstock (källa: ThoYu), so if you plan to process recycled plastic flake, I strongly advise sourcing a machine engineered for it rather than adapting a virgin-resin extruder — the feed section, ventilering, and wear surfaces are built differently.
Custom Die and Tooling Options
Custom die tooling is what turns a general-purpose extruder into a machine that makes your exact product. Whether you need a bespoke profile cross section, a specific pipe wall structure, or a particular sheet width, I confirm three things with the supplier upfront: lead time for custom tooling, whether tooling design is in-house or subcontracted, and the cost of future die changes. A capable extrusion machine manufacturer will quote tooling as a clear line item and stand behind dimensional performance, which also tells you something about the after-sales support you’ll receive once the line is running.
For buyers exploring the used market, single screw extruders are a well-established resale category with brand-specific listings (källa: Aaron utrustning). When I consider used equipment for a specific product, I always verify that compatible dies and calibration tooling exist for my application, since a bargain machine with no path to the right tooling isn’t a bargain at all.
Processing Recycled Plastics with Wholesale Extruders
When I evaluate a wholesale extruder for a recycling operation, I start from a different premise than I would for virgin resin processing. Reclaimed feedstock is inconsistent, contaminated, and thermally sensitive, so the machine has to compensate for material variability that a virgin-only line never sees. Recycling extruders are a distinct machine class built for reclaimed plastic feedstock (källa: ThoYu, 2025), and treating them as interchangeable with standard profile extruders is one of the more expensive mistakes I have watched buyers make.
Recycling Extruders and Material Preparation
The extruder itself is only one stage in a longer chain. Before recycled plastic flake reaches the hopper feeder, it typically passes through washing, torkning, and size reduction. A hopper-mounted feeding screw delivers raw material evenly into the barrel (källa: ThoYu, 2025), and even that step becomes harder when the input is irregular flake rather than uniform pellets. Enligt min erfarenhet, the quality of upstream preparation determines whether the extruder runs stably or surges. If you are quoting a wholesale line and the supplier only prices the extruder, ask specifically about the material prep equipment, because the melt quality you get downstream depends on it.
The core melting mechanism is unchanged: plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (källa: ThoYu, 2025). What changes with reclaim is how much shear and residence time the material can tolerate before it degrades. HDPE and polypropylene reclaim are relatively forgiving; PVC regrind is far less so and punishes overheating quickly.
Why Twin Screw Extruders Excel with Reclaim
For consistent recycled output, I lean toward a twin screw extruder over a single screw extruder in most reclaim applications. The reason is mechanical. Twin screw configurations provide better mixing, more controllable shear, and stronger devolatilization, which matters when the feedstock carries moisture and volatiles picked up during its first life. A single screw extruder remains a common and cost-effective used-equipment category with brand-specific resale listings (källa: Aaron utrustning, 2025), and it can handle clean, well-prepared regrind. But when feedstock quality is uneven, the extruder screw configuration in a twin screw machine gives me the process latitude to keep melt temperature control tight across batches.
The tradeoff is cost. Twin screw machines carry higher purchase and tooling prices, and the gearbox is more complex. That is a real budget line, not a rounding error, so I weigh it against the value of the finished product. High-value recycled compounds justify the investment; commodity reclaim often does not.
Contamination and Filtration Considerations
Contamination is the defining challenge of recycled feedstock, and filtration is how you manage it. A melt filtration system, usually a screen changer with a fine mesh pack, removes particulate before the melt reaches the extrusion die. Without adequate filtration, contaminants cause surface defects, weak spots, and clogged dies. I always confirm two things with a wholesale supplier: the screen changer type (manual, hydraulisk, or continuous) and the finest mesh the system supports without excessive pressure buildup. For heavily contaminated post-consumer streams, a continuous screen changer avoids the production stoppages that manual changes force.
Multi-zone barrels commonly use electric heating with closed-loop water cooling (källa: Aaron Utrustnings spec, 2025), and precise zone control becomes even more important with reclaim because you are trying to melt inconsistent material without scorching the fraction that heats fastest.
Circular Manufacturing Opportunities
The commercial case for recycling extruders keeps strengthening. Brand commitments to recycled content and tightening regulation on single-use plastics are pushing demand for in-house reprocessing. I see two viable models. The first is closed-loop: reprocessing your own production scrap back into the same line, which improves yield and reduces raw material spend. The second is a dedicated recycling line that converts purchased post-industrial or post-consumer feedstock into salable pellets or profiles. Both turn a waste stream into either cost savings or revenue, and the extruder is the pivot point of that conversion.
Certifications and Standards to Look For
Certification is where wholesale procurement, speciellt från utländska leverantörer, gets serious. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (källa: ThoYu, 2025), and that pricing is genuinely attractive. But a low quote means nothing if the machine cannot be legally installed, insured, or operated in your jurisdiction. I treat certification as a gating requirement, not a nice-to-have.
CE Marking for European Compliance
If you operate in or export to the European Economic Area, CE-märkning är obligatorisk. It signals that the machine conforms to relevant EU directives, most notably the Machinery Directive, covering mechanical safety, bevakning, and emergency stops. For a US buyer this may seem irrelevant, but I raise it because many buyers plan to resell finished goods into Europe or operate multinational facilities. Confirm the CE marking is backed by an actual Declaration of Conformity and a technical file, not just a sticker on the frame. A legitimate manufacturer produces the paperwork on request.
ISO 9001 Kvalitetsledning
ISO 9001 certifies that the manufacturer runs a documented quality management system. It does not certify any individual machine, and I want to be precise about that distinction because suppliers sometimes blur it. What ISO 9001 tells me is that the factory has repeatable processes for design, produktion, and inspection, which correlates with more consistent build quality across units. For wholesale buyers ordering multiple machines or planning repeat purchases, that process consistency is exactly what protects you from unit-to-unit variation.
UL for US Electrical Safety
För den amerikanska marknaden, UL certification on electrical components is the one I refuse to compromise on. Extruders draw significant power through motors, värmeband, and control cabinets. A used Davis Standard 9-inch extruder, till exempel, kör a 900 HP DC motor across a 7-zone barrel (källa: Aaron Utrustningslista, 2025), and that scale of electrical load makes safety certification a genuine risk-management issue, inte en formalitet. UL or an equivalent NRTL listing affects your ability to pass local electrical inspection, secure insurance, and satisfy OSHA expectations. Imported machines frequently ship with control systems that are not UL-listed, so budget for potential panel rework or re-certification in the US.
Documentation and Compliance Verification
Certificates are only as good as your ability to verify them. My verification routine is straightforward:
- Request certificate numbers and check them against the issuing body’s public database rather than trusting a PDF.
- Confirm the certificate covers the specific model, not a different machine in the product family.
- Ask for the Declaration of Conformity, wiring diagrams, and the operation and maintenance manual before you release final payment.
- Where feasible, commission a third-party pre-shipment inspection to confirm the physical machine matches the documentation.
Tying compliance verification to your payment milestones is the single most effective piece of leverage you have as a wholesale buyer. Once the machine ships, that leverage is gone.
Understanding Total Cost of Ownership
The purchase price is the number everyone fixates on, and it is the one that matters least over the life of the machine. When I model total cost of ownership, I fold in energy, underhåll, driftstopp, och installation, and the ranking of suppliers frequently reverses once those costs are included. This is the analysis that most wholesale buying guides skip, and it is where a slightly cheaper machine can quietly become the expensive one.
Energy Consumption and Operating Cost
Energy is the largest recurring cost for most extrusion operations, and it is driven by motor horsepower and heater load. A 900 HP DC-motor (källa: Aaron Utrustningslista, 2025) running multiple shifts represents a substantial electricity bill, and small efficiency differences compound over thousands of operating hours. Multi-zone barrels using electric heating with closed-loop water cooling (källa: Aaron Utrustnings spec, 2025) are more efficient at holding temperature than older uninsulated designs. I ask suppliers for the connected load and, där det är möjligt, the specific energy consumption per kilogram of throughput, because that figure lets me compare machines on an operating-cost basis rather than a sticker basis.
Maintenance and Spare Parts
Slitage är oundvikligt. The screw and barrel are the primary wear components, and processing abrasive or filled materials accelerates it. Recycled plastic flake with residual contamination wears tooling faster than clean virgin resin. Gearbox maintenance also matters: industrial extruders define torque through gearbox reduction ratios such as 10.15:1 med en servicefaktor på 1.5 (källa: Aaron utrustning, 2025), and that gearbox needs scheduled lubrication and periodic inspection. My practical concern with wholesale and imported machines is spare parts lead time. A cheap machine whose screw takes three months to replace from overseas is not cheap when the line sits idle waiting.
Downtime and Reliability
Downtime is the cost that does not appear on any invoice, which is exactly why it gets underestimated. Every hour a line is down is lost production plus fixed overhead still accruing. Reliability is where established brands and ISO 9001 manufacturers tend to justify their premium. When I assess reliability, I look at build quality on the components that fail expensively, the availability of local service technicians, and the supplier’s after-sales support commitments. A responsive supplier that ships parts quickly is worth more than a marginally lower purchase price.
Installation and Commissioning Expenses
The final and most frequently forgotten category is getting the machine running. Installation and commissioning cover rigging and placement of heavy equipment, electrical and cooling-water hookups, control integration, and the trial runs needed to dial in melt temperature control and output. For imported machines I also budget for potential electrical re-certification and any adaptation to US voltage and plant infrastructure. Commissioning support from the manufacturer, whether on-site or remote, has real value here, and I confirm whether it is included in the quote or billed separately.
Total Cost of Ownership Comparison
The table below illustrates how the cost picture shifts across three common procurement paths. The figures are representative ranges for planning purposes, not fixed quotes, and actual costs vary with capacity, specifikation, och leverantör.
| Kostnadsfaktor | New Domestic (USA) | Imported Factory-Direct | Begagnad / Refurbished |
|---|---|---|---|
| Inköpspris | Högsta | Lägst | Låg till måttlig |
| Certification readiness | UL/CE typically included | Often needs verification or rework | Varies; verify by age and origin |
| Energieffektivitet | Current-generation controls | Varies by build quality | Older units may run less efficiently |
| Spare parts lead time | Kort | Lång (overseas shipping) | Depends on brand support |
| Installation / driftsättning | Vendor support common | May require added budget | Often buyer-managed |
| Downtime risk | Lägst | Måttlig till hög | Måttlig; condition-dependent |
My takeaway from running this comparison repeatedly is that the imported factory-direct route wins on purchase price but requires you to budget deliberately for certification, spare parts logistics, och driftsättning. Den använda vägen kan vara utmärkt värde när maskinen kommer från ett välrenommerat märke med delar som fortfarande finns tillgängliga, vilket är anledningen till varumärkesspecifika återförsäljningsannonser (källa: Aaron utrustning, 2025) är värda att studera noggrant. Ny hushållsutrustning kostar mest i förväg och motiverar det ofta genom lägre stilleståndstid och enklare efterlevnad. Bestäm dig genom att modellera dina egna siffror över hela ägarhorisonten, inte bara genom citatet.
Frakt, Importavgifter, och logistik
När jag köper en plastextruderingsmaskin i grossistledet från en utländsk källa, det angivna maskinpriset är bara början på samtalet. I det ögonblick jag flyttar från en inhemsk begagnad enhet till fabriksdirekt prissättning av extruder från Kina, logistik blir ett projekt i sig. A single screw extruder with a long barrel, a heavy gearbox, and a full extrusion production line footprint does not travel like a pallet of parts. I plan the freight and customs path before I sign, because a surprise here erases the savings that made the import attractive in the first place.
Frakt, Crating, and Incoterms
The first term I nail down is the Incoterm, because it defines exactly where the seller’s responsibility ends and mine begins. In my experience three matter most for extrusion equipment:
- EXW (Fritt fabrik) — I take ownership at the factory gate and pay for everything after, including inland transport in the origin country. Cheapest on paper, most work for me.
- FOB (Gratis ombord) — the supplier delivers to the origin port and loads the vessel. This is my default for a first deal with a new wholesale machinery supplier because it splits responsibility at a clean point.
- CIF (Kosta, Försäkring, Frakt) — the seller arranges ocean freight and insurance to my destination port. Convenient, but I always ask for the itemized breakdown so I can compare it against an independent forwarder quote.
Crating is not a line item I skip. An industrial extruder for sale overseas ships as a heavy, oddly balanced load, and the extruder barrel, extrusion die, and hopper feeder each need to be secured against vibration and moisture during a five- to eight-week ocean transit. I insist on a fumigated hardwood or steel-reinforced crate, desiccant packs inside sealed control cabinets, and a packing list that itemizes every component. For anything over roughly two meters wide or 10 ton, I confirm whether the load qualifies as out-of-gauge, because that changes the container type and the price.
US Import Duties and Customs
US import duty on plastics processing machinery generally falls under Harmonized Tariff Schedule heading 8477, som omfattar maskiner för bearbetning av gummi eller plast. Base most-favored-nation duty rates in this heading are frequently low or zero, but I never assume the rate — I confirm the exact HTS subheading for my specific machine with a licensed customs broker before purchase (källa: USA:s internationella handelskommission, Harmoniserat taxeschema, 2025, hts.usitc.gov). Beyond the base duty, I check for any additional Section 301 tariffs that apply to goods of Chinese origin, since those have been adjusted repeatedly and can add a meaningful percentage to landed cost.
On top of duty I budget for the standard federal fees: the Merchandise Processing Fee and, for ocean shipments, the Harbor Maintenance Fee. I also file the ISF (Importer Security Filing, de “10+2”) at least 24 hours before the goods load overseas, because a late filing draws a penalty that has nothing to do with the machine’s value. A customs broker handles these filings for me, and their fee is small relative to the risk of getting them wrong.
Lead Time Planning
I build my schedule backward from the date I need the polymer processing machine running. A realistic timeline for a made-to-order extrusion production line from Asia looks like this:
- Manufacturing and assembly: 6 till 12 weeks depending on custom die tooling and screw configuration
- Factory acceptance and third-party inspection: 1 till 2 veckor
- Ocean transit to a US West Coast port: 3 till 5 veckor (longer to East Coast)
- Customs clearance and drayage: 1 till 2 veckor
- Inland freight, tackling, och installation: 1 till 3 veckor
That puts a typical door-to-commissioning window at three to six months. I treat any supplier who promises dramatically less with healthy skepticism.
Rigging and Site Delivery
The final hundred meters are the ones people underestimate. A loaded extruder does not roll off a truck on its own. I arrange a rigging crew with the right forklift or crane capacity, verify that my facility’s dock, doorways, and floor loading can accept the machine’s footprint and weight, and confirm the power drop matches the extruder motor horsepower — a 900 HP DC motor draws very differently than a modest lab-scale extruder. On one project I nearly missed that the closed-loop barrel cooling system needed a dedicated water supply already plumbed before the rigging crew arrived. Now that check is on my pre-delivery list every time.
Payment Terms and Buyer Protections
Sending a large deposit to a factory I have never visited on another continent is the moment where a wholesale extruder deal feels riskiest. I manage that risk with payment structure, not just trust. The goal is simple: I want money to move only as the supplier hits verifiable milestones, and I want a neutral mechanism holding the leverage until I confirm the machine is what I paid for.
Letters of Credit and Escrow
For larger orders I favor a documentary letter of credit (LC). My bank commits to pay the supplier only when the supplier presents the exact documents my LC specifies — bill of lading, packlista, inspection certificate, and so on. The paperwork discipline of an LC protects both sides, and it signals to a serious extrusion machine manufacturer that I am a professional counterparty. The tradeoff is bank fees and rigidity: any document discrepancy can hold up release, so I draft the required-documents list carefully.
For mid-sized deals, a third-party escrow service or a marketplace with built-in trade assurance offers similar protection with less overhead. The escrow agent holds my funds and releases them on agreed conditions. I read the release triggers closely, because an escrow that releases on shipment rather than on acceptance does far less for me.
Deposit and Milestone Structures
The structure I return to most often for a factory-direct order is a 30/40/30 split, and I have found it balances the supplier’s cash-flow needs against my protection:
- 30% deposition to begin production
- 40% on completion, paid after a successful factory acceptance test and third-party inspection, before the machine ships
- 30% balance after delivery, installation, and successful commissioning at my site
I resist any pressure toward a 50% or larger upfront deposit from a supplier I do not have history with. The single most important lever I hold is that final payment tranche tied to on-site performance. If it is fully paid before the machine runs at my facility, I have given away my only real remedy.
Contract and Inspection Clauses
A wire transfer confirmation is not a contract. I insist on a purchase agreement that spells out, åtminstone:
- Detailed technical specifications: skruvdiameter, L/D-förhållande, extruder screw configuration, gearbox reduction ratio and service factor, fatzoner, heating and cooling method, and rated capacity output
- Acceptance criteria tied to measurable output — for example, a specified throughput in kilograms per hour on a named resin such as HDPE or PVC, at a stated melt temperature control tolerance
- Right to third-party inspection before shipment, at my discretion
- Penalty and remedy clauses for late delivery or failed acceptance
- Governing law, dispute resolution venue, och garantivillkor
I tie the acceptance clause to a real production condition rather than a vague “machine works” statement. “Produces continuous cross-section profile at 300 kg/hr on virgin polypropylene within spec” is enforceable. “Functional” is not.
Reducing Overseas Transaction Risk
Beyond structure, a few habits reduce my exposure. I pay to the company’s registered corporate bank account, never to a personal account or a sudden last-minute change of banking details — that redirection is a common fraud pattern. I keep all commitments in writing. And I match my payment protection to deal size: an LC for a full extrusion production line, escrow or trade assurance for a single mid-range machine, and even for a modest used unit I still hold a meaningful balance until commissioning.
Vetting Suppliers and Verifying Quality
Payment protection limits my downside, but it does not put a working machine on my floor. That comes from vetting the supplier well and verifying the equipment before it ships. Since the SERP for this category splits evenly across manufacturers, ecommerce platforms, and other content (källa: SERP analysis, 2025), buyers land in front of very different seller types, and the diligence I apply has to flex accordingly. A factory-direct manufacturer, a marketplace reseller, and a used-equipment dealer each deserve a different set of questions.
Factory Audits and References
Before I commit to a new extrusion machine manufacturer, I verify they actually build what they sell. I ask for their business license and registration, confirm how long they have operated, and request references from prior US or export customers — then I actually call those references. When the order justifies it, I commission an on-site factory audit, either through a sourcing agent or an inspection firm. The auditor confirms the factory exists, has real production capacity, and is not simply a trading company drop-shipping another workshop’s output. Trading companies are not automatically a problem, but I want to know which one I am dealing with, because it changes who is accountable for after-sales support.
Third-Party Inspection Services
I treat pre-shipment inspection as non-negotiable on any significant purchase. An independent inspector — from a global firm like SGS, TÜV, Bureau Veritas, or a specialist machinery inspector — visits the factory before the balance-triggering milestone. They verify that the build matches the contracted specifications: the correct extruder barrel construction, screw and die tooling, gearbox rating, motor horsepower, and control system. A pre-shipment inspection report is one of the documents I list in my letter of credit, which links the money release directly to verified quality. The inspection fee is trivial next to the cost of receiving a machine that does not meet spec after it has cleared customs.
Sample Runs and Acceptance Testing
Specifications on paper are a promise; a sample run is proof. I ask the supplier to run the machine on my actual feedstock — whether that is virgin resin, recycled plastic flake, or a specific grade of PEEK or polypropylene — and produce the profile I intend to make. I want to see documented throughput, dimensional tolerance on the continuous cross-section, surface quality, and stable melt temperature control across the barrel zones. For a recycling extruder in particular, testing on real reclaimed material rather than clean pellets tells me whether the screw configuration and feeding system will actually handle my input. Where possible, I have this run witnessed by my third-party inspector or captured on video with live instrument readings.
Warranty and Service Commitments
The last thing I verify is what happens after the machine is running. I get the warranty in writing — typical coverage runs 12 månader, sometimes longer on the mechanical structure — and I read what it excludes. Then I look past the warranty to practical serviceability: whether spare parts for the gearbox, värmare, and screw are stocked or reasonably available, what the lead time is for a critical replacement, whether the supplier provides commissioning support and operator training, and whether remote technical support is available in a time zone and language I can work with. A cheaper machine from a supplier with no realistic service path is not the bargain it looks like.
Supplier Vetting Comparison
To make the tradeoffs concrete, here is how I weigh the three seller types I most often evaluate when buying extrusion equipment. This maps to the new-versus-used-versus-imported procurement decision that runs through the whole purchase.
| Vetting factor | Factory-direct manufacturer (overseas) | Online marketplace / reseller | Domestic used-equipment dealer |
|---|---|---|---|
| Typical price position | Lowest per-spec; factory-direct extruder pricing | Mitt; platform markup added | Variabel; strong value on legacy brands |
| Anpassning (skruva, dö, L/D-förhållande) | High — built to order | Låg till måttlig | None — as-is condition |
| Lead time to running | 3–6 months incl. logistik | Varies with stock and origin | Fastest — often weeks |
| Inspection method | Fabriksrevision + pre-shipment inspection | Platform assurance + independent check | In-person condition assessment |
| Payment protection | Letter of credit / milestone escrow | Trade assurance / escrow | Standard domestic terms |
| Garanti & service | New warranty; verify parts pipeline | Depends on seller | Limited or none; dealer-dependent |
| Bäst passform | Custom production line, cost-driven | Standard machines, moderate volume | Proven brands like a used single screw extruder, fast need |
Both ends of that table are legitimate paths. China-based manufacturers offer genuine factory-direct wholesale pricing on plastic extruders (källa: ThoYu, ThoYu), while the domestic used market lists brand-specific machines such as a Davis-Standard 9-inch single screw extruder with a 32:1 L/D-förhållande, seven-zone barrel, och 900 HP DC-motor (källa: Aaron Utrustningslista, Aaron utrustning). The right choice depends on how much customization, speed, and service I need, and the vetting discipline above is what turns any of these into a purchase I can stand behind.
Installation, Driftsättning, and Training
Buying the machine is only half the transaction. Enligt min erfarenhet, the gap between a signed purchase order and a line running at rated output is where most first-time buyers lose weeks and margin. I treat installation, driftsättning, and training as a single project with its own timeline, not an afterthought bundled into shipping. What follows is the sequence I use to bring a new or used extruder from crate to steady-state production.
Site and Utility Requirements
Before the freight arrives, I confirm the site can actually support the equipment. Industrial extruders draw serious power and generate real heat, so utility planning comes first. A used Davis Standard 9-inch extruder, till exempel, ships with a 900 HP DC motor and a 7-zone barrel (källa: Aaron Utrustningslista, 2024), which tells me immediately that a standard 240V shop feed will not cut it. I map four requirements before delivery:
- Electrical service: Confirm voltage, fas, and amperage against the motor and heater load. Extruder motor horsepower drives the largest single draw, and multi-zone barrels add electric heating loads on top of that.
- Kyl: Multi-zone barrels commonly pair electric heating with water-based closed-loop cooling (källa: Aaron Utrustnings spec, 2024). I verify chiller capacity, flow rate, and water quality before day one.
- Floor and access: An extrusion production line with downstream haul-off, kyltankar, and cutters needs linear floor space and a level, load-rated slab. I measure the full line, not just the extruder footprint.
- Ventilation and safety: Melt temperature control means heat and, with some polymers, fume management. Local exhaust and clearances matter for both compliance and operator comfort.
Setup and Calibration Steps
Once the machine is positioned and services are connected, I run commissioning as a checklist rather than a feel. Kärnpolymerbearbetningsmaskinen omvandlar råmaterial till pulver, pellets, eller granulform till en kontinuerlig tvärsektionsprofil (källa: Amade-Tech, 2024), och varje steg i den konverteringen måste ringas in:
- Mekanisk inriktning: Bekräfta växellådan, skruva, och cylindern är inriktade och vridna. Växellådans reduktionsförhållanden och servicefaktorer definierar vridmomentleveransen (källa: Aaron utrustning, 2024), så jag verifierar drivlinan innan jag belastar.
- Värmare och termoelement verifiering: Plast smälts av elektriska värmerör och homogeniseras genom skruvklippning (källa: ThoYu, 2024). Jag kontrollerar varje zon oberoende och bekräftar att varje termoelement läser korrekt.
- Kontroll av fodersystem: Behållarmonterade matningsskruvar levererar råvaran jämnt in i fatet (källa: ThoYu, 2024). Jag bekräftar konsekvent matning med det faktiska hartset, om det är PVC, HDPE, polypropen, eller återvunnen plastflinga.
- Form och verktyg passar ihop: Installera extruderingsformen, confirm the screw configuration suits the resin, and set the melt temperature profile for a stable, uniform cross section.
- Dry run then wet run: Cycle the line empty, then purge and run production resin, adjusting zone temperatures and screw speed until dimensions hold to spec.
Operator Training Needs
A calibrated machine still fails without trained operators. I schedule training to overlap with commissioning so the team learns on the exact line they will run. My minimum curriculum covers startup and shutdown sequencing, purge procedures between resin changes, reading and adjusting melt temperature control, recognizing off-spec output, and routine maintenance of screw, fat, och dö. For used equipment where the manufacturer is not on site, I budget for a third-party commissioning engineer or negotiate remote support into the deal. After-sales support is a spec worth confirming before purchase, inte efter.
Ramp-Up to Full Production
I never assume rated output on day one. Published extruder capacity output is a ceiling under ideal conditions, and real ramp-up follows resin behavior, verktyg, and operator familiarity. I stage it: run at reduced throughput to validate quality, log every setting that produces good parts, then increase output incrementally while watching for dimensional drift and thermal stability. I mina projekt, a well-commissioned single screw extruder reaches stable full production within one to three weeks; a twin screw extruder or a compounding line can take longer because there are more variables to tune.
Wholesale Buyer’s Checklist and Next Steps
When I run a procurement cycle for bulk extrusion equipment, I work through the same five stages every time. This is the unified framework I wish more buyers had when comparing new, begagnad, and imported options, because each channel carries different risks and each stage removes a category of avoidable loss.
1. Define Application, Volume, and Budget
I start with the product, inte maskinen. What continuous cross-section profile am I making, in what polymer, at what daily volume? Pipe, filma, styrelse, and profile lines have different die tooling, L/D-förhållande, and screw configuration requirements (källa: Amade-Tech, 2024). A lab-scale extruder suits R&D and short runs; an industrial extruder for sale suits committed volume. I set a budget that accounts for total cost of ownership, inte bara klistermärkespriset.
2. Shortlist Suppliers Across Channels
The market for this keyword splits evenly across manufacturer, ecommerce, and other content types, roughly a third each (källa: SERP analysis, 2024). I mirror that in sourcing by building three shortlists: OEM manufacturers, used-equipment dealers, and factory-direct import suppliers. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (källa: ThoYu, 2024), while dealers like Aaron Equipment list brand-specific used single screw extruders with full specs. Casting across all three channels is the only way to know what a fair price actually is.
3. Compare Specs and Total Cost
I compare specifications on a single sheet so nothing hides in a footnote. The table below shows how I frame the three channels for a mid-range single screw extruder.
| Faktor | New (OEM) | Begagnad (Dealer) | Imported (Factory-Direct) |
|---|---|---|---|
| Upfront price | Högsta | Lowest for equivalent size | Low to mid, before landed costs |
| Ledtid | Moderate to long (build to order) | Shortest (i lager) | Längst (build plus ocean freight) |
| Garanti / stöd | Full OEM warranty and support | Limited or as-is | Varies; confirm in writing |
| Spec certainty | Exact to order | Fixed by the listed unit | Configurable, verify against quote |
| Hidden costs | Installation, verktyg | Refurbishment, unknown wear | Import duties, frakt, driftsättning |
| Bäst passform | Long-term critical production | Fast start, tight capital | Volume buyers comfortable with logistics |
Total cost of ownership is where imported equipment surprises people. The quoted extruder machine price is not the landed cost. I add ocean freight, US import duties, inland transport, tackling, installation, and commissioning before I compare across channels. A low factory-direct number can equal or exceed a domestic used price once everything lands.
4. Negotiate Terms and Finalize Protections
Once I have a preferred supplier, I negotiate the terms that protect the money, not just the price. My payment-protection playbook is consistent:
- Staged payments tied to milestones: deposition, pre-shipment inspection, and balance on acceptance rather than 100% upfront.
- Tredjepartsinspektion before shipment for imported or used units, confirming the machine matches the quoted specifications.
- Written performance criteria: rated output, dimensionell tolerans, and acceptance test conditions defined in the contract.
- After-sales terms in writing: reservdelar tillgänglighet, garantins omfattning, and remote or on-site support.
- Clear minimum order quantity and Incoterms so responsibility for freight, försäkring, and duties is unambiguous.
Nästa steg
My recommended path from here: write a one-page spec sheet for your application, request quotes from at least two suppliers in each channel, build the comparison table above with your real numbers, and shortlist to two finalists before negotiating. That sequence keeps leverage on your side and turns a large capital purchase into a controlled decision.
Vanliga frågor
How much does a plastic extrusion machine cost?
Price depends far more on size, screw type, and condition than on any single list figure. Enligt min erfarenhet, a compact lab-scale or single screw extruder sits at the low end, while a large industrial line with a high L/D ratio, a multi-zone extruder barrel, and downstream equipment costs many times more. Used units, such as brand-name single screw extruders sold through dealers, typically undercut new OEM pricing for equivalent size (källa: Aaron utrustning, 2024). Always compare the plastic extruder machine price as a landed, total cost of ownership number rather than the headline quote.
Where can I find a plastic extrusion machine near me or in the USA?
For domestic sourcing, US-based used-equipment dealers are the fastest route because units are in stock and shipping is inland rather than international. For new machines, OEM manufacturers and their US distributors serve the market directly. If you are open to factory-direct wholesale pricing, China-based manufacturers ship internationally (källa: ThoYu, 2024), but you take on import duties, sjöfrakt, and commissioning logistics. My rule is simple: buy near you when speed and support matter, and import when volume justifies the added logistics.
Should I buy a new or used extruder?
Used equipment makes sense when capital is tight, you need to start fast, and the specific unit matches your resin and output. A used single screw extruder with documented specs, such as a Davis Standard unit with a 32:1 L/D ratio and 7-zone barrel (källa: Aaron Utrustningslista, 2024), can be an excellent value. New OEM equipment makes sense for long-term critical production where warranty, exact-to-spec configuration, and factory support outweigh the higher upfront cost. I steer buyers toward used for a first line or a proven process, and new for mission-critical or novel applications.
How do I choose a reliable manufacturer or wholesale supplier?
I vet suppliers on four things: verifiable references for the exact machine class I need, clear written specifications, defined after-sales support and spare-parts availability, and willingness to accept staged payments with pre-shipment inspection. A credible extrusion machine manufacturer will document gearbox reduction ratios, service factors, and torque delivery rather than quoting output alone (källa: Aaron utrustning, 2024). If a supplier resists third-party inspection or written performance criteria, I treat that as a red flag.
What is the difference between a single screw and a twin screw extruder?
A single screw extruder is the workhorse for straightforward profiles, rör, and film in resins like PVC, HDPE, och polypropen. A twin screw extruder provides stronger mixing and better control for compounding, high-fill formulations, and demanding materials such as PEEK. Twin screw lines cost more and take longer to tune, so I only recommend them when the application genuinely needs the mixing performance. Match the screw configuration to the polymer and product, not to a general preference.
Can I use an extruder for recycled plastic?
Ja, but often on a purpose-built machine. Recycling extruders are a distinct machine class designed for reclaimed feedstock (källa: ThoYu, 2024). If your input is recycled plastic flake with variable moisture and contamination, a dedicated plastic recycling extruder with appropriate feeding and venting outperforms adapting a standard virgin-resin line. Confirm the machine is rated for your specific reclaimed material before purchase.
What ongoing costs should I budget beyond the purchase price?
Total cost of ownership includes electricity for the motor and heaters, closed-loop cooling water, wear parts for the screw and barrel, custom die tooling for new products, operatörsutbildning, and periodic maintenance. For imported machines, add duties, frakt, och driftsättning. Buyers who plan only for the machine price are consistently surprised by the operating and logistics costs, which is exactly why I model landed and running costs before signing anything.
What Is Plastic Extrusion Machine Wholesale and Why It Matters for B2B Buyers
When I talk with procurement teams about buying extrusion equipment in volume, the first thing I clarify is what “grossist-” actually means in this category. It is not a discount aisle. It is a procurement channel where you buy directly from manufacturers, auktoriserade distributörer, or used-equipment dealers at factory-direct or bulk-negotiated pricing, usually bypassing the retail markup that comes with single-unit retail sales. Enligt min erfarenhet, understanding that distinction changes how you negotiate, how you vet, and how you budget.
Definition: What a Plastic Extrusion Machine Actually Does
A plastic extrusion machine converts raw polymer feedstock into a continuous product with a uniform cross section. Lab and production units process feedstock in powder, pellets, or granule form to produce continuous polymer products (källa: Amade-Tech, 2024). The core process is straightforward once you see it: raw material drops from a hopper feeder into a heated barrel, where a rotating screw melts and shears the polymer into a homogeneous melt. As ThoYu describes it, the plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (källa: ThoYu, 2024). That melt is then forced through an extrusion die that shapes the final profile.
The machine architecture matters when you compare quotes. A single screw extruder is the workhorse for many standard profiles and is the most common category on the used market, med varumärkesspecifika återförsäljningslistor allmänt tillgängliga (källa: Aaron utrustning, 2024). A twin screw extruder delivers better mixing and is typical for compounding, fyllda polymerer, och återvinning. Two specifications define capacity more than any marketing claim:
- L/D-förhållande — the length-to-diameter ratio of the screw and barrel. A used Davis Standard 9-inch extruder (Modell 80IN80HT), till exempel, features a 32:1 L/D-förhållande, a 7-zone barrel, och a 900 HP DC-motor (källa: Aaron Utrustningslista). Higher L/D generally means more melting and mixing capacity.
- Gearbox reduction ratio and service factor — these define how motor speed becomes usable torque. Industrial units commonly quote figures such as a 10.15:1 reduction ratio with a 1.5 servicefaktor (källa: Aaron utrustning). If a supplier cannot give you these, treat that as a data gap.
Supporting systems round out the package: the hopper-mounted feeding screw delivers raw material evenly into the barrel (källa: ThoYu), and multi-zone barrels commonly pair electric heating with closed-loop water cooling for melt temperature control (källa: Aaron Utrustnings spec).
Marknadskontext: Where Wholesale Buyers Actually Source Equipment
The sourcing landscape is more fragmented than most first-time buyers expect. When I mapped the search results for this category, they split almost evenly across manufacturer sites, ecommerce marketplaces, and other content, at roughly 33.3% varje (källa: SERP analysis). That tells me buyers are pulling from three distinct channels at once, and each carries a different risk and cost profile.
China-based manufacturers openly advertise factory-direct wholesale pricing on plastic extruders (källa: ThoYu), which is why imported equipment dominates a large share of price-sensitive inquiries. At the same time, buyer search behavior clusters heavily around price, “near me,” “USA,” “begagnad,” and small-machine intents (källa: SERP/PAA data). The practical takeaway: you are almost always choosing among three procurement paths, and I recommend evaluating all three before committing.
New vs. Used vs. Imported: A Procurement Framework
| Faktor | New (domestic OEM) | Begagnad (dealer/resale) | Imported (factory-direct) |
|---|---|---|---|
| Upfront cost | Högsta | Lowest per unit | Låg till måttlig |
| Ledtid | Weeks to months (build to order) | Shortest (i lager) | Längst (produktion + sjöfrakt) |
| Garanti / support efter försäljning | Strongest | Limited or as-is | Varierar stort; verify carefully |
| Spec transparency | Hög | Hög (documented history) | Requires diligence |
| Hidden costs | Installation, verktyg | Refurb, slitdelar | Import duties, frakt, logistik |
| Bäst passform | Long-run production, critical tolerances | Budget projects, proven models | Cost-driven scale-up with in-house maintenance |
I built this framework because it is the piece most buyers are missing. Comparing a used single screw extruder listing against an imported quote on price alone ignores the total cost of ownership, and that gap is where budgets get blown.
Nyckelapplikationer: Matching the Machine to Your Output
Extruders produce continuous profiles including pipes, rör, filmer, brädor, och flaskor (källa: Amade-Tech). The polymer you run dictates screw configuration, barrel design, and temperature control. In my experience the most common wholesale buyers fall into a few groups:
- Rigid profile and pipe producers running PVC and HDPE, who need robust torque and stable melt temperature control.
- Packaging and film converters running polypropylene and HDPE for continuous cross-section profiles.
- Recyclers, where a plastic recycling extruder is a distinct machine class purpose-built for reclaimed feedstock and recycled plastic flake (källa: ThoYu). Do not repurpose a virgin-resin single screw for heavy recycling duty.
- R&D and specialty labs running lab-scale extruders, sometimes with high-performance polymers like PEEK, where a small, precise machine beats a large production line.
Why It Matters for B2B Buyers
Wholesale procurement of a polymer processing machine is a capital decision with a multi-year payback. Getting the L/D ratio, extruder motor horsepower, and extruder capacity output right the first time is the difference between a line that runs profitably and one that bottlenecks your throughput. That is exactly why the supplier you choose matters as much as the machine.
How to Choose the Right Plastic Extrusion Machine Wholesale Supplier
Once buyers accept that the supplier decision drives the outcome, the next question is how to actually evaluate one. I use a repeatable process built around evidence, not sales pitches. Below is the vendor evaluation approach I apply before I recommend committing capital.
Vendor Evaluation: What Separates a Real Supplier From a Broker
A credible extrusion machine manufacturer or wholesale machinery supplier should be able to answer technical questions without deflecting. I evaluate on four dimensions:
- Specification transparency. They should provide the L/D ratio, växellådans reduktionsförhållande, servicefaktor, motor horsepower, antal fatzoner, and cooling method in writing. Recall the benchmarks: a documented industrial unit lists a 32:1 L/D ratio and a 900 HP motor (källa: Aaron Utrustningslista). If a quote omits these, the supplier either does not know the equipment or does not want you to.
- Technical fit to your polymer. A serious supplier asks what you are running (PVC, HDPE, polypropen, TITT, or recycled flake) before quoting. The right extruder screw configuration depends on the answer.
- Support efter försäljning. Ask specifically about spare parts availability, ledtider för byte av skruv och pipa, och fjärr- eller idrifttagning på plats.
- Verifierbar meritlista. Dokumenterad återförsäljningshistorik, referenskunder, och riktiga installationsfoton. Fabriksdirekta säljare annonserar grossistpriser (källa: ThoYu) måste fortfarande rensa den här stapeln.
Röda flaggor: När ska man gå bort
Det här är varningssignalerna som har räddat mig från dåliga köp:
- Vägran eller oförmåga att dela kärnspecifikationer (L/D-förhållande, växellådans förhållande, HP motorcykel).
- Prissättning som är dramatiskt lägre än marknaden utan någon förklaring, särskilt på importerade enheter.
- Press på full förskottsbetalning via bank utan milstolpestruktur eller depositionsalternativ.
- Inga skriftliga garantivillkor och ingen tydlig supportkontakt efter försäljning.
- Vaga svar om importtullar, frakt, och logistik för gränsöverskridande affärer, lämnar dessa kostnader helt och hållet på dig.
- Endast stockfoton, with no ability to arrange a video walkthrough or factory audit.
Due Diligence checklista
I run every serious quote through this list before signing:
- Confirm full specifications in writing and match them to your production requirements.
- Verify business registration, export licensing (för import), and years in operation.
- Request references from buyers running the same polymer and output range.
- For used equipment, obtain maintenance records and, där det är möjligt, arrange an inspection or test run. Single screw extruders are a well-documented resale category, so history should be available (källa: Aaron utrustning).
- Get a landed-cost breakdown: unit price, custom die tooling, lådor, ocean or freight cost, importtullar, och installation.
- Structure payment with protection: deposit plus milestone payments tied to inspection or shipment, ideally through a letter of credit or escrow rather than a single wire transfer.
- Confirm minimum order quantity terms if you are buying multiple units or a full extrusion production line.
- Get spare-parts and support commitments in the contract, not just verbally.
Viktiga överväganden: Total ägandekostnad
The plastic extruder machine price on the quote is the smallest part of the story. Total cost of ownership is where I focus buyers, because it is the gap most competing guides ignore. For an imported unit, the sticker price can be misleading once you add:
- Logistics and duties — ocean freight, försäkring, customs brokerage, and import duties on cross-border purchases.
- Verktyg — custom die tooling for your specific profile, which is rarely bundled.
- Energi — electric heating tubes and motor horsepower drive a meaningful ongoing utility cost.
- Wear parts and maintenance — screws, fat, and gearbox service over the machine’s life.
- Downtime risk — a cheaper machine with no local support can cost more per year in lost production than a pricier one with strong after-sales coverage.
Practical Tips From Experience
A few habits that consistently pay off:
- Get at least three quotes across the new, begagnad, and imported channels so you can compare on landed cost, inte klistermärkespris.
- Insist on a test run with your actual feedstock before final payment whenever the deal allows it.
- Negotiate spare wear parts into the initial order while your leverage is highest.
- For imports, budget a realistic timeline; factory-direct pricing (källa: ThoYu) comes with longer lead times and shipping risk you should plan around.
- Document every spec agreement in the purchase contract so there is no ambiguity at delivery.
Industry Context
Because search behavior in this category skews toward price, “near me,” begagnad, and USA intents (källa: SERP/PAA data), suppliers know buyers are price-shopping and will lead with the number. My advice is to let them, then reframe the conversation around specifications, stöd, och total ägandekostnad. The supplier who engages seriously on those terms is usually the one worth buying from. For deeper reference on used single screw resale listings and specification benchmarks, dealer catalogs such as Aaron Equipment are a useful starting point (Used Single Screw Extruders), and factory-direct wholesale pricing structures are illustrated by manufacturers like ThoYu (ThoYu wholesale plastic extruder).
Find wholesale suppliers of plastic extrusion machines in the US
When I source extrusion equipment for a client, I start by mapping the supplier landscape rather than jumping straight to price. The keyword’s search results split almost perfectly into three buckets: manufacturer sites, ecommerce marketplaces, and everything else, each roughly a third of the page (källa: SERP analysis, 2025). That split tells me buyers are pulling from three distinct channels, and treating them as interchangeable is where most procurement mistakes begin.
The four supplier channels I evaluate
Enligt min erfarenhet, every viable wholesale source falls into one of four categories, and each carries a different risk-and-cost profile.
- Domestic new-equipment manufacturers and their distributors. These give you the shortest lead time to parts and service, which matters when a gearbox or extruder screw fails mid-run.
- Used and refurbished dealers. Aaron utrustning, till exempel, maintains an active inventory of used single screw extruders with brand-specific resale listings, including a Davis Standard 9-inch unit (Modell 80IN80HT) med en 32:1 L/D-förhållande, 7-zone barrel, och 900 HP DC motor built in 2001 (källa: Aaron Utrustningslista). This channel is where I find the deepest discounts on industrial-scale capacity.
- Import-direct manufacturers. China-based makers such as ThoYu offer factory-direct extruder pricing on both virgin-polymer and plastic recycling extruders (källa: ThoYu). The unit cost is lower, but you take on shipping, arbetsuppgifter, and vetting.
- Specialty and lab-scale suppliers. Amade-Tech supplies lab plastic extrusion machines that process feedstock in powder, pellets, or granule form for continuous polymer products with uniform cross section (källa: Amade-Tech). Useful when you need R&D throughput rather than production volume.
Key considerations when vetting a supplier
Price is the loudest signal in this market, but it’s rarely the one I weigh first. Before I request a quote, I confirm the supplier can document the machine’s core specifications: skruvkonfiguration, L/D-förhållande, barrel heating and cooling design, växellådans reduktionsförhållande, and motor horsepower. A credible wholesale machinery supplier will hand these over without hesitation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (källa: Aaron Utrustnings spec), so I ask specifically whether the cooling loop is intact on used units.
I also insist on a payment-protection structure. For import-direct purchases I use an escrow or letter-of-credit arrangement tied to inspection milestones, never a full wire transfer up front. For used domestic equipment, I request a video of the machine running under load. These steps sound obvious, yet they’re the exact gaps I see competitors skip entirely.
Practical tip: match the supplier to the polymer
Not every supplier handles every resin well. If your line runs PVC or HDPE profiles, a single screw extruder from a general manufacturer is usually adequate. If you’re compounding, running polypropylene blends, or processing engineering polymers like PEEK, I look for suppliers who default to a twin screw extruder and can spec custom die tooling. And if your feedstock is recycled plastic flake, a purpose-built plastic recycling extruder is a distinct machine class (källa: ThoYu), not a general-purpose unit you retrofit.
Compare wholesale prices for plastic extrusion machines
Pricing is where this market frustrates buyers, because a single “plastic extruder machine price” number is almost meaningless. In my experience the quoted machine cost represents only part of what you’ll actually pay. Below is the comparison framework I give clients, organized by the four channels above and the total-cost factors that most listings leave out.
Channel comparison across new, begagnad, imported, and lab-scale
| Kanal | Typical unit cost position | Lead time to service | Bäst passform | Main hidden cost |
|---|---|---|---|---|
| Domestic new (manufacturer/distributor) | Högsta | Fastest — local parts and techs | Production lines needing uptime guarantees | Premium on capacity |
| Begagnad / refurbished (till exempel, Aaron utrustning) | Lowest per unit of capacity | Moderate — depends on age and brand | High-horsepower industrial throughput on a budget | Wear on screw, fat, and gearbox |
| Import-direct (till exempel, ThoYu) | Low sticker, variable landed | Slow — ocean freight plus support gap | Volume buyers who can absorb logistics | Duties, frakt, and after-sales distance |
| Lab-scale specialty (till exempel, Amade-Tech) | Low absolute, high per-kg | Måttlig | R&D, sampling, small-batch trials | Not built for production volume |
The total cost of ownership factors most quotes omit
When I compare factory-direct extruder pricing against a domestic quote, I normalize both against total cost of ownership, inte klistermärkespris. The line items that reshape the decision are:
- Import duties and freight. For import-direct machines, ocean shipping and US import duties can add a meaningful percentage to a low sticker price. I always model the landed cost before comparing.
- Minsta orderkvantitet. Several wholesale suppliers price attractively only at a stated MOQ. If you need one machine, the per-unit rate can climb sharply.
- After-sales support and parts distance. A cheaper imported unit with no domestic parts pipeline can cost more over five years than a pricier domestic machine, because every downtime day compounds.
- Energy and throughput. Extrudermotorhästkrafter och extruderkapacitet driver dina driftskostnader. A 900 HP-enheter (källa: Aaron Utrustningslista) är bara ekonomiskt om du springer nära dess nominella kapacitet.
Branschsammanhang: varför prisintentionen är så hög
Sökbeteendet kring denna kategori domineras av pris, “near me,” USA, begagnad, and small-machine intents (källa: SERP/PAA data, 2025). Det mönstret speglar en verklig fragmentering på marknaden: köpare sträcker sig från små butiker som vill ha en enda extruder i laboratorieskala till anläggningar som köper kompletta extruderingslinjer. Takeaway jag delar med kunder är att “grossistpris” du ser annonseras är ett startankare, inte en leveranskostnad, och att jämföra ankare över kanaler utan att normalisera för TCO leder till beslut du ångrar inom ett år.
Köp plastextruderingsmaskiner i bulk till grossistpriser
Buying in bulk changes the negotiation entirely. When you commit to multiple units, you gain leverage on price, verktyg, and support terms, but you also concentrate risk. Here’s the procurement playbook I run when a client places a multi-unit order.
Key considerations for a bulk purchase
Första, standardize your specification across the order. I define one screw configuration, one L/D ratio, and one barrel and hopper feeder design, then order against that spec. Uniformity keeps spare parts interchangeable and simplifies operator training. Plastic in these machines is melted by electric heating tubes and converted to a uniform melt through screw extrusion and shearing (källa: ThoYu), so a consistent thermal profile across identical units also stabilizes product quality line to line.
Andra, negotiate custom die tooling into the bulk deal. Extruders produce continuous profiles including pipes, rör, filmer, brädor, och flaskor (källa: Amade-Tech), and the extrusion die determines which of those you can make. At bulk volume, I push for die tooling and a spare-screw set to be bundled rather than quoted separately, because that’s where suppliers hold margin.
Practical tips for structuring the deal
- Stage payments against inspection. I tie disbursements to factory acceptance testing on the first unit before the balance ships. This protects you if the first machine reveals a spec deviation.
- Confirm gearbox and service factor. Industrial extruders define torque delivery through gearbox reduction ratios and service factors — a 10.15:1 ratio with a 1.5 service factor is one documented example (källa: Aaron utrustning). Verify these match your torque demand before you multiply the order.
- Lock after-sales terms in writing. Spare-parts pricing, response time, and warranty should be part of the bulk contract, not a handshake. This is the single most overlooked clause I see.
- Split channels if it lowers risk. For a large order, I sometimes source proven production units domestically and add import-direct capacity from a vetted maker such as ThoYu for non-critical lines, balancing cost against support proximity.
Branschsammanhang: where bulk buyers find value
For plants building out capacity, the used market is often the smartest bulk play. Dealers like Aaron utrustning carry brand-specific single screw extruder inventory that lets you acquire high-horsepower capacity at a fraction of new-equipment cost, provided you inspect wear on the screw, fat, and gearbox. For continuous-profile production at volume, I weigh that against a new twin screw line when the resin mix demands tighter melt temperature control. The right answer depends on your polymer, your throughput target, and how much logistics complexity your team can absorb — which is exactly why a unified new-versus-used-versus-imported framework beats chasing the lowest advertised rate.
Bringing Your Extruder Sourcing Strategy Together
After walking through machine classes, specifikationer, and procurement channels, my closing advice is simple: treat a wholesale extruder purchase as a total-cost decision, not a sticker-price one. Whether you lean toward a factory-direct China wholesale plastic extruder, a refurbished single screw unit, or a domestically supported line, the machine only earns its keep when the L/D ratio, barrel zoning, växellådans reduktionsförhållande, and motor horsepower match the polymer you actually run.
Enligt min erfarenhet, the buyers who avoid expensive mistakes are the ones who define their feedstock and output profile before they shop. A shop running rigid PVC pipe has different melt temperature control and die tooling needs than one extruding HDPE film or compounding PEEK on a twin screw platform. Recycled plastic flake adds another layer, since recycling extruders and their screw configurations are engineered around contaminated, non-uniform feedstock rather than virgin pellets. Get that alignment right, and the rest of the negotiation, from minimum order quantity to after-sales support, falls into place.
Used equipment can be a genuine bargain when the provenance is clear. A documented listing such as a Davis Standard 9-inch extruder with a 32:1 L/D-förhållande, 7-zone barrel, och 900 HP DC-motor (Aaron Utrustningslista) gives you verifiable specifications to price against. My rule is to insist on that same level of detail from any wholesale supplier or manufacturer, new or imported, and to hold back final payment until the machine performs against agreed benchmarks.
Expertinsikt
| Nyckelpunkt | Förklaring |
|---|---|
| Match the machine to the polymer, not the price tag | Screw configuration, L/D-förhållande, and closed-loop barrel cooling should be selected around your resin. PVC, HDPE, polypropen, and PEEK each demand different melt temperature control and die tooling (Amade-Tech; ThoYu). |
| Demand verifiable specifications before you commit | Reputable listings publish concrete figures, such as a 32:1 L/D-förhållande, 7-zone barrel, och 900 HP motor with a defined gearbox reduction ratio and service factor (Aaron utrustning). Vague specs are a warning sign. |
| Factory-direct pricing still needs a landed-cost check | China-based manufacturers offer competitive wholesale pricing (ThoYu), but import duties, frakt, and commissioning can reshape the true total cost of ownership versus a domestically supported unit. |
Actionable Sourcing Tips for B2B Buyers
- Document your feedstock form (pulver, pellets, granule, or recycled flake) and target continuous cross-section profile before requesting quotes, so suppliers spec the right hopper feeder and screw configuration.
- Build a total-cost-of-ownership model that adds import duties, frakt, installation, spare barrels and screws, and energy draw to the base plastic extruder machine price.
- Compare at least one factory-direct manufacturer quote against one used extrusion equipment listing to benchmark value and negotiate from real numbers.
- Vet every wholesale machinery supplier for verifiable specs, referenser, och support efter försäljning, and confirm minimum order quantity terms up front.
- Protect payment with milestone-based terms tied to factory acceptance testing, and hold final release until the extruder capacity output meets your agreed benchmark.
- Confirm die tooling and gearbox parts availability in the US, since long lead times on custom die tooling can idle an otherwise capable extrusion production line.
FAQ
Where can I find plastic extrusion machine wholesale suppliers near me?
Enligt min erfarenhet, “near me” matters less than it feels like it should. Domestic dealers of used extrusion equipment give you faster inspection access and simpler logistics, and outfits like Aaron utrustning list single screw extruders with searchable specifications. But the wholesale market is genuinely global. I recommend defining your radius by two practical constraints: how far you are willing to travel for a pre-purchase inspection, and how much freight you can absorb. A local broker with limited inventory rarely beats a factory-direct source that ships a machine matched to your exact screw configuration and output requirements.
What determines plastic extruder machine price at wholesale?
Price tracks a handful of variables far more than brand alone. Barrel diameter and L/D ratio set the throughput ceiling; motor horsepower and gearbox reduction ratio define torque; and melt temperature control, closed-loop barrel cooling, and die tooling drive both cost and consistency. A high-torque, multi-zone industrial line will sit at a different tier than a lab-scale extruder. When I benchmark factory-direct extruder pricing, I ask suppliers to itemize the barrel, skruva, motor, and control package separately. That breakdown exposes where a low headline number is hiding a downgraded component.
Is a used plastic extrusion machine a smart wholesale buy?
It can be, provided you buy the physics rather than the price tag. Used extrusion equipment often delivers robust, over-built hardware that new budget imports cannot match. As an example of what to scrutinize, one used Davis Standard 9-inch extruder (Modell 80IN80HT) inbyggd 2001 par a 32:1 L/D-förhållande, a 7-zone barrel, och a 900 HP DC-motor (källa: Aaron Utrustningslista). Those specs signal serious capacity. My rule is simple: inspect the screw and barrel for wear, confirm the control system is serviceable and not obsolete, and budget for a refurbishment reserve. A well-maintained used single screw extruder frequently outperforms a cheaper new machine of unknown provenance.
Can I buy a small plastic extrusion machine at wholesale scale?
Profilextrudering Ja, and small does not mean unserious. Lab-scale and pilot extruders process feedstock in powder, pellets, or granule form for continuous polymer products with uniform cross section (källa: Amade-Tech). I steer smaller operations, product developers, och R&D teams toward these because they let you validate melt behavior and die tooling for materials like polypropylene, HDPE, or PEEK before committing to a full extrusion production line. Watch the minimum order quantity when buying direct; some manufacturers price small machines attractively only at multi-unit volumes.
How is the plastic extrusion machine wholesale market structured in the USA?
Praktiskt taget, US buyers work three channels: domestic manufacturers and dealers, importers reselling overseas builds, and factory-direct purchases from foreign makers. China-based manufacturers openly offer factory-direct wholesale pricing on plastic extruders (källa: ThoYu), which is why import routes dominate on cost. Search demand in this space splits fairly evenly across manufacturer, ecommerce, and informational sources (källa: SERP analysis, 2025), which mirrors how fragmented the buying journey actually is. For domestic sourcing, established equipment marketplaces remain the most transparent starting point for an industrial extruder for sale.
How do I choose a reliable plastic extrusion machine supplier?
I vet suppliers on evidence, not promises. I ask for documented specifications, reference customers running comparable materials, and a clear after-sales support commitment covering spare screws, fat, and control components. Payment protection is non-negotiable; I structure deposits against inspection and commissioning milestones rather than paying in full up front. For imports, I confirm the supplier can produce accurate specs for customs and provide the closed-loop barrel cooling, växellåda, and hopper feeder details that let me verify torque and throughput claims independently. A supplier who welcomes a third-party factory inspection is one I trust further.
What is the tradeoff between wholesale price and machine quality?
Headline price and total cost of ownership are different numbers. A cheaper machine that consumes more energy, wears screws faster, or lacks responsive after-sales support will cost more across five years than a pricier, better-built unit. My framework weighs four factors against the quote: energy draw, expected component life, downtime risk, and parts availability. The lowest factory-direct extruder pricing is a genuine bargain only when build quality, extruder capacity output, and support hold up. When they do not, I have watched buyers pay twice.
Where can I find a used plastic extrusion machine for sale I can trust?
Specialist used-equipment marketplaces are my first stop because they publish real specifications and brand-specific resale listings rather than vague descriptions. ThoYu, till exempel, positions itself as a factory-direct wholesale source and also highlights recycling extruders as a distinct class for reclaimed plastic flake feedstock (källa: ThoYu). Whether I am sourcing a PVC profile line or a plastic recycling extruder, I insist on a documented service history, a functional test under load, and clarity on shipping and import duties before any funds move.
Referenser
- Used Davis Standard 9-inch extruder (Modell 80IN80HT) features a 32:1 L/D-förhållande, 7-zone barrel, och 900 HP DC-motor, built 2001 — source: Aaron Utrustningslista — Planning analysis
- Lab plastic extrusion machines process feedstock in powder, pellets, or granule form for continuous polymer products with uniform cross section — source: Amade-Tech — Planning analysis
- Plastic in an extruder is melted by electric heating tubes and transformed to uniform melt via screw extrusion and shearing — source: ThoYu — Planning analysis
- Extruders produce continuous profiles including pipes, rör, filmer, brädor, and bottles — source: Amade-Tech — Planning analysis
- Multi-zone barrels commonly use electric heating with water (closed-loop) cooling — source: Aaron Utrustnings spec — Planning analysis
- Gearbox reduction ratios (till exempel, 10.15:1) and service factors (1.5) define torque delivery in industrial extruders — source: Aaron utrustning — Planning analysis
- Hopper-mounted feeding screws deliver raw material evenly into the barrel — source: ThoYu — Planning analysis
- China-based manufacturers offer factory-direct wholesale pricing on plastic extruders — source: ThoYu — Planning analysis
- Recycling extruders are a distinct machine class for reclaimed plastic feedstock — source: ThoYu — Planning analysis
- Single screw extruders are a common used-equipment category with brand-specific resale listings — source: Aaron utrustning — Planning analysis