

Belangrijkste afhaalrestaurants
- Bij kunststofextrusie wordt de ruwe hars gesmolten en tot een doorlopend profiel met een vaste doorsnede gevormd, waardoor het zeer geschikt is voor lang, productieruns met grote volumes (SeaGate-kunststoffen, 2024).
- Wanneer ik een fabrikant van kunststofprofielen evalueer, Ik scheid aangepaste extrusie, waarvoor een eenmalige investering in matrijzen en gereedschappen nodig is, uit voorraad geëxtrudeerde vormen die de initiële kosten overslaan (Thomasnet-leveranciersbegeleiding, 2024).
- Materiaalkeuze drijft alles stroomafwaarts: Ik match de toepassing met het juiste polymeer, of dat nu PVC is voor buizen en profielen, ABS of polycarbonaat voor slagvastheid, HDPE en LDPE voor chemische bestendigheid, polypropyleen voor levende scharnieren, acryl (PMMA) voor de duidelijkheid, of nylon van technische kwaliteit (PA) en PEEK voor veeleisende onderdelen.
- PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, gemeenschappelijk voor alle profielen, pijp, en buizen, Daarom vermelden veel leveranciers dit als standaardmogelijkheid (Vereniging van de Kunststofindustrie, 2023).
- Extrusietoleranties zijn losser dan bij spuitgieten vanwege materiaalkrimp en continue vorming, dus ik plan toleranties vroeg in plaats van uit te gaan van de precisie van het gegoten onderdeel (Protolabs, 2023).
- Ik behandel ISO 9001 als basissignaal van een volwassen kwaliteitsmanagementsysteem, geen garantie, en koppel het aan een concrete controlelijst voor de capaciteit, co-extrusie mogelijkheid, en doorlooptijd (ISO, 2015).
- Voor locatie-intentie, inkoop bij een binnenlandse kunststoffabrikant kan de totale aanlandkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten, een punt dat alleen al tegen de eenheidsprijs moet worden afgewogen (Reshoring-initiatief, 2023).
- Thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie, die ik meeneem in gesprekken over zowel kosten als duurzaamheid (Amerikaanse EPA, 2023).
- Beweert als “grootste” of “best” fabriek betekent weinig zonder context, dus benchmark ik leveranciers op gereedschapskosten, MOQ, snelle productie, en in plaats daarvan bewezen ondersteuning van prototype tot productie.
Wat kunststofextrusiebedrijven en fabrieken feitelijk doen
Wanneer ik een leverancier voor een klant evalueer, Ik begin met te verduidelijken wat het woord is “extrusie” daadwerkelijk beschrijft op de winkelvloer. Bij kunststofextrusie smelt het ruwe kunststofmateriaal en vormt het tot een doorlopend profiel met een vaste doorsnede (SeaGate-kunststoffen, 2024). Die ene zin heeft veel gewicht: het proces is continu en niet stap voor stap, en de geometrie wordt gedefinieerd door een tweedimensionale doorsnede die over de volledige lengte van het onderdeel loopt. Daarom past het zo goed bij lange productieruns en productie van grote volumes, en het is een heel andere discipline dan spuitgieten of verspanen.
In de praktijk, “hars extrusie” is de motor achter drie brede outputfamilies die ik het vaakst gevraagd zie:
- Profielen — op maat gemaakte kunststofprofielen met een gedefinieerde doorsnede, van eenvoudige kanalen en randafwerkingen tot complexe vormen met meerdere lumen. Dit is waar profielextrusie en co-extrusie echt tot hun recht komen.
- Slangen – rond, ovaal, en een buis met meerdere lumen die in de medische sector wordt gebruikt, vloeistofbehandeling, en pneumatische toepassingen, afkomstig van een gespecialiseerde leverancier van plastic buizen.
- Laken — extrusie van kunststofplaten voor panelen, voeringen, en thermovormmateriaal, geproduceerd door middel van een platte matrijs en rollenstapel.
Fabrikanten, Fabrieken, en distributeurs zijn niet hetzelfde
Kopers gebruiken deze termen vaak door elkaar, en dat kost ze tijd. Hier is hoe ik ze scheid:
- A fabrikant of fabriek is eigenaar van de extrusielijnen, snijdt zijn eigen matrijzen, en regelt het proces van hars tot afgewerkt onderdeel. Dit is wie je zoekt voor maatwerk, strakke procesbeheersing, of kunststoffen van technische kwaliteit.
- A distributeur of wederverkoper heeft standaardvormen op voorraad en verzendt deze, maar voert deze doorgaans niet uit. Ideaal voor uit voorraad geëxtrudeerde vormen en snelle nabestellingen, bij maatwerk is dat minder het geval.
- A vervaardiger kan voorraadprofielen en machines kopen, lassen, of assembleer ze tot afgewerkte producten voor kunststoffabricagediensten.
Als ik Thomasnet zoek, Ik filter bewust, omdat die mappen Amerikaanse plastic-extrusiefabrikanten opsommen en categoriseren op capaciteit en regio (Thomasnet, 2024). Dat capaciteitsfilter vertelt u of u met een echte fabrikant van kunststofprofielen of met een tussenpersoon praat.
Waarom kopers zoeken naar “Fabriek” In plaats van “Leverancier”
In mijn ervaring, de verschuiving naar “fabriek” taal duidt op intentie. Kopers die het typen, willen een bron met interne controle over het ontwerp en de gereedschappen van de matrijzen, transparante MOQ-gesprekken, en de mogelijkheid om van prototype naar productie te schalen. Het weerspiegelt ook de reshoring-druk: Binnenlandse inkoop kan de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten (Reshoring-initiatief, 2023), en de Amerikaanse kunststofindustrie blijft een belangrijke bijdrage leveren aan de binnenlandse productie en de werkgelegenheid (Vereniging van de Kunststofindustrie, 2023). Op zoek naar een binnenlandse kunststoffabrikant, in plaats van een generieke leverancier, is vaak een bewuste risico- en kostenbeslissing.
Hoe het plastic extrusieproces werkt, Stap voor stap

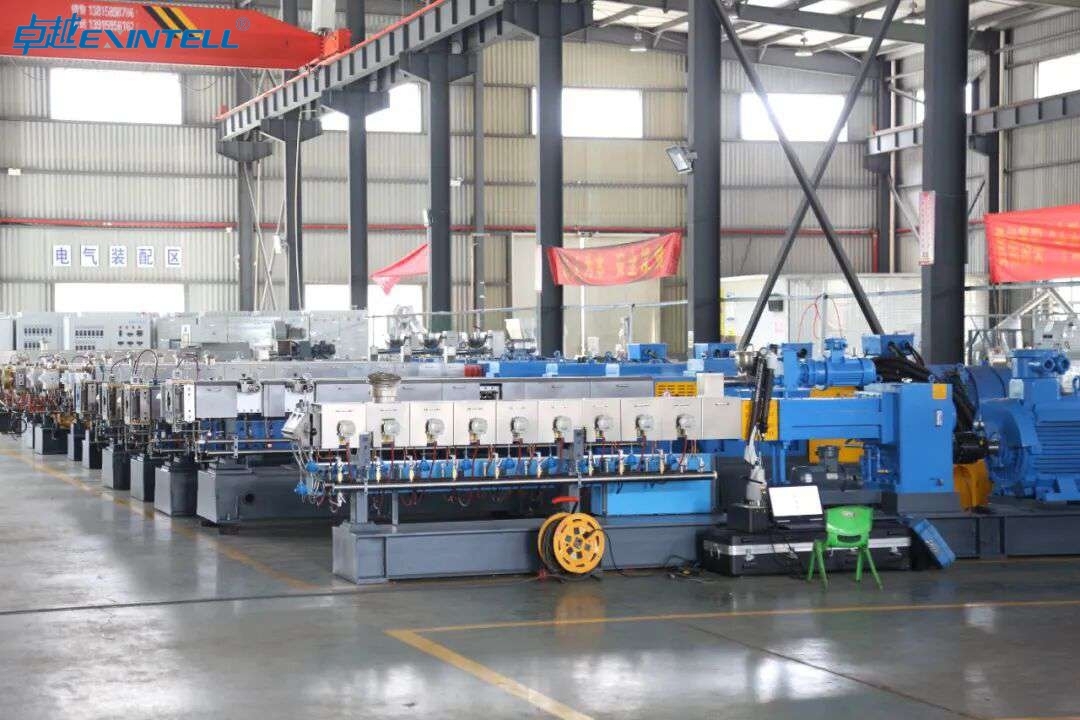
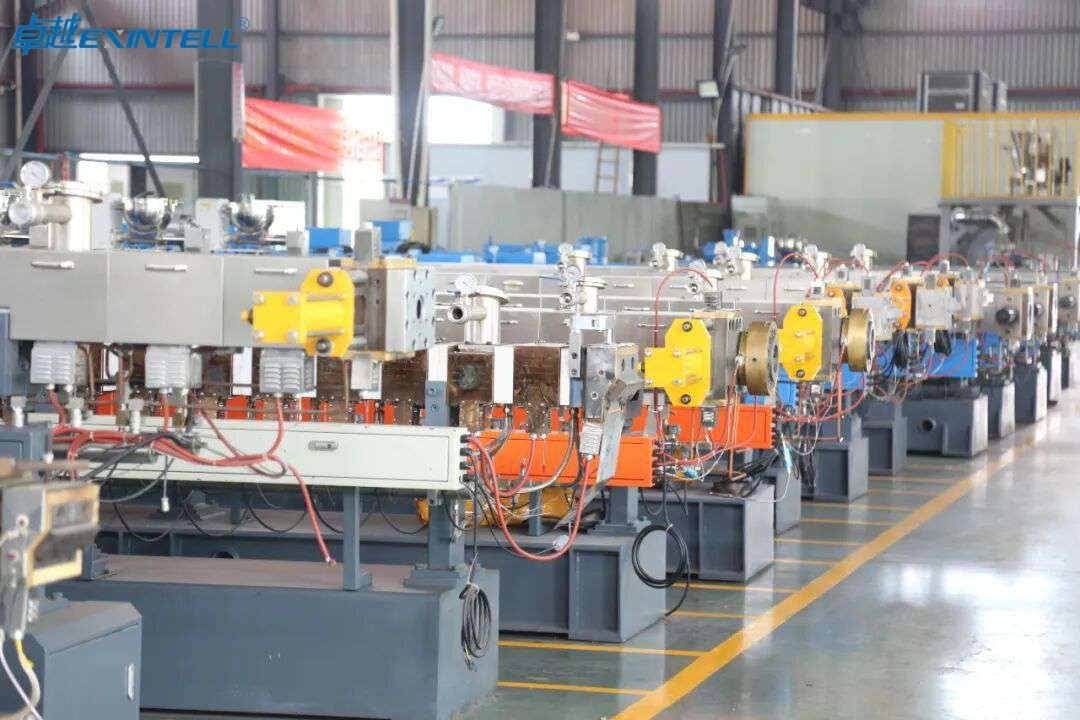
Als u de werking begrijpt, kunt u betere vragen stellen en een offerte nauwkeurig lezen. Fabrikant van dubbelschroefsextruders Ik begeleid klanten door vijf fasen van het continue extrusieproces.
1. Grondstoftoevoer en smelten in het vat
Thermoplastische pellets – gewoonlijk PVC, ABS, HDPE, LDPE, of polypropyleen – ga een trechter in en laat het met een roterende schroef in een verwarmd vat vallen. De combinatie van vatverwarmers en schroefschaar smelt de hars tot een homogene gesmolten stroom. Materiaalkeuze is hier van belang: PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, vaak gebruikt in profielen, pijp, en buizen (Vereniging van de Kunststofindustrie), terwijl polycarbonaat, acryl (PMMA), nylon (PA), en PEEK zijn veeleisender, toepassingen van technische kwaliteit. Gerecycled maalgoed kan vaak weer worden bijgemengd, en thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, Hergebruik van maalgoed verbetert dus de materiaalefficiëntie (Amerikaanse EPA, 2023).
2. Gesmolten plastic door een aangepaste matrijs dwingen
De smelt wordt door een matrijs geduwd die de profieldoorsnede definieert. Dit is de kern van het proces en de reden dat maatwerk gereedschapskosten met zich meebrengt. Bij een co-extrusieopstelling wordt gebruik gemaakt van meer dan één extruder die één matrijs voedt, waardoor u materialen kunt combineren: een stevig substraat met een zachte TPE/TPU-afdichtingslip, Bijvoorbeeld, of een gekleurde deklaag over een goedkopere kern.
3. Koeling, Maatvoering, en continue start
Het verlaten van de dobbelsteen, het zachte profiel gaat door een koel- en dimensioneringssysteem – meestal een waterbad of een vacuüm-sizentank – dat de afmetingen vastlegt. Een take-off (trekker) tekent het profiel met gecontroleerde snelheid. Omdat het onderdeel continu wordt gevormd en het materiaal krimpt als het afkoelt, extrusietoleranties zijn over het algemeen losser dan bij spuitgieten (Protolabs, 2023). Ik heb die verwachting vroeg gesteld, zodat klanten realistische toleranties specificeren in plaats van te betalen voor precisie die het proces economisch niet kan vasthouden.
4. Op lengte zagen en secundaire fabricage
Een lijnzaag of mes snijdt de continue uitvoer op lengte. Vanaf daar, secundaire bewerkingen — boren, ponsen, inkepingen, afdrukken, of assemblage: verander geëxtrudeerde plastic onderdelen in afgewerkte componenten. Dit is de brug tussen het ruwe profiel en een bruikbaar resultaat, en het is waar snelle productie wordt gewonnen of verloren.
Aangepaste versus standaard kunststof extrusies: Welke heb je nodig?
Dit is de beslissing waar ik het meest naar gevraagd word, en het eerlijke antwoord is: het hangt af van het volume, geometrie, en tijdlijn. Laat me elk pad opsplitsen.
Wanneer kant-en-klare voorraadprofielen de juiste keuze zijn
Voorraad geëxtrudeerde vormen - standaard staaf, buis, kanaal, hoek, en plaat — vermijd de gereedschapskosten volledig en verzend snel. Of een catalogusprofiel binnen aanvaardbare tolerantie bij uw toepassing past, aandelen kopen is bijna altijd goedkoper, sneller traject. Ik stuur klanten hierheen voor prototypes, lage volumes, en elk onderdeel waar een standaard doorsnede het werk doet.
Wanneer aangepaste gereedschappen en profielen gerechtvaardigd zijn
Aangepaste extrusie vereist doorgaans een eenmalige investering in gereedschap en matrijzen, terwijl aandelenprofielen deze kosten vermijden (begeleiding bij inkoop in de sector). Die matrijskosten zijn gerechtvaardigd als uw geometrie bedrijfseigen is, wanneer een aangepaste doorsnede de stroomafwaartse montage elimineert, of wanneer het jaarlijkse volume hoog genoeg is om het gereedschap af te schrijven. Boven een bepaalde runsize, de besparingen per voet van een speciaal gebouwde matrijs wegen zwaarder dan de uitgaven vooraf.
De hybride aanpak: Standaard profielen, Aangepaste onderdelen
Mijn favoriete middenweg wordt vaak over het hoofd gezien. Standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen (SeaGate-kunststoffen, 2024). Je slaat de dobbelsteeninvestering over, gebruik dan snijden, bewerking, en montage om tot een maatwerklevering te komen. Voor veel middenvolumeprogramma's, deze hybride verslaat zowel pure voorraad als volledig maatwerk wat de totale kosten betreft.
Vergelijking van kosten en doorlooptijd
Hier ziet u hoe de drie benaderingen zich in het algemeen met elkaar vergelijken. Behandel deze als richtinggevende planningsgebieden, geen citaten - werkelijke cijfers zijn afhankelijk van materiaal, geometrie, en volume.
|
Factor |
Voorraadprofielen |
Hybride (Vervaardigde standaard) |
Volledige aangepaste extrusie |
|---|---|---|---|
|
Gereedschapskosten vooraf |
Geen |
Geen te laag (alleen armaturen) |
Eenmalige investering in matrijzen |
|
Typische doorlooptijd |
Kortste (Vaak op voorraad) |
Kort tot matig |
Langste (sterven bouwen + eerste artikel) |
|
Minimale bestelling (MOQ) |
Laag |
Laag tot matig |
Hoger (gereedschap afschrijven) |
|
Flexibiliteit van de geometrie |
Alleen catalogusvormen |
Standaard vorm + bewerking |
Volledig op maat gemaakte doorsnede |
|
Beste pasvorm |
prototypen, laag volume |
Middenvolume, milde maatwerk |
Hoog volume, eigen profielen |
|
Factor |
Voorraadprofielen |
Hybride (Vervaardigde standaard) |
Volledige aangepaste extrusie |
|---|---|---|---|
|
Gereedschapskosten vooraf |
Geen |
Geen te laag (alleen armaturen) |
Eenmalige investering in matrijzen |
|
Typische doorlooptijd |
Kortste (Vaak op voorraad) |
Kort tot matig |
Langste (sterven bouwen + eerste artikel) |
|
Minimale bestelling (MOQ) |
Laag |
Laag tot matig |
Hoger (gereedschap afschrijven) |
|
Flexibiliteit van de geometrie |
Alleen catalogusvormen |
Standaard vorm + bewerking |
Volledig op maat gemaakte doorsnede |
|
Beste pasvorm |
prototypen, laag volume |
Middenvolume, milde maatwerk |
Hoog volume, eigen profielen |
Welk pad je ook kiest, Ik raad aan om te bevestigen dat de winkel een gedocumenteerd kwaliteitssysteem hanteert: ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (ISO, 2015) en blijft de meest algemeen aanvaarde benchmark in de kunststofsector. Voor een praktische kijk op hoe voorraad en maatwerkaanbod naast elkaar bestaan, Ik vind SeaGate-kunststoffen’ aangepast extrusieoverzicht een nuttig referentiepunt.
Soorten kunststof extrusieprofielen en producten

Wanneer ik een project evalueer voor extrusie, Ik begin met de dwarsdoorsnede, omdat de geometrie van het voltooide onderdeel bijna alles stroomafwaarts dicteert: het matrijsontwerp, de materiaalkeuze, en uiteindelijk de prijs die u betaalt. Bij kunststofextrusie wordt de ruwe hars gesmolten en tot een doorlopend profiel met een vaste doorsnede gevormd (SeaGate-kunststoffen, 2024). Dat ene principe levert een verrassend brede catalogus van vormen op, dus het helpt om ze te groeperen op complexiteit en functie.
Stevige profielen, Holle profielen, en complexe geometrieën
Solide profielen zijn de werkpaarden van de branche: staven, balken, randen, en trimmen zonder interne holtes. Ze zijn het gemakkelijkst te bewerken en het meest vergevingsgezind op het gebied van tolerantie, Daarom raad ik ze aan voor beginnende kopers die een ontwerp testen. Holle profielen introduceren interne kanalen, en ze eisen meer geavanceerde matrijzen met doornen of pennen om de holte open te houden terwijl de smelt afkoelt. Complexe geometrieën combineren meerdere wanden, ondersnijdingen, en dunne-naar-dik-overgangen in een enkele doorsnede, en dit is waar de expertise op het gebied van matrijsontwerp en gereedschap een capabele fabrikant van kunststofprofielen onderscheidt van een gemiddelde fabrikant. In mijn ervaring, ongelijkmatige wanddikte is de meest voorkomende oorzaak van kromtrekken, Daarom dring ik er al vroeg bij leveranciers op aan hoe ze de materiaalstroom over het hele profiel willen balanceren.
Slangen en extrusies met meerdere lumen
Tubing is een gespecialiseerde subset van holle extrusie, en het omvat alles, van eenvoudige buizen met één boring tot ontwerpen met meerdere lumen met verschillende parallelle kanalen over de lengte van het onderdeel. Kopers van medische apparatuur en analytische instrumenten vertrouwen op extrusies met meerdere lumen om vloeistoffen te transporteren, draden, en sensoren via één compact profiel. Een betrouwbare leverancier van plastic buizen zal strikte toleranties op het gebied van concentriciteit en binnendiameter hanteren, hoewel ik klanten er altijd aan herinner dat extrusietoleranties over het algemeen losser zijn dan bij spuitgieten vanwege materiaalkrimp en continue vorming (Protolabs-ontwerpbronnen, 2023). Plan uw fit en speling rond die realiteit in plaats van ertegen te vechten.
Co-extrusie en multimateriaalprofielen
Bij co-extrusie worden twee of meer harsen door een gedeelde matrijs geleid om één enkel profiel met verschillende materiaalzones te produceren. Ik gebruik het wanneer een onderdeel in één keer conflicterende eigenschappen nodig heeft, zoals een stijve PVC-constructie met een zachte TPE/TPU-pakkinglip, of een weerbestendige deklaag over een goedkoper substraat. Het elimineert secundaire montage- en verbindingsstappen, wat een betekenisvolle kostenbesparing op volume oplevert. De wisselwerking is het beheersen van de complexiteit, daarom reserveer ik co-extrusie voor ontwerpen waarbij het multimateriaalvoordeel de extra investering in de matrijs duidelijk rechtvaardigt.
Veel voorkomende industriële toepassingen voor elk type
Verschillende geometrieën neigen naar verschillende sectoren, Door ze vroegtijdig te matchen, blijven de gesprekken gefocust.
- Stevige profielen: rand van winkelschappen, meubelbekleding, zeehonden, en hekwerkonderdelen.
- Holle profielen: raam- en deurkozijnen, LED-lichtkanalen, en structurele bekleding.
- Slangen en multi-lumen: medische katheters, vloeistofoverdrachtlijnen, en pneumatische buizen.
- Gecoëxtrudeerde profielen: weer strippen, koelpakkingen, en handgrepen met dubbele durometer.
- Extrusie van platen: bewegwijzering, thermovormende voorraad, en beschermpanelen.
Omdat plastic extrusie continu is, proces met een hoog volume, het past bijzonder goed bij lange productieruns, en standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen (SeaGate-kunststoffen, 2024). Als uw jaarlijkse vraag stabiel is en wordt gemeten in de tienduizenden meters, extrusie-economie werkt sterk in uw voordeel.
Veel voorkomende materialen die worden gebruikt bij kunststofextrusie
Materiaalkeuze is de beslissing die kopers het vaakst zie onderschatten. De hars regelt de mechanische sterkte, chemische weerstand, temperatuur bereik, kosten, en zelfs hoe strak de tolerantie de extruder realistisch kan aanhouden. Ik groepeer extrusieharsen in drie lagen, Werk vervolgens samen met klanten om alleen vooruitgang te boeken voor zover de toepassing dit echt vereist.
Grondstofharsen: PVC, Polyethyleen, en polypropyleen
Grondstofharsen bestrijken het grootste deel van het geëxtrudeerde volume, en met goede reden. PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, gebruikelijk in profielen, pijp, en buizen (Vereniging van de Kunststofindustrie). Het biedt stijfheid, weerbestendigheid, en lage kosten, en het vergt kleur en oppervlakteafwerking goed. Polyethyleen komt voor in twee bekende kwaliteiten: HDPE voor stijf, chemisch bestendige profielen en LDPE waar flexibiliteit belangrijk is. Polypropyleen combineert chemische bestendigheid met een goede sterkte-gewichtsverhouding en goede scharnierprestaties. Wanneer een klant vraagt naar harsextrusie voor een groot volume, kostengevoelig onderdeel, dit is bijna altijd waar ik begin.
Technische harsen: ABS, Polycarbonaat, Nylon, en acryl
Kunststof van technische kwaliteit verbetert de mechanische en thermische prestaties. ABS levert slagvastheid en schone afwerkingen voor consumenten- en behuizingsonderdelen. Polycarbonaat zorgt voor een hoge slagvastheid en optische helderheid, waardoor het een basisproduct is voor verlichtingslenzen en veiligheidsbeglazing. Nylon (PA) biedt slijtvastheid en taaiheid voor mechanische componenten en kabelbeheer. Acryl (PMMA) biedt uitstekende helderheid en UV-stabiliteit voor display- en signage-profielen. Ik verplaats kopers naar dit niveau wanneer grondstoffenharsen niet aan de belasting kunnen voldoen, warmte, of duidelijkheidseisen, en ik zorg ervoor dat ze de harspremie afzetten tegen de prestatiewinst voordat ze zich engageren.
Hoogwaardige materialen zoals PEEK
Bovenaan zit een kleine groep hoogwaardige polymeren, met PEEK als referentiepunt. PEEK is bestand tegen continu hoge temperaturen, agressieve chemicaliën, en veeleisende mechanische belastingen, Daarom verschijnt het in de lucht- en ruimtevaart, medisch, en halfgeleidertoepassingen. De materiaalkosten zijn aanzienlijk, dus ik specificeer het alleen als de besturingsomgeving geen goedkopere optie biedt. Niet elke fabrikant van kunststofprofielen verwerkt PEEK, dus het screenen van capaciteiten is op dit niveau belangrijker.
Materiaaleigenschappen afstemmen op toepassingsvereisten
Mijn selectiekader is bewust eenvoudig gehouden: definieer eerst de niet-onderhandelbare eis, kies dan de minst dure hars die het reinigt. De onderstaande tabel vat samen hoe ik de gebruikelijke opties voor geëxtrudeerde kunststof onderdelen afweeg.
| Materiaal | Laag | Belangrijkste sterke punten | Relatieve kosten | Typische toepassingen |
|---|---|---|---|---|
| PVC | Product | Onbuigzaam, weerbestendig, lage kosten | $ | Profielen, pijp, trimmen |
| HDPE / LDPE | Product | Chemische resistentie; stijf of flexibel | $ | Slangen, voeringen, leidingwerk |
| Polypropyleen | Product | Chemische resistentie, levende scharnieren | $ | Vloeistofbehandeling, scharnieren |
| ABS | Engineering | Slagvastheid, schone afwerking | $$ | Behuizingen, consumenten onderdelen |
| Polycarbonaat | Engineering | Slagvastheid, helderheid | $$ | Lenzen, veiligheidsbeglazing |
| Nylon (PA) | Engineering | Slijtvastheid, taaiheid | $$ | Mechanisch, kabelgeleiders |
| Acryl (PMMA) | Engineering | Helderheid, UV-stabiliteit | $$ | Bewegwijzering, displays |
| KIJKJE | Hoge prestaties | Warmte, chemisch, en belastingsweerstand | $$$$ | Lucht- en ruimtevaart, medisch, halfgeleider |
Eén efficiëntiepunt dat de moeite waard is om bij elke leverancier te bespreken: thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie (Amerikaanse Environmental Protection Agency, 2023). Als ik vraag hoe een fabriek omgaat met maalgoed, zegt dat iets over zowel hun kostendiscipline als hun duurzaamheidspraktijken.
Fabrikanten van kunststofextrusie in de VS
Voor veel van de kopers adviseer ik, de sourcing-vraag is niet alleen “wie kan dit profiel extruderen” Maar “wie kan het hier extruderen.” Binnenlandse inkoop is van een voorkeur naar een strategische beslissing gegaan, en het verdient een heldere blik in plaats van reflexief patriottisme.
Waarom in de VS gevestigde sourcing voor veel kopers belangrijk is
De financiële argumenten zijn sterker dan op het eerste gezicht lijkt. Reshoring en binnenlandse inkoop kunnen de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten (Reshoring-initiatief, 2023). Wanneer ik een vergelijking van de totale kosten uitvoer in plaats van een vergelijking van de eenheidsprijzen, offshore-besparingen worden vaak kleiner als ik zeevracht erbij doe, tarieven, veiligheidsvoorraad, en het werkkapitaal dat vastzit aan lange transittijden. Voor een binnenlandse kunststoffabrikant die een Amerikaanse klant bedient, Doorlooptijden gemeten in weken in plaats van maanden betekenen ook minder risico als een ontwerp halverwege het programma verandert.
Regionale productiehubs in het hele land
De Amerikaanse extrusiecapaciteit is niet gelijkmatig verdeeld, en het kennen van de kaart versnelt de inkoop. De Grote Meren en het Upper Midwest concentreren universele profiel- en buisextruders in de buurt van de vraag uit de automobiel- en industriële sector. Het noordoosten herbergt een dicht cluster van medische en precisieslangspecialisten. Het zuidoosten is snel gegroeid rond het bouwen van producten en verpakkingen. De westkust en het zuidwesten bedienen elektronica, ruimtevaart, en consumentenmarkten. Leveranciersgidsen zoals Thomasnet geven een overzicht en categoriseren Amerikaanse fabrikanten van kunststofextrusie op basis van capaciteit en regio (Thomasnet, 2024), Hier maak ik meestal een eerste shortlist voordat ik bel.
Binnenlandse kwaliteit, Mededeling, en IP-voordelen
Buiten de kosten, drie praktische voordelen blijven kopers naar huis lokken. Eerst, kwaliteitssystemen zijn gemakkelijker persoonlijk te verifiëren; ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (Internationale Organisatie voor Standaardisatie, 2015), en ik kan de implementatie van een binnenlandse leverancier controleren zonder een internationale reis. Seconde, op tijdzone afgestemde communicatie verkort de feedbackloop van prototype naar productie, wat van belang is als een dobbelsteen halverwege de run moet worden aangepast. Derde, Bescherming van intellectueel eigendom is beter afdwingbaar onder Amerikaanse jurisdictie, een echte zorg wanneer een aangepast profiel een concurrentiedifferentiator is. Ik behandel deze als de verschillen die een spreadsheet alleen zal missen.
Hoe Amerikaanse fabrieken diverse industrieën bedienen
Amerikaanse extruders bestrijken het volledige scala van contractproductie, van uit voorraad geëxtrudeerde vormen verzonden vanuit de inventaris tot volledig op maat gemaakte matrijsprogramma's. Aangepaste extrusie vereist doorgaans een eenmalige investering in gereedschap of matrijzen, terwijl aandelenprofielen die kosten vermijden, dus ik stem het inkooppad af op hoe uniek de geometrie werkelijk moet zijn. De Amerikaanse kunststofindustrie blijft een belangrijke bijdrage leveren aan de binnenlandse productie en de werkgelegenheid (Vereniging van de Kunststofindustrie, 2023), en die diepte betekent dat een koper doorgaans een partner voor kunststoffabricagediensten kan vinden die geschikt is voor zijn volume, van prototype tot productie. Voor een breed overzicht van maatwerkmogelijkheden, Ik wijs cliënten vaak op overzichten zoals aangepaste fabrikanten van kunststof extrusie om de verwachtingen te kalibreren voordat u offertes aanvraagt.
Hoe u kunststofextrusiebedrijven bij u in de buurt kunt vinden
Als ik aan een sourcingproject begin, geografie is een van de eerste variabelen die ik weeg. Locatie bepaalt de vrachtkosten, communicatie cadans, en hoe snel ik van prototype naar productie kan itereren. Dat gezegd hebbende, Nabijheid is alleen waardevol als de nabijgelegen leverancier het werk ook daadwerkelijk kan doen. In mijn ervaring, de slimste aanpak behandelt “bij mij in de buurt” als filter, geen besluit.
Waarom lokale inkoop vaak loont
Een binnenlandse kunststoffabrikant bij u in de buurt biedt u drie concrete voordelen. Eerst, kortere verzendafstanden verlagen het vracht- en doorlooprisico, wat van belang is voor omvangrijke geëxtrudeerde plastic onderdelen en lange profielen die als extra grote vracht worden verzonden. Seconde, lokale partners maken bezoeken ter plaatse praktisch, en ik heb meer procesproblemen ontdekt tijdens een twee uur durende rondleiding door de fabriek dan in wekenlange e-mail. Derde, nabijheid versnelt de iteratie: wanneer een dobbelsteen een aanpassing nodig heeft, een leverancier op een paar uur afstand kan monsters sneller omdraaien dan een leverancier aan de andere kant van de oceaan.
De financiële argumenten reiken verder dan de eenheidsprijs. Volgens het Reshoring-initiatief (2023), Binnenlandse inkoop kan de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten. De binnenlandse basis is substantieel, te; de Vereniging van de Kunststofindustrie (2023) meldt dat de Amerikaanse kunststofindustrie een belangrijke bijdrage levert aan de binnenlandse productie en de werkgelegenheid, wat betekent dat gekwalificeerde capaciteit voor harsextrusie meestal binnen handbereik is.
Waar ik kijk: Telefoonboeken, Verenigingen, en verwijzingen
Om een eerste lijst met kandidaten op te stellen, Ik gebruik drie complementaire kanalen:
- Leveranciersgidsen. Thomasnet (2024) somt en categoriseert Amerikaanse fabrikanten van kunststofextrusie op capaciteit en regio, waardoor het eenvoudig is om op materiaal te filteren, proces, en locatie.
- Vakverenigingen. Het lidmaatschap van organen als de Plastics Industry Association duidt op een bedrijf dat investeert in normen en betrokkenheid van de industrie.
- Verwijzingen. Een aanbeveling van een ingenieur die productie heeft uitgevoerd bij een fabrikant van kunststofprofielen weegt zwaarder dan welke marketingpagina dan ook, omdat het de geleverde prestaties weerspiegelt.
Ik behandel de directory als startpunt voor een leverancier van kunststofbuizen of een profielwinkel, valideer vervolgens elke naam aan de hand van echte referenties voordat deze een plek op mijn shortlist verdient.
Nabijheid in evenwicht brengen met mogelijkheden en prijs
Afstand is een tiebreak, geen troefkaart. Als een winkel in de buurt niet aan uw toleranties kan voldoen, voer je hars uit, of voldoe aan uw volume, het gemak is waardeloos. Ik rangschik capaciteit en kwaliteit op de eerste plaats, dan prijs, dan locatie. Een plastic extrusiebedrijf dat twee staten verderop fabrieksleverancier is met de juiste co-extrusielijn en een bewezen ISO 9001 systeem zal mij meestal beter van dienst zijn dan een winkel dichterbij die deze mogelijkheden niet heeft.
Wanneer lokaal niet de beste optie is
Soms is de juiste partner niet in de buurt. Gespecialiseerd werk in kunststoffen van technische kwaliteit, zoals PEEK, polycarbonaat, of nylon (PA) kan landelijk alleen goed worden gedaan door een handvol winkels. Productieprogramma's voor grote volumes kunnen een scheepvaarteconomie rechtvaardigen die de voorkeur geeft aan een verre toekomst, meer geautomatiseerde fabriek. En als u mogelijkheden nodig heeft zoals de extrusie van kunststofplaten in combinatie met in-line fabricage, de pasvorm van het proces is belangrijker dan het aantal kilometers. In die gevallen vergroot ik de zoekradius en vertrouw ik op videorondleidingen door fabrieken en audits door derden om de afstandskloof te dichten.
Inzicht in de grootste kunststofextrusiebedrijven
Kopers worden vaak aangetrokken door de grootste namen, ervan uitgaande dat schaal een beter resultaat garandeert. Schaal levert echte voordelen op, maar het brengt ook afwegingen met zich mee. Begrijpen wat “grootste” betekent eigenlijk dat het mij helpt de voetafdruk van een leverancier af te stemmen op mijn programma in plaats van op een reputatie.
Wat schaal betekent voor capaciteit en betrouwbaarheid
Extrusie is een continu proces, hoogvolumeproces dat zeer geschikt is voor lange productieruns, en grote fabrieken worden rond die realiteit gebouwd. Meer extrusielijnen betekenen een hogere doorvoer, redundantie als een lijn uitvalt, en het vermogen om vraagpieken op te vangen. Schaal correleert meestal ook met volwassen kwaliteitssystemen; ISO 9001, de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (Internationale Organisatie voor Standaardisatie, 2015), is bijna een tafelpaal tussen grote planten. Die volwassenheid vertaalt zich in consistentere geëxtrudeerde plastic onderdelen over lange runs.
De afwegingen tussen grote fabrieken en. Gespecialiseerde winkels
Groter is niet automatisch beter. Grote planten optimaliseren het volume, wat hogere minimale bestelhoeveelheden kan betekenen, minder flexibiliteit bij kleine op maat gemaakte runs, en langzamere reactiesnelheid op prototypewerk. Een gespecialiseerde winkel kan uitblinken in op maat gemaakte kunststof profielen met nauwe toleranties, ongebruikelijke harsen, of productie met een snelle doorlooptijd die een fabriek met grote volumes als hinderlijk beschouwt. De onderstaande tabel vat samen hoe ik de twee weeg.
| Factor | Grootschalige fabriek | Gespecialiseerde winkel |
|---|---|---|
| Capaciteit | Hoog; meerdere lijnen, ontslag | Beperkt; minder lijnen |
| Minimale bestelhoeveelheid | Vaak hoog | Meestal flexibel |
| Snelheid prototype | Langzamer; volumegerichte planning | Sneller; wendbare opstelling |
| Materiaal bereik | Brede basisharsen (PVC, HDPE, LDPE, PP) | Vaak van technische kwaliteit (KIJKJE, PC, PA) |
| Prijs per eenheid op volume | Lager | Hoger |
| Beste pasvorm | Lange productieruns | Aangepast, laag tot midden volume, complexe profielen |
Wanneer capaciteit voor grote volumes essentieel is
Er zijn programma's waarbij ik geen concessies doe aan de schaalgrootte. Continu, lange termijn vraag naar gestandaardiseerde profielen, pijp, of slangen in basisharsen zijn de natuurlijke thuisbasis van een grote fabriek. PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, vaak gebruikt in profielen, pijp, en buizen, en het op grote schaal inkopen ervan beloont de economieën die een grote fabriek biedt. Als uw voorspelling miljoenen meters stabiele profieldwarsdoorsnede vereist, capaciteiten voor grote volumes gaan van nice-to-have naar essentieel.
Hoe u de geclaimde schaal en capaciteit kunt verifiëren
Beweringen op een website zijn geen bewijs. Voordat ik een “grootste” of “hoogste capaciteit” claim, Ik verifieer het met concrete vragen:
- Hoeveel extrusielijnen zijn er operationeel?, en wat is het matrijsdiameterbereik op elk?
- Wat is het huidige gebruik, en hoeveel reservecapaciteit er is voor mijn programma?
- Kunt u doorstroomcijfers delen? (kg/uur of voet/dag) voor een vergelijkbaar profiel?
- Welke redundantie bestaat er als een lijn halverwege uitvalt??
- Welke certificeringen, zoals ISO 9001, zijn actueel, en mag ik het certificaat zien?
Die antwoorden koppel ik aan een fabrieksrondleiding of audit. Fysiek bewijs van lopende lijnen, personeelsbezetting, en inventaris vertelt mij veel meer dan welk capaciteitscijfer dan ook dat in een brochure wordt vermeld.
Hoe u de beste kunststofextrusiefabriek voor uw project kunt identificeren
“Best” is een van de meest misbruikte woorden in leveranciersmarketing. In de praktijk, de beste fabrieksfabrikant van kunststofextrusiebedrijven is degene die het beste bij uw specifieke vereisten past, niet degene met de luidste bewering. Ik definieer de term in relatie tot mijn project, scoor vervolgens kandidaten op basis van die definitie.
Het definiëren “Best” In verhouding tot uw specifieke behoeften
Voordat u leveranciers gaat vergelijken, Ik documenteer wat mijn project eigenlijk vraagt: de hars (inspraak, ABS voor slagvastheid, acryl (PMMA) voor optische helderheid, of TPE/TPU voor flexibiliteit), de tolerantieband, het volume, de tijdlijn, en het niveau van technische ondersteuning dat ik nodig heb voor het ontwerp en de gereedschappen van matrijzen. Extrusietoleranties zijn over het algemeen losser dan bij spuitgieten vanwege materiaalkrimp en continue vorming (Protolabs-ontwerpbronnen, 2023), dus ik bevestig vroeg dat een kandidaat aan mijn maatvereisten kan voldoen in plaats van aan te nemen dat dit mogelijk is. Een werkplaats die ideaal is voor een groot volume aan HDPE-leidingen kan de verkeerde keuze zijn voor een polycarbonaatprofiel met nauwe toleranties.
Weegkwaliteit, Kosten, Snelheid, en ondersteuning
Bij elke inkoopbeslissing zijn vier hefbomen in evenwicht, en het verbeteren van de een zet de ander vaak onder druk:
- Kwaliteit. Gedocumenteerde kwaliteitssystemen, inspectie tijdens het proces, en traceerbaarheid van materialen. ISO 9001 is de meest algemeen aanvaarde standaard voor kwaliteitsmanagement in productiesectoren, inclusief kunststoffen.
- Kosten. Niet alleen de eenheidsprijs. Aangepaste extrusie vereist doorgaans een eenmalige investering in gereedschap en matrijzen, terwijl op voorraad geëxtrudeerde vormen die kosten vermijden, dus ik modelleer de totale kosten inclusief gereedschap en MOQ.
- Snelheid. Standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen (SeaGate-kunststoffen, 2024), maar de doorlooptijden variëren sterk tussen winkels.
- Steun. Technische input op het gebied van profieldoorsnede en materiaalkeuze kan kostbare herontwerpen voorkomen als u van prototype naar productie gaat.
Duurzaamheid speelt ook steeds meer een rol. Thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie (Amerikaanse Environmental Protection Agency, 2023), die zowel de kosten als de verspilling kunnen verminderen als een leverancier er op verantwoorde wijze mee omgaat.
Verleden lezen “Best” Marketingclaims
Superlatieven zijn gemakkelijk af te drukken en moeilijk te bewijzen. Als ik het zie “best,” “leidend,” of “premier,” Ik vertaal de claim naar een toetsbare vraag. In plaats van te accepteren “beste kwaliteit,” Ik vraag naar defectpercentages en inspectiegegevens. In plaats van “snelste,” Ik vraag om typische doorlooptijden voor mijn specifieke onderdeel. In plaats van “meest ervaren,” Ik vraag om referenties in mijn branche. Marketingtaal die een vervolgvraag niet kan overleven, heeft geen invloed op mijn shortlist.
Het bouwen van een shortlistscoremethode
Om de vergelijking objectief te houden, Ik gebruik een gewogen scoremodel. Ik zet mijn criteria op een rij, wijs elk een gewicht toe dat het belang ervan voor het project weerspiegelt, scoort elke kandidaat uit 1 naar 5, en vermenigvuldigen. De gewichten verschuiven per project; een prototypeprogramma zou snelheid en technische ondersteuning zwaar kunnen belasten, terwijl een volwassen productieprogramma kosten en capaciteit weegt.
- Lijstcriteria: kwaliteitssystemen, materieel vermogen, tolerantie, capaciteit, doorlooptijd, gereedschap kosten, technische ondersteuning, en locatie.
- Gewichten toewijzen dat totaal 100 procent, weerspiegelt uw prioriteiten.
- Geef elke leverancier een score 1 naar 5 op elk criterium, gebruik van geverifieerd bewijsmateriaal in plaats van marketingclaims.
- Bereken gewogen totalen en rangschik de kandidaten.
- Valideer de bovenste twee met referentieoproepen en, ideaal, een fabrieksbezoek voordat u zich engageert.
Deze gestructureerde werkwijze heeft mij consequent naar de partner gestuurd die bij het werk past, of dat een grote plant blijkt te zijn, een vlotte specialist, of een woonwinkel verderop in de straat. Voor een dieper inzicht in hoe aangepaste extrusiemogelijkheden betrekking hebben op toepassingen, middelen zoals SeaGate-kunststoffen’ aangepast extrusieoverzicht zijn een nuttige referentie als u uw eigen criteria verfijnt.
Belangrijkste mogelijkheden om te evalueren in een kunststofextrusiebedrijf
Wanneer ik een fabrikant van kunststofprofielen onderzoek, Ik kijk
Toleranties en precisie in geëxtrudeerde onderdelen
Wanneer ik een fabrikant van kunststofprofielen evalueer, toleranties zijn de eerste plaats waar ik op zoek ben naar een reality check. Extrusie is een continu vormingsproces, het gedraagt zich dus anders dan gieten. Zoals Protolabs opmerkt, extrusietoleranties zijn over het algemeen losser dan bij spuitgieten, omdat materiaalkrimp en continu vormen een variabiliteit introduceren die een gesloten mal niet heeft (Protolabs-ontwerpbronnen, 2023). Het vroegtijdig stellen van verwachtingen bespaart zowel geld als later herwerk.
Typische haalbare toleranties per materiaal en profiel
In mijn ervaring, De haalbare nauwkeurigheid hangt sterk af van de hars en de geometrie van de profieldwarsdoorsnede. Stijve kunststoffen van technische kwaliteit hebben kleinere afmetingen dan zachte of semi-kristallijne materialen, en eenvoudige vormen zitten steviger dan complexe holle profielen. De onderstaande bereiken weerspiegelen vaak genoemde commerciële extrusiemogelijkheden voor op maat gemaakte kunststofprofielen; Bevestig altijd aan de hand van de door uw leverancier gepubliceerde normen voor uw specifieke onderdeel.
| Materiaal | Dimensionale stabiliteit | Typische neiging tot tolerantie | Opmerkingen voor het specificeren |
|---|---|---|---|
| Hard PVC | Hoog | Strakker, goed gecontroleerd | Op grote schaal geëxtrudeerd; voorspelbaar in profielen en buizen |
| ABS | Hoog | Strak op stijve profielen | Goed voor structurele geëxtrudeerde plastic onderdelen |
| Polycarbonaat | Hoog | Nauw, lage krimp | Optische en slagvaste toepassingen |
| Acryl (PMMA) | Hoog | Nauw, maar broos bij dunne muren | Plaat- en duidelijke profielen |
| Nylon (PA) | Gematigd | Losser; vochtgevoelig | Houd rekening met de vochtopname na de extrusie |
| HDPE / LDPE | Matig tot laag | Losser; hogere krimp | Verwacht bredere banden op de muur en buitendiameter |
| Polypropyleen | Gematigd | Losser; semi-crystalline shrink | Allow generous tolerance on critical dims |
| KIJKJE | Hoog | Nauw, but specialized | High-temp engineering runs; higher cost |
| TPE / TPU | Laag | Loosest; flexible recovery | Soft profiles deform under measurement |
Factoren die de dimensionale stabiliteit beïnvloeden
Several variables move a part inside or outside its tolerance band. Wall thickness uniformity matters most: thick and thin sections in the same profile cool at different rates and warp. Semi-crystalline resins like polypropylene and HDPE shrink more than amorphous ones like polycarbonate and acrylic, so the die must be cut to compensate. I also watch for haul-off speed, smelt temperatuur, and cooling-bath control, since drift in any of these shows up as dimensional variation over a long run. For hygroscopic materials such as nylon, moisture absorbed after extrusion can change dimensions days later, which is why I ask how a supplier conditions and stores finished stock.
Specifying Tolerances in Your Drawings
The cleanest way to control cost is to tolerance only what functionally matters. I call out critical dimensions explicitly, apply a reasonable general tolerance block to everything else, and reference the datum features that mate with other components. Where a flexible TPE or TPU profile is involved, I specify the measurement method and fixture, because a soft part measures differently under light pressure than at rest. Being specific about which surfaces are cosmetic versus functional lets a plastic fabrication services partner set up the line intelligently instead of overbuilding to a blanket precision requirement.
Balancing Precision Against Cost
Tighter tolerances raise cost through slower line speeds, more scrap, added inspection, and sometimes secondary sizing or machining. In de praktijk, I treat precision as a dial rather than a switch: I hold the two or three dimensions that drive fit and function tightly and relax the rest. That approach keeps resin extrusion economical while still delivering parts that assemble correctly. When a design genuinely needs molding-level precision on every feature, that is a signal the part may not be a good extrusion candidate, and I revisit the process choice before committing to tooling.
Minimum Order Quantities and Lead Times
MOQs and lead times are where the difference between stock extruded shapes and true custom work becomes concrete. Custom extrusion typically requires a one-time tooling investment in a die, while stock profiles avoid that cost entirely, per common industry sourcing guidance. That single fact drives most of the ordering economics, so I plan around it from the start.
Typical MOQ Ranges for Stock vs Custom
Stock profiles and tubing can often be bought in small quantities, sometimes by the foot or in single boxes, because the supplier already runs them. As SeaGate Plastics points out, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround, which is a practical advantage when volumes are modest (SeaGate-kunststoffen, 2024). Custom profiles are different. Because the line has to be set up, purged, and stabilized before good parts come off, suppliers set a minimum run to amortize that setup. Ik zie vaak aangepaste MOQ's uitgedrukt in kilo's hars of in lineaire beelden in plaats van in aantal stuks, en de drempel stijgt met meer exotische kunststoffen van technische kwaliteit.
Hoe doorlooptijden variëren met gereedschap en volume
Voor een nieuw aangepast profiel, de dobbelsteen is het pacing-item. Gereedschapsontwerp, snijden, en proeven met eerste artikelen domineren doorgaans het oorspronkelijke schema, en ik besteed een aantal weken aan het ontwerpen en bewerken van matrijzen voordat er productieonderdelen bestaan. Zodra de dobbelsteen is bewezen, herhaalbestellingen verlopen snel omdat het gereedschap op de plank ligt. Hogere volumes helpen hier eigenlijk: extrusie is een continu proces, hoogvolumeproces dat zeer geschikt is voor lange productieruns, dus zodra een lijn is ingebeld, het toevoegen van beeldmateriaal is eerder efficiënt dan storend.
Opties voor snelle doorlooptijden en versnelde uitvoeringen
Wanneer een tijdlijn krap is, Ik kijk naar drie hendels. Eerst, use stock profiles or standard tubing that can ship from inventory and be cut or fabricated to length. Seconde, ask whether an existing die is close enough to modify rather than cutting a new one. Derde, request an expedited slot, which many suppliers offer for a premium by prioritizing line time. Quick-turnaround production is realistic for standard shapes; for genuinely new custom geometry, the tooling step still sets the floor on how fast you can go.
Planning Your Project Timeline
I work backward from the required delivery date and add explicit buffers for die design, first-article approval, en eventuele secundaire activiteiten. Moving from prototype to production is smoother when I lock the profile cross-section early, because late geometry changes mean recutting the die and resetting the clock. Aligning MOQ with real annual demand also matters: ordering an efficient run size once beats paying repeated setup charges on small, frequent custom orders.
Cost Drivers in Plastic Extrusion Pricing
Understanding what actually drives a quote lets me negotiate from evidence rather than instinct. Extrusion pricing breaks down into a handful of levers, and knowing which one dominates for a given part tells me where the savings live.
Material Selection and Resin Pricing
Resin is usually the largest recurring cost, and it varies widely by grade. Commodity materials like PVC, polypropyleen, HDPE, and LDPE sit at the low end; PVC in particular is among the most widely extruded plastics globally and is well supported across suppliers. Engineering-grade plastics such as polycarbonate, nylon, and especially PEEK command higher prices and can require specialized processing. One efficiency I always ask about is regrind: thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie, which can lower material cost on non-critical parts (Amerikaanse Environmental Protection Agency, 2023). Choosing the least expensive resin that meets the application requirement is the single highest-leverage decision in material selection.
Gereedschap, Installatie, and Run Volume
Custom work carries a one-time die cost that stock profiles avoid. That tooling charge is fixed, so it amortizes across the run: the more footage I order, the lower the per-part tooling burden. Setup time and line stabilization add cost to every job regardless of size, which is exactly why small custom orders feel expensive per piece. Co-extrusie, which combines two materials in one profile, adds tooling and process complexity and therefore cost, but it can eliminate secondary assembly, so I weigh the tradeoff on total value rather than tooling alone.
Secondary Operations and Finishing
Anything that happens after the profile leaves the die adds cost: op lengte snijden, boren, inkepingen, afdrukken, perforeren, tight-tolerance sizing, en verpakking. Individually these are minor, but they stack quickly on high piece counts. I decide deliberately which operations belong in-line with the extrusion and which are genuinely needed, because each added step also adds handling and inspection. Where a feature can be designed into the profile cross-section instead of machined afterward, I do that, since forming a feature is nearly free compared with a downstream operation.
Domestic vs Offshore Cost Comparisons
Headline piece price often favors offshore, but I evaluate total landed cost. The Reshoring Initiative notes that domestic sourcing can reduce total landed cost by lowering freight, plicht, en voorraadkosten (Reshoring-initiatief, 2023), and those factors are easy to underestimate when comparing unit prices alone. Working with a domestic plastics manufacturer also shortens lead times, simplifies communication, and reduces the inventory buffer I have to hold against long ocean transit. The US plastics industry is a substantial contributor to domestic manufacturing shipments and employment (Vereniging van de Kunststofindustrie, 2023), so the domestic supplier base for both stock and custom profiles is deep. Mijn vuistregel: voor hoog volume, low-mix commodity profiles, offshore can win on price; for responsive, higher-mix, or engineering-grade work, domestic contract manufacturing usually wins on total cost and risk. For a fuller look at custom capabilities, I point buyers to custom plastic extrusion manufacturers such as SeaGate Plastics as a reference point for scope and services.
Questions to Ask Before Choosing a Factory
Wanneer ik een fabrikant van kunststofprofielen onderzoek, I treat the first conversation as a structured interview rather than a sales call. The goal is to separate shops that can genuinely deliver my part from those that simply want the order. Over years of sourcing extruded plastic parts, I have found that a handful of pointed questions surface most of the risk before a single dollar changes hands. Below is the checklist I actually use.
Capaciteit, Certificeringen, and Material Expertise
I start by asking what the factory runs today, not what it claims it can run. Continuous extrusion is a high-volume manufacturing process, so I want to know line count, typical run lengths, and whether they have headroom for my volume without displacing existing customers. On the quality side, I ask directly about certification. ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (Internationale Organisatie voor Standaardisatie, 2015), and while certification is not a guarantee of good parts, its absence tells me the shop may lack documented process controls.
Material expertise is the third leg. A capable resin extrusion supplier should speak fluently about the polymers relevant to my application, whether that is PVC and HDPE for construction profiles, ABS and polycarbonate for enclosures, polypropylene and LDPE for packaging and tubing, or engineering-grade plastics like nylon (PA) and PEEK for demanding environments. PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, vaak gebruikt in profielen, pijp, en buizen (Vereniging van de Kunststofindustrie). If I need flexible sections, I confirm experience with TPE/TPU, and if my part demands a rigid core with a soft-touch or weather-resistant skin, I ask whether they offer co-extrusion. Groothandel in laboratoriumextruders
Prototyping and Design Support Availability
I ask whether the factory offers design consultation before tooling is cut. The best plastic fabrication services partners will review my cross-section for extrudability, flag thin walls or sharp corners that trap stress, and suggest material substitutions that lower cost without hurting performance. I also confirm they can produce a representative prototype rather than pointing me straight to a production die.
Doorlooptijden, MOQ's, and Delivery Track Record
Here I get specific. I ask for standard lead times on both tooling and production, the minimum order quantity, and how MOQ scales with material and profile complexity. Custom extrusion typically requires a one-time tooling investment for the die, while stock extruded shapes avoid that cost entirely (begeleiding bij inkoop in de sector). If my volumes are modest, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (SeaGate-kunststoffen, 2024), so I always ask what stock profiles they carry. On delivery, I want on-time performance data, not adjectives.
References and Industry Experience
Eindelijk, Ik vraag om referenties in mijn branche. A shop that regularly serves medical, automobiel, or building-products customers has already navigated the tolerances and documentation those sectors demand. I call the references and ask two questions: did the parts meet spec on the first production run, and how did the supplier handle the problem when something went wrong?
From Prototype to Production: How the Process Unfolds
Once I have chosen a supplier, the path from a drawing to shippable extruded plastic parts follows a predictable sequence. Understanding each stage helps me set realistic timelines internally and catch problems while they are still cheap to fix.
Submitting Drawings and Design Consultation
I begin by sending a dimensioned drawing of the profile cross-section, along with the target material, kleur, tolerantie eisen, and end-use environment. This is where design-for-manufacturing consultation earns its keep. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs-ontwerpbronnen, 2023), a good engineer will help me place critical dimensions where the process can reliably hold them and relax the ones that do not matter.
Sample and Prototype Validation
Next comes a sample or prototype. Depending on the shop, this may be pulled from a soft or temporary die, or matched from existing stock extruded shapes. I use this stage to validate fit, flexibiliteit, oppervlakteafwerking, and material behavior in my actual assembly. Catching a wall-thickness issue on a prototype costs me a revision; catching it after the production die is cut costs me the tooling.
Tooling Approval and First-Article Inspection
Extruder Twin Screw After I approve the design, the factory cuts the production die. The die design and tooling step is the largest one-time cost in custom extrusion, so I review the tooling drawing carefully before signing off. Once the die runs, I require a first-article inspection: a documented measurement of the initial output against my drawing. I do not release full production until the first article passes.
Ramping to Full Production
With the first article approved, the line ramps to full production. Plastic extrusion is a continuous, hoogvolumeproces dat zeer geschikt is voor lange productieruns (SPI/Plastics Industry Association overview), so unit costs typically drop as volume climbs. I confirm the quality plan for ongoing runs, including sampling frequency and the criteria for holding or scrapping out-of-spec material. Thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie (Amerikaanse Environmental Protection Agency, 2023), so I also clarify the shop’s regrind policy when appearance or mechanical properties are critical.
Domestic vs Overseas Extrusion Sourcing
One of the most consequential decisions I make is where to source. The instinct is to compare unit price, but in my experience that number alone is misleading. What matters is total landed cost and the operational realities that price hides.
Cost vs Total Landed Cost Considerations
Overseas suppliers often quote a lower piece price, but I add freight, plichten, customs handling, and the inventory carrying cost of larger safety stock and longer transit. Reshoring en binnenlandse inkoop kunnen de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten (Reshoring-initiatief, 2023). Once I build a full landed-cost model, the gap between a domestic plastics manufacturer and an overseas one usually narrows, and sometimes reverses.
Doorlooptijd, Verzending, and Communication Factors
Domestic sourcing shortens my supply chain and simplifies communication across time zones and languages, which matters most when I need quick-turnaround production or fast design changes. Overseas sourcing can suit stable, high-volume programs where the design is frozen and lead time is not a constraint.
Quality Control and IP Protection
Proximity makes on-site audits and first-article reviews far easier, and domestic contracts generally offer stronger, more enforceable intellectual property protection for a proprietary die design. When my profile represents real design investment, that protection weighs heavily.
Wanneer elke optie zinvol is
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (Vereniging van de Kunststofindustrie, 2023), and directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes local sourcing practical to research. The table below summarizes how I weigh the two paths.
| Factor | Binnenlandse inkoop | Overzeese inkoop |
|---|---|---|
| Eenheidsprijs | Higher piece price | Often lower piece price |
| Totale landkosten | Lower freight, plicht, and carrying cost | Added freight, plicht, and inventory cost |
| Doorlooptijd | Korter, more responsive | Langer, transit-dependent |
| Mededeling | Same time zone and language | Time-zone and language gaps |
| Quality audits | On-site visits practical | Remote or costly to audit |
| IP-bescherming | Sterker, more enforceable | Variable enforcement |
| Beste pasvorm | Aangepaste profielen, fast changes, proprietary tooling | Frozen designs, very high volume, price-driven programs |
In de praktijk, I lean domestic for custom plastic profiles that involve proprietary tooling, evolving designs, or short lead times, and I consider overseas contract manufacturing only for mature, stabiel, high-volume parts where the landed-cost math clearly favors it. For a starting point on capabilities and stock offerings, resources like SeaGate-kunststoffen are a useful reference when scoping a domestic partner.
Sustainability and Recyclability in Extrusion
When I evaluate a plastic extrusion companies factory today, sustainability is no longer a soft preference tucked into the back of a proposal. It sits alongside price, doorlooptijd, and quality as a core selection criterion. The good news is that extrusion is inherently well suited to responsible material use, and the suppliers I trust have built that advantage into their operations rather than treating it as an afterthought.
Recyclable Thermoplastics and Scrap Reuse
Most of the polymers I specify for extruded plastic parts are thermoplastics, which means they can be remelted and reformed multiple times without a complete loss of properties. According to the US Environmental Protection Agency (2023), thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie. That single characteristic separates them from thermosets and gives buyers real leverage on both cost and environmental footprint.
In de praktijk, this recyclability spans the common resins you will encounter across quotes. PVC, HDPE, LDPE, and Polypropylene are among the workhorses of profile extrusion and plastic tubing, and each reclaims well when handled correctly. Engineering-grade plastics such as ABS, Polycarbonaat, Nylon (PA), en acryl (PMMA) also tolerate controlled regrind, though I hold them to tighter blend ratios because their properties matter more in demanding applications. High-performance materials like PEEK and flexible TPE/TPU sit at the specialized end, where reuse requires more careful process control.
Regrind and Material Efficiency Practices
The continuous extrusion process generates predictable scrap: startup purge, trimmen door aanpassingen van de profieldwarsdoorsnede, en off-spec runs tijdens matrijswissels. Een capabele fabrikant van kunststofprofielen vangt dit materiaal op, granuleert het tot maalgoed, en herintroduceert het met een bepaald percentage terug in nieuwe hars. Ik vraag altijd naar de details, omdat uit de details blijkt hoe gedisciplineerd een operatie werkelijk is.
- Welk percentage maalgoed mengt u in de standaardproductie?, en verandert het voor cosmetische versus structurele onderdelen?
- Hoe scheid je harssoorten om kruisbesmetting tijdens harsextrusie te voorkomen??
- Kunt u de traceerbaarheid van materialen documenteren, van ruwe hars tot afgewerkt profiel??
- Biedt u post-industriële opties voor gerecyclede inhoud aan als mijn toepassing dit toestaat??
Co-extrusie verdient hier vermelding. Door een maagdelijke buitenlaag te combineren met een maalgoed of gerecyclede kern, some suppliers deliver the surface quality I need while lowering virgin material consumption. It is a practical way to reconcile appearance requirements with sustainability goals on the same part.
Choosing Environmentally Responsible Suppliers
In mijn ervaring, a domestic plastics manufacturer often carries a sustainability advantage that has nothing to do with marketing. The Reshoring Initiative (2023) notes that domestic sourcing can reduce total landed cost by lowering freight, plicht, en voorraadkosten, and shorter supply chains also mean lower transport emissions. When I compare a nearby US factory against overseas alternatives, the environmental and logistical benefits frequently reinforce each other.
Beyond geography, I look for suppliers whose quality systems formalize waste reduction. ISO 9001, described by the International Organization for Standardization (2015) as the internationally recognized standard for quality management systems, does not mandate sustainability by itself, but shops that maintain it tend to run tighter processes with less scrap and better material accountability.
Regulatory and Buyer Sustainability Expectations
My downstream customers increasingly ask about recycled content, chemical compliance, and end-of-life recyclability before they will approve a part. That pressure flows straight back to how I write specifications. I now treat sustainability documentation as part of the deliverable, not a bonus. When a supplier can hand me material certifications, regrind policies, and recyclability data without hesitation, it signals a partner ready for where the market is heading rather than where it has been.
Making Your Final Decision and Requesting a Quote
Once I have shortlisted candidates, the decision comes down to matching each supplier’s real capabilities against my project’s non-negotiables. The extrusion market rewards specialization, so the goal is not finding the largest or most decorated factory but the one whose strengths line up with my part, my volumes, and my timeline.
Consolidating Your Evaluation Criteria
I bring my findings together into a single scorecard so I am comparing suppliers on the same terms. Beweert als “grootste” of “best” mean little in isolation; a large plastic extrusion companies factory tuned for high-volume commodity profiles may be the wrong fit for a low-volume, tight-tolerance engineering part, en omgekeerd. The table below shows the weighting I typically apply, though I adjust it to the priorities of each program.
| Evaluation Criterion | Waar ik naar zoek | Typical Weight |
|---|---|---|
| Material capability | Experience with my resin (PVC, HDPE, Polycarbonaat, enz.) and co-extrusion if needed | Hoog |
| Tooling and die design | In-house die design, tooling lead time, revision support | Hoog |
| Quality system | ISO 9001 certification and documented process controls | Hoog |
| Volume fit | Alignment of MOQ and capacity with my annual demand | Medium |
| Doorlooptijd | Realistic tooling plus production schedule, quick-turnaround options | Medium |
| Locatie | Domestic sourcing benefits, vracht, and responsiveness | Medium |
| Duurzaamheid | Regrind practices, gerecyclede inhoud, traceerbaarheid van materialen | Rising |
Preparing a Clear RFQ Package
The quality of the quotes I receive is directly proportional to the quality of the request I send. A vague inquiry produces padded, cautious pricing; a complete RFQ produces sharp, comparable numbers. Extrusion carries specific cost drivers a supplier needs to see up front, chiefly the one-time tooling investment for custom profiles, which industry sourcing guidance confirms is avoided only when you use stock extruded shapes.
What Information to Include for Accurate Quotes
I make sure every RFQ package answers the questions a plastic fabrication services provider will otherwise have to ask, because each back-and-forth adds days to the timeline.
- A dimensioned drawing of the profile cross-section with tolerances. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming, per Protolabs (2023), I flag which dimensions are critical and which can float.
- Material specification, including resin type, grade, kleur, and any UV, flame, or food-contact requirements.
- Annual volume and order frequency, plus expected part length and cut tolerances.
- Whether I need custom tooling or can use a stock profile, and whether secondary operations such as cutting, ponsen, or printing apply.
- Target price, required delivery date, and destination for landed-cost accuracy.
- Application and industry context, which helps the supplier recommend the right material and process.
Next Steps to Start Your Project
With the scorecard filled in and the RFQ ready, I send it to two or three well-matched suppliers rather than blasting a dozen. I ask for a sample or first-article inspection before committing to full production, and I confirm the tooling ownership terms in writing. Moving from prototype to production this deliberately has consistently saved me from costly surprises. Directories such as Thomasnet (2024), which list and categorize US plastic extrusion manufacturers by capability and region, remain a useful starting point when I need to widen the field, and specialist custom extruders like SeaGate-kunststoffen illustrate how stock profiles and tubes can be fabricated into cost-effective custom parts.
Veelgestelde vragen
These are the questions buyers ask me most often when they are sourcing an extrusion partner. I have kept the answers concise and practical so you can act on them quickly.
How do I find a plastic extrusion companies factory near me or in the USA?
Start with capability, then filter by geography. I search supplier directories such as Thomasnet (2024) that categorize US plastic extrusion manufacturers by region and process, then cross-check each candidate’s material and volume fit. Choosing a domestic plastics manufacturer often pays off beyond convenience: the Reshoring Initiative (2023) reports that domestic sourcing can lower freight, plicht, en voorraadkosten, reducing total landed cost.
How much does custom plastic extrusion cost?
There are two cost layers. Custom profiles require a one-time tooling and die investment, after which per-part pricing depends on resin, wanddikte, uitvoersnelheid, en volume. Stock extruded shapes skip the tooling charge entirely, which is why I default to them when a standard profile meets the requirement. Omdat extrusie continu is, proces met een hoog volume, unit costs typically fall as run length increases.
What is the difference between custom and stock extruded profiles?
Standaardprofielen zijn standaarddoorsneden die een fabrikant van kunststofprofielen al produceert, ze hebben dus geen gereedschapskosten en korte doorlooptijden, ook al is de vorm vast. Aangepaste extrusie geeft mij een matrijs die is ontworpen volgens mijn exacte profieldoorsnede, wat de gereedschapsinvestering waard is als de geometrie, functie, of branding vereist dit. SeaGate-kunststoffen (2024) merkt ook op dat standaardprofielen en buizen kunnen worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen, een nuttige middenweg wanneer een volledig op maat gemaakte dobbelsteen niet gerechtvaardigd is.
Hoe kies ik het juiste materiaal voor mijn geëxtrudeerde onderdeel?
Ik stem de hars af op de toepassing. PVC is een van de meest geëxtrudeerde kunststoffen voor profielen, pijp, en buizen. HDPE, LDPE, en polypropyleen doen het goed in chemisch bestendige en flexibele toepassingen. Wanneer ik duidelijkheid nodig heb, slagsterkte, of hittebestendigheid, Ik ga over op kunststoffen van technische kwaliteit, zoals polycarbonaat, ABS, Acryl (PMMA), or Nylon (PA), and I reserve PEEK for extreme thermal and mechanical demands. Sharing your application and environment with the supplier is the fastest route to the right recommendation.
What certifications should a quality extrusion supplier hold?
ISO 9001 is my baseline. The International Organization for Standardization (2015) describes it as the internationally recognized standard for quality management systems used across manufacturing, and it is the most widely adopted quality standard in the plastics sector. Depending on your industry, you may also require food-contact, medisch, or flame-rating compliance, so confirm those specifics against your application.
What mistakes should I avoid when sourcing an extrusion partner?
The most common ones I see are chasing “grootste” of “best” claims without checking fit, sending incomplete drawings that produce inflated quotes, and underestimating tooling lead time. I also caution against ignoring MOQ alignment; a factory built for high-volume manufacturing may not welcome low-volume work, and a small shop may struggle with your scale. Match the supplier to the job rather than the reputation.
What are the next steps once I have chosen a supplier?
Send a complete RFQ, request a sample or first-article inspection, confirm tooling ownership in writing, and agree on a realistic schedule that separates tooling time from production time. Validating the part before full production is the single most reliable way I have found to move from prototype to production without expensive rework.
What Is a Plastic Extrusion Companies Factory and Why It Matters for B2B Buyers
When I evaluate a plastic extrusion companies factory for a client, Ik begin met het proces zelf, because the process defines what a supplier can and cannot do for you. Bij kunststofextrusie smelt het ruwe kunststofmateriaal en vormt het tot een doorlopend profiel met een vaste doorsnede (SeaGate-kunststoffen, 2024). That single sentence carries more purchasing implications than most buyers realize: de “vaste doorsnede” is why extrusion excels at long, uniform shapes like tubing, trimmen, en kanalen, and it is also why you cannot expect the same complex three-dimensional geometry you would get from molding.
Definition: What You Are Actually Buying
In practical terms, a plastic extrusion factory pushes softened resin through a shaped die to produce items such as custom plastic profiles, kunststof buizen, and plastic sheet. Because this is a continuous extrusion process, it runs well for high-volume manufacturing and long production runs rather than one-off complex parts. The two categories I ask buyers to distinguish early Leverancier van extrusiekunststofproductie are stock extruded shapes, which are ready-made and avoid tooling, and custom extruded plastic parts, which require a die designed to your cross-section. Standaard geëxtrudeerde profielen en buizen kunnen ook worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen met een snelle productie (SeaGate-kunststoffen, 2024), wat een nuttige middenweg is wanneer een volledig op maat gemaakte dobbelsteen niet gerechtvaardigd is.
Marktcontext
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (Vereniging van de Kunststofindustrie, 2023), u koopt dus niet in een nichehandel. Die schaal is van belang voor kopers: het betekent echte concurrentie tussen leveranciers, redundantie als één fabrikant van kunststofprofielen de doorlooptijd niet kan halen, en een volwassen basis van diensten op het gebied van contractproductie en kunststofproductie. Het betekent ook dat je beweert de “grootste” of “best” fabriek brengt steno op de markt, niet geverifieerde ranglijsten. Ik beschouw die labels als aanwijzingen om te vragen naar de werkelijke lijncapaciteit, certificeringen, en referentieklanten in plaats van als bewijsmateriaal.
Belangrijkste toepassingen en materialen
Materiaalkeuze bepaalt het grootste deel van het resultaat, dus koppel ik de hars aan de toepassing voordat ik een leverancier op de shortlist zet. Common choices I see across projects include:
- PVC — among the most widely extruded plastics globally, gebruikelijk in profielen, pijp, en buizen (Vereniging van de Kunststofindustrie).
- HDPE and LDPE — durable, chemically resistant polyethylenes used for tubing, voeringen, and industrial profiles.
- Polypropyleen — lightweight and fatigue-resistant, frequently chosen for living hinges and chemical handling.
- ABS and Polycarbonate — impact-resistant options for structural trim and enclosures; polycarbonate adds optical clarity and heat resistance.
- Acryl (PMMA) — clarity and weatherability for lenses, displays, and lighting profiles.
- Nylon (PA) en PEEK — engineering-grade plastics for wear, temperatuur, and mechanical demands; PEEK is the high-performance choice for aerospace and medical.
- TPE/TPU — flexible elastomers for seals, pakkingen, and grips, often produced through co-extrusion with a rigid substrate.
Co-extrusion deserves special attention because it lets a factory combine two materials in one profile, for example a rigid PVC body with a soft TPE sealing lip. If your part needs both stiffness and flexibility, confirm the supplier runs true co-extrusion rather than secondary assembly.
Why This Matters for B2B Buyers
Understanding the process changes how you write a request for quote. Extrusietoleranties zijn over het algemeen losser dan bij spuitgieten vanwege materiaalkrimp en continue vorming (Protolabs, 2023), so specifying injection-molding-tight tolerances on an extruded profile will either inflate your price or trigger a round of clarifying questions that delays the quote. On sustainability, thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie (Amerikaanse EPA, 2023), which gives you a legitimate lever for both cost and environmental goals when you discuss regrind percentages with a supplier.
How to Choose the Right Plastic Extrusion Companies Factory Supplier
Choosing a supplier is where I see the most avoidable mistakes, usually because buyers compare on unit price alone and ignore the cost drivers hiding behind that number. Hieronder staat het raamwerk dat ik gebruik, built around evaluation criteria, red flags, and a due diligence checklist you can lift directly into your sourcing process.
Evaluatiecriteria voor leveranciers
I score candidates against five dimensions rather than a single quote:
- Vermogensmatch. Does the factory routinely run your resin and profile size? A plastic tubing supplier optimized for small-diameter medical tubing is not the same shop as one running large architectural profile extrusion.
- Kwaliteitssystemen. ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (ISO, 2015) and remains the most widely adopted quality standard in the plastics sector. Certification is not a guarantee of good parts, but its absence tells me to dig deeper into inspection practices.
- Tooling and die design. Ask who owns the die, how long die design and tooling take, and what happens to the tool if you leave. Ownership terms are frequently buried in fine print.
- Lead time and capacity. Confirm whether quoted lead times reflect current backlog or ideal conditions. Quick-turnaround production claims should be tied to a specific committed date.
- Financial and operational stability. A supplier that becomes your sole source for a critical profile is a risk if it is financially fragile.
Understanding the Cost Drivers
Transparency on cost structure separates a strong plastic profile manufacturer from an opaque one. Three drivers determine your total price, and I ask suppliers to break them out explicitly:
| Kostendrijver | Stock extruded shapes | Op maat geëxtrudeerde profielen |
|---|---|---|
| Gereedschap / die investment | None — profile already exists | One-time die cost required before first run (begeleiding bij inkoop in de sector, Thomasnet supplier guides) |
| Minimale bestelhoeveelheid (MOQ) | Laag; buy by the length | Hoger; tied to setup and material changeover |
| Doorlooptijd | Short — often shelf stock | Langer; includes die fabrication and first-article approval |
| Per-unit price at volume | Fixed by catalog | Lower at high volume once tooling is amortized |
| Beste pasvorm | Prototyping, laag volume, standard cross-sections | Proprietary geometry, high-volume manufacturing, prototype to production scale-up |
Custom extrusion typically requires a one-time tooling investment, terwijl aandelenprofielen deze kosten vermijden (begeleiding bij inkoop in de sector). In mijn ervaring, buyers who plan to scale from prototype to production should quote the custom die early even if they start with stock shapes, so the amortized per-unit price is visible before volumes ramp.
Rode vlaggen waar ik naar uitkijk
- Refusal to share ISO or equivalent quality documentation, or vague answers about inspection frequency.
- Quotes with no tooling line item, which usually means the cost reappears later or the die is undersized.
- Unwillingness to provide references in your industry or sample parts.
- Tolerances promised on paper that are tighter than what continuous extrusion realistically holds — a sign the supplier may be overselling.
- “Largest” of “best” claims with no capacity data, certificeringen, or customer evidence behind them.
Due diligence-checklist
Before I commit to a Plastic Extrusion Companies Factory supplier, I confirm every item below in writing:
- Do you hold ISO 9001 or an equivalent, and can I see the certificate and scope?
- Which resins do you run in production, and can you handle my material — PVC, ABS, polycarbonaat, HDPE, LDPE, polypropyleen, or an engineering grade?
- What tolerances do you guarantee for this profile cross-section, and how are they measured?
- What is the tooling cost, doorlooptijd, and MOQ, and who owns the die?
- Do you offer co-extrusion and secondary fabrication in-house?
- What percentage of regrind is used, and how does that affect certification and appearance?
- Can you provide first-article inspection reports and material certifications?
- What is your realistic committed lead time given current backlog?
Find Plastic Extrusion Companies and Factories in the United States
Buyers frequently search for a plastic extrusion factory “bij mij in de buurt” of “in the USA,” and the location question is more strategic than it first appears. Domestic sourcing is not only about proximity; it changes your total landed cost and your supply-chain risk profile.
Where to Start Your Search
Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a practical first filter when you want to build a shortlist by material, proces, or state. I pair directory research with capability-specific sources such as custom plastic extrusion manufacturer references to understand what a given shop actually produces before I reach out. The goal at this stage is a shortlist of five to eight candidates whose capabilities genuinely match your resin and profile, not a long list of names. Kunststof extrusiebedrijven
Key Considerations for Domestic Sourcing
Reshoring en binnenlandse inkoop kunnen de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten (Reshoring-initiatief, 2023). For extruded parts, which are often bulky and low in value density, freight is a meaningful line item, so a domestic plastics manufacturer closer to your assembly point can offset a higher unit price. I weigh three factors:
- Totale landkosten, niet eenheidsprijs. Add freight, plicht, and the carrying cost of the safety stock you need to cover long overseas transit.
- Communication and design iteration. Domestic time-zone alignment speeds up die design and tooling revisions during the prototype-to-production phase.
- Supply resilience. Shorter lines reduce exposure to port delays and long lead-time shocks.
Interpreting “Largest” En “Best” Factory Claims
Location searches often surface superlatives, and I treat them skeptically. “Largest” tells you nothing about whether a factory runs your material or holds your tolerances. In plaats van, I convert vague claims into verifiable questions: How many extrusion lines run my resin family? What is your on-time delivery rate? Which certifications do you hold? A smaller shop that specializes in your profile is frequently a better partner than a large one for which your job is an afterthought.
Practical Tips and Industry Context
A few habits have consistently saved my clients time and money. Eerst, request stock extruded shapes for early validation before investing in a custom die — it lets you test fit and function cheaply. Seconde, share a dimensioned drawing with realistic extrusion tolerances up front so quotes are comparable. Derde, confirm the supplier’s regrind policy, since recyclable thermoplastics and regrind reuse improve material efficiency (Amerikaanse EPA, 2023) but can affect appearance on cosmetic parts. Eindelijk, remember that plastic extrusion is a continuous, hoogvolumeproces dat zeer geschikt is voor lange productieruns, so it rewards buyers who can consolidate demand and forecast accurately. Within the mature US plastics manufacturing base (Vereniging van de Kunststofindustrie, 2023), you have room to be selective — use it, and let a structured checklist rather than a headline claim decide your Plastic Extrusion Companies Factory supplier.
Locate a plastic extrusion factory near my location
When buyers ask me how to find a plastic extrusion factory nearby, I remind them that “bij mij in de buurt” is really shorthand for two goals: shorter freight lanes and easier communication. Extrusion melts raw plastic material and forms it into a continuous profile with a fixed cross-section (SeaGate-kunststoffen, 2024), and because that continuous extrusion process runs at high volume, the finished product is often bulky and freight-sensitive. In mijn ervaring, the cost of moving extruded plastic parts across the country can quietly erode the price advantage of a distant supplier, so location genuinely matters.
Key considerations for local sourcing
I start every local search by matching capability to geography rather than proximity alone. A plastic profile manufacturer two states away with the right die design and tooling almost always beats a closer shop that cannot hold your profile cross-section. I evaluate three things in order: the materials they run (PVC, ABS, polycarbonaat, HDPE, LDPE, polypropyleen, acryl, and engineering-grade resins such as nylon or PEEK), the processes they offer (profiel extrusie, extrusie van kunststofplaten, slangen, en co-extrusie), and their quality systems. ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (ISO, 2015), so I treat certification as a baseline filter, not a bonus.
Practical tips to find and vet a factory
Thomasnet supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a reliable starting point for a location-based shortlist. Vanaf daar, I qualify each candidate with a consistent set of questions before I ever request a quote.
My local supplier vetting checklist
- Which resins do you extrude in-house, and can you run regrind for material efficiency?
- Do you offer co-extrusion or dual-durometer profiles if my part needs a soft-touch or barrier layer?
- What tolerances can you hold, and how do you document them?
- Are you ISO 9001 gecertificeerd, and can you share a recent audit summary?
- What is your typical lead time from approved die to first article?
- Do you provide plastic fabrication services (snijden, ponsen, boren) so I receive finished parts, not just stock lengths?
Industriecontext
Domestic proximity is more strategic than it looks. Reshoring en binnenlandse inkoop kunnen de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, en voorraadkosten (Reshoring-initiatief, 2023). Because the US plastics industry is a major contributor to domestic manufacturing shipments and employment (Vereniging van de Kunststofindustrie, 2023), most regions have a viable domestic plastics manufacturer within a reasonable freight radius. I tell buyers that “bij mij in de buurt” should mean near enough to control landed cost and lead time, which is often a regional rather than a strictly local decision.
Identify the largest plastic extrusion companies in the US
Buyers frequently ask me to point them to the “grootste” kunststof extrusiebedrijven, and my first move is always to define what “grootste” means for their project. Size can describe revenue, plant footprint, aantal extrusielijnen, or annual resin throughput, and those metrics do not always move together. A plastic extrusion companies factory supplier with enormous pipe capacity may be the wrong fit for a low-volume acrylic profile, dus interpreteer ik schaal door de lens van de specifieke taak.
Belangrijke overwegingen wanneer “grootste” zaken
Schaal verdient zijn geld bij lange productieruns. Plastic extrusion is a continuous, hoogvolumeproces dat zeer geschikt is voor lange productieruns, dus de grootste producenten schitteren als je miljoenen meters PVC-profiel of HDPE-buis nodig hebt volgens een voorspelbaar schema. PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, vaak gebruikt in profielen, pijp, en buizen, Daarom hebben de grootste spelers de neiging hun capaciteit daar te concentreren. Als uw programma een hoog volume en gestandaardiseerd is, een grote fabrikant van kunststofprofielen biedt redundantie, buffervoorraad, en prijshefboomwerking. Als uw programma klein of zeer op maat is, diezelfde schaal kan zich vertalen in hogere minima en minder flexibiliteit.
Praktische tips voor het evalueren van schaalclaims
Ik neem nooit een marketingclaim aan “grootste” tegen nominale waarde. In plaats van, Ik vraag om concrete indicatoren: aantal extrusielijnen per grootteklasse, harsen draaien op volume, en de splitsing tussen geëxtrudeerde vormen en maatwerk. A large firm quoting a wholesale program should be able to show quick-turnaround production capacity, secondary plastic fabrication services, and a documented MOQ structure. The table below summarizes how I weigh large versus specialized suppliers.
Large versus specialized extrusion suppliers
| Factor | Largest producers | Specialized suppliers |
|---|---|---|
| Beste pasvorm | Hoog volume, standardized runs (pijp, PVC-profiel) | Custom plastic profiles, engineering-grade resins |
| Minimale bestelhoeveelheid | Higher MOQ to justify line time | Lower MOQ, more flexible |
| Gereedschapskosten | Amortized across large volumes | One-time die cost more visible per unit |
| Doorlooptijd | Voorspelbaar, buffered by capacity | Variabel, project-dependent |
| Materiaal bereik | Basisharsen (PVC, HDPE, LDPE, PP) | Specialty resins (PC, PMMA, PA, KIJKJE, TPE/TPU) |
| Co-extrusie | Common on standard lines | Often available for niche multi-layer parts |
Industriecontext
The largest US extruders are anchored in commodity, freight-heavy products where continuous, high-volume manufacturing rewards efficiency. Aangepaste extrusie vereist doorgaans een eenmalige investering in gereedschap of matrijzen, terwijl aandelenprofielen deze kosten vermijden, so large producers often lead with catalogs of stock extruded shapes. I remind buyers that “grootste” is a useful signal for reliability and capacity, but it is not a proxy for quality or fit. The right size is the one that matches your volume, materiaal, and tolerance needs.
Discover the best-rated plastic extrusion manufacturers
“Best-rated” is the claim I scrutinize most, because ratings can reflect genuine performance or simply strong marketing. In mijn ervaring, the manufacturers worth shortlisting are the ones that make their quality measurable. I look past star counts and testimonials for evidence I can verify: certificeringen, documented tolerances, traceerbaarheid van materialen, and a track record of moving projects from prototype to production without surprises.
Key considerations for judging quality
Quality management is the foundation. ISO 9001 is the most widely adopted quality management standard, used across manufacturing sectors including plastics, so I treat it as table stakes for a best-rated plastic extrusion companies factory manufacturer. Beyond certification, I assess how a supplier handles tolerances. Extrusietoleranties zijn over het algemeen losser dan bij spuitgieten vanwege materiaalkrimp en continue vorming (Protolabs, 2023), and the best manufacturers explain that reality up front rather than overpromising. A shop that gives me realistic tolerance ranges and a clear inspection plan earns more trust than one quoting numbers it cannot hold.
Practical tips for choosing the best-rated supplier
I use a material selection framework tied to the application. The resin drives the manufacturer, niet andersom.
- PVC — profiles, pijp, and tubing where cost and rigidity matter.
- ABS and polycarbonate — impact-resistant parts; polycarbonate adds clarity and heat tolerance.
- HDPE and LDPE — chemical resistance and flexibility for tubing and liners.
- Polypropyleen — lightweight parts needing fatigue and chemical resistance.
- Acryl (PMMA) — optical clarity for lighting and display profiles.
- Nylon (PA) en PEEK — engineering-grade parts under mechanical or thermal stress.
- TPE/TPU — flexible seals and gaskets, often via co-extrusion.
Once the material is set, I confirm the supplier offers the matching process, whether that is profile extrusion, extrusie van kunststofplaten, or resin extrusion with co-extrusion for multi-layer parts. Standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen (SeaGate-kunststoffen, 2024), so I favor manufacturers that pair extrusion with in-house fabrication and prototype-to-production support. For a working example of custom capability and stock profile options, I point buyers to references such as SeaGate-kunststoffen.
Industriecontext
The best-rated manufacturers increasingly compete on sustainability alongside quality. Thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie (Amerikaanse EPA, 2023), so I ask top candidates how they manage scrap and regrind. A manufacturer that documents its quality system, states honest tolerances, and runs an efficient material loop tends to be “best-rated” for reasons that hold up under a plant visit. That is the standard I apply, and it is the one I recommend every buyer use before committing to a contract manufacturing partner.
Understand how the plastic extrusion manufacturing process works
Wanneer ik een fabrikant van kunststofprofielen evalueer, I start by making sure the buyer understands what actually happens on the shop floor. Bij kunststofextrusie smelt het ruwe kunststofmateriaal en vormt het tot een doorlopend profiel met een vaste doorsnede (SeaGate-kunststoffen, 2024). That single sentence carries most of what you need to know: the process is continuous, the cross-section is constant along the length, and the shape is defined by tooling rather than by a closed mold.
The core stages of the continuous extrusion process
In de praktijk, I describe the workflow in five stages. Eerst, resin pellets are fed into a hopper. Seconde, a heated barrel with a rotating screw melts and pressurizes the material, which is why practitioners often call it resin extrusion. Derde, the molten polymer is forced through a die that establishes the profile cross-section. Vierde, the extrudate is cooled in a water bath or air rack so it holds its geometry. Fifth, pullers draw the part at a steady rate before a saw or cutter sizes it. Because nothing stops between stages, the method is genuinely a continuous extrusion process rather than a cycle-by-cycle one.
Why tolerances differ from injection molding
One point I raise early with engineering teams: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs-ontwerpbronnen, 2023). This is not a defect. It reflects the physics of pulling a hot polymer through open tooling and cooling it under tension. If your extruded plastic parts need tight dimensional control on a specific feature, plan for secondary machining or specify that feature as a fabrication step rather than expecting the die alone to hold it.
Co-extrusion and profile extrusion variants
Profile extrusion covers the custom cross-sections most buyers picture: kanalen, pakkingen, versieringen, en structurele vormen. Co-extrusion runs two or more materials through the die at once, which lets you combine, Bijvoorbeeld, a rigid PVC body with a flexible TPE/TPU sealing lip in a single pass. I find co-extrusion is where a capable factory earns its rate, because it removes a downstream assembly step and improves seal performance. Plastic sheet extrusion and tubing use the same fundamentals with different die and downstream setups.
Industry context and material efficiency
Extrusion suits high-volume manufacturing because it is inherently a continuous, hoogvolumeproces dat zeer geschikt is voor lange productieruns. Once a die is dialed in, output scales with line speed and run time. It also has a reasonable sustainability story: thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie (Amerikaanse EPA, 2023). In mijn ervaring, asking a supplier how they handle regrind tells you a lot about both their cost discipline and their process control.
Compare custom vs stock plastic extrusion suppliers
The most consequential sourcing decision I help buyers make is custom versus stock. It drives your tooling cost, minimale bestelhoeveelheid, and lead time all at once. Het juiste antwoord hangt af van hoe goed een standaardvorm bij uw toepassing past en hoeveel volume u verwacht te gebruiken.
Wat de twee paden scheidt
Aangepaste extrusie vereist doorgaans een eenmalige investering in gereedschap en matrijzen, terwijl aandelenprofielen deze kosten vermijden. Standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen (SeaGate-kunststoffen, 2024). Er is dus een middenweg die veel kopers missen: begin met een geëxtrudeerde vorm en fabriceer deze, een deel van het aanpassingsvoordeel vastleggen zonder voor een nieuwe dobbelsteen te betalen.
Kostendrijvers om te modelleren voordat u een offerte aanvraagt
Wanneer ik een sourcingmodel bouw, Ik scheid drie coureurs zodat de cijfers eerlijk blijven:
- Matrijsontwerp en gereedschap: een eenmalige kost voor maatwerk, doorgaans afgeschreven over uw eerste bestelling of twee.
- MOQ: aangepaste lijnen hebben hogere minimumwaarden om het instellen en verwijderen van materiaal te rechtvaardigen; Standaardvormen kunnen in kleine hoeveelheden worden verzonden.
- Doorlooptijd: voorraad wordt snel verzonden; op maat voegt matrijsfabricage en goedkeuring van het eerste artikel toe voordat de productie begint.
Vergelijkingstabel: aangepaste versus standaardextrusie
| Factor | Custom profile extrusion | Stock extruded shapes |
|---|---|---|
| Gereedschapskosten | One-time die investment required | Geen |
| Minimale bestelhoeveelheid | Hoger, to amortize setup | Laag, often cut-to-length |
| Doorlooptijd | Langer (sterven bouwen + eerste artikel) | Quick-turnaround production |
| Dimensional fit | Exact cross-section to spec | Nearest standard, plus fabrication |
| Beste voor | Sustained volume, unique geometry | prototypen, laag volume, near-fit needs |
| Unit price at scale | Lager zodra de gereedschappen zijn afgeschreven | Higher per unit for heavy customization |
A vetting checklist for either path
Whether you pursue a custom plastic profile manufacturer or a stock plastic tubing supplier, I ask the same core questions. Is the shop certified to ISO 9001, de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (ISO, 2015)? ISO 9001 is de meest algemeen aanvaarde standaard voor kwaliteitsmanagement in productiesectoren, inclusief kunststoffen, so its absence is worth a direct conversation. Beyond certification, I ask:
- Which resins do you run in-house, and can you handle engineering-grade plastics like polycarbonate, nylon (PA), of PEEK?
- Do you offer co-extrusion and downstream plastic fabrication services?
- How do you document tolerances and first-article inspection?
- What is your true MOQ, and how is tooling amortized on the initial order?
- Can you support the move from prototype to production without re-tooling?
Location intent: near me and in the USA
Buyers frequently search for a Plastic Extrusion Companies Factory supplier “bij mij in de buurt” or a domestic plastics manufacturer in the USA. Two resources help here. Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is a practical starting point for shortlisting. And the case for domestic sourcing is more than convenience: reshoring and domestic sourcing can reduce total landed cost by lowering freight, plicht, en voorraadkosten (Reshoring-initiatief, 2023). Ik behandel “grootste” En “best” factory claims with skepticism; capability fit for your specific resin, tolerantie, and volume matters far more than a superlative on a homepage.
Learn what products can be made through plastic extrusion
Extrusion produces a broader range of products than most buyers expect, and the material you choose shapes both what is possible and what it costs. I organize my recommendations around a material selection framework tied to application and industry rather than a generic parts list.
Common extruded product categories
The workhorse outputs are custom plastic profiles, slangen, laken, kanalen, versieringen, pakkingen, en structurele vormen. Anything with a consistent profile cross-section along its length is a candidate. PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, vaak gebruikt in profielen, pijp, en buizen (Vereniging van de Kunststofindustrie). That prevalence is why so many stock extruded shapes are available in PVC first.
Material selection framework
Here is how I match resins to needs across the polymers you will encounter most often:
- PVC: zuinig, rigid or flexible, strong for profiles, pijp, en buizen.
- ABS: tough and impact-resistant, common in housings and trims.
- Polycarbonaat: high impact strength and clarity for glazing and guards.
- HDPE and LDPE: chemically resistant polyolefins for tubing, voeringen, and low-cost profiles; HDPE brings more rigidity, LDPE more flexibility.
- Polypropyleen: licht, chemisch resistent, and fatigue-tolerant for living hinges and profiles.
- Acryl (PMMA): optical clarity for display and lighting profiles.
- Nylon (PA): wear resistance and strength for mechanical parts.
- KIJKJE: high-temperature, chemically robust engineering-grade plastic for demanding aerospace and medical work.
- TPE/TPU: flexible elastomers ideal for seals and soft-touch co-extruded lips.
Industry applications
Construction relies on PVC and ABS profiles for window frames, versieringen, and edging. Medical and lab work uses acrylic, polypropyleen, and PEEK tubing and channels. Electronics and appliances draw on polycarbonate and ABS housings. Industrial and fluid-handling lines lean on HDPE and nylon. Mapping your industry to these resins early keeps the quoting conversation focused and avoids specifying an over-engineered material you do not need.
Practical tips for moving from concept to production
In mijn ervaring, three habits keep extrusion projects on schedule. Eerst, prototype from stock shapes where the geometry allows, then commit to custom tooling only after the design is validated, which protects your die investment. Seconde, specify tolerances by feature rather than blanket-tightening the whole profile, since that respects the process and controls cost. Derde, confirm your supplier can carry the part from prototype to production on the same line, so scale-up does not force a re-quote. Handled this way, extrusion delivers custom parts economically, with the quick turnaround that makes the process attractive in the first place.
For a deeper look at fabricating cost-effective custom parts from standard and custom profiles, I point buyers to SeaGate-kunststoffen’ extrusion overview.
Bringing Your Extrusion Sourcing Strategy Together
After walking through capabilities, materialen, and vetting criteria, the through-line I keep returning to is this: choosing among plastic extrusion companies and factories is less about finding the “grootste” of “best” name and more about matching a supplier’s real strengths to your specific part, volume, en tijdlijn. A continuous, high-volume manufacturing process rewards long production runs, but the same shop that excels at a million linear feet of PVC profile may not be the partner I want for a low-volume PEEK prototype. In mijn ervaring, buyers who define the problem precisely before they request quotes get sharper pricing and fewer surprises downstream.
Material selection sits at the center of every good decision. Whether the application calls for rigid PVC or ABS in structural profiles, polycarbonate or acrylic (PMMA) voor optische helderheid, HDPE en LDPE voor chemische bestendigheid, polypropyleen voor levende scharnieren, nylon (PA) for wear surfaces, or TPE/TPU for flexible seals, the resin drives tooling, toleranties, en kosten. Extrusion melts raw plastic and forms it into a continuous profile with a fixed cross-section (SeaGate-kunststoffen, 2024), en standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen (SeaGate-kunststoffen, 2024). That combination of stock shapes and custom profile extrusion, sometimes paired with co-extrusion for multi-material geometry, is what makes the process so versatile from prototype to production.
On the commercial side, I always separate one-time and recurring costs. Custom extrusion typically carries a one-time tooling and die investment, while stock profiles avoid it, so the die design and tooling decision shapes the whole business case. Domestic sourcing deserves a second look too: reshoring and domestic sourcing can reduce total landed cost by lowering freight, plicht, en voorraadkosten (Reshoring-initiatief, 2023), which often narrows the gap that offshore unit pricing appears to open. And because thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (ONS. EPA, 2023), a quality-focused domestic plastics manufacturer can support both cost and sustainability goals at once.
Quality systems are the final filter I apply. ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt (ISO, 2015), and it remains the most widely adopted benchmark I look for when comparing a custom plastic extrusion manufacturer against its peers. Pair that with realistic expectations on precision, since extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs, 2023), and you have a grounded framework for evaluating any plastic profile manufacturer or plastic tubing supplier.
Deskundig inzicht
| Sleutelpunt | Uitleg |
|---|---|
| Match process to volume, not to reputation | Continue extrusie is een proces met grote volumes dat het meest geschikt is voor lange productieruns, dus weeg ik de echte sterke punten van een fabriek af tegen mijn ordergrootte in plaats van te jagen “grootste” of “best” beweringen. |
| Aparte tooling vanaf eenheidsprijs | Op maat gemaakte profielen vereisen een eenmalige investering in matrijzen, terwijl geëxtrudeerde vormen dit vermijden; Door deze splitsing te begrijpen, blijven de werkelijke kosten van op maat gemaakte kunststofprofielen verborgen in een opgegeven tarief per voet. |
| Controleer de kwaliteit vóór precisieverwachtingen | ISO 9001 certificering (ISO, 2015) duidt op een beheerd proces, en ik stel tolerantieverwachtingen in de wetenschap dat extrusie losser verloopt dan spuitgieten (Protolabs, 2023). |
Bruikbare sourcingtips voor B2B-kopers
- Definieer het onderdeel voordat u winkelt. Documenteer de profieldoorsnede, hars (PVC, ABS, polycarbonaat, HDPE, polypropyleen, of een kunststof van technische kwaliteit), jaarlijks volume, en doeltolerantie, zodat elke fabrieksleverancier van kunststofextrusiebedrijven dezelfde opdracht citeert.
- Vraag om gereedschap, MOQ, en doorlooptijdnummers afzonderlijk. Request the die cost, minimale bestelhoeveelheid, and quoted lead time as distinct line items to compare custom extrusion and stock profiles on equal footing.
- Confirm the quality system in writing. Ask for a current ISO 9001 certificate and the inspection points used on extruded plastic parts, rather than accepting a general quality claim.
- Weigh domestic sourcing on total landed cost. Compare a domestic plastics manufacturer against offshore options using freight, plicht, en voorraadkosten, niet alleen de eenheidsprijs (Reshoring-initiatief, 2023).
- Test the relationship with a small run. Move from prototype to production in stages so you validate quick-turnaround performance and communication before committing to high-volume manufacturing.
- Use supplier directories as a starting list, geen shortlist. Directories such as Thomasnet (2024) help you locate regional plastic fabrication services, but I still vet capability, materialen, and certification directly with each shop.
Veelgestelde vragen
Hoe vind ik kunststofextrusiebedrijven of een fabriek bij mij in de buurt?
Wanneer ik de locatie-intentie evalueer, Ik begin met het in kaart brengen van leveranciers aan de hand van mijn scheepvaartroutes in plaats van puur geografische nabijheid. Een fabrikant van kunststofprofielen twee staten verder met het juiste matrijsontwerp en gereedschapsvermogen verslaat vaak een winkel dichterbij die mijn hars mist. Ik gebruik leveranciersgidsen waarin Amerikaanse fabrikanten van kunststofextrusie worden vermeld en gecategoriseerd op capaciteit en regio om een shortlist samen te stellen, verifieer vervolgens met een fabrieksbezoek of video-walkthrough. Thomas-gidsen zijn hiervoor een praktisch startpunt (Thomasnet, 2024, thomasnet.com). In mijn ervaring, “bij mij in de buurt” kort zou moeten betekenen, voorspelbare doorlooptijden en lage vrachtkosten, niet alleen een postcode in de buurt.
Waar moet ik op letten bij fabrikanten van kunststofextrusie in de VS?
Voor binnenlandse inkoop, Ik weeg drie dingen: gecertificeerde kwaliteit, material breadth, en de totale landkosten. A domestic plastics manufacturer can reduce total landed cost by lowering freight, plicht, en voorraadkosten (Reshoring-initiatief, 2023, reshorenow.org), which often narrows the gap with offshore quotes once you account for the full picture. The US plastics industry is also a major contributor to domestic manufacturing shipments and employment (Vereniging van de Kunststofindustrie, 2023), so the supplier base is deep. I confirm they run the resins I need, from commodity grades like PVC, HDPE, LDPE, and polypropylene to engineering-grade plastics such as polycarbonate, nylon (PA), en PEEK.
How do I choose the right plastic extrusion supplier for my project?
I treat supplier selection as a vetting checklist, not a gut call. The concrete questions I ask every candidate:
- Do you hold ISO 9001 certificering, the internationally recognized standard for quality management systems (ISO, 2015)?
- Which resins and profiles do you run in production, and do you offer co-extrusion?
- What are your tolerances, en hoe ga je om met profieldoorsnedevalidatie?
- Wat is uw minimale bestelhoeveelheid (MOQ), tooling lead time, en productiedoorlooptijd?
- Kunt u het volledige traject van prototype tot productie en snelle productie voor nabestellingen ondersteunen??
Industriële kunststof extrusieonderdelen De grootste fout die ik kopers zie maken, is kiezen op basis van alleen de eenheidsprijs en het negeren van de gereedschapskosten, MOQ, en doorlooptijdrisico. Die drijfveren bepalen doorgaans of een programma daadwerkelijk rendabel is.
Wat is het verschil tussen op maat gemaakte en standaard kunststof extrusies?
Voorraad geëxtrudeerde vormen zijn standaardprofielen en buizen die een leverancier al produceert, zodat u het gereedschap overslaat en van de plank koopt. Aangepaste extrusie vereist een eenmalige investering in gereedschap en matrijzen om uw unieke profieldoorsnede te creëren. De afweging is eenvoudig: kunststof extrusies op voorraad minimaliseren de initiële kosten en doorlooptijd, while custom plastic profiles fit your exact geometry. Notably, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (SeaGate-kunststoffen, 2024, seagateplastics.com), so I often prototype with stock shapes before committing to a die.
How should I read “grootste” En “best” plastic extrusion factory claims?
I read those labels with healthy skepticism. “Largest” usually reflects capacity or revenue, which matters for high-volume manufacturing but tells me nothing about fit for a low-volume, tight-tolerance job. “Best” is subjective marketing unless it is backed by certifications, referenties, and capability data. My rule: rank suppliers against my own requirements, not against a generic superlative. The largest plastic extrusion company on a list may be the wrong contract manufacturing partner for a specialty acrylic (PMMA) or TPE/TPU part, while a mid-size specialist nails it.
What are plastic extrusion profiles, and how are they made?
A profile is a continuous shape with a fixed cross-section. Bij kunststofextrusie smelt het ruwe kunststofmateriaal en vormt het tot een doorlopend profiel met een vaste doorsnede (SeaGate-kunststoffen, 2024). Because it is a continuous forming process, resin extrusion is well suited to long production runs and high-volume manufacturing. It also supports plastic sheet extrusion and tubing. One thing I always plan around: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs-ontwerpbronnen, 2023), so I set tolerance expectations early with the plastic tubing supplier or profile shop.
Which plastic material should I choose for my extruded parts?
I anchor material selection to the application, not habit. PVC is among the most widely extruded plastics globally and is common in profiles, pijp, en buizen. For impact and appearance, I look at ABS or polycarbonate; voor chemische bestendigheid en levende scharnieren, polypropyleen; for outdoor and clarity, acryl (PMMA); and for demanding thermal or wear conditions, nylon (PA) of PEEK. I also confirm recyclability up front, since thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (Amerikaanse EPA, 2023). Matching resin to service environment prevents the costly redesigns I have watched derail otherwise solid programs.
What drives the cost of extruded plastic parts?
Three levers move price more than anything else. Eerst, gereedschap: a custom die is a one-time investment that stock profiles avoid entirely. Seconde, MOQ and run length, since extrusion rewards volume and unit cost drops as quantities rise. Derde, material grade, where engineering-grade plastics and specialty resins cost well above commodity options. When I request a quote, I ask suppliers to break out tooling, per-unit price, and secondary plastic fabrication services separately so I can compare offers on equal terms and identify where the real cost lives.
Referenties
- Bij kunststofextrusie smelt het ruwe kunststofmateriaal en vormt het tot een doorlopend profiel met een vaste doorsnede. — SeaGate-kunststoffen (2024)
- Standaard geëxtrudeerde profielen en buizen kunnen met een snelle doorlooptijd worden vervaardigd tot kosteneffectieve, op maat gemaakte onderdelen. — SeaGate-kunststoffen (2024)
- ISO 9001 is de internationaal erkende standaard voor kwaliteitsmanagementsystemen die in de hele productie worden gebruikt. — Internationale Organisatie voor Standaardisatie (2015)
- The US plastics industry is a major contributor to domestic manufacturing shipments and employment. — Vereniging van de Kunststofindustrie (2023)
- Reshoring en binnenlandse inkoop kunnen de totale landkosten verlagen door de vrachtkosten te verlagen, plicht, and inventory carying costs. — Reshoring-initiatief (2023)
- Extrusietoleranties zijn over het algemeen losser dan bij spuitgieten vanwege materiaalkrimp en continue vorming. — Protolabs-ontwerpbronnen (2023)
- Thermoplastische materialen die bij de extrusie worden gebruikt, zijn recyclebaar, en hergebruik van maalgoed verbetert de materiaalefficiëntie. — Amerikaanse Environmental Protection Agency (2023)
- De leveranciersgidsen van Thomas vermelden en categoriseren Amerikaanse fabrikanten van kunststofextrusie op basis van capaciteit en regio. — Thomasnet (2024)
- Plastic extrusion is a continuous, hoogvolumeproces dat zeer geschikt is voor lange productieruns, volgens algemene industriële productiereferenties (SPI/Plastics Industry Association overview). — Planningsanalyse
- PVC is wereldwijd een van de meest geëxtrudeerde kunststoffen, vaak gebruikt in profielen, pijp, en buizen (Vereniging van de Kunststofindustrie). — Planningsanalyse