

कुञ्जी टेकवेहरू
- प्लास्टिक एक्सट्रुजनले कच्चा राल पग्लन्छ र यसलाई निश्चित क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ।, जसले यसलाई लामो समयसम्म उपयुक्त बनाउँछ, उच्च मात्रा उत्पादन चल्छ (सीगेट प्लास्टिक, 2024).
- जब म प्लास्टिक प्रोफाइल निर्माताको मूल्याङ्कन गर्छु, अलग गर्छु अनुकूलन निकासी, जसमा एक पटकको डाइ र टूलिङ लगानी हुन्छ, स्टक एक्सट्रुडेड आकारहरूबाट जुन अग्रिम लागत छोड्छ (Thomasnet आपूर्तिकर्ता मार्गदर्शन, 2024).
- सामग्री चयनले सबै कुरालाई डाउनस्ट्रीम ड्राइभ गर्दछ: म दायाँ पोलिमरमा एप्लिकेसन मिलाउँछु, चाहे त्यो पाइप र प्रोफाइलहरूको लागि PVC हो, एबीएस वा पॉली कार्बोनेट प्रभाव शक्तिको लागि, रासायनिक प्रतिरोधको लागि HDPE र LDPE, जीवित टिकाहरूको लागि polypropylene, एक्रिलिक (PMMA) स्पष्टता को लागी, वा ईन्जिनियरिङ्-ग्रेड नायलन (PA) र माग भागहरु को लागी PEEK.
- PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्रोफाइलहरूमा साझा, पाइप, र ट्युबिङ, त्यसैले धेरै आपूर्तिकर्ताहरूले यसलाई पूर्वनिर्धारित क्षमताको रूपमा सूचीबद्ध गर्छन् (प्लास्टिक उद्योग संघ, 2023).
- सामग्री संकुचन र निरन्तर गठनको कारणले इन्जेक्सन मोल्डिङको तुलनामा एक्सट्रुजन सहिष्णुता कम हुन्छ।, त्यसैले म मोल्डेड-पार्ट परिशुद्धता मान्नु भन्दा पहिले सहिष्णुता योजना गर्छु (प्रोटोल्याबहरू, 2023).
- म ISO को उपचार गर्छु 9001 परिपक्व गुणस्तर व्यवस्थापन प्रणालीको आधारभूत संकेतको रूपमा, ग्यारेन्टी होइन, र यसलाई एक ठोस जाँच सूची कभर क्षमता संग जोडा, सह-निकासी क्षमता, र नेतृत्व समय (ISO, 2015).
- स्थान उद्देश्यका लागि, घरेलु प्लास्टिक निर्माताबाट सोर्सिङले भाडा घटाएर कुल ल्यान्डेड लागत घटाउन सक्छ, कर्तव्य, र सूची बोक्ने लागत, एक्लै एकाइ मूल्य विरुद्ध तौल लायक बिन्दु (पुन: प्राप्ति पहल, 2023).
- एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स पुन: प्रयोग गर्न मिल्ने हुन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ, जसलाई म लागत र स्थायित्व वार्तालापमा जोड दिन्छु (US EPA, 2023).
- जस्ता दाबी गर्छन् “सबैभन्दा ठूलो” वा “सबै भन्दा राम्रो” कारखानाको अर्थ बिना सन्दर्भको सानो हो, त्यसैले म टूलिङ्ग लागत मा बेन्चमार्क आपूर्तिकर्ताहरु, MOQ, द्रुत-परिवर्तन उत्पादन, र यसको सट्टा प्रमाणित प्रोटोटाइप-देखि-उत्पादन समर्थन.
प्लास्टिक एक्सट्रुजन कम्पनीहरू र कारखानाहरूले वास्तवमा के गर्छन्
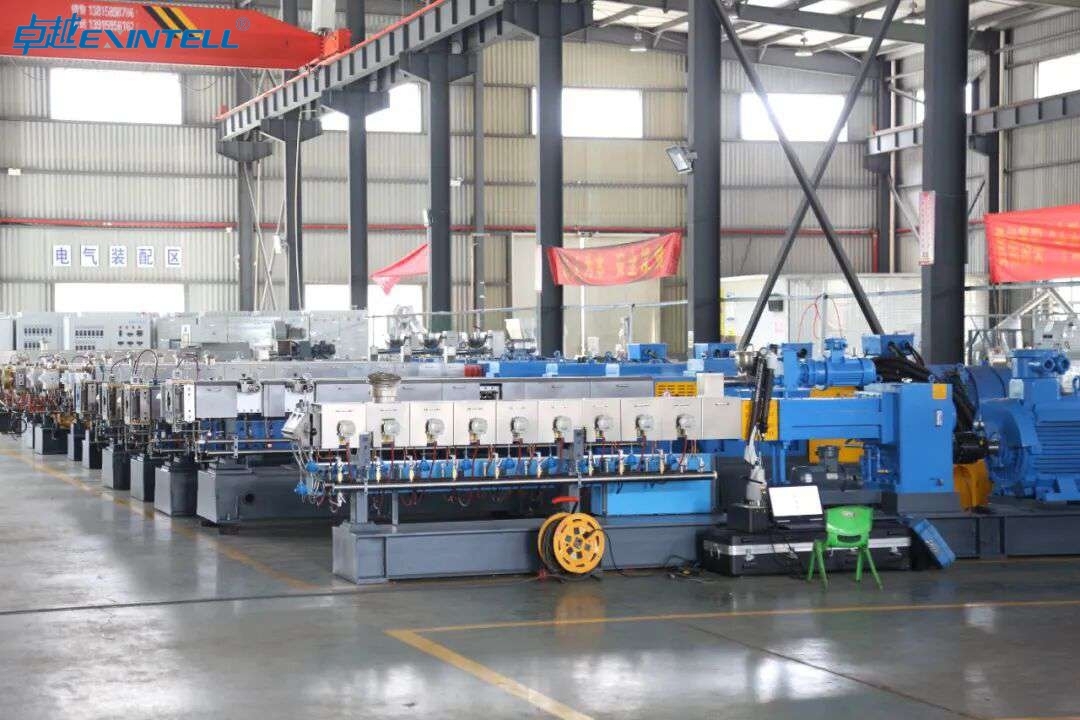
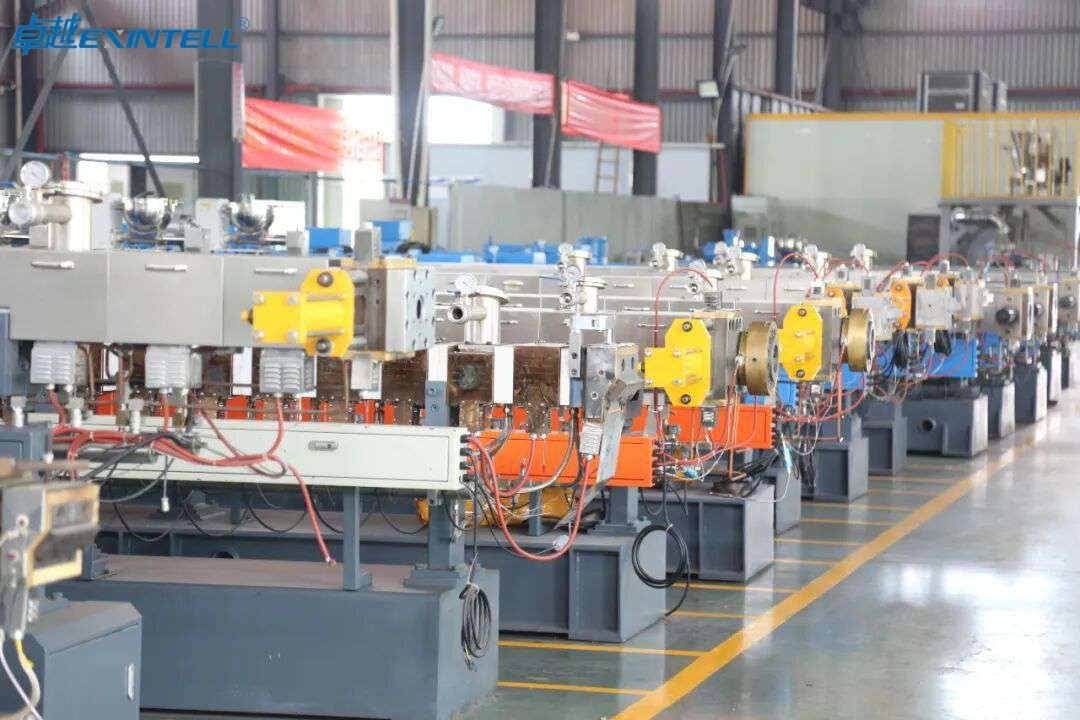
जब म ग्राहकको लागि आपूर्तिकर्ताको मूल्याङ्कन गर्छु, म शब्द के हो स्पष्ट पारेर सुरु गर्छु “बाहिर निकाल्ने” वास्तवमा पसल फ्लोरमा वर्णन गर्दछ. प्लास्टिक एक्सट्रुजनले कच्चा प्लास्टिक सामग्री पग्लन्छ र यसलाई स्थिर क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ। (सीगेट प्लास्टिक, 2024). त्यो एक वाक्यले धेरै भार बोक्छ: प्रक्रिया शट-द्वारा-शटको सट्टा निरन्तर छ, र ज्यामितिलाई दुई-आयामी क्रस-सेक्शन द्वारा परिभाषित गरिएको छ जुन भागको पूर्ण लम्बाइ चलाउँछ।. यसैले यो लामो उत्पादन रन र उच्च-भोल्युम निर्माण यति राम्रोसँग उपयुक्त छ, र यो इन्जेक्शन मोल्डिङ वा मेसिनिङबाट साँच्चै फरक अनुशासन हो.
व्यवहारमा, “राल निकासी” तीनवटा फराकिलो आउटपुट परिवारहरूको पछाडिको इन्जिन हो जुन मैले प्रायः अनुरोध गरेको देख्छु:
- प्रोफाइलहरू - परिभाषित क्रस-सेक्शनको साथ अनुकूलन प्लास्टिक प्रोफाइलहरू, साधारण च्यानलहरू र एज ट्रिमहरूबाट जटिल बहु-लुमेन आकारहरूमा. यो हो जहाँ प्रोफाइल एक्सट्रुजन र को-एक्सट्रुजन साँच्चै चम्किन्छ.
- ट्युबिङ - गोलो, अंडाकार, र मेडिकलमा बहु-लुमेन ट्यूब प्रयोग गरिन्छ, तरल पदार्थ ह्यान्डलिङ, र वायमेटिक अनुप्रयोगहरू, एक विशेष प्लास्टिक ट्युबिंग आपूर्तिकर्ता बाट स्रोत.
- पाना - प्यानलहरूको लागि प्लास्टिक पाना बाहिर निकाल्ने, लाइनरहरू, र थर्मोफर्मिङ स्टक, फ्ल्याट डाइ र रोल स्ट्याक मार्फत उत्पादन.
निर्माताहरू, कारखानाहरू, र वितरकहरू समान छैनन्
क्रेताहरूले प्रायः यी सर्तहरू आदानप्रदान गर्न प्रयोग गर्छन्, र यसले तिनीहरूलाई समय खर्च गर्दछ. यहाँ म तिनीहरूलाई कसरी अलग गर्छु:
- ए निर्माता वा कारखाना एक्सट्रुसन लाइनहरूको स्वामित्व छ, आफ्नै मृत्यु काट्छ, र राल देखि समाप्त भाग सम्म प्रक्रिया नियन्त्रण गर्दछ. यो तपाइँ अनुकूलन उपकरण को लागी चाहानुहुन्छ, कडा प्रक्रिया नियन्त्रण, वा इन्जिनियरिङ ग्रेड प्लास्टिक.
- ए वितरक वा पुनर्विक्रेता स्टक र जहाजहरू मानक आकारहरू तर सामान्यतया लाइन चलाउँदैन. स्टक एक्स्ट्रुडेड आकारहरू र द्रुत पुन: क्रमका लागि उत्कृष्ट, अनुकूलन कार्यको लागि कम.
- ए निर्माता स्टक प्रोफाइल र मेसिन किन्न सक्छ, वेल्ड, वा तिनीहरूलाई समाप्त प्लास्टिक निर्माण सेवा डेलिभरेबलहरूमा भेला गर्नुहोस्.
जब म Thomasnet खोज्छु, म जानाजानी फिल्टर गर्छु, किनभने ती डाइरेक्टरीहरूले यूएस प्लास्टिक एक्सट्रुजन निर्माताहरूलाई क्षमता र क्षेत्रद्वारा सूचीकृत र वर्गीकृत गर्छन् (Thomasnet, 2024). त्यो क्षमता फिल्टरले तपाईंलाई बताउँछ कि तपाईं वास्तविक प्लास्टिक प्रोफाइल निर्माता वा बिचौलियासँग कुरा गर्दै हुनुहुन्छ.
किन खरीददारहरू खोज्छन् “कारखाना” को सट्टा “आपूर्तिकर्ता”
मेरो अनुभवमा, तिर परिवर्तन “कारखाना” भाषा संकेत आशय. यसलाई टाइप गर्ने क्रेताहरूले डाइ डिजाइन र टूलिङमा इन-हाउस नियन्त्रणको साथ स्रोत चाहन्छन्, पारदर्शी MOQ कुराकानीहरू, र प्रोटोटाइप देखि उत्पादन मापन गर्ने क्षमता. यसले पुन: प्राप्तिको दबाब पनि प्रतिबिम्बित गर्दछ: आन्तरिक स्रोतले माल ढुवानी कम गरेर कुल भूमि लागत घटाउन सक्छ, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023), र अमेरिकी प्लास्टिक उद्योग घरेलु उत्पादन ढुवानी र रोजगारीमा प्रमुख योगदानकर्ता बनेको छ (प्लास्टिक उद्योग संघ, 2023). एक घरेलु प्लास्टिक निर्माता खोज्दै, एक सामान्य आपूर्तिकर्ता भन्दा, अक्सर जानाजानी जोखिम र लागत निर्णय हो.
कसरी प्लास्टिक एक्सट्रुजन प्रक्रिया काम गर्दछ, चरणबद्ध रूपमा

मेकानिक्स बुझ्दा तपाईंलाई राम्रो प्रश्नहरू सोध्न र उद्धरण सही रूपमा पढ्न मद्दत गर्दछ. ट्विन स्क्रू एक्स्ट्रुडर निर्माता निर्माता म निरन्तर निकासी प्रक्रियाको पाँच चरणहरूमा ग्राहकहरूलाई हिंड्छु.
1. कच्चा माल खुवाउने र ब्यारेलमा पग्लने
थर्मोप्लास्टिक छर्राहरू - सामान्यतया PVC, ABS, HDPE, LDPE, वा पोलीप्रोपाइलिन - एक हपर प्रविष्ट गर्नुहोस् र घुमाउने पेंचको साथ तातो ब्यारेलमा खसाउनुहोस्. ब्यारेल हीटर र स्क्रू शियरको संयोजनले राललाई एकसमान पिघलाएको धारामा पग्लन्छ।. सामग्री छनोट यहाँ महत्त्वपूर्ण छ: PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्राय: प्रोफाइलहरूमा प्रयोग गरिन्छ, पाइप, र ट्युबिङ (प्लास्टिक उद्योग संघ), जबकि polycarbonate, एक्रिलिक (PMMA), नायलन (PA), र PEEK ले थप माग सेवा गर्दछ, ईन्जिनियरिङ्-ग्रेड अनुप्रयोगहरू. पुनर्नवीनीकरण गरिएको रिग्राइन्डलाई प्राय: फिर्ता मिलाउन सकिन्छ, र एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिकहरू पुन: प्रयोग गर्न मिल्ने छन्, त्यसैले पुन: प्रयोगले सामग्रीको दक्षता सुधार गर्दछ (US EPA, 2023).
2. कस्टम डाइ मार्फत पग्लिएको प्लास्टिक जबरजस्ती
पिघलिएको एक डाइ मार्फत धकेलिएको छ जसले प्रोफाइल क्रस-सेक्शन परिभाषित गर्दछ. यो प्रक्रियाको मुटु हो र कारण अनुकूलन कार्यले टूलिङ्ग लागत बोक्छ. एक को-एक्सट्रुजन सेटअपले एकल डाइलाई खुवाउने एक भन्दा बढी एक्स्ट्रुडर प्रयोग गर्दछ, तपाईंलाई सामग्रीहरू संयोजन गर्न दिँदै — नरम TPE/TPU सील ओठको साथ एक कठोर सब्सट्रेट, उदाहरण को लागी, वा कम लागतको कोरमा रंगीन टोपी तह.
3. चिसो, साइजिङ, र निरन्तर टेक-अफ
मर्न छोडेर, नरम प्रोफाइल कूलिंग र साइजिङ प्रणाली मार्फत जान्छ - सामान्यतया पानीको नुहाउने वा भ्याकुम साइजिङ ट्याङ्की - जुन आयामहरूमा लक हुन्छ।. एक टेक अफ (तान्ने) नियन्त्रित गतिमा प्रोफाइल कोर्छ. किनभने यो भाग निरन्तर बनिरहन्छ र चिसो हुँदा सामग्री संकुचित हुन्छ, बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ (प्रोटोल्याबहरू, 2023). मैले त्यो अपेक्षा चाँडै सेट गर्छु ताकि ग्राहकहरूले सटीकको लागि भुक्तान गर्नुको सट्टा यथार्थपरक सहिष्णुताको अनुमान लगाउने प्रक्रिया आर्थिक रूपमा समात्न सक्दैन।.
4. लम्बाइ र माध्यमिक निर्माणमा काट्ने
इन-लाइन आरा वा चक्कुले निरन्तर आउटपुटलाई लम्बाइमा काट्छ. त्यहाँबाट, माध्यमिक कार्यहरू - ड्रिलिंग, मुक्का मार्दै, नचिङ, मुद्रण, वा असेंबली - एक्स्ट्रुडेड प्लास्टिक पार्ट्सलाई समाप्त कम्पोनेन्टमा बदल्नुहोस्. यो कच्चा प्रोफाइल र एक प्रयोगयोग्य डेलिभर योग्य बीचको पुल हो, र यो हो जहाँ द्रुत-परिवर्तन उत्पादन या त जितिन्छ वा हराउँछ.
कस्टम बनाम स्टक प्लास्टिक एक्सट्रुसन: तपाईलाई कुन चाहिन्छ?
यो निर्णय हो जुन मलाई प्रायः सोधिन्छ, र इमानदार जवाफ छ: यो मात्रा मा निर्भर गर्दछ, ज्यामिति, र टाइमलाइन. मलाई प्रत्येक बाटो तोड्न दिनुहोस्.
जब अफ-द-शेल्फ स्टक प्रोफाइलहरू सही विकल्प हुन्
स्टक एक्सट्रुडेड आकारहरू - मानक रड, ट्यूब, च्यानल, कोण, र पाना - टुलिङ लागत पूर्ण रूपमा बेवास्ता गर्नुहोस् र छिटो पठाउनुहोस्. यदि एक क्याटलग प्रोफाइल स्वीकार्य सहिष्णुता भित्र तपाईंको आवेदन फिट हुन्छ, स्टक खरिद लगभग सधैं सस्तो छ, छिटो मार्ग. म प्रोटोटाइपहरूको लागि यहाँ ग्राहकहरूलाई स्ट्रियर गर्छु, कम मात्रा, र कुनै पनि भाग जहाँ मानक क्रस-सेक्शनले काम गर्छ.
जब अनुकूलन उपकरण र प्रोफाइलहरू उचित हुन्छन्
कस्टम एक्सट्रुसनलाई सामान्यतया एक पटकको टूलिङ र डाइ लगानी चाहिन्छ, जबकि स्टक प्रोफाइल यो लागत जोगिन (उद्योग स्रोत निर्देशन). तपाईंको ज्यामिति स्वामित्व भएको बेला त्यो मर लागत उचित हुन्छ, जब अनुकूलन क्रस-सेक्शनले डाउनस्ट्रीम असेंबली हटाउँछ, वा जब वार्षिक मात्रा उपकरण परिशोधन गर्न पर्याप्त उच्च छ. एक निश्चित रन साइज माथि, उद्देश्य-निर्मित डाइको प्रति-फुट बचत अग्रिम खर्च भन्दा बढी हुन्छ.
हाइब्रिड दृष्टिकोण: मानक प्रोफाइलहरू, अनुकूलन भागहरू
मेरो मनपर्ने मध्य मार्ग अक्सर बेवास्ता गरिन्छ. मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024). तपाईं डाइ लगानी छोड्नुहोस्, त्यसपछि काट्ने प्रयोग गर्नुहोस्, मेसिनिङ, र एक अनुकूलन डेलिभर गर्न को लागी विधानसभा. धेरै मध्य-भोल्युम कार्यक्रमहरूको लागि, यो हाइब्रिडले कुल लागतमा शुद्ध स्टक र पूर्ण कस्टम दुवैलाई हराउँछ.
लागत र नेतृत्व-समय तुलना
यहाँ कसरी तीन दृष्टिकोणहरू सामान्यतया तुलना गरिन्छ. यसलाई दिशात्मक योजना दायराको रूपमा व्यवहार गर्नुहोस्, उद्धरणहरू होइन - वास्तविक तथ्याङ्कहरू सामग्रीमा निर्भर हुन्छन्, ज्यामिति, र भोल्युम.
|
कारक |
स्टक प्रोफाइलहरू |
हाइब्रिड (निर्मित मानक) |
पूर्ण कस्टम एक्सट्रुजन |
|---|---|---|---|
|
अग्रिम उपकरण लागत |
कुनै पनि छैन |
कुनै पनि कम छैन (फिक्स्चर मात्र) |
एक पटक मर्ने लगानी |
|
सामान्य नेतृत्व समय |
सबैभन्दा छोटो (अक्सर स्टक मा) |
छोटो देखि मध्यम |
सबैभन्दा लामो (मर्ने निर्माण + पहिलो लेख) |
|
न्यूनतम अर्डर (MOQ) |
कम |
कम देखि मध्यम |
उच्च (उपकरण परिशोधन गर्न) |
|
ज्यामिति लचिलोपन |
क्याटलग आकारहरू मात्र |
मानक आकार + मेसिनिङ |
पूर्ण रूपमा अनुरूप क्रस-सेक्शन |
|
उत्तम फिट |
प्रोटोटाइपहरू, कम मात्रा |
मध्य भोल्युम, हल्का अनुकूलन |
उच्च मात्रा, स्वामित्व प्रोफाइलहरू |
|
कारक |
स्टक प्रोफाइलहरू |
हाइब्रिड (निर्मित मानक) |
पूर्ण कस्टम एक्सट्रुजन |
|---|---|---|---|
|
अग्रिम उपकरण लागत |
कुनै पनि छैन |
कुनै पनि कम छैन (फिक्स्चर मात्र) |
एक पटक मर्ने लगानी |
|
सामान्य नेतृत्व समय |
सबैभन्दा छोटो (अक्सर स्टक मा) |
छोटो देखि मध्यम |
सबैभन्दा लामो (मर्ने निर्माण + पहिलो लेख) |
|
न्यूनतम अर्डर (MOQ) |
कम |
कम देखि मध्यम |
उच्च (उपकरण परिशोधन गर्न) |
|
ज्यामिति लचिलोपन |
क्याटलग आकारहरू मात्र |
मानक आकार + मेसिनिङ |
पूर्ण रूपमा अनुरूप क्रस-सेक्शन |
|
उत्तम फिट |
प्रोटोटाइपहरू, कम मात्रा |
मध्य भोल्युम, हल्का अनुकूलन |
उच्च मात्रा, स्वामित्व प्रोफाइलहरू |
जुन बाटो रोज्नुस, म पसलले कागजात गुणस्तर प्रणाली चलाएको पुष्टि गर्न सिफारिस गर्छु - ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो (ISO, 2015) र प्लास्टिक क्षेत्रमा सबैभन्दा व्यापक रूपमा अपनाइने बेन्चमार्क रहन्छ. स्टक र अनुकूलन प्रस्तावहरू कसरी साथसाथै बस्छन् भन्ने व्यावहारिक दृष्टिकोणको लागि, म फेला पार्छु सीगेट प्लास्टिक’ अनुकूलन एक्सट्रुजन सिंहावलोकन एक उपयोगी सन्दर्भ बिन्दु.
प्लास्टिक एक्सट्रुजन प्रोफाइल र उत्पादन को प्रकार

जब म एक्सट्रुसनको लागि परियोजनाको मूल्याङ्कन गर्छु, म क्रस-सेक्शनबाट सुरु गर्छु, किनभने समाप्त भागको ज्यामितिले लगभग सबै डाउनस्ट्रीमलाई निर्देशित गर्दछ: मर डिजाइन, सामग्री छनोट, र अन्ततः तपाईले तिर्नुपर्ने मूल्य. प्लास्टिक एक्सट्रुजनले कच्चा राल पग्लन्छ र यसलाई निश्चित क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ। (सीगेट प्लास्टिक, 2024). त्यो एकल सिद्धान्तले आकारहरूको आश्चर्यजनक रूपमा विस्तृत सूची उत्पादन गर्दछ, त्यसैले यसले तिनीहरूलाई जटिलता र कार्यद्वारा समूहबद्ध गर्न मद्दत गर्दछ.
ठोस प्रोफाइलहरू, खाली प्रोफाइलहरू, र जटिल ज्यामिति
ठोस प्रोफाइल उद्योग को workhorses हो: रडहरू, बारहरू, किनारा, र कुनै आन्तरिक रिक्तता बिना ट्रिम गर्नुहोस्. तिनीहरू उपकरणको लागि सबैभन्दा सजिलो र सहिष्णुतामा सबैभन्दा क्षमाशील छन्, यही कारणले गर्दा म तिनीहरूलाई डिजाइन परीक्षण गर्न पहिलो पटक खरीददारहरूको लागि सिफारिस गर्दछु. खाली प्रोफाइलहरूले आन्तरिक च्यानलहरू परिचय गर्दछ, र तिनीहरूले पिघल चिसो हुँदा गुफालाई खुला राख्नको लागि म्यान्डरेल वा पिनहरू सहित थप परिष्कृत डाइजहरू माग्छन्।. जटिल ज्यामितिहरूले धेरै पर्खालहरू जोड्छन्, अन्डरकटहरू, र एकल क्रस-सेक्शनमा पातलो देखि बाक्लो ट्रान्जिसनहरू, र यो जहाँ डाइ डिजाइन र टूलिङ विशेषज्ञताले एक सक्षम प्लास्टिक प्रोफाइल निर्मातालाई औसतबाट अलग गर्दछ. मेरो अनुभवमा, असमान पर्खाल मोटाई warping को सबैभन्दा सामान्य कारण हो, त्यसैले म आपूर्तिकर्ताहरूलाई प्रोफाईलमा सामग्रीको प्रवाहलाई सन्तुलनमा राख्ने योजनाको बारेमा चाँडै थिच्दछु.
ट्युबिङ र बहु-लुमेन एक्सट्रुसन
ट्युबिङ खोक्रो निकासी को एक विशेष उपसेट हो, र यसले भागको लम्बाइमा चल्ने धेरै समानान्तर च्यानलहरूसँग साधारण एकल-बोर ट्यूबदेखि बहु-लुमेन डिजाइनहरूसम्म सबै कुरा फैलाउँछ।. चिकित्सा उपकरण र विश्लेषणात्मक उपकरण खरीददारहरू तरल पदार्थ बोक्न बहु-लुमेन एक्सट्रुसनहरूमा झुक्छन्, तारहरू, र एक कम्प्याक्ट प्रोफाइल मार्फत सेन्सरहरू. एक भरपर्दो प्लास्टिक ट्युबिंग आपूर्तिकर्ताले कडा एकाग्रता र भित्री-व्यास सहिष्णुता राख्छ।, यद्यपि म सँधै ग्राहकहरूलाई सम्झाउँछु कि सामग्री संकुचन र निरन्तर गठनको कारणले गर्दा एक्स्ट्रुजन सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा कम हुन्छ। (Protolabs डिजाइन संसाधनहरू, 2023). त्यससँग लड्नुको सट्टा त्यो वास्तविकताको वरिपरि आफ्नो फिट र क्लियरेन्सको योजना बनाउनुहोस्.
सह-निकास र बहु-सामग्री प्रोफाइलहरू
को-एक्सट्रुजनले दुई वा बढी रेजिनहरू साझा डाइ मार्फत चलाउँछ अलग सामग्री क्षेत्रहरूको साथ एकल प्रोफाइल उत्पादन गर्न।. म यसलाई प्रयोग गर्छु जब एक भागलाई एकै पटक विरोधाभासी गुणहरू चाहिन्छ, जस्तै नरम TPE/TPU ग्यास्केट ओठको साथ कठोर PVC संरचनात्मक शरीर, वा कम लागत सब्सट्रेट माथि मौसम योग्य टोपी तह. यसले माध्यमिक विधानसभा र बन्धन चरणहरू हटाउँछ, जुन भोल्युममा सार्थक लागत बचत हो. ट्रेडअफ टूलिङ जटिलता हो, त्यसैले म डिजाइनहरूको लागि को-एक्सट्रुजन आरक्षित गर्छु जहाँ बहु-सामग्री लाभले थपिएको डाइ लगानीलाई स्पष्ट रूपमा औचित्य दिन्छ।.
प्रत्येक प्रकारको लागि साझा उद्योग अनुप्रयोगहरू
विभिन्न ज्यामितिहरू विभिन्न क्षेत्रहरूमा गुरुत्वाकर्षण हुन्छन्, र तिनीहरूलाई प्रारम्भिक मिलानले सोर्सिङ कुराकानीहरूलाई केन्द्रित राख्छ.
- ठोस प्रोफाइलहरू: खुद्रा शेल्फ किनारा, फर्निचर ट्रिम, सिलहरू, र फेंसिंग घटकहरू.
- खाली प्रोफाइलहरू: झ्याल र ढोका फ्रेमहरू, एलईडी प्रकाश च्यानलहरू, र संरचनात्मक आवरण.
- ट्युबिङ र बहु-लुमेन: मेडिकल क्याथेटरहरू, तरल स्थानान्तरण लाइनहरू, र वायमेटिक ट्युबिङ.
- सह-निकासी प्रोफाइलहरू: मौसम स्ट्रिपिङ, प्रशीतन gaskets, र डुअल ड्युरोमिटर ह्यान्डलहरू.
- पाना निकासी: चिन्ह, थर्मोफर्मिङ स्टक, र सुरक्षात्मक प्यानलहरू.
किनभने प्लास्टिक निकासी एक निरन्तर छ, उच्च मात्रा प्रक्रिया, यो लामो उत्पादन चल्छ विशेष गरी राम्रो संग, र मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024). यदि तपाईंको वार्षिक माग स्थिर छ र हजारौं फीट मा मापन, बाहिर निकाल्ने अर्थशास्त्रले तपाईंको पक्षमा कडा रूपमा काम गर्दछ.
प्लास्टिक एक्सट्रुजनमा प्रयोग हुने सामान्य सामग्री
सामग्री छनोट भनेको निर्णय हो जुन मैले खरीददारहरूलाई प्रायः कम मूल्याङ्कन गरेको देख्छु. रालले मेकानिकल शक्तिलाई नियन्त्रण गर्दछ, रासायनिक प्रतिरोध, तापमान दायरा, लागत, र एक्स्ट्रुडरले वास्तविक रूपमा समात्न सक्ने सहिष्णुता कति कडा हुन्छ. म एक्स्ट्रुजन रेजिनलाई तीन तहमा समूहबद्ध गर्छु, त्यसपछि एप्लिकेसनले वास्तविक रूपमा माग गरेसम्म मात्र माथि जानका लागि ग्राहकहरूसँग काम गर्नुहोस्.
कमोडिटी रेजिन्स: PVC, पोलिथीन, र Polypropylene
कमोडिटी रेजिन्सले बहुसंख्यक एक्सट्रुडेड भोल्युमलाई कभर गर्दछ, र राम्रो कारणको लागि. PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्रोफाइलहरूमा सामान्य, पाइप, र ट्युबिङ (प्लास्टिक उद्योग संघ). यसले कठोरता प्रदान गर्दछ, मौसम क्षमता, र कम लागत, र यसले रंग र सतह समाप्त राम्रोसँग लिन्छ. Polyethylene दुई परिचित ग्रेडहरूमा देखा पर्दछ: कडा लागि HDPE, रासायनिक प्रतिरोधी प्रोफाइलहरू र LDPE जहाँ लचिलोपन महत्त्वपूर्ण छ. Polypropylene राम्रो शक्ति-देखि-तौल अनुपात र जीवित-काज प्रदर्शन संग रासायनिक प्रतिरोध सन्तुलन।. जब एक ग्राहकले उच्च-भोल्युमको लागि राल एक्सट्रुसनको बारेमा सोध्छ, लागत-संवेदनशील भाग, यो लगभग सधैं जहाँ म सुरु गर्छु.
इन्जिनियरिङ रेजिन: ABS, पोली कार्बोनेट, नायलन, र एक्रिलिक
ईन्जिनियरिङ्-ग्रेड प्लास्टिकले मेकानिकल र थर्मल कार्यसम्पादनमा कदम चाल्छ. ABS delivers impact strength and clean finishes for consumer and enclosure parts. Polycarbonate brings high impact resistance and optical clarity, which makes it a staple for lighting lenses and safety glazing. नायलन (PA) offers wear resistance and toughness for mechanical components and cable management. एक्रिलिक (PMMA) provides excellent clarity and UV stability for display and signage profiles. I move buyers into this tier when commodity resins cannot meet load, गर्मी, or clarity requirements, and I make sure they price the resin premium against the performance gain before committing.
High-Performance Materials Like PEEK
At the top sits a small group of high-performance polymers, with PEEK as the reference point. PEEK withstands continuous high temperatures, आक्रामक रसायनहरू, and demanding mechanical loads, जसले गर्दा यो एयरोस्पेसमा देखिन्छ, चिकित्सा, and semiconductor applications. The material cost is substantial, त्यसैले म यसलाई मात्र निर्दिष्ट गर्छु जब अपरेटिङ वातावरणले सस्तो विकल्प छोड्दैन. प्रत्येक प्लास्टिक प्रोफाइल निर्माताले PEEK प्रक्रिया गर्दैन, त्यसैले क्षमता स्क्रिनिङ यस स्तरमा बढी महत्त्वपूर्ण छ.
अनुप्रयोग आवश्यकताहरूसँग मिल्दो सामग्री गुणहरू
मेरो चयन फ्रेमवर्क जानाजानी सरल छ: पहिले गैर-विवादनीय आवश्यकता परिभाषित गर्नुहोस्, त्यसपछि यसलाई खाली गर्ने कम्तीमा महँगो राल छान्नुहोस्. तलको तालिकाले म कसरी एक्सट्रुडेड प्लास्टिक पार्ट्सका लागि सामान्य विकल्पहरू तौल गर्छु भन्ने सारांश दिन्छ.
| सामग्री | टियर | कुञ्जी शक्तिहरू | सापेक्ष लागत | सामान्य अनुप्रयोगहरू |
|---|---|---|---|---|
| PVC | कमोडिटी | कडा, मौसम योग्य, कम लागत | $ | प्रोफाइलहरू, पाइप, ट्रिम |
| HDPE / LDPE | कमोडिटी | रासायनिक प्रतिरोध; कडा वा लचिलो | $ | ट्युबिङ, लाइनरहरू, डक्टिङ |
| Polypropylene | कमोडिटी | रासायनिक प्रतिरोध, जीवित टिकाहरू | $ | तरल पदार्थ व्यवस्थापन, टिका |
| ABS | इन्जिनियरिङ | प्रभाव शक्ति, सफा समाप्त | $$ | घेराहरू, उपभोक्ता भागहरू |
| पोली कार्बोनेट | इन्जिनियरिङ | प्रभाव प्रतिरोध, स्पष्टता | $$ | लेन्सहरू, सुरक्षा ग्लेजिङ्ग |
| नायलन (PA) | इन्जिनियरिङ | प्रतिरोध लगाउने, कठोरता | $$ | मेकानिकल, केबल गाइडहरू |
| एक्रिलिक (PMMA) | इन्जिनियरिङ | स्पष्टता, यूवी स्थिरता | $$ | साइनेज, प्रदर्शन गर्दछ |
| हेर्नुहोस | उच्च प्रदर्शन | गर्मी, रासायनिक, र लोड प्रतिरोध | $$$$ | एयरोस्पेस, चिकित्सा, अर्धचालक |
कुनै पनि आपूर्तिकर्ता संग उठाउन लायक एक दक्षता बिन्दु: एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स रिसाइकल गर्न सकिन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ (अमेरिकी पर्यावरण संरक्षण एजेन्सी, 2023). Asking how a factory handles regrind tells me something about both their cost discipline and their sustainability practices.
Plastic Extrusion Manufacturers in the USA
For many of the buyers I advise, the sourcing question is not only “who can extrude this profile” but “who can extrude it here.” Domestic sourcing has moved from a preference to a strategic decision, and it deserves a clear-eyed look rather than reflexive patriotism.
Why US-Based Sourcing Matters for Many Buyers
The financial case is stronger than it first appears. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023). When I run a total-cost comparison rather than a unit-price comparison, offshore savings often shrink once I add ocean freight, शुल्कहरू, सुरक्षा स्टक, and the working capital tied up in long transit times. For a domestic plastics manufacturer serving a US customer, lead times measured in weeks rather than months also mean less risk if a design changes mid-program.
Regional Manufacturing Hubs Across the Country
US extrusion capacity is not evenly distributed, and knowing the map speeds up sourcing. The Great Lakes and Upper Midwest concentrate general-purpose profile and tubing extruders near automotive and industrial demand. The Northeast holds a dense cluster of medical and precision tubing specialists. The Southeast has grown quickly around building products and packaging. The West Coast and Southwest serve electronics, एयरोस्पेस, and consumer markets. Supplier directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is where I usually build a first shortlist before making calls.
Domestic Quality, सञ्चार, and IP Advantages
Beyond cost, three practical advantages keep drawing buyers home. पहिले, quality systems are easier to verify in person; ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो (मानकीकरणको लागि अन्तर्राष्ट्रिय संगठन, 2015), and I can audit a domestic supplier’s implementation without an international trip. दोस्रो, time-zone-aligned communication shortens the feedback loop from prototype to production, which matters when a die needs a mid-run adjustment. तेस्रो, intellectual property protection is more enforceable under US jurisdiction, a real concern when a custom profile is a competitive differentiator. I treat these as the differences that a spreadsheet alone will miss.
How US Factories Serve Diverse Industries
American extruders span the full range of contract manufacturing, from stock extruded shapes shipped from inventory to fully custom die programs. Custom extrusion typically requires a one-time tooling or die investment, while stock profiles avoid that cost, so I match the sourcing path to how unique the geometry really needs to be. The US plastics industry remains a major contributor to domestic manufacturing shipments and employment (प्लास्टिक उद्योग संघ, 2023), and that depth means a buyer can usually find a plastic fabrication services partner suited to their volume, from prototype to production. For a broad view of custom capabilities, I often point clients to overviews such as custom plastic extrusion manufacturers to calibrate expectations before requesting quotes.
How to Find Plastic Extrusion Companies Near You
जब म सोर्सिङ परियोजना सुरु गर्छु, geography is one of the first variables I weigh. Location shapes freight cost, संचार ताल, and how quickly I can iterate from prototype to production. त्यो भने, proximity is only valuable when the nearby supplier can actually do the work. मेरो अनुभवमा, the smartest approach treats “मेरो नजिक” as a filter, निर्णय होइन.
Why Local Sourcing Often Pays Off
A domestic plastics manufacturer close to your facility gives you three concrete advantages. पहिले, shorter shipping distances lower freight and lead-time risk, which matters for bulky extruded plastic parts and long profiles that ship as oversized freight. दोस्रो, local partners make on-site visits practical, and I have caught more process issues in a two-hour plant walkthrough than in weeks of email. तेस्रो, proximity accelerates iteration: when a die needs a tweak, a supplier a few hours away can turn samples faster than one across an ocean.
The financial case reaches beyond the unit price. According to the Reshoring Initiative (2023), आन्तरिक स्रोतले माल ढुवानी कम गरेर कुल भूमि लागत घटाउन सक्छ, कर्तव्य, र सूची बोक्ने लागत. The domestic base is substantial, पनि; प्लास्टिक उद्योग संघ (2023) reports that the US plastics industry is a major contributor to domestic manufacturing shipments and employment, which means qualified capacity for resin extrusion is usually within reach.
Where I Look: Directories, Associations, and Referrals
To build an initial list of candidates, I use three complementary channels:
- Supplier directories. Thomasnet (2024) lists and categorizes US plastic extrusion manufacturers by capability and region, which makes it straightforward to filter by material, प्रक्रिया, and location.
- Trade associations. Membership in bodies like the Plastics Industry Association signals a firm that invests in standards and industry engagement.
- Referrals. A recommendation from an engineer who has run production with a plastic profile manufacturer carries more weight than any marketing page, because it reflects delivered performance.
I treat the directory as a starting point for a plastic tubing supplier or profile shop, then validate each name against real references before it earns a spot on my shortlist.
Balancing Proximity Against Capability and Price
Distance is a tiebreaker, not a trump card. If a nearby shop cannot hold your tolerances, run your resin, or meet your volume, the convenience is worthless. I rank capability and quality first, त्यसपछि मूल्य, then location. एक प्लास्टिक एक्सट्रुजन कम्पनी कारखाना आपूर्तिकर्ता सही सह-एक्सट्रुजन लाइन र प्रमाणित ISO संग दुई राज्य टाढा 9001 प्रणालीले सामान्यतया मलाई ती क्षमताहरू नभएको नजिकको पसल भन्दा राम्रो सेवा दिनेछ.
जब स्थानीय उत्तम विकल्प होइन
कहिलेकाहीँ सही पार्टनर नजिकै हुँदैन. PEEK जस्ता ईन्जिनियरिङ्-ग्रेड प्लास्टिकहरूमा विशेष काम, polycarbonate, वा नायलन (PA) राष्ट्रिय रूपमा मुट्ठीभर पसलहरूले मात्र राम्रो गर्न सक्छन्. उच्च-भोल्युम उत्पादन कार्यक्रमहरूले ढुवानी अर्थशास्त्रलाई औचित्य दिन सक्छ जुन टाढाको पक्षमा हुन्छ, अधिक स्वचालित बिरुवा. र जब तपाईलाई इन-लाइन फेब्रिकेसनसँग मिलाएर प्लास्टिक पाना एक्सट्रुसन जस्ता क्षमताहरू चाहिन्छ, प्रक्रियाको फिट माइलेज भन्दा बढी महत्त्वपूर्ण छ. ती अवस्थाहरूमा म खोजको दायरा फराकिलो गर्छु र दूरीको अन्तर बन्द गर्न भिडियो प्लान्ट टुरहरू र तेस्रो-पक्ष अडिटहरूमा झुक्छु।.
Understanding the Largest Plastic Extrusion Companies
Buyers often gravitate toward the biggest names, assuming scale guarantees a better outcome. Scale does deliver real advantages, but it also carries tradeoffs. Understanding what “सबैभन्दा ठूलो” actually means helps me match a supplier’s footprint to my program rather than to a reputation.
What Scale Means for Capacity and Reliability
निकासी एक निरन्तर छ, high-volume process well suited to long production runs, and large factories are built around that reality. More extrusion lines mean higher throughput, redundancy if one line goes down, and the ability to absorb demand spikes. Scale usually correlates with mature quality systems as well; ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (मानकीकरणको लागि अन्तर्राष्ट्रिय संगठन, 2015), is almost table stakes among large plants. That maturity translates into more consistent extruded plastic parts across long runs.
The Tradeoffs of Large Factories vs. Specialized Shops
Bigger is not automatically better. Large plants optimize for volume, which can mean higher minimum order quantities, less flexibility on small custom runs, and slower responsiveness on prototype work. A specialized shop may excel at tight-tolerance custom plastic profiles, unusual resins, or quick-turnaround production that a high-volume plant treats as a nuisance. The table below summarizes how I weigh the two.
| कारक | Large-Scale Factory | Specialized Shop |
|---|---|---|
| क्षमता | उच्च; multiple lines, redundancy | सीमित; fewer lines |
| न्यूनतम अर्डर मात्रा | Often high | Usually flexible |
| Prototype speed | ढिलो; volume-focused scheduling | छिटो; agile setup |
| सामग्री दायरा | Broad commodity resins (PVC, HDPE, LDPE, PP) | Often engineering-grade (हेर्नुहोस, पीसी, PA) |
| Price per unit at volume | तल्लो | उच्च |
| उत्तम फिट | Long production runs | अनुकूलन, कम देखि मध्य भोल्युम, complex profiles |
जब उच्च-भोल्युम क्षमता आवश्यक छ
त्यहाँ कार्यक्रमहरू छन् जहाँ म स्केलमा सम्झौता गर्दिन. निरन्तर, मानकीकृत प्रोफाइलहरूको लागि लामो समयको माग, पाइप, वा कमोडिटी रेजिन्समा ट्युबिङ ठूलो कारखानाको प्राकृतिक घर हो. PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्राय: प्रोफाइलहरूमा प्रयोग गरिन्छ, पाइप, र ट्युबिङ, र यसलाई भोल्युममा सोर्स गर्दा ठूलो प्लान्टले प्रदान गर्ने अर्थतन्त्रलाई पुरस्कृत गर्दछ. यदि तपाईंको पूर्वानुमानले स्थिर प्रोफाइल क्रस-सेक्शनको लाखौं फीटको लागि कल गर्दछ, उच्च-भोल्युम क्षमता राम्रो-देखि-आवश्यकमा सर्छ.
दावी गरिएको स्केल र क्षमता कसरी प्रमाणित गर्ने
वेबसाइटमा दावीहरू प्रमाण होइनन्. मैले स्वीकार गर्नु अघि ए “सबैभन्दा ठूलो” वा “उच्चतम क्षमता” दावी, म यसलाई ठोस प्रश्नहरूको साथ प्रमाणित गर्छु:
- कतिवटा एक्सट्रुसन लाइनहरू सञ्चालनमा छन्, र प्रत्येक मा डाइ व्यास दायरा के हो?
- वर्तमान उपयोगिता के हो, र मेरो कार्यक्रमको लागि कति अतिरिक्त क्षमता अवस्थित छ?
- के तपाइँ थ्रुपुट तथ्याङ्कहरू साझा गर्न सक्नुहुन्छ (lbs/घण्टा वा खुट्टा/दिन) तुलनात्मक प्रोफाइलको लागि?
- What redundancy exists if a line fails mid-run?
- Which certifications, जस्तै ISO 9001, are current, and may I see the certificate?
I pair those answers with a plant tour or audit. Physical evidence of running lines, staffing, and inventory tells me far more than any capacity figure quoted in a brochure.
How to Identify the Best Plastic Extrusion Factory for Your Project
“Best” is one of the most misused words in supplier marketing. व्यवहारमा, the best plastic extrusion companies factory manufacturer is the one that best fits your specific requirements, not the one with the loudest claim. I define the term relative to my project, then score candidates against that definition.
Defining “Best” Relative to Your Specific Needs
Before comparing suppliers, मेरो परियोजनाले वास्तवमा के माग गर्छ म दस्तावेज गर्छु: राल (भन्नुहोस्, प्रभाव प्रतिरोध को लागी ABS, एक्रिलिक (PMMA) अप्टिकल स्पष्टता को लागी, वा लचिलोपनको लागि TPE/TPU), सहिष्णुता ब्यान्ड, भोल्युम, समयरेखा, र ईन्जिनियरिङ् समर्थनको स्तर मलाई डाइ डिजाइन र टूलिङको लागि चाहिन्छ. सामग्री संकुचन र निरन्तर गठनको कारण बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ। (Protolabs डिजाइन संसाधनहरू, 2023), त्यसैले म प्रारम्भिक पुष्टि गर्छु कि उम्मेदवारले मेरो आयामी आवश्यकताहरू पूरा गर्न सक्छ भनी मान्नुको सट्टा. उच्च-भोल्युम एचडीपीई पाइप चलाउनको लागि आदर्श पसल कडा-सहिष्णु पोली कार्बोनेट प्रोफाइलको लागि गलत छनौट हुन सक्छ।.
तौल गुणस्तर, लागत, गति, र समर्थन
प्रत्येक सोर्सिङ निर्णयले चार लिभरहरूलाई सन्तुलनमा राख्छ, र एक सुधारले अक्सर अर्कोलाई दबाब दिन्छ:
- गुणस्तर. दस्तावेज गुणस्तर प्रणाली, प्रक्रियामा निरीक्षण, र सामग्री ट्रेसबिलिटी. ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics.
- लागत. Not just unit price. कस्टम एक्सट्रुसनलाई सामान्यतया एक पटकको टूलिङ र डाइ लगानी चाहिन्छ, while stock extruded shapes avoid that cost, so I model total cost including tooling and MOQ.
- गति. मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024), but lead times vary widely between shops.
- समर्थन. Engineering input on profile cross-section and material selection can prevent costly redesigns as you move from prototype to production.
Sustainability increasingly enters the equation as well. एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स पुन: प्रयोग गर्न मिल्ने हुन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ (अमेरिकी पर्यावरण संरक्षण एजेन्सी, 2023), which can reduce both cost and waste when a supplier manages it responsibly.
Reading Past “Best” Marketing Claims
Superlatives are easy to print and hard to prove. When I see “सबै भन्दा राम्रो,” “leading,” वा “premier,” I translate the claim into a testable question. Instead of accepting “best quality,” I ask for defect rates and inspection records. को सट्टा “fastest,” I ask for typical lead times on my specific part. को सट्टा “most experienced,” I ask for references in my industry. Marketing language that cannot survive a follow-up question does not influence my shortlist.
Building a Shortlist Scoring Method
To keep the comparison objective, I use a weighted scoring model. I list my criteria, assign each a weight that reflects its importance to the project, score every candidate from 1 को 5, and multiply. The weights shift by project; a prototype program might weight speed and engineering support heavily, while a mature production program weights cost and capacity.
- List criteria: गुणस्तर प्रणालीहरू, material capability, सहिष्णुता, क्षमता, नेतृत्व समय, उपकरण लागत, ईन्जिनियरिङ् समर्थन, and location.
- Assign weights that total 100 percent, reflecting your priorities.
- Score each supplier 1 को 5 on every criterion, using verified evidence rather than marketing claims.
- Calculate weighted totals and rank the candidates.
- Validate the top two with reference calls and, आदर्श रूपमा, प्रतिबद्ध गर्नु अघि एक बिरुवा भ्रमण.
यो संरचित विधिले मलाई काममा फिट हुने साझेदार तर्फ निरन्तर डोर्याएको छ, चाहे त्यो ठूलो बिरुवा हो, एक फुर्तिलो विशेषज्ञ, वा सडकको तल घरेलु पसल. अनुकूलन एक्सट्रुजन क्षमताहरूले अनुप्रयोगहरूमा कसरी नक्सा बनाउँछ भन्ने बारे गहिरो हेराइको लागि, स्रोतहरू जस्तै सीगेट प्लास्टिक’ अनुकूलन एक्सट्रुजन सिंहावलोकन तपाईं आफ्नो मापदण्ड परिष्कृत गर्दा उपयोगी सन्दर्भ हो.
प्लास्टिक एक्सट्रुजन कम्पनीमा मूल्याङ्कन गर्न प्रमुख क्षमताहरू
जब मैले प्लास्टिक प्रोफाइल निर्माताको जाँच गर्छु, म हेर्छु
Extruded भागहरूमा सहिष्णुता र परिशुद्धता
जब म प्लास्टिक प्रोफाइल निर्माताको मूल्याङ्कन गर्छु, सहिष्णुता पहिलो स्थान हो जुन मैले वास्तविकता जाँचको लागि हेर्छु. निकासी एक निरन्तर गठन प्रक्रिया हो, त्यसैले यो मोल्डिंग भन्दा फरक व्यवहार गर्दछ. Protolabs नोटहरूको रूपमा, extrusion tolerances are generally looser than injection molding because material shrinkage and continuous forming introduce variability that a closed mold does not (Protolabs डिजाइन संसाधनहरू, 2023). Setting expectations here early saves both money and rework later.
Typical Achievable Tolerances by Material and Profile
मेरो अनुभवमा, achievable precision depends heavily on the resin and the geometry of the profile cross-section. Rigid engineering-grade plastics hold tighter dimensions than soft or semi-crystalline materials, and simple shapes hold tighter than complex hollow profiles. The ranges below reflect commonly quoted commercial extrusion capabilities for custom plastic profiles; always confirm against your supplier’s published standards for your specific part.
| सामग्री | Dimensional stability | सामान्य सहिष्णुता प्रवृत्ति | निर्दिष्ट गर्नका लागि नोटहरू |
|---|---|---|---|
| कठोर पीवीसी | उच्च | कडा, राम्रोसँग नियन्त्रित | व्यापक रूपमा निकालिएको; प्रोफाइल र ट्युबिङ मा अनुमानित |
| ABS | उच्च | कठोर प्रोफाइलहरूमा कडा | संरचनात्मक extruded प्लास्टिक भागहरु को लागी राम्रो |
| पोली कार्बोनेट | उच्च | टाइट, कम संकुचन | अप्टिकल र प्रभाव-रेटेड अनुप्रयोगहरू |
| एक्रिलिक (PMMA) | उच्च | टाइट, तर पातलो पर्खालहरूमा भंगुर | पाना र स्पष्ट प्रोफाइलहरू |
| नायलन (PA) | मध्यम | लुजर; नमी-संवेदनशील | पोस्ट-एक्सट्रुजन नमी अपटेकको लागि खाता |
| HDPE / LDPE | मध्यम देखि कम | लुजर; उच्च संकुचन | पर्खाल र OD मा फराकिलो ब्यान्डहरू अपेक्षा गर्नुहोस् |
| Polypropylene | मध्यम | लुजर; अर्ध क्रिस्टलीय संकुचन | महत्वपूर्ण डिमहरूमा उदार सहिष्णुतालाई अनुमति दिनुहोस् |
| हेर्नुहोस | उच्च | टाइट, तर विशेष | उच्च-ताप इन्जिनियरिङ चल्छ; उच्च लागत |
| TPE / TPU | कम | सब भन्दा ढिलो; लचिलो रिकभरी | नरम प्रोफाइलहरू मापन अन्तर्गत विकृत हुन्छन् |
आयामिक स्थिरतालाई असर गर्ने कारकहरू
धेरै चरहरूले यसको सहिष्णुता ब्यान्ड भित्र वा बाहिर भाग सार्छन्. भित्ता मोटाई एकरूपता सबैभन्दा महत्त्वपूर्ण छ: एउटै प्रोफाइलमा बाक्लो र पातलो खण्डहरू विभिन्न दरहरूमा चिसो र ताना. Semi-crystalline resins like polypropylene and HDPE shrink more than amorphous ones like polycarbonate and acrylic, so the die must be cut to compensate. I also watch for haul-off speed, melt temperature, and cooling-bath control, since drift in any of these shows up as dimensional variation over a long run. For hygroscopic materials such as nylon, moisture absorbed after extrusion can change dimensions days later, which is why I ask how a supplier conditions and stores finished stock.
Specifying Tolerances in Your Drawings
The cleanest way to control cost is to tolerance only what functionally matters. I call out critical dimensions explicitly, apply a reasonable general tolerance block to everything else, and reference the datum features that mate with other components. Where a flexible TPE or TPU profile is involved, I specify the measurement method and fixture, because a soft part measures differently under light pressure than at rest. Being specific about which surfaces are cosmetic versus functional lets a plastic fabrication services partner set up the line intelligently instead of overbuilding to a blanket precision requirement.
Balancing Precision Against Cost
Tighter tolerances raise cost through slower line speeds, more scrap, added inspection, and sometimes secondary sizing or machining. व्यवहारमा, I treat precision as a dial rather than a switch: I hold the two or three dimensions that drive fit and function tightly and relax the rest. That approach keeps resin extrusion economical while still delivering parts that assemble correctly. When a design genuinely needs molding-level precision on every feature, that is a signal the part may not be a good extrusion candidate, and I revisit the process choice before committing to tooling.
Minimum Order Quantities and Lead Times
MOQs and lead times are where the difference between stock extruded shapes and true custom work becomes concrete. Custom extrusion typically requires a one-time tooling investment in a die, while stock profiles avoid that cost entirely, per common industry sourcing guidance. That single fact drives most of the ordering economics, so I plan around it from the start.
Typical MOQ Ranges for Stock vs Custom
Stock profiles and tubing can often be bought in small quantities, कहिले खुट्टा वा एकल बक्समा, किनभने आपूर्तिकर्ताले पहिले नै तिनीहरूलाई चलाउँछ. सीगेट प्लास्टिकले औंल्याए अनुसार, मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ।, भोल्युमहरू मामूली हुँदा एक व्यावहारिक लाभ हो (सीगेट प्लास्टिक, 2024). अनुकूलन प्रोफाइलहरू फरक छन्. किनकी लाईन मिलाउनुपर्छ, सफा गरियो, र राम्रो भागहरू आउन अघि स्थिर, आपूर्तिकर्ताहरूले त्यो सेटअपलाई परिशोधन गर्न न्यूनतम रन सेट गर्छन्. म सामान्यतया कस्टम MOQ हरू रालको पाउन्ड वा टुक्रा गणनाको सट्टा रैखिक फुटेजमा व्यक्त गरेको देख्छु, र थप विदेशी ईन्जिनियरिङ्-ग्रेड प्लास्टिकको साथ थ्रेसहोल्ड बढ्छ.
कसरी नेतृत्व समय उपकरण र भोल्युम संग भिन्न हुन्छ
नयाँ अनुकूलन प्रोफाइलको लागि, डाइ पेसिङ वस्तु हो. उपकरण डिजाइन, काट्ने, र पहिलो-लेख परीक्षणहरू सामान्यतया प्रारम्भिक तालिकामा हावी हुन्छन्, and I budget several weeks for die design and tooling before any production parts exist. Once the die is proven, repeat orders move quickly because the tooling is on the shelf. Higher volumes actually help here: extrusion is a continuous, high-volume process well suited to long production runs, so once a line is dialed in, adding footage is efficient rather than disruptive.
Quick-Turnaround Options and Expedited Runs
When a timeline is tight, I look at three levers. पहिले, use stock profiles or standard tubing that can ship from inventory and be cut or fabricated to length. दोस्रो, ask whether an existing die is close enough to modify rather than cutting a new one. तेस्रो, request an expedited slot, which many suppliers offer for a premium by prioritizing line time. Quick-turnaround production is realistic for standard shapes; for genuinely new custom geometry, the tooling step still sets the floor on how fast you can go.
Planning Your Project Timeline
I work backward from the required delivery date and add explicit buffers for die design, first-article approval, र कुनै पनि माध्यमिक कार्यहरू. Moving from prototype to production is smoother when I lock the profile cross-section early, because late geometry changes mean recutting the die and resetting the clock. Aligning MOQ with real annual demand also matters: ordering an efficient run size once beats paying repeated setup charges on small, frequent custom orders.
Cost Drivers in Plastic Extrusion Pricing
Understanding what actually drives a quote lets me negotiate from evidence rather than instinct. Extrusion pricing breaks down into a handful of levers, and knowing which one dominates for a given part tells me where the savings live.
Material Selection and Resin Pricing
Resin is usually the largest recurring cost, and it varies widely by grade. Commodity materials like PVC, polypropylene, HDPE, and LDPE sit at the low end; PVC in particular is among the most widely extruded plastics globally and is well supported across suppliers. Engineering-grade plastics such as polycarbonate, नायलन, and especially PEEK command higher prices and can require specialized processing. One efficiency I always ask about is regrind: एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स रिसाइकल गर्न सकिन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ, which can lower material cost on non-critical parts (अमेरिकी पर्यावरण संरक्षण एजेन्सी, 2023). Choosing the least expensive resin that meets the application requirement is the single highest-leverage decision in material selection.
उपकरण, सेटअप, and Run Volume
Custom work carries a one-time die cost that stock profiles avoid. That tooling charge is fixed, so it amortizes across the run: the more footage I order, the lower the per-part tooling burden. Setup time and line stabilization add cost to every job regardless of size, which is exactly why small custom orders feel expensive per piece. सह-निकासी, which combines two materials in one profile, adds tooling and process complexity and therefore cost, but it can eliminate secondary assembly, so I weigh the tradeoff on total value rather than tooling alone.
Secondary Operations and Finishing
Anything that happens after the profile leaves the die adds cost: cutting to length, ड्रिलिंग, नचिङ, मुद्रण, प्वाल मुक्का, tight-tolerance sizing, र प्याकेजिङ. Individually these are minor, but they stack quickly on high piece counts. I decide deliberately which operations belong in-line with the extrusion and which are genuinely needed, because each added step also adds handling and inspection. Where a feature can be designed into the profile cross-section instead of machined afterward, I do that, since forming a feature is nearly free compared with a downstream operation.
Domestic vs Offshore Cost Comparisons
Headline piece price often favors offshore, but I evaluate total landed cost. The Reshoring Initiative notes that domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023), and those factors are easy to underestimate when comparing unit prices alone. Working with a domestic plastics manufacturer also shortens lead times, simplifies communication, and reduces the inventory buffer I have to hold against long ocean transit. The US plastics industry is a substantial contributor to domestic manufacturing shipments and employment (प्लास्टिक उद्योग संघ, 2023), so the domestic supplier base for both stock and custom profiles is deep. मेरो औंठाको नियम: for high-volume, कम-मिक्स कमोडिटी प्रोफाइलहरू, offshore can win on price; for responsive, higher-mix, or engineering-grade work, domestic contract manufacturing usually wins on total cost and risk. For a fuller look at custom capabilities, I point buyers to custom plastic extrusion manufacturers such as SeaGate Plastics as a reference point for scope and services.
Questions to Ask Before Choosing a Factory
जब मैले प्लास्टिक प्रोफाइल निर्माताको जाँच गर्छु, I treat the first conversation as a structured interview rather than a sales call. The goal is to separate shops that can genuinely deliver my part from those that simply want the order. Over years of sourcing extruded plastic parts, I have found that a handful of pointed questions surface most of the risk before a single dollar changes hands. Below is the checklist I actually use.
क्षमता, प्रमाणपत्रहरू, and Material Expertise
I start by asking what the factory runs today, not what it claims it can run. Continuous extrusion is a high-volume manufacturing process, so I want to know line count, typical run lengths, and whether they have headroom for my volume without displacing existing customers. On the quality side, I ask directly about certification. ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो (मानकीकरणको लागि अन्तर्राष्ट्रिय संगठन, 2015), and while certification is not a guarantee of good parts, its absence tells me the shop may lack documented process controls.
Material expertise is the third leg. A capable resin extrusion supplier should speak fluently about the polymers relevant to my application, whether that is PVC and HDPE for construction profiles, ABS and polycarbonate for enclosures, polypropylene and LDPE for packaging and tubing, or engineering-grade plastics like nylon (PA) and PEEK for demanding environments. PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्राय: प्रोफाइलहरूमा प्रयोग गरिन्छ, पाइप, र ट्युबिङ (प्लास्टिक उद्योग संघ). If I need flexible sections, I confirm experience with TPE/TPU, and if my part demands a rigid core with a soft-touch or weather-resistant skin, I ask whether they offer co-extrusion. प्रयोगशाला एक्स्ट्रुडर थोक
Prototyping and Design Support Availability
I ask whether the factory offers design consultation before tooling is cut. The best plastic fabrication services partners will review my cross-section for extrudability, flag thin walls or sharp corners that trap stress, and suggest material substitutions that lower cost without hurting performance. I also confirm they can produce a representative prototype rather than pointing me straight to a production die.
लीड टाइम्स, MOQs, and Delivery Track Record
Here I get specific. I ask for standard lead times on both tooling and production, the minimum order quantity, and how MOQ scales with material and profile complexity. Custom extrusion typically requires a one-time tooling investment for the die, while stock extruded shapes avoid that cost entirely (उद्योग स्रोत निर्देशन). If my volumes are modest, मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024), so I always ask what stock profiles they carry. On delivery, I want on-time performance data, not adjectives.
References and Industry Experience
अन्तमा, I ask for references in my industry. A shop that regularly serves medical, मोटर वाहन, or building-products customers has already navigated the tolerances and documentation those sectors demand. I call the references and ask two questions: did the parts meet spec on the first production run, and how did the supplier handle the problem when something went wrong?
From Prototype to Production: How the Process Unfolds
Once I have chosen a supplier, the path from a drawing to shippable extruded plastic parts follows a predictable sequence. Understanding each stage helps me set realistic timelines internally and catch problems while they are still cheap to fix.
Submitting Drawings and Design Consultation
I begin by sending a dimensioned drawing of the profile cross-section, along with the target material, रंग, tolerance requirements, and end-use environment. This is where design-for-manufacturing consultation earns its keep. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs डिजाइन संसाधनहरू, 2023), a good engineer will help me place critical dimensions where the process can reliably hold them and relax the ones that do not matter.
Sample and Prototype Validation
Next comes a sample or prototype. Depending on the shop, this may be pulled from a soft or temporary die, or matched from existing stock extruded shapes. I use this stage to validate fit, लचिलोपन, सतह समाप्त, and material behavior in my actual assembly. Catching a wall-thickness issue on a prototype costs me a revision; catching it after the production die is cut costs me the tooling.
Tooling Approval and First-Article Inspection
Extruder Twin Screw After I approve the design, the factory cuts the production die. The die design and tooling step is the largest one-time cost in custom extrusion, so I review the tooling drawing carefully before signing off. Once the die runs, I require a first-article inspection: a documented measurement of the initial output against my drawing. I do not release full production until the first article passes.
Ramping to Full Production
With the first article approved, the line ramps to full production. Plastic extrusion is a continuous, high-volume process well suited to long production runs (SPI/Plastics Industry Association overview), so unit costs typically drop as volume climbs. I confirm the quality plan for ongoing runs, including sampling frequency and the criteria for holding or scrapping out-of-spec material. एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स पुन: प्रयोग गर्न मिल्ने हुन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ (अमेरिकी पर्यावरण संरक्षण एजेन्सी, 2023), so I also clarify the shop’s regrind policy when appearance or mechanical properties are critical.
Domestic vs Overseas Extrusion Sourcing
One of the most consequential decisions I make is where to source. The instinct is to compare unit price, but in my experience that number alone is misleading. What matters is total landed cost and the operational realities that price hides.
Cost vs Total Landed Cost Considerations
Overseas suppliers often quote a lower piece price, but I add freight, कर्तव्यहरू, customs handling, and the inventory carrying cost of larger safety stock and longer transit. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023). Once I build a full landed-cost model, the gap between a domestic plastics manufacturer and an overseas one usually narrows, and sometimes reverses.
नेतृत्व समय, ढुवानी, and Communication Factors
Domestic sourcing shortens my supply chain and simplifies communication across time zones and languages, which matters most when I need quick-turnaround production or fast design changes. Overseas sourcing can suit stable, high-volume programs where the design is frozen and lead time is not a constraint.
Quality Control and IP Protection
Proximity makes on-site audits and first-article reviews far easier, and domestic contracts generally offer stronger, more enforceable intellectual property protection for a proprietary die design. When my profile represents real design investment, that protection weighs heavily.
When Each Option Makes Sense
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (प्लास्टिक उद्योग संघ, 2023), and directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes local sourcing practical to research. The table below summarizes how I weigh the two paths.
| कारक | Domestic Sourcing | Overseas Sourcing |
|---|---|---|
| Unit price | Higher piece price | Often lower piece price |
| कुल जग्गा लागत | Lower freight, कर्तव्य, and carrying cost | Added freight, कर्तव्य, and inventory cost |
| नेतृत्व समय | छोटो, more responsive | लामो, transit-dependent |
| सञ्चार | Same time zone and language | Time-zone and language gaps |
| Quality audits | On-site visits practical | Remote or costly to audit |
| आईपी सुरक्षा | बलियो, more enforceable | Variable enforcement |
| उत्तम फिट | अनुकूलन प्रोफाइलहरू, fast changes, proprietary tooling | Frozen designs, very high volume, price-driven programs |
व्यवहारमा, I lean domestic for custom plastic profiles that involve proprietary tooling, evolving designs, or short lead times, and I consider overseas contract manufacturing only for mature, स्थिर, high-volume parts where the landed-cost math clearly favors it. For a starting point on capabilities and stock offerings, resources like सीगेट प्लास्टिक are a useful reference when scoping a domestic partner.
Sustainability and Recyclability in Extrusion
When I evaluate a plastic extrusion companies factory today, sustainability is no longer a soft preference tucked into the back of a proposal. It sits alongside price, नेतृत्व समय, and quality as a core selection criterion. The good news is that extrusion is inherently well suited to responsible material use, and the suppliers I trust have built that advantage into their operations rather than treating it as an afterthought.
Recyclable Thermoplastics and Scrap Reuse
Most of the polymers I specify for extruded plastic parts are thermoplastics, which means they can be remelted and reformed multiple times without a complete loss of properties. According to the US Environmental Protection Agency (2023), एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स रिसाइकल गर्न सकिन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ. That single characteristic separates them from thermosets and gives buyers real leverage on both cost and environmental footprint.
व्यवहारमा, this recyclability spans the common resins you will encounter across quotes. PVC, HDPE, LDPE, and Polypropylene are among the workhorses of profile extrusion and plastic tubing, and each reclaims well when handled correctly. Engineering-grade plastics such as ABS, पोली कार्बोनेट, नायलन (PA), र एक्रिलिक (PMMA) also tolerate controlled regrind, though I hold them to tighter blend ratios because their properties matter more in demanding applications. High-performance materials like PEEK and flexible TPE/TPU sit at the specialized end, where reuse requires more careful process control.
Regrind and Material Efficiency Practices
The continuous extrusion process generates predictable scrap: startup purge, trim from profile cross-section adjustments, and off-spec runs during die changeovers. A capable plastic profile manufacturer captures this material, granulates it into regrind, and reintroduces it at a defined percentage back into virgin resin. I always ask for the specifics because the details reveal how disciplined an operation really is.
- What regrind percentage do you blend into standard production, and does it change for cosmetic versus structural parts?
- How do you segregate resin types to prevent cross-contamination during resin extrusion?
- Can you document material traceability from raw resin through finished profile?
- Do you offer post-industrial recycled content options when my application allows it?
Co-extrusion deserves a mention here. By combining a virgin outer layer with a regrind or recycled core, some suppliers deliver the surface quality I need while lowering virgin material consumption. It is a practical way to reconcile appearance requirements with sustainability goals on the same part.
Choosing Environmentally Responsible Suppliers
मेरो अनुभवमा, a domestic plastics manufacturer often carries a sustainability advantage that has nothing to do with marketing. The Reshoring Initiative (2023) notes that domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत, and shorter supply chains also mean lower transport emissions. When I compare a nearby US factory against overseas alternatives, the environmental and logistical benefits frequently reinforce each other.
Beyond geography, I look for suppliers whose quality systems formalize waste reduction. ISO 9001, described by the International Organization for Standardization (2015) as the internationally recognized standard for quality management systems, does not mandate sustainability by itself, but shops that maintain it tend to run tighter processes with less scrap and better material accountability.
Regulatory and Buyer Sustainability Expectations
My downstream customers increasingly ask about recycled content, chemical compliance, and end-of-life recyclability before they will approve a part. That pressure flows straight back to how I write specifications. I now treat sustainability documentation as part of the deliverable, बोनस होइन. When a supplier can hand me material certifications, regrind policies, and recyclability data without hesitation, it signals a partner ready for where the market is heading rather than where it has been.
Making Your Final Decision and Requesting a Quote
Once I have shortlisted candidates, the decision comes down to matching each supplier’s real capabilities against my project’s non-negotiables. The extrusion market rewards specialization, so the goal is not finding the largest or most decorated factory but the one whose strengths line up with my part, my volumes, and my timeline.
Consolidating Your Evaluation Criteria
I bring my findings together into a single scorecard so I am comparing suppliers on the same terms. जस्ता दाबी गर्छन् “सबैभन्दा ठूलो” वा “सबै भन्दा राम्रो” mean little in isolation; a large plastic extrusion companies factory tuned for high-volume commodity profiles may be the wrong fit for a low-volume, tight-tolerance engineering part, र उल्टो. The table below shows the weighting I typically apply, though I adjust it to the priorities of each program.
| Evaluation Criterion | What I Look For | Typical Weight |
|---|---|---|
| Material capability | Experience with my resin (PVC, HDPE, पोली कार्बोनेट, आदि) and co-extrusion if needed | उच्च |
| Tooling and die design | In-house die design, tooling lead time, revision support | उच्च |
| गुणस्तर प्रणाली | ISO 9001 certification and documented process controls | उच्च |
| Volume fit | Alignment of MOQ and capacity with my annual demand | मध्यम |
| नेतृत्व समय | Realistic tooling plus production schedule, quick-turnaround options | मध्यम |
| स्थान | Domestic sourcing benefits, भाडा, and responsiveness | मध्यम |
| दिगोपन | Regrind practices, पुनर्नवीनीकरण सामग्री, सामग्री ट्रेसबिलिटी | Rising |
Preparing a Clear RFQ Package
The quality of the quotes I receive is directly proportional to the quality of the request I send. A vague inquiry produces padded, cautious pricing; a complete RFQ produces sharp, comparable numbers. Extrusion carries specific cost drivers a supplier needs to see up front, chiefly the one-time tooling investment for custom profiles, which industry sourcing guidance confirms is avoided only when you use stock extruded shapes.
What Information to Include for Accurate Quotes
I make sure every RFQ package answers the questions a plastic fabrication services provider will otherwise have to ask, because each back-and-forth adds days to the timeline.
- A dimensioned drawing of the profile cross-section with tolerances. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming, per Protolabs (2023), I flag which dimensions are critical and which can float.
- Material specification, including resin type, grade, रंग, and any UV, flame, or food-contact requirements.
- Annual volume and order frequency, plus expected part length and cut tolerances.
- Whether I need custom tooling or can use a stock profile, and whether secondary operations such as cutting, मुक्का मार्दै, or printing apply.
- Target price, required delivery date, and destination for landed-cost accuracy.
- Application and industry context, which helps the supplier recommend the right material and process.
Next Steps to Start Your Project
With the scorecard filled in and the RFQ ready, I send it to two or three well-matched suppliers rather than blasting a dozen. I ask for a sample or first-article inspection before committing to full production, and I confirm the tooling ownership terms in writing. Moving from prototype to production this deliberately has consistently saved me from costly surprises. Directories such as Thomasnet (2024), which list and categorize US plastic extrusion manufacturers by capability and region, remain a useful starting point when I need to widen the field, and specialist custom extruders like सीगेट प्लास्टिक illustrate how stock profiles and tubes can be fabricated into cost-effective custom parts.
बारम्बार सोधिने प्रश्नहरू
These are the questions buyers ask me most often when they are sourcing an extrusion partner. I have kept the answers concise and practical so you can act on them quickly.
How do I find a plastic extrusion companies factory near me or in the USA?
Start with capability, then filter by geography. I search supplier directories such as Thomasnet (2024) that categorize US plastic extrusion manufacturers by region and process, then cross-check each candidate’s material and volume fit. Choosing a domestic plastics manufacturer often pays off beyond convenience: the Reshoring Initiative (2023) reports that domestic sourcing can lower freight, कर्तव्य, र सूची बोक्ने लागत, reducing total landed cost.
कस्टम प्लास्टिक एक्सट्रुसन लागत कति हुन्छ?
There are two cost layers. Custom profiles require a one-time tooling and die investment, after which per-part pricing depends on resin, पर्खाल मोटाई, output rate, र भोल्युम. Stock extruded shapes skip the tooling charge entirely, which is why I default to them when a standard profile meets the requirement. किनभने निकासी निरन्तर छ, उच्च मात्रा प्रक्रिया, unit costs typically fall as run length increases.
What is the difference between custom and stock extruded profiles?
Stock profiles are standard cross-sections a plastic profile manufacturer already produces, so they carry no tooling cost and short lead times, though the shape is fixed. Custom extrusion gives me a die designed to my exact profile cross-section, which is worth the tooling investment when the geometry, प्रकार्य, or branding demands it. सीगेट प्लास्टिक (2024) also notes that standard profiles and tubes can be fabricated into cost-effective custom parts, a useful middle path when a full custom die is not justified.
How do I choose the right material for my extruded part?
I match the resin to the application. PVC is among the most widely extruded plastics for profiles, पाइप, र ट्युबिङ. HDPE, LDPE, and Polypropylene serve well in chemical-resistant and flexible applications. When I need clarity, प्रभाव शक्ति, or heat resistance, I move to engineering-grade plastics such as Polycarbonate, ABS, एक्रिलिक (PMMA), or Nylon (PA), and I reserve PEEK for extreme thermal and mechanical demands. Sharing your application and environment with the supplier is the fastest route to the right recommendation.
What certifications should a quality extrusion supplier hold?
ISO 9001 is my baseline. The International Organization for Standardization (2015) describes it as the internationally recognized standard for quality management systems used across manufacturing, and it is the most widely adopted quality standard in the plastics sector. Depending on your industry, you may also require food-contact, चिकित्सा, or flame-rating compliance, so confirm those specifics against your application.
What mistakes should I avoid when sourcing an extrusion partner?
The most common ones I see are chasing “सबैभन्दा ठूलो” वा “सबै भन्दा राम्रो” claims without checking fit, sending incomplete drawings that produce inflated quotes, and underestimating tooling lead time. I also caution against ignoring MOQ alignment; a factory built for high-volume manufacturing may not welcome low-volume work, and a small shop may struggle with your scale. Match the supplier to the job rather than the reputation.
What are the next steps once I have chosen a supplier?
Send a complete RFQ, request a sample or first-article inspection, confirm tooling ownership in writing, and agree on a realistic schedule that separates tooling time from production time. Validating the part before full production is the single most reliable way I have found to move from prototype to production without expensive rework.
What Is a Plastic Extrusion Companies Factory and Why It Matters for B2B Buyers
When I evaluate a plastic extrusion companies factory for a client, म प्रक्रिया आफैबाट सुरु गर्छु, because the process defines what a supplier can and cannot do for you. प्लास्टिक एक्सट्रुजनले कच्चा प्लास्टिक सामग्री पग्लन्छ र यसलाई स्थिर क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ। (सीगेट प्लास्टिक, 2024). That single sentence carries more purchasing implications than most buyers realize: द “निश्चित क्रस-सेक्शन” is why extrusion excels at long, uniform shapes like tubing, ट्रिम, र च्यानलहरू, and it is also why you cannot expect the same complex three-dimensional geometry you would get from molding.
परिभाषा: तपाई वास्तवमा के किन्दै हुनुहुन्छ
In practical terms, a plastic extrusion factory pushes softened resin through a shaped die to produce items such as custom plastic profiles, प्लास्टिक ट्युबिङ, and plastic sheet. Because this is a continuous extrusion process, it runs well for high-volume manufacturing and long production runs rather than one-off complex parts. The two categories I ask buyers to distinguish early एक्सट्रुजन प्लास्टिक निर्माण आपूर्तिकर्ता are stock extruded shapes, which are ready-made and avoid tooling, and custom extruded plastic parts, which require a die designed to your cross-section. Standard extruded profiles and tubes can also be fabricated into cost-effective custom parts with quick-turnaround production (सीगेट प्लास्टिक, 2024), which is a useful middle path when a full custom die is not justified.
बजार सन्दर्भ
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (प्लास्टिक उद्योग संघ, 2023), so you are not sourcing from a niche trade. That scale matters for buyers: it means real competition among suppliers, redundancy if one plastic profile manufacturer cannot meet lead time, and a mature base of contract manufacturing and plastic fabrication services. It also means claims of being the “सबैभन्दा ठूलो” वा “सबै भन्दा राम्रो” factory are marketing shorthand, not verified rankings. I treat those labels as prompts to ask about actual line capacity, प्रमाणपत्रहरू, and reference customers rather than as evidence.
Key Applications and Materials
Material selection drives most of the outcome, so I map the resin to the application before shortlisting any supplier. Common choices I see across projects include:
- PVC — among the most widely extruded plastics globally, प्रोफाइलहरूमा सामान्य, पाइप, र ट्युबिङ (प्लास्टिक उद्योग संघ).
- HDPE and LDPE — durable, chemically resistant polyethylenes used for tubing, लाइनरहरू, and industrial profiles.
- Polypropylene — lightweight and fatigue-resistant, frequently chosen for living hinges and chemical handling.
- ABS र Polycarbonate — impact-resistant options for structural trim and enclosures; polycarbonate adds optical clarity and heat resistance.
- एक्रिलिक (PMMA) — clarity and weatherability for lenses, प्रदर्शन गर्दछ, and lighting profiles.
- नायलन (PA) र PEEK — engineering-grade plastics for wear, तापमान, and mechanical demands; PEEK is the high-performance choice for aerospace and medical.
- TPE/TPU — flexible elastomers for seals, गास्केटहरू, and grips, often produced through co-extrusion with a rigid substrate.
Co-extrusion deserves special attention because it lets a factory combine two materials in one profile, for example a rigid PVC body with a soft TPE sealing lip. If your part needs both stiffness and flexibility, confirm the supplier runs true co-extrusion rather than secondary assembly.
Why This Matters for B2B Buyers
Understanding the process changes how you write a request for quote. सामग्री संकुचन र निरन्तर गठनको कारण बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ। (प्रोटोल्याबहरू, 2023), so specifying injection-molding-tight tolerances on an extruded profile will either inflate your price or trigger a round of clarifying questions that delays the quote. On sustainability, एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स रिसाइकल गर्न सकिन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ (US EPA, 2023), which gives you a legitimate lever for both cost and environmental goals when you discuss regrind percentages with a supplier.
How to Choose the Right Plastic Extrusion Companies Factory Supplier
Choosing a supplier is where I see the most avoidable mistakes, usually because buyers compare on unit price alone and ignore the cost drivers hiding behind that number. Below is the framework I use, built around evaluation criteria, red flags, and a due diligence checklist you can lift directly into your sourcing process.
विक्रेता मूल्याङ्कन मापदण्ड
I score candidates against five dimensions rather than a single quote:
- Capability match. Does the factory routinely run your resin and profile size? A plastic tubing supplier optimized for small-diameter medical tubing is not the same shop as one running large architectural profile extrusion.
- Quality systems. ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो (ISO, 2015) and remains the most widely adopted quality standard in the plastics sector. Certification is not a guarantee of good parts, but its absence tells me to dig deeper into inspection practices.
- Tooling and die design. Ask who owns the die, how long die design and tooling take, and what happens to the tool if you leave. Ownership terms are frequently buried in fine print.
- Lead time and capacity. Confirm whether quoted lead times reflect current backlog or ideal conditions. Quick-turnaround production claims should be tied to a specific committed date.
- Financial and operational stability. A supplier that becomes your sole source for a critical profile is a risk if it is financially fragile.
Understanding the Cost Drivers
Transparency on cost structure separates a strong plastic profile manufacturer from an opaque one. Three drivers determine your total price, and I ask suppliers to break them out explicitly:
| लागत चालक | Stock extruded shapes | Custom extruded profiles |
|---|---|---|
| उपकरण / die investment | None — profile already exists | One-time die cost required before first run (उद्योग स्रोत निर्देशन, Thomasnet supplier guides) |
| न्यूनतम अर्डर मात्रा (MOQ) | कम; buy by the length | उच्च; tied to setup and material changeover |
| नेतृत्व समय | Short — often shelf stock | लामो; includes die fabrication and first-article approval |
| Per-unit price at volume | Fixed by catalog | Lower at high volume once tooling is amortized |
| उत्तम फिट | प्रोटोटाइपिङ, कम मात्रा, standard cross-sections | Proprietary geometry, high-volume manufacturing, prototype to production scale-up |
Custom extrusion typically requires a one-time tooling investment, जबकि स्टक प्रोफाइल यो लागत जोगिन (उद्योग स्रोत निर्देशन). मेरो अनुभवमा, buyers who plan to scale from prototype to production should quote the custom die early even if they start with stock shapes, so the amortized per-unit price is visible before volumes ramp.
Red Flags I Watch For
- Refusal to share ISO or equivalent quality documentation, or vague answers about inspection frequency.
- Quotes with no tooling line item, which usually means the cost reappears later or the die is undersized.
- Unwillingness to provide references in your industry or sample parts.
- Tolerances promised on paper that are tighter than what continuous extrusion realistically holds — a sign the supplier may be overselling.
- “Largest” वा “सबै भन्दा राम्रो” claims with no capacity data, प्रमाणपत्रहरू, or customer evidence behind them.
उचित परिश्रम चेकलिस्ट
Before I commit to a Plastic Extrusion Companies Factory supplier, I confirm every item below in writing:
- Do you hold ISO 9001 or an equivalent, and can I see the certificate and scope?
- Which resins do you run in production, and can you handle my material — PVC, ABS, polycarbonate, HDPE, LDPE, polypropylene, or an engineering grade?
- What tolerances do you guarantee for this profile cross-section, and how are they measured?
- What is the tooling cost, नेतृत्व समय, and MOQ, and who owns the die?
- Do you offer co-extrusion and secondary fabrication in-house?
- What percentage of regrind is used, and how does that affect certification and appearance?
- Can you provide first-article inspection reports and material certifications?
- What is your realistic committed lead time given current backlog?
Find Plastic Extrusion Companies and Factories in the United States
Buyers frequently search for a plastic extrusion factory “मेरो नजिक” वा “in the USA,” and the location question is more strategic than it first appears. Domestic sourcing is not only about proximity; it changes your total landed cost and your supply-chain risk profile.
Where to Start Your Search
Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a practical first filter when you want to build a shortlist by material, प्रक्रिया, or state. I pair directory research with capability-specific sources such as custom plastic extrusion manufacturer references to understand what a given shop actually produces before I reach out. The goal at this stage is a shortlist of five to eight candidates whose capabilities genuinely match your resin and profile, not a long list of names. प्लास्टिक एक्सट्रुजन कम्पनीहरू
Key Considerations for Domestic Sourcing
Reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023). For extruded parts, which are often bulky and low in value density, freight is a meaningful line item, so a domestic plastics manufacturer closer to your assembly point can offset a higher unit price. I weigh three factors:
- कुल जग्गा लागत, एकाइ मूल्य होइन. Add freight, कर्तव्य, and the carrying cost of the safety stock you need to cover long overseas transit.
- Communication and design iteration. Domestic time-zone alignment speeds up die design and tooling revisions during the prototype-to-production phase.
- Supply resilience. Shorter lines reduce exposure to port delays and long lead-time shocks.
Interpreting “Largest” र “Best” Factory Claims
Location searches often surface superlatives, and I treat them skeptically. “Largest” tells you nothing about whether a factory runs your material or holds your tolerances. बरु, I convert vague claims into verifiable questions: How many extrusion lines run my resin family? What is your on-time delivery rate? Which certifications do you hold? A smaller shop that specializes in your profile is frequently a better partner than a large one for which your job is an afterthought.
Practical Tips and Industry Context
A few habits have consistently saved my clients time and money. पहिले, request stock extruded shapes for early validation before investing in a custom die — it lets you test fit and function cheaply. दोस्रो, share a dimensioned drawing with realistic extrusion tolerances up front so quotes are comparable. तेस्रो, confirm the supplier’s regrind policy, since recyclable thermoplastics and regrind reuse improve material efficiency (US EPA, 2023) but can affect appearance on cosmetic parts. अन्तमा, remember that plastic extrusion is a continuous, high-volume process well suited to long production runs, so it rewards buyers who can consolidate demand and forecast accurately. Within the mature US plastics manufacturing base (प्लास्टिक उद्योग संघ, 2023), you have room to be selective — use it, and let a structured checklist rather than a headline claim decide your Plastic Extrusion Companies Factory supplier.
Locate a plastic extrusion factory near my location
When buyers ask me how to find a plastic extrusion factory nearby, I remind them that “मेरो नजिक” is really shorthand for two goals: shorter freight lanes and easier communication. Extrusion melts raw plastic material and forms it into a continuous profile with a fixed cross-section (सीगेट प्लास्टिक, 2024), and because that continuous extrusion process runs at high volume, the finished product is often bulky and freight-sensitive. मेरो अनुभवमा, the cost of moving extruded plastic parts across the country can quietly erode the price advantage of a distant supplier, so location genuinely matters.
Key considerations for local sourcing
I start every local search by matching capability to geography rather than proximity alone. A plastic profile manufacturer two states away with the right die design and tooling almost always beats a closer shop that cannot hold your profile cross-section. I evaluate three things in order: the materials they run (PVC, ABS, polycarbonate, HDPE, LDPE, polypropylene, एक्रिलिक, and engineering-grade resins such as nylon or PEEK), the processes they offer (प्रोफाइल निकासी, प्लास्टिक पाना निकासी, ट्युबिङ, र सह-निकास), and their quality systems. ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो (ISO, 2015), so I treat certification as a baseline filter, बोनस होइन.
Practical tips to find and vet a factory
Thomasnet supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a reliable starting point for a location-based shortlist. त्यहाँबाट, I qualify each candidate with a consistent set of questions before I ever request a quote.
My local supplier vetting checklist
- Which resins do you extrude in-house, and can you run regrind for material efficiency?
- Do you offer co-extrusion or dual-durometer profiles if my part needs a soft-touch or barrier layer?
- What tolerances can you hold, and how do you document them?
- तपाईं ISO हुनुहुन्छ 9001 प्रमाणित, and can you share a recent audit summary?
- What is your typical lead time from approved die to first article?
- Do you provide plastic fabrication services (काट्ने, मुक्का मार्दै, ड्रिलिंग) so I receive finished parts, not just stock lengths?
उद्योग सन्दर्भ
Domestic proximity is more strategic than it looks. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023). Because the US plastics industry is a major contributor to domestic manufacturing shipments and employment (प्लास्टिक उद्योग संघ, 2023), most regions have a viable domestic plastics manufacturer within a reasonable freight radius. I tell buyers that “मेरो नजिक” should mean near enough to control landed cost and lead time, which is often a regional rather than a strictly local decision.
Identify the largest plastic extrusion companies in the US
Buyers frequently ask me to point them to the “सबैभन्दा ठूलो” प्लास्टिक निकासी कम्पनीहरु, and my first move is always to define what “सबैभन्दा ठूलो” means for their project. Size can describe revenue, plant footprint, number of extrusion lines, or annual resin throughput, and those metrics do not always move together. A plastic extrusion companies factory supplier with enormous pipe capacity may be the wrong fit for a low-volume acrylic profile, so I interpret scale through the lens of the specific job.
Key considerations when “सबैभन्दा ठूलो” मामिलाहरू
Scale earns its keep on long production runs. Plastic extrusion is a continuous, high-volume process well suited to long production runs, so the largest producers shine when you need millions of feet of PVC profile or HDPE pipe on a predictable schedule. PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्राय: प्रोफाइलहरूमा प्रयोग गरिन्छ, पाइप, र ट्युबिङ, which is why the biggest players tend to concentrate capacity there. If your program is high-volume and standardized, a large plastic profile manufacturer offers redundancy, buffer inventory, and pricing leverage. If your program is small or highly custom, that same scale can translate into higher minimums and less flexibility.
Practical tips for evaluating scale claims
I never take a marketing claim of “सबैभन्दा ठूलो” at face value. बरु, I ask for concrete indicators: number of extrusion lines by size class, resins run at volume, and the split between stock extruded shapes and custom work. A large firm quoting a wholesale program should be able to show quick-turnaround production capacity, secondary plastic fabrication services, and a documented MOQ structure. The table below summarizes how I weigh large versus specialized suppliers.
Large versus specialized extrusion suppliers
| कारक | Largest producers | Specialized suppliers |
|---|---|---|
| उत्तम फिट | उच्च मात्रा, standardized runs (पाइप, PVC profile) | Custom plastic profiles, engineering-grade resins |
| न्यूनतम अर्डर मात्रा | Higher MOQ to justify line time | Lower MOQ, more flexible |
| उपकरण लागत | Amortized across large volumes | One-time die cost more visible per unit |
| नेतृत्व समय | Predictable, buffered by capacity | चर, project-dependent |
| सामग्री दायरा | Commodity resins (PVC, HDPE, LDPE, PP) | Specialty resins (पीसी, PMMA, PA, हेर्नुहोस, TPE/TPU) |
| सह-निकासी | Common on standard lines | Often available for niche multi-layer parts |
उद्योग सन्दर्भ
The largest US extruders are anchored in commodity, freight-heavy products where continuous, high-volume manufacturing rewards efficiency. Custom extrusion typically requires a one-time tooling or die investment, जबकि स्टक प्रोफाइल यो लागत जोगिन, so large producers often lead with catalogs of stock extruded shapes. I remind buyers that “सबैभन्दा ठूलो” is a useful signal for reliability and capacity, but it is not a proxy for quality or fit. The right size is the one that matches your volume, सामग्री, and tolerance needs.
Discover the best-rated plastic extrusion manufacturers
“Best-rated” is the claim I scrutinize most, because ratings can reflect genuine performance or simply strong marketing. मेरो अनुभवमा, the manufacturers worth shortlisting are the ones that make their quality measurable. I look past star counts and testimonials for evidence I can verify: प्रमाणपत्रहरू, documented tolerances, सामग्री ट्रेसबिलिटी, and a track record of moving projects from prototype to production without surprises.
Key considerations for judging quality
Quality management is the foundation. ISO 9001 is the most widely adopted quality management standard, used across manufacturing sectors including plastics, so I treat it as table stakes for a best-rated plastic extrusion companies factory manufacturer. Beyond certification, I assess how a supplier handles tolerances. सामग्री संकुचन र निरन्तर गठनको कारण बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ। (प्रोटोल्याबहरू, 2023), and the best manufacturers explain that reality up front rather than overpromising. A shop that gives me realistic tolerance ranges and a clear inspection plan earns more trust than one quoting numbers it cannot hold.
Practical tips for choosing the best-rated supplier
I use a material selection framework tied to the application. The resin drives the manufacturer, वरपर अर्को तरिका होइन.
- PVC — profiles, पाइप, and tubing where cost and rigidity matter.
- ABS and polycarbonate — impact-resistant parts; polycarbonate adds clarity and heat tolerance.
- HDPE and LDPE — chemical resistance and flexibility for tubing and liners.
- Polypropylene — lightweight parts needing fatigue and chemical resistance.
- एक्रिलिक (PMMA) — optical clarity for lighting and display profiles.
- नायलन (PA) र PEEK — engineering-grade parts under mechanical or thermal stress.
- TPE/TPU — flexible seals and gaskets, often via co-extrusion.
Once the material is set, I confirm the supplier offers the matching process, whether that is profile extrusion, प्लास्टिक पाना निकासी, or resin extrusion with co-extrusion for multi-layer parts. मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024), so I favor manufacturers that pair extrusion with in-house fabrication and prototype-to-production support. For a working example of custom capability and stock profile options, म क्रेताहरूलाई सन्दर्भहरूमा संकेत गर्छु जस्तै सीगेट प्लास्टिक.
उद्योग सन्दर्भ
उत्कृष्ट मूल्याङ्कन गर्ने निर्माताहरूले गुणस्तरसँगै स्थिरतामा पनि प्रतिस्पर्धा गर्छन्. एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स पुन: प्रयोग गर्न मिल्ने हुन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ (US EPA, 2023), त्यसैले म शीर्ष उम्मेद्वारहरूलाई सोध्छु कि उनीहरूले कसरी स्क्र्याप र रिग्राइन्ड व्यवस्थापन गर्छन्. एक निर्माता जसले यसको गुणस्तर प्रणाली दस्तावेज गर्दछ, इमानदार सहिष्णुता राज्य गर्दछ, र एक कुशल सामग्री लूप चलाउँछ “सबै भन्दा राम्रो मूल्याङ्कन” बिरुवाको भ्रमण अन्तर्गत राख्ने कारणहरूका लागि. त्यो मैले लागू गरेको मानक हो, र यो एक हो जुन मैले प्रत्येक खरिदकर्तालाई एक सम्झौता निर्माण साझेदारलाई प्रतिबद्ध गर्नु अघि प्रयोग गर्न सिफारिस गर्दछु.
बुझ्नुहोस् कसरी प्लास्टिक बाहिर निकाल्ने निर्माण प्रक्रिया काम गर्दछ
जब म प्लास्टिक प्रोफाइल निर्माताको मूल्याङ्कन गर्छु, म पसल फ्लोरमा वास्तवमा के हुन्छ भनेर खरिदकर्ताले बुझेको कुरा सुनिश्चित गरेर सुरु गर्छु. प्लास्टिक एक्सट्रुजनले कच्चा प्लास्टिक सामग्री पग्लन्छ र यसलाई स्थिर क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ। (सीगेट प्लास्टिक, 2024). त्यो एकल वाक्यले तपाईलाई जान्न आवश्यक पर्ने धेरै कुराहरू बोक्छ: प्रक्रिया निरन्तर छ, क्रस-सेक्शन लम्बाइ संग स्थिर छ, र आकार बन्द ढाँचा द्वारा सट्टा उपकरण द्वारा परिभाषित गरिएको छ.
निरन्तर बाहिर निकाल्ने प्रक्रियाको मुख्य चरणहरू
व्यवहारमा, म कार्यप्रवाहलाई पाँच चरणमा वर्णन गर्छु. पहिले, राल छर्राहरू हपरमा खुवाइन्छ. दोस्रो, घुमाउने स्क्रूको साथ तातो ब्यारेल पग्लन्छ र सामग्रीलाई दबाब दिन्छ, यही कारणले गर्दा चिकित्सकहरूले यसलाई राल एक्सट्रुसन भन्छन्. तेस्रो, पग्लिएको पोलिमरलाई डाइ मार्फत बाध्य पारिन्छ जसले प्रोफाइल क्रस-सेक्शन स्थापना गर्दछ. चौथो, एक्स्ट्रुडेटलाई पानीको नुहाउने वा एयर र्याकमा चिसो गरिन्छ त्यसैले यसले यसको ज्यामिति राख्छ. पाँचौं, पुलरहरूले आरा वा कटरले यसलाई आकार दिनु अघि स्थिर दरमा भाग कोर्छन्. किनभने चरणहरू बीच केहि पनि रोकिदैन, यो विधि साँच्चै एक चक्र-द्वारा-साइकलको सट्टा निरन्तर बाहिर निकाल्ने प्रक्रिया हो.
किन सहिष्णुता इंजेक्शन मोल्डिंग बाट फरक छ
एउटा बिन्दु म ईन्जिनियरिङ् टोलीहरूसँग चाँडै उठाउँछु: सामग्री संकुचन र निरन्तर गठनको कारणले गर्दा बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ (Protolabs डिजाइन संसाधनहरू, 2023). यो कुनै दोष होइन. यसले खुला टुलिङ मार्फत तातो पोलिमर तान्ने र तनावमा चिसो पार्ने भौतिक विज्ञानलाई प्रतिबिम्बित गर्दछ. यदि तपाइँको extruded प्लास्टिक भागहरु एक विशेष सुविधा मा कडा आयामी नियन्त्रण आवश्यक छ भने, माध्यमिक मेशिनिङको लागि योजना बनाउनुहोस् वा त्यो सुविधालाई डाइले एक्लै समात्ने अपेक्षा गर्नुको सट्टा बनावटी चरणको रूपमा निर्दिष्ट गर्नुहोस्।.
को-एक्सट्रुजन र प्रोफाइल एक्सट्रुजन संस्करणहरू
प्रोफाइल एक्सट्रुजनले धेरै जसो खरीददारहरूले चित्रलाई अनुकूलन क्रस-सेक्शनहरू कभर गर्दछ: च्यानलहरू, गास्केटहरू, ट्रिमहरू, र संरचनात्मक आकारहरू. को-एक्सट्रुजनले एकैचोटि डाइ मार्फत दुई वा बढी सामग्रीहरू चलाउँछ, जसले तपाईंलाई संयोजन गर्न दिन्छ, उदाहरण को लागी, एकल पासमा लचिलो TPE/TPU सील ओठको साथ कठोर PVC बडी. मलाई सह-एक्सट्रुसन त्यो हो जहाँ सक्षम कारखानाले यसको दर कमाउँछ, किनभने यसले डाउनस्ट्रीम असेंबली चरण हटाउँछ र सील प्रदर्शन सुधार गर्दछ. प्लास्टिक पाना एक्सट्रुसन र ट्युबिङले विभिन्न डाइ र डाउनस्ट्रीम सेटअपहरूसँग समान आधारभूतहरू प्रयोग गर्दछ।.
उद्योग सन्दर्भ र सामग्री दक्षता
एक्सट्रुजन उच्च-भोल्युम निर्माणको लागि उपयुक्त छ किनभने यो स्वाभाविक रूपमा निरन्तर हो, high-volume process well suited to long production runs. एक पटक डायल इन गरेपछि, रेखा गति र रन टाइमको साथ आउटपुट स्केल. यसको पनि एक उचित स्थिरता कथा छ: एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स रिसाइकल गर्न सकिन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ (US EPA, 2023). मेरो अनुभवमा, एक आपूर्तिकर्तालाई सोध्दा उनीहरूले कसरी रिग्राइन्ड ह्यान्डल गर्छन् तपाइँलाई उनीहरूको लागत अनुशासन र उनीहरूको प्रक्रिया नियन्त्रणको बारेमा धेरै कुरा बताउँछ.
कस्टम बनाम स्टक प्लास्टिक एक्सट्रुजन आपूर्तिकर्ताहरू तुलना गर्नुहोस्
The most consequential sourcing decision I help buyers make is custom versus stock. It drives your tooling cost, न्यूनतम आदेश मात्रा, and lead time all at once. The right answer depends on how closely a standard shape fits your application and how much volume you expect to run.
What separates the two paths
कस्टम एक्सट्रुसनलाई सामान्यतया एक पटकको टूलिङ र डाइ लगानी चाहिन्छ, जबकि स्टक प्रोफाइल यो लागत जोगिन. मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024). So there is a middle path many buyers miss: start from a stock extruded shape and fabricate it, capturing part of the customization benefit without paying for a new die.
Cost drivers to model before you request a quote
When I build a sourcing model, I separate three drivers so the numbers stay honest:
- Die design and tooling: a one-time cost on custom work, typically amortized across your first order or two.
- MOQ: custom lines carry higher minimums to justify setup and purge material; stock shapes can ship in small quantities.
- नेतृत्व समय: stock ships quickly; custom adds die fabrication and first-article approval before production begins.
तुलना तालिका: custom vs stock extrusion
| कारक | अनुकूलन प्रोफाइल एक्सट्रुसन | Stock extruded shapes |
|---|---|---|
| उपकरण लागत | One-time die investment required | कुनै पनि छैन |
| न्यूनतम अर्डर मात्रा | उच्च, to amortize setup | कम, often cut-to-length |
| नेतृत्व समय | लामो (मर्ने निर्माण + पहिलो लेख) | Quick-turnaround production |
| Dimensional fit | Exact cross-section to spec | Nearest standard, plus fabrication |
| लागि उत्तम | Sustained volume, unique geometry | प्रोटोटाइपहरू, कम मात्रा, near-fit needs |
| Unit price at scale | एकपटक टुलिङलाई परिशोधन गरिएपछि तल्लो | Higher per unit for heavy customization |
A vetting checklist for either path
Whether you pursue a custom plastic profile manufacturer or a stock plastic tubing supplier, I ask the same core questions. Is the shop certified to ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015)? ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics, so its absence is worth a direct conversation. Beyond certification, I ask:
- Which resins do you run in-house, and can you handle engineering-grade plastics like polycarbonate, नायलन (PA), वा PEEK?
- Do you offer co-extrusion and downstream plastic fabrication services?
- How do you document tolerances and first-article inspection?
- What is your true MOQ, and how is tooling amortized on the initial order?
- Can you support the move from prototype to production without re-tooling?
Location intent: near me and in the USA
Buyers frequently search for a Plastic Extrusion Companies Factory supplier “मेरो नजिक” or a domestic plastics manufacturer in the USA. Two resources help here. Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is a practical starting point for shortlisting. And the case for domestic sourcing is more than convenience: reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023). I treat “सबैभन्दा ठूलो” र “सबै भन्दा राम्रो” factory claims with skepticism; capability fit for your specific resin, सहिष्णुता, and volume matters far more than a superlative on a homepage.
Learn what products can be made through plastic extrusion
Extrusion produces a broader range of products than most buyers expect, and the material you choose shapes both what is possible and what it costs. I organize my recommendations around a material selection framework tied to application and industry rather than a generic parts list.
Common extruded product categories
The workhorse outputs are custom plastic profiles, ट्युबिङ, पाना, च्यानलहरू, ट्रिमहरू, गास्केटहरू, र संरचनात्मक आकारहरू. Anything with a consistent profile cross-section along its length is a candidate. PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्राय: प्रोफाइलहरूमा प्रयोग गरिन्छ, पाइप, र ट्युबिङ (प्लास्टिक उद्योग संघ). That prevalence is why so many stock extruded shapes are available in PVC first.
Material selection framework
Here is how I match resins to needs across the polymers you will encounter most often:
- PVC: आर्थिक, rigid or flexible, strong for profiles, पाइप, र ट्युबिङ.
- ABS: कडा र प्रभाव प्रतिरोधी, आवास र ट्रिमहरूमा सामान्य.
- पोली कार्बोनेट: ग्लेजिङ्ग र गार्डहरूको लागि उच्च प्रभाव शक्ति र स्पष्टता.
- HDPE and LDPE: ट्यूबिंग को लागी रासायनिक प्रतिरोधी polyolefins, लाइनरहरू, र कम लागत प्रोफाइलहरू; HDPE थप कठोरता ल्याउँछ, LDPE थप लचिलोपन.
- Polypropylene: प्रकाश, रासायनिक प्रतिरोधी, र जीवित टिका र प्रोफाइलहरूको लागि थकान-सहनशील.
- एक्रिलिक (PMMA): प्रदर्शन र प्रकाश प्रोफाइल लागि अप्टिकल स्पष्टता.
- नायलन (PA): मेकानिकल भागहरूको लागि प्रतिरोध र बल लगाउने.
- हेर्नुहोस: उच्च तापमान, एयरोस्पेस र चिकित्सा कार्यको मागको लागि रासायनिक रूपमा बलियो ईन्जिनियरिङ्-ग्रेड प्लास्टिक.
- TPE/TPU: लचिलो इलास्टोमरहरू सिलहरू र नरम-टच सह-निकासी ओठहरूको लागि आदर्श.
उद्योग अनुप्रयोगहरू
निर्माण विन्डो फ्रेमहरूको लागि PVC र ABS प्रोफाइलहरूमा निर्भर गर्दछ, ट्रिमहरू, र किनारा. चिकित्सा र प्रयोगशाला कार्य एक्रिलिक प्रयोग गर्दछ, polypropylene, र PEEK ट्युबिङ र च्यानलहरू. इलेक्ट्रोनिक्स र उपकरणहरू पॉली कार्बोनेट र ABS आवासहरूमा आकर्षित हुन्छन्. Industrial and fluid-handling lines lean on HDPE and nylon. Mapping your industry to these resins early keeps the quoting conversation focused and avoids specifying an over-engineered material you do not need.
Practical tips for moving from concept to production
मेरो अनुभवमा, three habits keep extrusion projects on schedule. पहिले, prototype from stock shapes where the geometry allows, then commit to custom tooling only after the design is validated, which protects your die investment. दोस्रो, specify tolerances by feature rather than blanket-tightening the whole profile, since that respects the process and controls cost. तेस्रो, confirm your supplier can carry the part from prototype to production on the same line, so scale-up does not force a re-quote. Handled this way, extrusion delivers custom parts economically, with the quick turnaround that makes the process attractive in the first place.
For a deeper look at fabricating cost-effective custom parts from standard and custom profiles, I point buyers to सीगेट प्लास्टिक’ extrusion overview.
Bringing Your Extrusion Sourcing Strategy Together
After walking through capabilities, सामग्री, and vetting criteria, the through-line I keep returning to is this: choosing among plastic extrusion companies and factories is less about finding the “सबैभन्दा ठूलो” वा “सबै भन्दा राम्रो” name and more about matching a supplier’s real strengths to your specific part, मात्रा, र टाइमलाइन. A continuous, high-volume manufacturing process rewards long production runs, but the same shop that excels at a million linear feet of PVC profile may not be the partner I want for a low-volume PEEK prototype. मेरो अनुभवमा, buyers who define the problem precisely before they request quotes get sharper pricing and fewer surprises downstream.
Material selection sits at the center of every good decision. Whether the application calls for rigid PVC or ABS in structural profiles, polycarbonate or acrylic (PMMA) अप्टिकल स्पष्टता को लागी, रासायनिक प्रतिरोधको लागि HDPE र LDPE, जीवित टिकाहरूको लागि polypropylene, नायलन (PA) for wear surfaces, or TPE/TPU for flexible seals, the resin drives tooling, सहिष्णुता, र लागत. Extrusion melts raw plastic and forms it into a continuous profile with a fixed cross-section (सीगेट प्लास्टिक, 2024), र मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024). That combination of stock shapes and custom profile extrusion, sometimes paired with co-extrusion for multi-material geometry, is what makes the process so versatile from prototype to production.
On the commercial side, I always separate one-time and recurring costs. Custom extrusion typically carries a one-time tooling and die investment, while stock profiles avoid it, so the die design and tooling decision shapes the whole business case. Domestic sourcing deserves a second look too: reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023), which often narrows the gap that offshore unit pricing appears to open. And because thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (U.S. EPA, 2023), a quality-focused domestic plastics manufacturer can support both cost and sustainability goals at once.
Quality systems are the final filter I apply. ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो (ISO, 2015), and it remains the most widely adopted benchmark I look for when comparing a custom plastic extrusion manufacturer against its peers. Pair that with realistic expectations on precision, since extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (प्रोटोल्याबहरू, 2023), and you have a grounded framework for evaluating any plastic profile manufacturer or plastic tubing supplier.
Expert Insight
| Key Point | व्याख्या |
|---|---|
| Match process to volume, not to reputation | Continuous extrusion is a high-volume process best suited to long production runs, so I weigh a factory’s real strengths against my order size rather than chasing “सबैभन्दा ठूलो” वा “सबै भन्दा राम्रो” claims. |
| Separate tooling from unit price | Custom profiles require a one-time die investment while stock extruded shapes avoid it; understanding this split keeps the true cost of custom plastic profiles from hiding inside a quoted per-foot rate. |
| Verify quality before precision expectations | ISO 9001 प्रमाणीकरण (ISO, 2015) signals a managed process, and I set tolerance expectations knowing extrusion runs looser than injection molding (प्रोटोल्याबहरू, 2023). |
B2B खरीददारहरूको लागि कार्ययोग्य सोर्सिङ सुझावहरू
- Define the part before you shop. Document the profile cross-section, राल (PVC, ABS, polycarbonate, HDPE, polypropylene, or an engineering-grade plastic), वार्षिक मात्रा, and target tolerance so every plastic extrusion companies factory supplier quotes against the same brief.
- Ask for tooling, MOQ, and lead-time numbers separately. Request the die cost, न्यूनतम आदेश मात्रा, and quoted lead time as distinct line items to compare custom extrusion and stock profiles on equal footing.
- Confirm the quality system in writing. Ask for a current ISO 9001 certificate and the inspection points used on extruded plastic parts, rather than accepting a general quality claim.
- Weigh domestic sourcing on total landed cost. Compare a domestic plastics manufacturer against offshore options using freight, कर्तव्य, र सूची बोक्ने लागत, एकाइ मूल्य एक्लै होइन (पुन: प्राप्ति पहल, 2023).
- Test the relationship with a small run. Move from prototype to production in stages so you validate quick-turnaround performance and communication before committing to high-volume manufacturing.
- Use supplier directories as a starting list, छोटो सूची होइन. Directories such as Thomasnet (2024) help you locate regional plastic fabrication services, but I still vet capability, सामग्री, and certification directly with each shop.
FAQ
How do I find plastic extrusion companies or a factory near me?
When I evaluate location intent, I start by mapping suppliers against my shipping lanes rather than pure geographic proximity. A plastic profile manufacturer two states away with the right die design and tooling capability often beats a closer shop that lacks my resin. I use supplier directories that list and categorize US plastic extrusion manufacturers by capability and region to build a shortlist, then verify with a plant visit or video walkthrough. Thomas directories are a practical starting point for this (Thomasnet, 2024, thomasnet.com). मेरो अनुभवमा, “मेरो नजिक” should mean short, predictable lead times and low freight, not just a nearby ZIP code.
What should I look for in plastic extrusion manufacturers in the USA?
For domestic sourcing, I weigh three things: certified quality, material breadth, and total landed cost. A domestic plastics manufacturer can reduce total landed cost by lowering freight, कर्तव्य, र सूची बोक्ने लागत (पुन: प्राप्ति पहल, 2023, reshorenow.org), which often narrows the gap with offshore quotes once you account for the full picture. The US plastics industry is also a major contributor to domestic manufacturing shipments and employment (प्लास्टिक उद्योग संघ, 2023), so the supplier base is deep. I confirm they run the resins I need, from commodity grades like PVC, HDPE, LDPE, and polypropylene to engineering-grade plastics such as polycarbonate, नायलन (PA), र PEEK.
How do I choose the right plastic extrusion supplier for my project?
I treat supplier selection as a vetting checklist, not a gut call. The concrete questions I ask every candidate:
- Do you hold ISO 9001 प्रमाणीकरण, the internationally recognized standard for quality management systems (ISO, 2015)?
- Which resins and profiles do you run in production, and do you offer co-extrusion?
- What are your tolerances, and how do you handle profile cross-section validation?
- What is your minimum order quantity (MOQ), tooling lead time, and production lead time?
- Can you support the full path from prototype to production and quick-turnaround production for reorders?
Industrial Plastic Extrusion Parts The biggest mistake I see buyers make is choosing on unit price alone and ignoring tooling cost, MOQ, and lead-time risk. Those drivers usually decide whether a program is actually profitable.
What is the difference between custom and stock plastic extrusions?
Stock extruded shapes are standard profiles and tubes a supplier already produces, so you skip tooling and buy off the shelf. Custom extrusion requires a one-time tooling and die investment to create your unique profile cross-section. The tradeoff is straightforward: stock plastic extrusions minimize upfront cost and lead time, while custom plastic profiles fit your exact geometry. उल्लेखनीय रूपमा, मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ। (सीगेट प्लास्टिक, 2024, seagateplastics.com), so I often prototype with stock shapes before committing to a die.
How should I read “सबैभन्दा ठूलो” र “सबै भन्दा राम्रो” plastic extrusion factory claims?
I read those labels with healthy skepticism. “Largest” usually reflects capacity or revenue, which matters for high-volume manufacturing but tells me nothing about fit for a low-volume, tight-tolerance job. “Best” is subjective marketing unless it is backed by certifications, सन्दर्भहरू, and capability data. My rule: rank suppliers against my own requirements, not against a generic superlative. The largest plastic extrusion company on a list may be the wrong contract manufacturing partner for a specialty acrylic (PMMA) or TPE/TPU part, while a mid-size specialist nails it.
What are plastic extrusion profiles, and how are they made?
A profile is a continuous shape with a fixed cross-section. प्लास्टिक एक्सट्रुजनले कच्चा प्लास्टिक सामग्री पग्लन्छ र यसलाई स्थिर क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ। (सीगेट प्लास्टिक, 2024). Because it is a continuous forming process, resin extrusion is well suited to long production runs and high-volume manufacturing. It also supports plastic sheet extrusion and tubing. One thing I always plan around: सामग्री संकुचन र निरन्तर गठनको कारणले गर्दा बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ (Protolabs डिजाइन संसाधनहरू, 2023), so I set tolerance expectations early with the plastic tubing supplier or profile shop.
Which plastic material should I choose for my extruded parts?
I anchor material selection to the application, not habit. PVC is among the most widely extruded plastics globally and is common in profiles, पाइप, र ट्युबिङ. For impact and appearance, I look at ABS or polycarbonate; for chemical resistance and living hinges, polypropylene; for outdoor and clarity, एक्रिलिक (PMMA); and for demanding thermal or wear conditions, नायलन (PA) वा PEEK. I also confirm recyclability up front, since thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (US EPA, 2023). Matching resin to service environment prevents the costly redesigns I have watched derail otherwise solid programs.
What drives the cost of extruded plastic parts?
Three levers move price more than anything else. पहिले, टूलिङ: a custom die is a one-time investment that stock profiles avoid entirely. दोस्रो, MOQ and run length, since extrusion rewards volume and unit cost drops as quantities rise. तेस्रो, material grade, where engineering-grade plastics and specialty resins cost well above commodity options. When I request a quote, I ask suppliers to break out tooling, per-unit price, and secondary plastic fabrication services separately so I can compare offers on equal terms and identify where the real cost lives.
सन्दर्भहरू
- प्लास्टिक एक्सट्रुजनले कच्चा प्लास्टिक सामग्री पग्लन्छ र यसलाई स्थिर क्रस-सेक्शनको साथ निरन्तर प्रोफाइलमा बनाउँछ।. - सीगेट प्लास्टिक (2024)
- मानक एक्स्ट्रुडेड प्रोफाइलहरू र ट्यूबहरू द्रुत टर्नअराउन्डको साथ लागत-प्रभावी अनुकूलन भागहरूमा निर्माण गर्न सकिन्छ।. - सीगेट प्लास्टिक (2024)
- ISO 9001 उत्पादनमा प्रयोग हुने गुणस्तर व्यवस्थापन प्रणालीहरूको लागि अन्तर्राष्ट्रिय रूपमा मान्यता प्राप्त मानक हो. - मानकीकरणको लागि अन्तर्राष्ट्रिय संगठन (2015)
- The US plastics industry is a major contributor to domestic manufacturing shipments and employment. - प्लास्टिक उद्योग संघ (2023)
- Reshoring and domestic sourcing can reduce total landed cost by lowering freight, कर्तव्य, and inventory carying costs. - पुन: प्राप्ति पहल (2023)
- सामग्री संकुचन र निरन्तर गठनको कारण बाहिर निकाल्ने सहिष्णुता सामान्यतया इंजेक्शन मोल्डिंग भन्दा ढीला हुन्छ।. - Protolabs डिजाइन संसाधनहरू (2023)
- एक्सट्रुसनमा प्रयोग हुने थर्मोप्लास्टिक्स पुन: प्रयोग गर्न मिल्ने हुन्छ, र पुन: प्रयोग पुन: प्रयोगले सामग्री दक्षता सुधार गर्दछ. - अमेरिकी पर्यावरण संरक्षण एजेन्सी (2023)
- Thomas suplier directories list and categorize US plastic extrusion manufacturers by capability and region. - Thomasnet (2024)
- Plastic extrusion is a continuous, high-volume process well suited to long production runs, per general industry manufacturing references (SPI/Plastics Industry Association overview). — Planning analysis
- PVC विश्वव्यापी रूपमा सबैभन्दा व्यापक रूपमा निकालिएको प्लास्टिकहरू मध्ये एक हो, प्राय: प्रोफाइलहरूमा प्रयोग गरिन्छ, पाइप, र ट्युबिङ (प्लास्टिक उद्योग संघ). — Planning analysis