

Lub Hoobkas Twin Screw Extruder Elements Factory: Lub Definitive B2B Trade Guide rau Manufacturers, Lwm tus neeg & Wholesale buyers hauv
The global twin screw extruder elements market is experiencing significant momentum as plastics compounding, Kev ua zaub mov noj, tshuaj, thiab kev lag luam tshuaj lom neeg nthuav dav thoob plaws North America thiab Europe. Rau cov neeg yuav khoom B2B uas nrhiav ib tug neeg ntseeg tau twin screw extruder elements hoobkas, nkag siab txog thaj chaw tsim khoom, cov cai lag luam, cov kev thauj mus los, thiab nrhiav cov kev ua tau zoo tshaj plaws yog qhov tseem ceeb. This guide delivers an in-depth analysis of the twin screw extruder elements factory ecosystem—covering leading manufacturers, wholesale supplier evaluation, kev lag luam dynamics, tariff considerations, and actionable forecasts for Q3–Q4. Whether you are a compounder in Germany, a plastics processor in Ohio, or a trading company sourcing screw elements at scale, this resource equips you with the intelligence to make confident procurement decisions.
Nkag siab txog cov khoom siv ob lub nplhaib extruder: Core Components and Industrial Applications
Twin screw extruder elements are the modular building blocks inserted onto the shafts of co-rotating or counter-rotating twin screw extruders. These elements—including conveying elements, kneading blocks, Cov khoom sib xyaw, and reverse-flight elements—determine the shear, residence time, and throughput characteristics of the extrusion process. A specialized twin screw extruder elements hoobkas produces these components from tool steels (e.g., W6Mo5Cr4V2, 38CrMoAlA) or powder-metallurgy alloys with tight tolerances, feem ntau ±0.01 mm on the involute profile.
Key application sectors driving demand include:
- Plastics compounding: a, polymer blending, filled and reinforced compounds (fiber iav, carbon fiber, cov khoom siv mineral).
- Kev ua zaub mov: Snack extrusion, pet food, textured vegetable protein (TVP), and cereal production.
- Tshuaj: Hot-melt extrusion rau cov txheej txheem xa tshuaj—a rapidly growing segment in the EU and US.
- Chemical processing: Reactive extrusion, devolatilization, and continuous mixing of adhesives, sealants, and coatings.
- Recycling: Mechanical recycling of post-consumer plastics, a sector boosted by EU Circular Economy regulations and US EPA initiatives.
Double-Screw Extruder According to data from Grand View Research (2024), the global twin screw extruder market was valued at approximately USD 1.2 billion and is projected to grow at a CAGR of 5.2% through 2030. The replacement and upgrade cycle for screw elements—which are wear parts—generates a recurring aftermarket estimated at 30–40% of the total extruder market value, making the twin screw extruder elements factory segment a critical supply chain node. Mixing Equipment Supplier

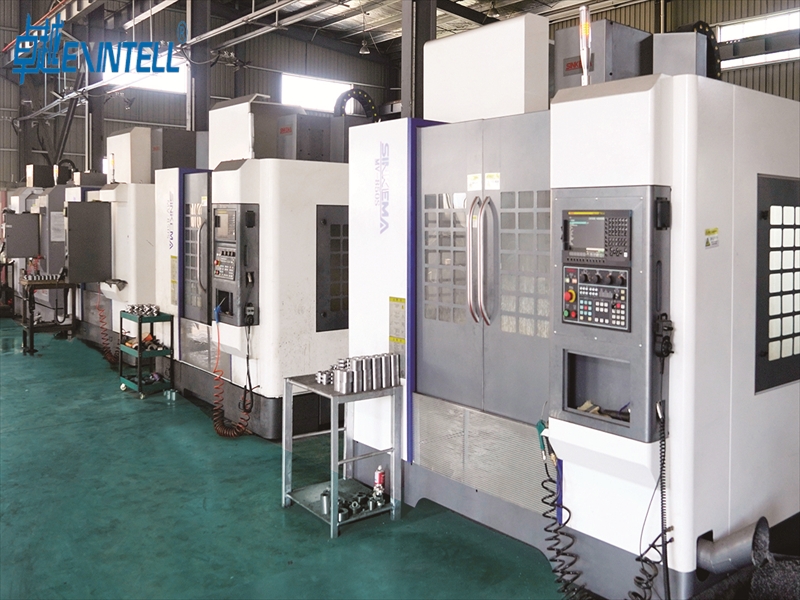
Industrial manufacturing facility with CNC machinery producing precision metal components for extrusion equipment
The Global Twin Screw Extruder Elements Factory Landscape: Who Makes What and Where
The manufacturing base for twin screw extruder elements is concentrated in several key regions, txhua qhov muaj qhov zoo sib tw tshwj xeeb:
Tuam Tshoj: The Volume Leader
China hosts the largest number of twin screw extruder elements factories, primarily clustered in Nanjing (Jiangsu xeev), which is often called the "Extruder Capital" of the world. Nanjing-based factories such as Nanjing Jieya Extrusion Equipment Co., Nanjing Haisi Extrusion Equipment Co., and Nanjing Kerke Extrusion Equipment Co. supply screw elements globally. Chinese factories offer competitive pricing—often 40–60% below European OEM equivalents—while increasingly matching quality through investments in CNC grinding centers (e.g., Kapp Niles, Reishauer) and metallurgical testing labs. Rau cov neeg yuav khoom wholesale, China remains the primary sourcing origin for cost-effective, high-volume orders.
Lub teb chaws Yelemees: The Precision Benchmark
Pince A Extruder Germany is home to the original twin screw extruder OEMs—Coperion (Stuttgart), KraussMaffei Extrusion (Hannover), thiab Leistritz (Nuremberg). These companies manufacture proprietary screw elements with the tightest tolerances and premium metallurgy. German-made elements command price premiums of 2–4× over Chinese equivalents but are preferred for critical applications in pharmaceuticals, high-performance polymers, and food-contact extrusion where traceability and certification (FDA, EU 1935/2004) are mandatory.
United States: Growing Domestic Capacity
US-based manufacturers like Entek (Lebanon, Oregon), Century Extrusion (Traverse City, Michigan), and CPM Extrusion Group supply both OEM and aftermarket screw elements. The reshoring trend, amplified by Section 301 tariffs on Chinese machinery components and the CHIPS and Science Act's broader manufacturing incentives, is encouraging domestic capacity expansion. However, US factories still represent a small fraction of global output.
Browse our complete catalog of twin screw extruder elements engineered for Coperion, Leistritz, JSW, and Berstorff shaft profiles. Twin Screw Extruder Machine Manufacturer
Trade Policy and Its Impact on Twin Screw Extruder Elements Sourcing
The transatlantic trade relationship between the United States and the European Union is the world's largest bilateral commercial partnership, with goods and services trade exceeding USD 1.3 trillion txhua xyoo raws li Chaw Haujlwm Tus Thawj Coj Lag Luam Asmeskas (USTR) (2024 cov ntaub ntawv). For B2B buyers of twin screw extruder elements, several policy dimensions are directly relevant:
Tariff Structure
Twin screw extruder elements typically fall under HS Code 8477.90 (parts of machinery for working rubber or plastics). The US MFN (Most Favored Nation) tariff rate for HS 8477.90 is 3.1% rau kev xa khoom los ntawm EU cov tswvcuab. EU imports from the US face a comparable rate of 2.7% under the EU Common Customs Tariff. These relatively low tariff rates facilitate bilateral trade in extruder components.
However, when sourcing from China, US importers face an additional 25% Seem 301 tariff on HS 8477.90 goods, imposed since 2018 and maintained through. This tariff differential has reshaped sourcing strategies: some Extruder Wholesale US compounders now source screw elements from EU factories (particularly Germany and Italy) to avoid the China tariff, while others absorb the cost due to the significant base-price advantage of Chinese elements. Wholesale Lab Extruders
EU Carbon Border Adjustment Mechanism (CBAM)
The EU's CBAM, which entered its transitional phase in October 2023 thiab yuav ua haujlwm tag nrho los ntawm 2026, applies to imports of steel and aluminum—key raw materials for screw element production. A twin screw extruder elements factory exporting to the EU will need to report embedded carbon emissions, and eventually purchase CBAM certificates. This regulation, documented by the European Commission – Taxation and Customs Union, adds compliance complexity and potential cost for non-EU manufacturers, particularly those in regions with carbon-intensive steel production.
Trade and Technology Council (TTC)
TTC, Tsim tsa hauv 2021, has working groups on supply chain resilience and standards alignment. For industrial machinery components like screw elements, the TTC's efforts to harmonize technical standards (e.g., material certifications, kev tso cai rau qhov ntev) could reduce non-tariff barriers and facilitate cross-border procurement. Cov International Trade Administration (ITA) provides regular updates on TTC progress.

Aerial view of a major European port with container ships and logistics infrastructure supporting international B2B trade
B2B Trade Opportunities for Twin Screw Extruder Elements in US and EU Markets
The convergence of several macro trends is creating substantial B2B opportunities for twin screw extruder elements factories serving the US and EU:
Lub sijhawm 1: Plastics Recycling Mandates
Dispermat Mixer The EU's Packaging and Packaging Waste Regulation (PPWR), tau txais kev pom zoo hauv 2024, mandates minimum recycled content in plastic packaging—30% by 2030 and 65% by 2040. Hauv As Mes Lis Kas, states like California (SB 54), New Jersey, and Oregon have enacted extended producer responsibility (EPR) laws with recycled content requirements. Mechanical recycling Single Screw Extruder Slideshare relies heavily on twin screw extruders for recompounding, and the wear rate on screw elements processing recycled feedstock (which contains contaminants, fillers, and mixed polymers) is 2–3× higher than virgin material processing. This accelerates the replacement cycle and increases demand for wear-resistant screw elements from specialized factories.
Lub sijhawm 2: Pharmaceutical Hot-Melt Extrusion
The FDA and EMA have approved an increasing number of drug products manufactured via hot-melt extrusion (HME). According to a 2024 review in the International Journal of Pharmaceutics, over 30 commercial drug products now use HME technology. Cov khoom ntsia hlau qib tshuaj yuav tsum tau kho saum npoo tshwj xeeb (e.g., electropolishing rau Ra ≤ 0.4 µm), material certifications (316L stainless steel lossis Hastelloy), thiab tag nrho cov ntaub ntawv taug qab. Qhov chaw muaj nyiaj ntau no nyiam cov hoobkas uas muaj ISO 13485 lossis cov txheej txheem zoo sib xws.
Lub sijhawm 3: Tsheb Hluav Taws Xob (EV) Cov Khoom Siv Roj Teeb
Twin screw extruders tab tom siv ntau dua rau kev sib xyaw cathode thiab anode slurries txuas ntxiv hauv kev tsim roj teeb lithium-ion—a process called "dry electrode" kev tsim khoom. Nrog EU Battery Regulation (2023) thiab US Inflation Reduction Act (IRA) tsav kev nqis peev loj hauv kev tsim roj teeb hauv tsev, kev thov rau cov khoom screw tshwj xeeb (tiv taus corrosion, cov qauv muaj zog siab) tab tom tshwm sim ua ib qho kev loj hlob tshiab. Blender Extrude A Curve
Kev Sib Tw 1: Kev tshuaj xyuas zoo ntawm qhov loj
Cov neeg yuav khoom B2B uas yuav khoom los ntawm lwm lub teb chaws cov khoom siv twin screw extruder ntsib teeb meem kuaj xyuas zoo. Kev raug ntawm qhov ntev, kev sib xyaw metallurgy, and heat treatment consistency can vary between batches. Mitigation strategies include requiring material test certificates (EN 10204 3.1), conducting pre-shipment inspections via third-party agencies (SGS, Bureau Veritas), and requesting sample elements for fit-testing before committing to volume orders.
Kev Sib Tw 2: Intellectual Property Concerns
OEM screw element designs are often proprietary, with specific involute profiles, tip angles, and flight geometries. Aftermarket factories that reverse-engineer these designs operate in a legal gray area. B2B buyers should ensure their supplier has legitimate design rights or is producing to openly published specifications to avoid IP infringement risks, particularly when importing into the US (where ITC Section 337 investigations can block infringing goods at the border).
Learn more about our quality inspection process for twin screw extruder elements thiab yuav ua li cas peb xyuas kom muaj kev sib haum xeeb ntawm batch-to-batch.
Cov txiaj ntsig ntawm thaj chaw thiab txoj cai uas pab txhawb kev lag luam B2B hauv cov khoom extruder
Asmeskas thiab EU tau txais txiaj ntsig los ntawm ntau yam zoo uas pab txhawb kev lag luam B2B hauv cov khoom lag luam xws li ob lub nplhaib extruder khoom:
Kev tsim kho logistics: The transatlantic shipping corridor is among the world's most efficient. Cov chaw nres nkoj loj—Rotterdam (Europe's largest), Hamburg, Antwerp-Bruges ntawm EU sab; Los Angeles/Long Beach, Savannah, thiab Newark ntawm sab US—muab kev caij nkoj ntau zaus nrog sijhawm thauj khoom 10–18 hnub. Tus nqi thauj khoom hauv thawv rau cov khoom tshuab tau rov qab zoo tom qab kab mob kis thoob ntiaj teb, nrog tus nqi nrawm ntawm Asia-Europe thiab Asia-US poob qis 70–80% los ntawm 2022 nce siab raws li Drewry World Container Index (May ).
Kev sib haum xeeb ntawm cov cai: Ob lub tebchaws Asmeskas thiab EU tswj hwm cov qauv kev lag luam ruaj khov. Cov khoom screw tsim raws li DIN, ISO, or ASTM standards are broadly interchangeable in specification language, reducing technical barriers. The mutual recognition of calibration certificates (ILAC MRA) and testing laboratory accreditations (ISO/IEC 17025) further streamlines cross-border quality assurance.
Trade finance and payment security: transactions benefit from mature trade finance instruments—letters of credit, cov ntaub ntawv sau tseg, thiab kev pov hwm nyiaj txiag lag luam (Euler Hermes, Coface, Atradius)—that reduce counterparty risk. This is a significant advantage compared to sourcing from regions with less developed financial infrastructure.
Free Trade Zones and bonded warehousing: Ob lub teb chaws US (Foreign Trade Zones program, tswj los ntawm ITA) thiab EU (Free Zones under the Union Customs Code) allow importers to defer or reduce duties on components held in inventory, improving cash flow for distributors who stock screw elements for rapid delivery.

Chaw khaws khoom logistics niaj hnub nrog kev npaj cov khoom khaws cia rau kev faib khoom B2B hauv kev lag luam
Case Study: Yuav ua li cas cov tuam txhab B2B ua tiav hauv kev lag luam ob lub nplhaib extruder khoom
Rooj plaub 1: Ib lub hoobkas nyob Nanjing nthuav dav mus rau EU aftermarket
Ib lub hoobkas nruab nrab ob lub nplhaib extruder hauv Nanjing, ua haujlwm kwv yees 120 cov neeg ua haujlwm thiab cov neeg ua haujlwm 15 CNC profile grinding machines, tau lees paub tias nws lub lag luam hauv tsev tab tom puv npo nrog kev sib tw nqi. Hauv 2023, lub tuam txhab hloov mus tsom rau kev lag luam tom qab hauv Europe los ntawm:
- tau txais ISO 9001:2015 ntawv pov thawj thiab nqis peev rau ib lub tshuab ntsuas coordinate (CMM) rau 100% kev tshuaj xyuas qhov ntev.
- txhim kho cov profile nplhaib uas haum nrog Coperion ZSK, Leistritz ZSE, thiab Berstorff ZE series extruders—peb lub platform nrov tshaj plaws hauv European compounding plants.
- koom tes nrog ib tug neeg muab kev thauj khoom los muab DDP (Delivered Duty Paid) pricing to EU customers, simplifying the procurement process.
- Attending K Fair (Düsseldorf, October cycle) and Chinaplas to build direct relationships with European compounders.
Hauv 18 lub hlis, the factory grew its EU revenue from near-zero to approximately 25% ntawm tag nrho cov kev muag khoom, with key accounts in Germany, Poland, thiab Ltalis. The company's success hinged on matching OEM dimensional accuracy while offering 45–55% cost savings and 4-week lead times (vs. 8–12 weeks from OEMs).
Rooj plaub 2: A US Distributor Building a Dual-Source Supply Chain
A specialty industrial distributor based in Houston, Texas, serving the US Gulf Coast petrochemical corridor, historically sourced screw elements exclusively from a single German OEM. When lead times extended to 16 weeks during the 2021–2022 supply chain crisis, the distributor nearly lost key accounts. In response, the company:
- Qualified a second source—a Chinese twin screw extruder elements factory—for standard conveying and kneading elements (approximately 70% of demand by volume).
- Maintained the German OEM relationship for specialized elements (e.g., pharmaceutical-grade, high-alloy compositions) where certification and traceability justified the premium.
- Established a bonded warehouse in a US Foreign Trade Zone near the Port of Houston, holding 90-day safety stock of fast-moving element sizes.
- Implemented a digital inventory management system allowing customers to check stock availability and place orders online.
This dual-source strategy reduced average lead times to 3–5 days for stocked items and 4–6 weeks for custom orders, while reducing procurement costs by approximately 30% on standard elements. The distributor's revenue grew 40% xyoo dhau xyoo hauv 2024, according to the company's published case study.
Rooj plaub 3: Ib lub tuam txhab Italian siv kev txawj ntse tshwj xeeb
Ib lub tuam txhab ua haujlwm precision machining tsev neeg ze Brescia, Ltalis—ib cheeb tsam nto moo rau kev ua hlau—hloov los ntawm kev machining CNC dav dav mus rau kev tsim cov khoom siv extruder twin screw tshwj xeeb 2019. Lub tuam txhab muaj qhov txawv ntawm:
- tsom rua cov alloy ua haujlwm siab xwb: PM (e) cov hlau cuab yeej, tungsten carbide composites, thiab nickel-based superalloys rau kev siv corrosion.
- Muab PVD hauv tsev (Physical Vapor Deposition) kev pab txheej txheej (TiAlN, CrN) kom nce lub neej hnav ntawm cov khoom los ntawm 3–5×.
- Muab kev pab tswv yim engineering—tshuaj xyuas cov neeg siv khoom' extrusion txheej txheem thiab pom zoo cov qauv screws zoo tshaj plaws.
Los ntawm 2024, lub tuam txhab tau tsim ib lub hauv paus neeg siv khoom thoob plaws 14 EU lub tebchaws thiab tab tom xa khoom mus rau As Mes Lis Kas, nqi zoo li German OEM tab sis ua haujlwm sai dua (3–4 lub lis piam vs. 8–12 weeks). Qhov xwm txheej no qhia tau tias lub hoobkas ua ob lub screw extruder elements tuaj yeem sib tw raws tus nqi es tsis yog tus nqi.

Tus engineer tab tom tshuaj xyuas cov khoom hlau uas tau machined zoo hauv ib lub chaw tsim khoom niaj hnub nrog cov cuab yeej tswj zoo
Kev kwv yees kev lag luam rau Twin Screw Extruder Elements: Q3–Q4 Outlook
Raws li cov cim kev lag luam tam sim no, txoj cai kev txhim kho, thiab cov ntaub ntawv kev lag luam, Cov kev hloov pauv hauv qab no yuav hloov pauv rau lub hoobkas ob lub screw extruder hauv 1–2 lub hlis thiab mus txog thaum kawg:
Kev kwv yees 1: Kev hloov pauv se yuav txuas ntxiv
Kev lag luam US tseem hloov pauv. Raws li nruab nrab-, Seem 301 se rau cov khoom siv tshuab Suav (25%) tseem muaj kev siv, thiab tsis muaj kev qhia tias yuav txo sai sai. Tsis tas li ntawd, tsoom fwv US tau qhia txog kev hloov tus nqi se rau EU steel thiab aluminium hauv Section 232, uas tej zaum yuav cuam tshuam tus nqi screw element yog tias tus nqi khoom siv hloov pauv. B2B buyers should build tariff scenario planning into their procurement models. Cov US Kev Lis Kev Cai thiab Ciam Teb Kev Tiv Thaiv (CBP) CROSS rulings database is the authoritative source for HS classification guidance.
Kev kwv yees 2: EU CBAM Compliance Will Become a Competitive Differentiator
As the EU CBAM transitions from reporting-only to certificate-purchase requirements (2026), twin screw extruder elements factories that can demonstrate low-carbon steel sourcing and provide verified emissions data will gain a competitive edge in the EU market. Factories in countries with clean electricity grids (e.g., Scandinavia, e) or those using electric arc furnace (EAF) steel will be advantaged. Chinese factories relying on blast furnace steel may face CBAM surcharges equivalent to 5–15% of product value, partially eroding their price advantage.
Kev kwv yees 3: Consolidation in the Aftermarket Segment
C, o. v&A activity, k (e.g., h, o) o. m.
Kev kwv yees 4: Digital Procurement Will Accelerate
s (i, m, Europages) v. However, the trend is moving toward configurator-based ordering—e, x, t, r, u, d. e, particularly among mid-sized compounders who lack dedicated procurement teams.
Kev kwv yees 5: Recycling-Driven Demand Surge
With the EU PPWR implementation timeline accelerating and major brand owners (Nestlé, Unilever, P&G) committing to recycled content targets, the installed base of recycling extruders in Europe is expected to grow 15–20% annually through 2027, ib Plastics Recyclers Europe estimates. Each new extruder installation represents a recurring screw element replacement opportunity, and the abrasive nature of recycled feedstock ensures high replacement frequency.

Industrial plastics recycling facility with extrusion machinery processing post-consumer materials
Material Science and Wear Protection: Safeguarding Performance and Operator Safety
The performance and longevity of twin screw extruder elements are fundamentally determined by material selection and surface engineering. Rau cov neeg yuav khoom B2B, understanding these factors is critical to optimizing total cost of ownership and ensuring safe, reliable operations. Twin-Screw Extruders Hoobkas
Base Material Options
A professional twin screw extruder elements factory typically offers multiple material grades:
- Nitrided steel (38CrMoAlA): The workhorse material for general-purpose compounding. Nitriding creates a hard surface layer (900–1100 HV) while maintaining a tough core. Cost-effective for non-abrasive applications.
- Tool steel (W6Mo5Cr4V2 / AISI M2): High-speed steel offering superior wear resistance for moderately abrasive compounds (Calcium carbonate, talc-filled polymers). Hardness after heat treatment: 62–65 HRC.
- Powder metallurgy (PM) steel (CPM 9V, CPM 10V): Produced by hot isostatic pressing, PM steels offer uniform carbide distribution and exceptional abrasion resistance—3–5× the wear life of conventional tool steels. Preferred for glass fiber-reinforced compounds.
- Nickel-based alloys (Hastelloy C-276, Inconel 625): For corrosive applications—processing fluoropolymers, PVC with aggressive stabilizer packages, or reactive extrusion with acidic byproducts.
- Tungsten carbide composites (HIP-clad): The ultimate wear solution for highly abrasive applications. Tungsten carbide particles in a metallic matrix provide hardness exceeding 1500 HV. Used in recycling applications where contaminated feedstock causes extreme wear.
Surface Treatment Technologies
Beyond base material selection, surface treatments extend element life and improve process performance:
- PVD coatings (TiN, TiAlN, CrN): Thin-film coatings (2–5 µm) applied at low temperatures, preserving substrate properties. TiAlN coatings offer oxidation resistance to 800°C, suitable for high-temperature engineering polymer processing.
- Plasma nitriding: A controlled nitriding process producing a uniform, deep hardened layer without the "white layer" defects common in gas nitriding. Preferred for food-contact applications where surface integrity is critical.
- Chrome plating (hard chrome): Traditional surface treatment offering good corrosion resistance and moderate wear protection. Being phased out in the EU due to REACH restrictions on hexavalent chromium (Cr6+), with HVOF (High Velocity Oxy-Fuel) thermal spray coatings emerging as the replacement.
- Laser cladding: Additive manufacturing technique depositing wear-resistant alloy layers (Stellite, Colmonoy) on element surfaces. Enables localized reinforcement of high-wear zones (e.g., kneading block tips) without treating the entire element.
Operator Safety Considerations
While twin screw extruder elements themselves are internal components, their condition directly impacts operational safety:
- Worn elements increase energy consumption: Degraded screw profiles reduce pumping efficiency, requiring higher motor torque and increasing energy costs by 10–25%. Monitoring specific energy consumption (kWh / kg) is a key indicator for element replacement timing.
- Metal contamination risk: Severely worn elements can shed metal particles into the product stream—a critical concern in food and pharmaceutical applications. Regular element inspection and proactive replacement prevent contamination events that could trigger product recalls.
- Shaft damage prevention: Worn elements with loose fits on the shaft can cause fretting corrosion and shaft damage. Shaft replacement costs 10–50× the cost of a single element, making timely element replacement a cost-effective maintenance strategy.
- Process stability: Consistent element geometry ensures stable melt temperature, pressure, and output rate. Worn elements cause process variability, leading to off-spec product and potential safety issues in downstream operations (e.g., inconsistent wall thickness in extruded pipe).
A responsible twin screw extruder elements factory provides detailed wear guidelines, recommended replacement intervals based on application type, and technical support for screw configuration Extruded Pvc Type A optimization. B2B buyers should evaluate suppliers not just on element price, but on the total value proposition including technical service, wear data, and application engineering support.
Plastic Extrusion Companies Manufacturer Access our screw element wear and replacement guide for detailed maintenance recommendations by application type.

Close-up of precision-engineered metal components showing surface treatment and quality finishing for industrial applications
Selecting the Right Twin Screw Extruder Elements Factory: A B2B Buyer's Checklist
For procurement professionals evaluating a twin screw extruder elements factory, the following criteria should guide supplier selection:
- Profile compatibility: Confirm the factory can produce elements matching your specific extruder shaft profile (spline geometry, OD/ID dimensions). Request sample elements for fit-testing.
- Material certifications: Require EN 10204 Hom 3.1 material test certificates for every batch. Rau kev siv zaub mov, verify FDA 21 CFR or EU 1935/2004 a.
- Dimensional inspection capability: The factory should operate calibrated CMMs (coordinate measuring machines) and provide inspection reports with each shipment. Request Cpk data for critical dimensions.
- Heat treatment control: Verify the factory has in-house or certified heat treatment facilities with temperature uniformity surveys (per AMS 2750 lossis sib npaug).
- Minimum order quantity (MOQ) yooj: Wholesale buyers need volume pricing, but also the ability to order small quantities of specialized elements. Evaluate the factory's MOQ policy across its product range.
- Lead time reliability: Request historical on-time delivery data. A factory with 95%+ OTD (e) performance demonstrates operational discipline.
- Kev txhawb nqa thev naus laus zis: The best factories offer screw design consultation, wear analysis, and process optimization support—not just component supply.
- Trade compliance: Rau kev yuav khoom thoob ntiaj teb, verify the factory's experience with export documentation, HS classification, and destination-country regulatory requirements.
Request a quote from our factory and receive a detailed proposal including material options, txhuas lub sijhawm, and volume pricing within 24 teev.
Logistics and Shipping Best Practices for Twin Screw Extruder Elements
Twin screw extruder elements are dense, precision-machined metal components that require careful handling during international shipping:
- Packaging: Individual elements should be wrapped in VCI (Vapor Corrosion Inhibitor) paper or film, then placed in compartmentalized wooden crates. Kneading blocks and mixing elements with protruding features require custom foam inserts to prevent contact damage.
- Shipping mode: For standard orders, LCL (Less than Container Load) ocean freight is cost-effective. For urgent orders or high-value pharmaceutical-grade elements, air freight is justified. A typical set of screw elements for a 40mm–90mm extruder weighs 50–300 kg, making air freight feasible.
- Incoterms: B2B buyers should negotiate FOB (Free on Board) or CIF (Tus Nqi, Insurance, Freight) terms for ocean shipments. DDP (Delivered Duty Paid) simplifies the process for buyers unfamiliar with import procedures but typically costs 5–10% more.
- Insurance: Marine cargo insurance (Institute Cargo Clauses A—all risks) is recommended for precision components. The cost is typically 0.3–0.5% of declared value.
- Customs documentation: Ensure the commercial invoice includes accurate HS codes (8477.90.XX), material composition, country of origin, and unit values. Incorrect documentation causes customs delays and potential penalty assessments.
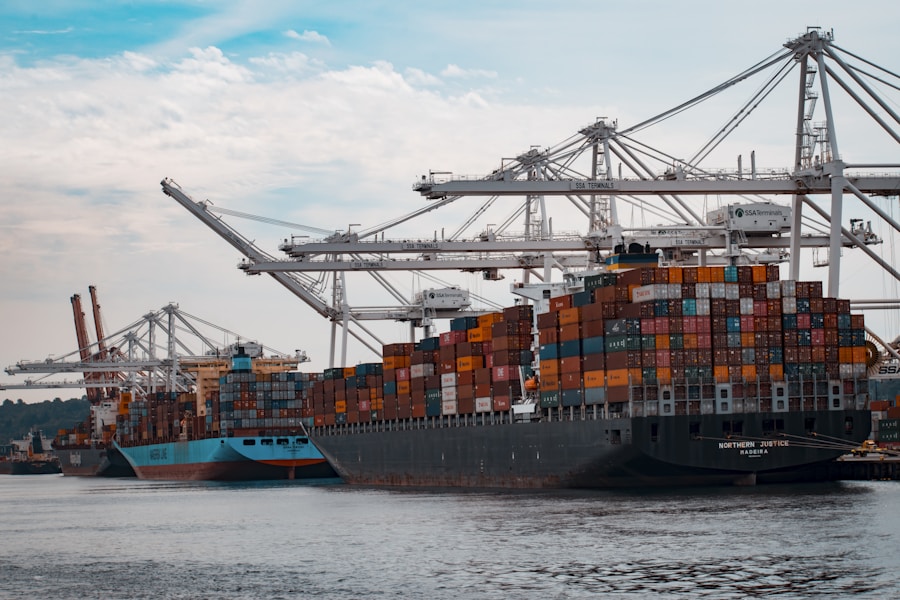
Container port with cargo ships and cranes facilitating global B2B trade logistics for industrial components
Industry Standards and Certifications Relevant to Twin Screw Extruder Elements
Twin ntsia hlau Extruder Elements Wholesale: Ua tiav B2B Sourcing Guide rau… · Twin Screw Extruder Gearbox Chaw Tsim Tshuaj Ntsuam Kev Lag Luam, Market Trends… · Twin Screw Extruder Gearbox Supplier: Complete B2B Sourcing Guide for T…