

Extruder Twin Screw Barrel Manufacturer Manufacturer: Lub Definitive B2B Sourcing & Trade Guide rau
The global twin screw extruder market is on a steep growth trajectory. Muaj nqi kwv yees li USD 9.7 billion in 2024, lub koom haum no kwv yees yuav mus txog USD 13.2–14.8 billion los ntawm 2030, nthuav dav nrog tus nqi loj hlob txhua xyoo (CAGR) ntawm 5.2–7.1% according to multiple industry research firms including Grand View Research and Mordor Intelligence. At the heart of every twin screw extruder sits the barrel — the precision-engineered cylinder that, together with intermeshing screw elements, determines output quality, throughput, thiab lub neej ntev. Rau B2B buyers thoob plaws Europe, North America, thiab emerging ciaj uas muag, choosing the right extruder twin screw barrel manufacturer is not merely a procurement decision; it is a strategic investment that shapes production economics for years to come.
This guide walks professional buyers through the current state of the twin screw barrel manufacturing industry, trade policies affecting cross-border sourcing, material science advances, kev tshawb fawb txog kev ua lag luam tiag tiag, thiab kev kwv yees ua tau rau lub hlis tom ntej. Whether you are an OEM integrator, a plastics compounder seeking replacement wear parts, lossis ib lub tuam txhab lag luam tsim ib lub saw khoom rau ob lub nplhaib nplhaib sib dhos, cov ntaub ntawv hauv qab no tsim los txhim kho koj txoj kev nrhiav khoom.

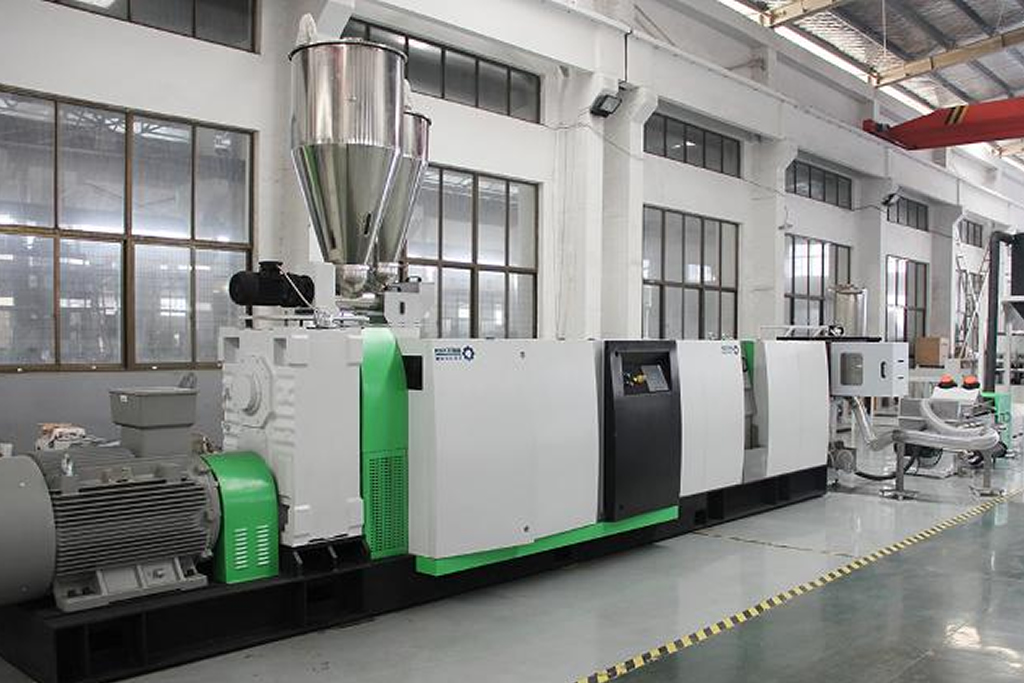
Lub chaw tsim khoom lag luam tsim cov khoom hlau raug rau tshuab extrusion
Nkag siab txog Twin Screw Extruder Barrel: Cov Khoom Hauv Nruab Nrab thiab Cov Haujlwm
Ib lub nplhaib ob nplhaib extruder yog ib qho phab ntsa hnyav, lub tog raj kheej segmented lossis monolithic uas tau bored kom txais tau ob lub nplhaib tig ua ke lossis tig rov qab. The barrel's inner surface must withstand extreme abrasion, corrosion, thiab kev hloov kub — cov xwm txheej uas txawv heev raws li cov khoom siv, los ntawm cov yas engineering uas muaj iav fiber mus rau cov starch qib zaub mov. Lub Tshuab Extrusion Yas Hlau
Cov cheeb tsam tseem ceeb hauv ib lub thawv twin screw feem ntau muaj xws li:
- Cheeb tsam pub mov — qhov chaw uas cov khoom raw nkag mus; barrel bore is often smooth or lightly grooved to control intake rate.
- Melting/plasticizing zone — high shear and compression; barrel liners here face the most aggressive wear.
- Mixing/kneading zone — distributive and dispersive mixing; barrel temperature control accuracy is critical.
- Metering/discharge zone — consistent melt pressure delivery; bore tolerances tighten to ±0.02 mm in premium barrels.
The barrel is typically manufactured from nitralloy 135M, 38CrMoAlA, or tool steel substrates, then treated via gas nitriding, bimetallic centrifugal casting, or HIP (hot isostatic pressing) cladding to achieve surface hardness of 58–72 HRC depending on the application. Understanding these fundamentals helps B2B buyers specify requirements accurately when engaging an extruder twin screw barrel supplier.
Global Market Landscape for Twin Screw Barrel Manufacturers in
Kev lag luam tshuab extrusion ob lub nplhaib yog Phaetus Apus 2 Extruder tau tsim los ntawm ntau yam kev sib koom ua ke hauv:
Cov cai rov siv yas. The European Union's revised Packaging and Packaging Waste Regulation (PPWR), tau ua tiav lig 2024, yuav tsum tau cov xeev tswv cuab ua haujlwm 55% Kev rov siv yas ntim los ntawm 2030. Cov kab rov siv tshuab feem ntau siv ob lub nplhaib extruders rau kev sib xyaw cov resins rov siv nrog cov khoom ntxiv, txhawb kev thov hloov lub thawv nce. Asmeskas. EPA's updated National Recycling Strategy similarly incentivizes domestic recycling infrastructure, tsim kev thov sib npaug hauv North America.
Tsheb hluav taws xob (EV) kev loj hlob ntawm kev muab khoom. Cov zaj duab xis cais roj teeb, cov khoom siv thermal interface, thiab cov polymer sib xyaw nyhav rau cov khoom EV raug ua haujlwm ntawm ob lub nplhaib extruders. BloombergNEF cov ntaub ntawv qhia tias kev muag tsheb hluav taws xob thoob ntiaj teb dhau mus 20 ib lab lub tsheb hauv, and each new compounding line requires high-performance barrels rated for abrasive ceramic fillers.
Food and pharmaceutical extrusion. Hot-melt extrusion (HME) for drug delivery and twin screw cooking extrusion for plant-based proteins are expanding segments. These applications demand FDA/EU-compliant barrel materials — typically stainless steel liners or nickel-based alloy overlays — pushing manufacturers to diversify their product lines.
Major manufacturing clusters for twin screw barrels include Zhoushan and Jingjiang in China, which collectively account for an estimated 45–50% of global barrel output by volume; the Ruhr and Baden-Württemberg regions in Germany, home to premium OEM barrel producers; and Brescia, Ltalis, a traditional hub for bimetallic barrel technology. Emerging capacity is also growing in India (Gujarat, Maharashtra) thiab Turkey.

Chaw nres nkoj thoob ntiaj teb nrog cov nkoj thawv sawv cev rau kev lag luam thoob ntiaj teb B2B rau cov khoom siv tshuab lag luam
Cov cai lag luam cuam tshuam rau kev nrhiav thoob ntiaj teb thoob ntiaj teb:, thiab ntau ntxiv
Single Screw Extruder Wholesale Cov neeg yuav khoom B2B uas nrhiav ob lub raj hlau thoob ntiaj teb yuav tsum tswj hwm ib qho kev cai lag luam uas nyuaj zuj zus: Plastic Extrusions For Gates
US tariff landscape. Raws li thaum ntxov, United States khaws Section 301 cov se rau ntau yam khoom lag luam los ntawm Suav. Ob lub thawv ntsia hlau raug faib rau HTS 8477.90 (cov khoom ntawm cov tshuab ua yas) face a 25% ad valorem se thaum nqa los ntawm Suav teb. Kev tshuaj xyuas se Biden-era, txuas ntxiv hauv lub sijhawm tam sim no, tau khaws cov nqi no. Tsis tas li ntawd, Seem 232 cov se hlau thiab aluminium (25% and 10% respectively) tuaj yeem siv rau kev yuav khoom raw barrel, ntxiv kev txhawj xeeb nqi rau cov tuam txhab tsim khoom uas yuav khoom hlau substrate thoob ntiaj teb. Hlis Plaub, cov kev ntsuas se tshiab tau tshaj tawm rau ntau pawg ntxiv, ua rau muaj kev tsis ntseeg ntxiv rau cov neeg npaj kev muab khoom (source: International Trade Administration).
EU cov cuab yeej tiv thaiv kev lag luam. The European Commission's anti-dumping framework continues to scrutinize Chinese steel and machinery components. Thaum ob lub raj screws tsis tau raug se tiv thaiv kev muag khoom tshwj xeeb, the EU's Carbon Border Adjustment Mechanism (CBAM), nkag mus rau nws lub sijhawm hloov pauv, yuav tsum tau cov neeg yuav khoom qhia txog carbon embedded hauv cov khoom siv hlau ntau pib 2026. Cov tuam txhab tsim raj uas muaj txheej txheem tsim khoom tsawg carbon tau lees paub yuav tau txais qhov zoo dua hauv kev lag luam EU (source: European Commission DG Trade).
Free trade agreements. EU-Japan EPA, CPTPP, and RCEP agreements offer preferential tariff treatment for qualifying machinery parts. Buyers in signatory Plastic Extruder Manufacturers Manufacturer countries can reduce landed costs by 3–8% by sourcing from manufacturers in partner nations and ensuring proper rules-of-origin documentation.
Export controls and dual-use considerations. High-precision barrel manufacturing equipment (CNC deep-hole boring machines, for instance) may fall under dual-use export control lists in certain jurisdictions. While finished barrels themselves are rarely restricted, buyers should verify end-use compliance when sourcing for defense or nuclear-adjacent applications.
B2B Trade Opportunities in the Twin Screw Barrel Sector
The intersection of rising extrusion demand and evolving trade policy creates distinct opportunities for B2B participants:
Replacement parts aftermarket. A twin screw barrel typically has a service life of 8,000–15,000 operating hours depending on processed material abrasiveness. With the installed base of twin screw extruders exceeding 120,000 units globally (estimated from Coperion, KraussMaffei, and Leistritz production data), the aftermarket for replacement barrels and screw elements represents a USD 1.8–2.4 billion annual opportunity. Distributors and trading companies that can offer rapid delivery of compatible barrels for major OEM platforms — Coperion ZSK, Leistritz ZSE, KraussMaffei ZE, JSW TEX, Nanjing-series machines — capture recurring revenue streams.
Custom-engineered barrels for niche applications. As extrusion moves into advanced materials (carbon fiber composites, battery electrode slurries, biodegradable polymers), standard nitrided barrels often fall short. Manufacturers offering application-specific solutions — tungsten carbide liners for highly abrasive compounds, Hastelloy overlays for corrosive fluoropolymer processing, segmented barrels with independent cooling channels for temperature-sensitive pharma applications — command premium pricing and build defensible market positions.

Nearshoring and supply chain diversification. Post-pandemic supply chain resilience strategies are driving European and American OEMs to diversify barrel sourcing beyond China. Qaib Cov Txwv, Is Nrias teb, and Eastern European manufacturers (Poland, Czech Republic) are gaining share as "China+1" alternatives. B2B intermediaries facilitating quality-assured sourcing from these emerging suppliers fill a valuable market gap.
Digital procurement platforms. i, Made-in-China, and GlobalSources remain dominant for initial supplier discovery, tab sis cov platform B2B tshwj xeeb thiab cov vev xaib ncaj qha ntawm cov tuam txhab tsim khoom nrog cov lus qhia ntxaws ntxaws, 3qauv 3D, thiab cov cuab yeej hais nqi tam sim ntawd tau nyiam ntau dua los ntawm cov neeg yuav khoom ua haujlwm. Cov tuam txhab tsim khoom nqis peev hauv digital muag khoom pom 20–35% tus nqi hloov pauv ntawm kev nug mus rau kev txiav txim siab siab dua raws li a 2024 McKinsey B2B kev tshawb fawb kev lag luam.
Cov Kev Nyuaj Rau Cov Neeg Yuav thiab Cov Chaw Tsim Khoom B2B
Alongside opportunities, kev lag luam twin screw barrels ntsib teeb meem tiag tiag:
Kev sib haum xeeb zoo. Kev sib txawv ntawm cov barrels zoo tshaj plaws hauv Europe/Japanese thiab cov kev xaiv pheej yig dua tuaj yeem loj heev. Bore concentricity, liner adhesion zoo, kev sib npaug ntawm kev kho cua sov, thiab kev tshuaj xyuas cov khoom metallurgyical tseem yog cov teeb meem nyuaj. Cov neeg yuav khoom qhia tias 10–15% ntawm cov barrels uas tau los ntawm cov neeg muab khoom tsis tau tshuaj xyuas tsis dhau kev tshuaj xyuas zoo, raws li a 2024 Plastics Technology kev tshawb fawb ntawm North American processors.
Kev txhawj xeeb txog cuab yeej tswv cuab. OEM barrel designs — bore profiles, kev teeb tsa cooling channel, segmented barrel interface geometries — are proprietary. Aftermarket manufacturers must navigate IP boundaries carefully, and buyers should verify that suppliers have legitimate engineering capabilities rather than simply copying OEM drawings.
Logistics and lead times. A standard segmented twin screw barrel set weighs 500–3,000 kg depending on extruder size. Shipping costs have stabilized from 2021–2022 peaks but remain 30–40% above pre-pandemic levels on Asia-Europe and Asia-North America routes. Lead times for custom bimetallic barrels range from 6–12 weeks, requiring buyers to plan procurement cycles well in advance.
Raw material price volatility. Nickel, cobalt, tungsten, and molybdenum — key alloying elements in barrel liner materials — have experienced 15–25% price swings over the past 12 lub hlis. Manufacturers without hedging strategies or long-term supply agreements pass this volatility to buyers, complicating budget planning.
Material Science and Manufacturing Technology: What Defines a Top-Tier Barrel Manufacturer
The technical differentiation among extruder twin screw barrel manufacturers comes down to materials and processes: Recycled Plastic Pellets Factory
Nitrided barrels. Gas nitriding of 38CrMoAlA or SACM645 steel produces a 0.5–0.7 mm hardened case (900–1100 HV). This is the most cost-effective treatment, suitable for processing non-abrasive polymers like PE, PP, thiab PS. Top manufacturers achieve nitriding uniformity within ±50 HV across the full barrel length — a metric that separates reliable suppliers from inconsistent ones.
Cov thawv Bimetallic. Centrifugal casting of iron-based (Fe-B), nickel-based (Ni-Cr-B-Si), or cobalt-based alloy liners inside a 4140/4340 steel shell delivers 2–5x the wear life of nitrided barrels. The critical quality factor is liner-to-substrate bond integrity; ultrasonic testing should show zero delamination across 100% of the bore surface. Leading manufacturers in Zhoushan, Tuam Tshoj, and Brescia, Ltalis, have refined this process over decades.
Powder metallurgy (PM) and HIP liners. Rau cov kev siv siab tshaj plaws — processing glass-fiber-filled PA66, mineral-filled PPS, or ceramic-loaded battery electrode compounds — HIP-applied tool steel or tungsten carbide liners offer hardness exceeding 65 HRC with superior toughness. This technology is dominated by a handful of European and Japanese specialists, with barrel costs 3–5x higher than standard bimetallic options.

Precision machining. Bore finishing to Ra 0.4 μm or better, concentricity within 0.03 mm over barrel lengths exceeding 3 meters, and H7-tolerance fit on barrel-to-barrel segment interfaces require deep-hole boring machines, CNC honing cuab yeej, thiab kev ntsuas nruj hauv txheej txheem. Cov tuam txhab tsim khoom nqis peev rau cov tshuab ntsuas coordinate (CMM) thiab laser bore gauging qhia txog kev mob siab rau qhov zoo uas cov neeg yuav khoom B2B yuav tsum xyuas thaum tshuaj xyuas hauv hoobkas.
Kev kho nto thiab txheej txheej. Chrome plating, PVD/CVD coatings, thiab thermal spray overlays (HVOF tungsten carbide) yog kev kho ntxiv uas ua rau barrel nyob ntev dua hauv qee qhov kev siv. A knowledgeable manufacturer recommends the optimal treatment based on the buyer's processing conditions rather than defaulting to the cheapest option.
Thaj chaw thiab kev cai hauv B2B Barrel Trade
Thaj chaw thiab kev cai lag luam tsim cov kev yuav khoom tshwj xeeb uas cov neeg yuav khoom B2B ntse siv:
Suav mus rau Europe los ntawm tsheb ciav hlau. The China-Europe Railway Express (CRE) network tam sim no ua haujlwm 15,000 kev mus ncig txhua xyoo, nrog sijhawm thauj khoom 15–18 days versus 30–35 days by sea. For time-sensitive barrel orders, rail freight offers a middle ground between air and ocean shipping costs. Key departure points — Yiwu, Chengdu, Xi'an — connect to Hamburg, Duisburg, and Madrid.
Turkey as a nearshore hub for EU buyers. Turkey's customs union with the EU eliminates duties on most industrial goods, including machinery parts. Turkish barrel manufacturers in Istanbul and Kocaeli offer 2–3 week delivery to Western Europe with competitive pricing, making Turkey an attractive alternative for EU-based compounders and OEMs seeking supply chain resilience.
India's production-linked incentive (PLI) scheme. India's PLI program for capital goods and specialty steel incentivizes domestic barrel manufacturing. For buyers serving the Indian subcontinent market, sourcing from Indian manufacturers avoids import duties of 7.5–15% and benefits from improving quality standards as Indian producers invest in European-grade equipment.
US-Mexico-Canada Agreement (USMCA). Barrels manufactured in Mexico with sufficient North American content qualify for duty-free entry into the US and Canada. Several Chinese and Taiwanese barrel manufacturers have established or are exploring Mexican production facilities to serve the North American market tariff-free.
Freight containers at a major international trade port representing cross-border B2B logistics for industrial equipment
Case Studies Barrel Sourcing in Practice
Rooj plaub 1: European compounder reduces downtime by 40% with dual-source strategy.
A mid-sized German plastics compounder operating 12 twin screw extruder lines (Coperion ZSK 58 and ZSK 92 platforms) historically sourced all replacement barrels from a single Chinese manufacturer. Hauv 2023, a quality issue with a batch of bimetallic barrels — insufficient liner thickness in the high-wear zone — caused unplanned downtime costing an estimated EUR 180,000. The company implemented a dual-source strategy: primary supply from a Zhoushan-based manufacturer with ISO 9001:2015 and PED certification, and secondary supply from a Turkish producer for urgent orders. Los ntawm, the company reports 40% reduction in unplanned barrel-related downtime and 12% lower average barrel procurement cost through competitive bidding between the two suppliers. The key lesson: qualifying two suppliers with rigorous incoming inspection protocols (ultrasonic testing, hardness mapping, kev txheeb xyuas qhov ntev) delivers both cost and reliability benefits.
Rooj plaub 2: US food extrusion OEM develops proprietary barrel specification with Chinese manufacturer.
A Wisconsin-based manufacturer of twin screw food extruders needed barrels with FDA-compliant stainless steel liners capable of withstanding the abrasive, corrosive environment of high-moisture pet food extrusion. Standard catalog barrels from domestic suppliers were priced at USD 28,000–35,000 per set with 10–14 e. The company partnered with a Jingjiang, Tuam Tshoj, manufacturer to co-develop a barrel using 316L stainless liner centrifugally cast into a 4140 shell, with custom cooling channel geometry. After a 6-month qualification process including on-site factory audits and trial barrel testing, the company achieved 35% cost reduction with equivalent performance. Annual procurement now exceeds USD 1.2 lab, with barrels shipped via ocean freight to the Port of Chicago. Seem 301 tariffs add 25% to landed cost, but the net savings versus domestic sourcing remain significant at approximately 15–18%.
Rooj plaub 3: Indian recycling startup scales with modular barrel system.
A Mumbai-based plastics recycling startup processing post-consumer PET bottle flakes needed to scale from a single 52mm twin screw line to four lines within 18 lub hlis. Capital constraints made purchasing complete new extruders impractical. Hloov chaw, the company sourced modular segmented barrel systems from a Guangzhou manufacturer, designed to retrofit onto locally assembled extruder frames. The segmented design allowed individual barrel sections to be replaced as they wore, reducing ongoing maintenance costs by an estimated 25% compared to monolithic barrel replacement. The manufacturer provided detailed engineering drawings and remote technical support for installation, demonstrating the value of manufacturer-buyer collaboration in emerging market contexts. Single Screw Extruder
Quality Assurance: What B2B Buyers Should Demand from Barrel Manufacturers
Professional procurement of twin screw barrels requires a structured quality assurance framework:
- Material certificates: Mill test reports (MTR) for barrel substrate steel and liner alloy, traceable to specific heat numbers. Verify chemical composition against specification (e.g., ASTM A322 for 4140 steel, DIN 1.8519 for 38CrMoAlA).
- Hardness testing: Rockwell or Vickers hardness measurements at minimum 5 points along barrel length, on both liner surface and substrate. Request hardness mapping reports.
- Dimensional inspection: Bore diameter, concentricity, straightness, and surface finish (Ra) measurements using calibrated instruments. CMM reports for critical interface dimensions.
- Non-destructive testing (NDT): Ultrasonic testing for liner bond integrity (100% bore coverage), magnetic particle inspection for surface cracks, and dye penetrant testing for barrel segment sealing surfaces.
- Cov Ntawv Pov Thawj: ISO 9001:2015 (kev tswj hwm zoo), ISO 14001 (kev tswj hwm ib puag ncig), and where applicable, PED 2014/68/EU (Pressure Equipment Directive) for barrels operating under pressure in EU jurisdictions.
Buyers should conduct factory audits — either in person or via third-party inspection agencies (SGS, Bureau Veritas, TÜV) — before committing to volume orders. The cost of a factory audit (USD 1,500–3,000) is trivial compared to the cost of receiving non-conforming barrels.
Quality control inspection of industrial metal components using precision measurement instruments
Forecasting Twin Screw Barrel Trade Trends: June–Lub Yim Hli
Raws li cov cim kev lag luam tam sim no, txoj cai kev txhim kho, thiab cov ntaub ntawv kev lag luam, the following trends are expected to shape the twin screw barrel B2B trade over the next one to two months:
Tariff uncertainty drives pre-buying. The April announcement of expanded US reciprocal tariffs has triggered a wave of pre-buying among North American distributors and OEMs. Barrel manufacturers in China report order backlogs extending to 10–14 weeks, up from the typical 6–8 weeks. Buyers who have not yet placed orders for Q3 delivery should expect longer lead times and consider expedited shipping options.
Cr10 Max Extruder Raw material costs stabilize. After a volatile Q1, nickel prices have settled in the USD 15,500–16,500/tonne range on the LME, and tungsten APT prices are holding at USD 325–340/MTU. This stabilization should translate to more predictable barrel pricing through the summer, though manufacturers may attempt to retain Q1 price increases. Buyers should negotiate based on current raw material indices rather than accepting legacy pricing.
Chinaplas aftereffects. Chinaplas, held in Shenzhen in April, showcased several barrel manufacturers' new product lines including segmented barrels with integrated sensor ports for Industry 4.0 monitoring, and next-generation PM-HIP liners with claimed 30% longer wear life. Expect these innovations to enter commercial availability in Q3–Q4, giving early-adopter buyers a competitive advantage in processing efficiency.
Lab Scale Extruder Manufacturer EU CBAM reporting drives supplier qualification. As the EU CBAM transitional phase progresses, European importers of steel-intensive products including extruder barrels are beginning to request carbon footprint data from manufacturers. Suppliers who can provide verified emissions data (Scope 1, 2, and 3) will be preferred. Chinese manufacturers with renewable energy-powered facilities (increasingly common in Zhejiang and Jiangsu provinces) are positioning themselves favorably.
Recycling infrastructure investment accelerates. Government funding programs — the EU's Circular Economy Action Plan, the US EPA's Solid Waste Infrastructure for Recycling (SWIFR) grants — are releasing capital for new recycling lines in mid-. Each new mechanical recycling line typically requires 2–4 twin screw extruders, translating to direct barrel demand. Manufacturers and distributors targeting the recycling sector should prepare inventory accordingly.
India emerges as a sourcing alternative. Indian barrel manufacturers exhibited at Plastivision India (January) with notably improved product quality. Several Ahmedabad and Pune-based manufacturers have achieved bimetallic barrel quality comparable to mid-tier Chinese producers at 10–15% lower pricing, driven by lower labor costs and India's growing specialty steel production capacity. For buyers serving South Asian, Middle Eastern, and African markets, Indian sourcing deserves serious evaluation.
Workplace Safety in Extrusion Environments: Protecting Operators from the Ground Up
While the focus of this guide is on barrel sourcing, responsible B2B trade in extrusion machinery must address the operational environment where these barrels are installed. Twin screw extrusion facilities present specific workplace hazards — high temperatures (barrel surfaces reach 200–400°C), heavy component handling (barrel segments weigh 50–300 kg each), molten polymer spills, and floor surfaces contaminated with processing oils and pellet dust. Foot injuries are among the most common and preventable workplace incidents in plastics processing plants.
The case for safety footwear in extrusion facilities. According to the U.S. Bureau of Labor Statistics (BLS), foot injuries account for approximately 60,000 kev raug mob hauv chaw ua haujlwm txhua xyoo hauv Tebchaws Asmeskas, nrog ib puag ncig tsim khoom muaj feem ntau dhau. The European Agency for Safety and Health at Work (EU-OSHA) reports similar patterns across EU member states. Hauv cov chaw extrusion tshwj xeeb, cov kev phom sij tseem ceeb rau ko taw muaj xws li:
- Crushing injuries from dropped barrel segments, screw elements, or die components during maintenance and changeover operations.
- Burn injuries from contact with hot barrel surfaces, molten polymer drips, or heated die assemblies.
- Puncture injuries from metal shavings, cov ntsia hlau tawg, or sharp-edged barrel liner fragments.
- Slip injuries on floors contaminated with processing oils, water from cooling systems, or spilled polymer pellets.
- Electrical hazards from barrel heater band wiring during maintenance.
Safety footwear standards and specifications. B2B buyers of extrusion equipment should ensure their facilities — and their customers' facilities — are equipped with appropriate safety footwear meeting recognized standards:
- ASTM F2413 (US standard): Specifies requirements for protective footwear including impact resistance (I/75 — 75 ft-lbs impact protection), kev tiv thaiv nias (C/75 — 2,500 lbs compression), kev tiv thaiv metatarsal (Mt/75), and electrical hazard (EH) ratings.
- EN ISO 20345 (EU standard): Defines safety footwear classes from SB (kev tiv thaiv ko taw yooj yim, 200J cuam tshuam) mus txog S5 (Kev tiv thaiv ntiv taw + khau kaw taw + antistatic + kev nqus zog + water resistance + penetration resistance + khau sab nraud muaj cleated). For extrusion environments, S3 or S5 rated footwear is recommended.
- Composite toe vs. steel toe: Modern composite toe caps (fiberglass, carbon fiber, or Kevlar) offer equivalent protection to steel at 30–40% nyhav tsawg dua, with the added benefit of thermal insulation — important in extrusion environments where floor temperatures near barrel heating zones can be elevated.
Sprite Extruder Bltouch Mount Heat-resistant soles. Standard rubber outsoles degrade at sustained contact temperatures above 150°C. Extrusion facility safety footwear Crality Dual Gear Extruder should feature nitrile rubber or Viton-compound outsoles rated for 300°C contact resistance, protecting against accidental stepping on hot polymer drips or near barrel heating zones.
Anti-fatigue and ergonomic considerations. Extrusion operators and maintenance technicians often work 8–12 ua haujlwm ib teev ntawm av pob zeb. Safety footwear with energy-return midsoles (PU or EVA foam), kev txhawb nqa arch, and moisture-wicking linings reduces fatigue-related accidents — a factor that safety managers increasingly recognize as contributing to overall workplace safety performance.

ROI of safety footwear programs. The National Safety Council estimates that the average cost of a workplace foot injury in the US is USD 9,600 hauv cov nqi ncaj qha (kev kho mob, cov neeg ua haujlwm' them nyiaj) and USD 29,000–42,000 in total costs including lost productivity, replacement labor, and administrative expenses. A quality pair of safety boots costs USD 80–250. Rau ib lub chaw uas muaj 50 extrusion operators, a comprehensive safety footwear program costs USD 4,000–12,500 txhua xyoo — a fraction of the cost of a single serious foot injury. European data from EU-OSHA shows comparable economics, with the added regulatory imperative of the EU Framework Directive 89/391/EEC requiring employers to provide appropriate PPE at no cost to workers.
Integration with barrel maintenance protocols. B2B barrel manufacturers and suppliers can add value by including safety recommendations in their technical documentation. Barrel installation and removal procedures should specify required PPE including safety footwear class, reinforcing a culture of safety that