Manifattur ta 'elementi ta' estrużur Twin Screw: Complete B2B Trade Analysis and Global Sourcing Guide for
The global market for twin screw extruder elements is experiencing significant transformation as B2B trade between the United States, Unjoni Ewropea, and Asia-Pacific manufacturing hubs intensifies. Twin screw extruder elements — including screw segments, blokki tal-għaġna, inforri tal-barmil, and mixing elements — are critical components in plastics compounding, ipproċessar tal-ikel, manifattura farmaċewtika, and chemical engineering. As demand for high-performance polymer compounds and advanced materials grows, sourcing from the right twin screw extruder elements manufacturer has become a strategic priority for processors worldwide. This article provides an in-depth analysis of the current trade landscape, supplier ecosystem, opportunitajiet tas-suq, and practical guidance for B2B buyers seeking reliable twin screw extruder elements suppliers u fabbriki.
Current State of the Twin Screw Extruder Elements Industry
The twin screw extruder market was valued at approximately USD 1.2 biljun fi 2024 u huwa pproġettat li jilħaq USD 1.7 biljun minn 2030, jikber f'CAGR ta' madwar 5.8%, according to data published by Grand View Research and MarketsandMarkets in their 2024 industry reports. The replacement parts and elements segment — covering screw elements, btieti, shafts, and wear-resistant components — represents a substantial share of aftermarket revenue, estimated at 30–40% of total extruder lifecycle spending.
Key drivers include:
- Rising demand for engineering plastics and polymer compounds in automotive lightweighting and EV battery separator production
- Growth in masterbatch and color concentrate manufacturing across Southeast Asia and Eastern Europe
- Increasing adoption of twin screw extrusion in pharmaceutical hot-melt extrusion (HME) applications
- Sustainability mandates pushing recyclers toward twin screw systems for post-consumer resin (PCR) taħlit
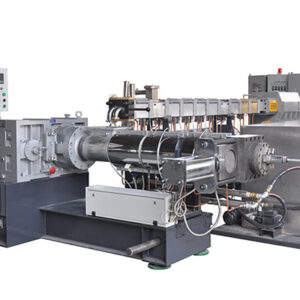
Major OEM extruder brands — Koperion (il-Ġermanja), KraussMaffei (il-Ġermanja), Leistritz (il-Ġermanja), JSW (Ġappun), and Nanjing-based Chinese manufacturers — all rely on precision-engineered screw elements. Madankollu, the aftermarket and third-party twin screw extruder elements manufacturer segment has grown rapidly, offering cost-effective alternatives with comparable metallurgy and tolerances. Sors: Grand View Riċerka, 2024; Swieq u Swieq, 2024. Parallel Twin-Screw Extruder
Industrial manufacturing facility with precision metal components representing twin screw extruder elements production
Trade Policy Landscape Affecting Industrial Components
The transatlantic trade relationship between the United States and the European Union remains the world's largest bilateral commercial partnership, bil-kummerċ totali ta 'oġġetti u servizzi li jaqbeż USD 1.3 trillion annually as reported by the U.S. Census Bureau and Eurostat in early. For industrial machinery components like twin screw extruder elements, several policy developments in the past two months are particularly relevant:
Tariff Environment (April–Ġunju ): L-U.S. administration's tariff actions in early have created significant uncertainty for industrial component trade. Taqsima 301 tariffs on Chinese-origin goods remain in effect, with machinery components facing duties of 25%. The EU's Carbon Border Adjustment Mechanism (CBAM) transitional phase continues to require importers to report embedded emissions in certain goods, though most extruder components fall outside the current CBAM scope (which covers steel, aluminju, siment, fertilizers, electricity, and hydrogen). Madankollu, raw material inputs — particularly tool steel and tungsten carbide used in screw element manufacturing — are indirectly affected. Sors: Amministrazzjoni tal-Kummerċ Internazzjonali (ITA), .
EU Trade Defense Instruments: The European Commission's Directorate-General for Trade has maintained anti-dumping duties on certain steel products from China, which impacts the cost structure for Chinese-origin extruder elements entering the EU market. This creates opportunities for manufacturers in India, Turkija, and domestic EU producers. Sors: EU Trade DG, .
Kunsill tal-Kummerċ u t-Teknoloġija (TTC): While the TTC has focused primarily on semiconductors and AI, its supply chain resilience workstream has implications for critical industrial equipment sourcing, encouraging diversification away from single-source dependencies.
Global Supplier Ecosystem: Where Twin Screw Extruder Elements Are Manufactured
The twin screw extruder elements factory landscape is geographically concentrated in several key regions:
Iċ-Ċina (Nanjing, Zhangjiagang, Kunshan Clusters)
China dominates global production volume for aftermarket twin screw extruder elements. The Nanjing cluster alone hosts over 50 manufacturers specializing in screw elements, btieti, and complete screw configurations. Key advantages include competitive pricing (typically 40–60% below European OEM pricing), rapid prototyping capabilities, and extensive material options including nitrided steel, ligi bimetalliċi, PM-HIP (powder metallurgy hot isostatic pressing) materjali, and tungsten carbide coatings. Notable manufacturers include Nanjing Kerke Extrusion Equipment, Nanjing Haisi Extrusion Equipment, and Jiangsu Xinda Tech. Chinese manufacturers have invested heavily in CNC grinding, tikkoordina magni tal-kejl (CMM), and metallurgical testing to meet European and American quality standards.
Germany and Western Europe
Germany remains the technology leader, with companies like Coperion, Leistritz, and specialized element producers offering premium-grade components with tight tolerances (tipikament ±0.01mm) and advanced metallurgies. European manufacturers emphasize traceability, material certification (IN 10204 3.1 certificates), and long-term dimensional stability. Pricing is at the premium end, but total cost of ownership can be competitive for high-wear applications.
India and Turkey (Emerging Suppliers)
India's twin screw extruder elements manufacturing sector is growing, with companies in Ahmedabad and Pune offering mid-range pricing with improving quality. Turkey has emerged as a nearshoring option for EU buyers seeking shorter lead times than China with lower costs than Western Europe.
Global shipping port with container vessels representing international B2B trade logistics for industrial components
B2B Trade Opportunities in the Twin Screw Extruder Elements Market
Għal xerrejja B2B — including plastics compounders, food processors, pharmaceutical manufacturers, and extruder OEMs — several significant opportunities have emerged in:
1. Supply Chain Diversification: The ongoing US-China trade tensions and tariff uncertainties have accelerated "China+1" strateġiji ta' sorsi. B2B buyers are actively seeking qualified twin screw extruder elements suppliers in alternative geographies. This creates opportunities for manufacturers in India, Vjetnam, and Turkey to capture market share, while established Chinese manufacturers are responding by setting up warehousing in the US and EU to offer local stock with faster delivery.
2. Aftermarket Growth: As the installed base of twin screw extruders grows globally — estimated at over 50,000 active machines worldwide — the demand for replacement elements, wear parts, and upgrade kits continues to expand. Third-party manufacturers offering OEM-equivalent quality at 30–50% lower cost are well-positioned. B2B e-commerce platforms like Alibaba, Magħmul fiċ-Ċina, and GlobalSources have made it easier for buyers to identify and qualify twin screw extruder elements wholesale suppliers.
3. Material Innovation: Advanced metallurgies are creating differentiation opportunities. PM-HIP (Powder Metallurgy Hot Isostatic Pressing) screw elements offer 3–5x longer service life compared to conventional Estrużur b'żewġ Stadji nitrided steel in abrasive applications (fibra tal-ħġieġ, mili minerali). Manufacturers investing in these technologies can command premium pricing while delivering lower total cost of ownership to buyers. Extruder Machine Manufacturer
4. Customization and Engineering Support: B2B buyers increasingly require not just components but screw configuration design support. Manufacturers offering simulation-backed screw design services (using tools like Ludovic or proprietary software) alongside element manufacturing are capturing higher-value orders.
Challenges Facing B2B Buyers and Manufacturers
Minkejja l-opportunitajiet, several challenges persist in the twin screw extruder elements trade:
Quality Verification: The gap between claimed and actual metallurgical quality remains a significant concern, particularly when sourcing from new suppliers. Buyers report issues with inconsistent hardness (HRC variations exceeding specifications), poor surface finish on spline profiles, and dimensional deviations that cause premature wear or processing instability. Mitigation strategies include requiring third-party inspection (SGS, Bureau Veritas), requesting material test certificates, and ordering trial quantities before committing to volume purchases.
Tħassib dwar il-Proprjetà Intellettwali: OEM extruder manufacturers have proprietary screw element geometries protected by patents. Third-party manufacturers must navigate IP boundaries carefully, offering compatible but non-infringing designs. This is particularly relevant for self-wiping profile geometries and specialized mixing element designs.
Loġistika u Lead Times: Sea freight from China to the US West Coast takes 14–21 jiem, with additional inland transit. EU-bound shipments via the Suez Canal route take 28–35 jiem. Air freight is available for urgent orders but increases cost by 5–8x. Il-Baħar l-Aħmar tfixkel it-tbaħħir tard 2024 and early caused significant delays and cost increases for Asia-Europe routes, pushing some buyers toward European or Turkish suppliers. Sors: Ġurnal tal-Kummerċ, .
Riskji tal-Munita u tal-Ħlas: B2B transactions in this sector typically involve wire transfers (T/T) ma 30% deposit and 70% balance against shipping documents or L/C at sight for larger orders. Currency fluctuations between USD, EUR, and CNY can impact landed costs by 3–8% over a procurement cycle.
Precision CNC machining center producing metal components similar to twin screw extruder elements manufacturing process
Geographic and Policy Advantages in Trade
The trade corridor offers distinct advantages for B2B buyers of industrial components:
Allinjament Regolatorju: Both the US and EU maintain high standards for industrial equipment safety and material compliance. Components manufactured to EU standards (marka CE, ATEX for explosive atmospheres) are generally accepted in the US market with minimal additional certification. This regulatory compatibility reduces compliance costs for manufacturers serving both markets.
Infrastruttura tal-Port: Major ports including Rotterdam (Europe's largest), Hamburg, Antwerp-Bruges, Los Angeles/Long Beach, and Savannah provide efficient handling of containerized industrial components. Rotterdam's Europoort complex handles over 14 million TEUs annually and offers direct connections to Europe's inland waterway network, enabling cost-effective distribution to manufacturing clusters in Germany, Belgium, and the Netherlands. Sors: Awtorità tal-Port ta' Rotterdam, 2024.
Żoni ta' Kummerċ Ħieles u Bonded Warehousing: Kemm l-Istati Uniti (Żoni ta' Kummerċ Barrani) u jien (Żoni Ħieles) offer duty deferral and reduction mechanisms that benefit importers of extruder components. Manufacturers establishing bonded warehouses in key markets can offer local stock availability while optimizing duty payments.
Trade Finance Infrastructure: The mature banking systems in both the US and EU provide reliable trade finance instruments including letters of credit, assigurazzjoni ta' kreditu għall-esportazzjoni (through agencies like Euler Hermes, EXIM Bank), and supply chain financing programs that reduce payment risk for both buyers and sellers.
Case Studies Success in the Extruder Elements Market
Studju ta' Każ 1: Chinese Manufacturer Establishing EU Distribution
A Nanjing-based twin screw extruder elements manufacturer with annual revenue of approximately USD 15 million recognized that European buyers were hesitant to order directly from China due to long lead times and quality concerns. Fil 2023, the company established a warehouse in Duisburg, il-Ġermanja — Europe's largest inland port and a key logistics hub on the Belt and Road rail corridor. By maintaining stock of 200+ common screw element Pelletizing Factory specifications (for Coperion ZSK, Leistritz ZSE, and KraussMaffei ZE series compatibility), they reduced delivery time from 35–45 days to 3–5 business days for EU customers. The company invested in EN 10204 3.1 material certification for all stocked items and hired a German-speaking technical sales engineer. Result: EU revenue grew 180% fi 18 xhur, with key accounts including compounders in Germany, l-Italja, and Poland.
Studju ta' Każ 2: US Compounder Implementing Dual-Source Strategy
A mid-size plastics compounder in Texas operating 12 twin screw extruder lines (mix of Coperion and Leistritz machines) was spending approximately USD 400,000 annually on OEM replacement elements. After qualifying two alternative suppliers — one in Nanjing, Iċ-Ċina, and one in Ahmedabad, l-Indja — the company reduced its annual spend to USD 220,000 while maintaining processing quality. The qualification process involved: Plastic Pellets Extruder (1) requesting sample elements with full material certificates, (2) conducting independent hardness and dimensional testing at a local metallurgical lab, (3) running 500-hour production trials on non-critical lines, u (4) gradually expanding to all lines over 6 xhur. The dual-source approach also provided supply chain resilience when the Chinese supplier experienced a 3-week shipping delay due to port congestion.
Studju ta' Każ 3: European OEM Partnering with Specialized Element Manufacturer
A mid-tier European extruder OEM based in Italy, producing approximately 80 twin screw extruder lines annually, transitioned from in-house screw element production to a partnership model with a specialized manufacturer. By outsourcing element production to a dedicated facility with advanced CNC grinding capabilities and PM-HIP material processing, the OEM reduced its manufacturing footprint, improved element quality consistency, and shortened delivery times for custom screw configurations. The partnership model allowed the OEM to focus on machine design, assemblaġġ, and customer application engineering while the element manufacturer handled the metallurgy-intensive production. This approach is increasingly common in the industry, as reported by Plastics Illum, 2024.
Business professionals in a B2B trade negotiation meeting discussing industrial component sourcing strategies
Trade Show and Industry Event Landscape
B2B buyers and manufacturers of twin screw extruder elements connect at several key industry events:
- K Trade Fair (Düsseldorf, il-Ġermanja): The world's largest plastics trade show, miżmuma kull tliet snin (edizzjoni li jmiss: Ottubru ). All major extruder OEMs and many element manufacturers exhibit. Essential for supplier discovery and technology benchmarking.
- ISEM (Orlando, USA): North America's largest plastics show, miżmuma kull tliet snin. Il- 2024 edition attracted over 50,000 visitors and featured extensive extrusion technology exhibits.
- Chinaplas (Shenzhen/Shanghai, alternating): Asia's largest plastics show, with strong representation from Chinese extruder element manufacturers. The edition in Shenzhen featured over 4,000 exhibitors.
- Fakuma (Friedrichshafen, il-Ġermanja): Annual European plastics show with strong extrusion technology focus, scheduled for October.
These events provide opportunities for hands-on quality assessment, face-to-face negotiation, and relationship building that are critical in the B2B industrial components trade. Sors: Messe Düsseldorf, .
Material Science and Technical Considerations for Buyers
Selecting the right twin screw extruder elements manufacturer requires understanding the technical specifications that impact performance and longevity:
Common Metallurgies for Screw Elements
- Nitrided Steel (eż., 1.8550 / 34CrAlNi7): The standard material for general-purpose compounding. Surface hardness of 900–1100 HV, nitriding depth of 0.3–0.7mm. Cost-effective but limited wear life in abrasive applications.
- Through-Hardened Tool Steel (eż., D2, CPM-9V): Higher bulk hardness (58–62 HRC) provides better resistance to abrasive wear from glass fiber and mineral fillers.
- PM-HIP Materials (eż., CPM-10V, Vancron 40): Powder metallurgy steels processed by hot isostatic pressing offer exceptional wear resistance (3–5x nitrided steel) with good toughness. Increasingly specified for high-fill compounds and recycling applications.
- Tungsten Carbide (WC/Co): The ultimate wear-resistant option for extremely abrasive applications. Typically applied as a coating or used in solid form for specific element types. Cost is 5–10x nitrided steel.
- Stellite and Colmonoy Coatings: Cobalt-based and nickel-based hard-facing alloys applied by welding or thermal spray for corrosion-resistant applications in chemical and pharmaceutical processing.
Buyers should request material test certificates (chemical composition, hardness profiles, microstructure images) and specify acceptance criteria in purchase orders. Reputable manufacturers welcome these requirements as they demonstrate quality commitment.
Advanced metallurgical testing and quality control equipment used in precision manufacturing of industrial components
Workplace Safety: Ħarsien tal-Ħaddiema f'Ambjenti tal-Manifattura tal-Estrużjoni
The twin screw extrusion industry presents significant workplace safety challenges that B2B operators must address. Extrusion facilities involve heavy machinery, high temperatures (barrel temperatures typically range from 150°C to 350°Ċ), tagħmir li jdur, and handling of raw materials including abrasive fillers and chemical additives. Worker safety — particularly foot protection — is a critical operational requirement.
Why Safety Footwear Is Essential in Extrusion Plants
Extrusion manufacturing environments expose workers to multiple foot injury hazards:
- Impatt Oġġett Tqil: Twin screw extruder elements — individual screw segments, sezzjonijiet tal-kanna, and die plates — can weigh from 2 kg to over 50 kg. A dropped screw element or barrel segment can cause severe crush injuries to unprotected feet. OSHA reports that foot injuries account for approximately 60,000 korrimenti fuq il-post tax-xogħol kull sena fil-manifattura tal-Istati Uniti, b'medja ta' 7 ġranet tax-xogħol mitlufa għal kull inċident. Sors: OSHA, 2024.
- Compression Hazards: During extruder assembly and maintenance, workers position heavy components using overhead cranes and hoists. Misalignment or equipment failure can result in compression injuries to feet positioned near the assembly area.
- Puncture Risks: Extrusion facilities often have metal shavings, broken screw element fragments, wire, and fasteners on the floor. Standard footwear provides no protection against puncture wounds from these sharp objects.
- Thermal Hazards: Molten polymer drips, hot purge material, and contact with heated barrel surfaces can cause severe burns. Heat-resistant safety footwear with appropriate sole ratings is essential for workers operating near the extrusion die and downstream equipment.
- Perikli ta' Żlieq: Pellets tal-polimeru, żjut għall-ipproċessar, and cleaning solvents create slippery floor conditions. Anti-slip safety footwear with SRC-rated soles (tested on both ceramic tile with sodium lauryl sulfate and steel with glycerol) significantly reduces slip-and-fall incidents.
- Perikli Elettriku: Extruder drive motors, meded tal-ħiters, and control systems present electrical shock risks. ESD (electrostatic dissipative) or EH (periklu elettriku) rated safety footwear provides an additional layer of protection.
Safety Footwear Standards and Certifications
B2B buyers sourcing safety footwear for extrusion plant workers should understand the applicable standards:
- FL-ISO 20345 (Standard tal-UE): Defines safety footwear with toe protection capable of withstanding 200J impact and 15kN compression. Classes include S1 (antistatiku, energy absorption at heel), S1P (adds puncture resistance), S3 (adds water resistance and profiled outsole), and the newer S5 (waterproof boot with puncture resistance).
- ASTM F2413 (Standard tal-Istati Uniti): Specifies performance requirements for protective footwear including impact resistance (I/75 = 75 ft-lbs), reżistenza għall-kompressjoni (C/75 = 2,500 lbs), protezzjoni metatarsali (Mt/75), and electrical hazard protection (EH).
- Kompost vs. Tappijiet tat-Toe tal-Azzar: Żraben tas-sigurtà moderni dejjem aktar juża kompost (fibreglass, fibra tal-karbonju, jew Kevlar) toe caps instead of steel. Composite toes are lighter (30–40% weight reduction), mhux metalliċi (no cold transfer, airport-friendly), and meet the same impact/compression standards. For extrusion plant environments where workers stand for 8–12 xiftijiet ta’ siegħa, the weight reduction significantly improves comfort and reduces fatigue.
B2B Sourcing of Safety Footwear for Industrial Operations
For B2B operators managing extrusion facilities, safety footwear procurement should be approached strategically:
Volume Purchasing: Facilities with 50+ workers can negotiate significant volume discounts (typically 15–30% below retail) by working directly with safety footwear manufacturers or authorized distributors. Annual replacement programs ensure workers always have footwear in good condition.
Application-Specific Selection: Different roles within an extrusion plant require different protection levels. Machine operators working near the extruder barrel need heat-resistant soles (HRO stmat għal 300°C contact heat). Maintenance technicians require metatarsal protection and puncture resistance. Warehouse staff handling raw materials and finished goods need impact protection and anti-slip soles. A tiered specification approach optimizes both protection and cost.
Comfort and Compliance: The most protective safety footwear is useless if workers refuse to wear it. Modern safety footwear from manufacturers like Uvex, Sigurtà Puma, Timberland PRO, Red Wing, and KEEN Utility combines protection with athletic shoe comfort features including EVA midsoles, moisture-wicking linings, and ergonomic footbeds. Investing in comfortable safety footwear improves compliance rates from typical 70–80% għal fuq 95%, directly reducing injury incidents.
Spiża Totali tas-Sjieda: Premium safety footwear costing USD 120–180 per pair with a 12-month service life is more cost-effective than budget options at USD 40–60 that require replacement every 4–6 xhur. The total cost including procurement, fitting, and disposal favors quality products. Barra minn hekk, each prevented foot injury saves an estimated USD 9,000–15,000 in direct medical costs and lost productivity, according to the National Safety Council. Sors: Kunsill Nazzjonali tas-Sigurtà, 2024.
Complete Extrusion Systems Factory Industrial safety boots with steel toe protection used in manufacturing and extrusion plant environments Amazon Extruder Screw
Future Trade Trends: X'għandek tistenna fil-Li jmiss 1-2 Xhur (Lulju–Awissu )
Ibbażat fuq indikaturi tas-suq kurrenti, żviluppi politiċi, u sinjali tal-industrija, several trends are likely to shape the twin screw extruder elements trade in the near term:
1. Tariff Uncertainty Will Drive Inventory Building: With ongoing US tariff policy volatility, B2B buyers are expected to increase safety stock levels of critical extruder components. Manufacturers with US and EU warehouse capabilities will see increased demand. Chinese manufacturers offering DDP (Dazju Mħallas Konsenjat) pricing to US destinations will gain competitive advantage by absorbing tariff complexity for buyers.
2. Sustainability Requirements Will Intensify: EU buyers are increasingly requesting carbon footprint data for purchased components. The CBAM reporting requirements, while not yet directly covering machinery components, are creating a culture of emissions transparency that extends through supply chains. Manufacturers providing EPD (Environmental Product Declarations) or carbon footprint calculations for their products will differentiate themselves. The recycling sector's growth — driven by EU packaging regulations mandating 30% kontenut riċiklat minn 2030 — will increase demand for wear-resistant screw elements optimized for processing contaminated post-consumer waste streams.
3D Extruder Radiator 3. L-Akkwist Diġitali Se Jaċċellera: B2B platforms are becoming more sophisticated in handling technical industrial components. Expect to see more twin screw extruder element manufacturers offering online configurators where buyers can select element type, daqs, materjal, and quantity with instant pricing. This reduces the traditional quote-negotiate-order cycle from 1–2 weeks to minutes, particularly for standard specifications.
4. Nearshoring Momentum in Europe: The combination of Red Sea shipping disruptions, rising Chinese labor costs, and EU supply chain due diligence regulations (the Corporate Sustainability Due Diligence Directive, effective 2026) will continue to push European buyers toward Turkish, Eastern European, and Indian suppliers. Turkey's proximity to EU markets (3–5 day shipping to major EU ports) and its customs union with the EU make it particularly attractive. Power Heater Extruder
5. Consolidation Among Manufacturers: The twin screw extruder elements manufacturing sector remains fragmented, partikolarment fiċ-Ċina. Expect continued consolidation as larger manufacturers acquire smaller competitors to gain capacity, technology, and customer relationships. This consolidation will ultimately benefit B2B buyers through improved quality consistency and financial stability of suppliers.
Aluminum Extruders Tennessee 6. Advanced Coating Technologies: PVD (Depożizzjoni Fiżika tal-Fwar) and CVD (Chemical Vapor Deposition) coatings for screw elements are moving from laboratory to commercial availability. These coatings — including TiAlN, CrN, and DLC (Diamond-Like Carbon) — can extend element life by 2–4x Tornado Extruder Kit in specific applications. Manufacturers investing in coating capabilities will capture premium market segments. Sors: Plastics Illum, ; ITA Market Intelligence, .

Modern warehouse and logistics facility for B2B industrial component distribution and wholesale operations
Practical Sourcing Guide: How to Select a Twin Screw Extruder Elements Manufacturer
Fornitur tal-Pelletizer taħt l-ilma For B2B buyers evaluating potential suppliers, il-qafas li ġej jipprovdi approċċ strutturat:
Pass 1: Define Technical Requirements
Document your extruder model, element specifications (OD, ID, length, profile type), material requirements, quantity, and delivery schedule. Include tolerance requirements and surface finish specifications. The more precise your specification, the more accurate and comparable the quotes you receive.
Pass 2: Identify Potential Suppliers
Use multiple channels platforms (Alibaba, Magħmul fiċ-Ċina, ThomasNet for US suppliers, Europages for EU suppliers), trade show exhibitor lists (K Uri, Chinaplas, ISEM), industry referrals, and direct Google searches for "twin screw extruder elements factory" with geographic qualifiers.
Pass 3: Initial Qualification
Request company profiles, production capability presentations, customer reference lists, and quality certifications (ISO 9001 minimu, ISO 14001 preferred). Evaluate response time and communication quality as indicators of service capability.
Pass 4: Sample and Test
Order sample elements (typically 2–5 biċċiet) with full material certificates. Conduct independent testing: spezzjoni dimensjonali (Kejl tas-CMM), hardness testing (surface and cross-section), and if possible, metallographic examination. Compare results against specifications and OEM benchmarks.
Pass 5: Trial Production Run
Install qualified sample elements on a non-critical extruder line and run for a defined period (typically 500–1000 sigħat). Monitor processing parameters, kwalità tal-prodott, and element wear. Document results for comparison with incumbent supplier performance.
Pass 6: Negotiate and Formalize
Based on successful trials, negotiate pricing (consider volume tiers, annual contracts, and consignment stock arrangements), termini ta' ħlas, warranty conditions, and quality assurance protocols. Formalize the relationship with a supply agreement that includes quality specifications, delivery requirements, u mekkaniżmi ta' riżoluzzjoni tat-tilwim.
Mistoqsijiet Frekwenti (FAQ)
- What materials are commonly used for twin screw extruder elements?
- The most common materials include nitrided steel (34CrAlNi7/1.8550), through-hardened tool steels (D2, CPM-9V), powder metallurgy HIP materials (CPM-10V, Vancron 40), and tungsten carbide for extreme wear applications. Material selection depends on the processed material's abrasiveness, corrosiveness, and processing temperature. A qualified manufacturer will recommend the optimal metallurgy based on your specific application.
- What is the typical lead time for custom twin screw extruder elements?
- Lead times vary by manufacturer and order complexity. Chinese manufacturers typically quote 3–5 weeks for standard specifications and 5–8 weeks for custom or PM-HIP materials. European manufacturers quote 4–8 weeks for standard and 8–12 weeks for specialized materials. Manufacturers maintaining warehouse stock of common sizes can ship within 1–5