

Schlëssel Takeaways
- A menger Erfahrung, déi schlau Grousshandel Décisiounen ufänken mat passende Maschinn Klass ze feedstock: Single Schraube extruders handhaben direkt PVC, HDPE, an polypropylene Profiler, Zwillingsschraufextruder passen d'Kompositioun an d'Ufuerderung vu Polymeren, an engagéierten Plastik Recycling extruders existéieren als z'ënnerscheedde Klass fir reclaimed Plastik flake (Quell: ThoYu, 2024).
- Ech evaluéieren ëmmer Spezifikatioune virum Präis. Kär Zuelen wéi de L / D Verhältnis, Faass Zone zielen, gearbox Reduktioun Verhältnis, Service Faktor, an Motor horsepower soen Iech vill méi iwwer real Kapazitéit wéi eng Iwwerschrëft Ausgang Figur. Fir Referenz, engem benotzt Davis Standard 9-Zoll extruder Puer a 32:1 L/D Verhältnis an 7-Zone Faass mat engem 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung).
- Factory-direkt Präisser vu China-baséiert Hiersteller ass wierklech kompetitiv fir nei Ausrüstung (Quell: ThoYu, 2024), mee ech weien et géint eng voll Ganzen Käschte vum Besëtz Bild datt Import Flichten enthält, Ozean Gidderween, rigging, Installatioun, an no-Ofsaz Ënnerstëtzung Zougang.
- Ech behandelen nei, benotzt, an als dräi getrennte Beschaffungsspuren importéiert, jidderee mat sengen eegenen Ausgläich. De Occasiounsmaart ass reift, Mark-spezifesch Opféierungen fir Single screw extruders (Quell: Aaron Equipement), wat mécht et e liewensfäeg Wee wann ech Zoustand a Verschleiung verifizéiere kann.
- Fournisseur Vetting a Bezuelungsschutz si sou vill wéi d'Spezifikatiounsblat. Ier Dir engagéiert, Ech confirméieren Minimum Bestellung Quantitéit, Leadzäiten, Garantiebedéngungen, an Ersatzdeeler Disponibilitéit, an ech strukturéieren Bezuelen géint Net-Liwwerung ze schützen.
- Prozess Fundamenter Guide meng Schecken: Matière première geet duerch en Hopper Feeder a Pulver, pellet, oder Granulatform, gëtt duerch elektresch Heizréier geschmollt, a gëtt duerch Schrauberschéier homogeniséiert, ier den Extrusiounsstierf e kontinuéierleche Querschnittsprofil formt (Quellen: ThoYu; Amade-Tech).
- Ech confirméieren thermesch Gestioun virun. Multi-Zone Fässer kombinéieren typesch elektresch Heizung mat zougemaach Waasserkühlen (Quell: Aaron Ausrüstung Spez), an zouverlässeg Schmelztemperaturkontrolle ass wat d'Ausgab dimensionell konsequent iwwer Päifen hält, Réier, Filmer, Brieder, an Fläschen.
- Schrauwen Konfiguratioun a personaliséiert Stierf Tooling definéieren wat eng Linn tatsächlech ka maachen, also ech moossen déi géint meng Produktmix anstatt generesch Kapazitéit ze kafen. Fir R&D oder kleng leeft, e Labo-Skala Extruder gebaut fir kontinuéierlech eenheetlech Querschnittausgang ass dacks de richtegen Entréespunkt (Quell: Amade-Tech).
Wat ass eng Plastiksextrusiounsmaschinn a wéi funktionnéiert et?
Wann ech all Polymer Veraarbechtung Maschinn bewäerten, Ech fänken un mam selwechte mentale Modell: en Extruder ass e kontrolléierte Schmelz-a-Formungssystem. Fest Plastik geet an engem Enn, an eng kontinuéierlech, eenheetlech Querschnëtt Profil kënnt eraus déi aner. Alles tëscht deenen zwee Punkte geet ëm d'Uwendung vun Hëtzt a mechanescher Schéier zum richtegen Taux. Dee Flux ze verstoen ass wat e zouversiichtleche Keefer trennt vun engem deen op Spezifeschblieder roden, an et formt direkt wéi ech un eng Plastic Extrusion Machine Grousshandel kafen.
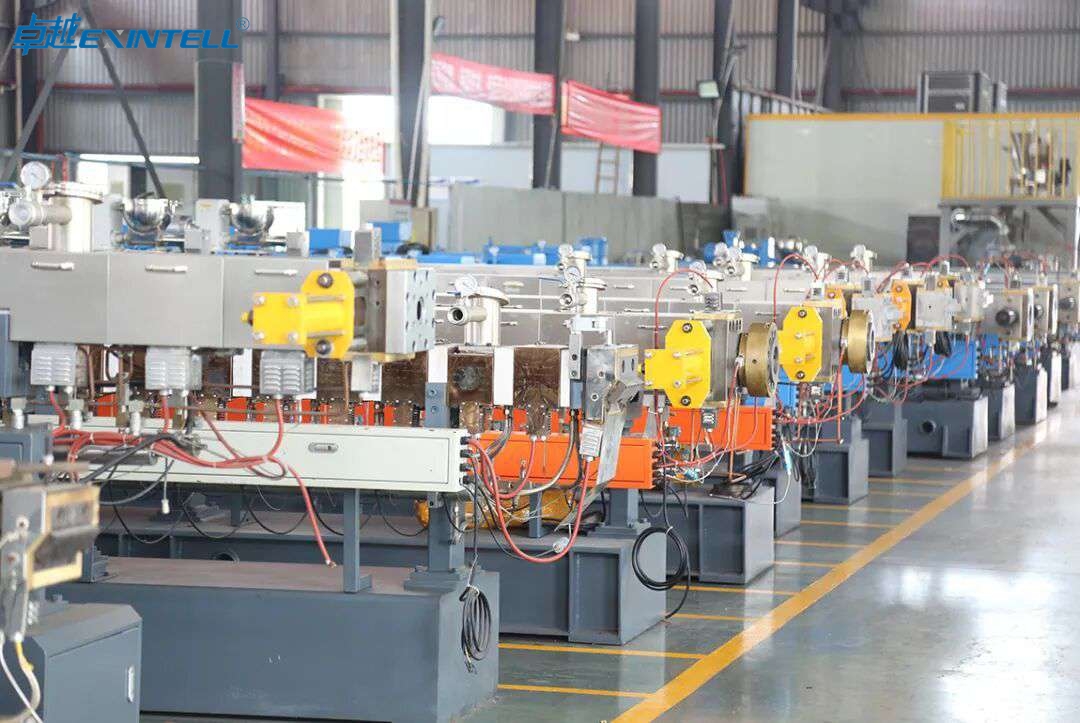
De Kär Schmelzprozess
Bannen an der Maschinn, zolidd Plastik gëtt duerch eng rotéierend Schraube weidergeleet, während elektresch Heizréier de Faass a verschidde Zonen wéckelen. De Plastik schmëlzt duerch eng Kombinatioun vun där externer Hëtzt an der interner Schéier generéiert wéi d'Schraube Material géint d'Fassmauer zwéngt. Laut ThoYu, Plastik an engem Extruder gëtt duerch elektresch Heizréier geschmolt an an eng eenheetlech Schmelz ëmgewandelt duerch Schrauwenextrusioun a Schéieraktioun (ThoYu, 2024). Dat duebel Mechanismus, konduktiv Hëtzt plus mechanesch Reibung, dofir ass d'Schraubegeometrie sou wichteg wéi d'Taasstemperatur.
Schmelztemperaturkontrolle ass deen Deel deen ech am meeschten an all Zitat ënnersicht. Multi-Zone Fässer paréieren allgemeng elektresch Heizung mat zougemaach Waasserkühlung fir all Zone an enger schmueler Band ze halen (Aaron Equipement Spezifizéierung). Wann e Faass net esou präzis killt wéi et erhëtzt, Dir verléiert d'Fäegkeet fir Hëtztempfindlech Harze propper ze lafen.
Feedstock Formen Dir kënnt lafen
D'Material dat Dir fiddert formt d'Maschinn déi Dir kaaft. An der Praxis gesinn ech véier gemeinsame Fudderformen:
- Pellets - de Standard fir virgin Harz, einfach ze mëschen a schmëlzen
- Granules - e bësse méi grober, heefeg a komponéiert Linnen
- Pudder - typesch fir PVC dréchen Mëschungen a Labo-Skala Aarbecht
- Recycléiert Flak - erëmgewielt Material mat variabelen Bulk Dicht
Amade-Tech stellt fest, datt Labo Plastiksextrusiounsmaschinne Veraarbechtungsmaterial a Pudder veraarbecht, pellet, oder Granuleform fir kontinuéierlech Polymerprodukter mat eenheetleche Querschnitt ze produzéieren (Amade-Tech, 2024). Eng Hopper-montéiert Fütterschraube liwwert dann dat Rohmaterial gläichméisseg an de Fass (ThoYu, 2024). Och d'Ernährung ass kee klengen Detail; inkonsistent Hopper Liwwerung weist sech als Iwwerschwemmungslinnen an Dimensiounsdrift am fäerdege Profil.
Wéi de Die Formen d'Output
D'Extrusiounsstierf ass dat lescht Tool dat d'Schmelz duerchgeet, an et definéiert de Produit Kräiz-Sektioun. Päifen, Réier, Filmer, Brieder, a Fläschen kommen all aus dem selwechte Faass mat verschiddene Stierwen (Amade-Tech, 2024). Well de Stierwen eng kontinuéierlech Querschnittsprofil produzéiert, eng Maschinn kann e puer Produit Linnen déngen wann Dir an Mooss stierwen tooling investéiert. Dat Tooling Flexibilitéit ass ee Grond firwat ech stierwen Inventar als Deel vun der totaler Kafentscheedung behandelen anstatt en Nodenken.
Kär Komponente ech Inspektéieren op all Maschinn
Ob ech iwwerschaffen en industrielle extruder fir Verkaf oder eng benotzt Eenheet, Ech Spadséiergank duerch déi selwecht Komponent Checklëscht:
- Faass - den erhëtzten Zylinder, Idealerweis Multi-Zone mat zougemaach-Loop Ofkillung
- Schrauwen - d'Häerz vu Schmelzen a Vermëttelen; Schraubekonfiguratioun bestëmmt Ausgangsqualitéit
- Motor - extruder Motor horsepower setzt Är Débit Plafong
- Gearbox - de Reduktiounsverhältnis an de Servicefaktor definéieren benotzbaren Dréimoment
- Kontrollen - Schmelztemperaturkontroll a Zonemanagement
- Stierwen - de Profilbildungsinstrument
Zwee Spezifikatioune verankert dës Evaluatioun. Éischten, L/D Verhältnis, der barrel Längt gedeelt duerch Schrauwen Duerchmiesser, seet mir wéi vill Residenz Zäit d'Schmelz kritt; engem benotzt Davis Standard 9-Zoll extruder (Modell 80IN80HT) agebaut 2001 paren a 32:1 L/D Verhältnis mat engem 7-Zone Faass an engem 900 HP DC Motor (Aaron Ausrüstung Oplëschtung). Zweeten, d'Gearbox Reduktiounsverhältnis an de Servicefaktor definéieren Dréimoment Liwwerung; industriell Unitéiten allgemeng Lëscht Verhältnisser wéi 10.15:1 mat engem Service Faktor vun 1.5 (Aaron Equipement). Dës Zuelen iwwersetzen direkt an wéi schwéier Dir viskos Materialien wéi HDPE oder gefëllte Verbindungen drécke kënnt ouni ze stéieren.
Firwat Kafen Plastik Extrusion Maschinnen Grousshandel?
D'Grousshandelsroute ass wou d'Beschaffungsstrategie säi Bestand verdéngt. A menger Erfahrung, den Ënnerscheed tëscht Retail an Fabréck-direkt Akeef ass selten e klenge Prozentsaz; et reshapes d'Wirtschaft vun enger ganzer extrusion Produktioun Linn. Drënner zerbriechen ech déi véier Grënn, déi ech konsequent recommandéieren Bulk Extrusiounsausrüstung duerch Grousshandelkanäl ze kafen.
Käschtespueren op Bulk a Factory-Direkt Bestellungen
Factory-direkt Präisser läscht d'Schichten vum Distributeur Markup, déi e Plastiksextruder Maschinn Präis opbléien. China-baséiert Hiersteller, zum Beispill, Offer Fabréck-direkt Grousshandel Präisser op Plastik extruders (ThoYu, 2024), dat ass firwat sou vill Präis-Zesummenhang Sich Absicht Richtung iwwerséiesch Fournisseuren weist. Wann ech vergläichen eng eenzeg Retail Eenheet géint eng bulk Bestellung vun engem Grousshandel Maschinnen Fournisseur, d'Käschte pro Maschinn fällt typesch genuch fir d'Payback Berechnung op de ganze Projet z'änneren. Dat gesot, Fabréck direkt Präisser bezilt nëmme wann Dir d'Gesamtkäschte vum Besëtz berücksichtegt, e Spalt ech spéider an dësem Guide Adress.
Zougang zu OEM an ODM Personnalisatioun
Grousshandel Bezéiungen maachen d'Dier op fir OEM an ODM Personnalisatioun déi Retail Channels selten ubidden. Amplaz vun engem Akzeptanz vun engem Stock Configuratioun, Ech kann Schrauwen Längt uginn, barrel Zonen, Kontroll Packages, a personaliséiert Stierf Tooling passend mat mengem Produkt. Fir jiddereen eng spezialiséiert kontinuéierlech Querschnitt Profil Lafen, dëst ass déi eenzeg stäerkste Argument fir eng kafen aus engem extrusion Maschinn Fabrikant beschwéiert direkt anstatt engem reseller.
Besser Konditioune fir Tooling an Ersatzdeeler
De Stierwen an Ersatzdeeler Gespréich ass wou Grousshandel Begrëffer roueg an Ärem Gonschten zesummesetzen. Verhandlungsinstrumenter an e Ersatzdeeler Package an der ursprénglecher Uerdnung schléit bal ëmmer se e bësse méi spéit. Ech behandelen Kleederartikelen, Schrauwen, Heizung Bands, an barrel liners, als Deel vum initialen Kontrakt, an ech drécke fir no-Ofsaz Ënnerstëtzung Engagementer schrëftlech. Staark After-Sales Ënnerstëtzung ass wat eng Linn hält; ouni et, eng bëlleg Maschinn gëtt en deier Flaschenhals.
Skaléieren Produktiounskapazitéit effizient
Endlech, Grousshandel Kaaf léisst mech d'Extruder Kapazitéit Output skala ouni de ganzen Akaafszyklus all Kéier ze widderhuelen. Standardiséierung op der Plattform vun engem Fournisseur bedeit konsequent Ersatzdeeler, kennt Kontrollen, a widderhuelend Bedreiwer Training iwwer verschidde Maschinnen. Wann d'Nofro wiisst, eng zweet oder drëtt identesch Eenheet bäizefügen ass vill méi glat wéi d'Integratioun vun onpassend Ausrüstung vu verschiddene Verkeefer.
Zorte vu Plastik Extruders: Single Screw vs Zwilling Schrauwen
Wiel tëscht engem eenzege Schrauwen Extruder an engem Zwilling Schrauwen Extruder ass déi konsequent technesch Entscheedung bei engem Grousshandel Kaf. Ech cadreieren et einfach: eenzeg Schraube Maschinnen vermëttelen a schmëlzen effizient, iwwerdeems Zwilling Schrauwen Maschinnen Mix a Verbindung. Gitt dëse Match richteg an de Rescht vun der Spezifizéierung fällt op Plaz.
Single Screw Extruders
Den eenzege Schraube-Extruder ass d'Aarbechtspäerd fir Standardprofile zu méi niddrege Käschten. Et exceléiert beim Schmelzen vu virgine Harz an dréckt et duerch e Stierf mat enger konstanter Ausgang, wat mécht et ideal fir Päifen, Réier, an einfach kontinuéierlech Profiler. Et ass och déi allgemeng benotzt Ausrüstungskategorie, mat Mark-spezifesche Resale Lëschte wäit verfügbar (Aaron Equipement). Wann Är Produktlinn konsequent Materialien wéi HDPE oder Polypropylen duerch e fixe Stierf leeft, eng eenzeg Schraube Maschinn liwwert normalerweis de beschte Wäert pro Ausgangsunitéit.
Zwilling Screw Extruders
Den Zwillingsschraube-Extruder verdéngt seng méi héich Käschten duerch Vermëschungsfäegkeet. Zwee intermeshing Schrauwen generéieren déi verdeelend an dispersiv Mëschung déi néideg ass fir d'Verbindung, addéieren Filler, Faarfstoffer, an Stabilisatoren, a fir d'Veraarbechtung vu recycléiertem Material mat variabelen Eegeschaften. Wann ech mat recycléiertem Plastikflake oder Hëtztempfindlechen Ingenieurspolymerer wéi PEEK schaffen, the twin screw’s superior control over shear and residence time is decisive. It is worth noting that recycling extruders are a distinct machine class built specifically for reclaimed feedstock (ThoYu, 2024), and many of those lines rely on twin screw designs for exactly this reason.
Output Rate and Material Compatibility
The two types diverge sharply on output behavior and material fit. Single screw output is largely a function of screw speed and motor horsepower, making it predictable for a single resin. Twin screw output is more flexible across formulations but is often optimized for compounding quality rather than raw throughput. Materials like PVC dry blends and recycled flake benefit from twin screw handling, while a clean single resin runs economically on a single screw.
Single Screw vs Zwilling Schrauwen: Verglach Table
|
Faktor |
Single Screw Extruder |
Zwilling Screw Extruder |
|---|---|---|
|
Primary strength |
Melting and conveying standard profiles |
Vermëschen, Zesummesetzung, an devolatilization |
|
Relative cost |
Ënneschten |
Méi héich |
|
Best materials |
HDPE, polypropylene, single virgin resins |
PVC dry blends, recycled flake, filled or PEEK compounds |
|
Mëschung Qualitéit |
Limitéiert |
exzellent (distributive and dispersive) |
|
Typesch Produkter |
Päifen, Réier, simple profiles |
Verbindungen, masterbatch, recycled pellet |
|
Used-market availability |
Breet, brand-specific listings common |
Narrower, more specialized |
|
Ideal buyer |
Fixed product line, cost-focused |
Recycling, custom formulations, R&D |
|
Faktor |
Single Screw Extruder |
Zwilling Screw Extruder |
|---|---|---|
|
Primary strength |
Melting and conveying standard profiles |
Vermëschen, Zesummesetzung, an devolatilization |
|
Relative cost |
Ënneschten |
Méi héich |
|
Best materials |
HDPE, polypropylene, single virgin resins |
PVC dry blends, recycled flake, filled or PEEK compounds |
|
Mëschung Qualitéit |
Limitéiert |
exzellent (distributive and dispersive) |
|
Typesch Produkter |
Päifen, Réier, simple profiles |
Verbindungen, masterbatch, recycled pellet |
|
Used-market availability |
Breet, brand-specific listings common |
Narrower, more specialized |
|
Ideal buyer |
Fixed product line, cost-focused |
Recycling, custom formulations, R&D |
Matching the Type to Your Product Line
My decision rule is straightforward. If I am extruding a consistent material into a stable profile, I choose a single screw machine and put the savings toward custom die tooling and spare parts. If my process involves compounding, Faarf Ännerungen, or a plastic recycling extruder handling reclaimed feedstock, I specify a twin screw platform and accept the higher price as the cost of process control. Fir Keefer déi e Labo-Skala-Extruder fir d'Produktentwécklung weien, déi selwecht Logik gëlt bei méi klengen Output: Match Schraube Typ ob Dir eng Formuléierung beweist (Zwilling) oder e Profil (eenzel). Verankeren d'Schraubentscheedung op Är aktuell Produktlinn, éischter als Iwwerschrëft Präis eleng, ass wat e Grousshandel Akaf iwwer säi ganzt Liewensdauer bezuelt. Dir kënnt real-Welt Konfiguratiounen iwwer Zouliwwerer a Wiederverkaaflëschten iwwerpréiwen, wéi z Aaron Equipment benotzt Single Schraube Inventar an ThoYu Grousshandel Extruder Säiten fir ze kucken wéi dës Spezifikatioune an der Praxis erschéngen.
Wéi vill kascht eng Plastiksextrusiounsmaschinn?
Wann Clienten froen mech fir eng eenzeg Zuel, Ech soen hinnen déi éierlech Äntwert: engem Plastik extrusion Maschinn kascht iwwerall aus e puer dausend Dollar ze gutt iwwer eng Millioun, an d'Verbreedung ass ganz iwwer Skala. A menger Erfahrung Sourcen Ausrüstung iwwer dräi Stäck, d'Präisbänner briechen propper laanscht d'Ausgabkapazitéit, Schrauwen Configuratioun, an den Niveau vun der Automatisatioun Dir braucht. Ier Dir en Devis ufrot, et hëlleft ze wëssen, wéi eng Tierm Dir eigentlech gehéiert, well e Labo-Skala Extruder an eng industriell Extrusiounsproduktiounslinn sinn net deeselwechte Kaf mat engem anere Präis Tag. Si sinn verschidden Maschinnen. Liichtgewiicht recycléierbar Plastiksverpackung
Präisbereich no Skala: Labo, Kleng, an Industrie
Ech Grupp Keefer an dräi praktesch Kategorien. Labo-Skala extruders sinn kompakt, Benchtop oder Buedem Eenheeten gebaut fir R&D, Zesummesetzung Tester, a Material Charakteriséierung. Si veraarbecht Fudder a Pulver, pellet, oder Granuleform fir kontinuéierlech Polymerprodukter mat engem eenheetleche Querschnitt ze produzéieren (Amade-Tech). Kleng kommerziell Unitéiten handhaben niddereg-Volumen Produktioun, Prototyping leeft, an Nischprofil Aarbecht. Industrie Maschinnen fueren voll extrusion Produktioun Linnen fir Päif, film, Verwaltungsrot, a Flaschenausgang ronderëm d'Auer.
Hei ass wéi d'Zuelen typesch landen op Basis vun Zitater déi ech gesammelt hunn an ëffentlechen Oplëschtungen. Behandelt dës als Planungsbereich, net fix Präisser, zanter Schraube Configuratioun an tooling Verréckelung hinnen bedeitend.
| Tier | Typesch Ausgang | Schrauwen Typ | New Präis Range (USD) | Benotzt Präis Range (USD) |
|---|---|---|---|---|
| Labo-Skala extruder | Bis zu ~5 kg/h | Eenzel oder Zwilling Schraube | $8,000 - $45,000 | $4,000 - $25,000 |
| Kleng kommerziell | ~20 - 150 kg/hr | Single screw extruder | $30,000 - $120,000 | $12,000 - $60,000 |
| Industriell Linn | 300 kg/h an op | Eenzel- oder Zwillingsschrauwen Extruder | $150,000 - $1,000,000+ | $50,000 - $400,000 |
Den ieweschten Enn vun der industrieller Band reflektéiert komplette Linnen mat Downstream Ausrüstung wéi Haul-Offs, Killmëttel Panzer, an winders, plus fortgeschratt Schmelze Temperatur Kontroll. E bloe Extruderkop kascht vill manner wéi eng schlësselfäerdeg Linn, also bestätegt ëmmer wat den Zitat tatsächlech enthält ier Dir Verkeefer vergläicht.
Wat sëtzt hannert dem Sticker Präis
Véier Variabelen bewegen d'Zuel méi wéi soss eppes. Kapazitéit ass déi offensichtlech: Duerchgang Skala mat barrel Duerchmiesser a Motor horsepower, a béid addéiere Käschten. Mark wichteg, well eng Maschinn vun engem etabléierten Extrusiounsmaschinn Hiersteller eng Premium dréit, déi un Zouverlässegkeet an Deeler Disponibilitéit gebonnen ass. Conditioun deelt de ganze Maart an nei a benotzt, déi ech ënnen am Detail Cover. An Tooling ass de rouege Budget-Buster. A Mooss stierwen fir eng spezifesch kontinuéierlech Querschnitt Profil kann Zénger vun dausende vun Dollar dobäi, an et gëtt dacks getrennt vun der Maschinn selwer zitéiert.
Verstoppt Käschten Iwwert den Zitat
Den Akafspräis ass selten d'Gesamtkäschte vum Besëtz, an dat ass wou ech gesinn éischte Kéier Keefer verbrannt ginn. Doriwwer eraus der Maschinn, Budget fir dës Linnen:
- Benotzerdefinéiert stierwen Tooling fir all Produktprofil Dir plangt ze lafen.
- Installatioun an rigging fir schwéier industriell Unitéiten, déi dacks Kranservice a verstäerkte Buedem erfuerderen.
- Elektresch an Utility Upgrades fir High-Päerdsmotoren a zougemaach-Loop Faasskühlsystemer ze liwweren.
- Gidderween an, fir Importer, Flichten déi ech an der Logistik Sektioun vun dësem Guide opbriechen.
- Ersatzstécker wéi Ersatzschrauwen, Fässer, an Heizung Bands.
- Kommissioun an Bedreiwer Training, besonnesch fir automatiséiert Kontrollsystemer.
Meng Fauschtregel: dobäizemaachen 15 zu 30 Prozent op d'Maschinn Präis fir déi voll installéiert ze schätzen, Produktioun-prett Käschten. Dës Mathematik iwwersprangen ass den eenzegen heefegsten Planungsfehler deen ech begéinen.
Plastic Extrusion Machine Grousshandel Präis: Wat dréit et?
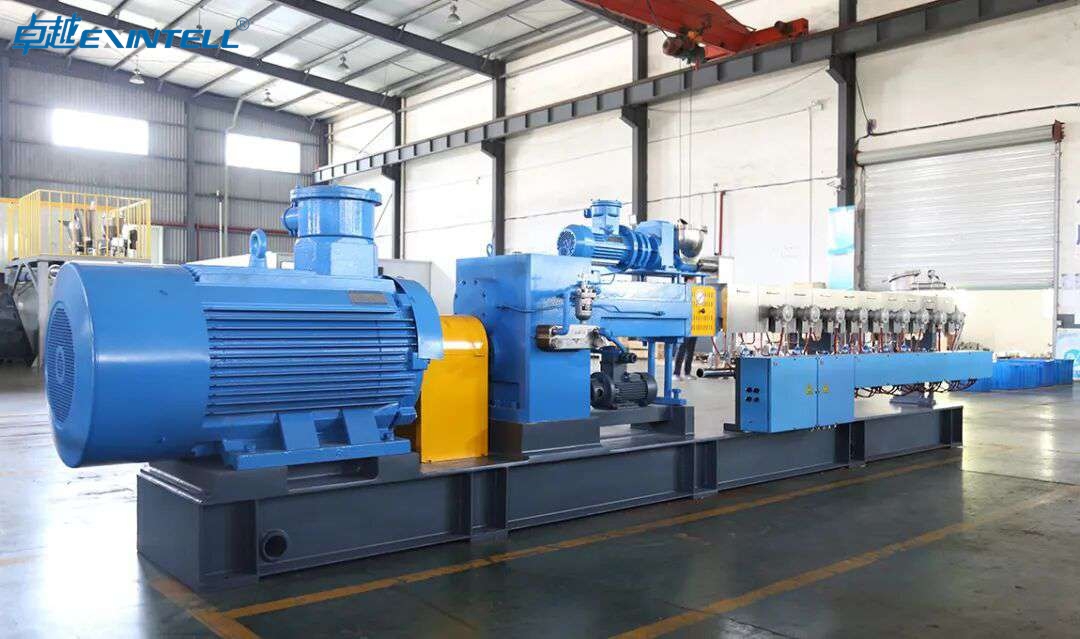
Grousshandel Präisser follegt déi selwecht Logik wéi Retail, awer mat méi Verhandlungsraum a méi Verännerlechen fir ze iwwerpréiwen. Wann ech e Fabréck direkt extruder Präis bewäerten, sief et vun engem Haushändler oder engem China-baséierte Fournisseur deen Grousshandel Tariffer ubitt (ThoYu), Ech schaffen duerch eng konsequent Checklëscht vun Spezifikatioune. Jiddereen huet eng direkt Linn fir Käschten, a se ze verstoen léisst Iech Zitater op gläiche Konditioune vergläichen anstatt ze roden.
Schrauwen a Faass Spezifikatioune
D'Schraube an d'Fass sinn d'Häerz vun der Maschinn, a si definéieren souwuel Fäegkeet a Präis. The most important spec is the L/D ratio, the length-to-diameter ratio of the screw. A higher L/D ratio delivers better mixing and melt uniformity, which matters for demanding polymers. Fir Referenz, engem benotzt Davis Standard 9-Zoll extruder (Modell 80IN80HT) runs a 32:1 L/D ratio with a 7-zone barrel (Aaron Ausrüstung Oplëschtung). More zones mean finer melt temperature control, since plastic is melted by electric heating tubes and converted to a uniform melt through screw shearing (ThoYu).
Screw configuration also decides the machine class. A single screw extruder is the workhorse for straightforward profiles and is the most common used-equipment category (Aaron Equipement). A twin screw extruder costs more but excels at compounding, mixing additives, and processing recycled plastic flake. If you are running PVC, HDPE, or polypropylene at volume, screw geometry should match the resin; PEEK and other high-performance polymers push you toward specialized, higher-cost configurations. Zwilling Screw Extruders Fabrikant
Motor and Gearbox Horsepower
Extruder motor horsepower is a direct proxy for throughput and, therefore, Präis. That same Davis Standard unit pairs its barrel with a 900 HP DC Motor (Aaron Ausrüstung Oplëschtung), which tells you it was built for heavy industrial output. The gearbox translates motor power into usable torque at the screw. Reduction ratios such as 10.15:1 combined with a service factor around 1.5 define how much torque the machine can safely deliver under load (Aaron Equipement). When I compare two similarly priced machines, a higher service factor signals more durability headroom, which is worth paying for on equipment you plan to run hard.
Automation and Control Systems
Control systems separate a basic machine from a modern one. Manual temperature dials and simple relays keep the price down but demand skilled operators and produce more scrap. PLC-driven systems with closed-loop barrel cooling, Rezept Stockage, and data logging cost more upfront but pay back through consistency and lower waste. A hopper feeder with a hopper-mounted feeding screw that delivers raw material evenly into the barrel (ThoYu) is standard, but gravimetric feeding and automated blending add cost and precision. For high-volume operations, I consider automation a value driver rather than a luxury.
Certifications and Origin
Origin and certification shape both price and risk. Domestic and European machines command higher prices, partly for build quality and partly for support proximity. Factory-direct pricing from China-based manufacturers (ThoYu) can cut the machine cost substantially, but you should verify CE marking, UL compliance for the US market, and documented electrical safety before committing. I always ask for certification documents in writing, because retrofitting an uncertified machine to meet US electrical code erases the savings that made the import attractive in the first place.
New vs Used Plastic Extrusion Machines
Dëst ass d'Entscheedung iwwer déi ech am meeschte gefrot ginn, and my answer is always the same: it depends on your risk tolerance and your timeline. Used extrusion equipment can cut capital costs by half or more, but the savings come with real exposure. New machines cost more and often carry longer lead times, yet they arrive with warranties, current controls, and predictable performance. Let me lay out both sides the way I would for a client.
Capital Savings vs Risk on Used Units
The financial case for used equipment is strong. As the pricing table above shows, a used industrial unit can run 40 zu 60 Prozent ënner nei, freeing capital for tooling and downstream equipment. For a startup or a shop testing a new product line, that difference can be the whole business case. The risk is that a polymer processing machine has wear components, screws and barrels degrade, heater bands fail, and motors lose efficiency, and those problems are not always visible in a listing photo. The savings are real, and so is the possibility of buying someone else’s problem.
Inspecting Condition, Hours, and Build Year
I never buy used equipment sight unseen, and I recommend you do not either. My inspection priorities, in order:
- Schrauwen a Faass droen: measure clearances if possible. Excessive clearance kills output and melt quality, and a replacement screw and barrel set is expensive.
- Build year and operating hours: a machine built in 2001, like the Davis Standard example, can still be excellent if maintained, but you need service records to judge.
- Heizung a Killsystemer: confirm all barrel zones heat correctly and that closed-loop water cooling holds temperature.
- Motor and gearbox condition: listen for bearing noise and check for oil leaks and gearbox play.
- Control panel function: verify every zone reads and controls accurately, since older controls may lack replacement parts.
When feasible, insist on a powered demonstration running actual Plastic Pellet Manufacturers Material. A cold machine hides most of its problems.
Warranty and Support Gaps on Used Equipment
The support gap is the cost that does not show on the invoice. New machines from an extrusion machine manufacturer typically include warranty coverage, commissioning help, and access to after-sales support. Used units are usually sold as-is, so you own every failure from day one. Before I buy used, I confirm two things: that spare parts remain available for that model, and that a service technician familiar with the brand can be reached. A cheap machine with no parts pipeline is a liability, net eng Affär.
Resale Value Considerations
Endlech, think about the exit before you enter. Machines from recognized brands hold their value far better on the secondary market, which is exactly why brand-specific resale listings command steady demand (Aaron Equipement). If there is any chance you will resize or exit within a few years, buying a well-known single screw extruder, even at a premium, protects your capital on the way out. A menger Erfahrung, resale strength is the most overlooked factor in the new versus used debate, and it often tips a borderline decision toward the established brand.
My bottom line: buy new when uptime is critical, support matters, and you plan to run the machine for a decade. Buy used when capital is tight, you have the technical capacity to inspect and maintain the equipment, and you stick to reputable brands with living parts supply. Egal wéi, do the total cost of ownership math first, because the quote is only the beginning of the spend.
Quellen: Aaron Equipement, Used Single Screw Extruders; ThoYu, Wholesale Price China Plastic Extruder; Amade-Tech, Lab Plastic Extrusion Machine.
Where to Find Used Plastic Extrusion Machines Wholesale
When I source equipment on a tight capital budget, the used market is usually my first stop. A well-maintained secondhand extruder can deliver 80 zu 90 percent of the service life of a new unit at a fraction of the cost, provided you know how to read a listing and verify condition before wiring any funds. The challenge is not finding machines. It is separating a genuine bargain from a decommissioned liability.
Marketplaces and Dealers Worth Knowing
Most of my used purchases have come through established dealer networks rather than open classified listings. Specialized resellers such as Aaron Equipment maintain rotating inventories of single screw and twin screw extruders, and they photograph, tag, and often power-test each unit before listing it. That vetting matters. A dealer with a physical yard and a reputation to protect gives me recourse that an anonymous marketplace posting never will. I still cross-check auction houses and industry-specific listing boards, but I treat a reputable dealer as the baseline for used extrusion equipment.
Reading a Listing Like an Engineer
A used listing is a spec sheet in disguise, and three numbers tell me most of what I need to know before I ever call. Consider a real example: engem benotzt Davis Standard 9-Zoll extruder (Modell 80IN80HT) agebaut 2001, advertised with a 32:1 L/D Verhältnis, a 7-zone barrel, an a 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung).
- L/D Verhältnis. The barrel length-to-diameter ratio governs residence time and mixing. A 32:1 ratio suits demanding melt homogeneity work; shorter ratios around 24:1 handle simpler profiles. If your polymer needs thorough melting, do not buy short.
- Barrel zones. Seven independently controlled heating zones give me granular melt temperature control across the barrel length. More zones mean finer thermal tuning, which is critical for heat-sensitive resins.
- Motor horsepower. A 900 HP drive signals a high-throughput production machine, not a lab tool. Motor HP scales roughly with output capacity, so match it to your target line speed rather than buying more drive than your die can use.
Listings also disclose the gearbox reduction ratio and service factor, which together define usable torque. A 10.15:1 reduction with a 1.5 Service Faktor, zum Beispill, tells me the drivetrain has headroom for sustained duty (Quell: Aaron Equipement). I read those figures as a durability signal, net eng Foussnot.
Brands That Hold Value on the Resale Market
Brand reputation follows a machine into its second life. Davis Standard, an meng Erfahrung, commands a premium on the resale market precisely because parts, Schrauwen, and service documentation remain available years after manufacture. That liquidity cuts both ways: I pay more up front, but I recover more when I resell, and I spend less time hunting for a replacement extruder screw configuration or barrel liner. When I compare two similar used units, a supported brand almost always wins on total cost of ownership even at a higher sticker price.
Verifying Condition Before You Commit
I never buy a used extruder on photographs alone. My pre-purchase checklist runs through the wear points that quietly drain performance:
- Schrauwen a Faass droen. Request bore measurements. Worn clearances degrade output and pressure stability, and reconditioning a barrel is expensive.
- Heater and thermocouple health. Confirm every zone reaches and holds setpoint. Dead zones on a multi-zone barrel are a red flag.
- Drive and gearbox. Listen for bearing noise and check for oil leaks. A failing gearbox can cost as much as the machine.
- Kühlsystem. Many industrial units use electric heating with closed-loop water cooling (Quell: Aaron Ausrüstung Spez). Verify the cooling circuit is intact and free of scale.
- Run test. Whenever possible, I insist on a powered demonstration under load, not just a cold spin.
If a seller resists an inspection or a run test, I walk. The savings on a used polymer processing machine evaporate the moment you have to rebuild a drivetrain.
Small and Lab-Scale Plastic Extrusion Machines
Not every buyer needs a 900 HP monster. A large share of the search interest around this keyword points toward small and near-me machines, and that tracks with what I see in practice: R&D Équipen, Universitéiten, and startups need compact extruders that fit a lab bench and run on standard power. These machines trade throughput for flexibility, and for the right use case that is exactly the trade you want.
What Lab-Scale Machines Actually Do
A lab-scale extruder processes feedstock in powder, pellet, oder Granuleform fir kontinuéierlech Polymerprodukter mat engem eenheetleche Querschnitt ze produzéieren (Quell: Amade-Tech). The core physics is identical to production equipment: a hopper feeder delivers raw material evenly into the barrel, electric heating tubes melt the polymer, and the screw shears and homogenizes it into a uniform melt before the extrusion die shapes the output (Quell: ThoYu). The difference is scale, not principle, which is what makes lab machines so useful for process development. What you learn at bench scale transfers to production.
Typical Products and Use Cases
I reach for a lab-scale unit in three situations:
- R&D and formulation. Testing new resin blends, Zousätz, or recycled plastic flake without committing a production line.
- Prototyping. Producing sample films, Réier, and small profiles for customer approval or tooling validation.
- Low-volume production. Serving niche markets where demand does not justify a full extrusion production line.
These machines readily handle common thermoplastics like PVC, HDPE, an polypropylene, and higher-spec units extend to engineering polymers such as PEEK when the barrel and screw are rated for the elevated melt temperatures.
Footprint and Power Requirements
The practical appeal of a lab extruder is that it lives in an ordinary room. Many bench units draw single-phase or light three-phase power and occupy a footprint measured in a few square feet, versus the dedicated bay and heavy three-phase service a production extruder demands. Before buying, I confirm two things: the electrical service my facility can supply, and whether the cooling requirement is air or water. Getting the utilities wrong is the most common reason a small machine sits idle after delivery.
Knowing When to Upgrade to Production Scale
A lab machine has a ceiling, and recognizing it early saves money. I plan the jump to production scale when sustained order volume outpaces the machine’s extruder capacity output, when I am running multiple shifts just to keep up, or when per-unit cost on the small line exceeds what a production extruder would deliver. The signal is economic, not emotional: once the lab unit becomes the bottleneck rather than the tool, it is time to scale. I typically keep the lab machine anyway, redeployed for the R&D work it does best.
Lab-Scale vs Production Extruders at a Glance
| Attribut | Labo / Small-Scale Extruder | Production Extruder |
|---|---|---|
| Primary use | R&D, prototyping, low-volume runs | Continuous commercial production |
| Typical motor | Fractional to ~20 HP | 50 zu 900+ HP (z.B., 900 HP Davis Standard) |
| L/D Verhältnis | ~20:1 zu 25:1 | 24:1 zu 32:1 |
| Barrel zones | 2 zu 4 | 5 zu 7+ |
| Power service | Single-phase / light 3-phase | Heavy 3-phase |
| Foussofdrock | Benchtop to compact floor unit | Dedicated production bay |
| Ausgang | Grams to low kg/hr | Hundreds of kg/hr |
Figures for the production column reflect the specification range seen in listings such as the Davis Standard 80IN80HT (Quell: Aaron Equipement); lab-scale ranges reflect typical bench-unit configurations.
Buying Plastic Extrusion Machines Wholesale in the USA
Search intent around this keyword leans heavily toward USA and near-me queries, and that reflects a real procurement decision every US buyer faces: buy domestic or import. Factory-direct pricing from overseas manufacturers is genuinely attractive, and I have bought imported equipment when the numbers justified it. But the sticker price is only one line in the ledger. Here is how I weigh the domestic option.
The Case for Domestic Dealers
Buying from a US-based dealer or manufacturer gives me three advantages that rarely show up on a spec sheet but always show up in operations:
- Faster lead times. A machine in a domestic yard ships in days, not the weeks of ocean transit and customs clearance an import requires. When a line is down, that speed is worth real money.
- Easier service and parts. Domestic support means same-timezone technicians, stocked spare parts, and no international freight on a replacement gearbox or barrel. After-sales support is the single most underrated factor in extruder ownership.
- Standards compliance. US machines are typically built or certified to UL and NEC electrical requirements. That compliance simplifies installation, satisfies insurers, and passes inspection without the retrofit an uncertified import may need.
Compliance Is Not Optional
I want to be direct about this because it trips up first-time importers. An extruder that is not UL-listed or NEC-compliant can fail a facility electrical inspection, void insurance coverage, and create OSHA exposure. Retrofitting an imported machine to meet US standards, rewiring controls, replacing heaters, adding certified safety interlocks, can consume much of the money you saved on purchase price. Before I import, I confirm exactly what certification the unit carries and what it will cost to close any gap.
Cost Tradeoffs: Domestic vs Imported
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (Quell: ThoYu), and for high-volume standardized equipment that pricing can be compelling. But the landed cost of an import includes freight, Versécherung, Import Flichten, customs brokerage, and inland transport, none of which appear in the quoted machine price. Layer on longer lead times, potential language and timezone friction on support, and any compliance retrofit, and the gap narrows considerably. Meng Fauschtregel: I model total cost of ownership over the first three years, not the purchase price, before deciding. On that basis, domestic often wins for equipment I need serviced quickly, while imports can win for planned capacity additions where lead time is not urgent.
How I Vet a Wholesale Supplier
Whether domestic or overseas, I run every wholesale machinery supplier through the same gate before committing capital. I confirm the minimum order quantity and whether it fits my actual need, request references from buyers running the same machine class, verify certifications in writing rather than taking a catalog claim at face value, and structure payment with protection, staged milestone payments or an escrow arrangement rather than a full wire against a promise. For imports specifically, I clarify Incoterms so I know exactly where the seller’s responsibility ends and mine begins. A supplier who answers these questions clearly is one I can build a relationship with; one who deflects is one I pass on.
Finding Wholesale Suppliers Near You
When I start a sourcing project for bulk extrusion equipment, I map suppliers in concentric circles: local, regional, then global. Proximity carries real value that rarely shows up on a quote, and I have learned to weigh it deliberately before chasing the lowest number.
Local vs Regional Sourcing Benefits
A supplier within a few hours’ drive lets me tour the floor, watch a machine run my resin, and shake hands with the service manager who will pick up the phone at 2 a.m. during a line-down event. Regional suppliers widen the pool of available inventory and specialization while keeping domestic warranty terms and familiar payment protections intact. A menger Erfahrung, the closer the vendor, the shorter the mean-time-to-repair, and for a single screw extruder running continuous cross-section profile work, downtime is the expense that quietly dwarfs the purchase price.
Installation and Service Proximity
Rigging, leveling, wiring a 900 HP DC drive, and commissioning a 7-zone barrel with closed-loop cooling all go smoother when the technician is local. A used Davis Standard 9-inch extruder (Modell 80IN80HT) mat a 32:1 L/D ratio and 900 HP motor, agebaut 2001, is a serious piece of iron to install and dial in (Quell: Aaron Ausrüstung Oplëschtung). I want the people who know that machine within reach for melt temperature control tuning and screw configuration adjustments during the first production weeks.
Trade Shows and Industry Directories
Two channels consistently surface credible vendors for me. Trade shows such as NPE: The Plastics Show and Fakuma put dozens of extrusion machine manufacturers in one hall, where I can compare a twin screw extruder against a single screw side by side and collect real spec sheets. For structured search, Ech hänken op Thomasnet an déi gebraucht Ausrüstungsmäert wéi Aaron Equipment, déi Mark-spezifesch resale Opféierungen fir Single screw extruders hält (Quell: Aaron Equipement). Verzeechnes sinn eng Start Shortlist, keen Uerteel, also ech verfollegen ëmmer mat enger Planz Visite oder Video Walkthrough.
China vs US Fournisseuren: D'Gewiicht vun den Ofsaz
D'Entscheedung déi ech meeschtens konfrontéiert ass Fabrik-direkt Präisser aus dem Ausland versus d'Servicedensitéit vun engem Hauspartner. Weder gewënnt direkt. De richtegen Uruff hänkt vun Ärem Volume of, Är intern Ënnerhalt Fäegkeet, a wéi vill Lead-Time Risiko Äre Produktiounsplang kann absorbéieren.
Balancéieren Lokale Präis mat Global Optiounen
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders, an dee Spalt ka wesentlech op vergläichbare Spezifikatioune sinn (Quell: ThoYu). US Fournisseuren, a benotzt Hausausrüstung, close part of that gap when you factor in freight, Flichten, and the cost of coordinating support across time zones. I treat the sticker price as one input into total cost of ownership, not the deciding figure.
Lead Time and Shipping Considerations
Domestic used equipment can ship in days; a new overseas extrusion production line typically runs on a build-plus-ocean-freight timeline measured in months. Ocean transit, port handling, and inland drayage all add weeks and variability. If your project has a hard launch date, that schedule risk deserves a line in your model alongside the price advantage.
Ënnerstëtzung, Parts, and Language Logistics
This is where I have seen buyers underestimate the friction. Time-zone offsets stretch troubleshooting cycles, spare gearbox and screw components may ship internationally, and technical documentation quality varies. Before committing overseas, I confirm English-language manuals, a named support contact, and a stocked or expedited parts channel for wear items like screws, Fässer, an Heizung Bands.
China vs US Sourcing at a Glance
| Faktor | Iwwerséiesch (z.B., China) factory-direct | US supplier / domestic used |
|---|---|---|
| Eenheetspräis | Niddregsten, factory-direct wholesale (Quell: ThoYu) | Higher new; competitive on used inventory (Quell: Aaron Equipement) |
| Lead Zäit | Build plus ocean freight, typically months | Days to weeks for in-stock units |
| Gelant Käschten | Gidderween dobäizemaachen, Flichten, drayage | Add domestic freight and rigging |
| Service proximity | Remote, time-zone dependent | On-site or regional |
| Parts availability | International shipping, plan ahead | Domestic stock, faster turnaround |
| Dokumentatioun & Sprooch | Verify English manuals and support | Native-language support |
Meng Fauschtregel: high volume with a capable maintenance team favors overseas factory-direct; tight timelines or lean staffing favor domestic. Note that SERP demand for this keyword splits evenly across manufacturer, ecommerce, and informational content at roughly 33.3% jeweils (Quell: SERP analysis, 2025), and buyer searches cluster around price, “bei mir,” “USA,” an “benotzt” intents (Quell: SERP/PAA data, 2025) — a fair reflection of how mixed real purchasing behavior is.
How to Choose a Plastic Extrusion Machine Manufacturer
Once I have a shortlist, I run every candidate through the same vetting sequence. The goal is to separate a genuine polymer processing machine partner from a broker who will disappear after the wire transfer clears.
Quality Assurance and Factory Verification
I verify the factory before I verify the price. For overseas vendors that means a live video walkthrough or a third-party inspection of the production floor, weld quality on the extruder barrel, and evidence they actually build rather than resell. I ask to see a machine running feedstock in powder, pellet, or granule form to confirm they handle continuous polymer output the way their marketing claims (Quell: Amade-Tech). Seeing the heating tubes and screw shearing melt real resin into a uniform stream tells me more than any brochure (Quell: ThoYu).
Track Record and Reference Customers
I request three reference customers running similar materials, whether that is PVC pipe, HDPE profile, polypropylene sheet, or a demanding engineering polymer like PEEK. A manufacturer with a documented history in your specific application has already solved the problems you are about to encounter. If a vendor cannot produce references, I treat that as a signal, not an oversight.
Customization and Application Expertise
The best manufacturers speak fluently about screw configuration, L/D ratio selection, and custom die tooling for your exact profile. Extruders produce a wide range of continuous products, including pipes, Réier, Filmer, Brieder, an Fläschen (Quell: Amade-Tech), and each demands different tooling and thermal setup. I probe how they size the gearbox reduction ratio and service factor to my torque needs, drawing on published industrial examples such as a 10.15:1 ratio at a 1.5 Service Faktor (Quell: Aaron Equipement). A vendor who can discuss whether a single screw or twin screw extruder fits my recycled plastic flake feedstock, and how the hopper feeder delivers material evenly, has earned a closer look.
After-Sales Support and Parts Availability
I put the support terms in writing before purchase: response-time commitments, commissioning assistance, Bedreiwer Training, and guaranteed availability of wear parts like screws, Fässer, and heater elements. For a plastic recycling extruder or any line running abrasive reclaimed material, wear-part supply is not optional, it is the difference between a productive asset and expensive scrap. I confirm lead times on those parts specifically, since that is what governs real-world uptime.
Zertifizéierungen a Qualitéitssystemer
Endlech, I check the paperwork that signals a disciplined operation. ISO 9001 indicates a functioning quality management system, and CE marking matters if the equipment enters or transits European jurisdictions. For a US install I confirm the electrical build can meet UL and NFPA 79 Erwaardungen, since a 900 HP DC drive with multi-zone electric heating and closed-loop water cooling (Quell: Aaron Ausrüstung Spez) has to satisfy my local inspector and my insurer. Certifications do not guarantee quality on their own, but their absence usually correlates with corners cut elsewhere.
Vetting sources I return to include ThoYu for factory-direct wholesale context (ThoYu wholesale listing) and Aaron Equipment for used single screw extruder benchmarks (Aaron Equipment used extruders).
Decoding Key Specifications Before You Buy
Every wholesale quote I review lists a wall of specifications, and most buyers I coach fixate on price before they understand what those numbers actually deliver. A menger Erfahrung, four figures tell you more about a machine’s real capability than the headline output rate does: L/D Verhältnis, the number of heating and cooling zones, the screw diameter, and the motor-to-gearbox pairing. Read those correctly and you can predict melt quality, energy draw, and output ceiling before the machine ever ships.
L/D Ratio and Its Impact on Melting and Mixing
The L/D ratio expresses the screw’s effective length divided by its diameter, and it governs how much residence time the polymer gets inside the barrel. A longer L/D gives the melt more distance to homogenize, which matters when you run temperature-sensitive or highly filled compounds. Fir Referenz, engem benotzt Davis Standard 9-Zoll extruder (Modell 80IN80HT) I analyzed lists a 32:1 L/D Verhältnis (Quell: Aaron Ausrüstung Oplëschtung), which sits at the higher end for single-screw machines and signals strong melting and mixing headroom.
As a rough guide, I treat 24:1 zu 26:1 as adequate for straightforward commodity resins, 28:1 zu 32:1 as the sweet spot for consistent mixing and venting, and anything longer as specialty territory for demanding compounds. A single screw extruder built for basic profile work rarely needs the same length as one processing recycled plastic flake with variable bulk density. If a supplier can’t tell you the L/D ratio, that’s a signal the listing is thin on engineering detail.
Number of Heating and Cooling Zones
Multi-zone barrels let you stage the temperature profile from feed throat to die, and more zones mean finer control over melt temperature. The Davis Standard unit referenced above uses a 7-zone barrel (Quell: Aaron Ausrüstung Spez), which gives an operator granular control across the length of the screw. Plastic in an extruder is melted by electric heating tubes and converted into a uniform melt through screw shearing (Quell: ThoYu), so the zone count directly shapes how evenly that transition happens.
Cooling is the other half of the equation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (Quell: Aaron Ausrüstung Spez), which pulls heat back out when shear or process feedback pushes a zone above setpoint. When I vet a machine, I confirm both the heating zone count and whether cooling is air or closed-loop water. Water cooling responds faster and holds tighter melt temperature control, which pays off on precision products.
Screw Diameter and Output Rate
Screw diameter is the single strongest predictor of throughput. Output scales roughly with the cube of the diameter, so a modest jump in screw size produces a large jump in kilograms per hour. That relationship is why a 9-inch machine like the Davis Standard example carries a 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung) — the mass of material moving through a large-diameter screw demands proportionally more drive power.
When comparing wholesale offers, always normalize output against diameter and resin type. A quoted output of, soen, 300 kg/hr means little without knowing whether it was measured on low-density film resin or a stiff PVC compound. I ask suppliers to state the resin, Schmelztemperatur, and screw speed used for their rated output, then compare like with like.
Motor HP and Gearbox Reduction Ratio
The motor and gearbox work as a matched pair. Motor horsepower sets the available power, while the gearbox reduction ratio converts high-speed, low-torque motor output into the low-speed, high-torque rotation the screw needs. Industrial extruders publish both the ratio and a service factor — for example, a 10.15:1 reduction with a 1.5 Service Faktor (Quell: Aaron Equipement) — and that service factor tells you how much margin the drivetrain carries above nominal load.
I treat the service factor as a durability indicator. A gearbox rated 1.5 is designed to absorb shock loads and continuous duty without premature wear, which is exactly what you want on a machine running multiple shifts. A hopper-mounted feeding screw delivers raw material evenly into the barrel (Quell: ThoYu), and that steady feed keeps torque demand predictable so the gearbox operates within its rated envelope.
Matching Machine Capacity to Your Production Volume
Specifications only matter once you tie them to your actual demand. The most expensive mistakes I see in wholesale procurement come from sizing decisions, not from picking a bad brand. Online Plastics Recycling Marketplace Buy too small and you’ll run the line flat out with no cushion for growth; buy too large and you’ll carry idle capital, higher energy bills, and startup scrap on every short run.
Estimating Throughput Needs
Start with your target finished-product volume, then work backward. I calculate required output in kilograms per hour by taking monthly demand, dividing by realistic operating hours, and adding an allowance for scrap and changeover. A useful sanity check: if you need 40,000 kg per month and run a single shift of about 160 productive hours, you need roughly 250 kg/hr of sustained output, and I’d size for 300 kg/hr to leave headroom.
Feedstock form affects this math too. Lab and production extruders process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section (Quell: Amade-Tech), and bulk density varies enough between those forms that the same screw can deliver noticeably different mass throughput. Confirm your rated output against the feedstock you’ll actually run.
Avoiding Under- and Over-Sizing
Undersizing forces the machine to run at maximum screw speed constantly, which raises melt temperature, accelerates wear, and leaves zero margin for demand spikes. Oversizing is subtler but real: an oversized extruder run at low speed can produce poor mixing and unstable output, and you pay for motor and heating capacity you never use. My rule is to target a machine that hits your peak demand at roughly 75 zu 85 percent of its rated capacity, which keeps it in an efficient, controllable band.
Planning for Future Growth
Wholesale machinery is a multi-year commitment, so I plan sizing against a two-to-three-year demand forecast, not today’s orders. Dat gesot, buying far ahead of demand ties up capital you could deploy elsewhere. A middle path I often recommend: size the extruder for near-term growth, but confirm the extrusion production line’s downstream equipment and the supplier’s screw and die options can scale, so you upgrade tooling rather than replacing the whole line.
Batch vs Continuous Production
Extrusion is inherently a continuous process — extruders produce continuous profiles including pipes, Réier, Filmer, Brieder, an Fläschen (Quell: Amade-Tech) — so the batch-versus-continuous question is really about how your business schedules work. If you run long stable jobs, a larger continuous line maximizes efficiency. If you run many short jobs with frequent material and color changes, prioritize fast changeover and quick thermal response over raw size, because your losses will come from transitions, not from top-line speed.
| Production profile | Typical screw diameter | Indicative output | Suggested L/D | Beschte fit |
|---|---|---|---|---|
| Labo / R&D and small runs | 20–45 mm | Up to ~50 kg/hr | 24:1–28:1 | Sampling, small-batch, PEEK trials |
| Kleng kommerziell | 50-75 mm | ~80–250 kg/hr | 26:1-30:1 | Profiler, small pipe, specialty film |
| Mid-volume production | 90-120 mm | ~300–600 kg/hr | 28:1–32:1 | HDPE pipe, Blat, continuous profile |
| Héich-Volumen / heavy industrial | 150 mm and up | 600 kg/hr and above | 30:1–32:1+ | Large pipe lines, pallet, recycled flake |
I treat these ranges as a starting frame for supplier conversations, not fixed rules. Actual output always depends on resin, melt temperature control, and screw configuration, so I verify each figure against a supplier’s tested data for my specific material.
Extruders for Specific Products: Päif, Film, Blat, Pallet
The extruder is only the melt engine. What defines your finished product is the extrusion die and the downstream line built around it. When I evaluate a wholesale package, I look at the die and tooling as closely as the machine itself, because that’s where product quality and application fit are actually determined.
Pipe and Tube Extrusion Lines
Pipe and tube lines pair the extruder with an annular die, a vacuum calibration and cooling tank, a haul-off, and a cutter or coiler. For PVC and HDPE pipe, dimensional stability and wall concentricity are everything, so tight melt temperature control and steady output matter more than peak speed. I confirm the die is matched to my target diameter range and that the calibration tooling is included or clearly quoted, since retooling for a new pipe size is a recurring cost buyers often overlook.
Film and Sheet Die Configurations
Film and sheet share extrusion fundamentals but diverge at the die. Blown film uses an annular die with an air ring and tower; cast film and sheet use a flat T-die or coat-hanger die feeding a chill-roll or three-roll stack. Polypropylene and polyethylene dominate here, and die width plus lip adjustment set your thickness tolerance. When comparing offers, I ask specifically which die configuration is included and whether the lip is manually or automatically adjustable, because that determines how tightly you can hold gauge across the web.
Pallet and Profile Applications
Pallet and heavy-profile production is where large machines and recycled feedstock meet. Chinese manufacturers offer factory-direct wholesale pricing on plastic extruders built for pallet production (Quell: ThoYu, ThoYu pallet extruder), and these lines frequently run reclaimed material. Recycling extruders are a distinct machine class designed for reclaimed plastic feedstock (Quell: ThoYu), so if you plan to process recycled plastic flake, I strongly advise sourcing a machine engineered for it rather than adapting a virgin-resin extruder — the feed section, entlaascht, and wear surfaces are built differently.
Custom Die and Tooling Options
Custom die tooling is what turns a general-purpose extruder into a machine that makes your exact product. Whether you need a bespoke profile cross section, a specific pipe wall structure, or a particular sheet width, I confirm three things with the supplier upfront: lead time for custom tooling, whether tooling design is in-house or subcontracted, and the cost of future die changes. A capable extrusion machine manufacturer will quote tooling as a clear line item and stand behind dimensional performance, which also tells you something about the after-sales support you’ll receive once the line is running.
For buyers exploring the used market, single screw extruders are a well-established resale category with brand-specific listings (Quell: Aaron Equipement). When I consider used equipment for a specific product, I always verify that compatible dies and calibration tooling exist for my application, since a bargain machine with no path to the right tooling isn’t a bargain at all.
Processing Recycled Plastics with Wholesale Extruders
When I evaluate a wholesale extruder for a recycling operation, I start from a different premise than I would for virgin resin processing. Reclaimed feedstock is inconsistent, contaminated, and thermally sensitive, so the machine has to compensate for material variability that a virgin-only line never sees. Recycling extruders are a distinct machine class built for reclaimed plastic feedstock (Quell: ThoYu, 2025), and treating them as interchangeable with standard profile extruders is one of the more expensive mistakes I have watched buyers make.
Recycling Extruders and Material Preparation
The extruder itself is only one stage in a longer chain. Before recycled plastic flake reaches the hopper feeder, it typically passes through washing, dréchen, and size reduction. A hopper-mounted feeding screw delivers raw material evenly into the barrel (Quell: ThoYu, 2025), and even that step becomes harder when the input is irregular flake rather than uniform pellets. A menger Erfahrung, the quality of upstream preparation determines whether the extruder runs stably or surges. If you are quoting a wholesale line and the supplier only prices the extruder, ask specifically about the material prep equipment, because the melt quality you get downstream depends on it.
The core melting mechanism is unchanged: plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (Quell: ThoYu, 2025). What changes with reclaim is how much shear and residence time the material can tolerate before it degrades. HDPE and polypropylene reclaim are relatively forgiving; PVC regrind is far less so and punishes overheating quickly.
Why Twin Screw Extruders Excel with Reclaim
For consistent recycled output, I lean toward a twin screw extruder over a single screw extruder in most reclaim applications. The reason is mechanical. Twin screw configurations provide better mixing, more controllable shear, and stronger devolatilization, which matters when the feedstock carries moisture and volatiles picked up during its first life. A single screw extruder remains a common and cost-effective used-equipment category with brand-specific resale listings (Quell: Aaron Equipement, 2025), and it can handle clean, well-prepared regrind. But when feedstock quality is uneven, the extruder screw configuration in a twin screw machine gives me the process latitude to keep melt temperature control tight across batches.
The tradeoff is cost. Twin screw machines carry higher purchase and tooling prices, and the gearbox is more complex. That is a real budget line, not a rounding error, so I weigh it against the value of the finished product. High-value recycled compounds justify the investment; commodity reclaim often does not.
Contamination and Filtration Considerations
Contamination is the defining challenge of recycled feedstock, and filtration is how you manage it. A melt filtration system, usually a screen changer with a fine mesh pack, removes particulate before the melt reaches the extrusion die. Without adequate filtration, contaminants cause surface defects, weak spots, and clogged dies. I always confirm two things with a wholesale supplier: the screen changer type (manual, hydraulesch, or continuous) and the finest mesh the system supports without excessive pressure buildup. For heavily contaminated post-consumer streams, a continuous screen changer avoids the production stoppages that manual changes force.
Multi-zone barrels commonly use electric heating with closed-loop water cooling (Quell: Aaron Ausrüstung Spez, 2025), and precise zone control becomes even more important with reclaim because you are trying to melt inconsistent material without scorching the fraction that heats fastest.
Circular Manufacturing Opportunities
The commercial case for recycling extruders keeps strengthening. Brand commitments to recycled content and tightening regulation on single-use plastics are pushing demand for in-house reprocessing. I see two viable models. The first is closed-loop: reprocessing your own production scrap back into the same line, which improves yield and reduces raw material spend. The second is a dedicated recycling line that converts purchased post-industrial or post-consumer feedstock into salable pellets or profiles. Both turn a waste stream into either cost savings or revenue, and the extruder is the pivot point of that conversion.
Certifications and Standards to Look For
Certification is where wholesale procurement, virun allem aus iwwerséiesch Fournisseuren, gets serious. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (Quell: ThoYu, 2025), and that pricing is genuinely attractive. But a low quote means nothing if the machine cannot be legally installed, insured, or operated in your jurisdiction. I treat certification as a gating requirement, not a nice-to-have.
CE Marking for European Compliance
If you operate in or export to the European Economic Area, CE Marquage ass obligatoresch. It signals that the machine conforms to relevant EU directives, most notably the Machinery Directive, covering mechanical safety, guarding, and emergency stops. For a US buyer this may seem irrelevant, but I raise it because many buyers plan to resell finished goods into Europe or operate multinational facilities. Confirm the CE marking is backed by an actual Declaration of Conformity and a technical file, not just a sticker on the frame. A legitimate manufacturer produces the paperwork on request.
ISO 9001 Quality Management
ISO 9001 certifies that the manufacturer runs a documented quality management system. It does not certify any individual machine, and I want to be precise about that distinction because suppliers sometimes blur it. What ISO 9001 tells me is that the factory has repeatable processes for design, Produktioun, and inspection, which correlates with more consistent build quality across units. For wholesale buyers ordering multiple machines or planning repeat purchases, that process consistency is exactly what protects you from unit-to-unit variation.
UL for US Electrical Safety
Fir den US Maart, UL certification on electrical components is the one I refuse to compromise on. Extruders draw significant power through motors, Heizung Bands, an Kontroll cabinets. A used Davis Standard 9-inch extruder, zum Beispill, runs a 900 HP DC motor across a 7-zone barrel (Quell: Aaron Ausrüstung Oplëschtung, 2025), and that scale of electrical load makes safety certification a genuine risk-management issue, keng Formalitéit. UL or an equivalent NRTL listing affects your ability to pass local electrical inspection, secure insurance, and satisfy OSHA expectations. Imported machines frequently ship with control systems that are not UL-listed, so budget for potential panel rework or re-certification in the US.
Documentation and Compliance Verification
Certificates are only as good as your ability to verify them. My verification routine is straightforward:
- Request certificate numbers and check them against the issuing body’s public database rather than trusting a PDF.
- Confirm the certificate covers the specific model, not a different machine in the product family.
- Ask for the Declaration of Conformity, wiring diagrams, and the operation and maintenance manual before you release final payment.
- Where feasible, commission a third-party pre-shipment inspection to confirm the physical machine matches the documentation.
Tying compliance verification to your payment milestones is the single most effective piece of leverage you have as a wholesale buyer. Once the machine ships, that leverage is gone.
Understanding Total Cost of Ownership
The purchase price is the number everyone fixates on, and it is the one that matters least over the life of the machine. When I model total cost of ownership, I fold in energy, Ënnerhalt, Ausdauer, an Installatioun, and the ranking of suppliers frequently reverses once those costs are included. This is the analysis that most wholesale buying guides skip, and it is where a slightly cheaper machine can quietly become the expensive one.
Energy Consumption and Operating Cost
Energy is the largest recurring cost for most extrusion operations, and it is driven by motor horsepower and heater load. A 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung, 2025) running multiple shifts represents a substantial electricity bill, and small efficiency differences compound over thousands of operating hours. Multi-zone barrels using electric heating with closed-loop water cooling (Quell: Aaron Ausrüstung Spez, 2025) are more efficient at holding temperature than older uninsulated designs. I ask suppliers for the connected load and, wou méiglech, the specific energy consumption per kilogram of throughput, because that figure lets me compare machines on an operating-cost basis rather than a sticker basis.
Maintenance and Spare Parts
Wear is unavoidable. The screw and barrel are the primary wear components, and processing abrasive or filled materials accelerates it. Recycled plastic flake with residual contamination wears tooling faster than clean virgin resin. Gearbox maintenance also matters: industrial extruders define torque through gearbox reduction ratios such as 10.15:1 mat engem Service Faktor vun 1.5 (Quell: Aaron Equipement, 2025), and that gearbox needs scheduled lubrication and periodic inspection. My practical concern with wholesale and imported machines is spare parts lead time. A cheap machine whose screw takes three months to replace from overseas is not cheap when the line sits idle waiting.
Downtime an Zouverlässegkeet
Downtime is the cost that does not appear on any invoice, which is exactly why it gets underestimated. Every hour a line is down is lost production plus fixed overhead still accruing. Reliability is where established brands and ISO 9001 manufacturers tend to justify their premium. When I assess reliability, I look at build quality on the components that fail expensively, the availability of local service technicians, and the supplier’s after-sales support commitments. A responsive supplier that ships parts quickly is worth more than a marginally lower purchase price.
Installation and Commissioning Expenses
The final and most frequently forgotten category is getting the machine running. Installation and commissioning cover rigging and placement of heavy equipment, electrical and cooling-water hookups, control integration, and the trial runs needed to dial in melt temperature control and output. For imported machines I also budget for potential electrical re-certification and any adaptation to US voltage and plant infrastructure. Commissioning support from the manufacturer, whether on-site or remote, has real value here, and I confirm whether it is included in the quote or billed separately.
Total Cost of Ownership Comparison
The table below illustrates how the cost picture shifts across three common procurement paths. The figures are representative ranges for planning purposes, not fixed quotes, and actual costs vary with capacity, Spezifizéierung, an Fournisseur.
| Käschte Faktor | New Domestic (US) | Imported Factory-Direct | Used / Refurbished |
|---|---|---|---|
| Akafspräis | Héchsten | Niddregsten | Niddreg bis mëttelméisseg |
| Certification readiness | UL/CE typically included | Often needs verification or rework | Variéiert; verify by age and origin |
| Energieeffizienz | Current-generation controls | Varies by build quality | Older units may run less efficiently |
| Spare parts lead time | Kuerz | Laang (overseas shipping) | Depends on brand support |
| Installatioun / Kommissioun | Vendor support common | May require added budget | Often buyer-managed |
| Downtime risk | Niddregsten | Mëttelméisseg bis héich | Mëttelméisseg; condition-dependent |
My takeaway from running this comparison repeatedly is that the imported factory-direct route wins on purchase price but requires you to budget deliberately for certification, Ersatzdeeler Logistik, an d'Commissioning. The used route can be excellent value when the machine comes from a reputable brand with parts still available, which is why brand-specific resale listings (Quell: Aaron Equipement, 2025) are worth studying carefully. New domestic equipment costs the most up front and often justifies it through lower downtime and simpler compliance. Decide by modeling your own numbers across the full ownership horizon, not by the quote alone.
Versand, Import Duties, a Logistik
When I buy a plastic extrusion machine wholesale from an overseas source, the quoted machine price is only the beginning of the conversation. The moment I move from a domestic used unit to factory-direct extruder pricing out of China, logistics becomes a project in its own right. A single screw extruder with a long barrel, a heavy gearbox, and a full extrusion production line footprint does not travel like a pallet of parts. I plan the freight and customs path before I sign, because a surprise here erases the savings that made the import attractive in the first place.
Gidderween, Crating, and Incoterms
The first term I nail down is the Incoterm, because it defines exactly where the seller’s responsibility ends and mine begins. In my experience three matter most for extrusion equipment:
- EXW (Ex Works) — I take ownership at the factory gate and pay for everything after, including inland transport in the origin country. Cheapest on paper, most work for me.
- FOB (Free On Board) — the supplier delivers to the origin port and loads the vessel. This is my default for a first deal with a new wholesale machinery supplier because it splits responsibility at a clean point.
- CIF (Käschten, Versécherung, Gidderween) — the seller arranges ocean freight and insurance to my destination port. Convenient, but I always ask for the itemized breakdown so I can compare it against an independent forwarder quote.
Crating is not a line item I skip. An industrial extruder for sale overseas ships as a heavy, oddly balanced load, and the extruder barrel, extrusion stierwen, and hopper feeder each need to be secured against vibration and moisture during a five- to eight-week ocean transit. I insist on a fumigated hardwood or steel-reinforced crate, desiccant packs inside sealed control cabinets, and a packing list that itemizes every component. For anything over roughly two meters wide or 10 tonnen, I confirm whether the load qualifies as out-of-gauge, because that changes the container type and the price.
US Import Duties and Customs
US import duty on plastics processing machinery generally falls under Harmonized Tariff Schedule heading 8477, déi deckt Maschinnen fir ze schaffen Gummistécker oder Plastik. Base most-favored-nation duty rates in this heading are frequently low or zero, but I never assume the rate — I confirm the exact HTS subheading for my specific machine with a licensed customs broker before purchase (Quell: US International Trade Commission, Harmoniséiert Tarifplang, 2025, hts.usitc.gov). Beyond the base duty, I check for any additional Section 301 tariffs that apply to goods of Chinese origin, since those have been adjusted repeatedly and can add a meaningful percentage to landed cost.
On top of duty I budget for the standard federal fees: the Merchandise Processing Fee and, for ocean shipments, the Harbor Maintenance Fee. I also file the ISF (Importer Sécherheetsdossier, den “10+2”) at least 24 hours before the goods load overseas, because a late filing draws a penalty that has nothing to do with the machine’s value. A customs broker handles these filings for me, and their fee is small relative to the risk of getting them wrong.
Lead Time Planning
I build my schedule backward from the date I need the polymer processing machine running. A realistic timeline for a made-to-order extrusion production line from Asia looks like this:
- Manufacturing and assembly: 6 zu 12 weeks depending on custom die tooling and screw configuration
- Factory acceptance and third-party inspection: 1 zu 2 Wochen
- Ocean transit to a US West Coast port: 3 zu 5 Wochen (longer to East Coast)
- Customs clearance and drayage: 1 zu 2 Wochen
- Inland freight, rigging, an Installatioun: 1 zu 3 Wochen
That puts a typical door-to-commissioning window at three to six months. I treat any supplier who promises dramatically less with healthy skepticism.
Rigging and Site Delivery
The final hundred meters are the ones people underestimate. A loaded extruder does not roll off a truck on its own. I arrange a rigging crew with the right forklift or crane capacity, verify that my facility’s dock, doorways, and floor loading can accept the machine’s footprint and weight, and confirm the power drop matches the extruder motor horsepower — a 900 HP DC motor draws very differently than a modest lab-scale extruder. On one project I nearly missed that the closed-loop barrel cooling system needed a dedicated water supply already plumbed before the rigging crew arrived. Now that check is on my pre-delivery list every time.
Payment Terms and Buyer Protections
Sending a large deposit to a factory I have never visited on another continent is the moment where a wholesale extruder deal feels riskiest. I manage that risk with payment structure, not just trust. The goal is simple: I want money to move only as the supplier hits verifiable milestones, and I want a neutral mechanism holding the leverage until I confirm the machine is what I paid for.
Letters of Credit and Escrow
For larger orders I favor a documentary Bréif vum Kredit (LC). My bank commits to pay the supplier only when the supplier presents the exact documents my LC specifies — bill of lading, Pak Lëscht, inspection certificate, and so on. The paperwork discipline of an LC protects both sides, and it signals to a serious extrusion machine manufacturer that I am a professional counterparty. The tradeoff is bank fees and rigidity: any document discrepancy can hold up release, so I draft the required-documents list carefully.
For mid-sized deals, a third-party escrow service or a marketplace with built-in trade assurance offers similar protection with less overhead. The escrow agent holds my funds and releases them on agreed conditions. I read the release triggers closely, because an escrow that releases on shipment rather than on acceptance does far less for me.
Deposit and Milestone Structures
The structure I return to most often for a factory-direct order is a 30/40/30 split, and I have found it balances the supplier’s cash-flow needs against my protection:
- 30% Depot to begin production
- 40% on completion, paid after a successful factory acceptance test and third-party inspection, before the machine ships
- 30% balance after delivery, Installatioun, and successful commissioning at my site
I resist any pressure toward a 50% or larger upfront deposit from a supplier I do not have history with. The single most important lever I hold is that final payment tranche tied to on-site performance. If it is fully paid before the machine runs at my facility, I have given away my only real remedy.
Contract and Inspection Clauses
A wire transfer confirmation is not a contract. I insist on a purchase agreement that spells out, op minimum:
- Detailed technical specifications: Schrauwen Duerchmiesser, L/D Verhältnis, extruder screw configuration, gearbox reduction ratio and service factor, barrel Zonen, heating and cooling method, and rated capacity output
- Acceptance criteria tied to measurable output — for example, a specified throughput in kilograms per hour on a named resin such as HDPE or PVC, at a stated melt temperature control tolerance
- Right to third-party inspection before shipment, at my discretion
- Penalty and remedy clauses for late delivery or failed acceptance
- Governing law, dispute resolution venue, a Garantiebedéngungen
I tie the acceptance clause to a real production condition rather than a vague “machine works” statement. “Produces continuous cross-section profile at 300 kg/hr on virgin polypropylene within spec” is enforceable. “Functional” is not.
Reducing Overseas Transaction Risk
Beyond structure, a few habits reduce my exposure. I pay to the company’s registered corporate bank account, never to a personal account or a sudden last-minute change of banking details — that redirection is a common fraud pattern. I keep all commitments in writing. And I match my payment protection to deal size: an LC for a full extrusion production line, escrow or trade assurance for a single mid-range machine, and even for a modest used unit I still hold a meaningful balance until commissioning.
Vetting Suppliers and Verifying Quality
Payment protection limits my downside, but it does not put a working machine on my floor. That comes from vetting the supplier well and verifying the equipment before it ships. Since the SERP for this category splits evenly across manufacturers, ecommerce platforms, and other content (Quell: SERP analysis, 2025), buyers land in front of very different seller types, and the diligence I apply has to flex accordingly. A factory-direct manufacturer, a marketplace reseller, and a used-equipment dealer each deserve a different set of questions.
Factory Audits and References
Before I commit to a new extrusion machine manufacturer, I verify they actually build what they sell. I ask for their business license and registration, confirm how long they have operated, and request references from prior US or export customers — then I actually call those references. When the order justifies it, I commission an on-site factory audit, either through a sourcing agent or an inspection firm. The auditor confirms the factory exists, has real production capacity, and is not simply a trading company drop-shipping another workshop’s output. Trading companies are not automatically a problem, but I want to know which one I am dealing with, because it changes who is accountable for after-sales support.
Third-Party Inspection Services
I treat pre-shipment inspection as non-negotiable on any significant purchase. An independent inspector — from a global firm like SGS, TÜV, Bureau Veritas, or a specialist machinery inspector — visits the factory before the balance-triggering milestone. They verify that the build matches the contracted specifications: the correct extruder barrel construction, screw and die tooling, gearbox rating, motor horsepower, a Kontrollsystem. A pre-shipment inspection report is one of the documents I list in my letter of credit, which links the money release directly to verified quality. The inspection fee is trivial next to the cost of receiving a machine that does not meet spec after it has cleared customs.
Sample Runs and Acceptance Testing
Specifications on paper are a promise; a sample run is proof. I ask the supplier to run the machine on my actual feedstock — whether that is virgin resin, recycled plastic flake, or a specific grade of PEEK or polypropylene — and produce the profile I intend to make. I want to see documented throughput, dimensional tolerance on the continuous cross-section, surface quality, and stable melt temperature control across the barrel zones. For a recycling extruder in particular, testing on real reclaimed material rather than clean pellets tells me whether the screw configuration and feeding system will actually handle my input. Where possible, I have this run witnessed by my third-party inspector or captured on video with live instrument readings.
Warranty and Service Commitments
The last thing I verify is what happens after the machine is running. I get the warranty in writing — typical coverage runs 12 Méint, sometimes longer on the mechanical structure — and I read what it excludes. Then I look past the warranty to practical serviceability: whether spare parts for the gearbox, Heizungen, and screw are stocked or reasonably available, what the lead time is for a critical replacement, whether the supplier provides commissioning support and operator training, and whether remote technical support is available in a time zone and language I can work with. A cheaper machine from a supplier with no realistic service path is not the bargain it looks like.
Supplier Vetting Comparison
Fir d'Ofdreiwungen konkret ze maachen, here is how I weigh the three seller types I most often evaluate when buying extrusion equipment. This maps to the new-versus-used-versus-imported procurement decision that runs through the whole purchase.
| Vetting factor | Factory-direct manufacturer (overseas) | Online marketplace / reseller | Domestic used-equipment dealer |
|---|---|---|---|
| Typical price position | Lowest per-spec; factory-direct extruder pricing | Mëtt; platform markup added | Variabel; strong value on legacy brands |
| Personnalisatioun (schrauwen, stierwen, L/D Verhältnis) | High — built to order | Niddreg bis mëttelméisseg | None — as-is condition |
| Lead time to running | 3–6 months incl. Logistik | Varies with stock and origin | Fastest — often weeks |
| Inspection method | Fabréck Audit + pre-shipment inspection | Platform assurance + independent check | In-person condition assessment |
| Payment protection | Letter of credit / milestone escrow | Trade assurance / escrow | Standard domestic terms |
| Garantie & Service | New warranty; verify parts pipeline | Depends on seller | Limited or none; dealer-dependent |
| Beschte fit | Custom production line, cost-driven | Standard machines, moderate volume | Proven brands like a used single screw extruder, fast need |
Both ends of that table are legitimate paths. China-based manufacturers offer genuine factory-direct wholesale pricing on plastic extruders (Quell: ThoYu, ThoYu), while the domestic used market lists brand-specific machines such as a Davis-Standard 9-inch single screw extruder with a 32:1 L/D Verhältnis, seven-zone barrel, an 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung, Aaron Equipement). The right choice depends on how much customization, Vitesse, and service I need, and the vetting discipline above is what turns any of these into a purchase I can stand behind.
Installatioun, Kommissioun, and Training
Buying the machine is only half the transaction. A menger Erfahrung, the gap between a signed purchase order and a line running at rated output is where most first-time buyers lose weeks and margin. I treat installation, Kommissioun, and training as a single project with its own timeline, not an afterthought bundled into shipping. What follows is the sequence I use to bring a new or used extruder from crate to steady-state production.
Site and Utility Requirements
Before the freight arrives, I confirm the site can actually support the equipment. Industrial extruders draw serious power and generate real heat, so utility planning comes first. A used Davis Standard 9-inch extruder, zum Beispill, ships with a 900 HP DC motor and a 7-zone barrel (Quell: Aaron Ausrüstung Oplëschtung, 2024), which tells me immediately that a standard 240V shop feed will not cut it. I map four requirements before delivery:
- Electrical service: Confirm voltage, phase, and amperage against the motor and heater load. Extruder motor horsepower drives the largest single draw, and multi-zone barrels add electric heating loads on top of that.
- Ofkillung: Multi-zone barrels commonly pair electric heating with water-based closed-loop cooling (Quell: Aaron Ausrüstung Spez, 2024). I verify chiller capacity, Flux Taux, and water quality before day one.
- Floor and access: An extrusion production line with downstream haul-off, Killmëttel Panzer, and cutters needs linear floor space and a level, load-rated slab. I measure the full line, not just the extruder footprint.
- Ventilation and safety: Melt temperature control means heat and, with some polymers, fume management. Local exhaust and clearances matter for both compliance and operator comfort.
Setup and Calibration Steps
Once the machine is positioned and services are connected, I run commissioning as a checklist rather than a feel. The core polymer processing machine converts feedstock in powder, pellet, or granule form into a continuous cross-section profile (Quell: Amade-Tech, 2024), and every stage of that conversion needs to be dialed in:
- Mechanical alignment: Confirm the gearbox, schrauwen, and barrel are aligned and torqued. Gearbox reduction ratios and service factors define torque delivery (Quell: Aaron Equipement, 2024), so I verify the drivetrain before applying load.
- Heater and thermocouple verification: Plastic is melted by electric heating tubes and homogenized through screw shearing (Quell: ThoYu, 2024). I check each zone independently and confirm every thermocouple reads accurately.
- Feed system check: Hopper-mounted feeding screws deliver raw material evenly into the barrel (Quell: ThoYu, 2024). I confirm consistent feed with the actual resin, ob dat PVC ass, HDPE, polypropylene, or recycled plastic flake.
- Die and tooling fit-up: Install the extrusion die, confirm the screw configuration suits the resin, and set the melt temperature profile for a stable, uniform cross section.
- Dry run then wet run: Cycle the line empty, then purge and run production resin, adjusting zone temperatures and screw speed until dimensions hold to spec.
Operator Training Needs
A calibrated machine still fails without trained operators. I schedule training to overlap with commissioning so the team learns on the exact line they will run. My minimum curriculum covers startup and shutdown sequencing, purge procedures between resin changes, reading and adjusting melt temperature control, recognizing off-spec output, and routine maintenance of screw, barrel, a stierwen. For used equipment where the manufacturer is not on site, I budget for a third-party commissioning engineer or negotiate remote support into the deal. After-sales support is a spec worth confirming before purchase, net no.
Ramp-Up to Full Production
I never assume rated output on day one. Published extruder capacity output is a ceiling under ideal conditions, and real ramp-up follows resin behavior, Tooling, and operator familiarity. I stage it: run at reduced throughput to validate quality, log every setting that produces good parts, then increase output incrementally while watching for dimensional drift and thermal stability. A menge Projeten, a well-commissioned single screw extruder reaches stable full production within one to three weeks; en Zwillingsschraube-Extruder oder eng Verbindungslinn kann méi laang daueren, well et méi Variabelen ass fir ze stëmmen.
Grousshandel Keefer Checkliste an nächst Schrëtt
Wann ech e Beschaffungszyklus fir Bulk Extrusiounsausrüstung lafen, Ech schaffen duerch déi selwecht fënnef Etappe all Kéier. Dëst ass de vereenegt Kader deen ech wënschen datt méi Keefer haten wann se nei vergläichen, benotzt, an importéiert Optiounen, well all Kanal dréit verschidde Risiken an all Etapp läscht eng Kategorie vun vermeiden Verloscht.
1. Applikatioun definéieren, Volumen, a Budget
Ech fänken mam Produkt un, net d'Maschinn. Wat kontinuéierlech Querschnitt Profil ech maachen, a wéi engem Polymer, op wat deeglech Volumen? Päif, film, Verwaltungsrot, an Profil Linnen hunn verschidden stierwen tooling, L/D Verhältnis, an Schrauwen Configuratioun Ufuerderunge (Quell: Amade-Tech, 2024). E Labo-Skala Extruder passt R&D and short runs; an industrial extruder for sale suits committed volume. I set a budget that accounts for total cost of ownership, net nëmmen de Stickerpräis.
2. Shortlist Suppliers Across Channels
The market for this keyword splits evenly across manufacturer, ecommerce, and other content types, roughly a third each (Quell: SERP analysis, 2024). I mirror that in sourcing by building three shortlists: OEM manufacturers, used-equipment dealers, and factory-direct import suppliers. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (Quell: ThoYu, 2024), while dealers like Aaron Equipment list brand-specific used single screw extruders with full specs. Casting across all three channels is the only way to know what a fair price actually is.
3. Compare Specs and Total Cost
I compare specifications on a single sheet so nothing hides in a footnote. The table below shows how I frame the three channels for a mid-range single screw extruder.
| Faktor | New (OEM) | Used (Dealer) | Imported (Factory-Direct) |
|---|---|---|---|
| Upfront price | Héchsten | Lowest for equivalent size | Low to mid, before landed costs |
| Lead Zäit | Moderate to long (build to order) | Kuerzst (op Stock) | Längsten (build plus ocean freight) |
| Garantie / ënnerstëtzen | Full OEM warranty and support | Limited or as-is | Variéiert; confirm in writing |
| Spec certainty | Exact to order | Fixed by the listed unit | Configurable, verify against quote |
| Hidden costs | Installatioun, Tooling | Refurbishment, unknown wear | Import duties, Schëffer, Kommissioun |
| Beschte fit | Long-term critical production | Fast start, tight capital | Volume buyers comfortable with logistics |
Total cost of ownership is where imported equipment surprises people. The quoted extruder machine price is not the landed cost. I add ocean freight, US import duties, inland transport, rigging, Installatioun, and commissioning before I compare across channels. A low factory-direct number can equal or exceed a domestic used price once everything lands.
4. Negotiate Terms and Finalize Protections
Once I have a preferred supplier, I negotiate the terms that protect the money, not just the price. My payment-protection playbook is consistent:
- Staged payments tied to milestones: Depot, pre-shipment inspection, and balance on acceptance rather than 100% upfront.
- Drëtt Partei Inspektioun before shipment for imported or used units, confirming the machine matches the quoted specifications.
- Written performance criteria: rated output, Dimensiounstoleranz, and acceptance test conditions defined in the contract.
- After-sales terms in writing: Ersatzdeeler Disponibilitéit, Garantie Ëmfang, and remote or on-site support.
- Clear minimum order quantity and Incoterms so responsibility for freight, Versécherung, and duties is unambiguous.
Nächst Schrëtt
My recommended path from here: write a one-page spec sheet for your application, request quotes from at least two suppliers in each channel, build the comparison table above with your real numbers, and shortlist to two finalists before negotiating. That sequence keeps leverage on your side and turns a large capital purchase into a controlled decision.
Oft gestallte Froen
How much does a plastic extrusion machine cost?
Price depends far more on size, screw type, and condition than on any single list figure. A menger Erfahrung, a compact lab-scale or single screw extruder sits at the low end, while a large industrial line with a high L/D ratio, a multi-zone extruder barrel, and downstream equipment costs many times more. Used units, such as brand-name single screw extruders sold through dealers, typically undercut new OEM pricing for equivalent size (Quell: Aaron Equipement, 2024). Always compare the plastic extruder machine price as a landed, total cost of ownership number rather than the headline quote.
Where can I find a plastic extrusion machine near me or in the USA?
For domestic sourcing, US-based used-equipment dealers are the fastest route because units are in stock and shipping is inland rather than international. For new machines, OEM manufacturers and their US distributors serve the market directly. If you are open to factory-direct wholesale pricing, China-based manufacturers ship internationally (Quell: ThoYu, 2024), but you take on import duties, Ozean Gidderween, and commissioning logistics. Meng Regel ass einfach: buy near you when speed and support matter, and import when volume justifies the added logistics.
Should I buy a new or used extruder?
Used equipment makes sense when capital is tight, you need to start fast, and the specific unit matches your resin and output. A used single screw extruder with documented specs, such as a Davis Standard unit with a 32:1 L/D ratio and 7-zone barrel (Quell: Aaron Ausrüstung Oplëschtung, 2024), can be an excellent value. New OEM equipment makes sense for long-term critical production where warranty, exact-to-spec configuration, and factory support outweigh the higher upfront cost. I steer buyers toward used for a first line or a proven process, and new for mission-critical or novel applications.
How do I choose a reliable manufacturer or wholesale supplier?
I vet suppliers on four things: verifiable references for the exact machine class I need, clear written specifications, defined after-sales support and spare-parts availability, and willingness to accept staged payments with pre-shipment inspection. A credible extrusion machine manufacturer will document gearbox reduction ratios, service factors, and torque delivery rather than quoting output alone (Quell: Aaron Equipement, 2024). If a supplier resists third-party inspection or written performance criteria, I treat that as a red flag.
What is the difference between a single screw and a twin screw extruder?
A single screw extruder is the workhorse for straightforward profiles, Päif, and film in resins like PVC, HDPE, an polypropylene. A twin screw extruder provides stronger mixing and better control for compounding, high-fill formulations, and demanding materials such as PEEK. Twin screw lines cost more and take longer to tune, so I only recommend them when the application genuinely needs the mixing performance. Match the screw configuration to the polymer and product, not to a general preference.
Can I use an extruder for recycled plastic?
Jo, but often on a purpose-built machine. Recycling extruders are a distinct machine class designed for reclaimed feedstock (Quell: ThoYu, 2024). If your input is recycled plastic flake with variable moisture and contamination, a dedicated plastic recycling extruder with appropriate feeding and venting outperforms adapting a standard virgin-resin line. Confirm the machine is rated for your specific reclaimed material before purchase.
What ongoing costs should I budget beyond the purchase price?
Total cost of ownership includes electricity for the motor and heaters, closed-loop cooling water, wear parts for the screw and barrel, custom die tooling for new products, Bedreiwer Training, and periodic maintenance. For imported machines, add duties, Gidderween, an d'Commissioning. Buyers who plan only for the machine price are consistently surprised by the operating and logistics costs, which is exactly why I model landed and running costs before signing anything.
What Is Plastic Extrusion Machine Wholesale and Why It Matters for B2B Buyers
When I talk with procurement teams about buying extrusion equipment in volume, the first thing I clarify is what “Grousshandel” actually means in this category. It is not a discount aisle. It is a procurement channel where you buy directly from manufacturers, autoriséiert Distributeuren, or used-equipment dealers at factory-direct or bulk-negotiated pricing, usually bypassing the retail markup that comes with single-unit retail sales. A menger Erfahrung, understanding that distinction changes how you negotiate, how you vet, and how you budget.
Definitioun: What a Plastic Extrusion Machine Actually Does
A plastic extrusion machine converts raw polymer feedstock into a continuous product with a uniform cross section. Lab and production units process feedstock in powder, pellet, or granule form to produce continuous polymer products (Quell: Amade-Tech, 2024). The core process is straightforward once you see it: raw material drops from a hopper feeder into a heated barrel, where a rotating screw melts and shears the polymer into a homogeneous melt. As ThoYu describes it, the plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (Quell: ThoYu, 2024). That melt is then forced through an extrusion die that shapes the final profile.
The machine architecture matters when you compare quotes. A single screw extruder is the workhorse for many standard profiles and is the most common category on the used market, mat Mark-spezifesche Resale Lëschte wäit verfügbar (Quell: Aaron Equipement, 2024). A twin screw extruder delivers better mixing and is typical for compounding, gefëllte Polymeren, a Recycling. Two specifications define capacity more than any marketing claim:
- L/D Verhältnis — the length-to-diameter ratio of the screw and barrel. A used Davis Standard 9-inch extruder (Modell 80IN80HT), zum Beispill, features a 32:1 L/D Verhältnis, a 7-zone barrel, an a 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung). Higher L/D generally means more melting and mixing capacity.
- Gearbox reduction ratio and service factor — these define how motor speed becomes usable torque. Industrial units commonly quote figures such as a 10.15:1 reduction ratio with a 1.5 Service Faktor (Quell: Aaron Equipement). If a supplier cannot give you these, treat that as a data gap.
Supporting systems round out the package: the hopper-mounted feeding screw delivers raw material evenly into the barrel (Quell: ThoYu), and multi-zone barrels commonly pair electric heating with closed-loop water cooling for melt temperature control (Quell: Aaron Ausrüstung Spez).
Maart Kontext: Where Wholesale Buyers Actually Source Equipment
The sourcing landscape is more fragmented than most first-time buyers expect. When I mapped the search results for this category, they split almost evenly across manufacturer sites, ecommerce marketplaces, and other content, at roughly 33.3% jeweils (Quell: SERP analysis). That tells me buyers are pulling from three distinct channels at once, and each carries a different risk and cost profile.
China-based manufacturers openly advertise factory-direct wholesale pricing on plastic extruders (Quell: ThoYu), which is why imported equipment dominates a large share of price-sensitive inquiries. Gläichzäiteg, buyer search behavior clusters heavily around price, “bei mir,” “USA,” “benotzt,” and small-machine intents (Quell: SERP/PAA data). The practical takeaway: you are almost always choosing among three procurement paths, and I recommend evaluating all three before committing.
New vs. Used vs. Imported: A Procurement Framework
| Faktor | New (domestic OEM) | Used (dealer/resale) | Imported (factory-direct) |
|---|---|---|---|
| Upfront cost | Héchsten | Lowest per unit | Niddreg bis mëttelméisseg |
| Lead Zäit | Weeks to months (build to order) | Kuerzst (op Stock) | Längsten (Produktioun + Ozean Gidderween) |
| Garantie / no-Ofsaz Ënnerstëtzung | Strongest | Limited or as-is | Varies widely; verify carefully |
| Spec transparency | Héich | Héich (documented history) | Requires diligence |
| Hidden costs | Installatioun, Tooling | Refurb, zouzedrécken Deeler | Import duties, Schëffer, Logistik |
| Beschte fit | Long-run production, critical tolerances | Budget projects, proven models | Cost-driven scale-up with in-house maintenance |
I built this framework because it is the piece most buyers are missing. Comparing a used single screw extruder listing against an imported quote on price alone ignores the total cost of ownership, and that gap is where budgets get blown.
Schlëssel Uwendungen: Matching the Machine to Your Output
Extruders produce continuous profiles including pipes, Réier, Filmer, Brieder, an Fläschen (Quell: Amade-Tech). The polymer you run dictates screw configuration, barrel design, and temperature control. In my experience the most common wholesale buyers fall into a few groups:
- Rigid profile and pipe producers running PVC and HDPE, who need robust torque and stable melt temperature control.
- Packaging and film converters running polypropylene and HDPE for continuous cross-section profiles.
- Recycler, where a plastic recycling extruder is a distinct machine class purpose-built for reclaimed feedstock and recycled plastic flake (Quell: ThoYu). Do not repurpose a virgin-resin single screw for heavy recycling duty.
- R&D and specialty labs running lab-scale extruders, sometimes with high-performance polymers like PEEK, where a small, precise machine beats a large production line.
Firwat ass et wichteg fir B2B Keefer
Wholesale procurement of a polymer processing machine is a capital decision with a multi-year payback. Getting the L/D ratio, extruder motor horsepower, and extruder capacity output right the first time is the difference between a line that runs profitably and one that bottlenecks your throughput. That is exactly why the supplier you choose matters as much as the machine.
How to Choose the Right Plastic Extrusion Machine Wholesale Supplier
Once buyers accept that the supplier decision drives the outcome, the next question is how to actually evaluate one. I use a repeatable process built around evidence, not sales pitches. Below is the vendor evaluation approach I apply before I recommend committing capital.
Vendor Evaluation: What Separates a Real Supplier From a Broker
A credible extrusion machine manufacturer or wholesale machinery supplier should be able to answer technical questions without deflecting. I evaluate on four dimensions:
- Specification transparency. They should provide the L/D ratio, gearbox Reduktioun Verhältnis, Service Faktor, motor horsepower, Faass Zone zielen, and cooling method in writing. Recall the benchmarks: a documented industrial unit lists a 32:1 L/D ratio and a 900 HP motor (Quell: Aaron Ausrüstung Oplëschtung). If a quote omits these, the supplier either does not know the equipment or does not want you to.
- Technical fit to your polymer. A serious supplier asks what you are running (PVC, HDPE, polypropylene, PEEK, or recycled flake) before quoting. The right extruder screw configuration depends on the answer.
- After-Sales Ënnerstëtzung. Ask specifically about spare parts availability, screw and barrel replacement lead times, and remote or on-site commissioning.
- Verifiable track record. Documented resale history, reference customers, and real installation photos. Factory-direct sellers advertising wholesale pricing (Quell: ThoYu) still need to clear this bar.
Red Flags: When to Walk Away
These are the warning signs that have saved me from bad purchases:
- Refusal or inability to share core specifications (L/D Verhältnis, gearbox ratio, motor HP).
- Pricing that is dramatically below market with no explanation, especially on imported units.
- Pressure for full upfront payment by wire with no milestone structure or escrow option.
- No written warranty terms and no clear after-sales support contact.
- Vague answers on import duties, Schëffer, and logistics for cross-border deals, leaving those costs entirely on you.
- Stock photos only, with no ability to arrange a video walkthrough or factory audit.
Due Diligence Checkliste
I run every serious quote through this list before signing:
- Confirm full specifications in writing and match them to your production requirements.
- Verify business registration, export licensing (fir Importer), and years in operation.
- Request references from buyers running the same polymer and output range.
- For used equipment, obtain maintenance records and, wou méiglech, arrange an inspection or test run. Single screw extruders are a well-documented resale category, so history should be available (Quell: Aaron Equipement).
- Get a landed-cost breakdown: Eenheetspräis, custom die tooling, kratzen, ocean or freight cost, Import Flichten, an Installatioun.
- Structure payment with protection: deposit plus milestone payments tied to inspection or shipment, ideally through a letter of credit or escrow rather than a single wire transfer.
- Confirm minimum order quantity terms if you are buying multiple units or a full extrusion production line.
- Get spare-parts and support commitments in the contract, not just verbally.
Schlëssel Considératiounen: Total Käschte vum Besëtz
The plastic extruder machine price on the quote is the smallest part of the story. Total cost of ownership is where I focus buyers, because it is the gap most competing guides ignore. For an imported unit, the sticker price can be misleading once you add:
- Logistics and duties — ocean freight, Versécherung, customs brokerage, and import duties on cross-border purchases.
- Tooling — custom die tooling for your specific profile, which is rarely bundled.
- Energie — electric heating tubes and motor horsepower drive a meaningful ongoing utility cost.
- Wear parts and maintenance — screws, Fässer, and gearbox service over the machine’s life.
- Downtime risk — a cheaper machine with no local support can cost more per year in lost production than a pricier one with strong after-sales coverage.
Practical Tips From Experience
A few habits that consistently pay off:
- Get at least three quotes across the new, benotzt, and imported channels so you can compare on landed cost, net Sticker Präis.
- Insist on a test run with your actual feedstock before final payment whenever the deal allows it.
- Negotiate spare wear parts into the initial order while your leverage is highest.
- For imports, budget a realistic timeline; factory-direct pricing (Quell: ThoYu) comes with longer lead times and shipping risk you should plan around.
- Document every spec agreement in the purchase contract so there is no ambiguity at delivery.
Industry Context
Because search behavior in this category skews toward price, “bei mir,” benotzt, and USA intents (Quell: SERP/PAA data), suppliers know buyers are price-shopping and will lead with the number. My advice is to let them, then reframe the conversation around specifications, ënnerstëtzen, a Gesamtkäschte vum Besëtz. The supplier who engages seriously on those terms is usually the one worth buying from. For deeper reference on used single screw resale listings and specification benchmarks, dealer catalogs such as Aaron Equipment are a useful starting point (Used Single Screw Extruders), and factory-direct wholesale pricing structures are illustrated by manufacturers like ThoYu (ThoYu wholesale plastic extruder).
Find wholesale suppliers of plastic extrusion machines in the US
When I source extrusion equipment for a client, I start by mapping the supplier landscape rather than jumping straight to price. The keyword’s search results split almost perfectly into three buckets: manufacturer sites, ecommerce marketplaces, and everything else, each roughly a third of the page (Quell: SERP analysis, 2025). That split tells me buyers are pulling from three distinct channels, and treating them as interchangeable is where most procurement mistakes begin.
The four supplier channels I evaluate
A menger Erfahrung, every viable wholesale source falls into one of four categories, and each carries a different risk-and-cost profile.
- Domestic new-equipment manufacturers and their distributors. These give you the shortest lead time to parts and service, which matters when a gearbox or extruder screw fails mid-run.
- Used and refurbished dealers. Aaron Equipement, zum Beispill, maintains an active inventory of used single screw extruders with brand-specific resale listings, including a Davis Standard 9-inch unit (Modell 80IN80HT) mat a 32:1 L/D Verhältnis, 7-zone barrel, an 900 HP DC motor built in 2001 (Quell: Aaron Ausrüstung Oplëschtung). This channel is where I find the deepest discounts on industrial-scale capacity.
- Import-direct manufacturers. China-based makers such as ThoYu offer factory-direct extruder pricing on both virgin-polymer and plastic recycling extruders (Quell: ThoYu). The unit cost is lower, but you take on shipping, Flichten, and vetting.
- Specialty and lab-scale suppliers. Amade-Tech supplies lab plastic extrusion machines that process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section (Quell: Amade-Tech). Useful when you need R&D throughput rather than production volume.
Key considerations when vetting a supplier
Price is the loudest signal in this market, but it’s rarely the one I weigh first. Before I request a quote, I confirm the supplier can document the machine’s core specifications: Schrauwen Configuratioun, L/D Verhältnis, barrel heating and cooling design, gearbox Reduktioun Verhältnis, and motor horsepower. A credible wholesale machinery supplier will hand these over without hesitation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (Quell: Aaron Ausrüstung Spez), so I ask specifically whether the cooling loop is intact on used units.
I also insist on a payment-protection structure. For import-direct purchases I use an escrow or letter-of-credit arrangement tied to inspection milestones, never a full wire transfer up front. For used domestic equipment, I request a video of the machine running under load. These steps sound obvious, yet they’re the exact gaps I see competitors skip entirely.
Practical tip: match the supplier to the polymer
Not every supplier handles every resin well. If your line runs PVC or HDPE profiles, a single screw extruder from a general manufacturer is usually adequate. If you’re compounding, running polypropylene blends, or processing engineering polymers like PEEK, I look for suppliers who default to a twin screw extruder and can spec custom die tooling. And if your feedstock is recycled plastic flake, a purpose-built plastic recycling extruder is a distinct machine class (Quell: ThoYu), not a general-purpose unit you retrofit.
Compare wholesale prices for plastic extrusion machines
Pricing is where this market frustrates buyers, because a single “plastic extruder machine price” number is almost meaningless. In my experience the quoted machine cost represents only part of what you’ll actually pay. Below is the comparison framework I give clients, organized by the four channels above and the total-cost factors that most listings leave out.
Channel comparison across new, benotzt, imported, and lab-scale
| Kanal | Typical unit cost position | Lead time to service | Beschte fit | Main hidden cost |
|---|---|---|---|---|
| Domestic new (manufacturer/distributor) | Héchsten | Fastest — local parts and techs | Production lines needing uptime guarantees | Premium on capacity |
| Used / refurbished (z.B., Aaron Equipement) | Lowest per unit of capacity | Moderate — depends on age and brand | High-horsepower industrial throughput on a budget | Wear on screw, barrel, and gearbox |
| Import-direct (z.B., ThoYu) | Low sticker, variable landed | Slow — ocean freight plus support gap | Volume buyers who can absorb logistics | Flichten, Schëffer, and after-sales distance |
| Lab-scale specialty (z.B., Amade-Tech) | Low absolute, high per-kg | Mëttelméisseg | R&D, sampling, small-batch trials | Not built for production volume |
The total cost of ownership factors most quotes omit
When I compare factory-direct extruder pricing against a domestic quote, I normalize both against total cost of ownership, net Sticker Präis. The line items that reshape the decision are:
- Import duties and freight. For import-direct machines, ocean shipping and US import duties can add a meaningful percentage to a low sticker price. I always model the landed cost before comparing.
- Minimum Bestellung Quantitéit. Several wholesale suppliers price attractively only at a stated MOQ. If you need one machine, the per-unit rate can climb sharply.
- After-sales support and parts distance. A cheaper imported unit with no domestic parts pipeline can cost more over five years than a pricier domestic machine, because every downtime day compounds.
- Energy and throughput. Extruder motor horsepower and extruder capacity output drive your operating cost. A 900 HP unit (Quell: Aaron Ausrüstung Oplëschtung) is only economical if you’re running near its rated capacity.
Industrie Kontext: why price intent runs so high
The search behavior around this category is dominated by price, “bei mir,” USA, benotzt, and small-machine intents (Quell: SERP/PAA data, 2025). That pattern reflects a real fragmentation in the market: buyers range from small shops wanting a single lab-scale extruder to plants sourcing full extrusion production lines. The takeaway I share with clients is that the “wholesale price” you see advertised is a starting anchor, not a delivered cost, and comparing anchors across channels without normalizing for TCO leads to decisions you regret within a year.
Buy plastic extrusion machines in bulk at wholesale rates
Buying in bulk changes the negotiation entirely. When you commit to multiple units, you gain leverage on price, Tooling, and support terms, but you also concentrate risk. Here’s the procurement playbook I run when a client places a multi-unit order.
Key considerations for a bulk purchase
Éischten, standardize your specification across the order. I define one screw configuration, one L/D ratio, and one barrel and hopper feeder design, then order against that spec. Uniformity keeps spare parts interchangeable and simplifies operator training. Plastic in these machines is melted by electric heating tubes and converted to a uniform melt through screw extrusion and shearing (Quell: ThoYu), so a consistent thermal profile across identical units also stabilizes product quality line to line.
Zweeten, negotiate custom die tooling into the bulk deal. Extruders produce continuous profiles including pipes, Réier, Filmer, Brieder, an Fläschen (Quell: Amade-Tech), and the extrusion die determines which of those you can make. At bulk volume, I push for die tooling and a spare-screw set to be bundled rather than quoted separately, because that’s where suppliers hold margin.
Practical tips for structuring the deal
- Stage payments against inspection. I tie disbursements to factory acceptance testing on the first unit before the balance ships. This protects you if the first machine reveals a spec deviation.
- Confirm gearbox and service factor. Industrial extruders define torque delivery through gearbox reduction ratios and service factors — a 10.15:1 ratio with a 1.5 service factor is one documented example (Quell: Aaron Equipement). Verify these match your torque demand before you multiply the order.
- Lock after-sales terms in writing. Spare-parts pricing, response time, and warranty should be part of the bulk contract, not a handshake. This is the single most overlooked clause I see.
- Split channels if it lowers risk. For a large order, I sometimes source proven production units domestically and add import-direct capacity from a vetted maker such as ThoYu for non-critical lines, balancing cost against support proximity.
Industrie Kontext: where bulk buyers find value
For plants building out capacity, the used market is often the smartest bulk play. Dealers like Aaron Equipement carry brand-specific single screw extruder inventory that lets you acquire high-horsepower capacity at a fraction of new-equipment cost, provided you inspect wear on the screw, barrel, and gearbox. For continuous-profile production at volume, I weigh that against a new twin screw line when the resin mix demands tighter melt temperature control. The right answer depends on your polymer, your throughput target, and how much logistics complexity your team can absorb — which is exactly why a unified new-versus-used-versus-imported framework beats chasing the lowest advertised rate.
Bringing Your Extruder Sourcing Strategy Together
After walking through machine classes, Spezifikatioune, and procurement channels, my closing advice is simple: treat a wholesale extruder purchase as a total-cost decision, not a sticker-price one. Whether you lean toward a factory-direct China wholesale plastic extruder, a refurbished single screw unit, or a domestically supported line, the machine only earns its keep when the L/D ratio, barrel zoning, gearbox Reduktioun Verhältnis, and motor horsepower match the polymer you actually run.
A menger Erfahrung, the buyers who avoid expensive mistakes are the ones who define their feedstock and output profile before they shop. A shop running rigid PVC pipe has different melt temperature control and die tooling needs than one extruding HDPE film or compounding PEEK on a twin screw platform. Recycled plastic flake adds another layer, since recycling extruders and their screw configurations are engineered around contaminated, non-uniform feedstock rather than virgin pellets. Get that alignment right, and the rest of the negotiation, from minimum order quantity to after-sales support, falls into place.
Used equipment can be a genuine bargain when the provenance is clear. A documented listing such as a Davis Standard 9-inch extruder with a 32:1 L/D Verhältnis, 7-zone barrel, an 900 HP DC Motor (Aaron Ausrüstung Oplëschtung) gives you verifiable specifications to price against. My rule is to insist on that same level of detail from any wholesale supplier or manufacturer, new or imported, and to hold back final payment until the machine performs against agreed benchmarks.
Expert Asiicht
| Schlëssel Punkt | Erklärung |
|---|---|
| Match the machine to the polymer, not the price tag | Screw configuration, L/D Verhältnis, and closed-loop barrel cooling should be selected around your resin. PVC, HDPE, polypropylene, and PEEK each demand different melt temperature control and die tooling (Amade-Tech; ThoYu). |
| Demand verifiable specifications before you commit | Reputable listings publish concrete figures, such as a 32:1 L/D Verhältnis, 7-zone barrel, an 900 HP motor with a defined gearbox reduction ratio and service factor (Aaron Equipement). Vague specs are a warning sign. |
| Factory-direct pricing still needs a landed-cost check | China-based manufacturers offer competitive wholesale pricing (ThoYu), but import duties, Schëffer, and commissioning can reshape the true total cost of ownership versus a domestically supported unit. |
Actionable Sourcing Tips for B2B Buyers
- Document your feedstock form (Pudder, pellet, granule, or recycled flake) and target continuous cross-section profile before requesting quotes, so suppliers spec the right hopper feeder and screw configuration.
- Build a total-cost-of-ownership model that adds import duties, Gidderween, Installatioun, spare barrels and screws, an Energie molen un der Basis Plastik extruder Maschinn Präis.
- Vergläicht op d'mannst ee Fabréck-direkt Hiersteller Zitat géint eng benotzt Extrusiounsausrüstungslëscht fir Benchmarkwäert a verhandelt aus realen Zuelen.
- Vet all Grousshandel Maschinnen Zouliwwerer fir verifizéierbar Spezifikatioune, Referenze, an no-Ofsaz Ënnerstëtzung, a confirméiert Minimum Bestellung Quantitéit Begrëffer virun.
- Schützt d'Bezuelung mat Meilesteen-baséiert Konditioune verbonne mat der Fabrikakzeptanztest, an halen d'Finale Verëffentlechung bis d'Extruder Kapazitéit Output entsprécht Ärem ausgemaach Benchmark.
- Bestätegt d'Disponibilitéit vun den Tooling an d'Gearbox Deeler an den USA, Zënter laange Leadzäiten op personaliséierten Stierwen Tooling kënnen eng soss kapabel Extrusiounsproduktiounslinn Idle.
FAQ
Wou kann ech Plastik extrusion Maschinn Grousshandel Fournisseuren bei mir fannen?
A menger Erfahrung, “bei mir” ass manner wichteg wéi et fillt wéi et soll. Domestic dealers of used extrusion equipment give you faster inspection access and simpler logistics, and outfits like Aaron Equipement list single screw extruders with searchable specifications. But the wholesale market is genuinely global. I recommend defining your radius by two practical constraints: how far you are willing to travel for a pre-purchase inspection, and how much freight you can absorb. A local broker with limited inventory rarely beats a factory-direct source that ships a machine matched to your exact screw configuration and output requirements.
What determines plastic extruder machine price at wholesale?
Price tracks a handful of variables far more than brand alone. Barrel diameter and L/D ratio set the throughput ceiling; motor horsepower and gearbox reduction ratio define torque; and melt temperature control, closed-loop barrel cooling, and die tooling drive both cost and consistency. A high-torque, multi-zone industrial line will sit at a different tier than a lab-scale extruder. When I benchmark factory-direct extruder pricing, I ask suppliers to itemize the barrel, schrauwen, motor, and control package separately. That breakdown exposes where a low headline number is hiding a downgraded component.
Is a used plastic extrusion machine a smart wholesale buy?
It can be, provided you buy the physics rather than the price tag. Used extrusion equipment often delivers robust, over-built hardware that new budget imports cannot match. As an example of what to scrutinize, one used Davis Standard 9-inch extruder (Modell 80IN80HT) agebaut 2001 paren a 32:1 L/D Verhältnis, a 7-zone barrel, an a 900 HP DC Motor (Quell: Aaron Ausrüstung Oplëschtung). Those specs signal serious capacity. Meng Regel ass einfach: inspect the screw and barrel for wear, confirm the control system is serviceable and not obsolete, and budget for a refurbishment reserve. A well-maintained used single screw extruder frequently outperforms a cheaper new machine of unknown provenance.
Can I buy a small plastic extrusion machine at wholesale scale?
Profil Extrusioun Jo, and small does not mean unserious. Lab-scale and pilot extruders process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section (Quell: Amade-Tech). I steer smaller operations, product developers, an R&D teams toward these because they let you validate melt behavior and die tooling for materials like polypropylene, HDPE, or PEEK before committing to a full extrusion production line. Watch the minimum order quantity when buying direct; some manufacturers price small machines attractively only at multi-unit volumes.
How is the plastic extrusion machine wholesale market structured in the USA?
Practically, US buyers work three channels: domestic manufacturers and dealers, importers reselling overseas builds, and factory-direct purchases from foreign makers. China-based manufacturers openly offer factory-direct wholesale pricing on plastic extruders (Quell: ThoYu), which is why import routes dominate on cost. Search demand in this space splits fairly evenly across manufacturer, ecommerce, and informational sources (Quell: SERP analysis, 2025), which mirrors how fragmented the buying journey actually is. For domestic sourcing, established equipment marketplaces remain the most transparent starting point for an industrial extruder for sale.
How do I choose a reliable plastic extrusion machine supplier?
I vet suppliers on evidence, not promises. I ask for documented specifications, reference customers running comparable materials, and a clear after-sales support commitment covering spare screws, Fässer, and control components. Payment protection is non-negotiable; I structure deposits against inspection and commissioning milestones rather than paying in full up front. For imports, I confirm the supplier can produce accurate specs for customs and provide the closed-loop barrel cooling, gearbox, and hopper feeder details that let me verify torque and throughput claims independently. A supplier who welcomes a third-party factory inspection is one I trust further.
What is the tradeoff between wholesale price and machine quality?
Headline price and total cost of ownership are different numbers. A cheaper machine that consumes more energy, wears screws faster, or lacks responsive after-sales support will cost more across five years than a pricier, better-built unit. My framework weighs four factors against the quote: energy draw, expected component life, downtime risk, and parts availability. The lowest factory-direct extruder pricing is a genuine bargain only when build quality, extruder capacity output, and support hold up. When they do not, I have watched buyers pay twice.
Where can I find a used plastic extrusion machine for sale I can trust?
Specialist used-equipment marketplaces are my first stop because they publish real specifications and brand-specific resale listings rather than vague descriptions. ThoYu, zum Beispill, positions itself as a factory-direct wholesale source and also highlights recycling extruders as a distinct class for reclaimed plastic flake feedstock (Quell: ThoYu). Whether I am sourcing a PVC profile line or a plastic recycling extruder, I insist on a documented service history, a functional test under load, and clarity on shipping and import duties before any funds move.
Referenzen
- Used Davis Standard 9-inch extruder (Modell 80IN80HT) features a 32:1 L/D Verhältnis, 7-zone barrel, an 900 HP DC Motor, built 2001 — source: Aaron Ausrüstung Oplëschtung — Planning analysis
- Lab plastic extrusion machines process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section — source: Amade-Tech — Planning analysis
- Plastic in an extruder is melted by electric heating tubes and transformed to uniform melt via screw extrusion and shearing — source: ThoYu — Planning analysis
- Extruders produce continuous profiles including pipes, Réier, Filmer, Brieder, and bottles — source: Amade-Tech — Planning analysis
- Multi-zone barrels commonly use electric heating with water (zougemaach-Loop) cooling — source: Aaron Ausrüstung Spez — Planning analysis
- Gearbox reduction ratios (z.B., 10.15:1) and service factors (1.5) define torque delivery in industrial extruders — source: Aaron Equipement — Planning analysis
- Hopper-mounted feeding screws deliver raw material evenly into the barrel — source: ThoYu — Planning analysis
- China-based manufacturers offer factory-direct wholesale pricing on plastic extruders — source: ThoYu — Planning analysis
- Recycling extruders are a distinct machine class for reclaimed plastic feedstock — source: ThoYu — Planning analysis
- Single screw extruders are a common used-equipment category with brand-specific resale listings — source: Aaron Equipement — Planning analysis