

Негізгі қорытындылар
- Менің тәжірибемде, ең ақылды көтерме шешімдер шикізатқа машина сыныбын сәйкестендіруден басталады: бір бұрандалы экструдерлер қарапайым ПВХ өңдейді, HDPE, және полипропилен профильдері, қос бұрандалы экструдерлер композициялық және талап етілетін полимерлерге сәйкес келеді, және пластикті қайта өңдеуге арналған арнайы экструдерлер қалпына келтірілген пластик қабыршақтары үшін ерекше класс ретінде бар (көзі: ТхоЮ, 2024).
- Мен әрқашан сипаттамаларды бағадан бұрын бағалаймын. L/D қатынасы сияқты негізгі сандар, баррель аймағының саны, беріліс қорабын азайту коэффициенті, қызмет көрсету факторы, және қозғалтқыштың ат күші сізге нақты қуат туралы негізгі шығыс көрсеткішінен әлдеқайда көп айтады. Анықтама үшін, пайдаланылған Davis Standard 9 дюймдік экструдер жұптары a 32:1 L/D қатынасы және а бар 7 аймақтық баррель 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі).
- Қытайлық өндірушілердің зауыттық бағасы жаңа жабдық үшін шынымен бәсекеге қабілетті (көзі: ТхоЮ, 2024), бірақ мен оны импорттық баждарды қамтитын меншіктің жалпы құнымен салыстырамын, мұхит жүктері, такелаж, орнату, және сатудан кейінгі қолдауға қол жеткізу.
- Мен жаңадан емдеймін, пайдаланылады, және үш бөлек сатып алу жолы ретінде импортталады, әрқайсысының өзіндік айырбастары бар. Пайдаланылған нарық жетілді, бір бұрандалы экструдерлерге арналған брендке арналған тізімдер (көзі: Aaron жабдықтары), бұл жағдай мен тозуды тексере алатын болсам, оны өміршең жолға айналдырады.
- Жеткізуші тексеру және төлемді қорғау техникалық парақ сияқты маңызды. Жасалмас бұрын, Мен ең аз тапсырыс санын растаймын, жеткізу уақыттары, кепілдік шарттары, және қосалқы бөлшектердің болуы, мен төлемдерді жеткізілмеуден қорғау үшін құрылымдаймын.
- Процесс негіздері менің тексерулерімді бағыттайды: шикізат ұнтақтағы бункерлік қоректендіргіш арқылы түседі, түйіршік, немесе түйіршік пішіні, электр жылыту түтіктері арқылы балқытады, and is homogenized through screw shearing before the extrusion die shapes a continuous cross-section profile (көздері: ТхоЮ; Amade-Tech).
- I confirm thermal management up front. Multi-zone barrels typically combine electric heating with closed-loop water cooling (көзі: Aaron Equipment spec), and reliable melt temperature control is what keeps output dimensionally consistent across pipes, түтіктер, фильмдер, тақталар, және бөтелкелер.
- Screw configuration and custom die tooling define what a line can actually make, so I scope those against my product mix rather than buying generic capacity. For R&D or small runs, a lab-scale extruder built for continuous uniform-cross-section output is often the right entry point (көзі: Amade-Tech).
What Is a Plastic Extrusion Machine and How Does It Work?
When I evaluate any polymer processing machine, I start with the same mental model: экструдер - басқарылатын балқыту және пішіндеу жүйесі. Қатты пластик бір ұшына кіреді, және үздіксіз, біркелкі қима профилі екіншісі шығады. Осы екі нүктенің арасындағы барлық нәрсе дұрыс жылдамдықпен жылу мен механикалық ығысуды қолдану туралы. Бұл ағынды түсіну сенімді сатып алушыны техникалық парақтарды болжайтын біреуден ажыратады, және ол менің а деген көзқарасымды тікелей қалыптастырады Пластикалық экструзия машинасының көтерме саудасы сатып алу.
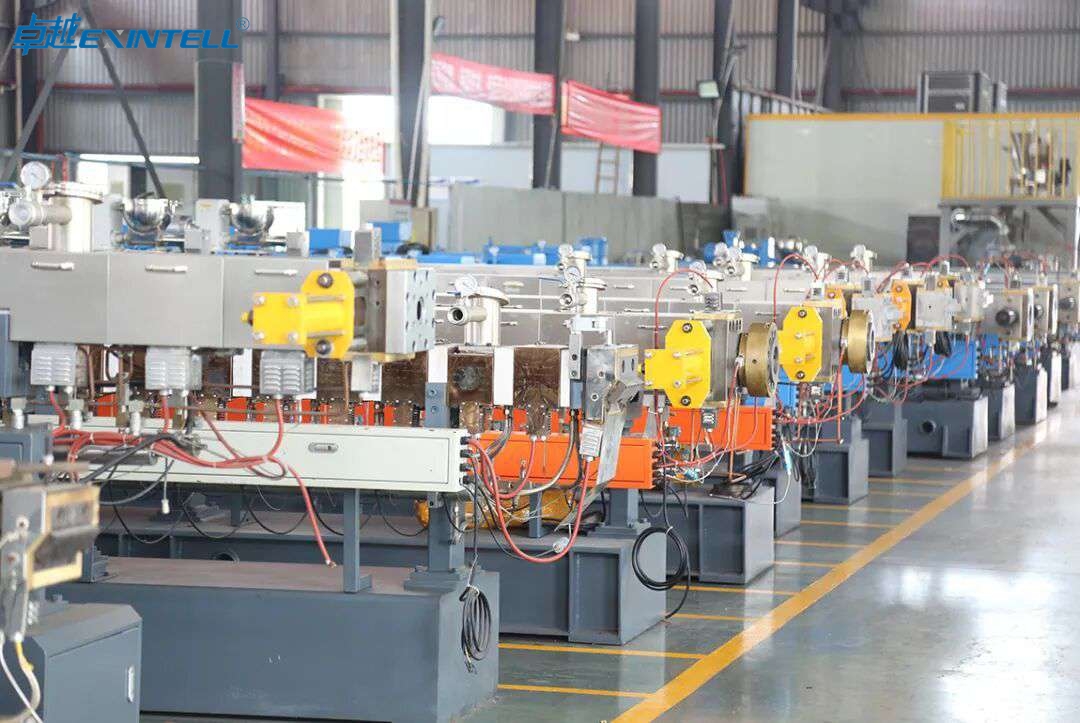
Негізгі балқыту процесі
Машинаның ішінде, қатты пластик айналмалы бұранда арқылы алға тасымалданады, ал электр жылыту түтіктері баррельді бірнеше аймаққа орап алады.. Пластмасса сыртқы жылу мен бұранда материалды бөшке қабырғасына күштеп соғатын кезде пайда болатын ішкі ығысу арқылы ериді.. ThoYu айтуынша, экструдердегі пластик электр жылыту түтіктері арқылы балқытылады және бұрандалы экструзия және кесу әрекеті арқылы біркелкі балқымаға айналады. (ТхоЮ, 2024). Бұл қос механизм, өткізгіш жылу плюс механикалық үйкеліс, сондықтан бұранда геометриясы баррель температурасы сияқты маңызды.
Балқыту температурасын бақылау - бұл кез келген дәйексөзде ең мұқият қарастыратын бөлігім. Көп аймақты бөшкелер, әдетте, әрбір аймақты тар жолақ ішінде ұстау үшін электр жылытуды жабық контурлы суды салқындатумен біріктіреді. (Aaron Жабдықтың сипаттамасы). Егер бөшке қызғандай дәл салқындата алмаса, ыстыққа сезімтал шайырларды таза іске қосу мүмкіндігін жоғалтасыз.
Іске қосуға болатын шикізат пішіндері
Сіз беретін материал сіз сатып алатын машинаны пішіндейді. Іс жүзінде мен шикізаттың төрт жалпы түрін көремін:
- Түйіршіктер — таза шайыр үшін әдепкі, өлшеуге және балқытуға оңай
- Түйіршіктер — сәл дөрекі, құрама сызықтарда жиі кездеседі
- Ұнтақ — ПВХ құрғақ қоспалары мен зертханалық жұмыстарға тән
- Қайта өңделген үлпек — ауыспалы көлемдік тығыздығы бар қалпына келтірілген материал
Amade-Tech зертханалық пластикалық экструзия машиналары шикізатты ұнтақ түрінде өңдейтінін атап өтеді, түйіршік, немесе түйіршік пішіні біркелкі көлденең қимасы бар үздіксіз полимерлі өнімдерді алу үшін (Amade-Tech, 2024). Бункерге орнатылған қоректендіру бұрандасы содан кейін бұл шикізатты бөшкеге біркелкі жеткізеді (ТхоЮ, 2024). Тіпті тамақтандыру да ұсақ-түйек емес; дәйекті емес бункер жеткізілімі дайын профильде асқын сызықтар мен өлшемді дрейф ретінде көрінеді.
Қалып шығаруды қалай қалыптастырады
Экструзия қалып - балқыма өтетін соңғы құрал, және ол өнімнің көлденең қимасын анықтайды. Құбырлар, түтіктер, фильмдер, тақталар, және бөтелкелердің барлығы бір бөшкеден әр түрлі қалыптармен келеді (Amade-Tech, 2024). Өйткені матрица үздіксіз қима профилін жасайды, one machine can serve several product lines if you invest in custom die tooling. That tooling flexibility is one reason I treat die inventory as part of the total purchase decision rather than an afterthought.
Core Components I Inspect on Every Machine
Whether I am reviewing an industrial extruder for sale or a used unit, I walk through the same component checklist:
- Бөшке — the heated cylinder, ideally multi-zone with closed-loop cooling
- Бұрандалы — the heart of melting and conveying; screw configuration determines output quality
- Мотор — extruder motor horsepower sets your throughput ceiling
- Беріліс қорабы — the reduction ratio and service factor define usable torque
- Басқару элементтері — melt temperature control and zone management
- Өл — the profile-forming tool
Two specs anchor this evaluation. Бірінші, L/D қатынасы, баррель ұзындығы бұранданың диаметріне бөлінеді, балқыманың қанша тұру уақытын алатынын айтады; пайдаланылған Davis Standard 9 дюймдік экструдер (80IN80HT үлгісі) салынған 2001 жұптар а 32:1 7 аймақтық баррельмен L/D қатынасы және а 900 HP тұрақты ток қозғалтқышы (Aaron жабдықтарының тізімі). Екінші, беріліс қорабын азайту коэффициенті және қызмет көрсету коэффициенті крутящий беруді анықтайды; сияқты өнеркәсіп бірліктері әдетте арақатынастарды тізеді 10.15:1 қызмет көрсету коэффициентімен 1.5 (Aaron жабдықтары). Бұл сандар HDPE немесе толтырылған қосылыстар сияқты тұтқыр материалдарды тоқтаусыз итеру қаншалықты қиын екенін тікелей көрсетеді..
Неліктен пластикалық экструзия машиналарын көтерме сатып алу керек?
Көтерме жол - бұл сатып алу стратегиясының сақталуын қамтамасыз ететін жер. Менің тәжірибемде, бөлшек сауда мен зауыттық тікелей сатып алу арасындағы айырмашылық сирек пайызды құрайды; ол тұтас экструзиялық өндіріс желісінің экономикасын қайта қалыптастырады. Төменде мен көтерме арналар арқылы жаппай экструзия жабдығын сатып алуды ұдайы ұсынатын төрт себебімді бөлемін.
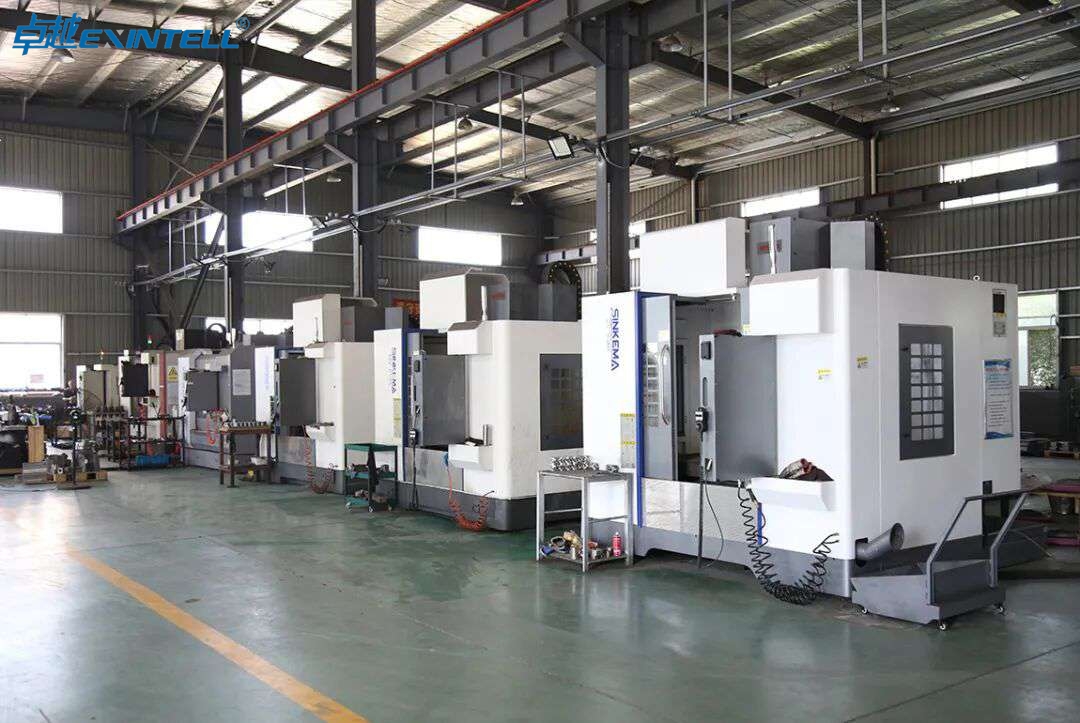
Жаппай және зауыттық тапсырыстар бойынша шығындарды үнемдеу
Зауыттың тікелей бағасы пластикалық экструдер машинасының бағасын арттыратын дистрибьютордың белгілеу қабаттарын жояды.. Қытайлық өндірушілер, мысалы, пластикалық экструдерлерге зауыттық көтерме бағаны ұсыныңыз (ТхоЮ, 2024), сондықтан бағаға байланысты іздеу мақсаты шетелдегі жеткізушілерге бағытталған. Мен бір бөлшек сауда бірлігін көтерме техника жеткізушісінің жаппай тапсырысымен салыстырған кезде, бір машинаның құны әдетте бүкіл жоба бойынша өтелімді есептеуді өзгерту үшін жеткілікті түрде төмендейді. Солай деді, зауыттық тікелей баға сіз иеленудің жалпы құнын есептегенде ғана өтеледі, a gap I address later in this guide.
Access to OEM and ODM Customization
Wholesale relationships open the door to OEM and ODM customization that retail channels rarely offer. Instead of accepting a stock configuration, I can specify screw length, barrel zones, control packages, and custom die tooling matched to my product. For anyone running a specialized continuous cross-section profile, this is the single strongest argument for buying from an extrusion machine manufacturer directly rather than a reseller.
Better Terms on Tooling and Spare Parts
The die and spare parts conversation is where wholesale terms quietly compound in your favor. Negotiating tooling and a spare-parts package into the original order almost always beats sourcing them piecemeal later. I treat wear items, бұрандалар, қыздырғыш жолақтар, және бөшкелер, as part of the initial contract, және мен жазбаша түрде сатудан кейінгі қолдау бойынша міндеттемелерді талап етемін. Сатудан кейінгі күшті қолдау - бұл желінің жұмысын қамтамасыз ететін нәрсе; онсыз, арзан машина қымбат тұйыққа айналады.
Өндіріс қуатын тиімді кеңейту
Ақырында, Көтерме сатып алу маған әр уақытта толық сатып алу циклін қайталамай-ақ, экструдер қуатын шығаруды масштабтауға мүмкіндік береді.. Бір жеткізушінің платформасында стандарттау дәйекті қосалқы бөлшектерді білдіреді, таныс басқару элементтері, және бірнеше машиналарда қайталанатын операторды оқыту. Сұраныс өскен кезде, екінші немесе үшінші бірдей құрылғыны қосу әртүрлі жеткізушілердің сәйкес келмейтін жабдықтарын біріктіруден әлдеқайда тегіс..
Пластикалық экструдерлердің түрлері: Жалғыз бұранда және қос бұранда
Бір бұрандалы экструдер мен қос бұрандалы экструдердің арасында таңдау көтерме сатып алудағы ең маңызды техникалық шешім болып табылады.. Мен оны қарапайым түрде саламын: бір бұрандалы машиналар тиімді тасымалдайды және балқытады, ал қос бұрандалы машиналар араласады және араласады. Осы сәйкестікті дұрыс қабылдаңыз және техникалық сипаттаманың қалған бөлігі орнына түседі.
Бір бұрандалы экструдерлер
Бір бұрандалы экструдер стандартты профильдер үшін төмен бағамен жұмыс істейді. Ол таза шайырды балқытуда және оны тұрақты шығу кезінде штамп арқылы итеруде керемет, бұл құбырлар үшін өте қолайлы етеді, түтіктер, және қарапайым үздіксіз профильдер. Бұл сондай-ақ ең көп қолданылатын жабдық санаты, брендке тән қайта сату тізімдері кеңінен қол жетімді (Aaron жабдықтары). Егер сіздің өнім желісі HDPE немесе полипропилен сияқты дәйекті материалдарды бекітілген қалып арқылы өткізсе, бір бұрандалы машина әдетте өнім бірлігіне ең жақсы мән береді.
Қос бұрандалы экструдерлер
Қос бұрандалы экструдер араластыру мүмкіндігі арқылы өзінің жоғары құнын алады. Екі аралық бұрандалар құрамдастыру үшін қажетті дистрибьюторлық және дисперсиялық араластыруды жасайды, толтырғыштарды қосу, бояғыштар, және тұрақтандырғыштар, және өзгермелі қасиеттері бар қайта өңделген материалдарды өңдеуге арналған. Қайта өңделген пластмасса үлпектерімен немесе PEEK сияқты ыстыққа сезімтал инженерлік полимерлермен жұмыс істегенде, қос бұранданың ығысу мен тұру уақытын жоғары бақылауы шешуші болып табылады. Қайта өңдеуге арналған экструдерлер қайта өңделген шикізат үшін арнайы жасалған машина класы екенін атап өткен жөн. (ТхоЮ, 2024), және осы желілердің көпшілігі дәл осы себепті қос бұрандалы конструкцияларға сүйенеді.
Шығару жылдамдығы және материалдың үйлесімділігі
Екі түрі шығу тәртібі мен материалдың сәйкестігі бойынша күрт ерекшеленеді. Бір бұранданың шығуы көбінесе бұранда жылдамдығы мен қозғалтқыштың ат күшіне байланысты, оны бір шайыр үшін болжауға мүмкіндік береді. Қос бұрандалы шығыс формулалар бойынша икемді, бірақ көбінесе өңделмеген өнімділікке емес, композициялық сапаға оңтайландырылған.. ПВХ құрғақ қоспалары және қайта өңделген үлпек сияқты материалдар қос бұрандамен өңдеудің пайдасын көреді, таза жалғыз шайыр бір бұрандада үнемді жұмыс істейді.
Жалғыз бұранда және қос бұранда: Салыстыру кестесі
|
Фактор |
Бір бұрандалы экструдер |
Қос бұрандалы экструдер |
|---|---|---|
|
Негізгі күш |
Стандартты профильдерді балқыту және тасымалдау |
Араластыру, құрамалау, және деволатиляция |
|
Салыстырмалы құн |
Төмен |
Жоғарырақ |
|
Ең жақсы материалдар |
HDPE, полипропилен, жалғыз таза шайырлар |
ПВХ құрғақ қоспалары, қайта өңделген үлпек, толтырылған немесе PEEK қосылыстары |
|
Араластыру сапасы |
Шектеулі |
Өте жақсы (дисперсиялық және дисперсиялық) |
|
Типтік өнімдер |
Құбырлар, түтіктер, қарапайым профильдер |
Қосылыстар, мастер-бет, қайта өңделген түйіршіктер |
|
Қолданылған нарықтағы қолжетімділік |
Кең, брендке тән тізімдер жиі кездеседі |
Тарырақ, көбірек мамандандырылған |
|
Идеал сатып алушы |
Тұрақты өнім желісі, шығындарға бағытталған |
Қайта өңдеу, реттелетін тұжырымдар, Р&D |
|
Фактор |
Бір бұрандалы экструдер |
Қос бұрандалы экструдер |
|---|---|---|
|
Негізгі күш |
Стандартты профильдерді балқыту және тасымалдау |
Араластыру, құрамалау, және деволатиляция |
|
Салыстырмалы құн |
Төмен |
Жоғарырақ |
|
Ең жақсы материалдар |
HDPE, полипропилен, жалғыз таза шайырлар |
ПВХ құрғақ қоспалары, қайта өңделген үлпек, толтырылған немесе PEEK қосылыстары |
|
Араластыру сапасы |
Шектеулі |
Өте жақсы (дисперсиялық және дисперсиялық) |
|
Типтік өнімдер |
Құбырлар, түтіктер, қарапайым профильдер |
Қосылыстар, мастер-бет, қайта өңделген түйіршіктер |
|
Қолданылған нарықтағы қолжетімділік |
Кең, брендке тән тізімдер жиі кездеседі |
Тарырақ, көбірек мамандандырылған |
|
Идеал сатып алушы |
Тұрақты өнім желісі, шығындарға бағытталған |
Қайта өңдеу, реттелетін тұжырымдар, Р&D |
Түрді өнім желісімен сәйкестендіру
Менің шешімім қарапайым. Егер мен тұрақты материалды тұрақты профильге экструд жасасам, Мен бір бұрандалы станокты таңдап, үнемдеуді тапсырыс бойынша дайындалған аспаптар мен қосалқы бөлшектерге жұмсаймын. Егер менің процессім құрамдасуды қамтыса, түсі өзгереді, немесе қайта өңделген шикізатты өңдейтін пластикті қайта өңдеуге арналған экструдер, Мен қос бұрандалы платформаны көрсетемін және процесті басқару құны ретінде жоғары бағаны қабылдаймын. Өнімді әзірлеуге арналған зертханалық масштабтағы экструдерді өлшейтін сатып алушылар үшін, сол логика кішірек шығыста қолданылады: бұранда түрін формуланы дәлелдеп жатқаныңызға сәйкестендіріңіз (егіз) немесе профиль (бойдақ). Бұрандалы шешімді нақты өнім желісіне бекіту, тек басты бағаға қарағанда, көтерме сатып алу толық қызмет ету мерзімінде өтелетін нәрсе. сияқты жеткізушілер мен қайта сату тізімдеріндегі нақты конфигурацияларды қарап шығуға болады Aaron Equiment пайдаланған бір бұрандалы инвентарь және ThoYu көтерме экструдер беттері бұл спецификациялардың іс жүзінде қалай пайда болатынын көру үшін.
Пластикалық экструзия машинасы қанша тұрады?
Клиенттер менен бір нөмір сұрағанда, Мен оларға шын жауабымды айтамын: пластикалық экструзия машинасының құны бірнеше мың доллардан миллионнан астам долларға дейін, және таралу толығымен ауқымға қатысты. Менің тәжірибемде үш деңгейлі жабдықты сатып алу, баға диапазондары шығару қуаты бойынша таза үзіледі, бұрандалы конфигурация, және сізге қажет автоматтандыру деңгейі. Баға сұрамас бұрын, бұл сіздің қай деңгейге жататынын білуге көмектеседі, өйткені зертханалық экструдер мен өнеркәсіптік экструзияны өндіру желісі басқа баға белгісімен бірдей сатып алу емес.. Олар әртүрлі машиналар. Қайта өңделетін жеңіл пластик қаптама
Масштаб бойынша баға диапазондары: Зертхана, Кішкентай, және өнеркәсіптік
Мен сатып алушыларды үш практикалық санатқа топтастырамын. Зертханалық масштабтағы экструдерлер жинақы, R үшін жасалған үстелдік немесе еден қондырғылары&D, күрделі сынақтар, және материалды сипаттау. Олар шикізатты ұнтақ түрінде өңдейді, түйіршік, немесе түйіршік пішіні біркелкі көлденең қимасы бар үздіксіз полимерлі өнімдерді алу үшін (Amade-Tech). Шағын коммерциялық бөлімшелер аз көлемді өндіріспен айналысады, прототиптеу жұмыстары жүргізіледі, және тауашалық профильді жұмыс. Өнеркәсіптік машиналар құбырға арналған толық экструзия өндіру желілерін басқарады, фильм, тақта, және тәулік бойы бөтелке шығару.
Міне, сандар әдетте мен жинаған тырнақшаларға және жалпыға қолжетімді тізімдерге негізделген. Оларды жоспарлау ауқымдары ретінде қарастырыңыз, тұрақты бағалар емес, өйткені бұрандалы конфигурация және құрал-саймандар оларды айтарлықтай өзгертеді.
| Деңгей | Әдеттегі шығыс | Бұрандалы түрі | Жаңа баға диапазоны (АҚШ доллары) | Қолданылған баға диапазоны (АҚШ доллары) |
|---|---|---|---|---|
| Зертханалық масштабтағы экструдер | ~5 кг/сағ дейін | Бір немесе қос бұранда | $8,000 – $45,000 | $4,000 – $25,000 |
| Шағын жарнама | ~20 – 150 кг/сағ | Бір бұрандалы экструдер | $30,000 – $120,000 | $12,000 – $60,000 |
| Өнеркәсіптік желі | 300 кг/сағ және одан жоғары | Бір немесе қос бұрандалы экструдер | $150,000 – $1,000,000+ | $50,000 – $400,000 |
Өнеркәсіптік жолақтың жоғарғы шеті жүк тасымалдау сияқты төменгі ағынды жабдықтары бар толық сызықтарды көрсетеді, салқындату цистерналары, және орауыштар, плюс балқыма температурасын бақылау. Жалаңаш экструдер басы кілт тапсыру желісіне қарағанда әлдеқайда аз тұрады, сондықтан жеткізушілерді салыстырмас бұрын әрқашан бағаның нені қамтитынын растаңыз.
Стикер бағасының артында не тұрады
Төрт айнымалы санды басқаларға қарағанда көбірек жылжытады. Сыйымдылығы айқын: бөшкенің диаметрі және қозғалтқыш ат күші бар өткізу қабілеті таразылары, және екеуі де шығындарды қосады. Бренд маңызды, өйткені экструзиялық машина өндірушісінің машинасы сенімділік пен бөлшектердің қолжетімділігіне байланысты жоғары бағаға ие.. Жағдай бүкіл нарықты жаңа және пайдаланылған деп бөледі, мен төменде егжей-тегжейлі қарастырамын. Ал құрал - бұл тыныш бюджет шығыны. Арнайы үздіксіз қима профилі үшін теңшелетін қалып ондаған мың долларды қоса алады, және ол көбінесе машинаның өзінен бөлек келтіріледі.
Баға ұсыныстарынан тыс жасырын шығындар
Сатып алу бағасы сирек меншіктің жалпы құны болып табылады, және бұл жерде мен бірінші рет сатып алушылардың күйіп қалғанын көремін. Машинадан тыс, осы жол элементтері үшін бюджет:
- Арнайы қалыптау құралы іске қосуды жоспарлаған әрбір өнім профилі үшін.
- Орнату және такелаж ауыр өнеркәсіп бөлімшелері үшін, бұл көбінесе кранға қызмет көрсетуді және күшейтілген еденді қажет етеді.
- Электр және коммуналдық қызметтерді жаңарту жоғары ат күші бар қозғалтқыштарды және жабық контурлы баррельді салқындату жүйелерін жеткізу үшін.
- Жүк және, импорт үшін, міндеттері Мен оны осы нұсқаулықтың логистика бөлімінде бөлемін.
- Қосалқы тозу бөлшектері ауыстыру бұрандалары сияқты, бөшкелер, және қыздырғыш жолақтар.
- Commissioning and operator training, especially for automated control systems.
Менің ережем: add 15 дейін 30 толық орнатылғанын бағалау үшін машина бағасына пайыз, дайын өндіріс құны. Skipping this math is the single most common planning mistake I encounter.
Plastic Extrusion Machine Wholesale Price: What Drives It?
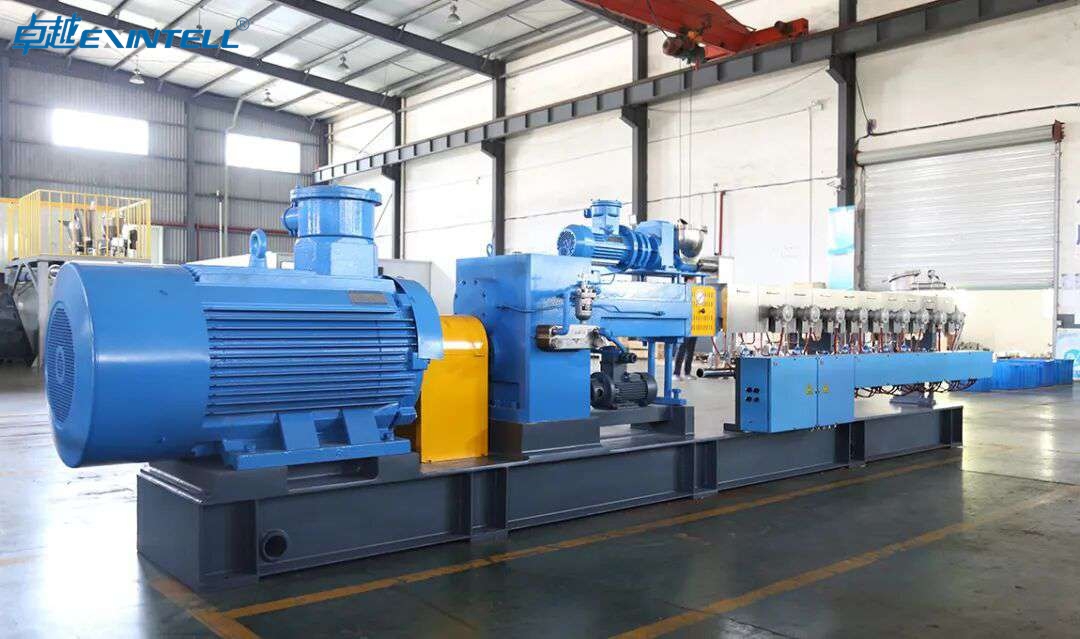
Wholesale pricing follows the same logic as retail, but with more room to negotiate and more variables to scrutinize. When I evaluate a factory-direct extruder price, whether from a domestic dealer or a China-based supplier offering wholesale rates (ТхоЮ), I work through a consistent checklist of specifications. Each one has a direct line to cost, and understanding them lets you compare quotes on equal terms instead of guessing.
Screw and Barrel Specifications
The screw and barrel are the heart of the machine, and they define both capability and price. The most important spec is the L/D ratio, the length-to-diameter ratio of the screw. A higher L/D ratio delivers better mixing and melt uniformity, which matters for demanding polymers. Анықтама үшін, пайдаланылған Davis Standard 9 дюймдік экструдер (80IN80HT үлгісі) runs a 32:1 L/D ratio with a 7-zone barrel (Aaron жабдықтарының тізімі). More zones mean finer melt temperature control, since plastic is melted by electric heating tubes and converted to a uniform melt through screw shearing (ТхоЮ).
Screw configuration also decides the machine class. A single screw extruder is the workhorse for straightforward profiles and is the most common used-equipment category (Aaron жабдықтары). A twin screw extruder costs more but excels at compounding, mixing additives, and processing recycled plastic flake. If you are running PVC, HDPE, or polypropylene at volume, бұрандалы геометрия шайырға сәйкес келуі керек; PEEK және басқа да жоғары өнімді полимерлер сізді мамандандырылғанға қарай итермелейді, құны жоғары конфигурациялар. Қос бұрандалы экструдерлерді өндіруші
Мотор және беріліс қорабы ат күші
Экструдер қозғалтқышының ат күші өткізу қабілеті мен үшін тікелей прокси болып табылады, сондықтан, бағасы. Дәл сол Davis Standard қондырғысы өз бөшкесін а 900 HP тұрақты ток қозғалтқышы (Aaron жабдықтарының тізімі), Бұл оның ауыр өнеркәсіп өндірісі үшін салынғанын көрсетеді. Беріліс қорабы қозғалтқыш қуатын бұрандадағы қолданылатын моментке айналдырады. сияқты қысқарту коэффициенттері 10.15:1 айналасындағы қызмет көрсету факторымен біріктірілген 1.5 машина жүктеме кезінде қаншалықты қауіпсіз түрде жеткізе алатынын анықтаңыз (Aaron жабдықтары). Мен екі бірдей бағадағы машинаны салыстырған кезде, жоғарырақ қызмет көрсету коэффициенті көбірек төзімділікті көрсетеді, бұл сіз қатты жұмыс істеуді жоспарлап отырған жабдыққа төлеуге тұрарлық.
Автоматтандыру және басқару жүйелері
Control systems separate a basic machine from a modern one. Manual temperature dials and simple relays keep the price down but demand skilled operators and produce more scrap. PLC-driven systems with closed-loop barrel cooling, рецепт сақтау, and data logging cost more upfront but pay back through consistency and lower waste. A hopper feeder with a hopper-mounted feeding screw that delivers raw material evenly into the barrel (ТхоЮ) is standard, but gravimetric feeding and automated blending add cost and precision. For high-volume operations, I consider automation a value driver rather than a luxury.
Certifications and Origin
Origin and certification shape both price and risk. Domestic and European machines command higher prices, partly for build quality and partly for support proximity. Қытайлық өндірушілердің зауыттық бағасы (ТхоЮ) машинаның құнын айтарлықтай төмендете алады, бірақ CE белгісін тексеру керек, АҚШ нарығы үшін UL сәйкестігі, және орындамас бұрын құжатталған электр қауіпсіздігі. Мен әрқашан жазбаша түрде сертификаттау құжаттарын сұраймын, өйткені сертификатталмаған машинаны АҚШ-тың электрлік кодексіне сәйкес қайта жабдықтау импортты тартымды еткен үнемдеуді жояды..
Жаңа және пайдаланылған пластикалық экструзия машиналары
Бұл мені ең көп сұрайтын шешім, және менің жауабым әрқашан бірдей: бұл сіздің тәуекелге төзімділік пен уақыт кестесіне байланысты. Пайдаланылған экструзия жабдығы күрделі шығындарды екі есе немесе одан да көп қысқартуы мүмкін, бірақ жинақ нақты экспозициямен бірге келеді. Жаңа машиналар қымбатырақ және жиі жеткізу мерзімі ұзағырақ болады, yet they arrive with warranties, current controls, and predictable performance. Let me lay out both sides the way I would for a client.
Capital Savings vs Risk on Used Units
The financial case for used equipment is strong. As the pricing table above shows, a used industrial unit can run 40 дейін 60 жаңа пайыздан төмен, freeing capital for tooling and downstream equipment. For a startup or a shop testing a new product line, that difference can be the whole business case. The risk is that a polymer processing machine has wear components, screws and barrels degrade, heater bands fail, and motors lose efficiency, and those problems are not always visible in a listing photo. The savings are real, and so is the possibility of buying someone else’s problem.
Inspecting Condition, Hours, and Build Year
I never buy used equipment sight unseen, and I recommend you do not either. My inspection priorities, in order:
- Бұрандалар мен бөшкелердің тозуы: measure clearances if possible. Excessive clearance kills output and melt quality, and a replacement screw and barrel set is expensive.
- Build year and operating hours: a machine built in 2001, like the Davis Standard example, can still be excellent if maintained, but you need service records to judge.
- Жылыту және салқындату жүйелері: confirm all barrel zones heat correctly and that closed-loop water cooling holds temperature.
- Motor and gearbox condition: listen for bearing noise and check for oil leaks and gearbox play.
- Control panel function: verify every zone reads and controls accurately, since older controls may lack replacement parts.
When feasible, insist on a powered demonstration running actual Plastic Pellet Manufacturers материал. A cold machine hides most of its problems.
Warranty and Support Gaps on Used Equipment
The support gap is the cost that does not show on the invoice. New machines from an extrusion machine manufacturer typically include warranty coverage, іске қосу бойынша көмек, and access to after-sales support. Used units are usually sold as-is, so you own every failure from day one. Before I buy used, I confirm two things: that spare parts remain available for that model, and that a service technician familiar with the brand can be reached. A cheap machine with no parts pipeline is a liability, not a bargain.
Resale Value Considerations
Ақырында, think about the exit before you enter. Machines from recognized brands hold their value far better on the secondary market, which is exactly why brand-specific resale listings command steady demand (Aaron жабдықтары). If there is any chance you will resize or exit within a few years, buying a well-known single screw extruder, even at a premium, protects your capital on the way out. Менің тәжірибемде, resale strength is the most overlooked factor in the new versus used debate, and it often tips a borderline decision toward the established brand.
My bottom line: buy new when uptime is critical, support matters, and you plan to run the machine for a decade. Buy used when capital is tight, you have the technical capacity to inspect and maintain the equipment, and you stick to reputable brands with living parts supply. Either way, do the total cost of ownership math first, because the quote is only the beginning of the spend.
Дереккөздер: Aaron жабдықтары, Used Single Screw Extruders; ТхоЮ, Wholesale Price China Plastic Extruder; Amade-Tech, Lab Plastic Extrusion Machine.
Where to Find Used Plastic Extrusion Machines Wholesale
When I source equipment on a tight capital budget, the used market is usually my first stop. A well-maintained secondhand extruder can deliver 80 дейін 90 percent of the service life of a new unit at a fraction of the cost, provided you know how to read a listing and verify condition before wiring any funds. The challenge is not finding machines. It is separating a genuine bargain from a decommissioned liability.
Marketplaces and Dealers Worth Knowing
Most of my used purchases have come through established dealer networks rather than open classified listings. Specialized resellers such as Aaron Equipment maintain rotating inventories of single screw and twin screw extruders, and they photograph, tag, and often power-test each unit before listing it. That vetting matters. A dealer with a physical yard and a reputation to protect gives me recourse that an anonymous marketplace posting never will. I still cross-check auction houses and industry-specific listing boards, but I treat a reputable dealer as the baseline for used extrusion equipment.
Reading a Listing Like an Engineer
A used listing is a spec sheet in disguise, and three numbers tell me most of what I need to know before I ever call. Consider a real example: пайдаланылған Davis Standard 9 дюймдік экструдер (80IN80HT үлгісі) салынған 2001, advertised with a 32:1 L/D қатынасы, a 7-zone barrel, және а 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі).
- L/D қатынасы. The barrel length-to-diameter ratio governs residence time and mixing. А 32:1 ratio suits demanding melt homogeneity work; shorter ratios around 24:1 handle simpler profiles. If your polymer needs thorough melting, do not buy short.
- Barrel zones. Seven independently controlled heating zones give me granular melt temperature control across the barrel length. More zones mean finer thermal tuning, which is critical for heat-sensitive resins.
- Motor horsepower. А 900 HP drive signals a high-throughput production machine, not a lab tool. Motor HP scales roughly with output capacity, so match it to your target line speed rather than buying more drive than your die can use.
Listings also disclose the gearbox reduction ratio and service factor, which together define usable torque. А 10.15:1 reduction with a 1.5 қызмет көрсету факторы, мысалы, tells me the drivetrain has headroom for sustained duty (көзі: Aaron жабдықтары). I read those figures as a durability signal, сілтеме емес.
Brands That Hold Value on the Resale Market
Brand reputation follows a machine into its second life. Davis Standard, менің тәжірибемде, commands a premium on the resale market precisely because parts, бұрандалар, and service documentation remain available years after manufacture. That liquidity cuts both ways: I pay more up front, but I recover more when I resell, and I spend less time hunting for a replacement extruder screw configuration or barrel liner. When I compare two similar used units, a supported brand almost always wins on total cost of ownership even at a higher sticker price.
Verifying Condition Before You Commit
I never buy a used extruder on photographs alone. My pre-purchase checklist runs through the wear points that quietly drain performance:
- Бұрандалар мен бөшкелердің тозуы. Request bore measurements. Worn clearances degrade output and pressure stability, and reconditioning a barrel is expensive.
- Heater and thermocouple health. Confirm every zone reaches and holds setpoint. Dead zones on a multi-zone barrel are a red flag.
- Drive and gearbox. Listen for bearing noise and check for oil leaks. A failing gearbox can cost as much as the machine.
- Салқындату жүйесі. Many industrial units use electric heating with closed-loop water cooling (көзі: Aaron Equipment spec). Verify the cooling circuit is intact and free of scale.
- Run test. Whenever possible, I insist on a powered demonstration under load, not just a cold spin.
If a seller resists an inspection or a run test, I walk. The savings on a used polymer processing machine evaporate the moment you have to rebuild a drivetrain.
Small and Lab-Scale Plastic Extrusion Machines
Not every buyer needs a 900 HP monster. A large share of the search interest around this keyword points toward small and near-me machines, and that tracks with what I see in practice: Р&D командалары, университеттер, and startups need compact extruders that fit a lab bench and run on standard power. These machines trade throughput for flexibility, and for the right use case that is exactly the trade you want.
What Lab-Scale Machines Actually Do
A lab-scale extruder processes feedstock in powder, түйіршік, немесе түйіршік пішіні біркелкі көлденең қимасы бар үздіксіз полимерлі өнімдерді алу үшін (көзі: Amade-Tech). The core physics is identical to production equipment: a hopper feeder delivers raw material evenly into the barrel, electric heating tubes melt the polymer, and the screw shears and homogenizes it into a uniform melt before the extrusion die shapes the output (көзі: ТхоЮ). The difference is scale, not principle, which is what makes lab machines so useful for process development. What you learn at bench scale transfers to production.
Typical Products and Use Cases
I reach for a lab-scale unit in three situations:
- Р&D and formulation. Testing new resin blends, қоспалар, or recycled plastic flake without committing a production line.
- Прототиптеу. Producing sample films, түтіктер, and small profiles for customer approval or tooling validation.
- Low-volume production. Serving niche markets where demand does not justify a full extrusion production line.
These machines readily handle common thermoplastics like PVC, HDPE, және полипропилен, and higher-spec units extend to engineering polymers such as PEEK when the barrel and screw are rated for the elevated melt temperatures.
Footprint and Power Requirements
The practical appeal of a lab extruder is that it lives in an ordinary room. Many bench units draw single-phase or light three-phase power and occupy a footprint measured in a few square feet, versus the dedicated bay and heavy three-phase service a production extruder demands. Before buying, I confirm two things: the electrical service my facility can supply, and whether the cooling requirement is air or water. Getting the utilities wrong is the most common reason a small machine sits idle after delivery.
Knowing When to Upgrade to Production Scale
A lab machine has a ceiling, and recognizing it early saves money. I plan the jump to production scale when sustained order volume outpaces the machine’s extruder capacity output, when I am running multiple shifts just to keep up, or when per-unit cost on the small line exceeds what a production extruder would deliver. The signal is economic, not emotional: once the lab unit becomes the bottleneck rather than the tool, it is time to scale. I typically keep the lab machine anyway, redeployed for the R&D work it does best.
Lab-Scale vs Production Extruders at a Glance
| Атрибут | Зертхана / Small-Scale Extruder | Production Extruder |
|---|---|---|
| Primary use | Р&D, прототиптеу, low-volume runs | Continuous commercial production |
| Typical motor | Fractional to ~20 HP | 50 дейін 900+ HP (мысалы, 900 HP Davis Standard) |
| L/D қатынасы | ~20:1 дейін 25:1 | 24:1 дейін 32:1 |
| Barrel zones | 2 дейін 4 | 5 дейін 7+ |
| Power service | Single-phase / light 3-phase | Heavy 3-phase |
| Із | Benchtop to compact floor unit | Dedicated production bay |
| Шығару | Grams to low kg/hr | Hundreds of kg/hr |
Figures for the production column reflect the specification range seen in listings such as the Davis Standard 80IN80HT (көзі: Aaron жабдықтары); lab-scale ranges reflect typical bench-unit configurations.
Buying Plastic Extrusion Machines Wholesale in the USA
Search intent around this keyword leans heavily toward USA and near-me queries, and that reflects a real procurement decision every US buyer faces: buy domestic or import. Factory-direct pricing from overseas manufacturers is genuinely attractive, and I have bought imported equipment when the numbers justified it. But the sticker price is only one line in the ledger. Here is how I weigh the domestic option.
The Case for Domestic Dealers
Buying from a US-based dealer or manufacturer gives me three advantages that rarely show up on a spec sheet but always show up in operations:
- Faster lead times. A machine in a domestic yard ships in days, not the weeks of ocean transit and customs clearance an import requires. Сызық төмендегенде, that speed is worth real money.
- Easier service and parts. Domestic support means same-timezone technicians, stocked spare parts, және ауыстырылатын беріліс қорабында немесе бөшкеде халықаралық жүк жоқ. Сатудан кейінгі қолдау экструдер иелігіндегі ең төмен бағаланған жалғыз фактор болып табылады.
- Стандарттардың сақталуы. АҚШ машиналары әдетте UL және NEC электр талаптарына сәйкес жасалған немесе сертификатталған. Бұл сәйкестік орнатуды жеңілдетеді, сақтандырушыларды қанағаттандырады, және сертификатталмаған импорт қажет болуы мүмкін қайта жаңартусыз тексеруден өтеді.
Сәйкестік міндетті емес
Мен бұл туралы тікелей айтқым келеді, өйткені ол бірінші рет импорттаушыларды жібереді. UL тізімінде жоқ немесе NEC стандартына сәйкес келмейтін экструдер нысанның электрлік тексеруінен өтуі мүмкін., жарамсыз сақтандыру өтемі, және OSHA экспозициясын жасаңыз. АҚШ стандарттарына сәйкес келетін импорттық машинаны қайта жабдықтау, басқару элементтерін қайта қосу, жылытқыштарды ауыстыру, сертификатталған қауіпсіздік блоктарын қосу, сатып алу бағасына жинаған ақшаңыздың көп бөлігін тұтынуы мүмкін. Мен импорттамас бұрын, I confirm exactly what certification the unit carries and what it will cost to close any gap.
Cost Tradeoffs: Domestic vs Imported
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (көзі: ТхоЮ), and for high-volume standardized equipment that pricing can be compelling. But the landed cost of an import includes freight, сақтандыру, импорттық баждар, кедендік делдалдық, және ішкі көлік, none of which appear in the quoted machine price. Layer on longer lead times, potential language and timezone friction on support, and any compliance retrofit, and the gap narrows considerably. Менің ережем: I model total cost of ownership over the first three years, not the purchase price, before deciding. On that basis, domestic often wins for equipment I need serviced quickly, while imports can win for planned capacity additions where lead time is not urgent.
How I Vet a Wholesale Supplier
Whether domestic or overseas, I run every wholesale machinery supplier through the same gate before committing capital. I confirm the minimum order quantity and whether it fits my actual need, request references from buyers running the same machine class, verify certifications in writing rather than taking a catalog claim at face value, and structure payment with protection, staged milestone payments or an escrow arrangement rather than a full wire against a promise. For imports specifically, I clarify Incoterms so I know exactly where the seller’s responsibility ends and mine begins. A supplier who answers these questions clearly is one I can build a relationship with; one who deflects is one I pass on.
Finding Wholesale Suppliers Near You
When I start a sourcing project for bulk extrusion equipment, I map suppliers in concentric circles: local, regional, then global. Proximity carries real value that rarely shows up on a quote, and I have learned to weigh it deliberately before chasing the lowest number.
Local vs Regional Sourcing Benefits
A supplier within a few hours’ drive lets me tour the floor, watch a machine run my resin, and shake hands with the service manager who will pick up the phone at 2 таңғы. during a line-down event. Regional suppliers widen the pool of available inventory and specialization while keeping domestic warranty terms and familiar payment protections intact. Менің тәжірибемде, the closer the vendor, the shorter the mean-time-to-repair, and for a single screw extruder running continuous cross-section profile work, downtime is the expense that quietly dwarfs the purchase price.
Installation and Service Proximity
Такелаж, leveling, wiring a 900 HP DC drive, and commissioning a 7-zone barrel with closed-loop cooling all go smoother when the technician is local. A used Davis Standard 9-inch extruder (80IN80HT үлгісі) а 32:1 L/D ratio and 900 HP motor, салынған 2001, is a serious piece of iron to install and dial in (көзі: Aaron жабдықтарының тізімі). I want the people who know that machine within reach for melt temperature control tuning and screw configuration adjustments during the first production weeks.
Trade Shows and Industry Directories
Two channels consistently surface credible vendors for me. Trade shows such as NPE: The Plastics Show and Fakuma put dozens of extrusion machine manufacturers in one hall, where I can compare a twin screw extruder against a single screw side by side and collect real spec sheets. For structured search, I lean on Thomasnet and the used-equipment marketplaces like Aaron Equipment, which maintains brand-specific resale listings for single screw extruders (көзі: Aaron жабдықтары). Directories are a starting shortlist, үкім емес, so I always follow up with a plant visit or video walkthrough.
China vs US Suppliers: Weighing the Tradeoffs
The decision I face most often is factory-direct pricing from overseas versus the service density of a domestic partner. Neither wins outright. The right call depends on your volume, your in-house maintenance capability, and how much lead-time risk your production schedule can absorb.
Balancing Local Price with Global Options
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders, and that gap can be substantial on comparable specifications (көзі: ТхоЮ). US suppliers, and used domestic equipment, close part of that gap when you factor in freight, міндеттері, and the cost of coordinating support across time zones. I treat the sticker price as one input into total cost of ownership, not the deciding figure.
Lead Time and Shipping Considerations
Domestic used equipment can ship in days; a new overseas extrusion production line typically runs on a build-plus-ocean-freight timeline measured in months. Ocean transit, port handling, and inland drayage all add weeks and variability. If your project has a hard launch date, that schedule risk deserves a line in your model alongside the price advantage.
Қолдау, Parts, and Language Logistics
This is where I have seen buyers underestimate the friction. Time-zone offsets stretch troubleshooting cycles, spare gearbox and screw components may ship internationally, and technical documentation quality varies. Before committing overseas, I confirm English-language manuals, a named support contact, and a stocked or expedited parts channel for wear items like screws, бөшкелер, және қыздырғыш жолақтар.
China vs US Sourcing at a Glance
| Фактор | Шетелде (мысалы, Қытай) factory-direct | US supplier / domestic used |
|---|---|---|
| Бірлік бағасы | Ең төменгі, factory-direct wholesale (көзі: ТхоЮ) | Higher new; competitive on used inventory (көзі: Aaron жабдықтары) |
| Тоқтау | Build plus ocean freight, typically months | Days to weeks for in-stock units |
| Жер құны | Жүкті қосыңыз, міндеттері, drayage | Add domestic freight and rigging |
| Service proximity | Қашықтан, уақыт белдеуіне байланысты | On-site or regional |
| Parts availability | International shipping, plan ahead | Domestic stock, жылдамырақ айналдыру |
| Құжаттама & language | Verify English manuals and support | Native-language support |
Менің ережем: high volume with a capable maintenance team favors overseas factory-direct; tight timelines or lean staffing favor domestic. Note that SERP demand for this keyword splits evenly across manufacturer, ecommerce, and informational content at roughly 33.3% әрқайсысы (көзі: SERP analysis, 2025), and buyer searches cluster around price, “жанымда,” “АҚШ,” және “пайдаланылады” intents (көзі: SERP/PAA data, 2025) — a fair reflection of how mixed real purchasing behavior is.
How to Choose a Plastic Extrusion Machine Manufacturer
Once I have a shortlist, I run every candidate through the same vetting sequence. The goal is to separate a genuine polymer processing machine partner from a broker who will disappear after the wire transfer clears.
Quality Assurance and Factory Verification
I verify the factory before I verify the price. For overseas vendors that means a live video walkthrough or a third-party inspection of the production floor, weld quality on the extruder barrel, and evidence they actually build rather than resell. I ask to see a machine running feedstock in powder, түйіршік, or granule form to confirm they handle continuous polymer output the way their marketing claims (көзі: Amade-Tech). Seeing the heating tubes and screw shearing melt real resin into a uniform stream tells me more than any brochure (көзі: ТхоЮ).
Track Record and Reference Customers
I request three reference customers running similar materials, whether that is PVC pipe, HDPE профилі, polypropylene sheet, немесе PEEK сияқты талап етілетін инженерлік полимер. A manufacturer with a documented history in your specific application has already solved the problems you are about to encounter. If a vendor cannot produce references, I treat that as a signal, not an oversight.
Customization and Application Expertise
The best manufacturers speak fluently about screw configuration, L/D ratio selection, and custom die tooling for your exact profile. Extruders produce a wide range of continuous products, including pipes, түтіктер, фильмдер, тақталар, және бөтелкелер (көзі: Amade-Tech), and each demands different tooling and thermal setup. I probe how they size the gearbox reduction ratio and service factor to my torque needs, drawing on published industrial examples such as a 10.15:1 ratio at a 1.5 қызмет көрсету факторы (көзі: Aaron жабдықтары). A vendor who can discuss whether a single screw or twin screw extruder fits my recycled plastic flake feedstock, and how the hopper feeder delivers material evenly, has earned a closer look.
After-Sales Support and Parts Availability
I put the support terms in writing before purchase: response-time commitments, commissioning assistance, операторларды оқыту, and guaranteed availability of wear parts like screws, бөшкелер, and heater elements. For a plastic recycling extruder or any line running abrasive reclaimed material, wear-part supply is not optional, it is the difference between a productive asset and expensive scrap. I confirm lead times on those parts specifically, since that is what governs real-world uptime.
Certifications and Quality Systems
Ақырында, I check the paperwork that signals a disciplined operation. ISO 9001 indicates a functioning quality management system, and CE marking matters if the equipment enters or transits European jurisdictions. For a US install I confirm the electrical build can meet UL and NFPA 79 күту, бері а 900 HP DC drive with multi-zone electric heating and closed-loop water cooling (көзі: Aaron Equipment spec) has to satisfy my local inspector and my insurer. Certifications do not guarantee quality on their own, but their absence usually correlates with corners cut elsewhere.
Vetting sources I return to include ThoYu for factory-direct wholesale context (ThoYu wholesale listing) and Aaron Equipment for used single screw extruder benchmarks (Aaron Equipment used extruders).
Decoding Key Specifications Before You Buy
Every wholesale quote I review lists a wall of specifications, and most buyers I coach fixate on price before they understand what those numbers actually deliver. Менің тәжірибемде, four figures tell you more about a machine’s real capability than the headline output rate does: L/D қатынасы, the number of heating and cooling zones, the screw diameter, and the motor-to-gearbox pairing. Read those correctly and you can predict melt quality, энергия тарту, and output ceiling before the machine ever ships.
L/D Ratio and Its Impact on Melting and Mixing
The L/D ratio expresses the screw’s effective length divided by its diameter, and it governs how much residence time the polymer gets inside the barrel. A longer L/D gives the melt more distance to homogenize, which matters when you run temperature-sensitive or highly filled compounds. Анықтама үшін, пайдаланылған Davis Standard 9 дюймдік экструдер (80IN80HT үлгісі) I analyzed lists a 32:1 L/D қатынасы (көзі: Aaron жабдықтарының тізімі), which sits at the higher end for single-screw machines and signals strong melting and mixing headroom.
As a rough guide, емдеймін 24:1 дейін 26:1 as adequate for straightforward commodity resins, 28:1 дейін 32:1 as the sweet spot for consistent mixing and venting, and anything longer as specialty territory for demanding compounds. A single screw extruder built for basic profile work rarely needs the same length as one processing recycled plastic flake with variable bulk density. If a supplier can’t tell you the L/D ratio, that’s a signal the listing is thin on engineering detail.
Number of Heating and Cooling Zones
Multi-zone barrels let you stage the temperature profile from feed throat to die, and more zones mean finer control over melt temperature. The Davis Standard unit referenced above uses a 7-zone barrel (көзі: Aaron Equipment spec), which gives an operator granular control across the length of the screw. Plastic in an extruder is melted by electric heating tubes and converted into a uniform melt through screw shearing (көзі: ТхоЮ), so the zone count directly shapes how evenly that transition happens.
Cooling is the other half of the equation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (көзі: Aaron Equipment spec), which pulls heat back out when shear or process feedback pushes a zone above setpoint. When I vet a machine, I confirm both the heating zone count and whether cooling is air or closed-loop water. Water cooling responds faster and holds tighter melt temperature control, which pays off on precision products.
Screw Diameter and Output Rate
Screw diameter is the single strongest predictor of throughput. Output scales roughly with the cube of the diameter, so a modest jump in screw size produces a large jump in kilograms per hour. That relationship is why a 9-inch machine like the Davis Standard example carries a 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі) — the mass of material moving through a large-diameter screw demands proportionally more drive power.
When comparing wholesale offers, always normalize output against diameter and resin type. A quoted output of, айту, 300 kg/hr means little without knowing whether it was measured on low-density film resin or a stiff PVC compound. I ask suppliers to state the resin, балқу температурасы, and screw speed used for their rated output, then compare like with like.
Motor HP and Gearbox Reduction Ratio
The motor and gearbox work as a matched pair. Motor horsepower sets the available power, while the gearbox reduction ratio converts high-speed, low-torque motor output into the low-speed, high-torque rotation the screw needs. Industrial extruders publish both the ratio and a service factor — for example, а 10.15:1 reduction with a 1.5 қызмет көрсету факторы (көзі: Aaron жабдықтары) — and that service factor tells you how much margin the drivetrain carries above nominal load.
I treat the service factor as a durability indicator. A gearbox rated 1.5 is designed to absorb shock loads and continuous duty without premature wear, which is exactly what you want on a machine running multiple shifts. A hopper-mounted feeding screw delivers raw material evenly into the barrel (көзі: ТхоЮ), and that steady feed keeps torque demand predictable so the gearbox operates within its rated envelope.
Matching Machine Capacity to Your Production Volume
Specifications only matter once you tie them to your actual demand. The most expensive mistakes I see in wholesale procurement come from sizing decisions, not from picking a bad brand. Online Plastics Recycling Marketplace Buy too small and you’ll run the line flat out with no cushion for growth; buy too large and you’ll carry idle capital, higher energy bills, and startup scrap on every short run.
Estimating Throughput Needs
Start with your target finished-product volume, then work backward. I calculate required output in kilograms per hour by taking monthly demand, dividing by realistic operating hours, and adding an allowance for scrap and changeover. A useful sanity check: if you need 40,000 kg per month and run a single shift of about 160 өнімді сағаттар, сізге шамамен қажет 250 kg/hr of sustained output, and I’d size for 300 kg/hr to leave headroom.
Feedstock form affects this math too. Lab and production extruders process feedstock in powder, түйіршік, or granule form for continuous polymer products with uniform cross section (көзі: Amade-Tech), and bulk density varies enough between those forms that the same screw can deliver noticeably different mass throughput. Confirm your rated output against the feedstock you’ll actually run.
Avoiding Under- and Over-Sizing
Undersizing forces the machine to run at maximum screw speed constantly, which raises melt temperature, accelerates wear, and leaves zero margin for demand spikes. Oversizing is subtler but real: an oversized extruder run at low speed can produce poor mixing and unstable output, and you pay for motor and heating capacity you never use. My rule is to target a machine that hits your peak demand at roughly 75 дейін 85 percent of its rated capacity, which keeps it in an efficient, controllable band.
Planning for Future Growth
Wholesale machinery is a multi-year commitment, so I plan sizing against a two-to-three-year demand forecast, not today’s orders. Солай деді, buying far ahead of demand ties up capital you could deploy elsewhere. A middle path I often recommend: size the extruder for near-term growth, but confirm the extrusion production line’s downstream equipment and the supplier’s screw and die options can scale, so you upgrade tooling rather than replacing the whole line.
Batch vs Continuous Production
Extrusion is inherently a continuous process — extruders produce continuous profiles including pipes, түтіктер, фильмдер, тақталар, және бөтелкелер (көзі: Amade-Tech) — so the batch-versus-continuous question is really about how your business schedules work. If you run long stable jobs, a larger continuous line maximizes efficiency. If you run many short jobs with frequent material and color changes, prioritize fast changeover and quick thermal response over raw size, because your losses will come from transitions, not from top-line speed.
| Production profile | Typical screw diameter | Indicative output | Suggested L/D | Ең қолайлы |
|---|---|---|---|---|
| Зертхана / Р&D and small runs | 20–45 mm | Up to ~50 kg/hr | 24:1–28:1 | Сынама алу, small-batch, PEEK trials |
| Шағын жарнама | 50–75 мм | ~80–250 kg/hr | 26:1–30:1 | Профильдер, small pipe, specialty film |
| Mid-volume production | 90– 120 мм | ~300–600 kg/hr | 28:1–32:1 | HDPE pipe, парақ, continuous profile |
| Жоғары көлемді / heavy industrial | 150 mm and up | 600 кг/сағ және одан жоғары | 30:1–32:1+ | Large pipe lines, pallet, қайта өңделген үлпек |
I treat these ranges as a starting frame for supplier conversations, not fixed rules. Actual output always depends on resin, melt temperature control, and screw configuration, so I verify each figure against a supplier’s tested data for my specific material.
Extruders for Specific Products: Құбыр, Фильм, Парақ, Pallet
The extruder is only the melt engine. What defines your finished product is the extrusion die and the downstream line built around it. When I evaluate a wholesale package, I look at the die and tooling as closely as the machine itself, because that’s where product quality and application fit are actually determined.
Pipe and Tube Extrusion Lines
Pipe and tube lines pair the extruder with an annular die, a vacuum calibration and cooling tank, a haul-off, and a cutter or coiler. For PVC and HDPE pipe, dimensional stability and wall concentricity are everything, so tight melt temperature control and steady output matter more than peak speed. I confirm the die is matched to my target diameter range and that the calibration tooling is included or clearly quoted, since retooling for a new pipe size is a recurring cost buyers often overlook.
Film and Sheet Die Configurations
Film and sheet share extrusion fundamentals but diverge at the die. Blown film uses an annular die with an air ring and tower; cast film and sheet use a flat T-die or coat-hanger die feeding a chill-roll or three-roll stack. Polypropylene and polyethylene dominate here, and die width plus lip adjustment set your thickness tolerance. When comparing offers, I ask specifically which die configuration is included and whether the lip is manually or automatically adjustable, себебі бұл өлшеуішті интернетте қаншалықты тығыз ұстай алатыныңызды анықтайды.
Паллет және профиль қолданбалары
Паллет және ауыр профильді өндіріс - бұл үлкен машиналар мен қайта өңделген шикізаттың кездесетін жері. Қытайлық өндірушілер паллет өндіруге арналған пластикалық экструдерлерге зауыттық көтерме бағаны ұсынады (көзі: ТхоЮ, ThoYu паллет экструдері), және бұл жолдар жиі қалпына келтірілген материалды өткізеді. Қайта өңдеуге арналған экструдерлер - қайта өңделген пластик шикізатына арналған ерекше машина класы (көзі: ТхоЮ), сондықтан қайта өңделген пластик қабыршағын өңдеуді жоспарласаңыз, Мен таза шайырлы экструдерді — қоректендіру бөлімін бейімдеудің орнына, ол үшін жасалған машинаны сатып алуға кеңес беремін., желдету, және тозу беттері басқаша салынған.
Теңшелетін қалып пен құрал опциялары
Арнайы қалыпқа арналған құрал - бұл жалпы мақсаттағы экструдерді нақты өнімді жасайтын машинаға айналдыратын нәрсе. Whether you need a bespoke profile cross section, a specific pipe wall structure, or a particular sheet width, I confirm three things with the supplier upfront: lead time for custom tooling, whether tooling design is in-house or subcontracted, and the cost of future die changes. A capable extrusion machine manufacturer will quote tooling as a clear line item and stand behind dimensional performance, which also tells you something about the after-sales support you’ll receive once the line is running.
For buyers exploring the used market, single screw extruders are a well-established resale category with brand-specific listings (көзі: Aaron жабдықтары). When I consider used equipment for a specific product, I always verify that compatible dies and calibration tooling exist for my application, since a bargain machine with no path to the right tooling isn’t a bargain at all.
Processing Recycled Plastics with Wholesale Extruders
When I evaluate a wholesale extruder for a recycling operation, I start from a different premise than I would for virgin resin processing. Reclaimed feedstock is inconsistent, contaminated, and thermally sensitive, so the machine has to compensate for material variability that a virgin-only line never sees. Recycling extruders are a distinct machine class built for reclaimed plastic feedstock (көзі: ТхоЮ, 2025), and treating them as interchangeable with standard profile extruders is one of the more expensive mistakes I have watched buyers make.
Recycling Extruders and Material Preparation
The extruder itself is only one stage in a longer chain. Before recycled plastic flake reaches the hopper feeder, it typically passes through washing, кептіру, and size reduction. A hopper-mounted feeding screw delivers raw material evenly into the barrel (көзі: ТхоЮ, 2025), and even that step becomes harder when the input is irregular flake rather than uniform pellets. Менің тәжірибемде, the quality of upstream preparation determines whether the extruder runs stably or surges. If you are quoting a wholesale line and the supplier only prices the extruder, ask specifically about the material prep equipment, because the melt quality you get downstream depends on it.
The core melting mechanism is unchanged: plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (көзі: ТхоЮ, 2025). What changes with reclaim is how much shear and residence time the material can tolerate before it degrades. HDPE and polypropylene reclaim are relatively forgiving; PVC regrind is far less so and punishes overheating quickly.
Why Twin Screw Extruders Excel with Reclaim
For consistent recycled output, I lean toward a twin screw extruder over a single screw extruder in most reclaim applications. The reason is mechanical. Twin screw configurations provide better mixing, more controllable shear, and stronger devolatilization, which matters when the feedstock carries moisture and volatiles picked up during its first life. A single screw extruder remains a common and cost-effective used-equipment category with brand-specific resale listings (көзі: Aaron жабдықтары, 2025), and it can handle clean, well-prepared regrind. But when feedstock quality is uneven, the extruder screw configuration in a twin screw machine gives me the process latitude to keep melt temperature control tight across batches.
The tradeoff is cost. Twin screw machines carry higher purchase and tooling prices, and the gearbox is more complex. That is a real budget line, not a rounding error, so I weigh it against the value of the finished product. High-value recycled compounds justify the investment; commodity reclaim often does not.
Contamination and Filtration Considerations
Contamination is the defining challenge of recycled feedstock, and filtration is how you manage it. A melt filtration system, usually a screen changer with a fine mesh pack, removes particulate before the melt reaches the extrusion die. Without adequate filtration, contaminants cause surface defects, weak spots, and clogged dies. I always confirm two things with a wholesale supplier: the screen changer type (manual, hydraulic, or continuous) and the finest mesh the system supports without excessive pressure buildup. For heavily contaminated post-consumer streams, a continuous screen changer avoids the production stoppages that manual changes force.
Multi-zone barrels commonly use electric heating with closed-loop water cooling (көзі: Aaron Equipment spec, 2025), and precise zone control becomes even more important with reclaim because you are trying to melt inconsistent material without scorching the fraction that heats fastest.
Circular Manufacturing Opportunities
The commercial case for recycling extruders keeps strengthening. Brand commitments to recycled content and tightening regulation on single-use plastics are pushing demand for in-house reprocessing. I see two viable models. The first is closed-loop: reprocessing your own production scrap back into the same line, which improves yield and reduces raw material spend. The second is a dedicated recycling line that converts purchased post-industrial or post-consumer feedstock into salable pellets or profiles. Both turn a waste stream into either cost savings or revenue, and the extruder is the pivot point of that conversion.
Certifications and Standards to Look For
Certification is where wholesale procurement, әсіресе шетелдік жеткізушілерден, gets serious. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (көзі: ТхоЮ, 2025), and that pricing is genuinely attractive. But a low quote means nothing if the machine cannot be legally installed, insured, or operated in your jurisdiction. I treat certification as a gating requirement, not a nice-to-have.
CE Marking for European Compliance
If you operate in or export to the European Economic Area, CE белгісі міндетті болып табылады. It signals that the machine conforms to relevant EU directives, most notably the Machinery Directive, covering mechanical safety, күзетші, and emergency stops. For a US buyer this may seem irrelevant, but I raise it because many buyers plan to resell finished goods into Europe or operate multinational facilities. Confirm the CE marking is backed by an actual Declaration of Conformity and a technical file, not just a sticker on the frame. A legitimate manufacturer produces the paperwork on request.
ISO 9001 Quality Management
ISO 9001 certifies that the manufacturer runs a documented quality management system. It does not certify any individual machine, and I want to be precise about that distinction because suppliers sometimes blur it. What ISO 9001 tells me is that the factory has repeatable processes for design, өндіріс, and inspection, which correlates with more consistent build quality across units. For wholesale buyers ordering multiple machines or planning repeat purchases, that process consistency is exactly what protects you from unit-to-unit variation.
UL for US Electrical Safety
АҚШ нарығы үшін, UL certification on electrical components is the one I refuse to compromise on. Extruders draw significant power through motors, қыздырғыш жолақтар, and control cabinets. A used Davis Standard 9-inch extruder, мысалы, runs a 900 HP DC motor across a 7-zone barrel (көзі: Aaron жабдықтарының тізімі, 2025), and that scale of electrical load makes safety certification a genuine risk-management issue, формальдылық емес. UL or an equivalent NRTL listing affects your ability to pass local electrical inspection, secure insurance, and satisfy OSHA expectations. Imported machines frequently ship with control systems that are not UL-listed, so budget for potential panel rework or re-certification in the US.
Documentation and Compliance Verification
Certificates are only as good as your ability to verify them. My verification routine is straightforward:
- Request certificate numbers and check them against the issuing body’s public database rather than trusting a PDF.
- Confirm the certificate covers the specific model, not a different machine in the product family.
- Ask for the Declaration of Conformity, wiring diagrams, and the operation and maintenance manual before you release final payment.
- Where feasible, commission a third-party pre-shipment inspection to confirm the physical machine matches the documentation.
Tying compliance verification to your payment milestones is the single most effective piece of leverage you have as a wholesale buyer. Once the machine ships, that leverage is gone.
Understanding Total Cost of Ownership
The purchase price is the number everyone fixates on, and it is the one that matters least over the life of the machine. Мен иеленудің жалпы құнын үлгілеген кезде, I fold in energy, техникалық қызмет көрсету, тоқтау уақыты, және орнату, and the ranking of suppliers frequently reverses once those costs are included. This is the analysis that most wholesale buying guides skip, and it is where a slightly cheaper machine can quietly become the expensive one.
Energy Consumption and Operating Cost
Energy is the largest recurring cost for most extrusion operations, and it is driven by motor horsepower and heater load. А 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі, 2025) running multiple shifts represents a substantial electricity bill, and small efficiency differences compound over thousands of operating hours. Multi-zone barrels using electric heating with closed-loop water cooling (көзі: Aaron Equipment spec, 2025) are more efficient at holding temperature than older uninsulated designs. I ask suppliers for the connected load and, мүмкін болған жерде, the specific energy consumption per kilogram of throughput, because that figure lets me compare machines on an operating-cost basis rather than a sticker basis.
Maintenance and Spare Parts
Тозу сөзсіз. The screw and barrel are the primary wear components, and processing abrasive or filled materials accelerates it. Recycled plastic flake with residual contamination wears tooling faster than clean virgin resin. Gearbox maintenance also matters: industrial extruders define torque through gearbox reduction ratios such as 10.15:1 қызмет көрсету коэффициентімен 1.5 (көзі: Aaron жабдықтары, 2025), and that gearbox needs scheduled lubrication and periodic inspection. My practical concern with wholesale and imported machines is spare parts lead time. A cheap machine whose screw takes three months to replace from overseas is not cheap when the line sits idle waiting.
Downtime and Reliability
Downtime is the cost that does not appear on any invoice, which is exactly why it gets underestimated. Every hour a line is down is lost production plus fixed overhead still accruing. Reliability is where established brands and ISO 9001 manufacturers tend to justify their premium. When I assess reliability, I look at build quality on the components that fail expensively, the availability of local service technicians, and the supplier’s after-sales support commitments. A responsive supplier that ships parts quickly is worth more than a marginally lower purchase price.
Installation and Commissioning Expenses
The final and most frequently forgotten category is getting the machine running. Installation and commissioning cover rigging and placement of heavy equipment, electrical and cooling-water hookups, control integration, and the trial runs needed to dial in melt temperature control and output. For imported machines I also budget for potential electrical re-certification and any adaptation to US voltage and plant infrastructure. Commissioning support from the manufacturer, whether on-site or remote, has real value here, and I confirm whether it is included in the quote or billed separately.
Total Cost of Ownership Comparison
The table below illustrates how the cost picture shifts across three common procurement paths. The figures are representative ranges for planning purposes, тұрақты тырнақшалар емес, and actual costs vary with capacity, спецификация, және жеткізуші.
| Cost Factor | New Domestic (АҚШ) | Imported Factory-Direct | Қолданылған / Refurbished |
|---|---|---|---|
| Сатып алу бағасы | Ең жоғары | Ең төменгі | Төмен және орташа |
| Certification readiness | UL/CE typically included | Often needs verification or rework | Әртүрлі; verify by age and origin |
| Энергия тиімділігі | Current-generation controls | Varies by build quality | Older units may run less efficiently |
| Spare parts lead time | Қысқа | Ұзын (overseas shipping) | Depends on brand support |
| Орнату / пайдалануға беру | Vendor support common | May require added budget | Often buyer-managed |
| Downtime risk | Ең төменгі | Орташа және жоғары | Орташа; condition-dependent |
My takeaway from running this comparison repeatedly is that the imported factory-direct route wins on purchase price but requires you to budget deliberately for certification, қосалқы бөлшектер логистикасы, және пайдалануға беру. The used route can be excellent value when the machine comes from a reputable brand with parts still available, which is why brand-specific resale listings (көзі: Aaron жабдықтары, 2025) are worth studying carefully. New domestic equipment costs the most up front and often justifies it through lower downtime and simpler compliance. Decide by modeling your own numbers across the full ownership horizon, not by the quote alone.
Жеткізілім, Import Duties, және логистика
When I buy a plastic extrusion machine wholesale from an overseas source, the quoted machine price is only the beginning of the conversation. The moment I move from a domestic used unit to factory-direct extruder pricing out of China, logistics becomes a project in its own right. A single screw extruder with a long barrel, a heavy gearbox, and a full extrusion production line footprint does not travel like a pallet of parts. I plan the freight and customs path before I sign, because a surprise here erases the savings that made the import attractive in the first place.
Жүк, Crating, және Incoterms
The first term I nail down is the Incoterm, because it defines exactly where the seller’s responsibility ends and mine begins. In my experience three matter most for extrusion equipment:
- EXW (Бұрынғы жұмыстар) — I take ownership at the factory gate and pay for everything after, including inland transport in the origin country. Cheapest on paper, most work for me.
- FOB (Бортта тегін) — the supplier delivers to the origin port and loads the vessel. This is my default for a first deal with a new wholesale machinery supplier because it splits responsibility at a clean point.
- CIF (Құны, Сақтандыру, Жүк) — the seller arranges ocean freight and insurance to my destination port. Convenient, but I always ask for the itemized breakdown so I can compare it against an independent forwarder quote.
Crating is not a line item I skip. An industrial extruder for sale overseas ships as a heavy, oddly balanced load, and the extruder barrel, экструзиялық қалып, and hopper feeder each need to be secured against vibration and moisture during a five- to eight-week ocean transit. I insist on a fumigated hardwood or steel-reinforced crate, desiccant packs inside sealed control cabinets, and a packing list that itemizes every component. For anything over roughly two meters wide or 10 тонна, I confirm whether the load qualifies as out-of-gauge, because that changes the container type and the price.
US Import Duties and Customs
US import duty on plastics processing machinery generally falls under Harmonized Tariff Schedule heading 8477, резеңке немесе пластмассаларды өңдеуге арналған машиналарды қамтиды. Base most-favored-nation duty rates in this heading are frequently low or zero, but I never assume the rate — I confirm the exact HTS subheading for my specific machine with a licensed customs broker before purchase (көзі: АҚШ халықаралық сауда комиссиясы, Үйлестірілген тарифтік кесте, 2025, hts.usitc.gov). Beyond the base duty, I check for any additional Section 301 tariffs that apply to goods of Chinese origin, since those have been adjusted repeatedly and can add a meaningful percentage to landed cost.
On top of duty I budget for the standard federal fees: the Merchandise Processing Fee and, for ocean shipments, the Harbor Maintenance Fee. I also file the ISF (Импорттаушы қауіпсіздік файлы, the “10+2”) at least 24 hours before the goods load overseas, because a late filing draws a penalty that has nothing to do with the machine’s value. A customs broker handles these filings for me, and their fee is small relative to the risk of getting them wrong.
Lead Time Planning
I build my schedule backward from the date I need the polymer processing machine running. A realistic timeline for a made-to-order extrusion production line from Asia looks like this:
- Manufacturing and assembly: 6 дейін 12 weeks depending on custom die tooling and screw configuration
- Factory acceptance and third-party inspection: 1 дейін 2 апта
- Ocean transit to a US West Coast port: 3 дейін 5 апта (longer to East Coast)
- Customs clearance and drayage: 1 дейін 2 апта
- Inland freight, такелаж, және орнату: 1 дейін 3 апта
That puts a typical door-to-commissioning window at three to six months. I treat any supplier who promises dramatically less with healthy skepticism.
Rigging and Site Delivery
The final hundred meters are the ones people underestimate. A loaded extruder does not roll off a truck on its own. I arrange a rigging crew with the right forklift or crane capacity, verify that my facility’s dock, doorways, and floor loading can accept the machine’s footprint and weight, and confirm the power drop matches the extruder motor horsepower — a 900 HP DC motor draws very differently than a modest lab-scale extruder. On one project I nearly missed that the closed-loop barrel cooling system needed a dedicated water supply already plumbed before the rigging crew arrived. Now that check is on my pre-delivery list every time.
Payment Terms and Buyer Protections
Sending a large deposit to a factory I have never visited on another continent is the moment where a wholesale extruder deal feels riskiest. I manage that risk with payment structure, not just trust. The goal is simple: I want money to move only as the supplier hits verifiable milestones, and I want a neutral mechanism holding the leverage until I confirm the machine is what I paid for.
Letters of Credit and Escrow
For larger orders I favor a documentary аккредитив (LC). My bank commits to pay the supplier only when the supplier presents the exact documents my LC specifies — bill of lading, тоғанақ парағы, inspection certificate, and so on. The paperwork discipline of an LC protects both sides, and it signals to a serious extrusion machine manufacturer that I am a professional counterparty. The tradeoff is bank fees and rigidity: any document discrepancy can hold up release, so I draft the required-documents list carefully.
For mid-sized deals, a third-party escrow service or a marketplace with built-in trade assurance offers similar protection with less overhead. The escrow agent holds my funds and releases them on agreed conditions. I read the release triggers closely, because an escrow that releases on shipment rather than on acceptance does far less for me.
Deposit and Milestone Structures
The structure I return to most often for a factory-direct order is a 30/40/30 split, and I have found it balances the supplier’s cash-flow needs against my protection:
- 30% депозит to begin production
- 40% on completion, paid after a successful factory acceptance test and third-party inspection, before the machine ships
- 30% balance after delivery, орнату, and successful commissioning at my site
I resist any pressure toward a 50% or larger upfront deposit from a supplier I do not have history with. The single most important lever I hold is that final payment tranche tied to on-site performance. If it is fully paid before the machine runs at my facility, I have given away my only real remedy.
Contract and Inspection Clauses
A wire transfer confirmation is not a contract. I insist on a purchase agreement that spells out, ең аз:
- Detailed technical specifications: бұранданың диаметрі, L/D қатынасы, extruder screw configuration, gearbox reduction ratio and service factor, barrel zones, heating and cooling method, and rated capacity output
- Acceptance criteria tied to measurable output — for example, a specified throughput in kilograms per hour on a named resin such as HDPE or PVC, at a stated melt temperature control tolerance
- Right to third-party inspection before shipment, at my discretion
- Penalty and remedy clauses for late delivery or failed acceptance
- Governing law, dispute resolution venue, және кепілдік шарттары
I tie the acceptance clause to a real production condition rather than a vague “machine works” statement. “Produces continuous cross-section profile at 300 kg/hr on virgin polypropylene within spec” is enforceable. “Functional” is not.
Reducing Overseas Transaction Risk
Beyond structure, a few habits reduce my exposure. I pay to the company’s registered corporate bank account, never to a personal account or a sudden last-minute change of banking details — that redirection is a common fraud pattern. I keep all commitments in writing. And I match my payment protection to deal size: an LC for a full extrusion production line, escrow or trade assurance for a single mid-range machine, and even for a modest used unit I still hold a meaningful balance until commissioning.
Vetting Suppliers and Verifying Quality
Payment protection limits my downside, but it does not put a working machine on my floor. That comes from vetting the supplier well and verifying the equipment before it ships. Since the SERP for this category splits evenly across manufacturers, ecommerce platforms, and other content (көзі: SERP analysis, 2025), buyers land in front of very different seller types, and the diligence I apply has to flex accordingly. A factory-direct manufacturer, a marketplace reseller, and a used-equipment dealer each deserve a different set of questions.
Factory Audits and References
Before I commit to a new extrusion machine manufacturer, I verify they actually build what they sell. I ask for their business license and registration, confirm how long they have operated, and request references from prior US or export customers — then I actually call those references. When the order justifies it, I commission an on-site factory audit, either through a sourcing agent or an inspection firm. The auditor confirms the factory exists, has real production capacity, and is not simply a trading company drop-shipping another workshop’s output. Trading companies are not automatically a problem, but I want to know which one I am dealing with, because it changes who is accountable for after-sales support.
Third-Party Inspection Services
I treat pre-shipment inspection as non-negotiable on any significant purchase. An independent inspector — from a global firm like SGS, TÜV, Bureau Veritas, or a specialist machinery inspector — visits the factory before the balance-triggering milestone. They verify that the build matches the contracted specifications: the correct extruder barrel construction, screw and die tooling, gearbox rating, motor horsepower, және басқару жүйесі. A pre-shipment inspection report is one of the documents I list in my letter of credit, which links the money release directly to verified quality. The inspection fee is trivial next to the cost of receiving a machine that does not meet spec after it has cleared customs.
Sample Runs and Acceptance Testing
Specifications on paper are a promise; a sample run is proof. I ask the supplier to run the machine on my actual feedstock — whether that is virgin resin, recycled plastic flake, or a specific grade of PEEK or polypropylene — and produce the profile I intend to make. I want to see documented throughput, dimensional tolerance on the continuous cross-section, surface quality, and stable melt temperature control across the barrel zones. For a recycling extruder in particular, testing on real reclaimed material rather than clean pellets tells me whether the screw configuration and feeding system will actually handle my input. Where possible, I have this run witnessed by my third-party inspector or captured on video with live instrument readings.
Warranty and Service Commitments
The last thing I verify is what happens after the machine is running. I get the warranty in writing — typical coverage runs 12 айлар, sometimes longer on the mechanical structure — and I read what it excludes. Then I look past the warranty to practical serviceability: whether spare parts for the gearbox, жылытқыштар, and screw are stocked or reasonably available, what the lead time is for a critical replacement, whether the supplier provides commissioning support and operator training, and whether remote technical support is available in a time zone and language I can work with. A cheaper machine from a supplier with no realistic service path is not the bargain it looks like.
Supplier Vetting Comparison
Келіссөздерді нақты ету үшін, here is how I weigh the three seller types I most often evaluate when buying extrusion equipment. This maps to the new-versus-used-versus-imported procurement decision that runs through the whole purchase.
| Vetting factor | Factory-direct manufacturer (шетелде) | Online marketplace / reseller | Domestic used-equipment dealer |
|---|---|---|---|
| Typical price position | Lowest per-spec; factory-direct extruder pricing | Ортасы; platform markup added | Айнымалы; strong value on legacy brands |
| Баптау (бұранда, өлу, L/D қатынасы) | High — built to order | Төмен және орташа | None — as-is condition |
| Lead time to running | 3–6 months incl. логистика | Varies with stock and origin | Fastest — often weeks |
| Inspection method | Factory audit + pre-shipment inspection | Platform assurance + independent check | In-person condition assessment |
| Payment protection | Letter of credit / milestone escrow | Trade assurance / escrow | Standard domestic terms |
| Кепілдік & қызмет | New warranty; verify parts pipeline | Depends on seller | Шектеулі немесе жоқ; dealer-dependent |
| Ең қолайлы | Custom production line, шығындарға негізделген | Standard machines, орташа көлем | Proven brands like a used single screw extruder, fast need |
Both ends of that table are legitimate paths. China-based manufacturers offer genuine factory-direct wholesale pricing on plastic extruders (көзі: ТхоЮ, ТхоЮ), while the domestic used market lists brand-specific machines such as a Davis-Standard 9-inch single screw extruder with a 32:1 L/D қатынасы, seven-zone barrel, және 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі, Aaron жабдықтары). The right choice depends on how much customization, жылдамдық, and service I need, and the vetting discipline above is what turns any of these into a purchase I can stand behind.
Орнату, Пайдалануға беру, және Тренинг
Buying the machine is only half the transaction. Менің тәжірибемде, the gap between a signed purchase order and a line running at rated output is where most first-time buyers lose weeks and margin. I treat installation, пайдалануға беру, and training as a single project with its own timeline, not an afterthought bundled into shipping. What follows is the sequence I use to bring a new or used extruder from crate to steady-state production.
Site and Utility Requirements
Before the freight arrives, I confirm the site can actually support the equipment. Industrial extruders draw serious power and generate real heat, so utility planning comes first. A used Davis Standard 9-inch extruder, мысалы, ships with a 900 HP DC motor and a 7-zone barrel (көзі: Aaron жабдықтарының тізімі, 2024), which tells me immediately that a standard 240V shop feed will not cut it. I map four requirements before delivery:
- Electrical service: Confirm voltage, кезең, and amperage against the motor and heater load. Extruder motor horsepower drives the largest single draw, and multi-zone barrels add electric heating loads on top of that.
- Салқындату: Multi-zone barrels commonly pair electric heating with water-based closed-loop cooling (көзі: Aaron Equipment spec, 2024). I verify chiller capacity, ағын жылдамдығы, and water quality before day one.
- Floor and access: An extrusion production line with downstream haul-off, салқындату цистерналары, and cutters needs linear floor space and a level, load-rated slab. I measure the full line, not just the extruder footprint.
- Ventilation and safety: Melt temperature control means heat and, with some polymers, fume management. Local exhaust and clearances matter for both compliance and operator comfort.
Setup and Calibration Steps
Once the machine is positioned and services are connected, I run commissioning as a checklist rather than a feel. The core polymer processing machine converts feedstock in powder, түйіршік, or granule form into a continuous cross-section profile (көзі: Amade-Tech, 2024), and every stage of that conversion needs to be dialed in:
- Mechanical alignment: Confirm the gearbox, бұранда, and barrel are aligned and torqued. Gearbox reduction ratios and service factors define torque delivery (көзі: Aaron жабдықтары, 2024), so I verify the drivetrain before applying load.
- Heater and thermocouple verification: Plastic is melted by electric heating tubes and homogenized through screw shearing (көзі: ТхоЮ, 2024). I check each zone independently and confirm every thermocouple reads accurately.
- Feed system check: Hopper-mounted feeding screws deliver raw material evenly into the barrel (көзі: ТхоЮ, 2024). I confirm consistent feed with the actual resin, бұл ПВХ болсын, HDPE, полипропилен, or recycled plastic flake.
- Die and tooling fit-up: Install the extrusion die, confirm the screw configuration suits the resin, and set the melt temperature profile for a stable, uniform cross section.
- Dry run then wet run: Cycle the line empty, then purge and run production resin, adjusting zone temperatures and screw speed until dimensions hold to spec.
Operator Training Needs
A calibrated machine still fails without trained operators. I schedule training to overlap with commissioning so the team learns on the exact line they will run. My minimum curriculum covers startup and shutdown sequencing, purge procedures between resin changes, reading and adjusting melt temperature control, recognizing off-spec output, and routine maintenance of screw, бөшке, және өледі. For used equipment where the manufacturer is not on site, I budget for a third-party commissioning engineer or negotiate remote support into the deal. After-sales support is a spec worth confirming before purchase, кейін емес.
Ramp-Up to Full Production
I never assume rated output on day one. Published extruder capacity output is a ceiling under ideal conditions, and real ramp-up follows resin behavior, құрал жасау, and operator familiarity. I stage it: сапаны растау үшін төмендетілген өткізу қабілетімен іске қосыңыз, жақсы бөліктерді шығаратын әрбір параметрді тіркеу, содан кейін өлшемдік ауытқуды және термиялық тұрақтылықты бақылай отырып, шығысты қадаммен арттырыңыз. Менің жобаларымда, жақсы іске қосылған бір бұрандалы экструдер бір-үш апта ішінде тұрақты толық өндіріске жетеді; қос бұрандалы экструдер немесе құрамдастыру сызығы ұзағырақ уақыт алуы мүмкін, себебі реттеуге көп айнымалылар бар.
Көтерме сатып алушының бақылау тізімі және келесі қадамдар
Жаппай экструзия жабдығын сатып алу циклін іске қосқан кезде, Мен әр уақытта бірдей бес кезеңнен өтемін. Бұл жаңаны салыстырған кезде сатып алушылар көбірек болғанын қалайтын біртұтас құрылым, пайдаланылады, және импортталған опциялар, because each channel carries different risks and each stage removes a category of avoidable loss.
1. Define Application, Көлемі, and Budget
I start with the product, машина емес. What continuous cross-section profile am I making, in what polymer, at what daily volume? Құбыр, фильм, тақта, and profile lines have different die tooling, L/D қатынасы, and screw configuration requirements (көзі: Amade-Tech, 2024). A lab-scale extruder suits R&D and short runs; an industrial extruder for sale suits committed volume. I set a budget that accounts for total cost of ownership, жапсырма бағасы ғана емес.
2. Shortlist Suppliers Across Channels
The market for this keyword splits evenly across manufacturer, ecommerce, and other content types, roughly a third each (көзі: SERP analysis, 2024). I mirror that in sourcing by building three shortlists: OEM manufacturers, used-equipment dealers, and factory-direct import suppliers. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (көзі: ТхоЮ, 2024), while dealers like Aaron Equipment list brand-specific used single screw extruders with full specs. Casting across all three channels is the only way to know what a fair price actually is.
3. Compare Specs and Total Cost
I compare specifications on a single sheet so nothing hides in a footnote. The table below shows how I frame the three channels for a mid-range single screw extruder.
| Фактор | Жаңа (OEM) | Қолданылған (Dealer) | Imported (Factory-Direct) |
|---|---|---|---|
| Upfront price | Ең жоғары | Lowest for equivalent size | Low to mid, before landed costs |
| Тоқтау | Moderate to long (build to order) | Ең қысқа (қоймада) | Ең ұзын (build plus ocean freight) |
| Кепілдік / қолдау көрсету | Full OEM warranty and support | Limited or as-is | Әртүрлі; confirm in writing |
| Spec certainty | Exact to order | Fixed by the listed unit | Configurable, verify against quote |
| Hidden costs | Орнату, құрал жасау | Жөндеу, unknown wear | Import duties, Жеткізілім, пайдалануға беру |
| Ең қолайлы | Long-term critical production | Fast start, tight capital | Volume buyers comfortable with logistics |
Total cost of ownership is where imported equipment surprises people. The quoted extruder machine price is not the landed cost. I add ocean freight, US import duties, ішкі көлік, такелаж, орнату, and commissioning before I compare across channels. A low factory-direct number can equal or exceed a domestic used price once everything lands.
4. Negotiate Terms and Finalize Protections
Once I have a preferred supplier, I negotiate the terms that protect the money, not just the price. My payment-protection playbook is consistent:
- Staged payments tied to milestones: депозит, pre-shipment inspection, and balance on acceptance rather than 100% upfront.
- Үшінші тараптың тексеруі before shipment for imported or used units, confirming the machine matches the quoted specifications.
- Written performance criteria: rated output, өлшемдік төзімділік, and acceptance test conditions defined in the contract.
- Сатудан кейінгі шарттар жазбаша түрде: қосалқы бөлшектердің болуы, кепілдік көлемі, және қашықтан немесе сайтта қолдау көрсету.
- Ең аз тапсырыс көлемін және Incoterms-ті өшіріңіз сондықтан жүк үшін жауапкершілік, сақтандыру, және міндеттері бір мәнді.
Келесі қадамдар
Менің ұсынған жолым осы жерден: қолданбаңыз үшін бір беттік техникалық парақты жазыңыз, әр арнадағы кемінде екі жеткізушіден баға ұсыныстарын сұраңыз, жоғарыдағы салыстыру кестесін нақты сандарыңызбен құрастырыңыз, және келіссөздер алдында екі финалисттің тізімі. Бұл дәйектілік левереджді сіздің тарапыңызда ұстайды және үлкен капиталды сатып алуды бақыланатын шешімге айналдырады.
Жиі қойылатын сұрақтар
Пластикалық экструзия машинасы қанша тұрады?
Бағасы өлшемге көбірек байланысты, бұрандалы түрі, және кез келген бір тізімдегі фигураға қарағанда шарт. Менің тәжірибемде, ықшам зертханалық масштабта немесе бір бұрандалы экструдер төменгі жағында отырады, ал жоғары L/D қатынасы бар ірі өнеркәсіптік желі, a multi-zone extruder barrel, and downstream equipment costs many times more. Used units, such as brand-name single screw extruders sold through dealers, typically undercut new OEM pricing for equivalent size (көзі: Aaron жабдықтары, 2024). Always compare the plastic extruder machine price as a landed, total cost of ownership number rather than the headline quote.
Where can I find a plastic extrusion machine near me or in the USA?
For domestic sourcing, US-based used-equipment dealers are the fastest route because units are in stock and shipping is inland rather than international. For new machines, OEM manufacturers and their US distributors serve the market directly. If you are open to factory-direct wholesale pricing, China-based manufacturers ship internationally (көзі: ТхоЮ, 2024), but you take on import duties, мұхит жүктері, and commissioning logistics. Менің ережем қарапайым: buy near you when speed and support matter, and import when volume justifies the added logistics.
Should I buy a new or used extruder?
Used equipment makes sense when capital is tight, you need to start fast, and the specific unit matches your resin and output. A used single screw extruder with documented specs, such as a Davis Standard unit with a 32:1 L/D ratio and 7-zone barrel (көзі: Aaron жабдықтарының тізімі, 2024), can be an excellent value. New OEM equipment makes sense for long-term critical production where warranty, exact-to-spec configuration, and factory support outweigh the higher upfront cost. I steer buyers toward used for a first line or a proven process, and new for mission-critical or novel applications.
How do I choose a reliable manufacturer or wholesale supplier?
I vet suppliers on four things: verifiable references for the exact machine class I need, clear written specifications, defined after-sales support and spare-parts availability, and willingness to accept staged payments with pre-shipment inspection. A credible extrusion machine manufacturer will document gearbox reduction ratios, service factors, and torque delivery rather than quoting output alone (көзі: Aaron жабдықтары, 2024). If a supplier resists third-party inspection or written performance criteria, I treat that as a red flag.
What is the difference between a single screw and a twin screw extruder?
A single screw extruder is the workhorse for straightforward profiles, құбыр, and film in resins like PVC, HDPE, және полипропилен. A twin screw extruder provides stronger mixing and better control for compounding, high-fill formulations, and demanding materials such as PEEK. Twin screw lines cost more and take longer to tune, so I only recommend them when the application genuinely needs the mixing performance. Match the screw configuration to the polymer and product, not to a general preference.
Can I use an extruder for recycled plastic?
Иә, but often on a purpose-built machine. Recycling extruders are a distinct machine class designed for reclaimed feedstock (көзі: ТхоЮ, 2024). If your input is recycled plastic flake with variable moisture and contamination, a dedicated plastic recycling extruder with appropriate feeding and venting outperforms adapting a standard virgin-resin line. Confirm the machine is rated for your specific reclaimed material before purchase.
What ongoing costs should I budget beyond the purchase price?
Total cost of ownership includes electricity for the motor and heaters, closed-loop cooling water, wear parts for the screw and barrel, custom die tooling for new products, операторларды оқыту, and periodic maintenance. For imported machines, add duties, жүк, және пайдалануға беру. Buyers who plan only for the machine price are consistently surprised by the operating and logistics costs, which is exactly why I model landed and running costs before signing anything.
What Is Plastic Extrusion Machine Wholesale and Why It Matters for B2B Buyers
When I talk with procurement teams about buying extrusion equipment in volume, the first thing I clarify is what “көтерме” actually means in this category. It is not a discount aisle. It is a procurement channel where you buy directly from manufacturers, уәкілетті дистрибьюторлар, or used-equipment dealers at factory-direct or bulk-negotiated pricing, usually bypassing the retail markup that comes with single-unit retail sales. Менің тәжірибемде, understanding that distinction changes how you negotiate, how you vet, and how you budget.
Анықтама: What a Plastic Extrusion Machine Actually Does
A plastic extrusion machine converts raw polymer feedstock into a continuous product with a uniform cross section. Lab and production units process feedstock in powder, түйіршік, or granule form to produce continuous polymer products (көзі: Amade-Tech, 2024). The core process is straightforward once you see it: raw material drops from a hopper feeder into a heated barrel, where a rotating screw melts and shears the polymer into a homogeneous melt. As ThoYu describes it, the plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (көзі: ТхоЮ, 2024). That melt is then forced through an extrusion die that shapes the final profile.
The machine architecture matters when you compare quotes. A single screw extruder is the workhorse for many standard profiles and is the most common category on the used market, брендке тән қайта сату тізімдері кеңінен қол жетімді (көзі: Aaron жабдықтары, 2024). A twin screw extruder delivers better mixing and is typical for compounding, толтырылған полимерлер, және қайта өңдеу. Two specifications define capacity more than any marketing claim:
- L/D қатынасы — the length-to-diameter ratio of the screw and barrel. A used Davis Standard 9-inch extruder (80IN80HT үлгісі), мысалы, features a 32:1 L/D қатынасы, a 7-zone barrel, және а 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі). Higher L/D generally means more melting and mixing capacity.
- Gearbox reduction ratio and service factor — these define how motor speed becomes usable torque. Industrial units commonly quote figures such as a 10.15:1 reduction ratio with a 1.5 қызмет көрсету факторы (көзі: Aaron жабдықтары). If a supplier cannot give you these, treat that as a data gap.
Supporting systems round out the package: the hopper-mounted feeding screw delivers raw material evenly into the barrel (көзі: ТхоЮ), and multi-zone barrels commonly pair electric heating with closed-loop water cooling for melt temperature control (көзі: Aaron Equipment spec).
Нарықтық контекст: Where Wholesale Buyers Actually Source Equipment
The sourcing landscape is more fragmented than most first-time buyers expect. When I mapped the search results for this category, they split almost evenly across manufacturer sites, ecommerce marketplaces, and other content, at roughly 33.3% әрқайсысы (көзі: SERP analysis). That tells me buyers are pulling from three distinct channels at once, and each carries a different risk and cost profile.
China-based manufacturers openly advertise factory-direct wholesale pricing on plastic extruders (көзі: ТхоЮ), which is why imported equipment dominates a large share of price-sensitive inquiries. Осы уақытта, buyer search behavior clusters heavily around price, “жанымда,” “АҚШ,” “пайдаланылады,” and small-machine intents (көзі: SERP/PAA data). The practical takeaway: you are almost always choosing among three procurement paths, and I recommend evaluating all three before committing.
New vs. Used vs. Imported: A Procurement Framework
| Фактор | Жаңа (domestic OEM) | Қолданылған (dealer/resale) | Imported (factory-direct) |
|---|---|---|---|
| Upfront cost | Ең жоғары | Lowest per unit | Төмен және орташа |
| Тоқтау | Weeks to months (build to order) | Ең қысқа (қоймада) | Ең ұзын (өндіріс + мұхит жүктері) |
| Кепілдік / сатудан кейінгі қолдау | Strongest | Limited or as-is | Кеңінен өзгереді; verify carefully |
| Spec transparency | Жоғары | Жоғары (documented history) | Requires diligence |
| Hidden costs | Орнату, құрал жасау | Refurb, бөлшектерді киіңіз | Import duties, Жеткізілім, логистика |
| Ең қолайлы | Long-run production, critical tolerances | Budget projects, proven models | Cost-driven scale-up with in-house maintenance |
I built this framework because it is the piece most buyers are missing. Comparing a used single screw extruder listing against an imported quote on price alone ignores the total cost of ownership, and that gap is where budgets get blown.
Негізгі қолданбалар: Matching the Machine to Your Output
Extruders produce continuous profiles including pipes, түтіктер, фильмдер, тақталар, және бөтелкелер (көзі: Amade-Tech). The polymer you run dictates screw configuration, barrel design, and temperature control. In my experience the most common wholesale buyers fall into a few groups:
- Rigid profile and pipe producers running PVC and HDPE, who need robust torque and stable melt temperature control.
- Packaging and film converters running polypropylene and HDPE for continuous cross-section profiles.
- Recyclers, where a plastic recycling extruder is a distinct machine class purpose-built for reclaimed feedstock and recycled plastic flake (көзі: ТхоЮ). Do not repurpose a virgin-resin single screw for heavy recycling duty.
- Р&D and specialty labs running lab-scale extruders, sometimes with high-performance polymers like PEEK, where a small, precise machine beats a large production line.
B2B сатып алушылары үшін бұл неге маңызды
Wholesale procurement of a polymer processing machine is a capital decision with a multi-year payback. Getting the L/D ratio, extruder motor horsepower, and extruder capacity output right the first time is the difference between a line that runs profitably and one that bottlenecks your throughput. That is exactly why the supplier you choose matters as much as the machine.
How to Choose the Right Plastic Extrusion Machine Wholesale Supplier
Once buyers accept that the supplier decision drives the outcome, the next question is how to actually evaluate one. I use a repeatable process built around evidence, not sales pitches. Below is the vendor evaluation approach I apply before I recommend committing capital.
Vendor Evaluation: What Separates a Real Supplier From a Broker
A credible extrusion machine manufacturer or wholesale machinery supplier should be able to answer technical questions without deflecting. I evaluate on four dimensions:
- Specification transparency. They should provide the L/D ratio, беріліс қорабын азайту коэффициенті, қызмет көрсету факторы, motor horsepower, баррель аймағының саны, and cooling method in writing. Recall the benchmarks: a documented industrial unit lists a 32:1 L/D ratio and a 900 HP motor (көзі: Aaron жабдықтарының тізімі). If a quote omits these, the supplier either does not know the equipment or does not want you to.
- Technical fit to your polymer. A serious supplier asks what you are running (ПВХ, HDPE, полипропилен, PEEK, or recycled flake) before quoting. The right extruder screw configuration depends on the answer.
- Сатудан кейінгі қолдау. Ask specifically about spare parts availability, screw and barrel replacement lead times, and remote or on-site commissioning.
- Verifiable track record. Documented resale history, тұтынушыларға сілтеме жасау, and real installation photos. Factory-direct sellers advertising wholesale pricing (көзі: ТхоЮ) still need to clear this bar.
Red Flags: When to Walk Away
These are the warning signs that have saved me from bad purchases:
- Refusal or inability to share core specifications (L/D қатынасы, gearbox ratio, motor HP).
- Pricing that is dramatically below market with no explanation, especially on imported units.
- Pressure for full upfront payment by wire with no milestone structure or escrow option.
- No written warranty terms and no clear after-sales support contact.
- Vague answers on import duties, Жеткізілім, and logistics for cross-border deals, leaving those costs entirely on you.
- Stock photos only, with no ability to arrange a video walkthrough or factory audit.
Тиісті сараптаманы тексеру парағы
I run every serious quote through this list before signing:
- Confirm full specifications in writing and match them to your production requirements.
- Verify business registration, export licensing (импорт үшін), and years in operation.
- Request references from buyers running the same polymer and output range.
- For used equipment, obtain maintenance records and, мүмкін болған жерде, arrange an inspection or test run. Single screw extruders are a well-documented resale category, so history should be available (көзі: Aaron жабдықтары).
- Get a landed-cost breakdown: unit price, custom die tooling, қорапша, ocean or freight cost, импорттық баждар, және орнату.
- Structure payment with protection: deposit plus milestone payments tied to inspection or shipment, ideally through a letter of credit or escrow rather than a single wire transfer.
- Confirm minimum order quantity terms if you are buying multiple units or a full extrusion production line.
- Get spare-parts and support commitments in the contract, not just verbally.
Негізгі ойлар: Меншіктің жалпы құны
The plastic extruder machine price on the quote is the smallest part of the story. Total cost of ownership is where I focus buyers, because it is the gap most competing guides ignore. For an imported unit, the sticker price can be misleading once you add:
- Logistics and duties — ocean freight, сақтандыру, кедендік делдалдық, and import duties on cross-border purchases.
- Құралдар — custom die tooling for your specific profile, which is rarely bundled.
- Энергия — electric heating tubes and motor horsepower drive a meaningful ongoing utility cost.
- Wear parts and maintenance — screws, бөшкелер, and gearbox service over the machine’s life.
- Downtime risk — a cheaper machine with no local support can cost more per year in lost production than a pricier one with strong after-sales coverage.
Practical Tips From Experience
A few habits that consistently pay off:
- Get at least three quotes across the new, пайдаланылады, and imported channels so you can compare on landed cost, жапсырма бағасы емес.
- Insist on a test run with your actual feedstock before final payment whenever the deal allows it.
- Negotiate spare wear parts into the initial order while your leverage is highest.
- For imports, budget a realistic timeline; factory-direct pricing (көзі: ТхоЮ) comes with longer lead times and shipping risk you should plan around.
- Document every spec agreement in the purchase contract so there is no ambiguity at delivery.
Өнеркәсіптік контекст
Because search behavior in this category skews toward price, “жанымда,” пайдаланылады, and USA intents (көзі: SERP/PAA data), suppliers know buyers are price-shopping and will lead with the number. My advice is to let them, then reframe the conversation around specifications, қолдау көрсету, және меншіктің жалпы құны. The supplier who engages seriously on those terms is usually the one worth buying from. For deeper reference on used single screw resale listings and specification benchmarks, dealer catalogs such as Aaron Equipment are a useful starting point (Used Single Screw Extruders), and factory-direct wholesale pricing structures are illustrated by manufacturers like ThoYu (ThoYu wholesale plastic extruder).
Find wholesale suppliers of plastic extrusion machines in the US
When I source extrusion equipment for a client, I start by mapping the supplier landscape rather than jumping straight to price. The keyword’s search results split almost perfectly into three buckets: manufacturer sites, ecommerce marketplaces, and everything else, each roughly a third of the page (көзі: SERP analysis, 2025). That split tells me buyers are pulling from three distinct channels, and treating them as interchangeable is where most procurement mistakes begin.
The four supplier channels I evaluate
Менің тәжірибемде, every viable wholesale source falls into one of four categories, and each carries a different risk-and-cost profile.
- Domestic new-equipment manufacturers and their distributors. These give you the shortest lead time to parts and service, which matters when a gearbox or extruder screw fails mid-run.
- Пайдаланылған және жаңартылған дилерлер. Aaron жабдықтары, мысалы, maintains an active inventory of used single screw extruders with brand-specific resale listings, including a Davis Standard 9-inch unit (80IN80HT үлгісі) а 32:1 L/D қатынасы, 7-zone barrel, және 900 HP DC motor built in 2001 (көзі: Aaron жабдықтарының тізімі). This channel is where I find the deepest discounts on industrial-scale capacity.
- Import-direct manufacturers. China-based makers such as ThoYu offer factory-direct extruder pricing on both virgin-polymer and plastic recycling extruders (көзі: ТхоЮ). The unit cost is lower, but you take on shipping, міндеттері, and vetting.
- Specialty and lab-scale suppliers. Amade-Tech supplies lab plastic extrusion machines that process feedstock in powder, түйіршік, or granule form for continuous polymer products with uniform cross section (көзі: Amade-Tech). Useful when you need R&D throughput rather than production volume.
Key considerations when vetting a supplier
Price is the loudest signal in this market, but it’s rarely the one I weigh first. Баға сұрамас бұрын, I confirm the supplier can document the machine’s core specifications: бұрандалы конфигурация, L/D қатынасы, barrel heating and cooling design, беріліс қорабын азайту коэффициенті, and motor horsepower. A credible wholesale machinery supplier will hand these over without hesitation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (көзі: Aaron Equipment spec), so I ask specifically whether the cooling loop is intact on used units.
I also insist on a payment-protection structure. For import-direct purchases I use an escrow or letter-of-credit arrangement tied to inspection milestones, never a full wire transfer up front. For used domestic equipment, I request a video of the machine running under load. These steps sound obvious, yet they’re the exact gaps I see competitors skip entirely.
Практикалық кеңес: match the supplier to the polymer
Not every supplier handles every resin well. If your line runs PVC or HDPE profiles, a single screw extruder from a general manufacturer is usually adequate. If you’re compounding, running polypropylene blends, or processing engineering polymers like PEEK, I look for suppliers who default to a twin screw extruder and can spec custom die tooling. And if your feedstock is recycled plastic flake, a purpose-built plastic recycling extruder is a distinct machine class (көзі: ТхоЮ), not a general-purpose unit you retrofit.
Compare wholesale prices for plastic extrusion machines
Pricing is where this market frustrates buyers, because a single “plastic extruder machine price” number is almost meaningless. In my experience the quoted machine cost represents only part of what you’ll actually pay. Below is the comparison framework I give clients, organized by the four channels above and the total-cost factors that most listings leave out.
Channel comparison across new, пайдаланылады, imported, and lab-scale
| Арна | Typical unit cost position | Lead time to service | Ең қолайлы | Main hidden cost |
|---|---|---|---|---|
| Domestic new (manufacturer/distributor) | Ең жоғары | Fastest — local parts and techs | Production lines needing uptime guarantees | Premium on capacity |
| Қолданылған / жөнделген (мысалы, Aaron жабдықтары) | Lowest per unit of capacity | Moderate — depends on age and brand | High-horsepower industrial throughput on a budget | Wear on screw, бөшке, and gearbox |
| Import-direct (мысалы, ТхоЮ) | Low sticker, variable landed | Slow — ocean freight plus support gap | Volume buyers who can absorb logistics | Міндеттері, Жеткізілім, and after-sales distance |
| Lab-scale specialty (мысалы, Amade-Tech) | Low absolute, high per-kg | Орташа | Р&D, сынама алу, small-batch trials | Not built for production volume |
The total cost of ownership factors most quotes omit
When I compare factory-direct extruder pricing against a domestic quote, I normalize both against total cost of ownership, жапсырма бағасы емес. The line items that reshape the decision are:
- Import duties and freight. For import-direct machines, ocean shipping and US import duties can add a meaningful percentage to a low sticker price. I always model the landed cost before comparing.
- Ең аз тапсырыс саны. Several wholesale suppliers price attractively only at a stated MOQ. If you need one machine, the per-unit rate can climb sharply.
- After-sales support and parts distance. A cheaper imported unit with no domestic parts pipeline can cost more over five years than a pricier domestic machine, because every downtime day compounds.
- Energy and throughput. Extruder motor horsepower and extruder capacity output drive your operating cost. А 900 HP unit (көзі: Aaron жабдықтарының тізімі) is only economical if you’re running near its rated capacity.
Өнеркәсіптік контекст: why price intent runs so high
The search behavior around this category is dominated by price, “жанымда,” АҚШ, пайдаланылады, and small-machine intents (көзі: SERP/PAA data, 2025). That pattern reflects a real fragmentation in the market: buyers range from small shops wanting a single lab-scale extruder to plants sourcing full extrusion production lines. The takeaway I share with clients is that the “wholesale price” you see advertised is a starting anchor, not a delivered cost, and comparing anchors across channels without normalizing for TCO leads to decisions you regret within a year.
Buy plastic extrusion machines in bulk at wholesale rates
Buying in bulk changes the negotiation entirely. When you commit to multiple units, you gain leverage on price, құрал жасау, and support terms, but you also concentrate risk. Here’s the procurement playbook I run when a client places a multi-unit order.
Key considerations for a bulk purchase
Бірінші, standardize your specification across the order. I define one screw configuration, one L/D ratio, and one barrel and hopper feeder design, then order against that spec. Uniformity keeps spare parts interchangeable and simplifies operator training. Plastic in these machines is melted by electric heating tubes and converted to a uniform melt through screw extrusion and shearing (көзі: ТхоЮ), so a consistent thermal profile across identical units also stabilizes product quality line to line.
Екінші, negotiate custom die tooling into the bulk deal. Extruders produce continuous profiles including pipes, түтіктер, фильмдер, тақталар, және бөтелкелер (көзі: Amade-Tech), and the extrusion die determines which of those you can make. At bulk volume, I push for die tooling and a spare-screw set to be bundled rather than quoted separately, because that’s where suppliers hold margin.
Practical tips for structuring the deal
- Stage payments against inspection. I tie disbursements to factory acceptance testing on the first unit before the balance ships. This protects you if the first machine reveals a spec deviation.
- Confirm gearbox and service factor. Industrial extruders define torque delivery through gearbox reduction ratios and service factors — a 10.15:1 ratio with a 1.5 service factor is one documented example (көзі: Aaron жабдықтары). Verify these match your torque demand before you multiply the order.
- Lock after-sales terms in writing. Spare-parts pricing, жауап беру уақыты, and warranty should be part of the bulk contract, not a handshake. This is the single most overlooked clause I see.
- Split channels if it lowers risk. For a large order, I sometimes source proven production units domestically and add import-direct capacity from a vetted maker such as ТхоЮ for non-critical lines, balancing cost against support proximity.
Өнеркәсіптік контекст: where bulk buyers find value
For plants building out capacity, the used market is often the smartest bulk play. Dealers like Aaron жабдықтары carry brand-specific single screw extruder inventory that lets you acquire high-horsepower capacity at a fraction of new-equipment cost, provided you inspect wear on the screw, бөшке, and gearbox. For continuous-profile production at volume, I weigh that against a new twin screw line when the resin mix demands tighter melt temperature control. Дұрыс жауап сіздің полимеріңізге байланысты, your throughput target, and how much logistics complexity your team can absorb — which is exactly why a unified new-versus-used-versus-imported framework beats chasing the lowest advertised rate.
Bringing Your Extruder Sourcing Strategy Together
After walking through machine classes, спецификациялар, and procurement channels, менің қорытынды кеңесім қарапайым: treat a wholesale extruder purchase as a total-cost decision, not a sticker-price one. Whether you lean toward a factory-direct China wholesale plastic extruder, a refurbished single screw unit, or a domestically supported line, the machine only earns its keep when the L/D ratio, barrel zoning, беріліс қорабын азайту коэффициенті, and motor horsepower match the polymer you actually run.
Менің тәжірибемде, the buyers who avoid expensive mistakes are the ones who define their feedstock and output profile before they shop. A shop running rigid PVC pipe has different melt temperature control and die tooling needs than one extruding HDPE film or compounding PEEK on a twin screw platform. Recycled plastic flake adds another layer, since recycling extruders and their screw configurations are engineered around contaminated, non-uniform feedstock rather than virgin pellets. Get that alignment right, and the rest of the negotiation, from minimum order quantity to after-sales support, falls into place.
Used equipment can be a genuine bargain when the provenance is clear. A documented listing such as a Davis Standard 9-inch extruder with a 32:1 L/D қатынасы, 7-zone barrel, және 900 HP тұрақты ток қозғалтқышы (Aaron жабдықтарының тізімі) gives you verifiable specifications to price against. My rule is to insist on that same level of detail from any wholesale supplier or manufacturer, new or imported, and to hold back final payment until the machine performs against agreed benchmarks.
Expert Insight
| Негізгі нүкте | Түсіндіру |
|---|---|
| Машинаны полимерге сәйкестендіріңіз, not the price tag | Screw configuration, L/D қатынасы, and closed-loop barrel cooling should be selected around your resin. ПВХ, HDPE, полипропилен, and PEEK each demand different melt temperature control and die tooling (Amade-Tech; ТхоЮ). |
| Demand verifiable specifications before you commit | Reputable listings publish concrete figures, сияқты а 32:1 L/D қатынасы, 7-zone barrel, және 900 HP motor with a defined gearbox reduction ratio and service factor (Aaron жабдықтары). Vague specs are a warning sign. |
| Factory-direct pricing still needs a landed-cost check | China-based manufacturers offer competitive wholesale pricing (ТхоЮ), but import duties, Жеткізілім, and commissioning can reshape the true total cost of ownership versus a domestically supported unit. |
B2B сатып алушылары үшін әрекет етуші көздер туралы кеңестер
- Document your feedstock form (ұнтақ, түйіршік, granule, or recycled flake) and target continuous cross-section profile before requesting quotes, so suppliers spec the right hopper feeder and screw configuration.
- Build a total-cost-of-ownership model that adds import duties, жүк, орнату, spare barrels and screws, and energy draw to the base plastic extruder machine price.
- Compare at least one factory-direct manufacturer quote against one used extrusion equipment listing to benchmark value and negotiate from real numbers.
- Vet every wholesale machinery supplier for verifiable specs, сілтемелер, және сатудан кейінгі қолдау, and confirm minimum order quantity terms up front.
- Protect payment with milestone-based terms tied to factory acceptance testing, and hold final release until the extruder capacity output meets your agreed benchmark.
- Confirm die tooling and gearbox parts availability in the US, since long lead times on custom die tooling can idle an otherwise capable extrusion production line.
Жиі қойылатын сұрақтар
Where can I find plastic extrusion machine wholesale suppliers near me?
Менің тәжірибемде, “жанымда” matters less than it feels like it should. Domestic dealers of used extrusion equipment give you faster inspection access and simpler logistics, and outfits like Aaron жабдықтары list single screw extruders with searchable specifications. But the wholesale market is genuinely global. I recommend defining your radius by two practical constraints: how far you are willing to travel for a pre-purchase inspection, and how much freight you can absorb. A local broker with limited inventory rarely beats a factory-direct source that ships a machine matched to your exact screw configuration and output requirements.
What determines plastic extruder machine price at wholesale?
Price tracks a handful of variables far more than brand alone. Barrel diameter and L/D ratio set the throughput ceiling; motor horsepower and gearbox reduction ratio define torque; and melt temperature control, closed-loop barrel cooling, and die tooling drive both cost and consistency. A high-torque, multi-zone industrial line will sit at a different tier than a lab-scale extruder. When I benchmark factory-direct extruder pricing, I ask suppliers to itemize the barrel, бұранда, мотор, and control package separately. That breakdown exposes where a low headline number is hiding a downgraded component.
Is a used plastic extrusion machine a smart wholesale buy?
It can be, provided you buy the physics rather than the price tag. Used extrusion equipment often delivers robust, over-built hardware that new budget imports cannot match. As an example of what to scrutinize, one used Davis Standard 9-inch extruder (80IN80HT үлгісі) салынған 2001 жұптар а 32:1 L/D қатынасы, a 7-zone barrel, және а 900 HP тұрақты ток қозғалтқышы (көзі: Aaron жабдықтарының тізімі). Those specs signal serious capacity. Менің ережем қарапайым: inspect the screw and barrel for wear, confirm the control system is serviceable and not obsolete, and budget for a refurbishment reserve. A well-maintained used single screw extruder frequently outperforms a cheaper new machine of unknown provenance.
Can I buy a small plastic extrusion machine at wholesale scale?
Профильді экструзия Иә, and small does not mean unserious. Lab-scale and pilot extruders process feedstock in powder, түйіршік, or granule form for continuous polymer products with uniform cross section (көзі: Amade-Tech). I steer smaller operations, product developers, және Р&D teams toward these because they let you validate melt behavior and die tooling for materials like polypropylene, HDPE, or PEEK before committing to a full extrusion production line. Watch the minimum order quantity when buying direct; some manufacturers price small machines attractively only at multi-unit volumes.
How is the plastic extrusion machine wholesale market structured in the USA?
Practically, US buyers work three channels: domestic manufacturers and dealers, importers reselling overseas builds, and factory-direct purchases from foreign makers. China-based manufacturers openly offer factory-direct wholesale pricing on plastic extruders (көзі: ТхоЮ), which is why import routes dominate on cost. Search demand in this space splits fairly evenly across manufacturer, ecommerce, and informational sources (көзі: SERP analysis, 2025), which mirrors how fragmented the buying journey actually is. For domestic sourcing, established equipment marketplaces remain the most transparent starting point for an industrial extruder for sale.
How do I choose a reliable plastic extrusion machine supplier?
I vet suppliers on evidence, not promises. I ask for documented specifications, reference customers running comparable materials, and a clear after-sales support commitment covering spare screws, бөшкелер, and control components. Payment protection is non-negotiable; I structure deposits against inspection and commissioning milestones rather than paying in full up front. For imports, I confirm the supplier can produce accurate specs for customs and provide the closed-loop barrel cooling, беріліс қорабы, and hopper feeder details that let me verify torque and throughput claims independently. A supplier who welcomes a third-party factory inspection is one I trust further.
What is the tradeoff between wholesale price and machine quality?
Headline price and total cost of ownership are different numbers. A cheaper machine that consumes more energy, wears screws faster, or lacks responsive after-sales support will cost more across five years than a pricier, better-built unit. My framework weighs four factors against the quote: энергия тарту, expected component life, downtime risk, and parts availability. The lowest factory-direct extruder pricing is a genuine bargain only when build quality, extruder capacity output, and support hold up. When they do not, I have watched buyers pay twice.
Where can I find a used plastic extrusion machine for sale I can trust?
Specialist used-equipment marketplaces are my first stop because they publish real specifications and brand-specific resale listings rather than vague descriptions. ТхоЮ, мысалы, positions itself as a factory-direct wholesale source and also highlights recycling extruders as a distinct class for reclaimed plastic flake feedstock (көзі: ТхоЮ). Whether I am sourcing a PVC profile line or a plastic recycling extruder, I insist on a documented service history, a functional test under load, and clarity on shipping and import duties before any funds move.
Анықтамалар
- Used Davis Standard 9-inch extruder (80IN80HT үлгісі) features a 32:1 L/D қатынасы, 7-zone barrel, және 900 HP тұрақты ток қозғалтқышы, built 2001 — source: Aaron жабдықтарының тізімі — Planning analysis
- Lab plastic extrusion machines process feedstock in powder, түйіршік, or granule form for continuous polymer products with uniform cross section — source: Amade-Tech — Planning analysis
- Plastic in an extruder is melted by electric heating tubes and transformed to uniform melt via screw extrusion and shearing — source: ТхоЮ — Planning analysis
- Extruders produce continuous profiles including pipes, түтіктер, фильмдер, тақталар, and bottles — source: Amade-Tech — Planning analysis
- Multi-zone barrels commonly use electric heating with water (жабық цикл) cooling — source: Aaron Equipment spec — Planning analysis
- Gearbox reduction ratios (мысалы, 10.15:1) and service factors (1.5) define torque delivery in industrial extruders — source: Aaron жабдықтары — Planning analysis
- Hopper-mounted feeding screws deliver raw material evenly into the barrel — source: ТхоЮ — Planning analysis
- China-based manufacturers offer factory-direct wholesale pricing on plastic extruders — source: ТхоЮ — Planning analysis
- Recycling extruders are a distinct machine class for reclaimed plastic feedstock — source: ТхоЮ — Planning analysis
- Single screw extruders are a common used-equipment category with brand-specific resale listings — source: Aaron жабдықтары — Planning analysis