

重要なポイント
- 私の経験では, the fastest way to save money and headaches is knowing what you’re buying from: a real Plastic Pelletizer Factory engineers and tests its own machines, 商社が再販する一方で、. I always confirm which one I’m dealing with before requesting a quote.
- 材料に合わせたペレット化方法. Water strand and water ring pelletizing are the standard options for PP and PE streams, while underwater pelletizers suit higher-throughput compounding — the choice directly affects pellet size uniformity and output (プラスチックペレット化機, 2024, yjプラスチック押出機.com).
- 仕様に応じた価格設定, 固定ステッカーではありません. A PP/PE masterbatch twin screw machine lists around US $42,000, 米国近郊の PVC 円錐ツイン スクリュー ライン $25,000, and pet-food extruders run US $25,000–$80,000 per set (中国製.com, 2024). これらをアンカーとして使用します, then map cost to screw configuration and capacity.
- 供給が集中している. こんにちはサプライヤーリスト 1,569 二軸押出機製品は主に山東省から調達, 浙江省, と江蘇省 (HiSupplier.com, 2024), which makes regional clustering a practical starting point for a shortlist.
- The secondary market is large and worth screening. 以上 74,000 卸売中古二軸押出機製品がリストされています (中国製.com, 2024), 販売者が条件を文書化すれば、精査された中古の配合およびペレット化装置を使用することで資本コストを削減できます。 (アーリントンマシナリー, 2024).
- 私の審査では認定について交渉の余地はありません. CEを探します, ISO 9001, UL, GMP, 最終用途に応じて、SA8000 と SA8000 (中国製.com, 2024) — UL は米国の電気コンプライアンスにとって最も重要です.
- 機械がポリマーを処理できることを確認する. Quality plastic pellet making machines are built to extrude, いいね, そしてサイコロPP, HDPE, LDPE, およびLLDPEリサイクルの流れ (リサイクルプラント.com, 2024); PET recycling typically needs a purpose-built extruder, だから私はそれを別途確認します.
- 総所有コストの予算, 請求書だけではなく. 米国の購入者の場合、インコタームズを考慮に入れます, 関税, 貨物, 予備のダイプレートとカッター, and expected downtime — these often shift the real ROI more than the base price does.
プラスチックペレタイザー工場とは?
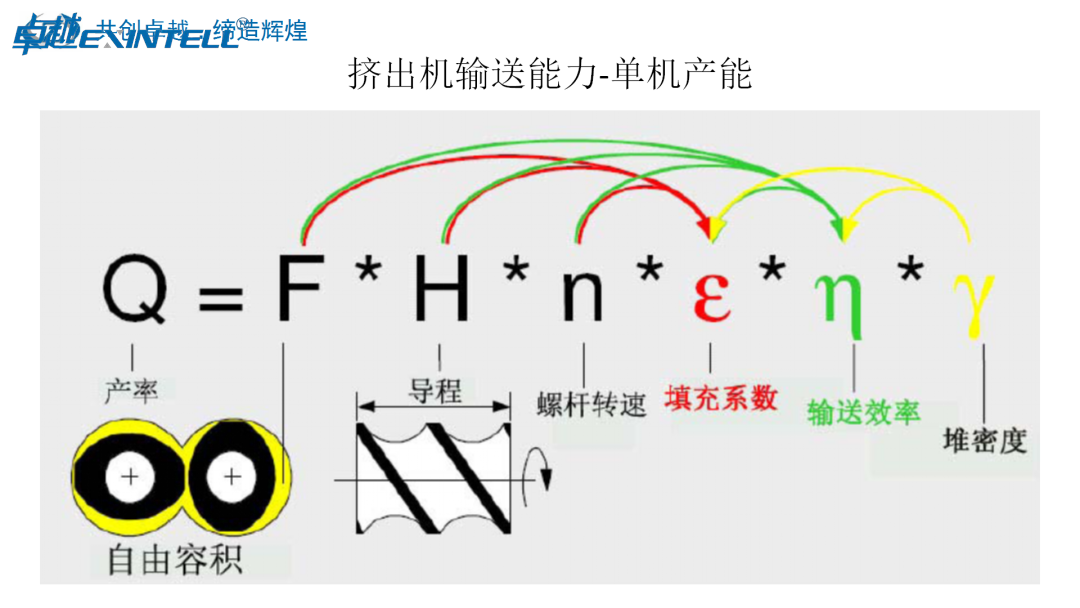
クライアントのためにサプライヤーを評価するとき, I start by clarifying what a plastic pelletizer factory actually is, because the term gets used loosely across marketplaces. 私の経験では, 本物の工場とは、設計を行う施設です。, エンジニア, 組み立てる, まったく触れたことのない機械を再販するのではなく、完全なペレット化システムを社内でテストします。. その区別が重要だ: 同じ統合されたアプローチが、その密接な関係を定義します, 押出工場, どれの “デザイン, エンジニア, 組み立てる, プラスチックの配合に使用される押出システムをテストします, 食べ物, 製薬, および化学産業” (二軸押出機工場とは – B2B ガイド, 2024). ペレタイザー工場は、特に溶融ポリマーまたは再生ポリマーを均一な顆粒に変えることにその規律を適用します。.
これらの工場がサービスを提供する産業
顧客ベースは、ほとんどの初めての購入者が想定しているよりも広い. 同じ工場がリサイクル作業を行っているのを定期的に見かけます, 複合住宅, マスターバッチプロデューサー, さらには食品や医薬品の加工業者も. リサイクルが大きなシェアを占める, プラスチックペレタイザー以来 “廃プラスチックを小さくします, ボトルの製造に使用される均一なペレット, コンテナ, パイプ, および自動車部品” (ケハオプラスチック機械, 2024). マスターバッチと複合バイヤー, 対照的に, 分散品質と色の一貫性をより重視する, 一方、食品や医薬品のバイヤーは衛生的な設計とGMPグレードの文書を優先します。.
工場が完成したラインを販売する理由, スタンドアロンユニットではない
購入者に強調したいことの 1 つは、: 最も評判の良い工場はフルペレット化ラインを見積もっています。, 裸のペレタイザーヘッドではない. プラスチック押出機と供給装置を組み合わせた作業ライン, 濾過, 冷却, そしてカッティングステージ, それらを同期するコントロールも追加. 特に中国の工場は “ツインを含む幅広い押出機およびペレタイザー製品ラインを提供, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー” (中国実験室二軸押出機工場カタログ, 2024). ラインをシステムとして販売すると、購入者の統合リスクが軽減されます。, なぜなら、押出機の性能に関係なく、カッターの不適合や冷却バスのサイズが小さすぎると、操作全体がボトルネックになるからです。.
工場が集中する場所とそこから購入する人
世界的な供給は地理的に集中している. こんにちはサプライヤーのみ “リスト 1,569 二軸押出機製品, 供給が山東省に集中している, 浙江省, と江蘇省” (HiSupplier.com, 2024), ポリマー配合装置貿易を支配する中国の 3 つの省. 流通市場も同様に活発です, と “以上 74,000 卸売中古二軸押出機製品” 利用可能 (中国製.com, 2024). 私が取引している米国のバイヤーは通常 2 つの陣営に分類されます: コスト競争力を求めるリサイクル業者, 特定の樹脂とスループット目標に合わせたカスタム押出ソリューションを必要とする配合業者.
プラスチックペレット化プロセスの仕組み
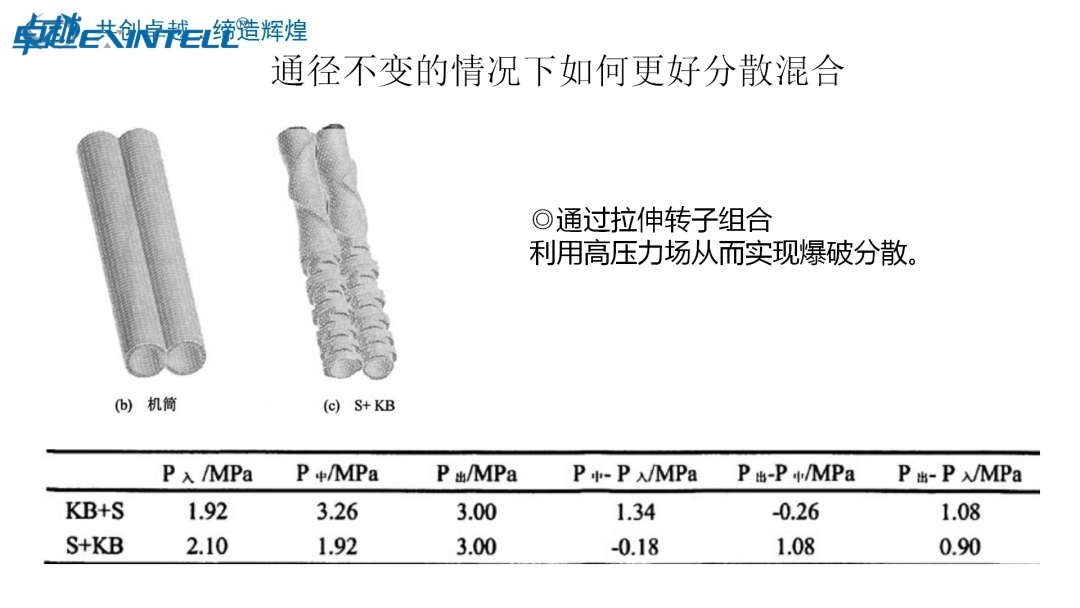
プロセスを理解すると、より明確な仕様を書くことができます, そこで私は購入者に段階的に説明します. すべてのペレット化ラインは同じ基本シーケンスに従います, バージン PP を実行するか、汚染された使用済み PE ストリームを実行するか.
餌やり, 溶融, 均質化
押出機モデル ラインはフィードスロートから始まります, どこの樹脂, 再研磨, または添加剤がバレルに入ります. 内部, 押出機のスクリュー構成が実際の機能を発揮します. 二軸押出機で, 噛み合うスクリューがせん断と混合を生成し、溶融物を均一化します。, これが、配合業者やマスターバッチ製造業者が分散が重要な作業にそれらを好む理由です。. 一軸スクリュー押出機はよりシンプルであり、多くの場合、簡単なリサイクルには十分です。. この溶融押出段階では、ポリマーが完全に溶融して温度が均一になってダイに到着するかどうかが決まります。, 下流での一貫したペレットの前提条件.
濾過と脱気
スクリュー押出機サプライヤー 溶融物がダイに到達する前に, 溶解していない粒子を捕捉するスクリーンチェンジャーを通過します。, 文字, そして異物混入, これはリサイクル原料を処理する際に非常に重要です. 2 段階の押出機で真空脱気を追加し、揮発性物質を取り除きます。, 水分, そして閉じ込められた空気. 私の経験では、このステップが、きれいな再生プラスチックペレットと、顧客側での品質検査に合格しない空隙だらけのペレットとの違いです。.
ダイ押出, 冷却, と切断
均質化された溶融物はダイプレートを通過します。, その後冷却し、ペレットにカットします. 具体的な仕組みはペレタイザーのタイプによって異なります, しかし目標は不変です: 高スループットでの均一な顆粒. リサイクル用に作られた機械は、 “押し出し, 冷却, ダイシングPP, HDPE, LDPE, およびLLDPEリサイクルの流れ” (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024). 冷却はウォーターバス内で行われるかどうか, 水の指輪, または水中切断室, ダイプレートとカッターの形状により、最終的なペレットの寸法が決まります.
ペレットの均一性が重要な理由
私は常にプロセスを、なぜ統一性にお金を払う価値があるのかに結び付けます。. 一貫したペレット サイズにより、お客様の下流の射出成形機またはブロー成形機への供給が安定します。, 溶融挙動を予測可能に保つ, スクラップを削減します. ペレットサイズの均一性が低い, 対照的に, フィードサージを引き起こす, 不均一な溶解, そして規格外の部品. そのため、ペレタイザーのタイプを製品に適合させることは見た目上の選択ではありません。, 買い手自身の利回りに直接影響します.
工場が生産するプラスチックペレタイザーの種類
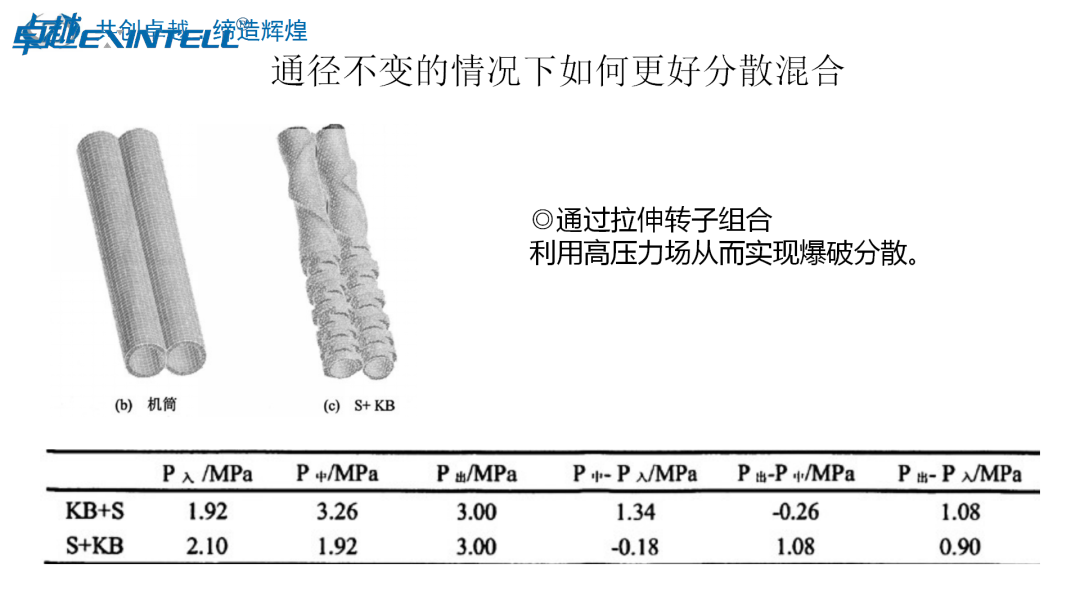
工場では通常 3 つのペレット化方法が提供されています。, そしてよく選ぶ “施設の生産量に大きな影響を与える, 製品の品質, 収益性” (アーリントンマシナリー, 2024). 以下に各タイプを分類し、それを購入者の製品と量にどのように適合させるかについて説明します。.
ストランド (ウォーターストランド) ペレタイザー
ストランドペレタイザー内, ダイは冷却水浴を通過する連続ストランドを押し出します。, 乾燥している, そして回転カッターで切り刻みます. 少量から中量のコンパウンダーやマスターバッチ生産者にはウォーターストランドシステムをお勧めします。, 最大のスループットの必要性よりも、頻繁な製品切り替えと簡単な検査の方が優先される場合. 水ストランドペレット化は 2 つのうちの 1 つです “プラスチック造粒に提供される標準的な方法” (プラスチックペレット化機, 2024), 操作が比較的簡単なのでメンテナンスも容易です.
水中 / ダイフェイスペレタイザー
高スループットの連続生産向け, 私は購入者に水中ペレタイザーを勧めます, ダイフェイスカッターと呼ばれることもあります. ここでは、カッターが水室内のダイ面に直接設置されています。, ポリマーが出た瞬間にペレットをスライス. この設計により、球面が得られます。, オペレーターの介入を最小限に抑えながら、均一性の高いペレットを大量に生成, それが、バージン樹脂工場や大規模なリサイクルラインを支配している理由です。. その代償として、資本コストが高くなり、カッターとダイのメンテナンスがより厳しくなります。.
ウォーターリングペレタイザー
ウォーターリングペレタイザーはその中間を占めます. ペレットはダイフェイスで切断され、冷却水の回転リングに投入されます。, フルダイフェイス装置よりも低価格と複雑さで、水中システムに近いスループットを実現します。. 工場が提供する他の標準的な造粒方法です (プラスチックペレット化機, 2024), そして、私はよく、ストランドラインが大きくなり過ぎたが、水中容量はまだ必要ではないリサイクル業者にそれを提案します。.
ペレタイザーのタイプを製品および量に適合させる方法
正しい選択は樹脂に帰着します, 音量, そして予算. 以下の表は、私が購入者に提供するガイダンスを反映しています。, 現在のマーケットプレイスのリストから抽出された参考価格を使用するため、仕様は静的な数値ではなく実際のコストにマッピングされます。.
|
ペレタイザータイプ |
最適なアプリケーション |
標準的なボリューム |
ペレットの均一性 |
参考価格 (市場) |
|---|---|---|---|---|
|
ストランド (水のストランド) |
配合, マスターバッチ, 頻繁な切り替え |
低から中程度 |
良い, 円筒形 |
PP/PE マスターバッチツインスクリューライン ~US $42,000/個 |
|
ウォーターリング |
中量リサイクル, PP/PEの再加工 |
中~高 |
とても良い, 球形に近い |
コニカルツインスクリュー (PVC) ~US $25,000/セット |
|
水中 / ダイフェイス |
バージン樹脂, 大規模継続リサイクル |
高い |
素晴らしい, 球状 |
食品/ハイスペックツインスクリュー ~US $25,000–$80,000/セット |
|
ペレタイザータイプ |
最適なアプリケーション |
標準的なボリューム |
ペレットの均一性 |
参考価格 (市場) |
|---|---|---|---|---|
|
ストランド (水のストランド) |
配合, マスターバッチ, 頻繁な切り替え |
低から中程度 |
良い, 円筒形 |
PP/PE マスターバッチツインスクリューライン ~US $42,000/個 |
|
ウォーターリング |
中量リサイクル, PP/PEの再加工 |
中~高 |
とても良い, 球形に近い |
コニカルツインスクリュー (PVC) ~US $25,000/セット |
|
水中 / ダイフェイス |
バージン樹脂, 大規模継続リサイクル |
高い |
素晴らしい, 球状 |
食品/ハイスペックツインスクリュー ~US $25,000–$80,000/セット |
上記の価格帯は、Made-in-China.com の卸売リストから引用されています。 (2024): 米国のPP/PEマスターバッチ二軸スクリューマシン $42,000 1個あたり, 米国近郊の PVC パイプ用円錐二軸押出機 $25,000 セットあたり, 米国間の食品生産用の二軸押出機 $25,000 そして $80,000 セットあたり. これらをアンカーとして扱います, 引用符ではありません, 最終価格はネジのサイズに応じて変化するため, スループット, オートメーション, および認証. 実際的なルールとして, 持続容積のピークに合わせてペレタイザーのサイズを調整します, 樹脂のフィットを確認します, HDPE 用にダイヤルインされた回線は、調整を行わないと LLDPE または PET では異なる動作をするため. 新品と中古を比較検討する購入者向け, 流通市場が活発であるということは、実行可能な選択肢が両端に存在することを意味します, ただし、私は常にスペアの入手可能性とサービス範囲を決定に考慮します。 (アーリントンマシナリー, 2024).
ストランドペレタイザー vs ウォーターリング vs 水中ペレタイザー
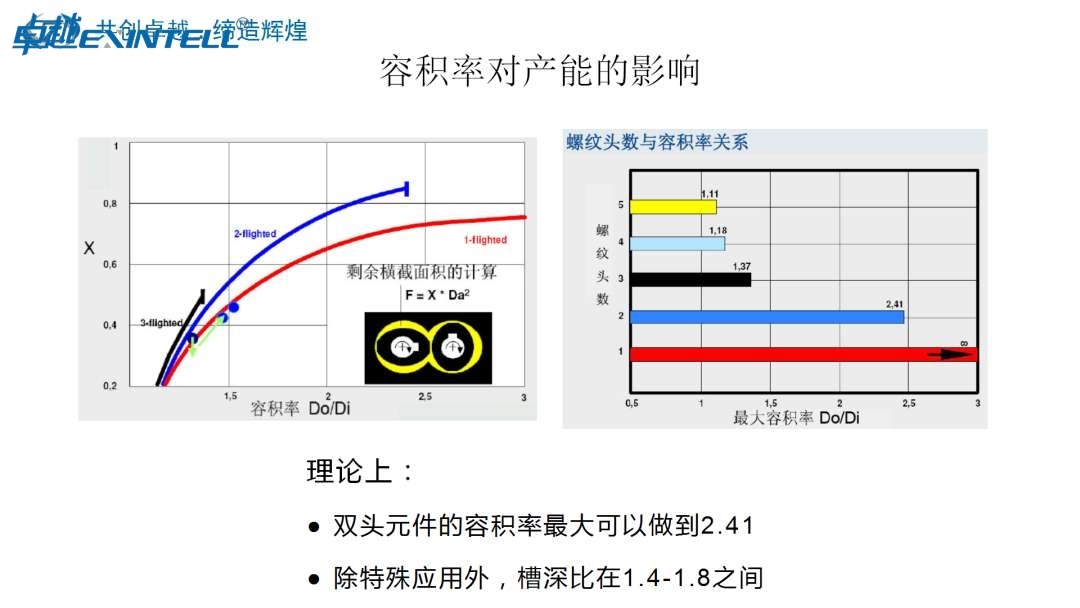
クライアントのプラスチックペレタイザー工場を評価するとき, 私が最初に前面に押し出す技術的な決定は、ラインがどの切断方法を使用するかです。. ストランド, 水リング, と水中ペレット化はそれぞれ同じ問題を解決します, 溶融ポリマーの流れを均一なペレットに変える, しかし、冷却と切断方法は根本的に異なります。. それらの違いはペレットの品質に影響します, 発塵, オペレータの作業負荷, そして最終的には総所有コスト. ウォーターリングとウォーターストランドペレット化はどちらも市場全体で提供されている標準的な造粒方法です, そして、私は水中オプションを、高スループットで形状に敏感な作業用のプレミアム層として扱います。 (プラスチックペレット化機, 2024).
3 つの方法による冷却と切断の違い
ストランドペレット化では、溶融物をダイを通して細いストランドにし、冷却水浴を通過します。, 乾燥する, カッターに入れて円筒形のペレットに切り分けます. 切断はポリマーが固化した後に起こります, そのため、切断の瞬間、材料は冷たくて安定しています。. このロジックに基づいて構築されたプラスチック ペレット製造機は、押出成形用に特別に設計されています。, 冷却, ダイシングPP, HDPE, LDPE, およびLLDPEリサイクルの流れ (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024).
水リングペレット化では、ダイ面で溶融物を切断し、回転する水のリングが切断されたばかりのペレットを洗い流し、一度の動作で冷却します。. 水中ペレット化がさらに進化: ダイプレートとカッターは温度制御された水室に完全に沈められます。, そのため、ポリマーは熱いうちに切断され、すぐに急冷されます。. 私の経験では, この水中カットにより、水中システムに特徴的な球形が与えられます。, 低応力ペレット, だからこそ、ダイプレートとカッターのアセンブリは工場監査の際に綿密な検査に値するのです。.
ペレットの形状, 一貫性, 発塵と発生
カットに沿った形状. ストランドシステムは円筒形のペレットを生成します, 水リングシステムはレンズまたは涙滴の形状を生成します, 水中システムでは、3 つのシステムの中で最も優れたペレット サイズの均一性を備えた球形に近いペレットが生成されます。. 工場現場で私が注目している実質的な差別化要因は粉塵です. 水中方式と水封方式により切削と冷却を同時に行うため, ドライカットプロセスよりもはるかに少ない微粉が発生します。. ストランドが脆かったり、カッターが鈍かったりすると、ストランドの切断でより多くの粉塵が発生する可能性があります。, ただし、よく維持されたストランドラインにより、この値は仕様の範囲内に収まります。.
メンテナンスとオペレーターのスキル要件
スキルの需要は複雑さに応じて拡大します. ストランドペレタイザーは最も操作が容易で、休憩後の糸巻き上げが最も簡単です。, だからこそ、ペレット化を初めて行うチームにお勧めします. ウォーターリングシステムにより手動での糸通しの負担が軽減されますが、水の管理が追加されます。. 水中ペレタイザーはオペレーターとメンテナンススタッフに最も多くのことを要求します: ダイプレート温度制御, カッター刃の磨耗, および水室の密閉にはすべて規律ある注意が必要です. 私は常に、将来のサプライヤーに、金型とカッターの交換に関してバイヤーをどのように訓練しているかを尋ねます。, そこにダウンタイムが隠れているからです.
比較表と最適なシナリオ
| 属性 | ストランドペレタイザー | ウォーターリングペレタイザー | 水中ペレタイザー |
|---|---|---|---|
| 切断点 | 冷却後 (ソリッドストランド) | ダイフェイスで, リング冷却 | ダイフェイスで, 完全に水没した |
| ペレット形状 | 円筒形 | レンズ / ティアドロップ | 球形に近い |
| ほこり / 罰金 | 低から中程度 | 低い | 非常に低い |
| オペレーターのスキル | エントリーレベル | 中級 | 高度な |
| ベストフィット | リサイクル, 中程度の出力, 混合ストリーム | 充填コンパウンド, ミッドレンジのスループット | 高スループット, マスターバッチ, 形状が重要なグレード |
私の経験則: PPの柔軟なリサイクルのためにストランドを選択, PE, シンプルさが重要な場合は HDPE; 充填剤または中程度の研磨性のコンパウンドにはウォーターリングを選択してください; ボリュームがある場合は水中を選択してください, ペレットの粘稠度, または、優れた製品品質により、追加の複雑さが正当化される. 適切なペレタイザー タイプの選択は、施設の生産量に大きく影響します。, 製品の品質, 収益性, 健全な中古機器市場は、新しい資本を投入する前に構成を検証できることを意味します (販売のための中古配合およびペレット化装置, アーリントンマシナリー, 2024). 見る このリサイクル機械のリファレンス これらの方法が特定の樹脂ストリームにどのようにマッピングされるかについて.
ペレタイザー vs エクストルーダー: 関係を理解する
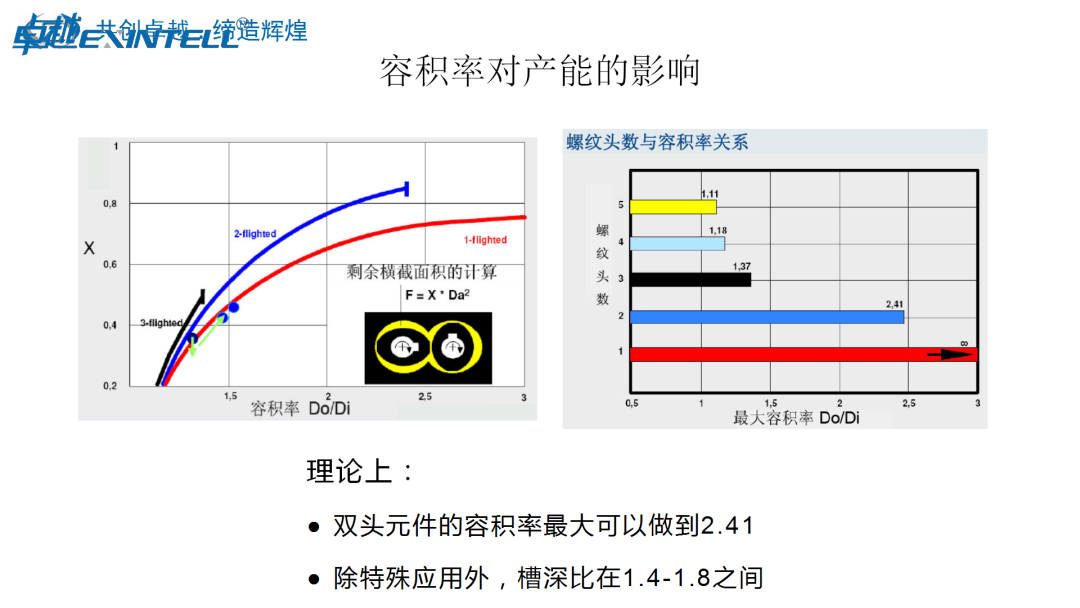
バイヤーからよく、押出機が必要かペレタイザーが必要かという質問を受けます。, そして私の答えは、その質問は誤った選択を引き起こすということです. この 2 つは補完的なマシンであり、ほとんどの場合、1 つの統合システムとして出荷されます。. 両者の役割分担を理解することで、仕様と予算の両方が明確になります。.
エクストルーダーが溶かして搬送; ペレタイザーのカットと成形
押出機は溶融押出の心臓部です. 加熱されたバレル内でネジが回転し、樹脂を溶かします。, 添加物を均質化する, 圧力を高める, 溶融したポリマーを金型に向かって搬送します. ペレタイザーがそのダイを引き継ぎます, 押出物を冷却し、完成した顆粒に切断します。. 要するに, the plastic extrusion machine handles thermal and mechanical processing, while the pelletizer handles forming. Treating them as a single value chain, rather than two isolated purchases, is how I keep specifications coherent.
Why They Are Usually Sold and Configured Together
A pelletizer is only as good as the melt feeding it, and an extruder producing off-spec melt cannot be rescued by a downstream cutter. That interdependence is why factories engineer and test them as matched systems. A twin screw extruder factory designs, エンジニア, 組み立てる, and tests complete extrusion systems used across plastics compounding, 食べ物, 製薬, および化学産業 (二軸押出機工場とは – B2B ガイド, 2024). When I audit a supplier, I want evidence they run the extruder and pelletizer together on the test floor with a representative material, not just individual component checks.
Two-Stage and Compounding Line Configurations
ラインアーキテクチャは関係が具体化される場所です. シングルステージラインはすべてを 1 回のパスで実行します. 2 段押出機では、一次押出機で溶融と混合を行い、二次押出機で脱気を行います。, 圧力の高まり, 優しく金型に伝えます, 熱に弱い材料や高充填材料を保護します。. フル配合ラインにサイドフィーダーを追加, 重量測定による投与, 真空排気機能により、ポリマー配合装置にフィラーを組み込むことができます, 色, そして正確に補強. 中国に本拠を置く工場は通常、ツインにまたがる幅広い製品ラインを提供しています, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー, そのため、多くの場合、単一のサプライヤーがペレット化ライン全体を構成できます。 (中国実験室二軸押出機工場カタログ, 2024).
これが購入決定に何を意味するか
機械が連結されているので、, 私は、押出機とペレタイザーを個別に価格設定するのではなく、常にシステム レベルで価格を仕様にマッピングします。. PP/PEマスターバッチ二軸スクリューマシンが米国各地で上場 $42,000 1個あたり, この数字は、裸のバレルではなく、押出機とペレタイザーの構成を反映しています。 (中国製.com, 2024). 見積もりを比較するとき, どの下流コンポーネントを正確に確認する, 冷却水浴, カッター, ドライヤー, とコントロール, 数字の中にいます.
ペレット化のための二軸スクリュー システムと一軸スクリュー システム
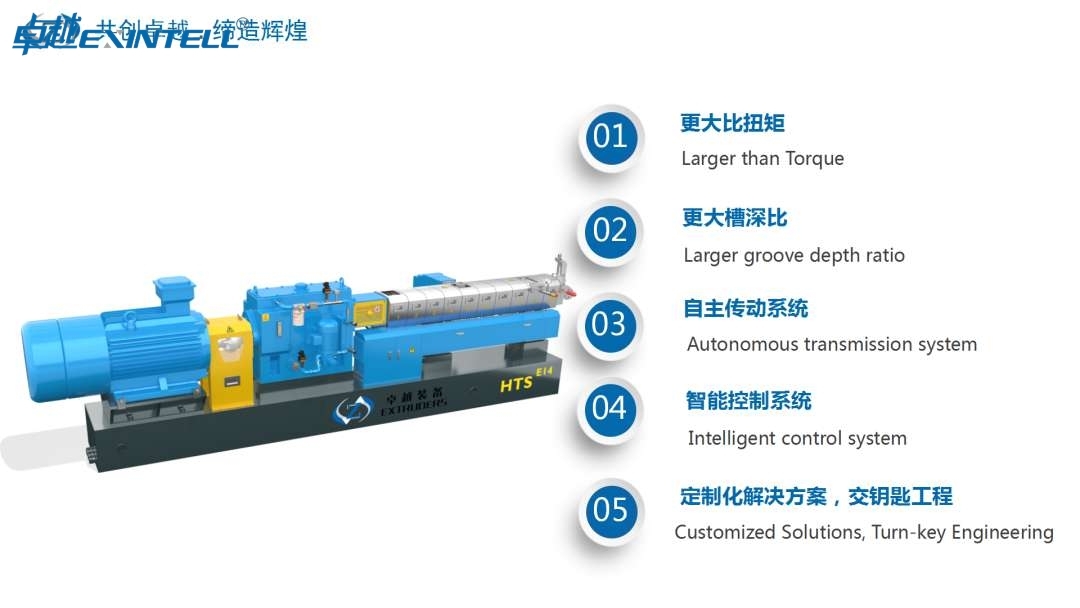
スクリュー構成は、ペレット化ラインにおいて最も重要なエンジニアリング上の選択です。, 私がバイヤーと最も多くの時間を過ごす場所です. 二軸ネジと一軸ネジのアーキテクチャはまったく異なる役割を果たします, and matching the right one to your material and output goals prevents expensive mismatches later.
Component Parts: Screw Elements, バレル, Shafts, and Side Feeders
Both systems share a common vocabulary. Screw elements are the modular segments, 運ぶ, 捏ねる, そして混ぜる, that thread onto the shafts. The barrel encloses the screws and carries the heating and cooling zones. Shafts transmit torque, and side feeders introduce fillers or reinforcements partway down the barrel. On a twin screw machine these elements are highly configurable, which is what gives the extruder screw configuration its flexibility. On a single screw, the geometry is largely fixed, which trades adaptability for simplicity and lower cost.
Intermeshing Twin Screws for Mixing and Compounding
Twin screw extruders use two intermeshing screws that continuously wipe each other, 配合に必要な集中的な分散混合を実現します。. これはマスターバッチに指定したアーキテクチャです, 充填化合物, およびリアクティブ処理, 噛み合うスクリューにより滞留時間とせん断を厳密に制御できるため. 加工材料や PET リサイクルの主力製品でもあります, マスターバッチ押出機または PET リサイクル押出機で添加剤を完全に均質化する必要がある場合.
単一のネジの強度でリサイクル作業を簡素化
単軸押出機は仕事が簡単な場合に威力を発揮します: 溶かしてきれいに運ぶ, 単一樹脂ストリーム. PPリサイクル用, HDPE, LDPE, とLLDPEをリサイクルプラスチックペレットに, 単軸プラスチック造粒機は、多くの場合、数分の一の資本コストとメンテナンスコストで処理量を実現します。. 私の経験では, buyers reprocessing their own uniform scrap rarely need the mixing power of a twin screw, and the simpler machine keeps operator skill requirements and spare-parts complexity low.
Triple Screw and Specialty Configurations
Beyond the two mainstream options, factory catalogs include triple screw and other specialty designs for niche mixing, 揮発分除去, or dedicated pipe extrusion. Conical twin screw extruders for PVC pipe, 例えば, are listed at approximately US $25,000 セットあたり, reflecting a purpose-built geometry rather than a general-purpose compounder (中国製.com, 2024). I treat these specialty units as material-specific tools; they excel at their intended job but are rarely the right general-purpose choice.
Matching Screw Design to Material and Output Goals
My selection framework comes down to two questions: how much mixing does the material need, and how much throughput do you require? High mixing demand or additive incorporation points to twin screw. Simple remelting of clean streams points to single screw. Output targets then set the screw diameter and line size. The table below summarizes how I steer that decision.
| 基準 | 単ネジ | ツインスクリュー (噛み合う) |
|---|---|---|
| 主な強み | 溶かして運ぶ | Mixing and compounding |
| Ideal materials | Clean single-resin recycling (PP, HDPE, LDPE, LLDPE) | マスターバッチ, 充填化合物, ペット, reactive systems |
| Configurability | Fixed geometry | Modular screw elements and side feeders |
| Capital and maintenance | より低い | より高い |
| Typical price signal | Entry-level recycling lines | ~US $42,000 for a PP/PE masterbatch system |
The market backs up how central these choices are. こんにちはサプライヤーリスト 1,569 twin screw extruder products with supply concentrated in Shandong, 浙江省, と江蘇省, giving US buyers real leverage to match screw design to their exact material and output goals (HiSupplier.com twin screw extruder directory, 2024). For a broader view of how compounding and pelletizing equipment is specified and traded, の Arlington Machinery compounding and pelletizing inventory is a useful reference point.
Matching Machines to Materials: PP, PE, ペット, PBAT, and More
In my experience sourcing equipment from a plastic pelletizer factory, the single biggest mistake buyers make is treating pelletizing lines as interchangeable. そうではありません. The resin you process dictates the screw configuration, the cooling method, the die plate and cutter design, and the pretreatment you need upstream. Before I ask any supplier about price, I define the material first. この規律により、数か月に及ぶやり直し作業が節約され、下流の購入者が期待するペレット サイズの均一性を物理的に提供できない機械の購入を防ぐことができます。.
PP, HDPE, LDPE, およびLLDPEリサイクルライン
ポリオレフィンはプラスチックリサイクルの主力製品です, そして、ほとんどの汎用ラインはそれらを中心に構築されています. このカテゴリのプラスチック ペレット製造機は、押出成形用に設計されています。, 冷却, ダイシングPP, HDPE, LDPE, およびLLDPEリサイクルの流れ (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024). これらの材料の場合、私は通常、一軸スクリュー押出機、またはウォーターリングまたはウォーターストランドペレット化と組み合わせた二段押出機を指定します。, どちらも業界全体の標準的な造粒方法です (プラスチックペレット化機, 2024).
実際的な違いは重要です. LDPE および LLDPE フィルムは密度が低く、湿気やインクで汚染されることがよくあります。, そのため、私は十分な冷却水バスと堅牢な脱気ゾーンを備えたストランドペレタイザーを好みます。. Rigid HDPE and PP flakes tolerate a water ring pelletizer well and run at higher throughput. If a supplier tries to sell one screw geometry for all four resins without discussion, that is a signal to slow down.
PET Recycling Extruders and Moisture Handling
PET is where inexperienced buyers get burned. Unlike polyolefins, PET is hygroscopic and hydrolyzes at melt temperature if residual moisture is present, which collapses intrinsic viscosity and produces brittle, off-spec recycled plastic pellets. A PET recycling extruder is not just a resin swap on a PP line. It requires crystallization and drying upstream, aggressive vacuum devolatilization during melt extrusion, and often a twin screw extruder for better mixing and moisture stripping. When I scope a PET line, I treat moisture handling as a non-negotiable line item, not an accessory.
PBAT and Bioplastic Pelletizing Considerations
PBAT and other compostable bioplastics behave differently again. They are heat-sensitive with a narrow processing window, and they tend to be sticky at the cutter. For these I lean toward an underwater pelletizer, which cuts pellets directly at the die face in a temperature-controlled water stream and minimizes thermal history. Gentle, precise temperature control across the extruder screw configuration protects the polymer and keeps pellet size uniformity within spec. If your product roadmap includes bioplastics, confirm the factory has actually run PBAT, not just polyolefins on similar hardware.
PVC, WPC, and Filler Masterbatch Requirements
PVC, 木材とプラスチックの複合材, and highly filled masterbatch push the line toward intermeshing screws and corrosion-resistant, wear-resistant metallurgy. PVC is thermally unstable and evolves corrosive gases, so conical twin screw machines are common here; conical twin screw extruders for PVC pipe are listed at approximately US $25,000 セットあたり (中国製.com, 2024). フィラーマスターバッチ, with heavy calcium carbonate or titanium dioxide loading, abrades screws and barrels quickly, so I always ask about barrel liner hardness and whether the die plate and cutter are rated for the abrasive load. A polymer compounding equipment line built for clean polyolefin will not survive long on 70% filled masterbatch.
Pelletizer Machine Price: What Actually Drives the Cost
購入者は仕様を与える前に価格を尋ねます, そして私は本能を理解しています. しかし、静的な定価だけではほとんど何も分かりません. 私の経験では、価格を仕様にマッピングすると、同じヘッドライン番号でも実際の価値の 2 対 1 の違いを隠すことができます。. ここでは、プラスチックペレタイザー工場から購入する際に実際にコストがどのように変動するかを分析します。.
kg/h 単位の容量が主な価格要因である
生産ライン能力, キログラム/時で測定される, 他の単一変数よりも相場を支配する. と評価されたライン 150 kg/h と 1 つの定格 1,000 kg/hはモーターサイズが異なります, ネジ径, ギアボックス, 冷却能力, とカッターのスループット. 入札額を比較すると, すべての見積もりを、kg/h あたりのコストの数値に正規化します。. It is the fastest way to see whether a low sticker price simply reflects a smaller machine rather than a better deal.
Screw Type, オートメーション, and Control System Impact
After capacity, screw architecture is the next big lever. A single screw extruder is the least expensive option and fine for straightforward polyolefin recycling. A twin screw extruder with intermeshing screws costs more but delivers superior mixing for masterbatch and moisture removal for PET. Automation adds real money: PLC control with recipe storage, 自動スクリーンチェンジャー, 重量送り, and pellet size monitoring all raise the price and lower the labor cost per ton. I decide how much automation to buy based on labor rates and volume, not on what looks impressive in a brochure.
Representative Price Ranges From Wholesale Listings
Public wholesale listings give useful anchors, provided you read them against specification. From current Made-in-China.com data (2024): a PP/PE pelletizer masterbatch twin screw machine is listed at US $42,000 1個あたり; conical twin screw extruders for PVC pipe run about US $25,000 セットあたり; and twin screw extruders configured for pet food production span US $25,000 に $80,000 per set depending on size and options. The table below maps those anchors to typical use.
| 構成 | Typical material | Screw type | Representative price |
|---|---|---|---|
| Conical PVC pipe extruder | PVC | コニカルツインスクリュー | ~US $25,000 / set |
| Masterbatch pelletizer | PP / PE | Twin screw | 私たち $42,000 / piece |
| 配合 / food-grade extruder | Various compounds | Twin screw | US $25,000–$80,000 / set |
Treat these as starting points. The right question is not “what does it cost” しかし “what capacity, screw type, and automation does that number include.”
Total Cost of Ownership Beyond the Purchase Price
The purchase price is the part everyone sees and the part that matters least over a machine’s life. My total cost of ownership model includes spare wear parts (ネジ, 樽, die plate and cutter blades), energy consumption per ton, water and cooling load, expected downtime, and the cost and lead time of service support from the supplier. A cheaper machine that idles for two weeks waiting on a screw from overseas can erase its entire price advantage in a single outage. I always ask for a recommended spares list and a written service response commitment before I sign.
New vs Used Plastic Pelletizing Equipment
The secondary market for pelletizing equipment is deep and active. 以上 74,000 wholesale used twin screw extruder products are listed on Made-in-China.com alone (2024), and specialist dealers maintain their own inventory. 適切なペレタイザー タイプの選択は、施設の生産量に大きく影響します。, 製品の品質, 収益性, and used inventory is genuinely available for buyers who know what to look for (アーリントンマシナリー, 2024). The question is when refurbished makes sense and when the premium for new is justified.
Cost Savings and Risks of Refurbished Machines
A quality refurbished line can cost 40% に 60% less than new and ship far faster, which is a strong argument when capital is tight or you need capacity quickly. The risk is that wear on the screw and barrel is invisible from the outside and directly determines mixing quality and output. A worn screw drops throughput, degrades pellet size uniformity, and raises energy use. Buying used without verifying wear is buying a number, not a machine. I only recommend used when I can inspect the core melt extrusion components or trust a dealer’s documented refurbishment.
What to Inspect on Used Compounding and Pelletizing Lines
My used-line inspection checklist is deliberate:
- スクリューとバレルの摩耗: measure clearance and check flight land condition, since this governs output and mixing.
- Die plate and cutter: inspect for erosion and confirm blade replacement availability.
- Gearbox and motor: listen and check for backlash, oil condition, and bearing noise under load.
- 制御システム: verify the PLC still boots, holds recipes, and has available parts, not an orphaned obsolete platform.
- Cooling water bath and pump: check for corrosion, scale, and leaks.
- Documentation: original spec sheet, run hours, prior processed materials (a machine run on abrasive filler wears faster).
If I cannot inspect in person, I insist on a video walkthrough under power and, 理想的には, a short trial run. プラスチック押出機メーカー メーカー
When Buying New From a Factory Is Worth the Premium
New is worth the premium in specific situations. If you need a warranty, a customized extrusion solution, a specific screw configuration for PET or bioplastics, or guaranteed spare-parts continuity for a decade, buy new from a factory. A twin screw extruder factory designs, エンジニア, 組み立てる, and tests extrusion systems for plastics compounding and adjacent industries (二軸押出機工場とは – B2B ガイド, 2024), and that engineering support is exactly what you are paying for. For a first line, a regulated end market, or any application where downtime is expensive, the certainty new equipment provides usually pays for itself.
Sources for Reliable Used Inventory
For used inventory I work from three channels. Established North American dealers such as Arlington Machinery carry vetted compounding and pelletizing lines with condition documentation (Used Compounding and Pelletizing Equipment for Sale, 2024), which lowers inspection risk. Global marketplaces like Made-in-China.com and HiSupplier list large volumes, 供給が山東省に集中している, 浙江省, と江蘇省 (HiSupplier.com, 2024) — strong on price, but you own the vetting. And factory refurbishment programs let you buy a rebuilt machine backed by the original manufacturer. Whichever channel you choose, apply the same inspection discipline; a listing is a lead, 保証ではありません. For a technical primer on machine types before you shop, の plastic pellet making machine overview (2024) 参考になります.
Certifications and Standards to Verify
Before I release a single dollar to any supplier, I treat certification as the entry ticket rather than a bonus. When I evaluate a Plastic Pelletizer Factory, the paperwork tells me whether the equipment will clear US customs, satisfy my insurer, and survive an OSHA walkthrough. According to Made-in-China.com certification filters (2024), the credentials that surface most often across extruder and pelletizer suppliers are CE, ISO 9001, UL, GMP, and SA8000. Each one answers a different question, so I read them as a set rather than treating any single mark as proof of quality.
CE Marking for Safety and EU-Aligned Design
CE marking is not a US requirement, but I still ask for it. 私の経験では, a factory that engineers to the CE machinery directive has already built guarding, 緊急停止, and documented risk assessments into the design. That discipline carries over to any market. If I ever resell or relocate a pelletizing line into Europe, the CE file saves me a costly retrofit. I request the Declaration of Conformity and the technical file references, not just a logo on a brochure.
ISO 9001 品質管理システム
ISO 9001 tells me the factory has a repeatable process behind the product. It does not certify that a specific twin screw extruder is good, so I never confuse it with a performance rating. What it gives me is traceability: material certificates for the screw and barrel steel, calibration records for the test bench, and corrective-action logs when a build fails inspection. I ask to see the certificate number and verify it against the issuing registrar, because an expired or fabricated ISO claim is a fast way to disqualify a supplier.
米国での使用に対する UL および電気安全の承認
これは米国のバイヤーが最も頻繁に見落とす資格です, そしてそれは試運転時にそれらを燃やします. 中国の工場では、UL または CSA の認定を受けていない制御コンポーネントを使用して 380V/50Hz まで構築することがよくあります。. パネルが UL 508A に準拠して構築されておらず、コンポーネントが NRTL リストに掲載されていない場合, 地元の電気検査官が機械への通電を拒否する場合があります. UL リストに登録されたコンタクタを指定します, ドライブ, および注文書の同封物, そして工場が北米の工場に 480V/60Hz 構成を供給できることを確認しました. サプライヤーがこれを行うことができない場合, 契約する前に国内パネルの再構築の予算を立てる.
医薬品および食品用途の GMP
ペレット化ラインが食品に触れた場合, ペットフード, または医薬品原料, GMP との関連性が任意から必須に移行. Twin screw extruders serve compounding, 食べ物, 製薬, および化学産業 (二軸押出機工場とは – B2B ガイド, 2024), and each of those downstream uses carries its own hygienic-design expectations. For food and pharma work I look for sanitary contact surfaces, clean-in-place capability, and documentation that supports FDA-compliant material contact. A factory that already builds GMP-oriented machines will understand these requirements without a long explanation.
How I Cross-Check a Certificate
Logos are cheap to copy, so I verify. I match the certificate number to the registrar or notified body database, confirm the scope actually covers extrusion machinery, and check that the issue and expiry dates are current. When a factory hesitates to share a machine-readable certificate or points me to a generic image, I treat that as a red flag and escalate my audit.
Factory vs Trading Company vs Marketplace
Where I buy shapes price, カスタマイズ, and the quality of support I get three years later when a die plate wears out. The market gives me three channels, and each behaves differently. Marketplaces demonstrate the scale of supply: 以上 74,000 wholesale used twin screw extruder products are listed on Made-in-China.com (2024), HiSupplier.com lists 1,569 twin screw extruder products concentrated in Shandong, 浙江省, と江蘇省 (2024), and China-based factories offer broad lines spanning twin, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー (中国実験室二軸押出機工場カタログ, 2024). That breadth is useful, but it also hides resellers among genuine manufacturers.
How to Tell a Real Manufacturer from a Reseller
A true Plastic Pelletizer Factory designs, エンジニア, 組み立てる, and tests its own extrusion systems (二軸押出機工場とは – B2B ガイド, 2024). A trading company brokers someone else’s output. I separate the two with a short set of probes. I ask for the manufacturing license and the physical plant address, then request a live video walkthrough of the machine shop and assembly floor. I ask engineering questions a broker cannot answer, such as the L/D ratio range they machine, their intermeshing screw element inventory, and how they configure the screw for a specific polymer. I also ask for the export license under their own name. A reseller can quote a price; only the maker can talk in depth about extruder screw configuration and melt extrusion behavior.
Verifying R&D and Production Capacity
Capacity claims are easy to inflate, so I look for evidence. I ask how many pelletizing lines the factory ships per month, whether it runs its own test bench for factory acceptance testing, and how many engineers sit in R&D versus sales. I request reference installations in North America and, when the order justifies it, I commission a third-party audit. A factory with real R&D can propose custom extrusion solutions; a shell operation will only echo my specification back to me.
Pros and Cons of Buying Through Made-in-China Style Platforms
Platforms are excellent for discovery and price benchmarking, less reliable for accountability. The advantage is reach and transparency on going rates. The disadvantage is that listing quality varies and after-sales support often evaporates once payment clears. I use marketplaces to build a shortlist, then move the qualified suppliers off-platform into a direct relationship with a proper contract before I place a deposit.
Channel Comparison
| 要素 | Direct Factory | Trading Company | Online Marketplace |
|---|---|---|---|
| Unit price | 最低; 中間マージンなし | より高い; broker markup added | Benchmark visible; final price negotiated |
| カスタマイズ (OEM/ODM) | Full; controls the build | 限定; relays requests | Varies by listed seller |
| Technical support | Direct to engineers | Indirect; slower turnaround | Inconsistent post-sale |
| Spare parts and service | Source of record for parts | Dependent on the underlying maker | Often unsupported |
| Best use | Long-run production lines | Small mixed orders, one contact | Discovery and price research |
私のルールはシンプルです: for a capital pelletizing line I want to run for a decade, I buy factory-direct so the party that built the die plate and cutter is the same party I call for a replacement.
OEM and ODM Customization Options
The reason I favor a genuine manufacturer becomes clearest here. A plastic pellet making machine has to be matched to the exact polymer stream it will process, whether that is PP, HDPE, LDPE, or LLDPE recycling material (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024). Off-the-shelf rarely fits a real plant, so I lean on OEM and ODM programs to get pellet size uniformity and throughput that match my process.
OEM vs ODM: Two Different Deals
I keep the distinction precise. Under OEM (own-brand) arrangements, I supply the design intent or brand and the factory builds to it, which suits private-label resellers and integrators who put their own plate on the machine. Under ODM, 工場が基本設計を所有しており、それを私の要件に合わせて調整します, ターゲットを絞った変更を伴う実証済みのエンジニアリングを求めるバイヤーに適しています。. 最初の商品を調達するほとんどの米国のバイヤーにとって, ODM は、カスタマイズとリスクのないエンジニアリングの間でより適切なバランスを実現します。.
特定のポリマー向けのカスタムスクリュー構成
スクリュー設計は、配合ラインが成功するか失敗するかを決めるものです. 適切な混合を実現するかみ合うツインスクリュー, 運ぶ, せん断要素は特定の樹脂の溶融品質を決定します, 硬質 PVC パイプ コンパウンドは、充填済み PP マスターバッチとはまったく異なります。. 実際の配合に対してスクリュー構成を指定します, フィラーと添加剤の充填を含む, そしてそれに応じてL/D比とバレルゾーンをモデル化するよう工場に依頼します。. ここでも、工場と再販業者のテストが効果を発揮します。, because only the maker can genuinely tailor the extruder screw configuration.
Pelletizing Method and Downstream Add-Ons
Customization extends past the screw. Water ring and water strand pelletizing are the standard granulation methods on offer (プラスチックペレット化機, 2024), and the choice affects pellet shape, cooling load, そしてメンテナンス. For clean, free-flowing pellets on many resins I favor an underwater pelletizer; for straightforward recycling streams a strand pelletizer with a cooling water bath is often more economical. I match the die plate, カッター, and cooling stage to the polymer and the target output.
Automation and Computerized Control Add-Ons
I ask about PLC control, recipe storage, 重量送り, およびリモート診断. Computerized control tightens pellet size uniformity, reduces operator error, and lets my team save and recall settings per formulation. For US installations I again insist on UL-listed control components and a 480V/60Hz build so the automation package does not stall at inspection.
How Customization Affects Lead Time and Price
Every custom element trades cost or time for fit, and I map that explicitly rather than reacting to a static list price. Marketplace listings give me a useful baseline: a PP/PE pelletizer masterbatch twin screw machine is listed at about US $42,000 1個あたり, conical twin screw extruders for PVC pipe at roughly US $25,000 セットあたり, and twin screw extruders for pet food production between US $25,000 そして $80,000 セットあたり (Made-in-China.com wholesale used twin screw extruder listings, 2024). From that base, a custom screw set, a specialized pelletizing method, and an automation package each add cost and typically extend lead time by weeks. 適切なペレタイザー タイプの選択は、施設の生産量に大きく影響します。, 製品の品質, 収益性 (販売のための中古配合およびペレット化装置, 2024), したがって、私はこれらのアドオンを総所有コストに対して測定された投資として扱います。, 項目経費ではない. 予算が厳しいとき, 中古機器の活発な流通市場が合理的な橋渡しとなる可能性がある, コアスクリューの形状が依然としてポリマーに適合する場合.
私のアプローチは、最初に仕様を書くことです, 次に、工場に価格と仕様の内訳をリクエストして、各カスタマイズにかかる金額とスケジュールを正確に確認できるようにします。. その透明感, どのヘッドライン価格よりも, 私のプロジェクトの利益を守るものです.
プラスチックペレタイザーのサプライヤーを評価する方法
プラスチックペレタイザー工場を精査したとき, 私は営業上の会話を最も信頼性の低いデータポイントとして扱います. マーケティング資料は簡単に作成できます; verifiable throughput, real reference installations, and documented service history are not. Below is the framework I use to separate a genuine manufacturer from a trading company reselling someone else’s machine.
Assessing Throughput Claims and Reference Installations
Rated capacity means little without context. A supplier that quotes “500 kg/h” should be able to tell me the polymer, the screw configuration, the moisture content of the feed, and whether that number reflects virgin resin or a contaminated recycling stream. 私の経験では, throughput drops 20 に 40 percent when you move from clean PP or PE pellets to post-consumer PET or LDPE film. I ask for two things: a spec sheet that ties the rating to a defined material and pellet size, and contact details for at least two reference installations running comparable output. If a factory cannot produce a single customer who will take a call, I treat the throughput figure as aspirational.
The market is large enough that references should be easy to supply. こんにちはサプライヤーリスト 1,569 twin screw extruder products with supply concentrated in Shandong, 浙江省, と江蘇省 (HiSupplier.com twin screw extruder directory, 2024), and Made-in-China.com shows over 74,000 wholesale used twin screw extruder listings (Made-in-China.com used equipment marketplace, 2024). A supplier operating at real scale in an active market has installed base to point to.
Reviewing Certifications, Warranties, and Service Scope
Certifications are a baseline filter, 保証ではありません, but their absence is a strong negative signal. Common factory credentials include CE, ISO 9001, UL, GMP, and SA8000 (Made-in-China.com certification filters, 2024). 米国の購入者の場合, CE marking on electrical components and a valid ISO 9001 quality-management certificate are the minimum I expect. I request the certificate PDFs with issuing-body numbers and verify at least one against the registrar’s database rather than accepting a logo on a brochure.
On warranties, I read the scope, not just the term. あ “12-month warranty” that excludes the die plate, カッター, ネジ, and barrel excludes the components most likely to fail. I want the warranty to name covered assemblies explicitly and to state whether it covers parts only or parts plus labor and shipping. I also confirm what the service scope includes: 試運転, オペレータートレーニング, リモート診断, and whether the factory has English-speaking engineers who can support a US time zone.
Checking Spare-Parts Availability and Response Times
A pelletizing line is only as productive as its uptime, and uptime depends on how fast you can replace a worn cutter or a cracked die plate. コミットする前に, I ask the supplier to quote lead times and prices for the top five wear items and to confirm whether those parts are stocked or built to order. A four-week manufacturing lead time on a cutter blade, plus ocean freight, can mean two months of lost production. I favor suppliers who either hold critical spares in inventory or can source interchangeable components from standard vendors.
Factory Versus Trading Company Versus Marketplace
Understanding who you are actually buying from shapes price, accountability, そしてサポート. 中国に本拠を置く工場は通常、ツインにまたがる幅広い製品ラインを提供しています, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー (中国実験室二軸押出機工場カタログ, 2024), which is one signal of genuine manufacturing depth. The table below maps the three sourcing channels against the criteria that matter most to a US buyer.
| 基準 | Direct factory (メーカー) | Trading company | Online marketplace listing |
|---|---|---|---|
| Price transparency | Ties price to spec; custom quotes | Marked up 10–25% over factory | 固定定価, 仕様は曖昧なことが多い |
| Technical support | エンジニアに直接アクセス | 中継中継に関する質問 | 販売後は限定的またはなし |
| スペアパーツの調達 | ソースからの OEM 部品 | 工場の関係によります | バイヤーが独自に調達する |
| 脂肪 / サンプルの実行 | オンサイトテストが可能 | 工場経由で手配 | まれに提供される |
| 保証責任 | 直接, 単一点 | 共有, 議論できる | 多くの場合、買い手のリスク |
プラスチック押出機と同じくらいサービス集約型の機械向け, 私は工場との直接的な関係を好みます. 市場取引によるわずかな節約で、ダイプレートやカッターに責任を負う人がいないペレット化ラインの停止コストを相殺できることはほとんどありません。.
実践的な工場監査チェックリスト
オンサイトで監査するか、ライブビデオウォークスルーで監査するか, I work from a fixed checklist so I compare suppliers on the same terms. The goal is to confirm that the factory can actually build, テスト, and support the machine I am buying, not just quote it.
Business License, カテゴリ, とR&D Capability Checks
I start with the legal foundation. I ask for the business license and confirm that its registered business scope includes manufacturing extrusion or plastic machinery, not just trading. A twin screw extruder factory that designs, エンジニア, 組み立てる, and tests extrusion systems for compounding, 食べ物, 製薬, and chemical applications carries an operating profile very different from a broker (二軸押出機工場とは – B2B ガイド, 2024). I look for evidence of R&D capability: an in-house design team, CAD drawings of screw configurations, and a machine shop that cuts its own screws and barrels rather than outsourcing every component.
On-Site or Virtual Audit Points to Confirm Capacity
On the floor, I confirm the things a brochure cannot fake. I want to see machines in various stages of assembly, a QC area with test equipment, and finished lines undergoing runoff. During a virtual audit I ask the guide to walk the full length of a production line and to open control cabinets so I can inspect wiring quality and the brand of PLCs, ドライブ, and heaters. I count active work cells against the stated headcount and monthly output. If a factory claims to ship a dozen pelletizing lines a month but the floor holds two machines, the numbers do not reconcile.
- Assembly floor with multiple lines in progress, matching stated capacity
- Dedicated QC and testing bay with calibrated instruments
- In-house machining of screws, 樽, and die plates
- Component brands visible in control cabinets (モーター, ドライブ, センサー)
- Raw-material and finished-goods inventory consistent with throughput claims
- Water strand and water ring pelletizing capability if your process needs it (プラスチックペレット化機, 2024)
Documentation: Certificates, Test Reports, 図面
A capable factory keeps a paper trail. I request certificate copies, prior factory acceptance test reports for similar machines, and general-arrangement drawings for the model I am ordering. Drawings matter for a US installation because they let my ラボスケール押出機 facilities team confirm footprint, utility loads, and cooling water bath connections before the machine leaves the port. If a supplier cannot produce a dimensioned drawing and an electrical schematic, integration surprises are almost guaranteed.
Red Flags That Signal an Unreliable Supplier
Certain patterns tell me to walk away regardless of price. A refusal to allow any audit, on-site or virtual, is the clearest. So is a quote that omits the polymer and pellet size the rating is based on, since that usually means the number is theoretical. Other warning signs: no named reference customers, warranties that exclude all wear components, prices dramatically below the market band with no explanation, and reluctance to put technical answers in writing. When I see prices well under the range for a given machine class, I ask why. コンテキストについて, PP/PE masterbatch twin screw machines list around US $42,000 per piece and conical twin screw extruders for PVC pipe around US $25,000 セットあたり (Made-in-China.com wholesale used twin screw extruder listings, 2024). A quote far below those levels for equivalent specs deserves scrutiny, not celebration.
品質管理, 脂肪, and Machine Testing
The single most important protection in a pelletizer purchase is a well-run factory acceptance test before the machine ships. Once a line clears customs in the US, resolving a defect becomes exponentially more expensive. FAT is where I confirm the machine performs to contract while the supplier still has full accountability and full access to their own floor.
Factory Acceptance Testing Before Shipment
I write FAT terms into the purchase order rather than treating them as a courtesy. The contract specifies the test material, target throughput, acceptable pellet size range, run duration, and pass/fail criteria, along with the right to witness in person or by live video. I insist the test uses my actual feedstock, or a representative equivalent, because a machine tuned on virgin PP will behave differently on recycled HDPE or contaminated LDPE film. Melt extrusion behavior, screen-pack pressure, and cutter load all shift with the material.
Verifying Output Rate, Pellet Size, and Stability
During the run I measure three things. 初め, sustained output rate over a defined period, not a peak reading, weighed against the contracted figure. 2番, pellet size uniformity, sampled at intervals and screened to confirm the fraction within tolerance. 三番目, process stability: I watch melt temperature, motor amperage, and die pressure hold steady across the run rather than drifting. A machine that hits target output for five minutes and then surges is not production-ready. This matters because pellet uniformity and consistent output directly drive downstream product quality and profitability (販売のための中古配合およびペレット化装置, アーリントンマシナリー, 2024).
Inspection of Critical Wear Components
Before and after the test run, I inspect the components that determine service life and pellet quality. Plastic pellet making machines are built to extrude, いいね, そしてサイコロPP, HDPE, LDPE, およびLLDPEリサイクルの流れ (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, リサイクルプラント.com, 2024), and each stage has a wear point I check:
- Die plate and cutter: flatness of the die face, sharpness and clearance of the blades, evidence of uneven wear that would produce tails or fines
- Screws and barrel: surface condition of intermeshing screws, matched screw configuration to the datasheet, no scoring in the barrel bore
- Cooling water bath and rings: uniform cooling, no clogging in a water ring pelletizer, correct water strand tension for a strand pelletizer
- Screen changer and heaters: even heat zones, functioning thermocouples, no dead zones that cause degradation
For an underwater pelletizer I pay particular attention to cutter-to-die contact and water temperature control, since both govern pellet shape and the risk of freeze-off.
Documenting Results to Protect Your Order
Testing only protects me if it is documented. I require a signed FAT report that records the test material, measured throughput, pellet size distribution, the process readings over the run, and photos of the inspected wear components. I tie the final payment milestone to a passed and signed FAT so there is a clear, contractual consequence if the machine underperforms. This documentation becomes the reference standard for the site acceptance test after installation and the baseline for any warranty claim. 私の経験では, a rigorous FAT report is the cheapest insurance a buyer can hold on a plastic pelletizer purchase, and it is the record that turns a warranty promise into an enforceable obligation.
MOQ, リードタイム, および支払い条件
When I move a project from quotation to purchase order, three commercial variables decide whether the deal is workable: 最低注文数量, リードタイム, and the payment structure. Capital extrusion equipment behaves nothing like consumable goods, so I treat these terms as engineering constraints rather than boilerplate. Getting them right protects both cash flow and the delivery schedule I have promised my own operations team.
Single-Line Versus Bulk Order Expectations
For most US buyers, ある “minimum order” is effectively a single pelletizing line. コモディティコンポーネントとは異なります, プラスチック押出機は仕様に従って作られています, そのため、工場が小規模な SKU に見られるような複数ユニットの MOQ を課すことはほとんどありません。. 私の経験では, 1 つの構成済みライン — 押出機, ダイプレートとカッター, 冷却水浴, そして下流では乾燥と分級が行われますが、これは完全に通常の独立した注文です.
大量の期待が会話を変える. マッチしたラインを複数購入する場合, またはリサイクルラインの横にマスターバッチ押出機を追加します, ボリュームを利用して、より良い単価設定を実現しています, ビルドキュー内の優先順位, およびバンドルされたスペア. PP/PEペレタイザーマスターバッチ二軸スクリューマシンが米国で上場 $42,000 1個あたり (Made in China.com の卸売リスト, 2024) 便利なアンカーです, しかし、私は複数行の取引で静的な定価を決して受け入れません。私は価格を正確なネジの構成にマッピングします。, スループット, 必要な自動化レベル.
Production and Shipping Lead-Time Planning
I plan lead time in two distinct phases. Production lead time covers fabrication, 組み立て, and factory acceptance testing; shipping lead time covers ocean freight, 税関, and inland drayage to my facility. Conflating the two is the most common scheduling mistake I see.
| 段階 | Typical duration | What I confirm in writing |
|---|---|---|
| Engineering and drawing approval | 2–4 weeks | ネジの形状, 金型設計, utility specs |
| Fabrication and assembly | 8–14 weeks | Milestone photos, コンポーネントブランド |
| Factory acceptance test (脂肪) | 1–2 weeks | Recorded throughput and pellet size uniformity |
| Ocean freight and customs | 4–8週間 | インコタームズ, port of entry, broker readiness |
| Inland delivery and rigging | 1–2 weeks | Rigging crew, dock or crane access |
These ranges are directional, not guarantees. I ask each Plastic Pelletizer Factory supplier for their own committed dates against these phases and tie milestone payments to them.
Deposit, Balance, and Escrow Structures
The conventional structure is a deposit against the balance: 頻繁 30% on order and 70% 出荷前に. I resist paying the full balance on a documents-only basis. その代わり, I negotiate the balance in tranches tied to verifiable milestones — for example, 30% デポジット, 40% on successful FAT, そして 30% after arrival or commissioning sign-off.
For larger capital purchases, I use an escrow arrangement or a documentary letter of credit so funds release only when defined conditions are met. On a first-time relationship with an unfamiliar manufacturer, escrow is the single most effective tool I have for aligning incentives without straining the factory’s working capital.
Protecting Cash Flow on Large Capital Purchases
A pelletizing line is a six-figure commitment once freight, 義務, and installation are included, so I manage the outflow deliberately. Milestone-based payments spread the exposure across the build. I also weigh equipment financing or leasing against a cash purchase, because preserving liquidity often matters more than the marginal interest cost. Where budgets are tight, a quality used line from a reputable dealer — pet food twin screw extruders, 例えば, run US $25,000–$80,000 per set (中国製.com, 2024) — can free capital for installation and spares.
Importing a Pelletizing Line into the US
Importing heavy machinery is where a sound purchase can quietly erode if I neglect the trade mechanics. The equipment cost is only part of the landed cost, and the difference between a smooth clearance and a stalled container usually comes down to preparation. I treat import planning as a parallel workstream that starts the day I place the order, not the week the ship arrives.
Tariffs and Duty Classification
Every plastic extrusion machine enters under a Harmonized Tariff Schedule (HTS) コード, and that classification drives the duty rate. Extrusion and pelletizing equipment generally falls within the machinery chapters, but the correct subheading depends on the machine’s function and configuration. I have a licensed customs broker confirm the HTS code before shipment, because a misclassification can trigger reassessment, penalties, and delays. I also check for any additional Section 301 duties that may apply to goods of Chinese origin, since these can materially change the landed cost.
インコタームズ: Who Bears Freight and Risk
Incoterms define exactly where cost and risk transfer between the factory and me, so I never leave them ambiguous on the contract.
- EXW (Ex Works): I take responsibility from the factory gate. Maximum control, maximum burden.
- FOB (Free On Board): The factory delivers to the origin port; I own ocean freight, 保険, and everything after. This is my usual choice because it balances control with simplicity.
- CIF (料金, 保険, 貨物): The seller arranges freight and insurance to the destination port; risk still transfers at origin.
- DDP (納入された関税の支払い): The seller handles nearly everything, including duties. Convenient, but I scrutinize the markup baked into the quote.
My rule is to match the Incoterm to my logistics competence. If I have Plastic Recycling Extruder Machine For Sale Manufacturer a reliable freight forwarder, FOB gives me the best cost visibility.
Heavy-Machinery Logistics and Rigging
A pelletizing line is heavy, tall, and awkward to move. I plan the last mile as carefully as the ocean leg: container destuffing, forklift or crane capacity, door and aisle clearances, and floor loading at the installation point. I book a professional rigging crew in advance rather than improvising on delivery day, because damage during offloading is both expensive and hard to attribute. Confirming that my dock, or a nearby crane point, can handle the crated weight is a five-minute check that prevents a very bad afternoon.
Customs Documentation and Compliance
Clearance depends on complete, accurate paperwork. I make sure the commercial invoice, 包装内容明細書, 船荷証券, and any certificates of origin match one another exactly — mismatches are a leading cause of holds. Where the equipment carries certifications such as CE or UL (common factory certifications include CE, ISO 9001, UL, GMP, and SA8000, Made-in-China.com による, 2024), I keep that documentation on file for compliance and for my own electrical inspection. I engage my broker early so entry is filed before the vessel arrives and demurrage never becomes an issue.
インストール, 試運転, and Operator Training
Delivery is a milestone, フィニッシュラインではない. The value of a Plastic Pelletizer Factory manufacturer relationship shows up during installation and the first weeks of production, when a well-supported startup separates a line that hits its rated throughput quickly from one that limps along producing off-spec pellets. I budget time, 公共事業, and attention for this phase deliberately.
Utility, フットプリント, and Power Requirements
Before the crate arrives, I confirm the site can actually run the machine. That means verifying electrical supply (電圧, phase, and amperage — imported lines often assume specifications that differ from US service), cooling water flow and temperature for the water bath, 圧縮空気, and adequate ventilation for melt extrusion. I lay out the footprint to allow clearance around the extruder screw, ダイプレートとカッター, and downstream conveying, plus safe operator movement. Mapping utilities to the factory’s spec sheet ahead of time is the cheapest insurance against a delayed startup.
オンサイトとリモートのコミッショニング サポート
コミッショニングはオンサイトまたはリモートで実施可能, そしてそれぞれに場所があります.
- オンサイトでの試運転: 工場の技術者が機械の調整を監督, 電気接続, そして最初の制作は直接行われます. 最初のラインまたは複雑な 2 段押出機にはこれを好みます, そしてエンジニアの旅費を誰が負担するのかを確認します, ビザ, 契約上の日当費用.
- リモート試運転: 地元の電気技師が現場で作業を行う、ビデオによるガイド付き起動. コストを削減し、スケジュールを迅速に立てる, 私のチームが以前の経験を持っている単純なストランドまたはウォーターリングペレタイザーの能力もますます高まっています.
どちらを選んでも, 私は、文書化された試運転チェックリストと、FAT の結果に関連付けられた署名済みの受諾記録を要求します。.
一貫したペレット品質を実現するためのオペレーターのトレーニング
Consistent output is an operator skill as much as a machine capability. During commissioning I have the factory technician train my team on the variables that govern pellet size uniformity: melt temperature profiles, スクリュー速度, cutter speed relative to throughput, cooling water bath conditions, and die maintenance. For recycling streams — PP, HDPE, LDPE, and LLDPE — I make sure operators understand how feedstock variability shifts those settings so they can hold quality as the material changes. Well-trained operators catch drift before it becomes scrap.
Ramp-Up to Rated Throughput
I treat the climb to rated capacity as a controlled process, not a switch. The line starts at a conservative rate, stabilizes pellet quality, and then steps up while I monitor motor load, melt pressure, and cut quality at each level. Reaching nameplate throughput typically takes days to a few weeks depending on material complexity and crew experience. I document the settings that produce good pellets at each rate so my operators have a repeatable recipe — that record becomes the foundation for the total cost of ownership case, because stable, in-spec production is what turns a capital purchase into a profitable asset.
スペアパーツ, Service, and Minimizing Downtime
Once a line is running, the purchase price stops being the number that matters most. 私の経験では, the operators who protect their margins are the ones who plan for wear before it happens. A pelletizing line is a chain of consumable contact surfaces, and every one of them degrades under heat, プレッシャー, と摩耗. Recycled feedstock accelerates that wear because contamination and filler content grind against metal far more aggressively than virgin resin.
Common wear parts and how they fail
Four component groups drive most of my maintenance budget on any plastic extrusion machine:
- ネジ. 二軸押出機で, the intermeshing screws and their individual segments wear at the flight edges. Abrasive fillers like glass fiber or calcium carbonate can cut screw life dramatically. A worn extruder screw configuration loses conveying efficiency and melt homogeneity before it ever fails outright.
- バレル. Barrel liners erode in the same high-shear zones as the screws. Because barrel replacement is expensive and slow, I treat barrel wear monitoring as a leading indicator, not a reactive fix.
- Die plates and cutters. The die plate and cutter assembly determines pellet size uniformity. On underwater pelletizer and water ring pelletizer systems, cutter blades and the die face see constant contact; dull blades produce tails, 罰金, and irregular granules.
- Screen packs and filters. Cheap to stock, quick to change, and the single most common cause of avoidable pressure spikes.
Building a critical-spares inventory
My rule is to keep on hand any part whose lead time from Asia exceeds the downtime cost of stocking it. For most US buyers importing from concentrated supply regions like Shandong, 浙江省, and Jiangsu — where HiSupplier catalogs roughly 1,569 二軸押出機製品 (HiSupplier.com twin screw extruder directory, 2024) — replacement screws and barrels can take weeks to ship. That makes a modest critical-spares kit cheaper than a single stalled production week. I stock at least one full set of cutter blades, a spare die plate, a screen-pack supply for several months, シール, 熱電対, and a heater band or two.
Service-level agreements and lead times
Before I sign a purchase order, I negotiate the service terms in writing. The questions I insist on answering:
- What is the guaranteed lead time for wear parts, and does the factory hold them in stock or manufacture to order?
- Are spare parts standardized, or are screws and dies proprietary to that manufacturer?
- Is remote commissioning and troubleshooting support included, and in what time zone?
- What is the warranty scope, and does it survive the use of third-party spares?
Because a genuine factory designs, エンジニア, 組み立てる, and tests its own extrusion systems (二軸押出機工場とは – B2B ガイド, 2024, exintellmach.com), it can usually supply matched spares faster and more reliably than a trading company reselling someone else’s machine. That is one of the strongest practical arguments for buying direct.
Preventive maintenance scheduling
I run maintenance on a tiered calendar rather than waiting for failure. Daily checks cover water bath temperature, cutter sound, and pellet appearance. Weekly work covers screen changes and torque logging. 四半期ごと, I pull and measure screw and barrel clearances to trend wear. This discipline is what keeps unplanned downtime rare, and it costs a fraction of an emergency rebuild.
スループット, エネルギーの使用, and Return on Investment
The right machine is the one sized to the production plan, 最大の見出し容量を持つものではない. バイヤーがペレット化ラインのサイズを大きくしすぎているのを見てきました, その後、半分空の状態で稼働させながら、エネルギーとメンテナンスのコストを全額支払います. 予測される需要に応じて容量をサイジングすることが最初の ROI 決定です, そしてそれはお金が人の手に移る前に起こります.
生産計画に合わせて容量をサイジングする
年間生産目標から始める, 現実的な稼働時間を差し引く (計画的なメンテナンス, 切り替え, 原料の変動), その後、ネームプレートのスループットをキログラム/時で確認します。. 安定した需要を大幅に上回る評価を受けたマシンは資本を無駄にします; 需要を正確に評価したものには、成長やダウンタイムの余地がありません. 年間を通じて空き容量を持たずに変動を吸収できる十分なヘッドルームを確保することを目指しています.
経常コストとしてのエネルギー消費量
溶融押出はエネルギーを大量に消費します. バレルヒーター, 駆動モーター, 冷却システム, and pelletizing water pumps run continuously, and over a machine’s life the electricity bill often rivals or exceeds the purchase price. 見積もりを比較してみると, I ask for installed motor power and specific energy consumption per kilogram of throughput, then model that against local industrial power rates. A cheaper machine that draws more power per pellet can lose money every hour it runs.
Estimating payback for a recycling or compounding line
Payback is straightforward arithmetic once you have the inputs. My model looks like this:
- Revenue per unit. The market price of recycled plastic pellets or compounded material, less feedstock and additive cost, gives contribution margin per kilogram.
- Annual output. Realistic throughput times operating hours.
- Recurring costs. エネルギー, 労働, 摩耗部品, そしてメンテナンス.
- Payback period. Total landed capital cost divided by annual net contribution.
The table below shows how upfront cost, capacity class, and typical application map together across the machine types I encounter. Prices are drawn from current marketplace listings and should be read as configuration-dependent starting points, not fixed quotes.
| 機械 / 構成 | Typical application | Indicative price | Notes on ROI profile |
|---|---|---|---|
| 円錐二軸押出機 | PVC pipe profile production | ~US $25,000 セットあたり | Lower entry cost; アプリケーション固有の, 柔軟性が低い |
| Twin screw extruder (ペットフード) | Food extrusion / ペットフード | US $25,000–$80,000 per set | Wide range reflects capacity and automation level |
| PP/PE masterbatch twin screw | Masterbatch and compounding | ~US $42,000 1個あたり | Mid-tier; strong fit for polymer compounding equipment |
| Recycling pellet making machine | PP, HDPE, LDPE, LLDPE recycling | Configuration-dependent | Payback driven by feedstock cost and pellet resale margin |
Price data: Made-in-China.com wholesale used twin screw extruder listings (2024). Recycling machines are designed to extrude, いいね, そしてサイコロPP, HDPE, LDPE, and LLDPE streams (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024, リサイクルプラント.com).
Balancing upfront cost against long-term output
An active secondary market — Made-in-China.com alone lists more than 74,000 卸売中古二軸押出機製品 (2024) — makes it tempting to chase the lowest sticker price. I resist that. A used or bargain machine with unknown wear on screws, 樽, and dies can carry hidden refurbishment and downtime costs that erase the savings. The right comparison is total cost of ownership over the payback horizon: capital plus energy plus spares plus expected downtime. When I run that math, a slightly higher upfront price from a factory that supports the machine usually wins.
Can You DIY a Plastic Pelletizer?
I get this question often, usually from startups trying to prove a concept on a tight budget. The honest answer is that a DIY build can demonstrate the principle of melt extrusion, but it rarely produces material a commercial buyer will accept. Understanding why saves a lot of wasted effort.
Why hobby-scale builds rarely meet commercial needs
A pelletizing line is a coordinated system: a heated barrel with a precisely matched screw, controlled melt pressure, a die plate sized for consistent flow, a cutter synchronized to output, and a cooling water bath tuned to the polymer. Homemade rigs almost always compromise on the screw geometry and temperature control, and those two factors govern melt homogeneity. Without them, pellet size uniformity collapses, and inconsistent granules cause dosing and processing problems downstream. Commercial customers buying recycled plastic pellets expect tight tolerances that improvised equipment cannot hold.
安全性, 一貫性, and throughput limitations
Three limits define the ceiling on any garage build:
- 安全性. Extruders combine high heat with high pressure. An unengineered barrel or a die that lacks a proper rupture and pressure-relief design is a genuine hazard. This is the risk I take most seriously, because a blocked die can build dangerous pressure quickly.
- 一貫性. Manual temperature control and unregulated feed produce batch-to-batch variation that makes the output hard to sell.
- スループット. Hobby builds measure output in grams per hour, not the kilograms per hour a business needs to be viable.
When lab-scale factory units make more sense
Rの場合&D, formulation trials, or small-batch validation, I steer people toward a purpose-built lab-scale machine rather than a homemade one. Factories catalog compact laboratory twin screw extruders alongside their production lines and offer broad ranges including twin, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー (中国実験室二軸押出機工場カタログ, 2024, zextrusion.com). A lab unit gives you controlled, repeatable results and a data path that scales cleanly to a production machine — something a one-off build cannot provide.
Risks of unengineered pressure and heat systems
My closing view is simple. The savings from a DIY pelletizer are illusory once you account for safety exposure, rejected material, and the throughput gap. Because choosing the right pelletizer type significantly affects facility output, 製品の品質, 収益性, and used inventory is readily available (販売のための中古配合およびペレット化装置, 2024, アーリントンマシナリー), even budget-constrained buyers have better options than building from scratch. A properly engineered lab or entry-level factory unit protects your people and your reputation, and that is worth far more than the cost it saves.
Brand and Benchmarking: MAAG and Comparable Factories
When I benchmark a pelletizing purchase, I start with the premium names because they set the reference points for what the technology can do at its best. Brands like MAAG have earned their reputation on tight pellet size uniformity, robust die plate and cutter engineering, and consistent long-run performance in demanding compounding applications. I treat those machines as the performance ceiling, then ask a more practical question: how much of that ceiling does my actual process require, and what am I willing to pay for the last increment of it?
What the Premium Price Actually Buys
私の経験では, the premium you pay for a top-tier brand buys three concrete things. 初め, metallurgical quality in wear parts, ネジ, and cutter blades that extends service intervals under abrasive loads. 2番, controls and process consistency that hold pellet dimensions within tighter tolerances across shifts. 三番目, a mature global service network that shortens response time when something fails. Those are real advantages. What the premium does not automatically buy is a better fit for a mid-volume recycling stream that tolerates slightly wider pellet variance, and that distinction matters when the price gap can be substantial.
How Specialized China Factories Compare on Cost and Lead Time
Specialized China factories compete hard on both acquisition cost and configuration breadth. Catalogs from these suppliers routinely span twin screw, triple screw, 二段式, and single screw machines alongside underwater pelletizers, so a buyer can source a full pelletizing line from one manufacturer (中国実験室二軸押出機工場カタログ, 2024, https://www.zextrusion.com). Published list prices give a useful anchor: a PP/PE masterbatch twin screw machine is listed at roughly US $42,000 1個あたり, 米国近郊の PVC パイプ用円錐二軸押出機 $25,000 セットあたり, and pet-food twin screw lines between US $25,000 そして $80,000 セットあたり (Made in China.com の卸売リスト, 2024, https://www.made-in-china.com). Supply is concentrated in Shandong, 浙江省, と江蘇省, where HiSupplier alone lists 1,569 二軸押出機製品 (HiSupplier.com directory, 2024, https://www.hisupplier.com).
Choosing Based on Total Value, Not Brand Alone
I make the decision on total value rather than the logo on the cabinet. That means mapping price to specification and then adding the full cost of ownership: spare screws and barrels, cutter refurbishment, expected downtime, そしてサービスの対応. より長い耐用年数とより迅速なサポートを備えたプレミアム ユニットは、総コストで有利になる可能性があります。 24/7 研磨操作. 専門工場での製造は、設備投資の節約によりスペア一式を調達できるにもかかわらず、プレミアム価格を下回る中量リサイクルラインで成功することがよくあります。. 以下の表は、その比較をどのように組み立てるかを示しています.
| 調達パス | 典型的な資本コスト | ペレットサイズの均一性 | リードタイム | サービスネットワーク | ベストフィット |
|---|---|---|---|---|---|
| プレミアムブランド (例えば, MAAGクラス) | 最高 | 最も厳しい公差 | より長い, クォータ主導型 | 成熟したグローバルサポート | 高価値の配合, 24/7 研磨義務 |
| 中国専門工場 | US $25,000–$80,000 per set (中国製.com, 2024) | 良い, アプリケーションに依存する | 適度, メーカー直送 | 地域別; 工場によって異なります | 中量リサイクル, カスタムライン |
| Trading company / 市場 | 変数マークアップ | 供給元のユニットに依存 | 在庫品に関しては最速 | 技術的な深さが限られている | 商品単位, 監査能力のない買い手 |
私のルールはシンプルです: use the premium brand as the benchmark for what good looks like, then verify whether a specialized manufacturer meets your process tolerances at a lower total cost before you pay for the badge.
Common Pelletizing Problems and How Factories Solve Them
Most of the pelletizing complaints I hear trace back to a short list of recurring issues. Understanding the mechanism behind each one tells you which factory capabilities actually matter, and it is where responsive supplier support pays for itself.
Inconsistent Pellet Size and Cutter Wear
Inconsistent pellet size is usually a symptom rather than a root cause. In strand and water ring systems, it points to uneven melt flow across the die plate, worn cutter blades, or a cooling water bath that is not stabilizing strand diameter before the cut. A good factory diagnoses this by checking blade-to-die clearance, melt pressure uniformity, and screw configuration rather than simply replacing parts. Because water ring and water strand pelletizing are standard offered methods for plastic granulation (プラスチックペレット化機, 2024, https://www.yjplasticextruder.com/plastic-pelletizing-machine/), a capable manufacturer can advise which method holds size best for your polymer before you commit.
Moisture, 脱気, and Contamination Issues
Moisture and volatiles cause voids, splay, and weak pellets, and they are especially punishing on recycled feedstock. The fix lives in the extruder: adequate venting, vacuum degassing zones, and in some cases a two-stage extruder that separates melting from devolatilization. Contamination from mixed streams calls for melt filtration ahead of the die. When I evaluate a supplier, I ask specifically how their screw configuration and venting handle wet or dirty recycled input, because plastic pellet making machines built for PP, HDPE, LDPE, and LLDPE recycling must manage exactly these conditions (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024, https://www.recycle-plant.com/plastic-pellet-making-machine-2.html).
Screw and Barrel Wear from Abrasive Fillers
Abrasive fillers such as glass, タルク, and calcium carbonate erode screws and barrels, and that wear quietly degrades output and pellet quality long before a failure. This is where premium metallurgy earns its keep, but specialized factories address it too through bimetallic barrels, nitrided or tool-steel screw elements, and honest wear-life estimates. I always ask for the wear-part material spec and expected service interval at my filler loading, then price a spares package accordingly.
How Good Factory Support Shortens Troubleshooting
The difference between a two-hour fix and a two-day outage is almost always support quality. A factory that engineers, 組み立てる, and tests its own extrusion systems can interpret a symptom over a video call and ship the right part first time (二軸押出機工場とは, 2024, https://www.exintelmach.com). That is why I weight remote diagnostic capability, spare-part stocking, and documented screw configurations heavily in supplier selection. Good support does not just fix problems faster; it prevents the misdiagnosis that turns a cutter adjustment into an unnecessary screw replacement.
よくある質問
Where can I find pelletizer machines for sale, and what are typical prices?
You have three main channels: direct factory purchase, 商社, and equipment marketplaces. Marketplaces show an active market with over 74,000 wholesale used twin screw extruder listings (中国製.com, 2024, https://www.made-in-china.com), and used compounding and pelletizing inventory is also available through North American dealers (アーリントンマシナリー, 2024, https://www.arlingtonmachinery.com/plastic-extruder/pl.sl.3.0/compounding-pelletizing/). As a price anchor, PP/PE masterbatch twin screw machines list around US $42,000, PVC conical units near US $25,000 セットあたり, and pet-food lines from US $25,000 に $80,000 セットあたり (中国製.com, 2024). Treat these as starting points and price to your exact specification.
What is the best pelletizer type for recycled PP and PE?
For recycled PP and PE, I usually recommend a water strand or water ring pelletizer paired with a properly vented single or twin screw extruder. These streams carry moisture and contamination, so venting and melt filtration matter more than raw throughput. PP専用の機械, HDPE, LDPE, およびLLDPEのリサイクルは押出を処理します, 冷却, これらのポリマーに必要なダイシングシーケンス (プラスチックペレット製造機, 2024, https://www.recycle-plant.com/plastic-pellet-making-machine-2.html). 水中ペレット化は、ペレットの形状とダスト制御により複雑さが増すことを正当化できる、より大量の場合に検討する価値があります。.
木材またはバイオマスペレタイザーはプラスチックユニットとは異なりますか?
はい, 実質的に. 木材およびバイオマスのペレタイザーは、リングまたはフラット ダイを通して乾燥繊維を圧縮するダイ アンド ローラー圧縮機構を使用します。, 溶融相なし. プラスチックペレタイザーは、溶融押出とその後の切断およびウォーターバスでの冷却に依存しています。. この 2 つは交換可能ではありません, プラスチックリサイクルライン用のバイオマス機械を見積もるサプライヤーは要件を読み間違えた. 装置がダイプレートとカッターを備えたプラスチック押出機であることを確認します。, not a compression pellet mill.
How do I choose the right factory rather than just the cheapest quote?
I run every candidate through a short vetting framework: confirm they are a manufacturer rather than a trading company, verify relevant certifications, and request wear-part specs and screw configurations for my material. Common factory certifications include CE, ISO 9001, UL, GMP, and SA8000 (中国製.com, 2024, https://www.made-in-china.com). I also ask for reference installations running my polymer and filler loading, since a factory that engineers and tests its own systems will answer those questions specifically rather than generically.
What total cost of ownership should I budget beyond the machine price?
The sticker price is only the beginning. I budget for spare screws and barrels, cutter blade refurbishment, melt filter screens, expected downtime, and service response time. On abrasive filler applications, wear parts can dominate multi-year cost. A slightly more expensive machine with longer wear life and faster support often delivers a lower total cost of ownership, which is why I model spares and downtime before comparing quotes rather than after.
How long do delivery and commissioning usually take?
For a standard configuration from a specialized China factory, I plan on roughly 8 に 16 weeks for build and shipping, with premium brands often running longer due to production queues. Commissioning and startup on-site typically add one to three weeks depending on line complexity and operator training. 米国の購入者向け, I build in additional time for ocean freight, 通関, and any applicable tariffs, and I confirm Incoterms early so responsibility for freight and duties is unambiguous. Marketplace stock units can ship faster, but factory-built lines to your specification are worth the wait when quality and support are the priority.
What Is a Plastic Pelletizer Factory and Why It Matters for B2B Buyers
When I evaluate sourcing decisions for procurement teams, I start by defining what a plastic pelletizer factory actually is, because the label gets applied loosely across the market. 私の経験では, a genuine factory designs, エンジニア, 組み立てる, and tests complete extrusion and pelletizing systems in-house rather than reselling machines it never built. A comparable pattern holds in adjacent equipment categories: a twin screw extruder factory “デザイン, エンジニア, 組み立てる, プラスチックの配合に使用される押出システムをテストします, 食べ物, 製薬, および化学産業” (二軸押出機工場とは – B2B ガイド, 2024). That vertical integration is the distinction I care about most, because it determines who is accountable when a die plate wears out or a screw configuration underperforms.
意味: What the Factory Actually Builds
A plastic pelletizer factory produces the machinery that converts molten or reclaimed polymer into uniform pellets. The core process is straightforward in principle: melt extrusion pushes material through a die, a cooling water bath solidifies it, and a cutter dices it into granules. 実際に, the equipment spans several categories. Chinese and international factories commonly offer “ツイン, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー” (中国実験室二軸押出機工場カタログ, 2024). Alongside those, I typically see strand pelletizers and water ring pelletizers, 以来 “water ring and water strand pelletizing are standard offered methods for plastic granulation” (プラスチックペレット化機, 2024).
市場の状況: An Active, Concentrated Supply Base
The supply market is large and geographically concentrated, which matters for buyers weighing lead times and travel for audits. HiSupplier “リスト 1,569 二軸押出機製品, 供給が山東省に集中している, 浙江省, と江蘇省” (HiSupplier.com twin screw extruder directory, 2024). The secondary market is even deeper: “以上 74,000 wholesale used twin screw extruder products are available, indicating an active secondary market” (Made-in-China.com used equipment marketplace, 2024). I read that volume as both an opportunity and a risk. There is abundant inventory, but the sheer number of listings makes it easy to mistake a trading company or marketplace reseller for an actual manufacturer.
主な用途: Where the Pellets Go
The reason this equipment matters commercially is the end product. Plastic pelletizers “廃プラスチックを小さくします, ボトルの製造に使用される均一なペレット, コンテナ, パイプ, および自動車部品” (トップ 10 plastic pelletizer Factory in the world, 2024). On the recycling side, plastic pellet making machines are “designed for extruding, 冷却, ダイシングPP, HDPE, LDPE, およびLLDPEリサイクルの流れ” (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024). For buyers running masterbatch, 配合する, or PET recycling operations, the polymer you process dictates the machine type. A PET recycling extruder has different drying and shear demands than a PVC line, and matching the extruder screw configuration to your resin is where uniform pellet size and profitability are won or lost.
How to Choose the Right Plastic Pelletizer Factory Supplier
Choosing a supplier is where most of the risk concentrates, and it is also where competitor guides tend to go quiet. I want to give you a buyer-side framework rather than a static price list, because “choosing the right pelletizer type significantly affects facility output, 製品の品質, 収益性” (販売のための中古配合およびペレット化装置, 2024). 以下は私が使用するプロセスです.
Vendor Evaluation: Factory vs. Trading Company vs. Marketplace
The first question I ask any prospective supplier is who owns the production. 3 つのチャネルは価格に関して大きく異なります, accountability, 販売後のサポート.
| チャネル | 彼らは誰ですか | Price transparency | アフターセールス & 保存されました | に最適 |
|---|---|---|---|---|
| Direct factory (メーカー) | デザイン, ビルドします, 社内で機械をテストします | 仕様にマッピングされた見積もり; カスタマイズ可能 | エンジニアリングへの直接アクセス; 純正OEM部品 | カスタム押出ソリューションと長期サービスを必要とするバイヤー |
| Trading company | 複数の工場からの調達仲介 | 工場出荷時の価格に重ねて値上げ; 限られた仕様の制御 | Indirect; 実際のメーカーとの関係によります | バイヤーの注文基準, 既製ライン |
| Marketplace / 中古在庫 | 新品と中古品を集約したリスト | 表示価格, 例えば, PP/PE マスターバッチツインスクリュー、US $42,000/個 | 変数; 中古機器の場合は現状のままであることが多い | 予算重視の購入者は改装のリスクを受け入れる |
上記の表示価格は、 “PP/PEペレタイザーマスターバッチ二軸スクリューマシンが米国で上場 $42,000 1個あたり” (Made-in-China.com wholesale used twin screw extruder listings, 2024). 私は市場の数字をアンカーとして扱います, 最終的なコストではない.
Price-to-Specification Mapping
Static list prices mislead buyers because the same category spans a wide range based on capacity and application. Twin screw extruders for pet food production, 例えば, は “listed between US $25,000 そして $80,000 セットあたり,” while conical twin screw extruders for PVC pipe run “approximately US $25,000 セットあたり” (Made-in-China.com wholesale used twin screw extruder listings, 2024). Rather than asking “what does it cost,” I ask suppliers to tie every quote to throughput, ネジ径, intermeshing screw design, and target pellet size uniformity. If a vendor cannot map price to specification, that is a signal in itself.
私が注目する危険信号
- No verifiable factory address, or a refusal to permit a virtual or on-site audit.
- Certifications claimed but never documented. Common legitimate marks include “CE, ISO 9001, UL, GMP, and SA8000” (Made-in-China.com certification filters, 2024); ask for the actual certificate numbers.
- Quotes with no throughput figures, no test protocol, and no spare parts list.
- あ “メーカー” whose catalog spans dozens of unrelated product families, which often signals a trading company.
- Reluctance to discuss Incoterms, US import tariffs, or logistics responsibility.
デューデリジェンスチェックリスト
- Confirm in-house design and assembly, ideally with a factory acceptance test (脂肪) you can witness by video.
- Request certificate copies for CE, ISO 9001, およびUL, then verify numbers with the issuing body.
- Ask for three reference customers running comparable resins and capacities.
- Get a written spare parts and lead-time schedule for the die plate, カッター, and screws.
- インコタームズを明確にする (I favor FOB or CIF for first orders) and confirm HS codes for accurate US duty estimation.
- Require a sample pellet run on your resin to validate melt extrusion quality and pellet size uniformity.
総所有コスト
The purchase price is rarely the largest number. 私の経験では, 保存されました, service response time, ダウンタイム, and energy consumption dominate a five-year total cost of ownership. A cheaper polymer compounding equipment line that idles for weeks awaiting a cutter from overseas can erase its savings in a single quarter. I ask suppliers to quantify mean time to repair and to hold critical wear parts in a US or regional warehouse where possible.
What Is a Plastic Pelletizer Factory and What Does It Produce
To close the loop, I want to consolidate exactly what these factories output and how the machine types differ, because the terminology confuses even experienced procurement staff. A plastic pelletizer factory is a manufacturer of the complete pelletizing line: the plastic extrusion machine, the cooling water bath, the die plate and cutter, and the downstream handling that turns polymer into recycled plastic pellets or virgin compound.
Key Considerations by Machine Type
ツインスクリュー vs. 単軸押出機
A twin screw extruder uses intermeshing screws that give strong mixing and shear control, which suits masterbatch, 配合する, およびリアクティブ処理. A single screw extruder is simpler and often more economical for straightforward reprocessing of a single, clean resin stream. Two-stage extruders add venting for moisture-sensitive materials like PET.
Pelletizer Cutting Methods
The three methods I encounter most are the strand pelletizer, the water ring pelletizer, and the underwater pelletizer. Strand and water ring approaches are standard, cost-effective choices for many PP, PE, HDPE, LDPE, and LLDPE streams. Underwater pelletizing produces very uniform, low-dust pellets and is often my recommendation for high-throughput or high-value polymer lines where consistency drives downstream quality.
Practical Tips
- Match the machine to the resin first, then to throughput. A PVC line and a PET recycling extruder are not interchangeable regardless of price.
- Insist on a sample run. Pellet size uniformity on your own material tells you more than any brochure.
- Budget for spares up front, especially die plates, カッター, およびネジ要素, which are consumable.
- Treat marketplace and wholesale plastic machinery prices as reference points, then negotiate against a documented specification.
Industry Context
The broader picture is a mature, globally distributed supply base with deep new and used inventory, concentrated manufacturing in Chinese provinces, and a strong pull from recycling and circular-economy demand. As one industry overview frames it, pelletizers are the machines that turn waste plastics into the feedstock for bottles, コンテナ, パイプ, および自動車部品 (トップ 10 plastic pelletizer Factory in the world, 2024). 米国の購入者向け, the practical implication is that abundant supply rewards disciplined vetting: the framework, checklist, and total-cost lens above are what separate a durable sourcing decision from a low-price gamble. For further technical grounding, I point teams to overviews of plastic pellet making machines for PP, LDPE, and HDPE recycling and to available used compounding and pelletizing equipment listings to benchmark specifications against real market inventory.
How does a plastic pelletizing process work end to end
When I walk a buyer through a pelletizing line for the first time, I describe it as a controlled sequence of five stages, each of which determines a piece of your final pellet quality. A plastic pellet making machine does not simply “chop plastic.” It melts, homogenizes, 形, cools, and dices a polymer stream into uniform granules that a downstream processor can meter reliably. Understanding that chain end to end is what lets you match a machine to a resin and a target output instead of buying on price alone.
The five core stages
実際に, the flow I audit on the factory floor looks like this:
- Feeding and dosing. リグラインド, virgin resin, or masterbatch enters the throat, often through a force feeder or gravimetric dosing unit. Consistent feed is the first defense against pellet size variation.
- Melt extrusion. The extruder screw configuration conveys, 圧縮する, せん断熱とバレル熱によって材料を溶かします. 二軸押出機の噛み合うスクリューにより、コンパウンディングやマスターバッチ作業に必要な混合エネルギーが得られます。; 単軸押出機はよりシンプルで洗浄に適しています。, 均一なリサイクルの流れ.
- ろ過とダイ. スクリーンチェンジャーは、溶融物がダイプレートとカッターに到達する前に汚染物質を除去します。. ダイ穴の形状によりストランドの直径と, 結局のところ, ペレット寸法.
- 冷却. 方法によっては, ポリマーは冷却水浴で冷却されます, 水の指輪, またはウォーターボックス. 冷却速度は結晶化度とペレットのきれいな切断に影響します。.
- 切断と乾燥. 回転ナイフでストランドまたはダイ面を細切りしてペレットにします, その後脱水される, 乾燥した, そして分類された. ペレットサイズの均一性はここで測定されます.
主な考慮事項
樹脂は上流のほぼすべてを決定します. Plastic pellet making machines are commonly designed to extrude, いいね, そしてサイコロPP, HDPE, LDPE, およびLLDPEリサイクルの流れ (PP、LDPE、HDPEリサイクル用プラスチックペレット製造機, 2024), and each of those behaves differently at the die. LDPE and LLDPE tend to be tacky and reward gentler cooling; HDPE and PP cut cleanly once crystallized; PET and PVC bring moisture sensitivity and thermal-stability constraints that push you toward specific screw and drying setups. I ask suppliers to state the target throughput per resin, not a single headline number, because production line capacity for a soft LDPE stream rarely matches the same machine’s rated output on rigid HDPE.
実践的なヒント
Ask the factory to run your actual material, not a house resin, during the factory acceptance test. Confirm melt-pressure stability, watch for die-hole freeze-off, and pull a pellet sample for sieve analysis. 私の経験では, a consistent melt-extrusion profile at the die is the single best predictor of whether a line will hold spec once it ships and gets installed under a US buyer’s utilities and ambient conditions.
業界の背景
The reason this end-to-end view matters commercially is that pelletizers turn waste plastics into small, ボトルの製造に使用される均一なペレット, コンテナ, パイプ, および自動車部品 (トップ 10 plastic pelletizer Factory, ケハオプラスチック機械, 2024). Your customer’s part quality traces directly back to how well each of these five stages was tuned at the factory before the machine ever left the floor.
Difference between a plastic pelletizer and a plastic extruder
Buyers frequently use “押出機” そして “ペレタイザー” interchangeably in RFQs, and that ambiguity causes scope problems during quoting. I keep the distinction simple: the extruder makes the melt, and the pelletizer turns that melt into finished granules. In most compounding and recycling installations you are actually buying a pelletizing line where the extruder is one subsystem feeding the pelletizer.
Where the roles diverge
A plastic extrusion machine is the melting and conveying engine. A twin screw extruder factory typically designs, エンジニア, 組み立てる, プラスチックの配合に使用される押出システムをテストします, 食べ物, 製薬, および化学産業 (二軸押出機工場とは – B2B ガイド, 2024). The extruder can terminate in many ways: a sheet die, a pipe die, a profile die, or a pelletizing die. The pelletizer is specifically the cooling-and-cutting section that produces recycled plastic pellets or compounded granules. So a plastic granulator or granules making machine is a downstream device, while an extruder is a platform that may or may not feed one.
主な考慮事項
Confirm exactly what is inside the price. When I see a listing such as a PP/PE pelletizer masterbatch twin screw machine at roughly US $42,000 1個あたり (中国製.com, 2024), I ask whether that figure covers only the extruder, or the full line including die plate and cutter, 冷却水浴, ドライヤー, および制御盤. Scope, not sticker, drives your total cost.
| 属性 | Plastic extruder | Plastic pelletizer |
|---|---|---|
| Primary function | Melt, ミックス, and convey polymer | Cool and cut melt into uniform pellets |
| Core components | スクリュー(s), バレル, ヒーター, drive, feeder | 冷却システム, ダイプレートとカッター, ナイフ, ドライヤー |
| 出力 | Homogenized melt stream | Finished granules / recycled plastic pellets |
| Typical variants | Twin screw, single screw, two-stage extruder | ストランド, 水中, 水リング, die face |
| Bought standalone? | Often, for sheet/pipe/profile lines | Usually as part of a pelletizing line |
実践的なヒント
Write your RFQ around the finished pellet, not the machine label. Specify resin, throughput in kg/h, target pellet dimension, and required pellet size uniformity, then let the supplier propose the extruder-plus-pelletizer combination. This avoids the common trap of receiving a competitively priced extruder that quietly excludes the pelletizing back end.
業界の背景
Chinese suppliers commonly present both together, offering broad extruder and pelletizer product lines including twin, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー (中国実験室二軸押出機工場カタログ, 2024). That bundling is convenient, but it makes disciplined scope definition more important, not less.
Types of plastic pelletizers (ストランド, 水中, 水リング, die face)
Choosing the pelletizer type is one of the highest-leverage decisions in a sourcing project. The right choice significantly affects facility output, 製品の品質, 収益性 (アーリントンマシナリー, Used Compounding and Pelletizing Equipment, 2024). Below is how I frame the four mainstream methods for US buyers, along with where each earns its keep. Water ring and water strand pelletizing are both standard offered methods for plastic granulation (プラスチックペレット化機, yjプラスチック押出機.com, 2024), so most factories can quote more than one — which means you should specify the one you actually want. Twin Screw Extruder Barrel
ストランドペレタイザー
The melt exits the die as continuous strands, passes through a cooling water bath, is dewatered, then fed into a cutting chamber. It is mechanically straightforward, forgiving to maintain, and produces excellent pellet size uniformity for a wide range of PP, PE, およびエンジニアリング樹脂. I recommend it as the default for compounding and general recycling where operators can thread strands and manage a water bath.
水中ペレタイザー
Cutting happens directly at the die face while submerged, with pellets carried away by a water stream and dried. Underwater pelletizers deliver dust-free, near-spherical pellets at high throughput and are the go-to for large-volume PE and PET recycling extruder lines. The tradeoff is higher capital cost and more sensitive die and knife maintenance, so I only steer buyers here when volume justifies the complexity.
Water ring pelletizer
Also a die-face method, but pellets are thrown into a rotating ring of water on the cutting chamber wall rather than a full underwater flow. It sits between strand and underwater systems in cost and complexity, and handles many polyolefins and masterbatch extruder applications well. It is a practical middle option when you want die-face cutting without full underwater system overhead.
Die face (hot face) ペレタイザー
Cutting occurs at the die face with air cooling or minimal water, which suits highly filled compounds and some adhesives that do not tolerate a long water contact. Pellet shape can be less uniform than strand cutting, so I match it to applications where the material chemistry, not appearance, drives the decision.
主な考慮事項
Map type to resin and volume before you compare prices. Underwater and water ring systems reward high, steady throughput; strand systems reward flexibility and easy changeover across recycled plastic pellets of varying quality. For moisture-sensitive PET or heat-sensitive PVC, the cooling and drying subsystem deserves as much scrutiny as the cutter itself.
実践的なヒント
Because factories can quote several methods, I require each proposal to state the pelletizer type explicitly and to include a pellet sample from that exact configuration. I also check the secondary market before committing: 以上 74,000 卸売中古二軸押出機製品がリストされています, indicating an active resale market (中国製.com, 2024), which gives you both a price benchmark and an exit option if your product mix changes.
業界の背景
Pricing varies widely with type and application, which is why I map price to specification rather than trusting a single list figure. For reference points across polymer compounding equipment, conical twin screw extruders for PVC pipe are listed at roughly US $25,000 セットあたり, twin screw extruders for pet food run between US $25,000 そして $80,000 セットあたり, and a PP/PE masterbatch machine appears near US $42,000 1個あたり (中国製.com, 2024). Supply is also concentrated: one directory lists 1,569 twin screw extruder products with sourcing centered in Shandong, 浙江省, と江蘇省 (HiSupplier.com, 2024), so comparing several regional factories on the same pelletizer type is realistic. For deeper method-by-method detail, I point buyers to a supplier reference such as the plastic pelletizing machine overview そして used compounding and pelletizing equipment listings to calibrate expectations before requesting quotes.
Bringing Your Sourcing Strategy Together
Choosing a plastic pelletizer factory is less about finding the lowest sticker price and more about matching machine architecture to your material stream, throughput targets, and long-term service needs. Throughout this guide I have argued that the right partner depends on what you actually run: a twin screw extruder for demanding masterbatch and compounding work, a single screw extruder for straightforward recycling of PP and PE, and a pelletizing method (水中ペレタイザー, ストランドペレタイザー, or water ring pelletizer) chosen for the pellet size uniformity your downstream process requires. Water ring and water strand pelletizing remain the two standard granulation methods offered across the market (プラスチックペレット化機, 2024, yjプラスチック押出機.com), and the difference between them shows up directly in your finished pellet quality.
In my experience the buyers who avoid costly mistakes treat the purchase as a total cost of ownership decision rather than a single transaction. A conical twin screw line for PVC pipe near US $25,000 per set and a pet food twin screw system priced between US $25,000 そして $80,000 per set illustrate how widely quotes swing with specification (中国製.com, 2024, made-in-china.com). The number that matters is the loaded cost: 保存されました, service response, downtime risk, and the years of production line capacity you expect to run. Verify a factory rather than a trading company, confirm certifications such as CE, ISO 9001, およびUL (Made-in-China.com certification filters, 2024), and map US import factors like tariffs and Incoterms into your landed cost before you sign anything.
Whether you buy new or explore the active secondary market of over 74,000 wholesale used extruder listings (中国製.com, 2024), the same discipline applies. Get your material specification, スループット, and pellet geometry documented first, then let those requirements drive the conversation with any Plastic Pelletizer Factory supplier or manufacturer you evaluate.
専門家の洞察
| キーポイント | 説明 |
|---|---|
| Match the machine to the material, not the brochure | Twin screw extruders suit compounding and masterbatch work, while single screw extruders handle basic PP, PE, HDPE, and LDPE recycling. Pelletizer type (水中, ストランド, or water ring) drives pellet size uniformity, so specify your polymer and output before comparing quotes. |
| Price only means something against specification | Listings range from roughly US $25,000 for a conical twin screw PVC line to US $80,000 for pet food systems (中国製.com, 2024). A static list price tells you little; ask suppliers to map cost to screw configuration, 容量, and pelletizing method. |
| Verify the factory, then verify the total cost | Confirm you are dealing with a manufacturer rather than a reseller, check CE, ISO 9001, およびUL認証 (中国製.com, 2024), and factor spares, サービス, 関税, and Incoterms into landed cost and ROI. |
B2B バイヤー向けの実用的な調達のヒント
- Write your specification first: define resin type (HDPE, LDPE, LLDPE, ペット, PVC, or masterbatch), target throughput, and required pellet geometry before requesting quotes, so every vendor prices the same scope.
- Confirm you are buying from a factory, not a trading company, by asking to see the production floor, die plate and cutter tooling, and in-house extruder assembly and testing capability.
- Request certification documentation up front. CE, ISO 9001, and UL are common baselines (中国製.com, 2024), and GMP or SA8000 matter if you serve food or pharma streams.
- Build a landed-cost model that includes tariffs, インコタームズ, 海上貨物, そしてインストール, rather than comparing ex-works prices alone.
- 総所有コストを評価する: スペアパーツの入手可能性, screw and die replacement intervals, service response time, and expected downtime over the machine’s life.
- Consider the used market as a benchmark. 以上で 74,000 wholesale used extruder listings available (中国製.com, 2024), refurbished lines can validate fair pricing even if you ultimately buy new.
よくある質問
Where can I find plastic pelletizer machines for sale, and what does the pelletizing process actually involve?
When buyers ask me where to source a plastic pellet making machine, I point them to three distinct channels: direct-from-factory purchasing, established trading companies, and B2B marketplaces such as Made-in-China.com, which currently lists over 74,000 wholesale used twin screw extruder products alone (中国製.com, 2024). The pelletizing process itself is straightforward to describe but demanding to execute well. A plastic extrusion machine melts your feedstock through a heated barrel, forces the melt extrusion through a die plate, cools the output in a water bath or air stream, then dices it into uniform granules. Water ring and water strand pelletizing are the two standard methods offered for plastic granulation (yjプラスチック押出機.com, 2024). The channel you choose matters: a factory gives you control over screw configuration and after-sales service, while a marketplace gives you speed and price comparison at the cost of direct accountability.
What is a realistic plastic pelletizing machine price for my capacity?
I always steer buyers away from static price lists toward price-to-specification mapping, because a headline number tells you almost nothing. As a reference range: a PP/PE masterbatch twin screw machine is listed around US $42,000 1個あたり, conical twin screw extruders for PVC pipe run near US $25,000 セットあたり, and application-specific twin screw lines for pet food fall between US $25,000 そして $80,000 セットあたり (中国製.com, 2024). Your actual Plastic Pelletizer Factory price depends on throughput, screw type, intermeshing screw design, 自動化レベル, and cooling configuration. 私の経験では, the machine is only the visible portion of total cost of ownership. Factor in spare die plates and cutters, screw wear parts, service response time, and downtime risk, and budget for those from day one rather than discovering them in year two.
Is a DIY plastic pelletizer a viable option for a business?
For hobbyists processing a few kilograms, a DIY plastic pelletizer can work. For any commercial operation, I advise against it. Homemade granules making machines rarely achieve the pellet size uniformity that downstream molders and compounders require, and inconsistent pellets translate directly into rejected batches and lost customers. A proper plastic pellet making machine is engineered for extruding, 冷却, ダイシングPP, HDPE, LDPE, and LLDPE recycling streams at stable output (リサイクルプラント.com, 2024). The gap between a workshop build and a production-grade pelletizing line is not just capacity; it is repeatability, safety compliance, and the ability to hold spec across shifts. If margins matter, buy purpose-built equipment.
What is the difference between a strand pelletizer, an underwater pelletizer, and a water ring pelletizer?
These three approaches define most of the market. A strand pelletizer (also called a plastic strand pelletizer) pulls cooled strands from the die through a water bath and feeds them into a rotating cutter, which gives you excellent size uniformity and easy inspection. An underwater pelletizer cuts the melt directly at the die face beneath circulating water, which suits high volumes and heat-sensitive polymers. A water ring pelletizer sits between the two, cutting at the die face with a water curtain for cooling. China-based factories commonly offer twin, トリプル, 二段式, and single screw machines plus underwater pelletizers within a single catalog (zextrusion.com, 2024). Choosing the right type significantly affects facility output, 製品の品質, 収益性 (アーリントンマシナリー, 2024), so I match the pelletizer to the polymer and volume, not to whichever unit is cheapest.
Can I use a wood pelletizer machine for plastic, and where does MAAG fit in?
いいえ. A wood pelletizer machine uses a die-and-roller press to compress dry biomass, a fundamentally different mechanism from the melt-and-cut process plastics require. If your feedstock is polymer, you need a plastic-specific pelletizing line, full stop. On the premium end, MAAG is a well-known name in high-performance pelletizing and melt-processing systems, frequently cited as a quality benchmark for demanding applications like PET recycling extruders and masterbatch extruders. I mention MAAG to clients as a reference point for what top-tier engineering looks like, then we decide whether their throughput and quality tolerances justify that tier or whether a well-vetted mid-market factory delivers sufficient value.
How do I choose a reliable plastic pelletizer supplier?
This is the question that protects your capital, so I use a structured vetting framework rather than gut feel. 初め, confirm you are dealing with an actual manufacturer, not a trading company relabeling someone else’s equipment; a genuine Plastic Pelletizer Factory designs, エンジニア, 組み立てる, and tests its extrusion systems in-house (exintellmach.com, 2024). 2番, 認証を確認する: 一般的で意味のあるものには CE が含まれます, ISO 9001, UL, GMP, and SA8000 (中国製.com, 2024). 三番目, 地理的な集中と実績を確認する; 供給は山東省に集中している, 浙江省, と江蘇省, HiSupplier リストのようなディレクトリを使用 1,569 二軸押出機製品 (HiSupplier.com, 2024). 私の監査チェックリストには、ライブ工場ツアーまたはビデオウォークスルーが含まれています, ポリマーの立会い実行テスト, スペアパーツの入手可能性を文書化する, お住まいの地域の顧客を紹介する, インコタームズをクリア. 私が目にする最も一般的な間違いは、実行テストをスキップし、パンフレットの仕様を信頼することです。.
海外でペレタイザーを調達する場合のコストと品質のトレードオフは何ですか??
海外調達, 特に中国からの, 設備コストを大幅に削減できる, しかし、トレードオフは現実のものであり、明確に名前を付ける価値があります. 単価が低いとリードタイムが長くなることが多い, サプライヤー間でのビルド品質のばらつき, and slower parts logistics that can turn a two-day repair into a two-week shutdown. 私の経験では, the buyers who win offshore are the ones who invest upfront in verification: they pay for third-party inspection, insist on a witnessed acceptance test, and negotiate a stocked spares package as part of the contract. The buyers who lose are the ones optimizing purely for the lowest quote. Treat the price gap as a budget for risk mitigation, not pure savings, and the overseas route becomes a sound strategy rather than a gamble.
What US import factors should I plan for before buying?
米国の購入者向け, landed cost is where sourcing plans succeed or fail, and it is a gap most competitor guides ignore entirely. Before I approve a purchase, I confirm the Incoterms explicitly, because the difference between EXW, FOB, and DDP shifts thousands of dollars and significant liability onto or off your books. I check the current tariff classification for the machinery under the relevant HTS code, since duty rates on industrial extrusion equipment change and directly affect ROI. Then I plan logistics: ocean freight timing, port handling, inland delivery, and rigging for what is often a multi-ton pelletizing line. Building these into your total cost of ownership model, alongside the machine price and spares, gives you an honest breakeven timeline instead of a pleasant purchase price followed by unpleasant surprises.
参考文献
- A twin screw extruder factory designs, エンジニア, 組み立てる, プラスチックの配合に使用される押出システムをテストします, 食べ物, 製薬, および化学産業 — 二軸押出機工場とは – B2B ガイド (2024)
- China-based factories offer broad extruder and pelletizer product lines including twin, トリプル, 二段式, 単軸スクリュー機械と水中ペレタイザー — 中国実験室二軸押出機工場カタログ (2024)
- A PP/PE pelletizer masterbatch twin screw machine is listed at US $42,000 1個あたり — Made-in-China.com wholesale used twin screw extruder listings (2024)
- Twin screw extruders for pet food production are listed between US $25,000 そして $80,000 セットあたり — Made-in-China.com wholesale used twin screw extruder listings (2024)
- 以上 74,000 wholesale used twin screw extruder products are available, indicating an active secondary market — Made-in-China.com used equipment marketplace (2024)
- こんにちはサプライヤーリスト 1,569 二軸押出機製品, 供給が山東省に集中している, 浙江省, と江蘇省 — HiSupplier.com twin screw extruder directory (2024)
- Common factory certifications include CE, ISO 9001, UL, GMP, and SA8000 — Made-in-China.com certification filters (2024)
- Plastic pellet making machines are designed for extruding, 冷却, ダイシングPP, HDPE, LDPE, およびLLDPEリサイクルの流れ — PP、LDPE、HDPEリサイクル用プラスチックペレット製造機 (2024)
- Water ring and water strand pelletizing are standard offered methods for plastic granulation — プラスチックペレット化機 (2024)
- 適切なペレタイザー タイプの選択は、施設の生産量に大きく影響します。, 製品の品質, 収益性, and used inventory is available — 販売のための中古配合およびペレット化装置 (2024)