

フィラーマスターバッチ押出機: グローバル製造業者向けの決定版 B2B 取引ガイド, サプライヤー, とバイヤー
フィラーマスターバッチ押出機市場は、大きな変革を経験しています。, コスト効率の高いプラスチック配合ソリューションに対する需要の高まりが原動力, 米国とEU全体で環境規制が強化されている, 循環経済に基づく製造業への世界的な推進. あなたが フィラーマスターバッチ押出機メーカー 大西洋横断市場への拡大を目指す, ある フィラーマスターバッチ押出機サプライヤー 信頼できる卸売パートナーシップを求めています, または信頼できる企業からの新しい資本設備を評価するプラスチック加工業者 フィラーマスターバッチ押出機工場, この包括的なガイドは、ポリシーのコンテキストを提供します, 市場データ, 実践的なケーススタディ, 情報に基づいて B2B 調達の意思決定を行うために必要な将来の予測. 以降のセクションでは、, 貿易動向を調査します, 二軸同時回転配合押出機の競争環境を分析する, 国境を越えた調達のための実行可能な戦略の概要を説明します — すべては権威ある機関からの検証可能なデータに基づいています.
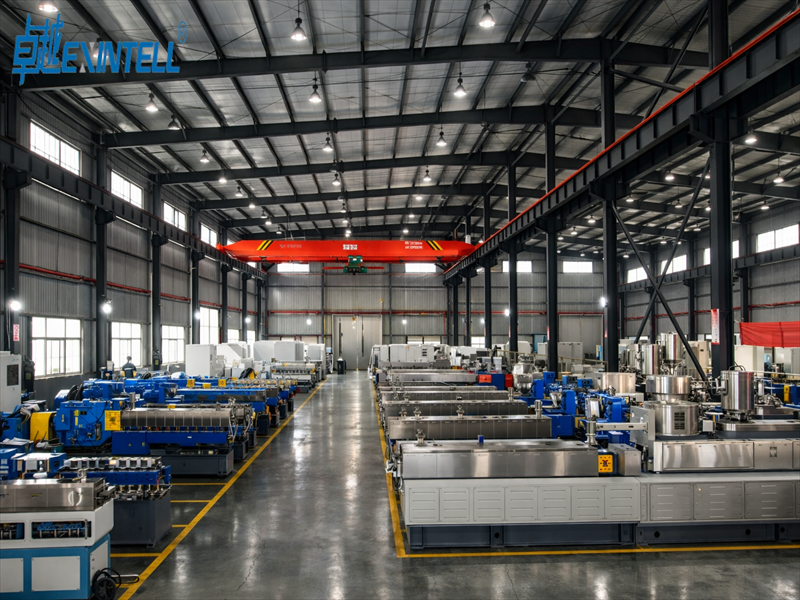
フィラーマスターバッチ押出機の生産環境を代表する重機を備えた工業用製造施設
外国貿易政策の展望と産業機械への影響
米国と欧州連合の貿易関係は依然として世界最大の二国間商業パートナーシップである. によると、 国際貿易局 (ITA), 物品貿易総額が米ドルを超えた 880 億で 2024, 産業機械と一緒に — フィラーマスターバッチ押出機などのプラスチック加工装置を含む — 両方向の資本財の流れのかなりの部分を占める.
前半のいくつかの政策展開は、どのような方法で再形成されつつあるのか フィラーマスターバッチ押出機卸売 取引は大西洋を越えて構造化されている:
米国通商法の枠組みに基づく関税調整. 特定のセクションの終了後 232 後半の関税免除 2024, 米国商務省は輸入産業機械の関税スケジュールを見直している. HTS に分類される EU 原産の押出機用 8477 (ゴムやプラスチックを加工するための機械), 実効デューティ比は次の間で変動しました。 0% そして 3.4%, 特定の小見出しと組み立て国に応じて. の 米国国際貿易委員会 (USITC) 調和関税率データベースは、引き続き現在の料金の信頼できる参照となります。.
EU 炭素国境調整メカニズム (CBAM) 遷移. CBAM は主に鉄鋼を対象としていますが、, アルミニウム, セメント, 肥料, 電気, そして水素, その広範なシグナル伝達効果により、EU を拠点とするプラスチック配合会社はエネルギー効率の高い押出装置を要求しています。. これにより、高効率フィラーマスターバッチ押出機モデルのプルファクターが生み出されます。 — 特に文書化されたキログラムあたりのエネルギー指標を持つもの — 世界中のメーカーから. の European Commission's CBAM portal 最新の実装タイムラインを提供します.
EU の包装および包装廃棄物に関する規制 (PPWR). 後期に採用された 2024, PPWR は、EU 単一市場で販売されるプラスチック包装にリサイクル含有量の最低基準を義務付けています. による 2030, 接触に弱いプラスチック包装には、少なくとも次のものを含める必要があります。 10% 使用済みリサイクル (PCR) コンテンツ, に上昇する 50% による 2040. この規制は、リサイクル炭酸カルシウムを組み込んだフィラーマスターバッチ配合物の需要を直接的に増加させます。 (CaCO3) およびその他のミネラルフィラー, これにより、さまざまな品質の原料を処理できる先進的な押出ラインへの設備投資が促進されます。. からのデータ the European Parliament's legislative observatory confirms the regulation's phased timeline.
米国インフレ抑制法 (アイラ) 国内製造奨励金. While the IRA's most publicized provisions target clean energy, 先進製造業の税額控除 (セクション 45X) 国内コンテンツのボーナス規定により、米国に本拠を置くプラスチック加工業者は新しい配合ラインへの投資を奨励しています。. クリーンエネルギーのサプライチェーンで使用されるコンポーネントの国内生産をサポートする設備の購入 — バッテリーハウジングやソーラーパネルフレーム用の充填ポリプロピレン化合物など — 加速償却または直接税額控除の対象となる可能性があります. の 米国エネルギー省 資格を得る活動に関するガイダンスを維持する.
一緒に, これらの政策ベクトルは、フィラーマスターバッチ押出機の国境を越えたB2B取引に有利な環境を生み出します。. CE認証を取得したEUメーカー, エネルギー効率の高いラインは、IRAと提携した機器を求める米国の調合業者の間で好意的な買い手を見つける. 逆に, コスト競争力のあるアジア製機械 — 多くの場合、フィラー マスターバッチ押出機工場の直接チャネルを通じて販売されます。 — コンプライアンス文書に対する厳しい監視に直面している, エネルギー定格, 両市場におけるアフターサービスインフラストラクチャ.
フィラーマスターバッチ押出機について理解する: 技術と応用
フィラー マスターバッチ押出機は、高濃度のミネラルフィラー マスターバッチ ペレットを製造するために設計された特殊な配合システムです。 — 通常は炭酸カルシウムをベースとする (CaCO3), 硫酸バリウム (BaSO4), またはポリオレフィンキャリア樹脂に分散されたタルク (HDPE, LDPE, またはPP). これらのマスターバッチペレットは、その後、下流のフィルムブロー中にバージンポリマーまたはリサイクルポリマーに降ろされます。, 射出成形, またはパイプ押出プロセス, 原材料コストを15削減–40% 剛性などの機械的特性を変更しながら, 不透明度, 寸法安定性.
コア マシン アーキテクチャには通常、次のものが含まれます。:
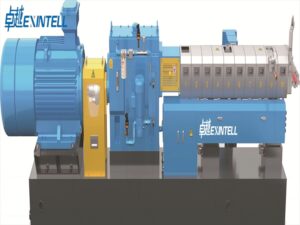
共回転二軸押出機. 現代のフィラーマスターバッチ生産の主力製品. ネジ径の範囲は次のとおりです。 52 mm (実験室/パイロットスケール) に 175 mm (大量生産), L/D比が 36:1 そして 52:1. スループット容量の範囲は次のとおりです。 200 kg/h以上 2,000 kg/h(構成に応じて). Leading filler masterbatch extrusion machine manufacturers differentiate on screw-element metallurgy (窒化鋼, powder-metallurgy tool steel, or tungsten-carbide-coated elements), barrel cooling efficiency, and gearbox torque density.
Volumetric or gravimetric feeding systems. Accurate dosing of CaCO3 powder (often at 70–85% loading by weight) alongside carrier resin and processing aids (ステアリン酸, paraffin PolystyrèNe Extrude wax, or coupling agents) is critical to masterbatch quality consistency. Loss-in-weight feeders with twin-screw metering are the industry standard for premium lines.
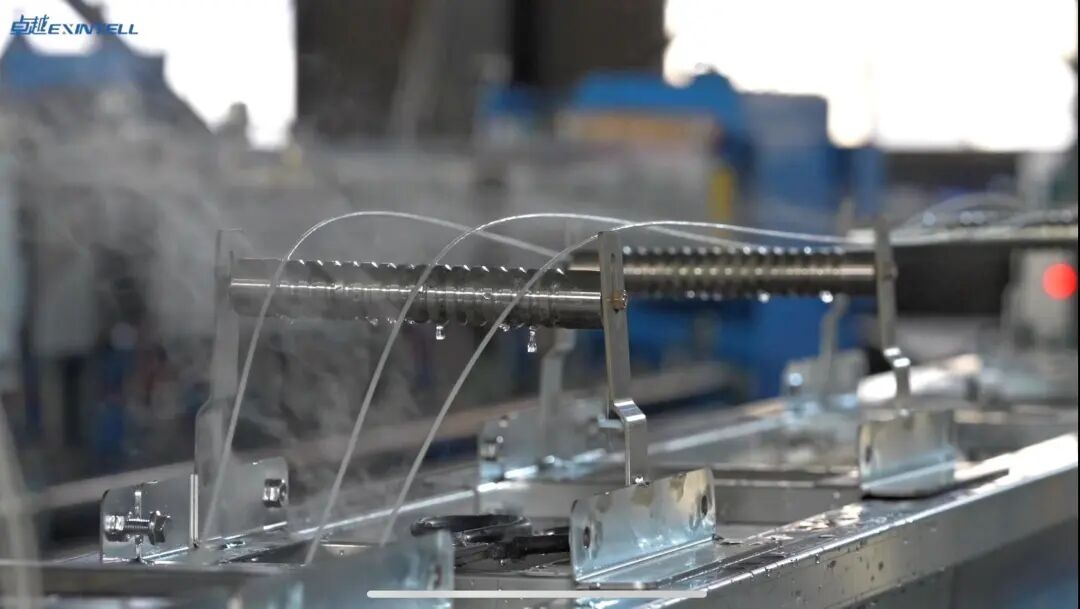
ストランドペレット化または水中ペレット化システム. ストランドペレット化 (water-bath cooling followed by rotary-knife cutting) remains dominant for CaCO3 masterbatch due to lower capital cost and simpler maintenance. Underwater pelletizing is gaining share for high-output lines (>1,500 kg/h) ペレット形状の均一性と発塵の低減により投資が正当化される場合.
フィラーマスターバッチに使用される二軸押出機技術を代表する産業用押出機械コンポーネントの拡大図
フィラーマスターバッチ押出機の世界市場規模とB2B取引機会
世界のフィラーマスターバッチ市場の価値は約米ドル 4.8 億で 2024, からまとめられた推定によると グランドビューリサーチ そして モルドール・インテリジェンス 業界レポート. 市場は CAGR 5.2 で成長すると予測されています–6.1% を通して 2030, パッケージングによって推進される, 工事, 自動車, および農業最終用途部門. この下流の需要は、フィラーマスターバッチ押出機のサプライヤーおよび OEM にとって資本設備の機会に直接変換されます。.
地域別需要の内訳 (2024– 見積もり):
アジア太平洋地域が大まかに占める 55% 世界のフィラーマスターバッチ消費量の割合, 中国と, インド, ベトナム, とインドネシアが主要な生産拠点として. しかし, 米国と EU は合わせて約 28% 消費の — そして批判的に, プレミアム装備の調達に占める割合が不釣り合いに高い, より厳格な品質を考慮して, 安全性, 欧米市場におけるエネルギー効率の要件.
米国では, プラスチック配合装置市場 (フィラーマスターバッチラインを含む) 米ドルで見積もられました 1.1 億で 2024 によって プラスチック工業協会 (プラスチック). 老朽化した単軸スクリューラインの交換サイクル, IRA に基づくリショアリングインセンティブと組み合わせる, 米国南東部とメキシコ湾岸地域の中規模調合業者の間で設備投資承認の波を起こしている.
欧州連合では, の プラスチックヨーロッパ 2024 年次報告書には、欧州のプラスチックコンバーターがユーロを投資したことが記載されている 8.2 2023 年に機械および設備が 10 億ドルに達する–2024, 推定12の配合およびマスターバッチ生産ラインを備えています。–15% その合計のうち. ドイツ, イタリア, 七面鳥 (EU隣接市場として), ポーランドとポーランドは、より広範な欧州貿易圏内で最大の機器輸入国である.
フィラーマスターバッチ押出機の B2B 取引フロー パターン:
主要な貿易の流れは中国の製造元からのものです (南京, 張家港市, と広州クラスター), ドイツ (シュトゥットガルトとハノーバー地域), イタリア (ブレシアとミラノ), 日本から世界中のエンドユーザー市場へ. 中国のフィラーマスターバッチ押出機工場の運営は、過去 10 年間で 40–60% ヨーロッパの同等品と比べてコスト面で有利, ビルド品質の差を徐々に縮めながら, 自動化の統合, および CE/UL 準拠文書. プラスチック押出製品
米国および EU の B2B バイヤー向け, 調達の決定はますます総所有コストに依存するようになる (TCO) 購入価格だけではなく. 生産量1kgあたりのエネルギー消費量などの要素, スペアパーツの入手可能性, リモート診断機能, 調達評価では、地域のサービス エンジニア ネットワークが重視されます。 — 特に運行が予想される路線については 7,000+ 年間数時間.
プラスチックシート押出工場 産業機械の B2B 越境貿易物流を代表する主要国際港の国際輸送コンテナ アルミ押出形マルチトラック
フィラーマスターバッチ装置市場でB2Bの買い手と売り手が直面する課題
中国アスファルト混合装置 良好なマクロ環境にもかかわらず, いくつかの課題 ベント付き単軸押出機 フィラーマスターバッチ押出機の国境を越えたB2B取引が複雑になる:
コンプライアンスと認証の複雑さ. EU 市場をターゲットとするフィラー マスターバッチ押出機メーカーは、EU 機械指令への完全な準拠を保証する必要があります。 (2006/42/EC, 新しい機械規則への移行 2023/1230 1月発効 2027), CEマーキング要件, そして — 電気部品用 — 低電圧指令およびEMC指令. 米国市場向け, OSHA 機械保護基準 (29 CFR 1910 サブパートO), NEC/NFPA 79 電気規格, および制御パネルの UL リストはベースライン要件です. 二重市場コンプライアンスの対応により 8 が追加–15% 両方の地域にまだサービスを提供していないメーカーのエンジニアリングおよび文書化のコストがかかります。.
物流とリードタイムの変動性. アジアの海上運賃–北米とアジア–ヨーロッパ路線, 2021年からはダウン–2022 ピーク, 引き続き混乱の影響を受ける. 晩年に始まった紅海/スエズ運河ルートの課題 2023 アジアに影響を与え続けた–ヨーロッパの乗り継ぎ時間は早朝まで, 10を足す–14 喜望峰経由で輸送が変更されるまで数日. 押出ラインなどの重資本設備用 (通常の配送重量: 15–45 完全なラインあたりのメートルトン), これらの遅延は、プロジェクトのタイムラインのリスクと倉庫保管コストの増加につながります。. からのデータ フレイトス・バルティック指数 (FBX) リアルタイムのコンテナレートベンチマークを追跡します.
アフターサービスインフラ. 米国とEUのB2Bバイヤーは、スペアパーツの納期に関する契約上の保証をますます要求しています。 (通常48–72 重要なコンポーネントに数時間), オンサイト試運転サポート, IoT対応マシンモニタリングによるリモートトラブルシューティング. 北米または西ヨーロッパにサービスハブを確立していないフィラーマスターバッチ押出機のサプライヤーは、競争上不利な状況に直面しています, たとえより低いFOB価格を提供する場合でも.
プラスチック押出サプライヤー メーカー 通貨と支払期間のリスク. EUR/USD の為替レートは 1.03 の範囲内で変動します。–1.12 過去を超えたバンド 12 月, 資本設備の一般的な支払い条件は 30 年に及びます–180 日 (LC 裏付け取引の場合はそれ以上), 買い手と売り手の両方が重大な為替エクスポージャに直面する. 確認済み信用状などの貿易金融商品, 銀行保証, および輸出信用機関 (ECA) 裏付けのある融資 — などの機関を通じて入手可能 米国輸出入銀行 または アリアンツトレード (以前はオイラーヘルメス) — このリスクは軽減しますが、排除するものではありません.
B2B の外国貿易を可能にする地理的および政策的利点
大西洋横断回廊は、産業機械の B2B 貿易に利益をもたらす構造上の利点を提供します, フィラーマスターバッチ押出機を含む:
港湾インフラストラクチャとマルチモーダル接続. 米国東海岸の港、ニューヨーク/ニュージャージー, サバンナ, そしてチャールストン — ヒューストンのようなメキシコ湾岸の港と一緒に — ロッテルダムを含むEUの主要港への直接定期船サービスの接続を提供します, ハンブルク, アントワープ-ブルージュ, そしてジェノバ. 通過時間10–16 日 (東海岸) そして25–35 日 (大西洋横断ルートによるメキシコ湾岸) 重機出荷の予測可能なサプライチェーン計画を可能にする. の ロッテルダム港管理局 産業機械および装置はおよそ 8% ブレークバルクおよびプロジェクト貨物のスループット.
相互認識と規制の調整. 米国とEUは別々の規制枠組みを維持しているが、, 数十年にわたる二国間技術対話 — などの団体によって促進されています。 米国国立標準技術研究所 (NIST) そして 欧州標準化委員会 (セン) — 電気安全などの分野で大幅な収束をもたらしました, 機械の警備, および圧力機器の規格. これにより、一方の市場ですでに認定されているフィラーマスターバッチ押出機工場が、他方の市場に参入する際の追加的なコンプライアンスの負担が軽減されます。.
貿易円滑化協定. 環大西洋貿易投資パートナーシップとはいえ、 (TTIP) 交渉は中断された, 既存のWTO約束, 貿易技術評議会 (TTC) フレームワーク, 二国間の税関協力協定により、産業機器の通関手続きがよりスムーズに促進され続けます。. The TTC's 2024 共同声明では、規制協力の優先分野として先端製造装置を特に強調した.
国際 B2B 貿易をサポートする貨物船と物流インフラのあるヨーロッパの主要港の航空写真
Practical Case Studies Enterprises Operating in the Filler Masterbatch Equipment Market
Examining real-world operational models provides actionable insights for businesses navigating this market:
ケーススタディ 1: Chinese manufacturer establishing EU distribution. A Nanjing-based filler masterbatch extrusion machine manufacturer with annual production capacity of 200+ complete lines recognized that direct-export sales to EU customers were limited by after-sales service concerns. で 2023, the company established a technical-service partnership with a German engineering firm based near Düsseldorf, creating a local spare-parts warehouse (stocking 500+ 摩耗部品のSKU, バレルセグメント, およびネジ要素) and deploying two full-time service engineers for the DACH region. 内で 18 月, EU sales grew from 8% に 22% 総収益の, with average selling prices 15% higher than comparable FOB-China transactions — 購入者がローカライズされたサポートにかける価値を反映. 同社はその後、このモデルを米国南東部でも複製しました。, シャーロットと提携, NCをベースとした産業機器サービスプロバイダー.
ケーススタディ 2: イタリアの OEM、米国市場参入に IRA インセンティブを活用. ブレシアに本拠を置く二軸押出機メーカー — 歴史的にはヨーロッパと中東の市場に焦点を当ててきました — identified an opportunity in the US market following the IRA's passage. 同社の押出ラインがクリーンエネルギー用途に使用されるバイオベースおよびリサイクル含有ポリマー化合物を処理できることを文書化することによって (具体的には, EVバッテリーモジュールハウジング用充填PPコンパウンド), 同社は、米国の顧客が第 45X 条の先進製造業税額控除の資格を得るのを支援しました。. この価値提案は — "buy our machine, あなたの生産物は連邦税額控除の対象となる可能性があります" — アジアの低価格代替品に対する競争入札で非常に効果的であることが証明された. 同社は次のように報告した。 340% 第 3 四半期間の米国の見積もりリクエストの増加 2023 そしてQ1.
ケーススタディ 3: US compounder's dual-sourcing strategy. ヒューストンに拠点を置く中規模のプラスチック配合業者, テキサス州, 3つのフィラーマスターバッチ生産ラインを稼働, はデュアルソーシング戦略を採用しました。 2024 容量拡張. 会社は高出力回線を 1 本購入しました (1,800 kg/h) 最も要求の厳しいアプリケーション向けにドイツの OEM から提供 (厳しい特性公差を必要とする自動車グレードの充填コンパウンド) と 2 本の標準ライン (800 各kg/h) 商品包装グレードのマスターバッチ用の中国のフィラーマスターバッチ押出機サプライヤーから. 総資本支出は約米ドルでした 2.8 百万 — だいたい 35% 全ヨーロッパの調達戦略よりもコストがかからない, 自動車認定生産に必要な品質レベルを維持しながら. The company negotiated identical 24-month warranty terms and 48-hour critical-spare delivery commitments from both suppliers.
Engineers reviewing industrial machinery specifications in a manufacturing facility representing B2B equipment procurement an
Selecting the Right Filler Masterbatch Extrusion Machine Supplier: A B2B Buyer's Framework
For procurement professionals evaluating filler masterbatch extrusion machine wholesale or single-unit purchases, a structured evaluation framework reduces risk and improves outcomes:
技術力評価. Request detailed screw-configuration proposals for your specific formulation (filler type, loading percentage, キャリア樹脂, and target throughput). A competent manufacturer will provide screw-element layout drawings, predicted specific energy consumption (kWh/kg), and melt-temperature profiles — not just generic brochure specifications. 同様の配合を行っている顧客に参考資料を求める.
工場監査と品質システムの検証. 米ドルを超えるご注文の場合 200,000, 現場での工場監査が標準的な慣行です. ISO を検証する 9001 認証 (最小), EU 向けマシンの場合, confirm that the manufacturer's quality system supports CE technical-file compilation. バレルの穴とネジ要素の加工公差を検査します — これらは分散品質と摩耗寿命に直接影響します。.
総所有コストのモデリング. を組み込んだ 5 年間の TCO モデルを構築する: 購入価格, 海上運賃と関税, 設置および試運転の費用, 年間エネルギー消費量 (地域の電気料金で), 計画的なメンテナンス費用 (スクリュー/バレルの交換間隔), 予定外のダウンタイムの見積もり (based on supplier's mean-time-between-failure data), およびスペアパーツの価格. というマシンが 30% FOBでは安いが消耗する 20% more energy and requires barrel replacement 40% more frequently may have a higher 5-year TCO.
Contractual protections. Ensure purchase contracts include: 性能保証 (スループット, specific energy, and product quality metrics tested during factory acceptance trials), liquidated damages for late delivery, warranty terms covering both parts and labor, and clearly defined Incoterms (CIF or DDP preferred for first-time cross-border purchases to simplify logistics risk allocation).
Sustainability and Energy Efficiency: The New Competitive Frontier for Filler Masterbatch Extrusion Machine Manufacturers
Scaffold Material Hand Signals Sustainability considerations are no longer peripheral to B2B purchasing decisions — they are increasingly central, particularly for buyers in the EU market where the EU Circular Economy Action Plan and corporate sustainability reporting directives (CSRD) create tangible compliance incentives.
Energy efficiency benchmarks. State-of-the-art co-rotating twin-screw filler masterbatch extrusion machines achieve specific energy consumption (SEC) of 0.10–0.16 kWh/kg for CaCO3 masterbatch at 70–80% フィラーローディング. This represents a 25–35% improvement over machines manufactured a decade ago, driven by advances in screw-element geometry (optimized distributive and dispersive mixing zones), high-efficiency direct-drive motors (IE4/IE5クラス), and intelligent process-control systems that minimize energy waste during transitions and startups. A filler masterbatch extrusion machine factory that can document SEC performance with third-party test data holds a significant competitive advantage.
Material-efficiency contributions. Filler masterbatch itself is inherently a sustainability-enabling product: by replacing 20–40% of virgin polymer with mineral filler, it reduces the carbon footprint of finished plastic products. の 欧州バイオプラスチック協会 and various LCA studies have documented that CaCO3-filled PE films can achieve 15–30% lower cradle-to-gate CO2 emissions compared to unfilled equivalents, depending on filler loading and sourcing geography. Extrusion machines capable of processing higher filler loadings (80–87%) without compromising pellet quality or downstream processability therefore deliver compounding environmental and economic benefits.
Circular-economy integration. Advanced filler masterbatch extrusion lines are increasingly designed to co-process post-consumer recycled (PCR) polyolefin flake alongside virgin carrier resin and mineral filler. This requires robust melt-filtration systems (continuous screen changers rated for contaminated feedstocks), enhanced degassing (multiple vacuum venting zones), and adaptive process-control algorithms that compensate for melt-viscosity variability inherent in PCR streams. Manufacturers offering these capabilities as standard or optional configurations are well-positioned for the EU market's recycled-content mandates.
Sustainable manufacturing concept with recycling symbols and green industrial processes representing energy-efficient extrusi
Workplace Safety in Plastics Manufacturing: Protecting Operators of Filler Masterbatch Extrusion Machines
Operating a filler masterbatch extrusion machine involves exposure to several occupational hazards that demand rigorous safety protocols and appropriate personal protective equipment (PPE). For B2B buyers and plant managers, understanding these safety dimensions is essential — both for regulatory compliance and for protecting the workforce that operates this capital equipment.
熱による危険性. Barrel temperatures on filler masterbatch extrusion lines typically range from 160°C to 240°C (320°F to 464°F), depending on carrier-resin type and filler loading. Contact burns represent a primary risk during maintenance, ダイチェンジ, および起動/停止手順. OSHA's general industry standards (29 CFR 1910.147 — lockout/tagout) Pelletizing Extruder Wholesale and the EU Machinery Directive's essential health and safety requirements mandate that machine designs incorporate thermal guarding, warning signage, and interlocked access panels. Operators must wear heat-resistant gloves (で 407 rated) and appropriate forearm protection during any task requiring proximity to heated surfaces.
Mechanical hazards and the critical role of safety footwear. Filler masterbatch production environments present significant foot-injury risks that are often underestimated. Heavy screw elements (individual elements can weigh 5–15 kg), バレルセグメント (50–200 kg), ダイプレート, and pelletizer components are routinely handled during assembly, メンテナンス, そして切り替え作業. A dropped screw element or coupling component can cause severe crush injuries to unprotected feet.
衝撃の危険を超えて, the production floor around filler masterbatch extrusion machines presents slip hazards (from process water, 潤滑剤, and spilled pellets/powder), puncture hazards (from metal fragments, fasteners, and cutting tools), and compression hazards (from heavy mobile equipment such as forklifts and pallet jacks used to transport raw materials and finished masterbatch). The fine CaCO3 dust that is inherent to filler masterbatch operations — even with dust-collection systems — creates slippery floor conditions that compound fall risk. Single Screw Pipe Extruders
Safety footwear standards and selection for extrusion-machine operators. Appropriate safety footwear is not optional — it is a regulatory requirement in both the US and EU for workers in plastics-manufacturing environments:
米国では, OSHA's PPE standard (29 CFR 1910.136) requires protective footwear for employees exposed to foot injuries from falling or rolling objects, 足裏を突き刺す物体, または電気的危険. Safety shoes and boots must meet ASTM F2413 パフォーマンス 単軸押出機サプライヤー 要件, which specify impact resistance (I/75 — withstanding 75 foot-pounds of impact energy), 圧縮抵抗 (C/75 — withstanding 2,500 pounds of compression force), 中足骨保護のためのオプションの評価も可能 (山), 耐パンク性 (PR), 電気的危険からの保護 (えー), と静電気の放散 (SD). 二軸押出機 メーカー メーカー
欧州連合では, 安全靴は以下に分類されます ISO で 20345 (安全靴), ISO で 20346 (保護靴), およびEN ISO 20347 (職業用靴). For filler masterbatch extrusion machine operators, ISO で 20345 S3 classification is the recommended minimum, 提供する: a 200-joule toe cap (鋼または複合材料), 耐貫通ミッドソール, closed heel region, 帯電防止特性, かかとのエネルギー吸収, and water-resistant upper. For environments with heavy liquid exposure (process-water systems, 冷却槽), S5-rated safety boots with full waterproofing are appropriate.
Why toe protection matters — the data. によると、 米国労働統計局 (BLS), 足の怪我は約6万件を占めている–70,000 米国では毎年発生する労働災害, with the manufacturing sector consistently ranking among the top three industries for foot-injury incidence. The BLS reports that roughly 75% of workers who suffered foot injuries were not wearing safety footwear at the time of the incident. EUでは, EU-OSHA data indicates that lower-extremity injuries represent approximately 12% 製造業における致命的ではないすべての職場災害の割合, with crush and impact injuries to toes and metatarsals being the most common mechanism.
For operators working around filler masterbatch extrusion machines specifically, the combination of heavy-component handling, hot-surface proximity, slippery floors (CaCO3 dust + 水), and forklift traffic creates a multi-hazard environment where composite-toe or steel-toe safety shoes with slip-resistant outsoles (SRC定格 — tested on both ceramic/water and steel/glycerol surfaces) provide essential protection. Modern composite-toe safety shoes offer the same 200-joule impact protection as steel-toe equivalents at 30–40% 体重が減る, reducing operator fatigue during 8–12 時間シフト — a meaningful ergonomic benefit in continuous-production environments.
Integrating safety footwear into B2B procurement specifications. Progressive filler masterbatch extrusion machine manufacturers and plant operators are increasingly specifying PPE requirements — 安全靴を含む — as part of their machine-commissioning and operator-training packages. When evaluating a filler masterbatch extrusion machine supplier, B2B buyers should confirm that the supplier's installation and training documentation includes a comprehensive risk assessment identifying foot-hazard zones around the equipment, recommended PPE specifications (including safety-footwear class), and operator-training materials covering safe work practices during routine operation, メンテナンス, and emergency procedures.
The business case for safety investment. 規制遵守を超えて, investing in appropriate safety footwear and comprehensive PPE programs delivers measurable ROI. の 国家安全評議会 (NSC) estimates that the average cost of a workplace foot injury in the US — 医療費も含めて, 生産性の低下, そして労働者' 補償 — 米ドルを超える 10,000 インシデントごとに. For a plastics-manufacturing facility operating multiple filler masterbatch extrusion lines with 20–50 生産労働者, even a modest reduction in foot-injury incidence translates into significant cost savings and reduced operational disruption. EU employers face similar cost structures, with the added regulatory risk of enforcement actions under national implementations of the EU Framework Directive on Safety and Health at Work (89/391/EEC).
職場を表す製造環境で保護靴などの安全装備を着用する産業労働者
見本市と業界イベントカレンダー: B2Bバイヤーとフィラーマスターバッチ押出機のサプライヤーが出会う場所
資本設備の購入には対面評価が引き続き重要です. 主な業界イベントには以下が含まれます:
K (デュッセルドルフ, ドイツ — 10月 ). The world's largest plastics and rubber trade fair, 3年ごとに開催. K は、世界的メーカーのフィラー マスターバッチ押出機技術を評価するための最高の会場です. 以上 3,000 出展者と 170,000+ 訪問者が予想されます. の
フィラーマスターバッチ押出機: 人間のための完全な B2B 取引ガイド… · フィラーマスターバッチ製造機: マニュファク向けの完全な B2B 取引ガイド… · カラーマスターバッチ押出機: グローバルB2B貿易分析, メーカー…