

Helstu veitingar
- Plastpressun bræðir hrá plastefni og myndar það í samfellt snið með föstum þversniði, sem gerir það að verkum að það hentar vel í langan tíma, framleiðslukeyrslur í miklu magni (SeaGate Plast, 2024).
- Þegar ég met framleiðanda plastprófíla, Ég skil sérsniðin útpressun, sem hefur í för með sér einskiptis teninga og verkfærafjárfestingu, úr útpressuðum formum sem sleppa þessum fyrirframkostnaði (Thomasnet birgja leiðsögn, 2024).
- Efnisval knýr allt niður á við: Ég passa umsóknina við rétta fjölliðuna, hvort það sé PVC fyrir rör og snið, ABS eða polycarbonate fyrir höggstyrk, HDPE og LDPE fyrir efnaþol, pólýprópýlen fyrir lifandi lamir, akrýl (PMMA) til glöggvunar, eða nælon í verkfræði (PA) og PEEK fyrir krefjandi hluta.
- PVC er meðal útbreiddasta plastsins í heiminum, algengt á sniðum, pípa, og slöngur, sem er ástæðan fyrir því að margir birgjar skrá það sem sjálfgefna getu (Samtök plastiðnaðarins, 2023).
- Extrusion tolerances run looser than injection molding because of material shrinkage and continuous forming, so I plan tolerances early rather than assuming molded-part precision (Protolabs, 2023).
- Ég meðhöndla ISO 9001 as a baseline signal of a mature quality management system, not a guarantee, and pair it with a concrete vetting checklist covering capacity, co-extrusion capability, og afgreiðslutími (ISO, 2015).
- For location intent, sourcing from a domestic plastics manufacturer can lower total landed cost by cutting freight, skylda, og birgðahaldskostnaður, a point worth weighing against unit price alone (Reshoring Initiative, 2023).
- Thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency, which I factor into both cost and sustainability conversations (US EPA, 2023).
- Claims like “stærsti” eða “best” factory mean little without context, so I benchmark suppliers on tooling cost, MOQ, quick-turnaround production, og sannað stuðning við frumgerð til framleiðslu í staðinn.
Það sem plastpressufyrirtæki og verksmiðjur gera í raun og veru
Þegar ég met birgir fyrir viðskiptavin, Ég byrja á því að skýra hvað orðið “extrusion” lýsir í raun á verslunargólfinu. Plastpressun bræðir hráefni úr plasti og myndar það í samfellt snið með föstum þversniði (SeaGate Plast, 2024). Þessi eina setning hefur mikið vægi: ferlið er samfellt frekar en skot fyrir skot, og rúmfræðin er skilgreind af tvívíðum þversniði sem liggur yfir alla lengd hlutans. Þess vegna hentar það langri framleiðslulotu og mikilli framleiðslu svo vel, og það er sannarlega önnur fræðigrein en sprautumótun eða vinnsla.
Í reynd, “plastefni útpressun” er vélin á bak við þrjár breiðar framleiðslufjölskyldur sem ég sé oftast beðið um:
- Snið — sérsniðin plastprófílar með skilgreindu þversniði, allt frá einföldum rásum og brúnum til flókinna forma með mörgum holum. Þetta er þar sem prófílútpressun og co-extrusion skína virkilega.
- Slöngur — umferð, sporöskjulaga, og multi-lumen rör notað í læknisfræði, meðhöndlun vökva, og pneumatic forrit, fengin frá sérhæfðum plastslöngum.
- Blað — plastplötuútpressun fyrir spjöld, línuskip, og hitamótandi efni, framleitt í gegnum flatan tening og rúlla stafla.
Framleiðendur, Verksmiðjur, og dreifingaraðilar eru ekki þeir sömu
Kaupendur nota þessi hugtök oft til skiptis, og það kostar þá tíma. Hér er hvernig ég aðskil þau:
- A framleiðanda eða verksmiðju á extrusion línurnar, sker sína eigin bana, og stjórnar ferlinu frá plastefni til fullunnar hluta. Þetta er sá sem þú vilt fyrir sérsniðin verkfæri, þétt ferli stjórna, eða plasti í verkfræði.
- A dreifingaraðili eða söluaðili selur og sendir venjuleg form en keyrir venjulega ekki línuna. Frábært fyrir útpressuð form á lager og hraðar endurpantanir, síður fyrir sérsmíði.
- A framleiðandi getur keypt lager snið og vél, suðu, eða settu þau saman í fullunna plastframleiðsluþjónustu.
Þegar ég leita á Thomasnet, Ég sía viljandi, vegna þess að þessar möppur skrá og flokka bandaríska plastpressuframleiðendur eftir getu og svæðum (Thomasnet, 2024). Þessi hæfisía er það sem segir þér hvort þú ert að tala við alvöru plastprófílframleiðanda eða milliliða.
Af hverju kaupendur leita að “Verksmiðja” Í staðinn fyrir “Birgir”
Í minni reynslu, breytingin í átt að “verksmiðju” tungumál gefur til kynna ásetning. Kaupendur sem slá það inn vilja fá heimild með innri stjórn á hönnun og verkfærum, gagnsæ MOQ samtöl, og getu til að stækka frá frumgerð til framleiðslu. Það endurspeglar einnig endurnýjunarþrýsting: Innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023), og bandaríski plastiðnaðurinn er enn stór þáttur í innlendri framleiðslu og atvinnu (Samtök plastiðnaðarins, 2023). Leita að innlendum plastframleiðanda, frekar en almennur birgir, er oft vísvitandi ákvörðun um áhættu og kostnað.
Hvernig plastpressunarferlið virkar, Skref fyrir skref

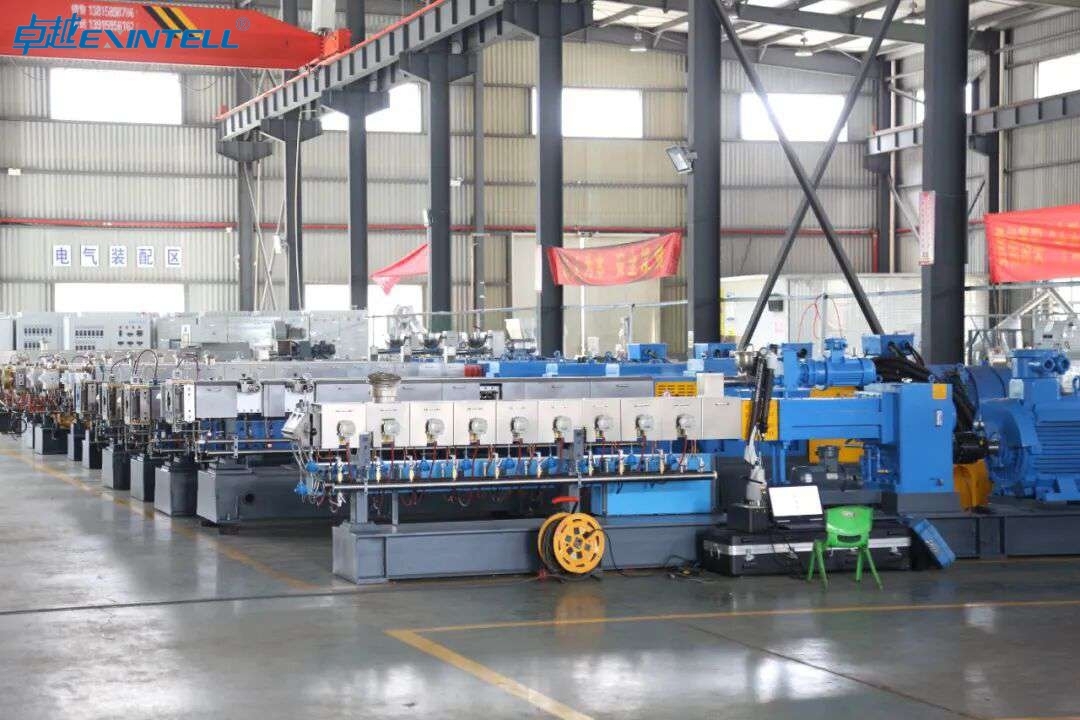
Skilningur á vélfræðinni hjálpar þér að spyrja betri spurninga og lesa tilvitnun nákvæmlega. Twin Skrúfa Extruder Framleiðendur Framleiðandi Ég fer með viðskiptavini í gegnum fimm stig af samfelldu útpressunarferlinu.
1. Hráefnisfóðrun og bráðnun í tunnunni
Hitaplastkögglar - venjulega PVC, ABS, HDPE, LDPE, eða pólýprópýlen - farðu inn í hylki og slepptu í upphitaða tunnu með snúningsskrúfu. Sambland af tunnuhitara og skrúfuskurði bræðir plastefnið í einsleitan bráðinn straum. Efnisval skiptir máli hér: PVC er meðal útbreiddasta plastsins í heiminum, almennt notað í sniðum, pípa, og slöngur (Samtök plastiðnaðarins), meðan pólýkarbónat, akrýl (PMMA), nylon (PA), og PEEK þjóna meira krefjandi, forrit í verkfræði. Oft er hægt að blanda endurunnið endurmalað aftur í, og hitauppstreymi sem notað er við útpressun er endurvinnanlegt, þannig að endurnýting endurmala bætir efnisnýtni (US EPA, 2023).
2. Þvinga bráðið plast í gegnum sérsniðna deyja
Bræðslunni er ýtt í gegnum deyja sem skilgreinir þversnið sniðsins. Þetta er hjarta ferlisins og ástæðan fyrir því að sérsniðin vinna ber verkfærakostnað. Samþynningaruppsetning notar fleiri en einn þrýstibúnað sem fóðrar einn móta, sem gerir þér kleift að sameina efni — stíft undirlag með mjúkri TPE/TPU þéttivör, til dæmis, eða litað hettulag yfir lægri kjarna.
3. Kæling, Stærð, og stöðugt flugtak
Að yfirgefa teninginn, mjúka sniðið fer í gegnum kæli- og stærðarkerfi - venjulega vatnsbað eða lofttæmingartank - sem læsist í stærðum. Flugtak (togari) teiknar sniðið á stýrðum hraða. Vegna þess að hluturinn myndast stöðugt og efnið minnkar þegar það kólnar, útpressunarþol eru almennt lausari en sprautumótun (Protolabs, 2023). Ég setti þær væntingar snemma svo viðskiptavinir tilgreina raunhæf vikmörk frekar en að borga fyrir nákvæmni sem ferlið getur ekki staðist efnahagslega.
4. Skurður í lengd og aukaframleiðsla
Innbyggð sag eða hníf sker stöðugt framleiðsla í lengd. Þaðan, aukaaðgerðir — boranir, gata, hak, prentun, eða samsetning - breyttu pressuðu plasthlutum í fullbúna íhluti. Þetta er brúin á milli hráefnis og nothæfs afhendingarefnis, og það er þar sem framleiðsla með hraða viðsnúningi er annað hvort unnin eða tapað.
Sérsniðnar vs lager plastútdrættir: Sem Þú þarft?
Þetta er sú ákvörðun sem ég er mest spurður um, og heiðarlega svarið er: það fer eftir magni, rúmfræði, og tímalína. Leyfðu mér að brjóta niður hverja leið.
Þegar lagerprófílar frá hillum eru rétti kosturinn
Lager útpressuð form — venjuleg stangir, rör, rás, horn, og blað — forðastu verkfærakostnað alveg og sendu hratt. Ef vörulistasnið passar við umsókn þína innan viðunandi vikmarka, að kaupa hlutabréf er nánast alltaf ódýrara, hraðari leið. Ég stýra viðskiptavinum hér fyrir frumgerðir, lágt magn, og hvaða hluta sem er þar sem venjulegt þversnið gerir starfið.
Þegar sérsniðin verkfæri og snið eru réttlætanleg
Sérsniðin útpressun krefst venjulega fjárfestingar í einu sinni í verkfærum og deyja, á meðan hlutabréfasnið forðast þennan kostnað (leiðbeiningar um uppsprettu iðnaðarins). Sá deyjakostnaður er réttlætanlegur þegar rúmfræði þín er séreign, þegar sérsniðið þversnið útilokar samsetningu niðurstreymis, eða þegar árlegt magn er nógu mikið til að afskrifa tólið. Yfir ákveðinni hlaupastærð, sparnaður á hvern feta af sérsmíðaðri teygju vegur þyngra en fyrirframútgjöldin.
Hybrid nálgunin: Stöðluð snið, Sérsniðnir varahlutir
Uppáhalds meðalvegurinn minn er oft gleymdur. Hægt er að búa til staðlaða pressuðu snið og rör í hagkvæma sérsniðna hluta með skjótum viðsnúningi (SeaGate Plast, 2024). Þú sleppir deyjafjárfestingunni, notaðu síðan klippingu, vinnsla, og samsetningu til að ná sérsniðinni afhendingu. Fyrir mörg forrit á miðjum bindi, þessi blendingur slær bæði hreinan lager og fulla sérsniðna heildarkostnað.
Samanburður á kostnaði og afgreiðslutíma
Hér er hvernig aðferðirnar þrjár bera almennt saman. Meðhöndlaðu þetta sem stefnumarkandi skipulagssvið, ekki tilvitnanir - raunverulegar tölur eru háðar efni, rúmfræði, og rúmmáli.
|
Þáttur |
Hlutabréfasnið |
Hybrid (Framleiddur staðall) |
Full sérsniðin útpressun |
|---|---|---|---|
|
Verkfærakostnaður fyrirfram |
Engin |
Enginn til lágs (eingöngu innréttingar) |
Einu sinni deyja fjárfesting |
|
Dæmigerður afgreiðslutími |
Stysta (oft á lager) |
Stutt til í meðallagi |
Lengst (deyja byggingu + fyrstu grein) |
|
Lágmarkspöntun (MOQ) |
Lágt |
Lágt til í meðallagi |
Hærri (að afskrifa verkfæri) |
|
Sveigjanleiki í rúmfræði |
Aðeins vörulistaform |
Standard lögun + vinnsla |
Alveg sérsniðinn þversnið |
|
Besta passa |
Frumgerðir, lágt hljóðstyrkur |
Mið bindi, væg aðlögun |
Hátt hljóðstyrkur, sérsniðnar snið |
|
Þáttur |
Hlutabréfasnið |
Hybrid (Framleiddur staðall) |
Full sérsniðin útpressun |
|---|---|---|---|
|
Verkfærakostnaður fyrirfram |
Engin |
Enginn til lágs (eingöngu innréttingar) |
Einu sinni deyja fjárfesting |
|
Dæmigerður afgreiðslutími |
Stysta (oft á lager) |
Stutt til í meðallagi |
Lengst (deyja byggingu + fyrstu grein) |
|
Lágmarkspöntun (MOQ) |
Lágt |
Lágt til í meðallagi |
Hærri (að afskrifa verkfæri) |
|
Sveigjanleiki í rúmfræði |
Aðeins vörulistaform |
Standard lögun + vinnsla |
Alveg sérsniðinn þversnið |
|
Besta passa |
Frumgerðir, lágt hljóðstyrkur |
Mið bindi, væg aðlögun |
Hátt hljóðstyrkur, sérsniðnar snið |
Hvaða leið sem þú velur, Ég mæli með því að staðfesta að búðin reki skjalfest gæðakerfi - ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu (ISO, 2015) og er enn útbreiddasta viðmiðið í plastgeiranum. Til að fá hagnýt yfirlit yfir hvernig birgðir og sérsniðnar vörur sitja hlið við hlið, ég finn SeaGate Plast’ sérsniðið yfirlit yfir útpressun gagnlegur viðmiðunarstaður.
Tegundir plastútdráttarsniða og vara

Þegar ég met verkefni fyrir extrusion, Ég byrja á þversniðinu, vegna þess að rúmfræði fullunnar hluta ræður næstum öllu niðurstreymis: teygjuhönnunin, efnisvalið, og að lokum verðið sem þú munt borga. Plastpressun bræðir hrá plastefni og myndar það í samfellt snið með föstum þversniði (SeaGate Plast, 2024). Þessi eina meginregla framleiðir furðu breiðan lista yfir form, svo það hjálpar til við að flokka þau eftir flækjum og virkni.
Solid snið, Holur snið, og flóknar rúmfræði
Solid snið eru vinnuhestar iðnaðarins: stangir, börum, kanta, og klippa án innra tóma. Auðveldast er að nota þau og fyrirgefa mest um umburðarlyndi, Þess vegna mæli ég með þeim fyrir fyrstu kaupendur sem prófa hönnun. Holir snið kynna innri rásir, og þeir krefjast flóknari stansa með dornum eða pinna til að halda holrúminu opnu þegar bræðslan kólnar. Flókin rúmfræði sameina marga veggi, undirskurðir, og þunnt til þykkt umbreytingar í einum þversniði, og það er þar sem sérfræðiþekking á mótahönnun og verkfærum skilur hæfan plastprófílframleiðanda frá meðaltali. Í minni reynslu, ójöfn veggþykkt er algengasta orsök vinda, svo ég ýti snemma á birgja hvernig þeir ætla að koma jafnvægi á efnisflæði yfir sniðið.
Slöngur og Multi-Lumen Extrusions
Slöngur eru sérhæfð undirmengi holur útpressunar, og það spannar allt frá einföldum eins-holu röri til multi-lumen hönnun með nokkrum samsíða rásum sem liggja eftir lengd hlutans. Kaupendur lækningatækja og greiningartækja halla sér á útpressur með mörgum holum til að flytja vökva, vír, og skynjara í gegnum eitt þétt snið. Áreiðanlegur birgir plastslöngur mun halda þéttri sammiðju og innri þvermál vikmörkum, þó ég minni viðskiptavini alltaf á að útpressunarþol eru almennt lausari en sprautumótun vegna rýrnunar efnis og stöðugrar mótunar (Protolabs hönnunarauðlindir, 2023). Skipuleggðu passa þína og úthreinsun í kringum þann veruleika frekar en að berjast við hann.
Co-Extrusion og Multi-Material snið
Co-extrusion keyrir tvö eða fleiri plastefni í gegnum sameiginlega mótun til að framleiða eitt snið með aðskildum efnissvæðum. Ég nota það þegar hluti þarfnast misvísandi eiginleika í einu, eins og stíft PVC burðarvirki með mjúkri TPE/TPU þéttingarvör, eða veðranlegt hettulag yfir ódýrt undirlag. Það útilokar aukasamsetningar- og tengingarskref, sem er þýðingarmikill kostnaðarsparnaður miðað við magn. Málið er flókið verkfæri, þannig að ég áskil mér co-extrusion fyrir hönnun þar sem fjölefnisávinningurinn réttlætir greinilega aukna deyjafjárfestingu.
Algengar iðnaðarumsóknir fyrir hverja tegund
Mismunandi rúmfræði teygjast að mismunandi geirum, og að passa við þau snemma heldur uppspretta samtölum einbeitt.
- Solid snið: hillukantur í smásölu, innrétting á húsgögnum, innsigli, og girðingarhlutar.
- Holir snið: glugga- og hurðarkarma, LED ljósarásir, og burðarvirkisklæðningu.
- Slöngur og multi-lumen: lækningaþræðir, vökvaflutningslínur, og pneumatic slöngur.
- Sampressuð snið: veðráttur, kæliþéttingar, og handföng með tvöföldu slagþoli.
- Útpressun á plötum: skilti, hitamótandi efni, og hlífðarplötur.
Vegna þess að plastpressun er samfelld, mikið magn ferli, það hentar langri framleiðsluferli sérstaklega vel, og stöðluð pressuð snið og rör er hægt að búa til hagkvæma sérsniðna hluta með skjótum viðsnúningi (SeaGate Plast, 2024). Ef árleg eftirspurn þín er stöðug og mæld í tugum þúsunda feta, extrusion hagfræði virkar mjög þér í hag.
Algeng efni sem notuð eru í plastpressu
Efnisval er sú ákvörðun sem ég sé að kaupendur vanmeta oftast. Trjáefnið stjórnar vélrænni styrkleika, efnaþol, hitastig, kostnaður, og jafnvel hversu þétt umburðarlyndi pressuvélin getur í raun og veru haldið. Ég flokka útpressunarresín í þrjú þrep, vinndu síðan með viðskiptavinum að því að hækka aðeins eins langt og umsóknin krefst raunverulega.
Vöru kvoða: PVC, Pólýetýlen, og pólýprópýlen
Vöruplastefni þekja meirihluta pressuðu rúmmálsins, og ekki að ástæðulausu. PVC er meðal útbreiddasta plastsins í heiminum, algengt í prófílum, pípa, og slöngur (Samtök plastiðnaðarins). Það býður upp á stífleika, veðurhæfni, og litlum tilkostnaði, og það tekur lit og yfirborðsáferð vel. Pólýetýlen kemur fyrir í tveimur kunnuglegum flokkum: HDPE fyrir stífur, efnaþolin snið og LDPE þar sem sveigjanleiki skiptir máli. Pólýprópýlen kemur jafnvægi á efnaþol með góðu styrkleika-til-þyngdarhlutfalli og frammistöðu lifandi lamir. Þegar viðskiptavinur spyr um plastefnisútpressun fyrir mikið magn, kostnaðarviðkvæmur hluti, þetta er næstum alltaf þar sem ég byrja.
Verkfræðikvoða: ABS, Pólýkarbónat, Nylon, og akrýl
Verkfræði-gráða plast stígur upp í vélrænni og hitauppstreymi. ABS skilar höggstyrk og hreinum frágangi fyrir neytenda- og girðingarhluta. Pólýkarbónat gefur mikla höggþol og sjónrænan skýrleika, sem gerir það að grunni fyrir lýsingu á linsum og öryggisglerjun. Nylon (PA) býður upp á slitþol og hörku fyrir vélræna íhluti og kapalstjórnun. Akrýl (PMMA) veitir framúrskarandi skýrleika og UV-stöðugleika fyrir skjá- og merkingarsnið. Ég flyt kaupendur inn á þetta stig þegar kvoða úr vöru getur ekki staðið undir álagi, hita, eða kröfur um skýrleika, og ég er viss um að þeir verðleggja trjákvoðaálagið á móti frammistöðuhagnaðinum áður en þeir skuldbinda sig.
Hágæða efni eins og PEEK
Efst situr lítill hópur af afkastamiklum fjölliðum, með PEEK sem viðmiðunarpunkt. PEEK þolir stöðugan háan hita, árásargjarn efni, og krefjandi vélrænt álag, þess vegna birtist það í geimferðum, læknisfræði, og hálfleiðaraforrit. Efniskostnaður er verulegur, svo ég tilgreini það aðeins þegar rekstrarumhverfið skilur ekki eftir ódýrari kost. Not every plastic profile manufacturer processes PEEK, so capability screening matters more at this level.
Matching Material Properties to Application Requirements
My selection framework is deliberately simple: define the non-negotiable requirement first, then choose the least expensive resin that clears it. The table below summarizes how I weigh the common options for extruded plastic parts.
| Efni | Tier | Key Strengths | Hlutfallslegur kostnaður | Dæmigert forrit |
|---|---|---|---|---|
| PVC | Vöruvara | Stífur, veðurfarslegt, litlum tilkostnaði | $ | Snið, pípa, snyrta |
| HDPE / LDPE | Vöruvara | Efnaþol; stiff or flexible | $ | Slöngur, línuskip, ducting |
| Pólýprópýlen | Vöruvara | Efnaþol, lifandi lamir | $ | Fluid handling, lamir |
| ABS | Verkfræði | Höggstyrkur, clean finish | $$ | Hólf, consumer parts |
| Pólýkarbónat | Verkfræði | Höggþol, skýrleika | $$ | Linsur, öryggisglerjun |
| Nylon (PA) | Verkfræði | Slitþol, hörku | $$ | Vélrænn, cable guides |
| Akrýl (PMMA) | Verkfræði | Skýrleiki, UV stöðugleiki | $$ | Merki, sýnir |
| KIKIÐ | Afkastamikil | Hiti, efna, and load resistance | $$$$ | Aerospace, læknisfræði, hálfleiðari |
One efficiency point worth raising with any supplier: thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency (Umhverfisverndarstofnun Bandaríkjanna, 2023). Asking how a factory handles regrind tells me something about both their cost discipline and their sustainability practices.
Framleiðendur plastpressu í Bandaríkjunum
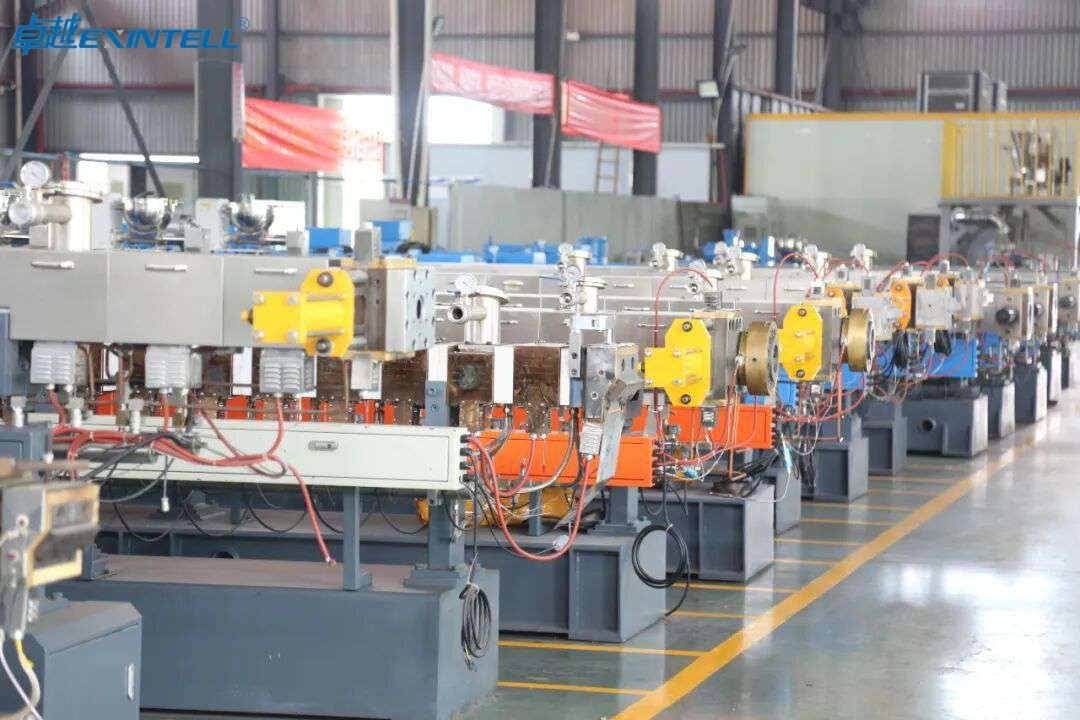
Fyrir marga kaupendur ráðlegg ég, uppspretta spurningin er ekki aðeins “hver getur pressað þennan prófíl” en “hver getur útskúfað það hér.” Innlend uppspretta hefur færst frá vali yfir í stefnumótandi ákvörðun, og það á skilið glöggt útlit frekar en endurspegla ættjarðarást.
Af hverju uppspretta í Bandaríkjunum skiptir máli fyrir marga kaupendur
Fjárhagsmálið er sterkara en það virðist í fyrstu. Endurheimt og innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023). Þegar ég keyri heildarkostnaðarsamanburð frekar en einingaverðssamanburð, sparnaður á sjó minnkar oft þegar ég bæti við sjófrakt, gjaldskrár, öryggis lager, og rekstrarfé bundið í löngum flutningstíma. Fyrir innlendan plastframleiðanda sem þjónar bandarískum viðskiptavinum, lead times measured in weeks rather than months also mean less risk if a design changes mid-program.
Regional Manufacturing Hubs Across the Country
US extrusion capacity is not evenly distributed, and knowing the map speeds up sourcing. The Great Lakes and Upper Midwest concentrate general-purpose profile and tubing extruders near automotive and industrial demand. The Northeast holds a dense cluster of medical and precision tubing specialists. The Southeast has grown quickly around building products and packaging. The West Coast and Southwest serve electronics, loftrými, and consumer markets. Supplier directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is where I usually build a first shortlist before making calls.
Domestic Quality, Samskipti, and IP Advantages
Beyond cost, three practical advantages keep drawing buyers home. Fyrst, quality systems are easier to verify in person; ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu (Alþjóðastaðlastofnunin, 2015), and I can audit a domestic supplier’s implementation without an international trip. Í öðru lagi, time-zone-aligned communication shortens the feedback loop from prototype to production, which matters when a die needs a mid-run adjustment. Þriðja, intellectual property protection is more enforceable under US jurisdiction, a real concern when a custom profile is a competitive differentiator. I treat these as the differences that a spreadsheet alone will miss.
How US Factories Serve Diverse Industries
American extruders span the full range of contract manufacturing, from stock extruded shapes shipped from inventory to fully custom die programs. Custom extrusion typically requires a one-time tooling or die investment, while stock profiles avoid that cost, so I match the sourcing path to how unique the geometry really needs to be. The US plastics industry remains a major contributor to domestic manufacturing shipments and employment (Samtök plastiðnaðarins, 2023), and that depth means a buyer can usually find a plastic fabrication services partner suited to their volume, from prototype to production. For a broad view of custom capabilities, I often point clients to overviews such as custom plastic extrusion manufacturers to calibrate expectations before requesting quotes.
Hvernig á að finna plastpressufyrirtæki nálægt þér
When I begin a sourcing project, geography is one of the first variables I weigh. Location shapes freight cost, communication cadence, and how quickly I can iterate from prototype to production. Sem sagt, proximity is only valuable when the nearby supplier can actually do the work. Í minni reynslu, the smartest approach treats “nálægt mér” as a filter, ekki ákvörðun.
Why Local Sourcing Often Pays Off
A domestic plastics manufacturer close to your facility gives you three concrete advantages. Fyrst, shorter shipping distances lower freight and lead-time risk, which matters for bulky extruded plastic parts and long profiles that ship as oversized freight. Í öðru lagi, local partners make on-site visits practical, and I have caught more process issues in a two-hour plant walkthrough than in weeks of email. Þriðja, proximity accelerates iteration: when a die needs a tweak, a supplier a few hours away can turn samples faster than one across an ocean.
The financial case reaches beyond the unit price. According to the Reshoring Initiative (2023), Innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, og birgðahaldskostnaður. The domestic base is substantial, líka; Plastiðnaðarsambandsins (2023) reports that the US plastics industry is a major contributor to domestic manufacturing shipments and employment, which means qualified capacity for resin extrusion is usually within reach.
Where I Look: Directories, Associations, og tilvísanir
To build an initial list of candidates, I use three complementary channels:
- Supplier directories. Thomasnet (2024) lists and categorizes US plastic extrusion manufacturers by capability and region, which makes it straightforward to filter by material, ferli, and location.
- Trade associations. Membership in bodies like the Plastics Industry Association signals a firm that invests in standards and industry engagement.
- Referrals. A recommendation from an engineer who has run production with a plastic profile manufacturer carries more weight than any marketing page, because it reflects delivered performance.
I treat the directory as a starting point for a plastic tubing supplier or profile shop, then validate each name against real references before it earns a spot on my shortlist.
Balancing Proximity Against Capability and Price
Distance is a tiebreaker, not a trump card. If a nearby shop cannot hold your tolerances, run your resin, or meet your volume, the convenience is worthless. I rank capability and quality first, síðan verð, then location. A plastic extrusion companies factory supplier two states away with the right co-extrusion line and a proven ISO 9001 system will usually serve me better than a closer shop lacking those capabilities.
When Local Is Not the Best Option
Sometimes the right partner is not nearby. Specialized work in engineering-grade plastics such as PEEK, polycarbonate, eða nylon (PA) may only be done well by a handful of shops nationally. High-volume manufacturing programs can justify shipping economics that favor a distant, more automated plant. And when you need capabilities like plastic sheet extrusion combined with in-line fabrication, the fit of the process matters more than the mileage. In those cases I widen the search radius and lean on video plant tours and third-party audits to close the distance gap.
Understanding the Largest Plastic Extrusion Companies
Buyers often gravitate toward the biggest names, assuming scale guarantees a better outcome. Scale does deliver real advantages, but it also carries tradeoffs. Understanding what “stærsti” actually means helps me match a supplier’s footprint to my program rather than to a reputation.
What Scale Means for Capacity and Reliability
Extrusion er samfelld, high-volume process well suited to long production runs, and large factories are built around that reality. More extrusion lines mean higher throughput, redundancy if one line goes down, and the ability to absorb demand spikes. Scale usually correlates with mature quality systems as well; ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (Alþjóðastaðlastofnunin, 2015), is almost table stakes among large plants. That maturity translates into more consistent extruded plastic parts across long runs.
The Tradeoffs of Large Factories vs. Specialized Shops
Bigger is not automatically better. Large plants optimize for volume, which can mean higher minimum order quantities, less flexibility on small custom runs, and slower responsiveness on prototype work. A specialized shop may excel at tight-tolerance custom plastic profiles, unusual resins, or quick-turnaround production that a high-volume plant treats as a nuisance. The table below summarizes how I weigh the two.
| Þáttur | Large-Scale Factory | Specialized Shop |
|---|---|---|
| Getu | Hátt; multiple lines, redundancy | Takmarkað; fewer lines |
| Lágmarks pöntunarmagn | Often high | Usually flexible |
| Prototype speed | Hægari; volume-focused scheduling | Hraðari; agile setup |
| Material range | Broad commodity resins (PVC, HDPE, LDPE, PP) | Often engineering-grade (KIKIÐ, PC, PA) |
| Price per unit at volume | Neðri | Hærri |
| Besta passa | Long production runs | Sérsniðin, lágt til miðlungs hljóðstyrk, complex profiles |
When High-Volume Capability Is Essential
There are programs where I will not compromise on scale. Stöðugt, long-run demand for standardized profiles, pípa, or tubing in commodity resins is the natural home of a large factory. PVC er meðal útbreiddasta plastsins í heiminum, almennt notað í sniðum, pípa, og slöngur, and sourcing it at volume rewards the economies a big plant provides. If your forecast calls for millions of feet of a stable profile cross-section, high-volume capability moves from nice-to-have to essential.
How to Verify Claimed Scale and Capacity
Claims on a website are not evidence. Before I accept a “stærsti” eða “highest capacity” claim, I verify it with concrete questions:
- How many extrusion lines are operational, and what is the die diameter range on each?
- What is current utilization, and how much spare capacity exists for my program?
- Can you share throughput figures (lbs/hour or feet/day) for a comparable profile?
- What redundancy exists if a line fails mid-run?
- Which certifications, eins og ISO 9001, are current, and may I see the certificate?
I pair those answers with a plant tour or audit. Physical evidence of running lines, staffing, and inventory tells me far more than any capacity figure quoted in a brochure.
How to Identify the Best Plastic Extrusion Factory for Your Project
“Best” is one of the most misused words in supplier marketing. Í reynd, the best plastic extrusion companies factory manufacturer is the one that best fits your specific requirements, not the one with the loudest claim. I define the term relative to my project, then score candidates against that definition.
Defining “Best” Relative to Your Specific Needs
Before comparing suppliers, I document what my project actually demands: the resin (segja, ABS for impact resistance, akrýl (PMMA) fyrir sjónrænan skýrleika, or TPE/TPU for flexibility), the tolerance band, hljóðstyrknum, the timeline, and the level of engineering support I need for die design and tooling. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs hönnunarauðlindir, 2023), so I confirm early that a candidate can meet my dimensional requirements rather than assuming it can. A shop that is ideal for a high-volume HDPE pipe run may be the wrong choice for a tight-tolerance polycarbonate profile.
Weighing Quality, Kostnaður, Hraði, and Support
Every sourcing decision balances four levers, and improving one often pressures another:
- Gæði. Documented quality systems, in-process inspection, and material traceability. ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics.
- Kostnaður. Not just unit price. Sérsniðin útpressun krefst venjulega fjárfestingar í einu sinni í verkfærum og deyja, while stock extruded shapes avoid that cost, so I model total cost including tooling and MOQ.
- Hraði. Hægt er að búa til staðlaða pressuðu snið og rör í hagkvæma sérsniðna hluta með skjótum viðsnúningi (SeaGate Plast, 2024), but lead times vary widely between shops.
- Stuðningur. Engineering input on profile cross-section and material selection can prevent costly redesigns as you move from prototype to production.
Sustainability increasingly enters the equation as well. Thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency (Umhverfisverndarstofnun Bandaríkjanna, 2023), which can reduce both cost and waste when a supplier manages it responsibly.
Reading Past “Best” Marketing Claims
Superlatives are easy to print and hard to prove. When I see “best,” “leiðandi,” eða “premier,” I translate the claim into a testable question. Instead of accepting “best quality,” I ask for defect rates and inspection records. Í staðinn fyrir “fastest,” I ask for typical lead times on my specific part. Í staðinn fyrir “most experienced,” I ask for references in my industry. Marketing language that cannot survive a follow-up question does not influence my shortlist.
Building a Shortlist Scoring Method
To keep the comparison objective, I use a weighted scoring model. I list my criteria, assign each a weight that reflects its importance to the project, score every candidate from 1 til 5, and multiply. The weights shift by project; a prototype program might weight speed and engineering support heavily, while a mature production program weights cost and capacity.
- List criteria: gæðakerfi, efnisgeta, umburðarlyndi, getu, leiðtíma, verkfærakostnaður, verkfræðiaðstoð, and location.
- Assign weights that total 100 percent, reflecting your priorities.
- Score each supplier 1 til 5 on every criterion, using verified evidence rather than marketing claims.
- Calculate weighted totals and rank the candidates.
- Validate the top two with reference calls and, ideally, a plant visit before committing.
This structured method has consistently steered me toward the partner that fits the work, whether that turns out to be a large plant, a nimble specialist, or a domestic shop just down the road. For a deeper look at how custom extrusion capabilities map to applications, resources such as SeaGate Plast’ sérsniðið yfirlit yfir útpressun are a useful reference as you refine your own criteria.
Key Capabilities to Evaluate in a Plastic Extrusion Company
When I vet a plastic profile manufacturer, I look
Tolerances and Precision in Extruded Parts
Þegar ég met framleiðanda plastprófíla, tolerances are the first place I look for a reality check. Extrusion er stöðugt mótunarferli, so it behaves differently from molding. As Protolabs notes, extrusion tolerances are generally looser than injection molding because material shrinkage and continuous forming introduce variability that a closed mold does not (Protolabs hönnunarauðlindir, 2023). Setting expectations here early saves both money and rework later.
Typical Achievable Tolerances by Material and Profile
Í minni reynslu, achievable precision depends heavily on the resin and the geometry of the profile cross-section. Rigid engineering-grade plastics hold tighter dimensions than soft or semi-crystalline materials, and simple shapes hold tighter than complex hollow profiles. The ranges below reflect commonly quoted commercial extrusion capabilities for custom plastic profiles; always confirm against your supplier’s published standards for your specific part.
| Efni | Stöðugleiki í stærð | Typical tolerance tendency | Notes for specifying |
|---|---|---|---|
| Stíft PVC | Hátt | Tighter, well-controlled | Widely extruded; predictable in profiles and tubing |
| ABS | Hátt | Tight on rigid profiles | Good for structural extruded plastic parts |
| Pólýkarbónat | Hátt | Þétt, low shrink | Optical and impact-rated applications |
| Akrýl (PMMA) | Hátt | Þétt, but brittle at thin walls | Sheet and clear profiles |
| Nylon (PA) | Í meðallagi | Looser; moisture-sensitive | Account for post-extrusion moisture uptake |
| HDPE / LDPE | Moderate to low | Looser; higher shrink | Expect wider bands on wall and OD |
| Pólýprópýlen | Í meðallagi | Looser; semi-crystalline shrink | Allow generous tolerance on critical dims |
| KIKIÐ | Hátt | Þétt, but specialized | High-temp engineering runs; higher cost |
| TPE / TPU | Lágt | Loosest; flexible recovery | Soft profiles deform under measurement |
Factors That Affect Dimensional Stability
Several variables move a part inside or outside its tolerance band. Wall thickness uniformity matters most: thick and thin sections in the same profile cool at different rates and warp. Semi-crystalline resins like polypropylene and HDPE shrink more than amorphous ones like polycarbonate and acrylic, so the die must be cut to compensate. I also watch for haul-off speed, melt temperature, og kælibaðsstýring, þar sem svif í einhverju af þessu kemur fram sem víddarbreytingar yfir langan tíma. Fyrir rakafræðileg efni eins og nylon, raki sem frásogast eftir útpressun getur breytt stærð dögum síðar, þess vegna spyr ég hvernig birgir skilgreinir og geymir fullunna lager.
Tilgreina vikmörk í teikningum þínum
Hreinasta leiðin til að stjórna kostnaði er að þola aðeins það sem virkni skiptir máli. Ég kalla skýrt fram mikilvægar víddir, beita hæfilegum almennum þolmörkum á allt annað, og vísa til datumeiginleika sem passa við aðra hluti. Þar sem sveigjanlegt TPE eða TPU snið á við, Ég tilgreini mælingaraðferðina og búnaðinn, vegna þess að mjúkur hluti mælist öðruvísi undir léttum þrýstingi en í hvíld. Being specific about which surfaces are cosmetic versus functional lets a plastic fabrication services partner set up the line intelligently instead of overbuilding to a blanket precision requirement.
Balancing Precision Against Cost
Tighter tolerances raise cost through slower line speeds, more scrap, added inspection, and sometimes secondary sizing or machining. Í reynd, I treat precision as a dial rather than a switch: I hold the two or three dimensions that drive fit and function tightly and relax the rest. That approach keeps resin extrusion economical while still delivering parts that assemble correctly. When a design genuinely needs molding-level precision on every feature, that is a signal the part may not be a good extrusion candidate, and I revisit the process choice before committing to tooling.
Minimum Order Quantities and Lead Times
MOQs and lead times are where the difference between stock extruded shapes and true custom work becomes concrete. Custom extrusion typically requires a one-time tooling investment in a die, while stock profiles avoid that cost entirely, per common industry sourcing guidance. That single fact drives most of the ordering economics, so I plan around it from the start.
Typical MOQ Ranges for Stock vs Custom
Stock profiles and tubing can often be bought in small quantities, sometimes by the foot or in single boxes, because the supplier already runs them. As SeaGate Plastics points out, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround, which is a practical advantage when volumes are modest (SeaGate Plast, 2024). Custom profiles are different. Because the line has to be set up, purged, and stabilized before good parts come off, suppliers set a minimum run to amortize that setup. I commonly see custom MOQs expressed in pounds of resin or in linear footage rather than piece count, and the threshold rises with more exotic engineering-grade plastics.
How Lead Times Vary With Tooling and Volume
For a new custom profile, the die is the pacing item. Tooling design, klippa, and first-article trials typically dominate the initial schedule, and I budget several weeks for die design and tooling before any production parts exist. Once the die is proven, repeat orders move quickly because the tooling is on the shelf. Higher volumes actually help here: extrusion is a continuous, high-volume process well suited to long production runs, so once a line is dialed in, adding footage is efficient rather than disruptive.
Quick-Turnaround Options and Expedited Runs
When a timeline is tight, I look at three levers. Fyrst, use stock profiles or standard tubing that can ship from inventory and be cut or fabricated to length. Í öðru lagi, ask whether an existing die is close enough to modify rather than cutting a new one. Þriðja, request an expedited slot, which many suppliers offer for a premium by prioritizing line time. Quick-turnaround production is realistic for standard shapes; for genuinely new custom geometry, the tooling step still sets the floor on how fast you can go.
Planning Your Project Timeline
I work backward from the required delivery date and add explicit buffers for die design, first-article approval, og hvers kyns aukaaðgerðir. Moving from prototype to production is smoother when I lock the profile cross-section early, because late geometry changes mean recutting the die and resetting the clock. Aligning MOQ with real annual demand also matters: ordering an efficient run size once beats paying repeated setup charges on small, frequent custom orders.
Cost Drivers in Plastic Extrusion Pricing
Understanding what actually drives a quote lets me negotiate from evidence rather than instinct. Extrusion pricing breaks down into a handful of levers, and knowing which one dominates for a given part tells me where the savings live.
Material Selection and Resin Pricing
Resin is usually the largest recurring cost, and it varies widely by grade. Commodity materials like PVC, pólýprópýlen, HDPE, and LDPE sit at the low end; PVC in particular is among the most widely extruded plastics globally and is well supported across suppliers. Engineering-grade plastics such as polycarbonate, nylon, and especially PEEK command higher prices and can require specialized processing. One efficiency I always ask about is regrind: thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency, which can lower material cost on non-critical parts (Umhverfisverndarstofnun Bandaríkjanna, 2023). Choosing the least expensive resin that meets the application requirement is the single highest-leverage decision in material selection.
Verkfæri, Uppsetning, and Run Volume
Custom work carries a one-time die cost that stock profiles avoid. That tooling charge is fixed, so it amortizes across the run: the more footage I order, the lower the per-part tooling burden. Setup time and line stabilization add cost to every job regardless of size, which is exactly why small custom orders feel expensive per piece. Co-extrusion, which combines two materials in one profile, adds tooling and process complexity and therefore cost, but it can eliminate secondary assembly, so I weigh the tradeoff on total value rather than tooling alone.
Secondary Operations and Finishing
Anything that happens after the profile leaves the die adds cost: cutting to length, borun, hak, prentun, hole punching, tight-tolerance sizing, og umbúðir. Individually these are minor, but they stack quickly on high piece counts. I decide deliberately which operations belong in-line with the extrusion and which are genuinely needed, because each added step also adds handling and inspection. Where a feature can be designed into the profile cross-section instead of machined afterward, I do that, since forming a feature is nearly free compared with a downstream operation.
Domestic vs Offshore Cost Comparisons
Headline piece price often favors offshore, but I evaluate total landed cost. The Reshoring Initiative notes that domestic sourcing can reduce total landed cost by lowering freight, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023), and those factors are easy to underestimate when comparing unit prices alone. Working with a domestic plastics manufacturer also shortens lead times, einfaldar samskipti, and reduces the inventory buffer I have to hold against long ocean transit. The US plastics industry is a substantial contributor to domestic manufacturing shipments and employment (Samtök plastiðnaðarins, 2023), so the domestic supplier base for both stock and custom profiles is deep. Þumalputtareglan mín: for high-volume, low-mix commodity profiles, offshore can win on price; for responsive, higher-mix, or engineering-grade work, domestic contract manufacturing usually wins on total cost and risk. For a fuller look at custom capabilities, I point buyers to custom plastic extrusion manufacturers such as SeaGate Plastics as a reference point for scope and services.
Questions to Ask Before Choosing a Factory
When I vet a plastic profile manufacturer, I treat the first conversation as a structured interview rather than a sales call. The goal is to separate shops that can genuinely deliver my part from those that simply want the order. Over years of sourcing extruded plastic parts, I have found that a handful of pointed questions surface most of the risk before a single dollar changes hands. Below is the checklist I actually use.
Getu, Vottanir, and Material Expertise
I start by asking what the factory runs today, not what it claims it can run. Continuous extrusion is a high-volume manufacturing process, so I want to know line count, typical run lengths, and whether they have headroom for my volume without displacing existing customers. On the quality side, I ask directly about certification. ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu (Alþjóðastaðlastofnunin, 2015), and while certification is not a guarantee of good parts, its absence tells me the shop may lack documented process controls.
Material expertise is the third leg. A capable resin extrusion supplier should speak fluently about the polymers relevant to my application, whether that is PVC and HDPE for construction profiles, ABS and polycarbonate for enclosures, polypropylene and LDPE for packaging and tubing, or engineering-grade plastics like nylon (PA) and PEEK for demanding environments. PVC er meðal útbreiddasta plastsins í heiminum, almennt notað í sniðum, pípa, og slöngur (Samtök plastiðnaðarins). If I need flexible sections, I confirm experience with TPE/TPU, and if my part demands a rigid core with a soft-touch or weather-resistant skin, I ask whether they offer co-extrusion. Lab Extruder Heildverslun
Prototyping and Design Support Availability
I ask whether the factory offers design consultation before tooling is cut. The best plastic fabrication services partners will review my cross-section for extrudability, flag thin walls or sharp corners that trap stress, and suggest material substitutions that lower cost without hurting performance. I also confirm they can produce a representative prototype rather than pointing me straight to a production die.
Leiðtími, MOQs, and Delivery Track Record
Here I get specific. I ask for standard lead times on both tooling and production, the minimum order quantity, and how MOQ scales with material and profile complexity. Custom extrusion typically requires a one-time tooling investment for the die, while stock extruded shapes avoid that cost entirely (leiðbeiningar um uppsprettu iðnaðarins). If my volumes are modest, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (SeaGate Plast, 2024), so I always ask what stock profiles they carry. On delivery, I want on-time performance data, not adjectives.
References and Industry Experience
Loksins, I ask for references in my industry. A shop that regularly serves medical, bifreiða, or building-products customers has already navigated the tolerances and documentation those sectors demand. I call the references and ask two questions: did the parts meet spec on the first production run, and how did the supplier handle the problem when something went wrong?
From Prototype to Production: How the Process Unfolds
Once I have chosen a supplier, the path from a drawing to shippable extruded plastic parts follows a predictable sequence. Understanding each stage helps me set realistic timelines internally and catch problems while they are still cheap to fix.
Submitting Drawings and Design Consultation
I begin by sending a dimensioned drawing of the profile cross-section, along with the target material, lit, tolerance requirements, and end-use environment. This is where design-for-manufacturing consultation earns its keep. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs hönnunarauðlindir, 2023), a good engineer will help me place critical dimensions where the process can reliably hold them and relax the ones that do not matter.
Sample and Prototype Validation
Next comes a sample or prototype. Depending on the shop, this may be pulled from a soft or temporary die, or matched from existing stock extruded shapes. I use this stage to validate fit, sveigjanleika, yfirborðsfrágangur, and material behavior in my actual assembly. Catching a wall-thickness issue on a prototype costs me a revision; catching it after the production die is cut costs me the tooling.
Tooling Approval and First-Article Inspection
Extruder Twin Screw After I approve the design, the factory cuts the production die. The die design and tooling step is the largest one-time cost in custom extrusion, so I review the tooling drawing carefully before signing off. Once the die runs, I require a first-article inspection: a documented measurement of the initial output against my drawing. I do not release full production until the first article passes.
Ramping to Full Production
With the first article approved, the line ramps to full production. Plastic extrusion is a continuous, high-volume process well suited to long production runs (SPI/Plastics Industry Association overview), so unit costs typically drop as volume climbs. I confirm the quality plan for ongoing runs, including sampling frequency and the criteria for holding or scrapping out-of-spec material. Thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency (Umhverfisverndarstofnun Bandaríkjanna, 2023), so I also clarify the shop’s regrind policy when appearance or mechanical properties are critical.
Domestic vs Overseas Extrusion Sourcing
One of the most consequential decisions I make is where to source. The instinct is to compare unit price, but in my experience that number alone is misleading. What matters is total landed cost and the operational realities that price hides.
Cost vs Total Landed Cost Considerations
Overseas suppliers often quote a lower piece price, en ég bæti frakt, skyldur, customs handling, and the inventory carrying cost of larger safety stock and longer transit. Endurheimt og innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023). Once I build a full landed-cost model, the gap between a domestic plastics manufacturer and an overseas one usually narrows, and sometimes reverses.
Leiðslutími, Sending, and Communication Factors
Domestic sourcing shortens my supply chain and simplifies communication across time zones and languages, which matters most when I need quick-turnaround production or fast design changes. Overseas sourcing can suit stable, high-volume programs where the design is frozen and lead time is not a constraint.
Quality Control and IP Protection
Proximity makes on-site audits and first-article reviews far easier, and domestic contracts generally offer stronger, more enforceable intellectual property protection for a proprietary die design. When my profile represents real design investment, that protection weighs heavily.
Þegar hver valkostur er skynsamlegur
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (Samtök plastiðnaðarins, 2023), and directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes local sourcing practical to research. The table below summarizes how I weigh the two paths.
| Þáttur | Domestic Sourcing | Overseas Sourcing |
|---|---|---|
| Unit price | Higher piece price | Often lower piece price |
| Heildar löndunarkostnaður | Lower freight, skylda, and carrying cost | Added freight, skylda, and inventory cost |
| Leiðslutími | Styttri, more responsive | Lengri, transit-dependent |
| Samskipti | Same time zone and language | Time-zone and language gaps |
| Quality audits | On-site visits practical | Remote or costly to audit |
| IP vernd | Sterkari, more enforceable | Variable enforcement |
| Besta passa | Sérsniðin snið, fast changes, proprietary tooling | Frozen designs, mjög mikið magn, price-driven programs |
Í reynd, I lean domestic for custom plastic profiles that involve proprietary tooling, evolving designs, or short lead times, and I consider overseas contract manufacturing only for mature, stöðugt, high-volume parts where the landed-cost math clearly favors it. For a starting point on capabilities and stock offerings, resources like SeaGate Plast are a useful reference when scoping a domestic partner.
Sustainability and Recyclability in Extrusion
When I evaluate a plastic extrusion companies factory today, sustainability is no longer a soft preference tucked into the back of a proposal. It sits alongside price, leiðtíma, and quality as a core selection criterion. The good news is that extrusion is inherently well suited to responsible material use, and the suppliers I trust have built that advantage into their operations rather than treating it as an afterthought.
Recyclable Thermoplastics and Scrap Reuse
Most of the polymers I specify for extruded plastic parts are thermoplastics, which means they can be remelted and reformed multiple times without a complete loss of properties. According to the US Environmental Protection Agency (2023), thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency. That single characteristic separates them from thermosets and gives buyers real leverage on both cost and environmental footprint.
Í reynd, this recyclability spans the common resins you will encounter across quotes. PVC, HDPE, LDPE, and Polypropylene are among the workhorses of profile extrusion and plastic tubing, and each reclaims well when handled correctly. Engineering-grade plastics such as ABS, Pólýkarbónat, Nylon (PA), og akrýl (PMMA) also tolerate controlled regrind, though I hold them to tighter blend ratios because their properties matter more in demanding applications. High-performance materials like PEEK and flexible TPE/TPU sit at the specialized end, where reuse requires more careful process control.
Regrind and Material Efficiency Practices
The continuous extrusion process generates predictable scrap: startup purge, trim from profile cross-section adjustments, and off-spec runs during die changeovers. A capable plastic profile manufacturer captures this material, granulates it into regrind, and reintroduces it at a defined percentage back into virgin resin. I always ask for the specifics because the details reveal how disciplined an operation really is.
- What regrind percentage do you blend into standard production, and does it change for cosmetic versus structural parts?
- How do you segregate resin types to prevent cross-contamination during resin extrusion?
- Can you document material traceability from raw resin through finished profile?
- Do you offer post-industrial recycled content options when my application allows it?
Co-extrusion deserves a mention here. By combining a virgin outer layer with a regrind or recycled core, some suppliers deliver the surface quality I need while lowering virgin material consumption. It is a practical way to reconcile appearance requirements with sustainability goals on the same part.
Choosing Environmentally Responsible Suppliers
Í minni reynslu, a domestic plastics manufacturer often carries a sustainability advantage that has nothing to do with marketing. The Reshoring Initiative (2023) notes that domestic sourcing can reduce total landed cost by lowering freight, skylda, og birgðahaldskostnaður, and shorter supply chains also mean lower transport emissions. When I compare a nearby US factory against overseas alternatives, the environmental and logistical benefits frequently reinforce each other.
Beyond geography, I look for suppliers whose quality systems formalize waste reduction. ISO 9001, described by the International Organization for Standardization (2015) as the internationally recognized standard for quality management systems, does not mandate sustainability by itself, but shops that maintain it tend to run tighter processes with less scrap and better material accountability.
Regulatory and Buyer Sustainability Expectations
My downstream customers increasingly ask about recycled content, chemical compliance, and end-of-life recyclability before they will approve a part. That pressure flows straight back to how I write specifications. I now treat sustainability documentation as part of the deliverable, ekki bónus. When a supplier can hand me material certifications, regrind policies, and recyclability data without hesitation, it signals a partner ready for where the market is heading rather than where it has been.
Making Your Final Decision and Requesting a Quote
Once I have shortlisted candidates, the decision comes down to matching each supplier’s real capabilities against my project’s non-negotiables. The extrusion market rewards specialization, so the goal is not finding the largest or most decorated factory but the one whose strengths line up with my part, my volumes, and my timeline.
Consolidating Your Evaluation Criteria
I bring my findings together into a single scorecard so I am comparing suppliers on the same terms. Claims like “stærsti” eða “best” mean little in isolation; a large plastic extrusion companies factory tuned for high-volume commodity profiles may be the wrong fit for a low-volume, tight-tolerance engineering part, og öfugt. The table below shows the weighting I typically apply, though I adjust it to the priorities of each program.
| Evaluation Criterion | What I Look For | Typical Weight |
|---|---|---|
| Material capability | Experience with my resin (PVC, HDPE, Pólýkarbónat, o.s.frv.) and co-extrusion if needed | Hátt |
| Tooling and die design | In-house die design, tooling lead time, revision support | Hátt |
| Gæðakerfi | ISO 9001 certification and documented process controls | Hátt |
| Volume fit | Alignment of MOQ and capacity with my annual demand | Miðlungs |
| Leiðslutími | Realistic tooling plus production schedule, quick-turnaround options | Miðlungs |
| Staðsetning | Domestic sourcing benefits, frakt, and responsiveness | Miðlungs |
| Sjálfbærni | Regrind practices, endurunnið efni, rekjanleika efnis | Rising |
Preparing a Clear RFQ Package
The quality of the quotes I receive is directly proportional to the quality of the request I send. A vague inquiry produces padded, cautious pricing; a complete RFQ produces sharp, comparable numbers. Extrusion carries specific cost drivers a supplier needs to see up front, aðallega einskiptis fjárfestingu í verkfærum fyrir sérsniðin snið, sem leiðbeiningar um uppsprettu iðnaðarins staðfesta er aðeins forðast þegar þú notar útpressuð form á lager.
Hvaða upplýsingar á að hafa með fyrir nákvæmar tilvitnanir
Ég er viss um að sérhver RFQ pakki svari þeim spurningum sem plastframleiðandi þjónustuaðili verður annars að spyrja, vegna þess að hver fram og til baka bætir dögum við tímalínuna.
- Málteikning af þversniði sniðs með vikmörkum. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming, á Protolabs (2023), Ég flagga hvaða stærðir eru mikilvægar og hverjar geta flotið.
- Efnislýsing, þar á meðal plastefni gerð, bekk, lit, og hvaða UV sem er, loga, eða kröfur um snertingu við matvæli.
- Árlegt magn og pöntunartíðni, auk væntanlegrar hlutalengd og skurðarvikmörk.
- Hvort sem ég þarf sérsniðin verkfæri eða get notað lagersnið, og hvort aukaaðgerðir eins og klippa, gata, eða prentun gilda.
- Ásett verð, required delivery date, and destination for landed-cost accuracy.
- Application and industry context, which helps the supplier recommend the right material and process.
Next Steps to Start Your Project
With the scorecard filled in and the RFQ ready, I send it to two or three well-matched suppliers rather than blasting a dozen. I ask for a sample or first-article inspection before committing to full production, and I confirm the tooling ownership terms in writing. Moving from prototype to production this deliberately has consistently saved me from costly surprises. Directories such as Thomasnet (2024), which list and categorize US plastic extrusion manufacturers by capability and region, remain a useful starting point when I need to widen the field, and specialist custom extruders like SeaGate Plast illustrate how stock profiles and tubes can be fabricated into cost-effective custom parts.
Algengar spurningar
These are the questions buyers ask me most often when they are sourcing an extrusion partner. I have kept the answers concise and practical so you can act on them quickly.
How do I find a plastic extrusion companies factory near me or in the USA?
Start with capability, then filter by geography. I search supplier directories such as Thomasnet (2024) that categorize US plastic extrusion manufacturers by region and process, then cross-check each candidate’s material and volume fit. Choosing a domestic plastics manufacturer often pays off beyond convenience: the Reshoring Initiative (2023) reports that domestic sourcing can lower freight, skylda, og birgðahaldskostnaður, reducing total landed cost.
Hvað kostar sérsniðin plastpressun?
There are two cost layers. Custom profiles require a one-time tooling and die investment, after which per-part pricing depends on resin, veggþykkt, output rate, og rúmmáli. Stock extruded shapes skip the tooling charge entirely, which is why I default to them when a standard profile meets the requirement. Vegna þess að extrusion er samfelld, mikið magn ferli, unit costs typically fall as run length increases.
What is the difference between custom and stock extruded profiles?
Stock profiles are standard cross-sections a plastic profile manufacturer already produces, so they carry no tooling cost and short lead times, though the shape is fixed. Custom extrusion gives me a die designed to my exact profile cross-section, which is worth the tooling investment when the geometry, virka, or branding demands it. SeaGate Plast (2024) also notes that standard profiles and tubes can be fabricated into cost-effective custom parts, a useful middle path when a full custom die is not justified.
How do I choose the right material for my extruded part?
I match the resin to the application. PVC is among the most widely extruded plastics for profiles, pípa, og slöngur. HDPE, LDPE, and Polypropylene serve well in chemical-resistant and flexible applications. When I need clarity, höggstyrkur, or heat resistance, I move to engineering-grade plastics such as Polycarbonate, ABS, Akrýl (PMMA), or Nylon (PA), and I reserve PEEK for extreme thermal and mechanical demands. Sharing your application and environment with the supplier is the fastest route to the right recommendation.
What certifications should a quality extrusion supplier hold?
ISO 9001 is my baseline. The International Organization for Standardization (2015) describes it as the internationally recognized standard for quality management systems used across manufacturing, and it is the most widely adopted quality standard in the plastics sector. Depending on your industry, you may also require food-contact, læknisfræði, or flame-rating compliance, so confirm those specifics against your application.
What mistakes should I avoid when sourcing an extrusion partner?
The most common ones I see are chasing “stærsti” eða “best” claims without checking fit, sending incomplete drawings that produce inflated quotes, and underestimating tooling lead time. I also caution against ignoring MOQ alignment; a factory built for high-volume manufacturing may not welcome low-volume work, and a small shop may struggle with your scale. Match the supplier to the job rather than the reputation.
What are the next steps once I have chosen a supplier?
Send a complete RFQ, request a sample or first-article inspection, confirm tooling ownership in writing, and agree on a realistic schedule that separates tooling time from production time. Validating the part before full production is the single most reliable way I have found to move from prototype to production without expensive rework.
What Is a Plastic Extrusion Companies Factory and Why It Matters for B2B Buyers
When I evaluate a plastic extrusion companies factory for a client, Ég byrja á ferlinu sjálfu, because the process defines what a supplier can and cannot do for you. Plastpressun bræðir hráefni úr plasti og myndar það í samfellt snið með föstum þversniði (SeaGate Plast, 2024). That single sentence carries more purchasing implications than most buyers realize: the “fast þversnið” is why extrusion excels at long, uniform shapes like tubing, snyrta, og rásir, and it is also why you cannot expect the same complex three-dimensional geometry you would get from molding.
Skilgreining: What You Are Actually Buying
In practical terms, a plastic extrusion factory pushes softened resin through a shaped die to produce items such as custom plastic profiles, plastslöngur, and plastic sheet. Because this is a continuous extrusion process, it runs well for high-volume manufacturing and long production runs rather than one-off complex parts. The two categories I ask buyers to distinguish early Framleiðsla á pressuðu plasti are stock extruded shapes, which are ready-made and avoid tooling, and custom extruded plastic parts, which require a die designed to your cross-section. Standard extruded profiles and tubes can also be fabricated into cost-effective custom parts with quick-turnaround production (SeaGate Plast, 2024), which is a useful middle path when a full custom die is not justified.
Markaðssamhengi
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (Samtök plastiðnaðarins, 2023), so you are not sourcing from a niche trade. That scale matters for buyers: it means real competition among suppliers, redundancy if one plastic profile manufacturer cannot meet lead time, and a mature base of contract manufacturing and plastic fabrication services. It also means claims of being the “stærsti” eða “best” factory are marketing shorthand, not verified rankings. I treat those labels as prompts to ask about actual line capacity, vottorð, and reference customers rather than as evidence.
Key Applications and Materials
Material selection drives most of the outcome, so I map the resin to the application before shortlisting any supplier. Common choices I see across projects include:
- PVC — among the most widely extruded plastics globally, algengt í prófílum, pípa, og slöngur (Samtök plastiðnaðarins).
- HDPE and LDPE — durable, chemically resistant polyethylenes used for tubing, línuskip, and industrial profiles.
- Pólýprópýlen — lightweight and fatigue-resistant, frequently chosen for living hinges and chemical handling.
- ABS og pólýkarbónat — impact-resistant options for structural trim and enclosures; polycarbonate adds optical clarity and heat resistance.
- Akrýl (PMMA) — clarity and weatherability for lenses, sýnir, and lighting profiles.
- Nylon (PA) og kíkja — engineering-grade plastics for wear, hitastig, and mechanical demands; PEEK is the high-performance choice for aerospace and medical.
- TPE/TPU — flexible elastomers for seals, þéttingar, and grips, often produced through co-extrusion with a rigid substrate.
Co-extrusion deserves special attention because it lets a factory combine two materials in one profile, for example a rigid PVC body with a soft TPE sealing lip. If your part needs both stiffness and flexibility, confirm the supplier runs true co-extrusion rather than secondary assembly.
Why This Matters for B2B Buyers
Understanding the process changes how you write a request for quote. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs, 2023), so specifying injection-molding-tight tolerances on an extruded profile will either inflate your price or trigger a round of clarifying questions that delays the quote. On sustainability, thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency (US EPA, 2023), which gives you a legitimate lever for both cost and environmental goals when you discuss regrind percentages with a supplier.
How to Choose the Right Plastic Extrusion Companies Factory Supplier
Choosing a supplier is where I see the most avoidable mistakes, usually because buyers compare on unit price alone and ignore the cost drivers hiding behind that number. Below is the framework I use, built around evaluation criteria, red flags, and a due diligence checklist you can lift directly into your sourcing process.
Matsskilyrði söluaðila
I score candidates against five dimensions rather than a single quote:
- Capability match. Does the factory routinely run your resin and profile size? A plastic tubing supplier optimized for small-diameter medical tubing is not the same shop as one running large architectural profile extrusion.
- Gæðakerfi. ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu (ISO, 2015) and remains the most widely adopted quality standard in the plastics sector. Certification is not a guarantee of good parts, but its absence tells me to dig deeper into inspection practices.
- Tooling and die design. Ask who owns the die, how long die design and tooling take, and what happens to the tool if you leave. Ownership terms are frequently buried in fine print.
- Lead time and capacity. Confirm whether quoted lead times reflect current backlog or ideal conditions. Quick-turnaround production claims should be tied to a specific committed date.
- Financial and operational stability. A supplier that becomes your sole source for a critical profile is a risk if it is financially fragile.
Understanding the Cost Drivers
Transparency on cost structure separates a strong plastic profile manufacturer from an opaque one. Three drivers determine your total price, and I ask suppliers to break them out explicitly:
| Kostnaðarbílstjóri | Stock extruded shapes | Custom extruded profiles |
|---|---|---|
| Verkfæri / die investment | None — profile already exists | One-time die cost required before first run (leiðbeiningar um uppsprettu iðnaðarins, Thomasnet supplier guides) |
| Lágmarks pöntunarmagn (MOQ) | Lágt; buy by the length | Hærri; tied to setup and material changeover |
| Leiðslutími | Short — often shelf stock | Lengri; includes die fabrication and first-article approval |
| Per-unit price at volume | Fixed by catalog | Lower at high volume once tooling is amortized |
| Besta passa | Frumgerð, lágt hljóðstyrkur, standard cross-sections | Proprietary geometry, high-volume manufacturing, prototype to production scale-up |
Custom extrusion typically requires a one-time tooling investment, á meðan hlutabréfasnið forðast þennan kostnað (leiðbeiningar um uppsprettu iðnaðarins). Í minni reynslu, buyers who plan to scale from prototype to production should quote the custom die early even if they start with stock shapes, so the amortized per-unit price is visible before volumes ramp.
Red Flags I Watch For
- Refusal to share ISO or equivalent quality documentation, or vague answers about inspection frequency.
- Quotes with no tooling line item, which usually means the cost reappears later or the die is undersized.
- Unwillingness to provide references in your industry or sample parts.
- Tolerances promised on paper that are tighter than what continuous extrusion realistically holds — a sign the supplier may be overselling.
- “Largest” eða “best” claims with no capacity data, vottorð, or customer evidence behind them.
Gátlisti fyrir áreiðanleikakönnun
Before I commit to a Plastic Extrusion Companies Factory supplier, I confirm every item below in writing:
- Do you hold ISO 9001 or an equivalent, and can I see the certificate and scope?
- Which resins do you run in production, and can you handle my material — PVC, ABS, polycarbonate, HDPE, LDPE, pólýprópýlen, eða verkfræðieinkunn?
- What tolerances do you guarantee for this profile cross-section, and how are they measured?
- What is the tooling cost, leiðtíma, and MOQ, og hver á deyja?
- Do you offer co-extrusion and secondary fabrication in-house?
- What percentage of regrind is used, and how does that affect certification and appearance?
- Can you provide first-article inspection reports and material certifications?
- What is your realistic committed lead time given current backlog?
Find Plastic Extrusion Companies and Factories in the United States
Buyers frequently search for a plastic extrusion factory “nálægt mér” eða “in the USA,” and the location question is more strategic than it first appears. Domestic sourcing is not only about proximity; it changes your total landed cost and your supply-chain risk profile.
Where to Start Your Search
Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a practical first filter when you want to build a shortlist by material, ferli, or state. I pair directory research with capability-specific sources such as custom plastic extrusion manufacturer references to understand what a given shop actually produces before I reach out. The goal at this stage is a shortlist of five to eight candidates whose capabilities genuinely match your resin and profile, not a long list of names. Plastpressufyrirtæki
Key Considerations for Domestic Sourcing
Endurheimt og innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023). For extruded parts, which are often bulky and low in value density, freight is a meaningful line item, so a domestic plastics manufacturer closer to your assembly point can offset a higher unit price. I weigh three factors:
- Heildar löndunarkostnaður, ekki einingarverð. Add freight, skylda, and the carrying cost of the safety stock you need to cover long overseas transit.
- Communication and design iteration. Domestic time-zone alignment speeds up die design and tooling revisions during the prototype-to-production phase.
- Supply resilience. Shorter lines reduce exposure to port delays and long lead-time shocks.
Interpreting “Largest” og “Best” Factory Claims
Location searches often surface superlatives, and I treat them skeptically. “Largest” tells you nothing about whether a factory runs your material or holds your tolerances. Í staðinn, I convert vague claims into verifiable questions: How many extrusion lines run my resin family? What is your on-time delivery rate? Which certifications do you hold? A smaller shop that specializes in your profile is frequently a better partner than a large one for which your job is an afterthought.
Practical Tips and Industry Context
A few habits have consistently saved my clients time and money. Fyrst, request stock extruded shapes for early validation before investing in a custom die — it lets you test fit and function cheaply. Í öðru lagi, share a dimensioned drawing with realistic extrusion tolerances up front so quotes are comparable. Þriðja, confirm the supplier’s regrind policy, since recyclable thermoplastics and regrind reuse improve material efficiency (US EPA, 2023) but can affect appearance on cosmetic parts. Loksins, remember that plastic extrusion is a continuous, high-volume process well suited to long production runs, so it rewards buyers who can consolidate demand and forecast accurately. Within the mature US plastics manufacturing base (Samtök plastiðnaðarins, 2023), you have room to be selective — use it, and let a structured checklist rather than a headline claim decide your Plastic Extrusion Companies Factory supplier.
Locate a plastic extrusion factory near my location
When buyers ask me how to find a plastic extrusion factory nearby, I remind them that “nálægt mér” is really shorthand for two goals: shorter freight lanes and easier communication. Extrusion melts raw plastic material and forms it into a continuous profile with a fixed cross-section (SeaGate Plast, 2024), and because that continuous extrusion process runs at high volume, the finished product is often bulky and freight-sensitive. Í minni reynslu, the cost of moving extruded plastic parts across the country can quietly erode the price advantage of a distant supplier, so location genuinely matters.
Key considerations for local sourcing
I start every local search by matching capability to geography rather than proximity alone. A plastic profile manufacturer two states away with the right die design and tooling almost always beats a closer shop that cannot hold your profile cross-section. I evaluate three things in order: the materials they run (PVC, ABS, polycarbonate, HDPE, LDPE, pólýprópýlen, akrýl, and engineering-grade resins such as nylon or PEEK), the processes they offer (snið útpressun, útpressun úr plastplötum, slöngur, og co-extrusion), and their quality systems. ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu (ISO, 2015), so I treat certification as a baseline filter, ekki bónus.
Practical tips to find and vet a factory
Thomasnet supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a reliable starting point for a location-based shortlist. Þaðan, I qualify each candidate with a consistent set of questions before I ever request a quote.
My local supplier vetting checklist
- Which resins do you extrude in-house, and can you run regrind for material efficiency?
- Do you offer co-extrusion or dual-durometer profiles if my part needs a soft-touch or barrier layer?
- What tolerances can you hold, and how do you document them?
- Are you ISO 9001 vottað, and can you share a recent audit summary?
- What is your typical lead time from approved die to first article?
- Do you provide plastic fabrication services (klippa, gata, borun) so I receive finished parts, not just stock lengths?
Iðnaðarsamhengi
Domestic proximity is more strategic than it looks. Endurheimt og innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023). Because the US plastics industry is a major contributor to domestic manufacturing shipments and employment (Samtök plastiðnaðarins, 2023), most regions have a viable domestic plastics manufacturer within a reasonable freight radius. I tell buyers that “nálægt mér” should mean near enough to control landed cost and lead time, which is often a regional rather than a strictly local decision.
Identify the largest plastic extrusion companies in the US
Buyers frequently ask me to point them to the “stærsti” plastpressufyrirtæki, and my first move is always to define what “stærsti” means for their project. Size can describe revenue, plant footprint, number of extrusion lines, or annual resin throughput, and those metrics do not always move together. A plastic extrusion companies factory supplier with enormous pipe capacity may be the wrong fit for a low-volume acrylic profile, so I interpret scale through the lens of the specific job.
Key considerations when “stærsti” skiptir máli
Scale earns its keep on long production runs. Plastic extrusion is a continuous, high-volume process well suited to long production runs, so the largest producers shine when you need millions of feet of PVC profile or HDPE pipe on a predictable schedule. PVC er meðal útbreiddasta plastsins í heiminum, almennt notað í sniðum, pípa, og slöngur, which is why the biggest players tend to concentrate capacity there. If your program is high-volume and standardized, a large plastic profile manufacturer offers redundancy, buffer inventory, and pricing leverage. If your program is small or highly custom, that same scale can translate into higher minimums and less flexibility.
Practical tips for evaluating scale claims
I never take a marketing claim of “stærsti” at face value. Í staðinn, I ask for concrete indicators: number of extrusion lines by size class, resins run at volume, and the split between stock extruded shapes and custom work. A large firm quoting a wholesale program should be able to show quick-turnaround production capacity, secondary plastic fabrication services, and a documented MOQ structure. The table below summarizes how I weigh large versus specialized suppliers.
Large versus specialized extrusion suppliers
| Þáttur | Largest producers | Specialized suppliers |
|---|---|---|
| Besta passa | Hátt hljóðstyrkur, standardized runs (pípa, PVC snið) | Custom plastic profiles, engineering-grade resins |
| Lágmarks pöntunarmagn | Higher MOQ to justify line time | Lower MOQ, more flexible |
| Verkfærakostnaður | Amortized across large volumes | One-time die cost more visible per unit |
| Leiðslutími | Predictable, buffered by capacity | Breytilegt, project-dependent |
| Material range | Commodity resins (PVC, HDPE, LDPE, PP) | Specialty resins (PC, PMMA, PA, KIKIÐ, TPE/TPU) |
| Co-extrusion | Common on standard lines | Often available for niche multi-layer parts |
Iðnaðarsamhengi
The largest US extruders are anchored in commodity, freight-heavy products where continuous, high-volume manufacturing rewards efficiency. Custom extrusion typically requires a one-time tooling or die investment, á meðan hlutabréfasnið forðast þennan kostnað, so large producers often lead with catalogs of stock extruded shapes. I remind buyers that “stærsti” is a useful signal for reliability and capacity, but it is not a proxy for quality or fit. The right size is the one that matches your volume, efni, and tolerance needs.
Discover the best-rated plastic extrusion manufacturers
“Best-rated” is the claim I scrutinize most, because ratings can reflect genuine performance or simply strong marketing. Í minni reynslu, the manufacturers worth shortlisting are the ones that make their quality measurable. I look past star counts and testimonials for evidence I can verify: vottorð, documented tolerances, rekjanleika efnis, and a track record of moving projects from prototype to production without surprises.
Key considerations for judging quality
Quality management is the foundation. ISO 9001 is the most widely adopted quality management standard, used across manufacturing sectors including plastics, so I treat it as table stakes for a best-rated plastic extrusion companies factory manufacturer. Beyond certification, I assess how a supplier handles tolerances. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs, 2023), and the best manufacturers explain that reality up front rather than overpromising. A shop that gives me realistic tolerance ranges and a clear inspection plan earns more trust than one quoting numbers it cannot hold.
Practical tips for choosing the best-rated supplier
I use a material selection framework tied to the application. The resin drives the manufacturer, ekki öfugt.
- PVC — profiles, pípa, and tubing where cost and rigidity matter.
- ABS og polycarbonate — impact-resistant parts; polycarbonate adds clarity and heat tolerance.
- HDPE and LDPE — chemical resistance and flexibility for tubing and liners.
- Pólýprópýlen — lightweight parts needing fatigue and chemical resistance.
- Akrýl (PMMA) — optical clarity for lighting and display profiles.
- Nylon (PA) og kíkja — engineering-grade parts under mechanical or thermal stress.
- TPE/TPU — flexible seals and gaskets, often via co-extrusion.
Once the material is set, I confirm the supplier offers the matching process, whether that is profile extrusion, útpressun úr plastplötum, or resin extrusion with co-extrusion for multi-layer parts. Hægt er að búa til staðlaða pressuðu snið og rör í hagkvæma sérsniðna hluta með skjótum viðsnúningi (SeaGate Plast, 2024), so I favor manufacturers that pair extrusion with in-house fabrication and prototype-to-production support. For a working example of custom capability and stock profile options, I point buyers to references such as SeaGate Plast.
Iðnaðarsamhengi
The best-rated manufacturers increasingly compete on sustainability alongside quality. Thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency (US EPA, 2023), so I ask top candidates how they manage scrap and regrind. A manufacturer that documents its quality system, states honest tolerances, and runs an efficient material loop tends to be “best-rated” for reasons that hold up under a plant visit. That is the standard I apply, and it is the one I recommend every buyer use before committing to a contract manufacturing partner.
Understand how the plastic extrusion manufacturing process works
Þegar ég met framleiðanda plastprófíla, I start by making sure the buyer understands what actually happens on the shop floor. Plastpressun bræðir hráefni úr plasti og myndar það í samfellt snið með föstum þversniði (SeaGate Plast, 2024). That single sentence carries most of what you need to know: the process is continuous, the cross-section is constant along the length, and the shape is defined by tooling rather than by a closed mold.
Kjarnastig hins samfellda útpressunarferlis
Í reynd, Ég lýsi verkflæðinu í fimm þrepum. Fyrst, kvoðakögglar eru færðir í tank. Í öðru lagi, upphituð tunna með snúningsskrúfu bráðnar og þrýstir efnið, þess vegna kalla iðkendur það oft plastútpressun. Þriðja, bráðnu fjölliðunni er þvingað í gegnum deyja sem kemur á fót þversniði sniðsins. Í fjórða lagi, extrudate er kælt í vatnsbaði eða loftrikki svo það haldi rúmfræði sinni. Fimmta, dráttarvélar draga hlutinn á jöfnum hraða áður en sag eða skeri stærðir hann. Því ekkert stoppar á milli stiga, aðferðin er raunverulega samfellt útpressunarferli frekar en hringrás-fyrir-lotu.
Hvers vegna vikmörk eru frábrugðin sprautumótun
Eitt atriði sem ég vek snemma upp við verkfræðiteymi: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs hönnunarauðlindir, 2023). This is not a defect. It reflects the physics of pulling a hot polymer through open tooling and cooling it under tension. If your extruded plastic parts need tight dimensional control on a specific feature, plan for secondary machining or specify that feature as a fabrication step rather than expecting the die alone to hold it.
Co-extrusion and profile extrusion variants
Profile extrusion covers the custom cross-sections most buyers picture: rásir, þéttingar, snyrtingar, og byggingarform. Co-extrusion runs two or more materials through the die at once, which lets you combine, til dæmis, a rigid PVC body with a flexible TPE/TPU sealing lip in a single pass. I find co-extrusion is where a capable factory earns its rate, because it removes a downstream assembly step and improves seal performance. Plastic sheet extrusion and tubing use the same fundamentals with different die and downstream setups.
Industry context and material efficiency
Extrusion suits high-volume manufacturing because it is inherently a continuous, high-volume process well suited to long production runs. Once a die is dialed in, output scales with line speed and run time. It also has a reasonable sustainability story: thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency (US EPA, 2023). Í minni reynslu, asking a supplier how they handle regrind tells you a lot about both their cost discipline and their process control.
Compare custom vs stock plastic extrusion suppliers
The most consequential sourcing decision I help buyers make is custom versus stock. It drives your tooling cost, lágmarks pöntunarmagn, and lead time all at once. The right answer depends on how closely a standard shape fits your application and how much volume you expect to run.
What separates the two paths
Sérsniðin útpressun krefst venjulega fjárfestingar í einu sinni í verkfærum og deyja, á meðan hlutabréfasnið forðast þennan kostnað. Hægt er að búa til staðlaða pressuðu snið og rör í hagkvæma sérsniðna hluta með skjótum viðsnúningi (SeaGate Plast, 2024). So there is a middle path many buyers miss: start from a stock extruded shape and fabricate it, capturing part of the customization benefit without paying for a new die.
Cost drivers to model before you request a quote
When I build a sourcing model, I separate three drivers so the numbers stay honest:
- Die design and tooling: a one-time cost on custom work, typically amortized across your first order or two.
- MOQ: custom lines carry higher minimums to justify setup and purge material; stock shapes can ship in small quantities.
- Leiðslutími: stock ships quickly; custom adds die fabrication and first-article approval before production begins.
Comparison table: custom vs stock extrusion
| Þáttur | Sérsniðin útpressun sniðs | Stock extruded shapes |
|---|---|---|
| Verkfærakostnaður | One-time die investment required | Engin |
| Lágmarks pöntunarmagn | Hærri, to amortize setup | Lágt, often cut-to-length |
| Leiðslutími | Lengri (deyja byggingu + fyrstu grein) | Quick-turnaround production |
| Dimensional fit | Exact cross-section to spec | Nearest standard, plus fabrication |
| Best fyrir | Sustained volume, unique geometry | Frumgerðir, lágt hljóðstyrkur, near-fit needs |
| Unit price at scale | Lækka þegar verkfæri eru afskrifuð | Higher per unit for heavy customization |
A vetting checklist for either path
Whether you pursue a custom plastic profile manufacturer or a stock plastic tubing supplier, I ask the same core questions. Is the shop certified to ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015)? ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics, so its absence is worth a direct conversation. Beyond certification, I ask:
- Which resins do you run in-house, and can you handle engineering-grade plastics like polycarbonate, nylon (PA), eða kíkja?
- Do you offer co-extrusion and downstream plastic fabrication services?
- How do you document tolerances and first-article inspection?
- What is your true MOQ, and how is tooling amortized on the initial order?
- Can you support the move from prototype to production without re-tooling?
Location intent: near me and in the USA
Buyers frequently search for a Plastic Extrusion Companies Factory supplier “nálægt mér” or a domestic plastics manufacturer in the USA. Two resources help here. Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is a practical starting point for shortlisting. And the case for domestic sourcing is more than convenience: reshoring and domestic sourcing can reduce total landed cost by lowering freight, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023). I treat “stærsti” og “best” factory claims with skepticism; capability fit for your specific resin, umburðarlyndi, and volume matters far more than a superlative on a homepage.
Learn what products can be made through plastic extrusion
Extrusion produces a broader range of products than most buyers expect, and the material you choose shapes both what is possible and what it costs. I organize my recommendations around a material selection framework tied to application and industry rather than a generic parts list.
Common extruded product categories
The workhorse outputs are custom plastic profiles, slöngur, blað, rásir, snyrtingar, þéttingar, og byggingarform. Anything with a consistent profile cross-section along its length is a candidate. PVC er meðal útbreiddasta plastsins í heiminum, almennt notað í sniðum, pípa, og slöngur (Samtök plastiðnaðarins). That prevalence is why so many stock extruded shapes are available in PVC first.
Material selection framework
Here is how I match resins to needs across the polymers you will encounter most often:
- PVC: hagkvæmt, rigid or flexible, strong for profiles, pípa, og slöngur.
- ABS: tough and impact-resistant, common in housings and trims.
- Pólýkarbónat: high impact strength and clarity for glazing and guards.
- HDPE and LDPE: chemically resistant polyolefins for tubing, línuskip, and low-cost profiles; HDPE brings more rigidity, LDPE more flexibility.
- Pólýprópýlen: ljós, efnafræðilega ónæmur, and fatigue-tolerant for living hinges and profiles.
- Akrýl (PMMA): optical clarity for display and lighting profiles.
- Nylon (PA): wear resistance and strength for mechanical parts.
- KIKIÐ: high-temperature, chemically robust engineering-grade plastic for demanding aerospace and medical work.
- TPE/TPU: flexible elastomers ideal for seals and soft-touch co-extruded lips.
Industry applications
Construction relies on PVC and ABS profiles for window frames, snyrtingar, og kanta. Medical and lab work uses acrylic, pólýprópýlen, and PEEK tubing and channels. Electronics and appliances draw on polycarbonate and ABS housings. Industrial and fluid-handling lines lean on HDPE and nylon. Mapping your industry to these resins early keeps the quoting conversation focused and avoids specifying an over-engineered material you do not need.
Practical tips for moving from concept to production
Í minni reynslu, three habits keep extrusion projects on schedule. Fyrst, prototype from stock shapes where the geometry allows, then commit to custom tooling only after the design is validated, which protects your die investment. Í öðru lagi, specify tolerances by feature rather than blanket-tightening the whole profile, since that respects the process and controls cost. Þriðja, confirm your supplier can carry the part from prototype to production on the same line, so scale-up does not force a re-quote. Handled this way, extrusion delivers custom parts economically, with the quick turnaround that makes the process attractive in the first place.
For a deeper look at fabricating cost-effective custom parts from standard and custom profiles, I point buyers to SeaGate Plast’ extrusion overview.
Bringing Your Extrusion Sourcing Strategy Together
After walking through capabilities, efni, and vetting criteria, the through-line I keep returning to is this: choosing among plastic extrusion companies and factories is less about finding the “stærsti” eða “best” name and more about matching a supplier’s real strengths to your specific part, bindi, og tímalína. A continuous, high-volume manufacturing process rewards long production runs, but the same shop that excels at a million linear feet of PVC profile may not be the partner I want for a low-volume PEEK prototype. Í minni reynslu, buyers who define the problem precisely before they request quotes get sharper pricing and fewer surprises downstream.
Material selection sits at the center of every good decision. Whether the application calls for rigid PVC or ABS in structural profiles, polycarbonate or acrylic (PMMA) fyrir sjónrænan skýrleika, HDPE og LDPE fyrir efnaþol, pólýprópýlen fyrir lifandi lamir, nylon (PA) for wear surfaces, or TPE/TPU for flexible seals, the resin drives tooling, vikmörk, og kostnaður. Extrusion melts raw plastic and forms it into a continuous profile with a fixed cross-section (SeaGate Plast, 2024), og stöðluð pressuð snið og rör er hægt að búa til hagkvæma sérsniðna hluta með skjótum viðsnúningi (SeaGate Plast, 2024). That combination of stock shapes and custom profile extrusion, sometimes paired with co-extrusion for multi-material geometry, is what makes the process so versatile from prototype to production.
On the commercial side, I always separate one-time and recurring costs. Custom extrusion typically carries a one-time tooling and die investment, while stock profiles avoid it, so the die design and tooling decision shapes the whole business case. Domestic sourcing deserves a second look too: reshoring and domestic sourcing can reduce total landed cost by lowering freight, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023), sem oft minnkar bilið sem aflandsverðlagning eininga virðist opna. Og vegna þess að hitauppstreymi sem notað er við útpressun er endurvinnanlegt og endurnýting endurmala bætir skilvirkni efnisins (U.S. EPA, 2023), Gæðamiðaður innlendur plastframleiðandi getur stutt bæði kostnaðar- og sjálfbærnimarkmið í einu.
Gæðakerfi eru lokasían sem ég beiti. ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu (ISO, 2015), og það er áfram útbreiddasta viðmiðið sem ég leita að þegar ég ber saman a sérsniðin plastpressuframleiðandi gegn jafnöldrum sínum. Paraðu það við raunhæfar væntingar um nákvæmni, þar sem útpressunarþol eru almennt lausari en sprautumótun vegna rýrnunar efnis og stöðugrar mótunar (Protolabs, 2023), og þú ert með jarðtengda ramma til að meta hvaða plastprófílframleiðanda eða plastslöngubirgja sem er.
Sérfræðingar innsýn
| Lykilatriði | Skýring |
|---|---|
| Passaðu ferli við hljóðstyrk, ekki til orðspors | Continuous extrusion is a high-volume process best suited to long production runs, so I weigh a factory’s real strengths against my order size rather than chasing “stærsti” eða “best” claims. |
| Separate tooling from unit price | Custom profiles require a one-time die investment while stock extruded shapes avoid it; understanding this split keeps the true cost of custom plastic profiles from hiding inside a quoted per-foot rate. |
| Verify quality before precision expectations | ISO 9001 vottun (ISO, 2015) signals a managed process, and I set tolerance expectations knowing extrusion runs looser than injection molding (Protolabs, 2023). |
Hagnýt uppspretta ráð fyrir B2B kaupendur
- Define the part before you shop. Document the profile cross-section, plastefni (PVC, ABS, polycarbonate, HDPE, pólýprópýlen, or an engineering-grade plastic), árlegt magn, and target tolerance so every plastic extrusion companies factory supplier quotes against the same brief.
- Ask for tooling, MOQ, and lead-time numbers separately. Request the die cost, lágmarks pöntunarmagn, and quoted lead time as distinct line items to compare custom extrusion and stock profiles on equal footing.
- Confirm the quality system in writing. Ask for a current ISO 9001 certificate and the inspection points used on extruded plastic parts, rather than accepting a general quality claim.
- Weigh domestic sourcing on total landed cost. Compare a domestic plastics manufacturer against offshore options using freight, skylda, og birgðahaldskostnaður, ekki einingaverð eitt og sér (Reshoring Initiative, 2023).
- Test the relationship with a small run. Move from prototype to production in stages so you validate quick-turnaround performance and communication before committing to high-volume manufacturing.
- Use supplier directories as a starting list, ekki stuttlisti. Directories such as Thomasnet (2024) help you locate regional plastic fabrication services, but I still vet capability, efni, and certification directly with each shop.
Algengar spurningar
How do I find plastic extrusion companies or a factory near me?
When I evaluate location intent, I start by mapping suppliers against my shipping lanes rather than pure geographic proximity. A plastic profile manufacturer two states away with the right die design and tooling capability often beats a closer shop that lacks my resin. I use supplier directories that list and categorize US plastic extrusion manufacturers by capability and region to build a shortlist, then verify with a plant visit or video walkthrough. Thomas directories are a practical starting point for this (Thomasnet, 2024, thomasnet.com). Í minni reynslu, “nálægt mér” should mean short, predictable lead times and low freight, not just a nearby ZIP code.
What should I look for in plastic extrusion manufacturers in the USA?
Fyrir innlenda uppsprettu, I weigh three things: certified quality, material breadth, og heildar löndunarkostnaður. A domestic plastics manufacturer can reduce total landed cost by lowering freight, skylda, og birgðahaldskostnaður (Reshoring Initiative, 2023, reshorenow.org), which often narrows the gap with offshore quotes once you account for the full picture. The US plastics industry is also a major contributor to domestic manufacturing shipments and employment (Samtök plastiðnaðarins, 2023), so the supplier base is deep. I confirm they run the resins I need, from commodity grades like PVC, HDPE, LDPE, and polypropylene to engineering-grade plastics such as polycarbonate, nylon (PA), og kíkja.
How do I choose the right plastic extrusion supplier for my project?
I treat supplier selection as a vetting checklist, not a gut call. The concrete questions I ask every candidate:
- Do you hold ISO 9001 vottun, the internationally recognized standard for quality management systems (ISO, 2015)?
- Which resins and profiles do you run in production, and do you offer co-extrusion?
- What are your tolerances, and how do you handle profile cross-section validation?
- What is your minimum order quantity (MOQ), tooling lead time, and production lead time?
- Can you support the full path from prototype to production and quick-turnaround production for reorders?
Industrial Plastic Extrusion Parts The biggest mistake I see buyers make is choosing on unit price alone and ignoring tooling cost, MOQ, and lead-time risk. Those drivers usually decide whether a program is actually profitable.
What is the difference between custom and stock plastic extrusions?
Stock extruded shapes are standard profiles and tubes a supplier already produces, so you skip tooling and buy off the shelf. Custom extrusion requires a one-time tooling and die investment to create your unique profile cross-section. Viðskiptin eru einföld: stock plastic extrusions minimize upfront cost and lead time, while custom plastic profiles fit your exact geometry. Sérstaklega, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (SeaGate Plast, 2024, seagateplastics.com), so I often prototype with stock shapes before committing to a die.
How should I read “stærsti” og “best” plastic extrusion factory claims?
I read those labels with healthy skepticism. “Largest” usually reflects capacity or revenue, which matters for high-volume manufacturing but tells me nothing about fit for a low-volume, tight-tolerance job. “Best” is subjective marketing unless it is backed by certifications, tilvísanir, and capability data. My rule: rank suppliers against my own requirements, not against a generic superlative. The largest plastic extrusion company on a list may be the wrong contract manufacturing partner for a specialty acrylic (PMMA) or TPE/TPU part, while a mid-size specialist nails it.
What are plastic extrusion profiles, and how are they made?
A profile is a continuous shape with a fixed cross-section. Plastpressun bræðir hráefni úr plasti og myndar það í samfellt snið með föstum þversniði (SeaGate Plast, 2024). Because it is a continuous forming process, resin extrusion is well suited to long production runs and high-volume manufacturing. It also supports plastic sheet extrusion and tubing. One thing I always plan around: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs hönnunarauðlindir, 2023), so I set tolerance expectations early with the plastic tubing supplier or profile shop.
Which plastic material should I choose for my extruded parts?
I anchor material selection to the application, not habit. PVC is among the most widely extruded plastics globally and is common in profiles, pípa, og slöngur. For impact and appearance, I look at ABS or polycarbonate; for chemical resistance and living hinges, pólýprópýlen; for outdoor and clarity, akrýl (PMMA); and for demanding thermal or wear conditions, nylon (PA) eða kíkja. I also confirm recyclability up front, since thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (US EPA, 2023). Matching resin to service environment prevents the costly redesigns I have watched derail otherwise solid programs.
What drives the cost of extruded plastic parts?
Three levers move price more than anything else. Fyrst, verkfæri: a custom die is a one-time investment that stock profiles avoid entirely. Í öðru lagi, MOQ and run length, since extrusion rewards volume and unit cost drops as quantities rise. Þriðja, efnis einkunn, where engineering-grade plastics and specialty resins cost well above commodity options. When I request a quote, I ask suppliers to break out tooling, einingarverð, and secondary plastic fabrication services separately so I can compare offers on equal terms and identify where the real cost lives.
Heimildir
- Plastpressun bræðir hráefni úr plasti og myndar það í samfellt snið með föstum þversniði. — SeaGate Plast (2024)
- Hægt er að búa til staðlaða pressuðu snið og rör í hagkvæma sérsniðna hluta með skjótum viðsnúningi. — SeaGate Plast (2024)
- ISO 9001 er alþjóðlega viðurkenndur staðall fyrir gæðastjórnunarkerfi sem notuð eru í framleiðslu. — Alþjóðastaðlastofnunin (2015)
- The US plastics industry is a major contributor to domestic manufacturing shipments and employment. — Samtök plastiðnaðarins (2023)
- Endurheimt og innlend uppspretta getur dregið úr heildarkostnaði við land með því að lækka vöruflutninga, skylda, and inventory carying costs. — Reshoring Initiative (2023)
- Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming. — Protolabs hönnunarauðlindir (2023)
- Thermoplastics used in extrusion are recyclable, and regrind reuse improves material efficiency. — Umhverfisverndarstofnun Bandaríkjanna (2023)
- Thomas suplier directories list and categorize US plastic extrusion manufacturers by capability and region. — Thomasnet (2024)
- Plastic extrusion is a continuous, high-volume process well suited to long production runs, per general industry manufacturing references (SPI/Plastics Industry Association overview). — Planning analysis
- PVC er meðal útbreiddasta plastsins í heiminum, almennt notað í sniðum, pípa, og slöngur (Samtök plastiðnaðarins). — Planning analysis