

Nā mea lawe nui
- Hoʻoheheʻe ʻia ka extrusion plastik i ka resin maka a hoʻolilo iā ia i kahi kikoʻī mau me kahi ʻāpana keʻa paʻa, he mea kūpono ia i ka lōʻihi, holo hana nui (ʻO SeaGate Plastics, 2024).
- I koʻu loiloi ʻana i kahi mea hana kiʻi plastik, Hoʻokaʻawale wau custom extrusion, e lawe ana i hoʻokahi manawa make a me nā mea hana hoʻolimalima, mai nā ʻano kiʻi i hoʻokuʻu ʻia e hoʻokuʻu i kēlā kumukūʻai mua (ʻO Thomasnet alakaʻi alakaʻi, 2024).
- ʻO ke koho ʻana i nā mea āpau e alakaʻi i nā mea āpau: Hoʻohālikelike au i ka noi i ka polymer kūpono, inā he PVC ia no ka paipu a me nā profiles, ʻO ABS a i ʻole polycarbonate no ka ikaika hopena, HDPE a me LDPE no ke kū'ē kemika, polypropylene no nā ʻeke ola, acrylic (PMMA) no ka akaka, a i ʻole naylon pae ʻenekinia (PA) a PEEK no nā ʻāpana koi.
- ʻO PVC kekahi o nā plastic extruded loa i ka honua, maʻamau ma nā ʻaoʻao pili, paipu, a me ka paipu, ʻo ia ke kumu i helu ai nā mea hoʻolako iā ia ma ke ʻano he mana paʻamau (ʻAhahui ʻOihana Pākīpika, 2023).
- ʻOi aku ka maʻalahi o ka hoʻomanawanui ʻana ma mua o ka hoʻoheheʻe ʻia ʻana ma muli o ka emi ʻana o nā mea a me ka hoʻomau mau ʻana, no laila ke hoʻolālā mua nei au i ka hoʻomanawanui ma mua o ka manaʻo ʻana i ka pololei o ka ʻāpana (Protolabs, 2023).
- Hana wau iā ISO 9001 ma ke ʻano he hōʻailona kumu o kahi ʻōnaehana hoʻokele maikaʻi, ʻaʻole hōʻoia, a hoʻohui pū me kahi papa helu hoʻopaʻapaʻa e uhi ana i ka hiki, hiki i ka co-extrusion, a me ka manawa alakai (ISO, 2015).
- No ka manao wahi, ʻO ka loaʻa ʻana mai kahi mea hana plastics home hiki ke hoʻohaʻahaʻa i ka nui o ke kumu kūʻai ma ka ʻoki ʻana i ka ukana, dute, a me nā koina lawe waihona, he kiko kūpono ke kaupaona ʻana me ke kumu kūʻai ʻāpana wale nō (Hoʻomaka hou ʻana, 2023).
- Hiki ke hoʻohana hou ʻia nā Thermoplastics i hoʻohana ʻia i ka extrusion, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai, ʻo ia kaʻu e hoʻopili ai i nā kūkākūkā kumukūʻai a me ka hoʻomau (EPA US, 2023).
- Nā koi like “nui loa” a i ʻole “maikaʻi loa” ʻano liʻiliʻi ka hale hana me ka ʻole o ka pōʻaiapili, no laila ke kuhikuhi nei au i nā mea hoʻolako i ke kumukūʻai mea hana, MOQ, hana hoʻololi wikiwiki, a me ke kākoʻo prototype-to-production ma kahi.
He aha nā ʻoihana a me nā hale hana Plastic Extrusion i hana maoli ai
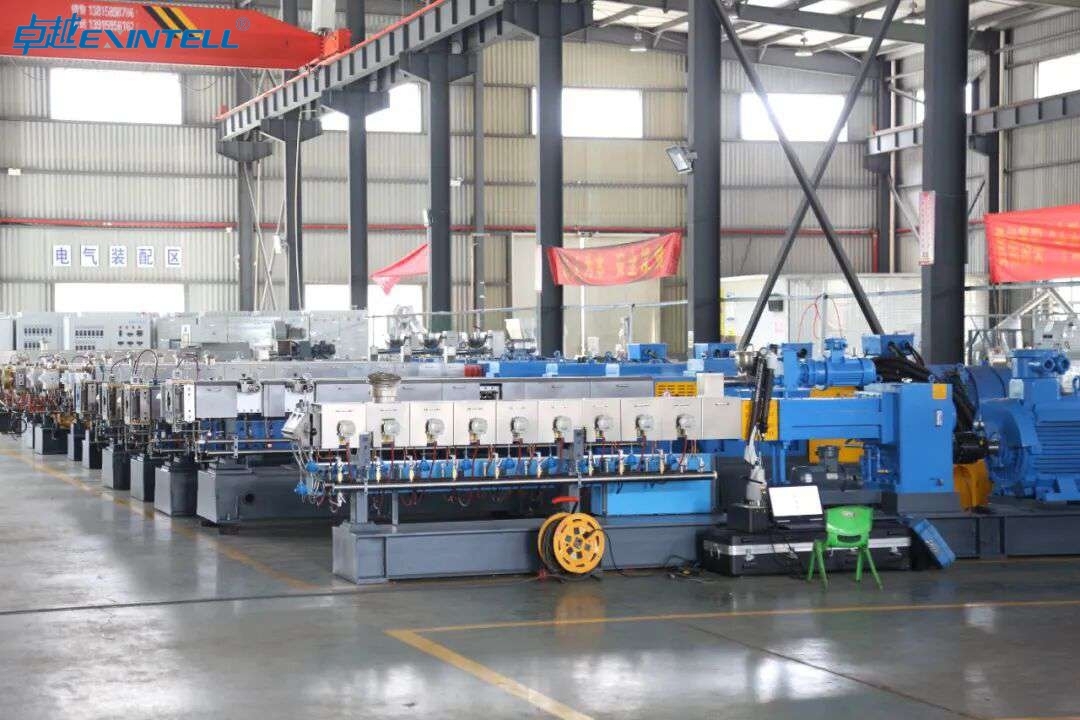
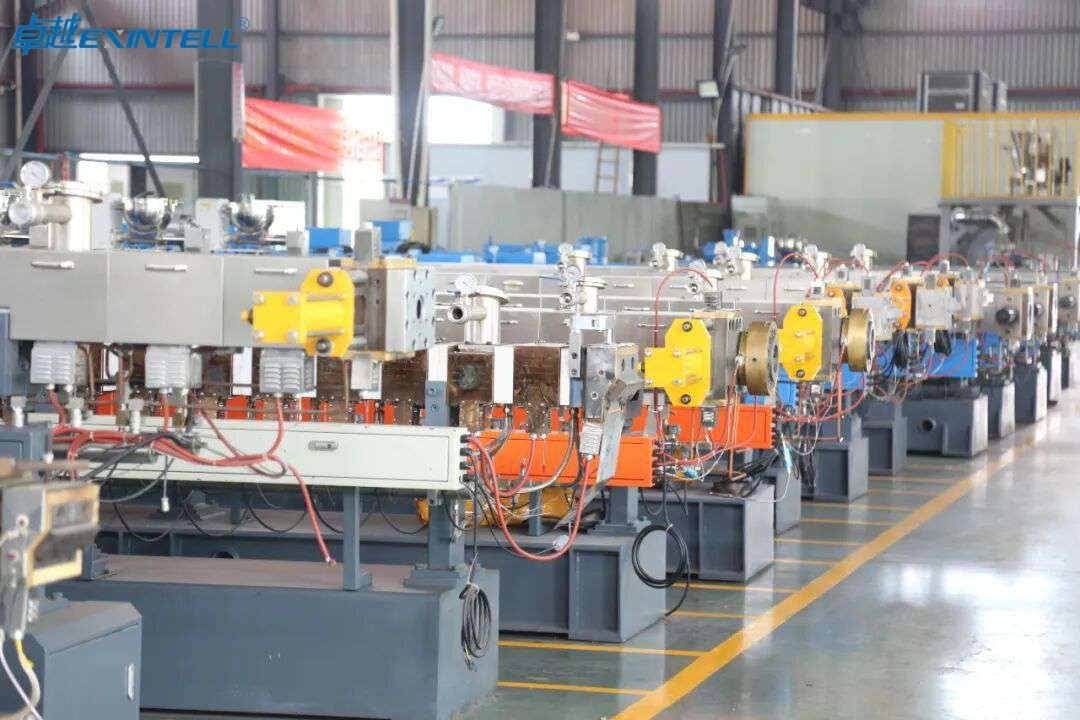
Ke loiloi au i ka mea hoʻolako no ka mea kūʻai, Hoʻomaka wau ma ka wehewehe ʻana i ka ʻōlelo “extrusion” wehewehe maoli ma ka papahele hale kūʻai. Hoʻoheheʻe ʻia ka mea hoʻoheheʻe ʻia i ka plastik maka a hoʻoheheʻe ʻia i loko o kahi ʻano hoʻomau me ka ʻāpana keʻa paʻa (ʻO SeaGate Plastics, 2024). ʻO kēlā ʻōlelo hoʻokahi e lawe nui i ke kaumaha: hoʻomau ka hana ma mua o ka pana ʻana, a ua wehewehe ʻia ka geometry e kahi ʻāpana ʻāpana ʻelua e holo i ka lōʻihi piha o ka ʻāpana. ʻO ia ke kumu kūpono ia i nā holo hana lōʻihi a me ka hana nui-nui, a he aʻo ʻokoʻa maoli ia mai ka hoʻoheheʻe ʻana a i ʻole ka mīkini.
Ma ka hana, “resin extrusion” ʻo ia ka ʻenekini ma hope o ʻekolu ʻohana puka ākea aʻu i ʻike ai i noi pinepine ʻia:
- Nā moʻolelo - nā ʻaoʻao plastik maʻamau me kahi ʻāpana i wehewehe ʻia, mai nā ala maʻalahi a me nā ʻoki ʻoki a hiki i nā ʻano lumen paʻakikī. ʻO kēia kahi e ʻike maoli ai ka extrusion profile a me ka co-extrusion.
- Paipu — poepoe, oval, a me multi-lumen tube i hoʻohana ʻia i ka lāʻau lapaʻau, lawelawe wai, a me nā noi pneumatic, loaʻa mai kahi mea hoʻolako paipu plastik kūikawā.
- Pepa - ka hoʻokuʻu ʻia ʻana o ka pepa plastik no nā panela, nā laina laina, a me ka waihona thermoforming, i hana ʻia ma o ka ʻōpala paʻa a me ka ʻōwili pahu.
Nā mea hana, Nā hale hana, ʻAʻole like nā mea hoʻolaha
Hoʻohana pinepine nā mea kūʻai i kēia mau huaʻōlelo, a ʻo ia ke kumu o ka manawa. Eia kaʻu e hoʻokaʻawale ai iā lākou:
- A mea hana a hale hana nona nā laina extrusion, oki i kona make ponoi, a hoʻomalu i ke kaʻina hana mai ka resin a i ka ʻāpana pau. ʻO kēia ka mea āu e makemake ai no ka mea hana maʻamau, paʻa kaʻina hana, a i ʻole nā mea plastik pae ʻenekinia.
- A mea kūʻai aku a kūʻai aku paha nā mea kūʻai a me nā moku i nā ʻano maʻamau akā ʻaʻole i holo ka laina. Maikaʻi no nā kiʻi extruded stock a me nā hoʻonohonoho hou wikiwiki, emi mai no ka hana ma'amau.
- A mea hana hana hiki ke kūʻai aku i nā profile stock a me ka mīkini, wiliwili, a i ʻole e hōʻuluʻulu iā lākou i loko o nā lawelawe hana i hoʻopau ʻia.
Ke huli au iā Thomasnet, Ke kānana nei au, no ka mea ua papa inoa kēlā mau papa kuhikuhi a hoʻokaʻawale i nā mea hana extrusion plastik US ma o ka hiki a me ka ʻāina (Thomasnet, 2024). ʻO kēlā kānana hiki ke haʻi iā ʻoe inā ʻoe e kamaʻilio nei i kahi mea hana kiʻi palaki maoli a i ʻole he middleman.
No ke aha e ʻimi ai nā mea kūʻai aku “Hale hana” Ma kahi o “Mea hoolako”
Ma koʻu ʻike, ka nee ana aku “hale hana” ʻōlelo hōʻailona manaʻo. Makemake nā mea kūʻai aku i kahi kumu me ka mana o ka hale ma luna o ka hoʻolālā make a me nā mea hana, kamaʻilio MOQ maopopo, a me ka hiki ke hoʻonui mai ka prototype i ka hana. Hōʻike pū ia i ke kaomi reshoring: Hiki ke ho'ēmi i ka nui o ke kumukūʻai pae ʻāina ma ka hoʻohaʻahaʻa ʻana i ka ukana, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023), a ʻo ka ʻoihana plastics US ka mea kōkua nui i ka hoʻouna ʻana i ka hale hana a me ka hana (ʻAhahui ʻOihana Pākīpika, 2023). Ke ʻimi nei i kahi mea hana plastics home, ma mua o ka mea hoʻolako maʻamau, ʻO ka hoʻoholo pinepine ʻana i ka pilikia a me ke kumu kūʻai.
Pehea e hana ai ke kaʻina hana hoʻoheheʻe plastik, Kaʻanuʻu i ka ʻanuʻu

ʻO ka hoʻomaopopo ʻana i ka mechanics e kōkua iā ʻoe e nīnau i nā nīnau maikaʻi aʻe a heluhelu pololei i kahi ʻōlelo. Mālua Screw Extruder Manufacturers Manufacturers Hele au i nā mea kūʻai aku ma o ʻelima mau pae o ke kaʻina hana extrusion mau.
1. Hanai a me ka hoohehee ana iloko o ka Barela
Nā pellet Thermoplastic - PVC maʻamau, ABS, HDPE, LDPE, a i ʻole polypropylene - e hoʻokomo i kahi hopper a hāʻule i loko o kahi pahu wela me ka wili kaʻa. ʻO ka hui pū ʻana o nā mea hoʻomehana barela a me ka shear shear e hoʻoheheʻe i ka resin i loko o kahi kahawai hoʻoheheʻe homogeneous. He mea nui ke koho waiwai maanei: ʻO PVC kekahi o nā plastic extruded loa i ka honua, hoʻohana mau ʻia i nā profiles, paipu, a me ka paipu (ʻAhahui ʻOihana Pākīpika), ʻoiai ka polycarbonate, acrylic (PMMA), nylon (PA), a ʻo PEEK lawelawe ʻoi aku ka koi, ʻenehana-papa noi. Hiki ke hoʻohui pinepine ʻia ka recycled regrind, a me nā thermoplastics i hoʻohana ʻia i ka extrusion hiki ke hana hou ʻia, no laila, ʻoi aku ka maikaʻi o ka hoʻohana hou ʻana (EPA US, 2023).
2. Kaʻi ʻana i ka ʻilika hoʻoheheʻe ʻia ma o ka make maʻamau
Hoʻokuʻu ʻia ka hoʻoheheʻe ʻana i loko o kahi make e wehewehe ai i ka ʻaoʻao kea. ʻO kēia ka puʻuwai o ke kaʻina hana a me ke kumu e lawe ai ka hana maʻamau i ke kumukūʻai mea hana. Hoʻohana ʻia kahi hoʻonohonoho co-extrusion ma mua o hoʻokahi extruder e hānai ana i hoʻokahi make, ʻae iā ʻoe e hoʻohui i nā mea - he substrate paʻa me kahi lehelehe hoʻopaʻa TPE/TPU palupalu, ʻo kahi laʻana, a i ʻole kahi papale kala ma luna o ke kumu kūʻai haʻahaʻa.
3. Hoʻoluʻu, Ka nui ana, a me ka Hoʻokuʻu ʻana mau
Ke waiho nei i ka make, hele ka ʻaoʻao palupalu i loko o kahi ʻōnaehana hoʻoluʻu a nui - maʻamau ka ʻauʻau wai a i ʻole ka pahu hoʻomaʻamaʻa nui - e laka i nā ana.. He hoʻokuʻu (hukihuki) kahakiʻi i ka ʻaoʻao me ka māmā māmā. No ka mea, ua hoʻomau mau ʻia ka ʻāpana a emi ka mea i ka wā e maʻalili ai, ʻoi aku ka maʻamau o ka hoʻomanawanui extrusion ma mua o ka hoʻoheheʻe ʻana (Protolabs, 2023). Ua hoʻonohonoho mua wau i kēlā manaʻolana no laila e ʻike ka poʻe kūʻai aku i ka hoʻomanawanui maoli ma mua o ka uku ʻana no ka pololei ʻaʻole hiki i ke kaʻina hana ke mālama pono..
4. ʻOki ʻana i ka lōʻihi a me ka hana lua
ʻOki i ka ʻike laina a i ʻole ka pahi i ka hoʻopuka hoʻomau i ka lōʻihi. Mai laila mai, hana lua - wili, kuʻi ʻana, ʻōniʻoniʻo, paʻi ʻana, a i ʻole hui - hoʻololi i nā ʻāpana plastik i hoʻopau ʻia. ʻO kēia ke alahaka ma waena o ka ʻike maka a me kahi mea hiki ke hoʻohana, a ma laila e lanakila ai a nalowale paha ka hana hoʻololi wikiwiki.
Kuʻi kūʻokoʻa vs: He aha kāu e pono ai?
ʻO kēia ka hoʻoholo i nīnau nui ʻia iaʻu, a o ka pane pololei: pili i ka leo, geometry, a me ka laina manawa. E hoʻokaʻawale wau i kēlā me kēia ala.
Ke koho pololei ʻia nā ʻikepili kūʻai ma waho o ka papa
Stock extruded shapes - koʻokoʻo maʻamau, paipu, kaila, kihi, a me ka pepa - e pale i ke kumukūʻai mea hana a holo wikiwiki. Inā kūpono kahi moʻolelo papa inoa i kāu noi i loko o ka ʻae ʻae ʻia, ʻO ka kūʻai ʻana i nā mea kūʻai ʻoi aku ka liʻiliʻi, ala wikiwiki. Hoʻokele au i nā mea kūʻai aku ma ʻaneʻi no nā prototypes, nā puke haʻahaʻa, a me kekahi ʻāpana kahi e hana ai ka ʻāpana keʻa maʻamau i ka hana.
I ka wā e hoʻāpono ʻia ai nā mea hana maʻamau a me nā kiʻi
ʻO ka extrusion maʻamau e koi i kahi mea hana hoʻokahi manawa a make hoʻolimalima, ʻoiai ke pale aku nei nā ʻikepili waiwai i kēia kumukūʻai (alakaʻi kumu ʻoihana). Hoʻopaʻa ʻia kēlā kumukūʻai make inā pono kāu geometry, i ka wā e hoʻopau ai ka ʻāpana kūʻai maʻamau i ka hui o lalo, a i ʻole ke kiʻekiʻe ka nui o ka makahiki no ka amortize i ka mea hana. Ma luna o kekahi nui holo, ʻoi aku ka nui o ka mālama ʻana i kēlā me kēia kapuaʻi o kahi make i kūkulu ʻia me ka manaʻo.
ʻO ke ala huila: Nā Kūlana Kūlana, Māhele Kūʻai
ʻIke pinepine ʻia kaʻu ala waena punahele. Hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau me ka hoʻololi wikiwiki (ʻO SeaGate Plastics, 2024). Hoʻokuʻu ʻoe i ka hoʻopukapuka make, a laila hoʻohana i ka ʻokiʻoki, mīkini hana, a me ka hui ʻana e hiki ai i kahi hāʻawi maʻamau. No nā papahana waena waena, ʻoi aku kēia hybrid i ka waiwai maʻemaʻe a me ka hana maʻamau i ka huina kālā.
Kumukuai a me Lead-Time Hoʻohālikelike
Penei ka hoʻohālikelike ʻana o nā ala ʻekolu. E mālama i kēia mau pae hoʻolālā kuhikuhi, ʻaʻole nā huaʻōlelo - pili nā kiʻi maoli i ka mea, geometry, a me ka leo.
|
Kumukumu |
Nā Palapala Kūʻai |
Huinaʻi (Hana ʻia) |
Hoʻopiʻi Kūʻai piha |
|---|---|---|---|
|
ʻO ke kumukūʻai mea hana mua |
ʻAʻohe |
ʻAʻohe mea haʻahaʻa (nā mea paʻa wale nō) |
Hoʻokahi-manawa make kālā |
|
Ka manawa alakaʻi maʻamau |
pōkole loa (pinepine i ka waihona) |
Pōkole a haʻahaʻa |
ʻO ka lōʻihi loa (make kukulu + ʻatikala mua) |
|
kauoha liʻiliʻi (MOQ) |
Haʻahaʻa |
Haʻahaʻa a haʻahaʻa |
Kiʻekiʻe (e amortize mea paahana) |
|
ʻoluʻolu o Geometry |
Nā ʻano helu helu wale nō |
ʻAno maʻamau + mīkini hana |
ʻO ka ʻāpana keʻa i kauoha ʻia |
|
Kūpono maikaʻi loa |
Prototypes, haʻahaʻa leo |
leo waena, hana maʻalahi |
Kiʻekiʻe leo, nā ʻaoʻao ponoʻī |
|
Kumukumu |
Nā Palapala Kūʻai |
Huinaʻi (Hana ʻia) |
Hoʻopiʻi Kūʻai piha |
|---|---|---|---|
|
ʻO ke kumukūʻai mea hana mua |
ʻAʻohe |
ʻAʻohe mea haʻahaʻa (nā mea paʻa wale nō) |
Hoʻokahi-manawa make kālā |
|
Ka manawa alakaʻi maʻamau |
pōkole loa (pinepine i ka waihona) |
Pōkole a haʻahaʻa |
ʻO ka lōʻihi loa (make kukulu + ʻatikala mua) |
|
kauoha liʻiliʻi (MOQ) |
Haʻahaʻa |
Haʻahaʻa a haʻahaʻa |
Kiʻekiʻe (e amortize mea paahana) |
|
ʻoluʻolu o Geometry |
Nā ʻano helu helu wale nō |
ʻAno maʻamau + mīkini hana |
ʻO ka ʻāpana keʻa i kauoha ʻia |
|
Kūpono maikaʻi loa |
Prototypes, haʻahaʻa leo |
leo waena, hana maʻalahi |
Kiʻekiʻe leo, nā ʻaoʻao ponoʻī |
ʻO kēlā me kēia ala āu e koho ai, Manaʻo wau e hōʻoia i ka holo ʻana o ka hale kūʻai i kahi ʻōnaehana maikaʻi palapala - ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015) and remains the most widely adopted benchmark in the plastics sector. For a practical look at how stock and custom offerings sit side by side, I find ʻO SeaGate Plastics’ custom extrusion overview a useful reference point.
Types of Plastic Extrusion Profiles and Products

When I evaluate a project for extrusion, I start with the cross-section, because the geometry of the finished part dictates almost everything downstream: the die design, the material choice, and ultimately the price you will pay. Hoʻoheheʻe ʻia ka extrusion plastik i ka resin maka a hoʻolilo iā ia i kahi kikoʻī mau me kahi ʻāpana keʻa paʻa (ʻO SeaGate Plastics, 2024). That single principle produces a surprisingly wide catalog of shapes, so it helps to group them by complexity and function.
Solid Profiles, Hollow Profiles, and Complex Geometries
ʻO nā profile paʻa nā mea hana o ka ʻoihana: lāʻau lāʻau, nā pā, lihilihi, a ʻoki ʻia me nā hakahaka o loko. ʻO lākou ka mea maʻalahi i ka mea hana a me ke kala ʻana i ka hoʻomanawanui, ʻo ia ke kumu aʻu e paipai ai iā lākou no nā mea kūʻai mua e hoʻāʻo ana i kahi hoʻolālā. Hoʻokomo nā ʻaoʻao hollow i nā kahawai kūloko, a koi lākou i nā mea make ʻoi aku ka maʻalahi me nā mandrel a i ʻole nā pine e paʻa ai ka lua i ka wā e maʻalili ai ka hehee.. Hoʻohui nā geometries paʻakikī i nā paia he nui, undercuts, a me nā hoʻololi lahilahi a mānoanoa i hoʻokahi ʻāpana keʻa, a ʻo kēia kahi e hoʻokaʻawale ai ka hoʻolālā make a me ka ʻike mea hana i kahi mea hana kiʻi kiʻi kiʻi mai ka awelika. Ma koʻu ʻike, ʻO ka mānoanoa o ka paia ʻole ke kumu maʻamau o ka warping, No laila, paʻi mua au i nā mea hoʻolako i ke ʻano o kā lākou hoʻolālā ʻana e kaulike i ke kahe waiwai ma ka ʻaoʻao.
Hoʻokuʻu ʻia ʻo Tubing a me Multi-Lumen
ʻO Tubing kahi ʻāpana kūikawā o ka hollow extrusion, a hoʻopaʻa ʻo ia i nā mea āpau mai ka paipu pahu hoʻokahi maʻalahi a hiki i nā hoʻolālā multi-lumen me nā kaha like ʻole e holo ana i ka lōʻihi o ka ʻāpana.. Ke hilinaʻi nei ka poʻe kūʻai aku i nā lāʻau lapaʻau a me nā mea hana analytical i nā extrusions multi-lumen e lawe i nā wai, uwea, a me nā mea ʻike ma o hoʻokahi ʻaoʻao paʻa. ʻO ka mea hoʻolako paipu plastik hilinaʻi e hoʻopaʻa paʻa i ka concentricity a me ka ʻae ʻana i loko, ʻoiai ke hoʻomanaʻo mau nei au i nā mea kūʻai aku ʻoi aku ka maʻalahi o ka extrusion tolerances ma mua o ka hoʻoheheʻe ʻia ʻana ma muli o ka emi ʻana o nā mea a me ka hana mau ʻana. (Nā Punawai Hoʻolālā Protolabs, 2023). E hoʻolālā i kāu kūpono a me ka hoʻomaʻemaʻe a puni kēlā ʻoiaʻiʻo ma mua o ka hakakā ʻana.
ʻO ka hoʻokuʻu ʻana a me nā ʻano mea he nui
Hoʻohana ʻo Co-extrusion i ʻelua a ʻoi aku paha resins ma o ka make kaʻana like e hana i hoʻokahi ʻaoʻao me nā ʻāpana waiwai ʻokoʻa. Hoʻohana wau ia i ka wā e pono ai kahi ʻāpana i nā waiwai hakakā i ka manawa hoʻokahi, e like me kahi kino kino PVC paʻa me ka lehelehe TPE / TPU gasket palupalu, a i ʻole kahi ʻāpana pāpale hiki ke ʻike ʻia ma luna o kahi substrate kumu kūʻai haʻahaʻa. Hoʻopau ia i ka hui lua a me nā ʻanuʻu paʻa, ʻo ia ka mea mālama kumu kūʻai ma ka leo. ʻO ka tradeoff ka paʻakikī o nā mea hana, No laila, mālama au i ka co-extrusion no nā hoʻolālā kahi e hōʻoia pono ai ka pōmaikaʻi multi-material i ka hoʻokomo kālā make..
Nā noi ʻoihana maʻamau no kēlā me kēia ʻano
Hoʻopili nā geometries ʻokoʻa i nā ʻāpana like ʻole, a ʻo ka hoʻohālikelike ʻana iā lākou i ka wā mua e hoʻomau i ka ʻimi ʻana i nā kamaʻilio.
- Nā ʻaoʻao paʻa: lihi pā hale kūʻai, ʻoki lako, sila, a me na mea pa.
- Hollow profiles: pukaaniani a me na pani puka, Nā ala kukui LED, a me ka hoʻopili hale.
- Tubing a me ka nui-lumen: catheters lapaʻau, laina hoʻoili wai, a me ka paipu pneumatic.
- Nā ʻaoʻao i hoʻokuʻu ʻia: ka wehe ʻana i ka wā, pahu hau hau, a me nā lima ʻelua-durometer.
- Hoʻokuʻu pepa: hōʻailona, mea hoʻoheheʻe thermoforming, a me nā panela pale.
No ka mea, he mau ka extrusion plastic, kaʻina hana kiʻekiʻe, kūpono ia i ka hana lōʻihi e holo maikaʻi loa, a hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau kumukūʻai me ka huli wikiwiki (ʻO SeaGate Plastics, 2024). Inā paʻa kāu koi makahiki a ana ʻia i nā ʻumi kaukani kapuaʻi, extrusion economics hana ikaika i kou makemake.
Nā mea maʻamau i hoʻohana ʻia i ka Extrusion Plastic
ʻO ke koho waiwai ka hoʻoholo aʻu i ʻike ai e hoʻohaʻahaʻa pinepine ʻia nā mea kūʻai aku. Hoʻoponopono ka resin i ka ikaika mechanical, pale kemika, pae wela, koina, a me ka paʻa o ka hoʻomanawanui i hiki i ka extruder ke paʻa maoli. Hoʻohui au i nā resins extrusion i ʻekolu papa, a laila e hana pū me nā mea kūʻai aku e neʻe i luna e like me ka makemake maoli o ka noi.
Nā Resins Mea kūʻai: PVC, Polyethylene, a me ka Polypropylene
Hoʻopili nā resins waiwai i ka hapa nui o ka leo extruded, a no ke kumu maikai. ʻO PVC kekahi o nā plastic extruded loa i ka honua, maʻamau i nā profiles, paipu, a me ka paipu (ʻAhahui ʻOihana Pākīpika). Hāʻawi ia i ka rigidity, hiki i ka makani, a me ke kumukuai haahaa, a lawe maikaʻi ʻia ke kala a me ka hoʻopau ʻana o ka ʻili. Hōʻike ʻia ka polyethylene i ʻelua mau māka maʻamau: HDPE no ka oolea, nā ʻaoʻao kūʻē kemika a me ka LDPE kahi e pono ai ka maʻalahi. Hoʻohālikelike ka Polypropylene i ke kūpaʻa kemika me kahi ratio ikaika-a-kaumaha maikaʻi a me ka hana ola-hinge. Ke nīnau ka mea kūʻai e pili ana i ka extrusion resin no ka leo kiʻekiʻe, ʻāpana koʻikoʻi koʻikoʻi, ʻaneʻane i nā manawa a pau aʻu e hoʻomaka ai.
ʻOihana ʻenekinia: ABS, Polycarbonate, Nylon, a me ka acrylic
Piʻi aʻe nā plastics-grade engineering i ka hana mechanical a me ka wela. ABS delivers impact strength and clean finishes for consumer and enclosure parts. Polycarbonate brings high impact resistance and optical clarity, which makes it a staple for lighting lenses and safety glazing. Nylon (PA) offers wear resistance and toughness for mechanical components and cable management. ʻAlika (PMMA) provides excellent clarity and UV stability for display and signage profiles. I move buyers into this tier when commodity resins cannot meet load, wela, or clarity requirements, and I make sure they price the resin premium against the performance gain before committing.
High-Performance Materials Like PEEK
At the top sits a small group of high-performance polymers, with PEEK as the reference point. PEEK withstands continuous high temperatures, kemika hoʻopaʻapaʻa, and demanding mechanical loads, ʻo ia ke kumu e hōʻike ai i ka aerospace, lāʻau lapaʻau, and semiconductor applications. The material cost is substantial, so I only specify it when the operating environment leaves no cheaper option. Not every plastic profile manufacturer processes PEEK, so capability screening matters more at this level.
Matching Material Properties to Application Requirements
My selection framework is deliberately simple: define the non-negotiable requirement first, then choose the least expensive resin that clears it. The table below summarizes how I weigh the common options for extruded plastic parts.
| Mea waiwai | ʻĀpana | Key Strengths | Uku Pili | Nā noi maʻamau |
|---|---|---|---|---|
| PVC | Mea kūʻai | ʻoʻoleʻa, hikiwawe, kumu kūʻai haʻahaʻa | $ | Nā moʻolelo, paipu, ʻokiʻoki |
| HDPE / LDPE | Mea kūʻai | Kūleʻa kimemika; stiff or flexible | $ | Paipu, nā laina laina, ducting |
| Polypropylene | Mea kūʻai | Kūleʻa kimemika, nā hinges ola | $ | Fluid handling, hinges |
| ABS | ʻenekinia | Ka ikaika pili, clean finish | $$ | Nā pā, consumer parts |
| Polycarbonate | ʻenekinia | Ke kū'ē i ka hopena, akaka | $$ | Nā leka uila, pale aniani |
| Nylon (PA) | ʻenekinia | Wear resistance, ʻoʻoleʻa | $$ | Mechanical, cable guides |
| ʻAlika (PMMA) | ʻenekinia | Maopopo, UV stability | $$ | hōʻailona, hōʻike |
| PEEK | High-performance | Wela, kemika, and load resistance | $$$$ | Aerospace, lāʻau lapaʻau, semiconductor |
One efficiency point worth raising with any supplier: thermoplastics used in extrusion are recyclable, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai (ʻOihana Hoʻomalu Kaiapuni ʻAmelika, 2023). Asking how a factory handles regrind tells me something about both their cost discipline and their sustainability practices.
ʻO nā mea hana ʻo Plastic Extrusion ma USA
For many of the buyers I advise, the sourcing question is not only “who can extrude this profile” aka “who can extrude it here.” Domestic sourcing has moved from a preference to a strategic decision, and it deserves a clear-eyed look rather than reflexive patriotism.
Why US-Based Sourcing Matters for Many Buyers
The financial case is stronger than it first appears. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023). When I run a total-cost comparison rather than a unit-price comparison, offshore savings often shrink once I add ocean freight, uku uku, safety stock, and the working capital tied up in long transit times. For a domestic plastics manufacturer serving a US customer, lead times measured in weeks rather than months also mean less risk if a design changes mid-program.
Regional Manufacturing Hubs Across the Country
US extrusion capacity is not evenly distributed, and knowing the map speeds up sourcing. The Great Lakes and Upper Midwest concentrate general-purpose profile and tubing extruders near automotive and industrial demand. The Northeast holds a dense cluster of medical and precision tubing specialists. The Southeast has grown quickly around building products and packaging. The West Coast and Southwest serve electronics, aerospace, and consumer markets. Supplier directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is where I usually build a first shortlist before making calls.
Domestic Quality, Kūkākūkā, and IP Advantages
Beyond cost, three practical advantages keep drawing buyers home. Ka mua, quality systems are easier to verify in person; ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing (International Organization for Standardization, 2015), and I can audit a domestic supplier’s implementation without an international trip. Ka lua, time-zone-aligned communication shortens the feedback loop from prototype to production, which matters when a die needs a mid-run adjustment. Ke kolu, intellectual property protection is more enforceable under US jurisdiction, a real concern when a custom profile is a competitive differentiator. I treat these as the differences that a spreadsheet alone will miss.
How US Factories Serve Diverse Industries
American extruders span the full range of contract manufacturing, from stock extruded shapes shipped from inventory to fully custom die programs. Custom extrusion typically requires a one-time tooling or die investment, while stock profiles avoid that cost, so I match the sourcing path to how unique the geometry really needs to be. The US plastics industry remains a major contributor to domestic manufacturing shipments and employment (ʻAhahui ʻOihana Pākīpika, 2023), and that depth means a buyer can usually find a plastic fabrication services partner suited to their volume, from prototype to production. For a broad view of custom capabilities, I often point clients to overviews such as custom plastic extrusion manufacturers to calibrate expectations before requesting quotes.
How to Find Plastic Extrusion Companies Near You
When I begin a sourcing project, geography is one of the first variables I weigh. Location shapes freight cost, kaʻina kamaʻilio, and how quickly I can iterate from prototype to production. ʻŌlelo kēlā, proximity is only valuable when the nearby supplier can actually do the work. Ma koʻu ʻike, the smartest approach treats “kokoke iaʻu” as a filter, ʻaʻole he hoʻoholo.
Why Local Sourcing Often Pays Off
A domestic plastics manufacturer close to your facility gives you three concrete advantages. Ka mua, shorter shipping distances lower freight and lead-time risk, which matters for bulky extruded plastic parts and long profiles that ship as oversized freight. Ka lua, local partners make on-site visits practical, a ua loaʻa iaʻu nā pilikia kaʻina hana ʻoi aʻe i loko o kahi hele wāwae ʻelua hola ma mua o nā pule o ka leka uila. Ke kolu, ʻO ke kokoke e hoʻokē ʻai i ka ʻike: i ka wā e pono ai kahi make i kahi tweak, hiki i ka mea hoʻolako i kekahi mau hola ke hoʻohuli i nā laʻana i ʻoi aku ka wikiwiki ma mua o ka hoʻokahi ma kēlā ʻaoʻao o ka moana.
ʻOi aku ka hihia kālā ma mua o ke kumu kūʻai. Wahi a ka Reshoring Initiative (2023), Hiki ke ho'ēmi i ka nui o ke kumukūʻai pae ʻāina ma ka hoʻohaʻahaʻa ʻana i ka ukana, dute, a me nā koina lawe waihona. He mea nui ka waihona home, pū kekahi; ka Hui ʻOihana Pākīpika (2023) hōʻike ʻo ka ʻoihana plastics US he mea kōkua nui i nā moku hana hale a me ka hana, 'o ia ho'i, 'o ka hiki 'ana o ka hiki no ka resin extrusion.
Kahi a'u e nana ai: Papa kuhikuhi, Nā hui, a me nā kuhikuhi
E kūkulu i papa inoa mua o nā moho, Hoʻohana au i ʻekolu mau ala hoʻohui:
- Nā papa kuhikuhi mea hoʻolako. Thomasnet (2024) papa inoa a hoʻokaʻawale i nā mea hana extrusion plastik US ma o ka hiki a me ka ʻāina, which makes it straightforward to filter by material, kaʻina hana, and location.
- Trade associations. Membership in bodies like the Plastics Industry Association signals a firm that invests in standards and industry engagement.
- Referrals. A recommendation from an engineer who has run production with a plastic profile manufacturer carries more weight than any marketing page, because it reflects delivered performance.
I treat the directory as a starting point for a plastic tubing supplier or profile shop, then validate each name against real references before it earns a spot on my shortlist.
Balancing Proximity Against Capability and Price
Distance is a tiebreaker, not a trump card. If a nearby shop cannot hold your tolerances, run your resin, or meet your volume, the convenience is worthless. I rank capability and quality first, alaila kumukuai, then location. A plastic extrusion companies factory supplier two states away with the right co-extrusion line and a proven ISO 9001 system will usually serve me better than a closer shop lacking those capabilities.
When Local Is Not the Best Option
Sometimes the right partner is not nearby. Specialized work in engineering-grade plastics such as PEEK, polycarbonate, aiʻole naylon (PA) may only be done well by a handful of shops nationally. High-volume manufacturing programs can justify shipping economics that favor a distant, more automated plant. And when you need capabilities like plastic sheet extrusion combined with in-line fabrication, the fit of the process matters more than the mileage. In those cases I widen the search radius and lean on video plant tours and third-party audits to close the distance gap.
Understanding the Largest Plastic Extrusion Companies
Buyers often gravitate toward the biggest names, assuming scale guarantees a better outcome. Scale does deliver real advantages, but it also carries tradeoffs. Understanding what “nui loa” actually means helps me match a supplier’s footprint to my program rather than to a reputation.
What Scale Means for Capacity and Reliability
ʻO ka extrusion kahi mau, high-volume process well suited to long production runs, and large factories are built around that reality. More extrusion lines mean higher throughput, redundancy if one line goes down, and the ability to absorb demand spikes. Scale usually correlates with mature quality systems as well; ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (International Organization for Standardization, 2015), is almost table stakes among large plants. That maturity translates into more consistent extruded plastic parts across long runs.
The Tradeoffs of Large Factories vs. Specialized Shops
ʻAʻole ʻoi aku ka maikaʻi o ka nui. Large plants optimize for volume, which can mean higher minimum order quantities, less flexibility on small custom runs, and slower responsiveness on prototype work. A specialized shop may excel at tight-tolerance custom plastic profiles, unusual resins, or quick-turnaround production that a high-volume plant treats as a nuisance. The table below summarizes how I weigh the two.
| Kumukumu | Large-Scale Factory | Specialized Shop |
|---|---|---|
| Ka hiki | Kiʻekiʻe; multiple lines, redundancy | kaupalena; fewer lines |
| Ka nui kauoha liʻiliʻi | Often high | Usually flexible |
| Prototype speed | ʻOi aku ka mālie; volume-focused scheduling | ʻOi aku ka wikiwiki; agile setup |
| Laulā mea | Broad commodity resins (PVC, HDPE, LDPE, PP) | Often engineering-grade (PEEK, PC, PA) |
| Price per unit at volume | lalo | Kiʻekiʻe |
| Kūpono maikaʻi loa | Long production runs | Kuʻuna, low-to-mid volume, complex profiles |
When High-Volume Capability Is Essential
There are programs where I will not compromise on scale. Hoʻomau, long-run demand for standardized profiles, paipu, or tubing in commodity resins is the natural home of a large factory. ʻO PVC kekahi o nā plastic extruded loa i ka honua, hoʻohana mau ʻia i nā profiles, paipu, a me ka paipu, and sourcing it at volume rewards the economies a big plant provides. If your forecast calls for millions of feet of a stable profile cross-section, high-volume capability moves from nice-to-have to essential.
How to Verify Claimed Scale and Capacity
Claims on a website are not evidence. Before I accept a “nui loa” a i ʻole “highest capacity” claim, I verify it with concrete questions:
- How many extrusion lines are operational, and what is the die diameter range on each?
- What is current utilization, and how much spare capacity exists for my program?
- Can you share throughput figures (lbs/hour or feet/day) for a comparable profile?
- What redundancy exists if a line fails mid-run?
- Which certifications, e like me ISO 9001, are current, and may I see the certificate?
I pair those answers with a plant tour or audit. Physical evidence of running lines, staffing, and inventory tells me far more than any capacity figure quoted in a brochure.
How to Identify the Best Plastic Extrusion Factory for Your Project
“Best” is one of the most misused words in supplier marketing. Ma ka hana, the best plastic extrusion companies factory manufacturer is the one that best fits your specific requirements, not the one with the loudest claim. I define the term relative to my project, then score candidates against that definition.
Defining “Best” Relative to Your Specific Needs
Before comparing suppliers, I document what my project actually demands: the resin (ʻōlelo, ABS for impact resistance, acrylic (PMMA) for optical clarity, or TPE/TPU for flexibility), the tolerance band, the volume, the timeline, and the level of engineering support I need for die design and tooling. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Nā Punawai Hoʻolālā Protolabs, 2023), so I confirm early that a candidate can meet my dimensional requirements rather than assuming it can. A shop that is ideal for a high-volume HDPE pipe run may be the wrong choice for a tight-tolerance polycarbonate profile.
Weighing Quality, Koina, Ka māmā holo, a me Kākoʻo
Every sourcing decision balances four levers, and improving one often pressures another:
- ʻAno maikaʻi. Documented quality systems, in-process inspection, and material traceability. ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics.
- Koina. Not just unit price. ʻO ka extrusion maʻamau e koi i kahi mea hana hoʻokahi manawa a make hoʻolimalima, while stock extruded shapes avoid that cost, so I model total cost including tooling and MOQ.
- Ka māmā holo. Hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau me ka hoʻololi wikiwiki (ʻO SeaGate Plastics, 2024), but lead times vary widely between shops.
- Kākoʻo. Engineering input on profile cross-section and material selection can prevent costly redesigns as you move from prototype to production.
Sustainability increasingly enters the equation as well. Hiki ke hoʻohana hou ʻia nā Thermoplastics i hoʻohana ʻia i ka extrusion, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai (ʻOihana Hoʻomalu Kaiapuni ʻAmelika, 2023), which can reduce both cost and waste when a supplier manages it responsibly.
Reading Past “Best” Marketing Claims
Superlatives are easy to print and hard to prove. When I see “maikaʻi loa,” “alakaʻi,” a i ʻole “premier,” I translate the claim into a testable question. Instead of accepting “best quality,” I ask for defect rates and inspection records. Ma kahi o “fastest,” I ask for typical lead times on my specific part. Ma kahi o “most experienced,” I ask for references in my industry. Marketing language that cannot survive a follow-up question does not influence my shortlist.
Building a Shortlist Scoring Method
To keep the comparison objective, I use a weighted scoring model. I list my criteria, assign each a weight that reflects its importance to the project, score every candidate from 1 i 5, and multiply. The weights shift by project; a prototype program might weight speed and engineering support heavily, while a mature production program weights cost and capacity.
- List criteria: ʻōnaehana maikaʻi, material capability, hoʻomanawanui, hiki, ka manawa o waena o ka hoʻomaka a i ka wā pau, kumukūʻai mea hana, kākoʻo ʻenekinia, and location.
- Assign weights that total 100 pākēneka, reflecting your priorities.
- Score each supplier 1 i 5 on every criterion, using verified evidence rather than marketing claims.
- Calculate weighted totals and rank the candidates.
- Validate the top two with reference calls and, kūpono loa, a plant visit before committing.
This structured method has consistently steered me toward the partner that fits the work, whether that turns out to be a large plant, a nimble specialist, or a domestic shop just down the road. For a deeper look at how custom extrusion capabilities map to applications, resources such as ʻO SeaGate Plastics’ custom extrusion overview are a useful reference as you refine your own criteria.
Key Capabilities to Evaluate in a Plastic Extrusion Company
When I vet a plastic profile manufacturer, I look
Tolerances and Precision in Extruded Parts
I koʻu loiloi ʻana i kahi mea hana kiʻi plastik, tolerances are the first place I look for a reality check. Extrusion is a continuous forming process, so it behaves differently from molding. As Protolabs notes, extrusion tolerances are generally looser than injection molding because material shrinkage and continuous forming introduce variability that a closed mold does not (Nā Punawai Hoʻolālā Protolabs, 2023). Setting expectations here early saves both money and rework later.
Typical Achievable Tolerances by Material and Profile
Ma koʻu ʻike, achievable precision depends heavily on the resin and the geometry of the profile cross-section. Rigid engineering-grade plastics hold tighter dimensions than soft or semi-crystalline materials, and simple shapes hold tighter than complex hollow profiles. The ranges below reflect commonly quoted commercial extrusion capabilities for custom plastic profiles; always confirm against your supplier’s published standards for your specific part.
| Mea waiwai | Paʻa paʻa | Typical tolerance tendency | Notes for specifying |
|---|---|---|---|
| PVC paakiki | Kiʻekiʻe | Tighter, well-controlled | Widely extruded; predictable in profiles and tubing |
| ABS | Kiʻekiʻe | Tight on rigid profiles | Good for structural extruded plastic parts |
| Polycarbonate | Kiʻekiʻe | Tight, low shrink | Optical and impact-rated applications |
| ʻAlika (PMMA) | Kiʻekiʻe | Tight, but brittle at thin walls | Sheet and clear profiles |
| Nylon (PA) | Kaumaha | Looser; moisture-sensitive | Account for post-extrusion moisture uptake |
| HDPE / LDPE | Moderate to low | Looser; higher shrink | Expect wider bands on wall and OD |
| Polypropylene | Kaumaha | Looser; semi-crystalline shrink | Allow generous tolerance on critical dims |
| PEEK | Kiʻekiʻe | Tight, but specialized | High-temp engineering runs; higher cost |
| TPE / TPU | Haʻahaʻa | Loosest; flexible recovery | Soft profiles deform under measurement |
Factors That Affect Dimensional Stability
Several variables move a part inside or outside its tolerance band. Wall thickness uniformity matters most: thick and thin sections in the same profile cool at different rates and warp. Semi-crystalline resins like polypropylene and HDPE shrink more than amorphous ones like polycarbonate and acrylic, so the die must be cut to compensate. I also watch for haul-off speed, wela hoohehee, and cooling-bath control, since drift in any of these shows up as dimensional variation over a long run. For hygroscopic materials such as nylon, moisture absorbed after extrusion can change dimensions days later, which is why I ask how a supplier conditions and stores finished stock.
Specifying Tolerances in Your Drawings
The cleanest way to control cost is to tolerance only what functionally matters. I call out critical dimensions explicitly, apply a reasonable general tolerance block to everything else, and reference the datum features that mate with other components. Where a flexible TPE or TPU profile is involved, I specify the measurement method and fixture, because a soft part measures differently under light pressure than at rest. Being specific about which surfaces are cosmetic versus functional lets a plastic fabrication services partner set up the line intelligently instead of overbuilding to a blanket precision requirement.
Balancing Precision Against Cost
Tighter tolerances raise cost through slower line speeds, more scrap, added inspection, and sometimes secondary sizing or machining. Ma ka hana, I treat precision as a dial rather than a switch: I hold the two or three dimensions that drive fit and function tightly and relax the rest. That approach keeps resin extrusion economical while still delivering parts that assemble correctly. When a design genuinely needs molding-level precision on every feature, that is a signal the part may not be a good extrusion candidate, and I revisit the process choice before committing to tooling.
Minimum Order Quantities and Lead Times
MOQs and lead times are where the difference between stock extruded shapes and true custom work becomes concrete. Custom extrusion typically requires a one-time tooling investment in a die, while stock profiles avoid that cost entirely, per common industry sourcing guidance. That single fact drives most of the ordering economics, so I plan around it from the start.
Typical MOQ Ranges for Stock vs Custom
Stock profiles and tubing can often be bought in small quantities, sometimes by the foot or in single boxes, because the supplier already runs them. As SeaGate Plastics points out, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround, which is a practical advantage when volumes are modest (ʻO SeaGate Plastics, 2024). Custom profiles are different. Because the line has to be set up, purged, and stabilized before good parts come off, suppliers set a minimum run to amortize that setup. I commonly see custom MOQs expressed in pounds of resin or in linear footage rather than piece count, and the threshold rises with more exotic engineering-grade plastics.
How Lead Times Vary With Tooling and Volume
For a new custom profile, the die is the pacing item. Tooling design, ʻoki ʻoki, and first-article trials typically dominate the initial schedule, and I budget several weeks for die design and tooling before any production parts exist. Once the die is proven, repeat orders move quickly because the tooling is on the shelf. Higher volumes actually help here: extrusion is a continuous, high-volume process well suited to long production runs, so once a line is dialed in, adding footage is efficient rather than disruptive.
Quick-Turnaround Options and Expedited Runs
When a timeline is tight, I look at three levers. Ka mua, use stock profiles or standard tubing that can ship from inventory and be cut or fabricated to length. Ka lua, ask whether an existing die is close enough to modify rather than cutting a new one. Ke kolu, request an expedited slot, which many suppliers offer for a premium by prioritizing line time. Quick-turnaround production is realistic for standard shapes; for genuinely new custom geometry, the tooling step still sets the floor on how fast you can go.
Planning Your Project Timeline
I work backward from the required delivery date and add explicit buffers for die design, apono 'atikala mua, a me nā hana lua. Moving from prototype to production is smoother when I lock the profile cross-section early, because late geometry changes mean recutting the die and resetting the clock. Aligning MOQ with real annual demand also matters: ordering an efficient run size once beats paying repeated setup charges on small, frequent custom orders.
Cost Drivers in Plastic Extrusion Pricing
Understanding what actually drives a quote lets me negotiate from evidence rather than instinct. Extrusion pricing breaks down into a handful of levers, and knowing which one dominates for a given part tells me where the savings live.
Material Selection and Resin Pricing
Resin is usually the largest recurring cost, and it varies widely by grade. Commodity materials like PVC, polypropylene, HDPE, and LDPE sit at the low end; PVC in particular is among the most widely extruded plastics globally and is well supported across suppliers. Engineering-grade plastics such as polycarbonate, nylon, and especially PEEK command higher prices and can require specialized processing. One efficiency I always ask about is regrind: thermoplastics used in extrusion are recyclable, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai, which can lower material cost on non-critical parts (ʻOihana Hoʻomalu Kaiapuni ʻAmelika, 2023). Choosing the least expensive resin that meets the application requirement is the single highest-leverage decision in material selection.
Tooling, Hoʻonoho, and Run Volume
Custom work carries a one-time die cost that stock profiles avoid. That tooling charge is fixed, so it amortizes across the run: the more footage I order, the lower the per-part tooling burden. Setup time and line stabilization add cost to every job regardless of size, which is exactly why small custom orders feel expensive per piece. Hoʻokuʻu hui, which combines two materials in one profile, adds tooling and process complexity and therefore cost, but it can eliminate secondary assembly, so I weigh the tradeoff on total value rather than tooling alone.
Secondary Operations and Finishing
Anything that happens after the profile leaves the die adds cost: cutting to length, wili ʻana, ʻōniʻoniʻo, paʻi ʻana, kuʻi puka, tight-tolerance sizing, a me ka paʻi ʻana. Individually these are minor, but they stack quickly on high piece counts. I decide deliberately which operations belong in-line with the extrusion and which are genuinely needed, because each added step also adds handling and inspection. Where a feature can be designed into the profile cross-section instead of machined afterward, I do that, since forming a feature is nearly free compared with a downstream operation.
Domestic vs Offshore Cost Comparisons
Headline piece price often favors offshore, but I evaluate total landed cost. The Reshoring Initiative notes that domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023), and those factors are easy to underestimate when comparing unit prices alone. Working with a domestic plastics manufacturer also shortens lead times, hoʻomāmā ke kamaʻilio, and reduces the inventory buffer I have to hold against long ocean transit. The US plastics industry is a substantial contributor to domestic manufacturing shipments and employment (ʻAhahui ʻOihana Pākīpika, 2023), so the domestic supplier base for both stock and custom profiles is deep. ʻO kaʻu lula: for high-volume, low-mix commodity profiles, offshore can win on price; for responsive, higher-mix, or engineering-grade work, domestic contract manufacturing usually wins on total cost and risk. For a fuller look at custom capabilities, I point buyers to custom plastic extrusion manufacturers such as SeaGate Plastics as a reference point for scope and services.
Questions to Ask Before Choosing a Factory
When I vet a plastic profile manufacturer, I treat the first conversation as a structured interview rather than a sales call. The goal is to separate shops that can genuinely deliver my part from those that simply want the order. Over years of sourcing extruded plastic parts, I have found that a handful of pointed questions surface most of the risk before a single dollar changes hands. Below is the checklist I actually use.
Ka hiki, Nā palapala hōʻoia, and Material Expertise
I start by asking what the factory runs today, not what it claims it can run. Continuous extrusion is a high-volume manufacturing process, so I want to know line count, typical run lengths, and whether they have headroom for my volume without displacing existing customers. On the quality side, I ask directly about certification. ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing (International Organization for Standardization, 2015), and while certification is not a guarantee of good parts, its absence tells me the shop may lack documented process controls.
Material expertise is the third leg. A capable resin extrusion supplier should speak fluently about the polymers relevant to my application, inā paha ʻo ia ka PVC a me ka HDPE no nā kiʻi kūkulu, ʻO ABS a me ka polycarbonate no nā pā, polypropylene a me LDPE no ka hoʻopili ʻana a me ka paipu, a i ʻole nā mea ʻenekinia-grade plastics e like me ka nylon (PA) a PEEK no nā kaiapuni koi. ʻO PVC kekahi o nā plastic extruded loa i ka honua, hoʻohana mau ʻia i nā profiles, paipu, a me ka paipu (ʻAhahui ʻOihana Pākīpika). Inā makemake au i nā ʻāpana maʻalahi, Ke hōʻoia nei au i ka ʻike me TPE/TPU, a inā koi koʻu ʻāpana i ke kumu ʻoʻoleʻa me ka ʻili palupalu a i ʻole ka ʻili ʻili, Nīnau au inā hāʻawi lākou i ka co-extrusion. Kūʻai nui ʻo Lab Extruder
Loaʻa ke kākoʻo prototyping a me ka hoʻolālā
Nīnau au inā hāʻawi ka hale hana i nā kūkākūkā hoʻolālā ma mua o ka ʻoki ʻia ʻana o nā mea hana. E nānā nā hoa lawelawe ʻoihana palaki maikaʻi loa i kaʻu ʻāpana no ka extrudability, hae i nā paia lahilahi a i ʻole nā kihi ʻoi e pahele i ke kaumaha, a manaʻo i nā mea hoʻololi e hoʻohaʻahaʻa i ke kumukūʻai me ka ʻole e hōʻeha i ka hana. I also confirm they can produce a representative prototype rather than pointing me straight to a production die.
Manawa alakai, MOQ, and Delivery Track Record
Here I get specific. I ask for standard lead times on both tooling and production, the minimum order quantity, and how MOQ scales with material and profile complexity. Custom extrusion typically requires a one-time tooling investment for the die, while stock extruded shapes avoid that cost entirely (alakaʻi kumu ʻoihana). If my volumes are modest, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (ʻO SeaGate Plastics, 2024), so I always ask what stock profiles they carry. On delivery, I want on-time performance data, not adjectives.
References and Industry Experience
ʻO ka hope loa, I ask for references in my industry. A shop that regularly serves medical, kaʻa kaʻa, or building-products customers has already navigated the tolerances and documentation those sectors demand. I call the references and ask two questions: did the parts meet spec on the first production run, and how did the supplier handle the problem when something went wrong?
From Prototype to Production: How the Process Unfolds
Once I have chosen a supplier, the path from a drawing to shippable extruded plastic parts follows a predictable sequence. Understanding each stage helps me set realistic timelines internally and catch problems while they are still cheap to fix.
Submitting Drawings and Design Consultation
I begin by sending a dimensioned drawing of the profile cross-section, along with the target material, kala kala, tolerance requirements, and end-use environment. This is where design-for-manufacturing consultation earns its keep. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Nā Punawai Hoʻolālā Protolabs, 2023), a good engineer will help me place critical dimensions where the process can reliably hold them and relax the ones that do not matter.
Sample and Prototype Validation
Next comes a sample or prototype. Depending on the shop, this may be pulled from a soft or temporary die, or matched from existing stock extruded shapes. I use this stage to validate fit, hikiwawe, hoʻopau ʻili, and material behavior in my actual assembly. Catching a wall-thickness issue on a prototype costs me a revision; catching it after the production die is cut costs me the tooling.
Tooling Approval and First-Article Inspection
Extruder Twin Screw After I approve the design, the factory cuts the production die. The die design and tooling step is the largest one-time cost in custom extrusion, so I review the tooling drawing carefully before signing off. Once the die runs, I require a first-article inspection: a documented measurement of the initial output against my drawing. I do not release full production until the first article passes.
Ramping to Full Production
With the first article approved, the line ramps to full production. Plastic extrusion is a continuous, high-volume process well suited to long production runs (SPI/Plastics Industry Association overview), so unit costs typically drop as volume climbs. I confirm the quality plan for ongoing runs, including sampling frequency and the criteria for holding or scrapping out-of-spec material. Hiki ke hoʻohana hou ʻia nā Thermoplastics i hoʻohana ʻia i ka extrusion, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai (ʻOihana Hoʻomalu Kaiapuni ʻAmelika, 2023), so I also clarify the shop’s regrind policy when appearance or mechanical properties are critical.
Domestic vs Overseas Extrusion Sourcing
One of the most consequential decisions I make is where to source. The instinct is to compare unit price, but in my experience that number alone is misleading. What matters is total landed cost and the operational realities that price hides.
Cost vs Total Landed Cost Considerations
Overseas suppliers often quote a lower piece price, but I add freight, nā hana, customs handling, and the inventory carrying cost of larger safety stock and longer transit. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023). Once I build a full landed-cost model, the gap between a domestic plastics manufacturer and an overseas one usually narrows, and sometimes reverses.
Ka manawa o waena o ka hoʻomaka a i ka wā pau, Hoʻouna, and Communication Factors
Domestic sourcing shortens my supply chain and simplifies communication across time zones and languages, which matters most when I need quick-turnaround production or fast design changes. Overseas sourcing can suit stable, high-volume programs where the design is frozen and lead time is not a constraint.
Quality Control and IP Protection
Proximity makes on-site audits and first-article reviews far easier, and domestic contracts generally offer stronger, more enforceable intellectual property protection for a proprietary die design. When my profile represents real design investment, that protection weighs heavily.
Ke Manaʻo kēlā me kēia koho
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (ʻAhahui ʻOihana Pākīpika, 2023), and directories such as Thomasnet list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes local sourcing practical to research. The table below summarizes how I weigh the two paths.
| Kumukumu | Domestic Sourcing | Overseas Sourcing |
|---|---|---|
| Kumukuai hui | Higher piece price | Often lower piece price |
| Huina koina pae aina | Lower freight, dute, and carrying cost | Added freight, dute, and inventory cost |
| Ka manawa o waena o ka hoʻomaka a i ka wā pau | Pōkole, more responsive | ʻOi aku ka lōʻihi, transit-dependent |
| Kūkākūkā | Same time zone and language | Time-zone and language gaps |
| Quality audits | On-site visits practical | Remote or costly to audit |
| pale IP | ʻOi aku ka ikaika, more enforceable | Variable enforcement |
| Kūpono maikaʻi loa | Nā moʻolelo pilikino, fast changes, proprietary tooling | Frozen designs, very high volume, price-driven programs |
Ma ka hana, I lean domestic for custom plastic profiles that involve proprietary tooling, evolving designs, or short lead times, and I consider overseas contract manufacturing only for mature, hale paʻa, high-volume parts where the landed-cost math clearly favors it. For a starting point on capabilities and stock offerings, resources like ʻO SeaGate Plastics are a useful reference when scoping a domestic partner.
Sustainability and Recyclability in Extrusion
When I evaluate a plastic extrusion companies factory today, sustainability is no longer a soft preference tucked into the back of a proposal. It sits alongside price, ka manawa o waena o ka hoʻomaka a i ka wā pau, and quality as a core selection criterion. The good news is that extrusion is inherently well suited to responsible material use, and the suppliers I trust have built that advantage into their operations rather than treating it as an afterthought.
Recyclable Thermoplastics and Scrap Reuse
Most of the polymers I specify for extruded plastic parts are thermoplastics, which means they can be remelted and reformed multiple times without a complete loss of properties. According to the US Environmental Protection Agency (2023), thermoplastics used in extrusion are recyclable, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai. That single characteristic separates them from thermosets and gives buyers real leverage on both cost and environmental footprint.
Ma ka hana, this recyclability spans the common resins you will encounter across quotes. PVC, HDPE, LDPE, and Polypropylene are among the workhorses of profile extrusion and plastic tubing, and each reclaims well when handled correctly. Engineering-grade plastics such as ABS, Polycarbonate, Nylon (PA), a me ka acrylic (PMMA) also tolerate controlled regrind, though I hold them to tighter blend ratios because their properties matter more in demanding applications. High-performance materials like PEEK and flexible TPE/TPU sit at the specialized end, where reuse requires more careful process control.
Regrind and Material Efficiency Practices
The continuous extrusion process generates predictable scrap: startup purge, trim from profile cross-section adjustments, and off-spec runs during die changeovers. A capable plastic profile manufacturer captures this material, granulates it into regrind, and reintroduces it at a defined percentage back into virgin resin. I always ask for the specifics because the details reveal how disciplined an operation really is.
- What regrind percentage do you blend into standard production, and does it change for cosmetic versus structural parts?
- How do you segregate resin types to prevent cross-contamination during resin extrusion?
- Can you document material traceability from raw resin through finished profile?
- Do you offer post-industrial recycled content options when my application allows it?
Co-extrusion deserves a mention here. By combining a virgin outer layer with a regrind or recycled core, some suppliers deliver the surface quality I need while lowering virgin material consumption. It is a practical way to reconcile appearance requirements with sustainability goals on the same part.
Choosing Environmentally Responsible Suppliers
Ma koʻu ʻike, a domestic plastics manufacturer often carries a sustainability advantage that has nothing to do with marketing. The Reshoring Initiative (2023) notes that domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona, and shorter supply chains also mean lower transport emissions. When I compare a nearby US factory against overseas alternatives, the environmental and logistical benefits frequently reinforce each other.
Beyond geography, I look for suppliers whose quality systems formalize waste reduction. ISO 9001, described by the International Organization for Standardization (2015) as the internationally recognized standard for quality management systems, does not mandate sustainability by itself, but shops that maintain it tend to run tighter processes with less scrap and better material accountability.
Regulatory and Buyer Sustainability Expectations
My downstream customers increasingly ask about recycled content, chemical compliance, and end-of-life recyclability before they will approve a part. That pressure flows straight back to how I write specifications. I now treat sustainability documentation as part of the deliverable, not a bonus. When a supplier can hand me material certifications, regrind policies, and recyclability data without hesitation, it signals a partner ready for where the market is heading rather than where it has been.
Making Your Final Decision and Requesting a Quote
Once I have shortlisted candidates, the decision comes down to matching each supplier’s real capabilities against my project’s non-negotiables. The extrusion market rewards specialization, so the goal is not finding the largest or most decorated factory but the one whose strengths line up with my part, my volumes, and my timeline.
Consolidating Your Evaluation Criteria
I bring my findings together into a single scorecard so I am comparing suppliers on the same terms. Nā koi like “nui loa” a i ʻole “maikaʻi loa” mean little in isolation; a large plastic extrusion companies factory tuned for high-volume commodity profiles may be the wrong fit for a low-volume, tight-tolerance engineering part, a me ka hope. The table below shows the weighting I typically apply, though I adjust it to the priorities of each program.
| Evaluation Criterion | What I Look For | Typical Weight |
|---|---|---|
| Material capability | Experience with my resin (PVC, HDPE, Polycarbonate, etc.) and co-extrusion if needed | Kiʻekiʻe |
| Mea hana a me ka hoʻolālā make | In-house die design, tooling lead time, revision support | Kiʻekiʻe |
| Quality system | ISO 9001 certification and documented process controls | Kiʻekiʻe |
| Volume fit | Alignment of MOQ and capacity with my annual demand | Kauwaena |
| Ka manawa o waena o ka hoʻomaka a i ka wā pau | Realistic tooling plus production schedule, quick-turnaround options | Kauwaena |
| Wahi | Domestic sourcing benefits, ukana, and responsiveness | Kauwaena |
| Hoʻomau | Regrind practices, maʻiʻo hana hou, hiki ke ʻike i nā mea | Rising |
Preparing a Clear RFQ Package
The quality of the quotes I receive is directly proportional to the quality of the request I send. A vague inquiry produces padded, cautious pricing; a complete RFQ produces sharp, comparable numbers. Extrusion carries specific cost drivers a supplier needs to see up front, chiefly the one-time tooling investment for custom profiles, which industry sourcing guidance confirms is avoided only when you use stock extruded shapes.
What Information to Include for Accurate Quotes
I make sure every RFQ package answers the questions a plastic fabrication services provider will otherwise have to ask, because each back-and-forth adds days to the timeline.
- A dimensioned drawing of the profile cross-section with tolerances. Because extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming, per Protolabs (2023), I flag which dimensions are critical and which can float.
- Material specification, including resin type, grade, kala kala, and any UV, flame, or food-contact requirements.
- Annual volume and order frequency, plus expected part length and cut tolerances.
- Whether I need custom tooling or can use a stock profile, and whether secondary operations such as cutting, kuʻi ʻana, or printing apply.
- Target price, required delivery date, and destination for landed-cost accuracy.
- Application and industry context, which helps the supplier recommend the right material and process.
Next Steps to Start Your Project
With the scorecard filled in and the RFQ ready, I send it to two or three well-matched suppliers rather than blasting a dozen. I ask for a sample or first-article inspection before committing to full production, and I confirm the tooling ownership terms in writing. Moving from prototype to production this deliberately has consistently saved me from costly surprises. Directories such as Thomasnet (2024), which list and categorize US plastic extrusion manufacturers by capability and region, remain a useful starting point when I need to widen the field, and specialist custom extruders like ʻO SeaGate Plastics illustrate how stock profiles and tubes can be fabricated into cost-effective custom parts.
Nīnau pinepine
These are the questions buyers ask me most often when they are sourcing an extrusion partner. I have kept the answers concise and practical so you can act on them quickly.
How do I find a plastic extrusion companies factory near me or in the USA?
Start with capability, then filter by geography. I search supplier directories such as Thomasnet (2024) that categorize US plastic extrusion manufacturers by region and process, then cross-check each candidate’s material and volume fit. Choosing a domestic plastics manufacturer often pays off beyond convenience: the Reshoring Initiative (2023) reports that domestic sourcing can lower freight, dute, a me nā koina lawe waihona, reducing total landed cost.
ʻEhia ke kumu kūʻai o ka extrusion plastic maʻamau?
There are two cost layers. Custom profiles require a one-time tooling and die investment, after which per-part pricing depends on resin, mānoanoa pā, ka helu puka, a me ka leo. Stock extruded shapes skip the tooling charge entirely, which is why I default to them when a standard profile meets the requirement. Because extrusion is a continuous, kaʻina hana kiʻekiʻe, unit costs typically fall as run length increases.
What is the difference between custom and stock extruded profiles?
Stock profiles are standard cross-sections a plastic profile manufacturer already produces, so they carry no tooling cost and short lead times, though the shape is fixed. Custom extrusion gives me a die designed to my exact profile cross-section, which is worth the tooling investment when the geometry, hana, or branding demands it. ʻO SeaGate Plastics (2024) also notes that standard profiles and tubes can be fabricated into cost-effective custom parts, a useful middle path when a full custom die is not justified.
How do I choose the right material for my extruded part?
I match the resin to the application. PVC is among the most widely extruded plastics for profiles, paipu, a me ka paipu. HDPE, LDPE, and Polypropylene serve well in chemical-resistant and flexible applications. When I need clarity, ikaika hopena, or heat resistance, I move to engineering-grade plastics such as Polycarbonate, ABS, ʻAlika (PMMA), or Nylon (PA), and I reserve PEEK for extreme thermal and mechanical demands. Sharing your application and environment with the supplier is the fastest route to the right recommendation.
What certifications should a quality extrusion supplier hold?
ISO 9001 is my baseline. The International Organization for Standardization (2015) describes it as the internationally recognized standard for quality management systems used across manufacturing, and it is the most widely adopted quality standard in the plastics sector. Depending on your industry, you may also require food-contact, lāʻau lapaʻau, or flame-rating compliance, so confirm those specifics against your application.
What mistakes should I avoid when sourcing an extrusion partner?
The most common ones I see are chasing “nui loa” a i ʻole “maikaʻi loa” claims without checking fit, sending incomplete drawings that produce inflated quotes, and underestimating tooling lead time. I also caution against ignoring MOQ alignment; a factory built for high-volume manufacturing may not welcome low-volume work, and a small shop may struggle with your scale. Match the supplier to the job rather than the reputation.
What are the next steps once I have chosen a supplier?
Send a complete RFQ, request a sample or first-article inspection, confirm tooling ownership in writing, and agree on a realistic schedule that separates tooling time from production time. Validating the part before full production is the single most reliable way I have found to move from prototype to production without expensive rework.
What Is a Plastic Extrusion Companies Factory and Why It Matters for B2B Buyers
When I evaluate a plastic extrusion companies factory for a client, Hoʻomaka wau me ke kaʻina hana ponoʻī, because the process defines what a supplier can and cannot do for you. Hoʻoheheʻe ʻia ka mea hoʻoheheʻe ʻia i ka plastik maka a hoʻoheheʻe ʻia i loko o kahi ʻano hoʻomau me ka ʻāpana keʻa paʻa (ʻO SeaGate Plastics, 2024). That single sentence carries more purchasing implications than most buyers realize: ka “ʻāpana keʻa paʻa” is why extrusion excels at long, uniform shapes like tubing, ʻokiʻoki, a me nā kahawai, and it is also why you cannot expect the same complex three-dimensional geometry you would get from molding.
Wehewehe: What You Are Actually Buying
Ma nā ʻōlelo kūpono, a plastic extrusion factory pushes softened resin through a shaped die to produce items such as custom plastic profiles, paipu plastik, and plastic sheet. Because this is a continuous extrusion process, it runs well for high-volume manufacturing and long production runs rather than one-off complex parts. The two categories I ask buyers to distinguish early Extrusion Plastic Manufacturing Supplier are stock extruded shapes, which are ready-made and avoid tooling, and custom extruded plastic parts, which require a die designed to your cross-section. Standard extruded profiles and tubes can also be fabricated into cost-effective custom parts with quick-turnaround production (ʻO SeaGate Plastics, 2024), which is a useful middle path when a full custom die is not justified.
Kūlana Mākeke
The US plastics industry is a major contributor to domestic manufacturing shipments and employment (ʻAhahui ʻOihana Pākīpika, 2023), so you are not sourcing from a niche trade. That scale matters for buyers: it means real competition among suppliers, redundancy if one plastic profile manufacturer cannot meet lead time, and a mature base of contract manufacturing and plastic fabrication services. It also means claims of being the “nui loa” a i ʻole “maikaʻi loa” factory are marketing shorthand, not verified rankings. I treat those labels as prompts to ask about actual line capacity, palapala hōʻoia, and reference customers rather than as evidence.
Nā noi nui a me nā mea waiwai
Material selection drives most of the outcome, so I map the resin to the application before shortlisting any supplier. Common choices I see across projects include:
- PVC — among the most widely extruded plastics globally, maʻamau i nā profiles, paipu, a me ka paipu (ʻAhahui ʻOihana Pākīpika).
- HDPE and LDPE — durable, chemically resistant polyethylenes used for tubing, nā laina laina, and industrial profiles.
- Polypropylene — lightweight and fatigue-resistant, frequently chosen for living hinges and chemical handling.
- ABS and Polycarbonate — impact-resistant options for structural trim and enclosures; polycarbonate adds optical clarity and heat resistance.
- ʻAlika (PMMA) — clarity and weatherability for lenses, hōʻike, and lighting profiles.
- Nylon (PA) a PEEK — engineering-grade plastics for wear, mahana wela, and mechanical demands; PEEK is the high-performance choice for aerospace and medical.
- TPE/TPU — flexible elastomers for seals, nā kīʻaha, and grips, often produced through co-extrusion with a rigid substrate.
Co-extrusion deserves special attention because it lets a factory combine two materials in one profile, for example a rigid PVC body with a soft TPE sealing lip. If your part needs both stiffness and flexibility, confirm the supplier runs true co-extrusion rather than secondary assembly.
Why This Matters for B2B Buyers
Understanding the process changes how you write a request for quote. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs, 2023), so specifying injection-molding-tight tolerances on an extruded profile will either inflate your price or trigger a round of clarifying questions that delays the quote. On sustainability, thermoplastics used in extrusion are recyclable, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai (EPA US, 2023), which gives you a legitimate lever for both cost and environmental goals when you discuss regrind percentages with a supplier.
How to Choose the Right Plastic Extrusion Companies Factory Supplier
Choosing a supplier is where I see the most avoidable mistakes, usually because buyers compare on unit price alone and ignore the cost drivers hiding behind that number. Below is the framework I use, built around evaluation criteria, nā hae ʻulaʻula, and a due diligence checklist you can lift directly into your sourcing process.
Vendor Evaluation Criteria
I score candidates against five dimensions rather than a single quote:
- Pāʻani hiki. Does the factory routinely run your resin and profile size? A plastic tubing supplier optimized for small-diameter medical tubing is not the same shop as one running large architectural profile extrusion.
- Quality systems. ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015) and remains the most widely adopted quality standard in the plastics sector. Certification is not a guarantee of good parts, but its absence tells me to dig deeper into inspection practices.
- Mea hana a me ka hoʻolālā make. Ask who owns the die, how long die design and tooling take, and what happens to the tool if you leave. Ownership terms are frequently buried in fine print.
- Lead time and capacity. Confirm whether quoted lead times reflect current backlog or ideal conditions. Quick-turnaround production claims should be tied to a specific committed date.
- Financial and operational stability. A supplier that becomes your sole source for a critical profile is a risk if it is financially fragile.
Understanding the Cost Drivers
Transparency on cost structure separates a strong plastic profile manufacturer from an opaque one. Three drivers determine your total price, and I ask suppliers to break them out explicitly:
| Ke kalaiwa kumu kūʻai | Stock extruded shapes | Custom extruded profiles |
|---|---|---|
| Tooling / die investment | None — profile already exists | One-time die cost required before first run (alakaʻi kumu ʻoihana, Thomasnet supplier guides) |
| Ka nui kauoha liʻiliʻi (MOQ) | Haʻahaʻa; buy by the length | Kiʻekiʻe; tied to setup and material changeover |
| Ka manawa o waena o ka hoʻomaka a i ka wā pau | Short — often shelf stock | ʻOi aku ka lōʻihi; includes die fabrication and first-article approval |
| Per-unit price at volume | Fixed by catalog | Lower at high volume once tooling is amortized |
| Kūpono maikaʻi loa | Prototyping, haʻahaʻa leo, standard cross-sections | Proprietary geometry, high-volume manufacturing, prototype to production scale-up |
Custom extrusion typically requires a one-time tooling investment, ʻoiai ke pale aku nei nā ʻikepili waiwai i kēia kumukūʻai (alakaʻi kumu ʻoihana). Ma koʻu ʻike, buyers who plan to scale from prototype to production should quote the custom die early even if they start with stock shapes, so the amortized per-unit price is visible before volumes ramp.
Red Flags I Watch For
- Refusal to share ISO or equivalent quality documentation, or vague answers about inspection frequency.
- Quotes with no tooling line item, which usually means the cost reappears later or the die is undersized.
- Unwillingness to provide references in your industry or sample parts.
- Tolerances promised on paper that are tighter than what continuous extrusion realistically holds — a sign the supplier may be overselling.
- “Largest” a i ʻole “maikaʻi loa” claims with no capacity data, palapala hōʻoia, or customer evidence behind them.
Ka Papa Hoopono Pono
Before I commit to a Plastic Extrusion Companies Factory supplier, I confirm every item below in writing:
- Do you hold ISO 9001 or an equivalent, and can I see the certificate and scope?
- Which resins do you run in production, and can you handle my material — PVC, ABS, polycarbonate, HDPE, LDPE, polypropylene, or an engineering grade?
- What tolerances do you guarantee for this profile cross-section, and how are they measured?
- What is the tooling cost, ka manawa o waena o ka hoʻomaka a i ka wā pau, and MOQ, and who owns the die?
- Do you offer co-extrusion and secondary fabrication in-house?
- What percentage of regrind is used, and how does that affect certification and appearance?
- Can you provide first-article inspection reports and material certifications?
- What is your realistic committed lead time given current backlog?
Find Plastic Extrusion Companies and Factories in the United States
Buyers frequently search for a plastic extrusion factory “kokoke iaʻu” a i ʻole “in the USA,” and the location question is more strategic than it first appears. Domestic sourcing is not only about proximity; it changes your total landed cost and your supply-chain risk profile.
Where to Start Your Search
Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a practical first filter when you want to build a shortlist by material, kaʻina hana, or state. I pair directory research with capability-specific sources such as custom plastic extrusion manufacturer references to understand what a given shop actually produces before I reach out. The goal at this stage is a shortlist of five to eight candidates whose capabilities genuinely match your resin and profile, not a long list of names. ʻO nā hui hoʻoheheʻe plastik
Key Considerations for Domestic Sourcing
Reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023). For extruded parts, which are often bulky and low in value density, freight is a meaningful line item, so a domestic plastics manufacturer closer to your assembly point can offset a higher unit price. I weigh three factors:
- Huina koina pae aina, ʻaʻole ke kumu kūʻai. Add freight, dute, and the carrying cost of the safety stock you need to cover long overseas transit.
- Communication and design iteration. Domestic time-zone alignment speeds up die design and tooling revisions during the prototype-to-production phase.
- Supply resilience. Shorter lines reduce exposure to port delays and long lead-time shocks.
Interpreting “Largest” a “Best” Factory Claims
Location searches often surface superlatives, and I treat them skeptically. “Largest” tells you nothing about whether a factory runs your material or holds your tolerances. aka, I convert vague claims into verifiable questions: How many extrusion lines run my resin family? What is your on-time delivery rate? Which certifications do you hold? A smaller shop that specializes in your profile is frequently a better partner than a large one for which your job is an afterthought.
Practical Tips and Industry Context
A few habits have consistently saved my clients time and money. Ka mua, request stock extruded shapes for early validation before investing in a custom die — it lets you test fit and function cheaply. Ka lua, share a dimensioned drawing with realistic extrusion tolerances up front so quotes are comparable. Ke kolu, confirm the supplier’s regrind policy, since recyclable thermoplastics and regrind reuse improve material efficiency (EPA US, 2023) but can affect appearance on cosmetic parts. ʻO ka hope loa, remember that plastic extrusion is a continuous, high-volume process well suited to long production runs, so it rewards buyers who can consolidate demand and forecast accurately. Within the mature US plastics manufacturing base (ʻAhahui ʻOihana Pākīpika, 2023), you have room to be selective — use it, and let a structured checklist rather than a headline claim decide your Plastic Extrusion Companies Factory supplier.
Locate a plastic extrusion factory near my location
When buyers ask me how to find a plastic extrusion factory nearby, I remind them that “kokoke iaʻu” is really shorthand for two goals: shorter freight lanes and easier communication. Extrusion melts raw plastic material and forms it into a continuous profile with a fixed cross-section (ʻO SeaGate Plastics, 2024), and because that continuous extrusion process runs at high volume, the finished product is often bulky and freight-sensitive. Ma koʻu ʻike, the cost of moving extruded plastic parts across the country can quietly erode the price advantage of a distant supplier, so location genuinely matters.
Key considerations for local sourcing
I start every local search by matching capability to geography rather than proximity alone. A plastic profile manufacturer two states away with the right die design and tooling almost always beats a closer shop that cannot hold your profile cross-section. I evaluate three things in order: the materials they run (PVC, ABS, polycarbonate, HDPE, LDPE, polypropylene, acrylic, and engineering-grade resins such as nylon or PEEK), the processes they offer (extrusion profile, extrusion pepa iila, paipu, a me ka co-extrusion), and their quality systems. ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015), so I treat certification as a baseline filter, not a bonus.
Practical tips to find and vet a factory
Thomasnet supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which makes them a reliable starting point for a location-based shortlist. Mai laila mai, I qualify each candidate with a consistent set of questions before I ever request a quote.
My local supplier vetting checklist
- Which resins do you extrude in-house, and can you run regrind for material efficiency?
- Do you offer co-extrusion or dual-durometer profiles if my part needs a soft-touch or barrier layer?
- What tolerances can you hold, and how do you document them?
- Are you ISO 9001 hooiaio, and can you share a recent audit summary?
- What is your typical lead time from approved die to first article?
- Do you provide plastic fabrication services (ʻoki ʻoki, kuʻi ʻana, wili ʻana) so I receive finished parts, not just stock lengths?
pōʻaiapili ʻoihana
Domestic proximity is more strategic than it looks. Reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023). Because the US plastics industry is a major contributor to domestic manufacturing shipments and employment (ʻAhahui ʻOihana Pākīpika, 2023), most regions have a viable domestic plastics manufacturer within a reasonable freight radius. I tell buyers that “kokoke iaʻu” should mean near enough to control landed cost and lead time, which is often a regional rather than a strictly local decision.
Identify the largest plastic extrusion companies in the US
Buyers frequently ask me to point them to the “nui loa” ʻoihana extrusion plastic, and my first move is always to define what “nui loa” means for their project. Size can describe revenue, plant footprint, number of extrusion lines, or annual resin throughput, and those metrics do not always move together. A plastic extrusion companies factory supplier with enormous pipe capacity may be the wrong fit for a low-volume acrylic profile, so I interpret scale through the lens of the specific job.
Key considerations when “nui loa” mea pili
Scale earns its keep on long production runs. Plastic extrusion is a continuous, high-volume process well suited to long production runs, so the largest producers shine when you need millions of feet of PVC profile or HDPE pipe on a predictable schedule. ʻO PVC kekahi o nā plastic extruded loa i ka honua, hoʻohana mau ʻia i nā profiles, paipu, a me ka paipu, which is why the biggest players tend to concentrate capacity there. If your program is high-volume and standardized, a large plastic profile manufacturer offers redundancy, buffer inventory, and pricing leverage. If your program is small or highly custom, that same scale can translate into higher minimums and less flexibility.
Practical tips for evaluating scale claims
I never take a marketing claim of “nui loa” at face value. aka, I ask for concrete indicators: number of extrusion lines by size class, resins run at volume, and the split between stock extruded shapes and custom work. A large firm quoting a wholesale program should be able to show quick-turnaround production capacity, secondary plastic fabrication services, and a documented MOQ structure. The table below summarizes how I weigh large versus specialized suppliers.
Large versus specialized extrusion suppliers
| Kumukumu | Largest producers | Specialized suppliers |
|---|---|---|
| Kūpono maikaʻi loa | Nui-nui, standardized runs (paipu, Hōʻike PVC) | Custom plastic profiles, engineering-grade resins |
| Ka nui kauoha liʻiliʻi | Higher MOQ to justify line time | Lower MOQ, more flexible |
| Uku mea hana | Amortized across large volumes | One-time die cost more visible per unit |
| Ka manawa o waena o ka hoʻomaka a i ka wā pau | Predictable, buffered by capacity | Hoʻololi, project-dependent |
| Laulā mea | Commodity resins (PVC, HDPE, LDPE, PP) | Specialty resins (PC, PMMA, PA, PEEK, TPE/TPU) |
| Hoʻokuʻu hui | Common on standard lines | Often available for niche multi-layer parts |
pōʻaiapili ʻoihana
The largest US extruders are anchored in commodity, freight-heavy products where continuous, high-volume manufacturing rewards efficiency. Custom extrusion typically requires a one-time tooling or die investment, ʻoiai ke pale aku nei nā ʻikepili waiwai i kēia kumukūʻai, so large producers often lead with catalogs of stock extruded shapes. I remind buyers that “nui loa” is a useful signal for reliability and capacity, but it is not a proxy for quality or fit. The right size is the one that matches your volume, mea waiwai, and tolerance needs.
Discover the best-rated plastic extrusion manufacturers
“Best-rated” is the claim I scrutinize most, because ratings can reflect genuine performance or simply strong marketing. Ma koʻu ʻike, the manufacturers worth shortlisting are the ones that make their quality measurable. I look past star counts and testimonials for evidence I can verify: palapala hōʻoia, documented tolerances, hiki ke ʻike i nā mea, and a track record of moving projects from prototype to production without surprises.
Key considerations for judging quality
Quality management is the foundation. ISO 9001 is the most widely adopted quality management standard, used across manufacturing sectors including plastics, so I treat it as table stakes for a best-rated plastic extrusion companies factory manufacturer. Beyond certification, I assess how a supplier handles tolerances. Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs, 2023), and the best manufacturers explain that reality up front rather than overpromising. A shop that gives me realistic tolerance ranges and a clear inspection plan earns more trust than one quoting numbers it cannot hold.
Practical tips for choosing the best-rated supplier
I use a material selection framework tied to the application. The resin drives the manufacturer, not the other way around.
- PVC — profiles, paipu, and tubing where cost and rigidity matter.
- ABS and polycarbonate — impact-resistant parts; polycarbonate adds clarity and heat tolerance.
- HDPE and LDPE — chemical resistance and flexibility for tubing and liners.
- Polypropylene — lightweight parts needing fatigue and chemical resistance.
- ʻAlika (PMMA) — optical clarity for lighting and display profiles.
- Nylon (PA) a PEEK — engineering-grade parts under mechanical or thermal stress.
- TPE/TPU — flexible seals and gaskets, often via co-extrusion.
Once the material is set, I confirm the supplier offers the matching process, whether that is profile extrusion, extrusion pepa iila, or resin extrusion with co-extrusion for multi-layer parts. Hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau me ka hoʻololi wikiwiki (ʻO SeaGate Plastics, 2024), so I favor manufacturers that pair extrusion with in-house fabrication and prototype-to-production support. For a working example of custom capability and stock profile options, I point buyers to references such as ʻO SeaGate Plastics.
pōʻaiapili ʻoihana
The best-rated manufacturers increasingly compete on sustainability alongside quality. Hiki ke hoʻohana hou ʻia nā Thermoplastics i hoʻohana ʻia i ka extrusion, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai (EPA US, 2023), so I ask top candidates how they manage scrap and regrind. A manufacturer that documents its quality system, states honest tolerances, and runs an efficient material loop tends to be “best-rated” for reasons that hold up under a plant visit. That is the standard I apply, and it is the one I recommend every buyer use before committing to a contract manufacturing partner.
Understand how the plastic extrusion manufacturing process works
I koʻu loiloi ʻana i kahi mea hana kiʻi plastik, I start by making sure the buyer understands what actually happens on the shop floor. Hoʻoheheʻe ʻia ka mea hoʻoheheʻe ʻia i ka plastik maka a hoʻoheheʻe ʻia i loko o kahi ʻano hoʻomau me ka ʻāpana keʻa paʻa (ʻO SeaGate Plastics, 2024). That single sentence carries most of what you need to know: the process is continuous, the cross-section is constant along the length, and the shape is defined by tooling rather than by a closed mold.
The core stages of the continuous extrusion process
Ma ka hana, I describe the workflow in five stages. Ka mua, resin pellets are fed into a hopper. Ka lua, a heated barrel with a rotating screw melts and pressurizes the material, which is why practitioners often call it resin extrusion. Ke kolu, the molten polymer is forced through a die that establishes the profile cross-section. Ka ʻehā, the extrudate is cooled in a water bath or air rack so it holds its geometry. Ka lima, pullers draw the part at a steady rate before a saw or cutter sizes it. Because nothing stops between stages, the method is genuinely a continuous extrusion process rather than a cycle-by-cycle one.
Why tolerances differ from injection molding
One point I raise early with engineering teams: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Nā Punawai Hoʻolālā Protolabs, 2023). This is not a defect. It reflects the physics of pulling a hot polymer through open tooling and cooling it under tension. If your extruded plastic parts need tight dimensional control on a specific feature, plan for secondary machining or specify that feature as a fabrication step rather than expecting the die alone to hold it.
Co-extrusion and profile extrusion variants
Profile extrusion covers the custom cross-sections most buyers picture: nā kahawai, nā kīʻaha, ʻokiʻoki, a me nā ʻano hana. Co-extrusion runs two or more materials through the die at once, which lets you combine, ʻo kahi laʻana, a rigid PVC body with a flexible TPE/TPU sealing lip in a single pass. I find co-extrusion is where a capable factory earns its rate, because it removes a downstream assembly step and improves seal performance. Plastic sheet extrusion and tubing use the same fundamentals with different die and downstream setups.
Industry context and material efficiency
Extrusion suits high-volume manufacturing because it is inherently a continuous, high-volume process well suited to long production runs. Once a die is dialed in, output scales with line speed and run time. It also has a reasonable sustainability story: thermoplastics used in extrusion are recyclable, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai (EPA US, 2023). Ma koʻu ʻike, asking a supplier how they handle regrind tells you a lot about both their cost discipline and their process control.
Compare custom vs stock plastic extrusion suppliers
The most consequential sourcing decision I help buyers make is custom versus stock. It drives your tooling cost, ka nui kauoha liʻiliʻi, and lead time all at once. The right answer depends on how closely a standard shape fits your application and how much volume you expect to run.
What separates the two paths
ʻO ka extrusion maʻamau e koi i kahi mea hana hoʻokahi manawa a make hoʻolimalima, ʻoiai ke pale aku nei nā ʻikepili waiwai i kēia kumukūʻai. Hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau me ka hoʻololi wikiwiki (ʻO SeaGate Plastics, 2024). So there is a middle path many buyers miss: start from a stock extruded shape and fabricate it, capturing part of the customization benefit without paying for a new die.
Cost drivers to model before you request a quote
When I build a sourcing model, I separate three drivers so the numbers stay honest:
- Die design and tooling: a one-time cost on custom work, typically amortized across your first order or two.
- MOQ: custom lines carry higher minimums to justify setup and purge material; stock shapes can ship in small quantities.
- Ka manawa o waena o ka hoʻomaka a i ka wā pau: stock ships quickly; custom adds die fabrication and first-article approval before production begins.
Papa hoʻohālikelike: custom vs stock extrusion
| Kumukumu | Custom profile extrusion | Stock extruded shapes |
|---|---|---|
| Uku mea hana | One-time die investment required | ʻAʻohe |
| Ka nui kauoha liʻiliʻi | Kiʻekiʻe, to amortize setup | Haʻahaʻa, often cut-to-length |
| Ka manawa o waena o ka hoʻomaka a i ka wā pau | ʻOi aku ka lōʻihi (make kukulu + ʻatikala mua) | Quick-turnaround production |
| Dimensional fit | Exact cross-section to spec | Nearest standard, plus fabrication |
| Best for | Sustained volume, unique geometry | Prototypes, haʻahaʻa leo, near-fit needs |
| Unit price at scale | E hoʻohaʻahaʻa i ka wā e hoʻopau ʻia ai nā mea hana | Higher per unit for heavy customization |
A vetting checklist for either path
Whether you pursue a custom plastic profile manufacturer or a stock plastic tubing supplier, I ask the same core questions. Is the shop certified to ISO 9001, the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015)? ISO 9001 is the most widely adopted quality management standard across manufacturing sectors including plastics, so its absence is worth a direct conversation. Beyond certification, I ask:
- Which resins do you run in-house, and can you handle engineering-grade plastics like polycarbonate, nylon (PA), or PEEK?
- Do you offer co-extrusion and downstream plastic fabrication services?
- How do you document tolerances and first-article inspection?
- What is your true MOQ, and how is tooling amortized on the initial order?
- Can you support the move from prototype to production without re-tooling?
Location intent: near me and in the USA
Buyers frequently search for a Plastic Extrusion Companies Factory supplier “kokoke iaʻu” or a domestic plastics manufacturer in the USA. Two resources help here. Thomas supplier directories list and categorize US plastic extrusion manufacturers by capability and region (Thomasnet, 2024), which is a practical starting point for shortlisting. And the case for domestic sourcing is more than convenience: reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023). I treat “nui loa” a “maikaʻi loa” factory claims with skepticism; capability fit for your specific resin, hoʻomanawanui, and volume matters far more than a superlative on a homepage.
Learn what products can be made through plastic extrusion
Extrusion produces a broader range of products than most buyers expect, and the material you choose shapes both what is possible and what it costs. I organize my recommendations around a material selection framework tied to application and industry rather than a generic parts list.
Common extruded product categories
The workhorse outputs are custom plastic profiles, paipu, pepa, nā kahawai, ʻokiʻoki, nā kīʻaha, a me nā ʻano hana. Anything with a consistent profile cross-section along its length is a candidate. ʻO PVC kekahi o nā plastic extruded loa i ka honua, hoʻohana mau ʻia i nā profiles, paipu, a me ka paipu (ʻAhahui ʻOihana Pākīpika). That prevalence is why so many stock extruded shapes are available in PVC first.
Material selection framework
Here is how I match resins to needs across the polymers you will encounter most often:
- PVC: waiwai, rigid or flexible, strong for profiles, paipu, a me ka paipu.
- ABS: tough and impact-resistant, common in housings and trims.
- Polycarbonate: high impact strength and clarity for glazing and guards.
- HDPE and LDPE: chemically resistant polyolefins for tubing, nā laina laina, and low-cost profiles; HDPE brings more rigidity, LDPE more flexibility.
- Polypropylene: māmā, pale kemika, and fatigue-tolerant for living hinges and profiles.
- ʻAlika (PMMA): optical clarity for display and lighting profiles.
- Nylon (PA): wear resistance and strength for mechanical parts.
- PEEK: high-temperature, chemically robust engineering-grade plastic for demanding aerospace and medical work.
- TPE/TPU: flexible elastomers ideal for seals and soft-touch co-extruded lips.
Industry applications
Construction relies on PVC and ABS profiles for window frames, ʻokiʻoki, and edging. Medical and lab work uses acrylic, polypropylene, a me nā paipu PEEK a me nā kahawai. Hoʻopili nā mea uila a me nā mea hana i nā hale polycarbonate a me ABS. Ke hilinaʻi nei nā laina ʻoihana a me ka hoʻohana wai i ka HDPE a me ka nylon. ʻO ka hoʻopaʻa ʻana i kāu ʻoihana i kēia mau resins e hoʻomau i ke kamaʻilio ʻōlelo ʻana a pale aku i ka wehewehe ʻana i kahi mea i hana ʻia ʻaʻole pono ʻoe..
Nā ʻōlelo aʻoaʻo no ka neʻe ʻana mai ka manaʻo i ka hana
Ma koʻu ʻike, ʻekolu mau maʻamau e mālama i nā papahana extrusion ma ka papa manawa. Ka mua, prototype mai nā kiʻi kiʻi i ʻae ʻia e ka geometry, a laila hoʻopaʻa i nā mea hana maʻamau ma hope o ka hōʻoia ʻana o ka hoʻolālā, ka mea e pale ana i kou hoʻolilo make. Ka lua, e kuhikuhi i ka ʻae ʻana ma ka hiʻohiʻona ma mua o ka hoʻopaʻa paʻa ʻana i ka ʻaoʻao holoʻokoʻa, no ka mea e pili ana i ke kaʻina hana a me ka mālama ʻana i ke kumukūʻai. Ke kolu, hōʻoia e hiki i kāu mea hoʻolako ke lawe i ka ʻāpana mai ka prototype i ka hana ma ka laina like, no laila ʻaʻole e koi ka scale-up i kahi ʻōlelo hou. Handled this way, extrusion delivers custom parts economically, with the quick turnaround that makes the process attractive in the first place.
For a deeper look at fabricating cost-effective custom parts from standard and custom profiles, I point buyers to ʻO SeaGate Plastics’ extrusion overview.
Bringing Your Extrusion Sourcing Strategy Together
After walking through capabilities, mea waiwai, and vetting criteria, the through-line I keep returning to is this: choosing among plastic extrusion companies and factories is less about finding the “nui loa” a i ʻole “maikaʻi loa” name and more about matching a supplier’s real strengths to your specific part, leo nui, a me ka laina manawa. A continuous, high-volume manufacturing process rewards long production runs, but the same shop that excels at a million linear feet of PVC profile may not be the partner I want for a low-volume PEEK prototype. Ma koʻu ʻike, buyers who define the problem precisely before they request quotes get sharper pricing and fewer surprises downstream.
Material selection sits at the center of every good decision. Whether the application calls for rigid PVC or ABS in structural profiles, polycarbonate or acrylic (PMMA) for optical clarity, HDPE a me LDPE no ke kū'ē kemika, polypropylene no nā ʻeke ola, nylon (PA) for wear surfaces, or TPE/TPU for flexible seals, the resin drives tooling, hoʻomanawanui, a me ke kumukuai. Extrusion melts raw plastic and forms it into a continuous profile with a fixed cross-section (ʻO SeaGate Plastics, 2024), a hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau kumukūʻai me ka huli wikiwiki (ʻO SeaGate Plastics, 2024). That combination of stock shapes and custom profile extrusion, sometimes paired with co-extrusion for multi-material geometry, is what makes the process so versatile from prototype to production.
On the commercial side, I always separate one-time and recurring costs. Custom extrusion typically carries a one-time tooling and die investment, while stock profiles avoid it, so the die design and tooling decision shapes the whole business case. Domestic sourcing deserves a second look too: reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023), which often narrows the gap that offshore unit pricing appears to open. And because thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (U.S. EPA, 2023), a quality-focused domestic plastics manufacturer can support both cost and sustainability goals at once.
Quality systems are the final filter I apply. ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing (ISO, 2015), and it remains the most widely adopted benchmark I look for when comparing a custom plastic extrusion manufacturer against its peers. Pair that with realistic expectations on precision, since extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Protolabs, 2023), and you have a grounded framework for evaluating any plastic profile manufacturer or plastic tubing supplier.
ʻIke ʻike
| Lae Kii | Wehewehe |
|---|---|
| Match process to volume, not to reputation | Continuous extrusion is a high-volume process best suited to long production runs, so I weigh a factory’s real strengths against my order size rather than chasing “nui loa” a i ʻole “maikaʻi loa” claims. |
| Separate tooling from unit price | Custom profiles require a one-time die investment while stock extruded shapes avoid it; understanding this split keeps the true cost of custom plastic profiles from hiding inside a quoted per-foot rate. |
| Verify quality before precision expectations | ISO 9001 palapala hōʻoia (ISO, 2015) signals a managed process, and I set tolerance expectations knowing extrusion runs looser than injection molding (Protolabs, 2023). |
Nā ʻōlelo aʻoaʻo no nā mea kūʻai mai B2B
- Define the part before you shop. Document the profile cross-section, resin (PVC, ABS, polycarbonate, HDPE, polypropylene, or an engineering-grade plastic), nui makahiki, and target tolerance so every plastic extrusion companies factory supplier quotes against the same brief.
- Ask for tooling, MOQ, and lead-time numbers separately. Request the die cost, ka nui kauoha liʻiliʻi, and quoted lead time as distinct line items to compare custom extrusion and stock profiles on equal footing.
- Confirm the quality system in writing. Ask for a current ISO 9001 certificate and the inspection points used on extruded plastic parts, rather than accepting a general quality claim.
- Weigh domestic sourcing on total landed cost. Compare a domestic plastics manufacturer against offshore options using freight, dute, a me nā koina lawe waihona, not unit price alone (Hoʻomaka hou ʻana, 2023).
- Test the relationship with a small run. Move from prototype to production in stages so you validate quick-turnaround performance and communication before committing to high-volume manufacturing.
- Use supplier directories as a starting list, ʻaʻole he papa inoa pōkole. Directories such as Thomasnet (2024) help you locate regional plastic fabrication services, but I still vet capability, mea waiwai, and certification directly with each shop.
FAQ
How do I find plastic extrusion companies or a factory near me?
When I evaluate location intent, I start by mapping suppliers against my shipping lanes rather than pure geographic proximity. A plastic profile manufacturer two states away with the right die design and tooling capability often beats a closer shop that lacks my resin. I use supplier directories that list and categorize US plastic extrusion manufacturers by capability and region to build a shortlist, then verify with a plant visit or video walkthrough. Thomas directories are a practical starting point for this (Thomasnet, 2024, thomasnet.com). Ma koʻu ʻike, “kokoke iaʻu” should mean short, predictable lead times and low freight, not just a nearby ZIP code.
What should I look for in plastic extrusion manufacturers in the USA?
For domestic sourcing, I weigh three things: certified quality, material breadth, a me ka huina o ke kumukuai pae aina. A domestic plastics manufacturer can reduce total landed cost by lowering freight, dute, a me nā koina lawe waihona (Hoʻomaka hou ʻana, 2023, reshorenow.org), which often narrows the gap with offshore quotes once you account for the full picture. The US plastics industry is also a major contributor to domestic manufacturing shipments and employment (ʻAhahui ʻOihana Pākīpika, 2023), so the supplier base is deep. I confirm they run the resins I need, from commodity grades like PVC, HDPE, LDPE, and polypropylene to engineering-grade plastics such as polycarbonate, nylon (PA), a PEEK.
How do I choose the right plastic extrusion supplier for my project?
I treat supplier selection as a vetting checklist, not a gut call. The concrete questions I ask every candidate:
- Do you hold ISO 9001 palapala hōʻoia, the internationally recognized standard for quality management systems (ISO, 2015)?
- Which resins and profiles do you run in production, and do you offer co-extrusion?
- What are your tolerances, and how do you handle profile cross-section validation?
- What is your minimum order quantity (MOQ), tooling lead time, and production lead time?
- Can you support the full path from prototype to production and quick-turnaround production for reorders?
Industrial Plastic Extrusion Parts The biggest mistake I see buyers make is choosing on unit price alone and ignoring tooling cost, MOQ, and lead-time risk. Those drivers usually decide whether a program is actually profitable.
What is the difference between custom and stock plastic extrusions?
Stock extruded shapes are standard profiles and tubes a supplier already produces, so you skip tooling and buy off the shelf. Custom extrusion requires a one-time tooling and die investment to create your unique profile cross-section. He maʻalahi ke kālepa: stock plastic extrusions minimize upfront cost and lead time, while custom plastic profiles fit your exact geometry. ʻIke ʻia, standard extruded profiles and tubes can be fabricated into cost-effective custom parts with quick turnaround (ʻO SeaGate Plastics, 2024, seagateplastics.com), so I often prototype with stock shapes before committing to a die.
How should I read “nui loa” a “maikaʻi loa” plastic extrusion factory claims?
I read those labels with healthy skepticism. “Largest” usually reflects capacity or revenue, which matters for high-volume manufacturing but tells me nothing about fit for a low-volume, tight-tolerance job. “Best” is subjective marketing unless it is backed by certifications, nā kuhikuhi, and capability data. My rule: rank suppliers against my own requirements, not against a generic superlative. The largest plastic extrusion company on a list may be the wrong contract manufacturing partner for a specialty acrylic (PMMA) or TPE/TPU part, while a mid-size specialist nails it.
What are plastic extrusion profiles, and how are they made?
A profile is a continuous shape with a fixed cross-section. Hoʻoheheʻe ʻia ka mea hoʻoheheʻe ʻia i ka plastik maka a hoʻoheheʻe ʻia i loko o kahi ʻano hoʻomau me ka ʻāpana keʻa paʻa (ʻO SeaGate Plastics, 2024). Because it is a continuous forming process, resin extrusion is well suited to long production runs and high-volume manufacturing. It also supports plastic sheet extrusion and tubing. One thing I always plan around: extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming (Nā Punawai Hoʻolālā Protolabs, 2023), so I set tolerance expectations early with the plastic tubing supplier or profile shop.
Which plastic material should I choose for my extruded parts?
I anchor material selection to the application, not habit. PVC is among the most widely extruded plastics globally and is common in profiles, paipu, a me ka paipu. For impact and appearance, I look at ABS or polycarbonate; for chemical resistance and living hinges, polypropylene; for outdoor and clarity, acrylic (PMMA); and for demanding thermal or wear conditions, nylon (PA) or PEEK. I also confirm recyclability up front, since thermoplastics used in extrusion are recyclable and regrind reuse improves material efficiency (EPA US, 2023). Matching resin to service environment prevents the costly redesigns I have watched derail otherwise solid programs.
What drives the cost of extruded plastic parts?
Three levers move price more than anything else. Ka mua, mea paahana: a custom die is a one-time investment that stock profiles avoid entirely. Ka lua, MOQ and run length, since extrusion rewards volume and unit cost drops as quantities rise. Ke kolu, pae waiwai, where engineering-grade plastics and specialty resins cost well above commodity options. When I request a quote, I ask suppliers to break out tooling, per-unit price, and secondary plastic fabrication services separately so I can compare offers on equal terms and identify where the real cost lives.
Nā kuhikuhi
- Hoʻoheheʻe ʻia ka mea hoʻoheheʻe ʻia i ka plastik maka a hoʻoheheʻe ʻia i loko o kahi ʻano hoʻomau me ka ʻāpana keʻa paʻa. — ʻO SeaGate Plastics (2024)
- Hiki ke hana ʻia nā ʻaoʻao extruded maʻamau a me nā paipu i loko o nā ʻāpana maʻamau me ka hoʻololi wikiwiki. — ʻO SeaGate Plastics (2024)
- ISO 9001 is the internationally recognized standard for quality management systems used across manufacturing. — International Organization for Standardization (2015)
- The US plastics industry is a major contributor to domestic manufacturing shipments and employment. — ʻAhahui ʻOihana Pākīpika (2023)
- Reshoring and domestic sourcing can reduce total landed cost by lowering freight, dute, and inventory carying costs. — Hoʻomaka hou ʻana (2023)
- Extrusion tolerances are generally looser than injection molding due to material shrinkage and continuous forming. — Nā Punawai Hoʻolālā Protolabs (2023)
- Hiki ke hoʻohana hou ʻia nā Thermoplastics i hoʻohana ʻia i ka extrusion, a ʻo ka hoʻohana hou ʻana e hoʻomaikaʻi i ka pono waiwai. — ʻOihana Hoʻomalu Kaiapuni ʻAmelika (2023)
- Thomas suplier directories list and categorize US plastic extrusion manufacturers by capability and region. — Thomasnet (2024)
- Plastic extrusion is a continuous, high-volume process well suited to long production runs, per general industry manufacturing references (SPI/Plastics Industry Association overview). — Planning analysis
- ʻO PVC kekahi o nā plastic extruded loa i ka honua, hoʻohana mau ʻia i nā profiles, paipu, a me ka paipu (ʻAhahui ʻOihana Pākīpika). — Planning analysis