

Aportacions clau
- En la meva experiència, les decisions a l'engròs més intel·ligents comencen amb la comparació de la classe de la màquina amb la matèria primera: Les extrusores d'un sol cargol manegen PVC senzill, HDPE, i perfils de polipropilè, Les extrusores de doble cargol s'adapten a polímers complexos i exigents, i les extrusores de reciclatge de plàstic dedicades existeixen com una classe diferent per a escates de plàstic recuperades (font: ThoYu, 2024).
- Sempre avaluo les especificacions abans del preu. Nombres bàsics com la relació L/D, recompte de zones de barrils, relació de reducció de la caixa de canvis, factor de servei, i la potència del motor us diuen molt més sobre la capacitat real que una xifra de sortida del titular. Per referència, uns parells d'extrusora Davis Standard de 9 polzades utilitzats a 32:1 Relació L/D i canó de 7 zones amb a 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron).
- Els preus directes de fàbrica dels fabricants de la Xina són realment competitius per als equips nous (font: ThoYu, 2024), però ho sospeso amb una imatge total del cost total de propietat que inclou els drets d'importació, mercaderies marítimes, aparell, instal·lació, i accés al suport postvenda.
- Tracto el nou, utilitzat, i s'han importat com a tres vies de contractació separades, cadascun amb els seus propis compromisos. El mercat d'ocasió ha madurat, Llistes específiques de marca per a extrusores d'un sol cargol (font: Equips Aaron), que el converteix en un camí viable quan puc verificar l'estat i el desgast.
- La verificació del proveïdor i la protecció de pagaments importen tant com la fitxa d'especificacions. Abans de comprometre's, Confirmo la quantitat mínima de comanda, terminis de lliurament, termes de garantia, i disponibilitat de recanvis, i estructuré els pagaments per protegir-nos de la manca de lliurament.
- Els fonaments del procés guien els meus controls: la matèria primera entra per un alimentador de tremuja en pols, pellet, o en forma de grànuls, es fon amb tubs de calefacció elèctrica, i s'homogeneïtza mitjançant una cisalla de cargol abans que la matriu d'extrusió formi un perfil de secció transversal contínua (fonts: ThoYu; Amade-Tech).
- Confirmo la gestió tèrmica per endavant. Els barrils multizona solen combinar calefacció elèctrica amb refrigeració per aigua de circuit tancat (font: Especificacions de l'equip Aaron), i un control fiable de la temperatura de fusió és el que manté la sortida dimensionalment coherent entre les canonades, tubs, pel·lícules, taules, i ampolles.
- La configuració del cargol i les eines de matriu personalitzades defineixen el que realment pot fer una línia, així que els abasto contra la meva combinació de productes en lloc de comprar capacitat genèrica. Per a R&D o tirades petites, una extrusora a escala de laboratori construïda per a una sortida contínua de secció transversal uniforme és sovint el punt d'entrada correcte (font: Amade-Tech).
Què és una màquina d'extrusió de plàstic i com funciona?
Quan avaluo qualsevol màquina de processament de polímers, Començo amb el mateix model mental: una extrusora és un sistema de fusió i conformació controlada. El plàstic sòlid va en un extrem, i un continu, perfil de secció transversal uniforme surt de l'altre. Tot entre aquests dos punts es tracta d'aplicar calor i cisalla mecànica al ritme adequat. Entendre aquest flux és el que separa un comprador confiat d'algú que endevini els fulls d'especificacions, i modela directament com m'apropo a Venda a l'engròs de màquines d'extrusió de plàstic compra.
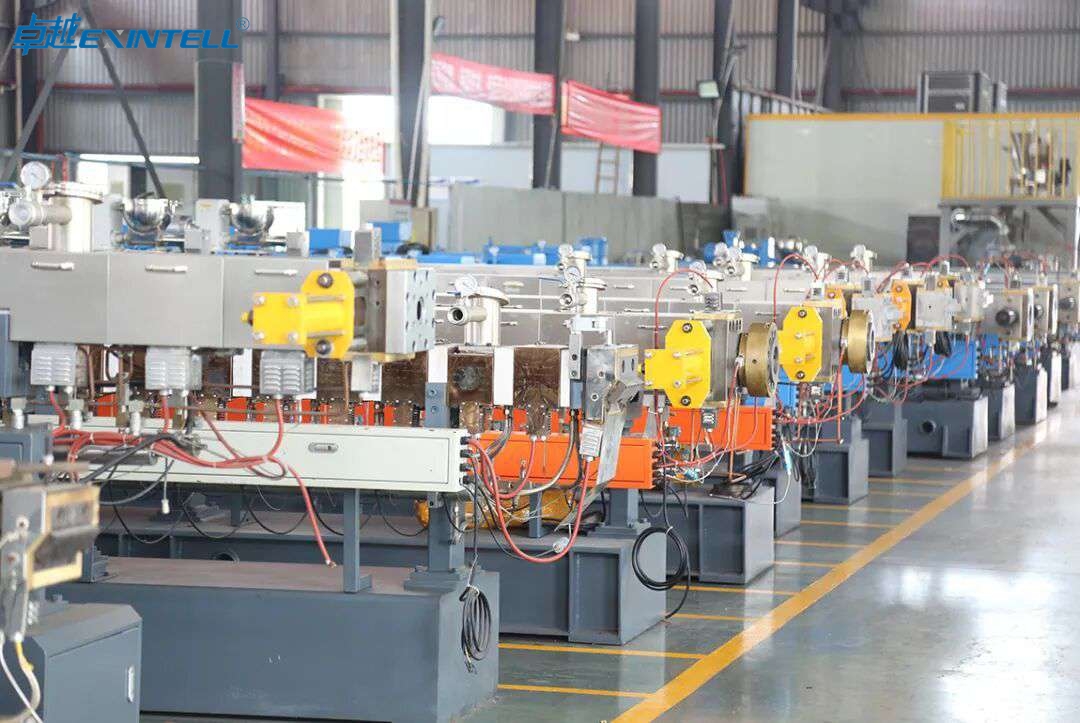
El procés de fusió del nucli
Dins de la màquina, El plàstic sòlid es transporta cap endavant mitjançant un cargol giratori mentre els tubs de calefacció elèctrica embolcallen el canó en diverses zones. El plàstic es fon mitjançant una combinació d'aquesta calor externa i la cisalla interna generada quan el cargol força el material contra la paret del canó.. Segons ThoYu, El plàstic d'una extrusora es fon mitjançant tubs de calefacció elèctrica i es transforma en una fusió uniforme mitjançant l'extrusió de cargols i l'acció de tall (ThoYu, 2024). Aquell mecanisme dual, calor conductora més fricció mecànica, és per això que la geometria del cargol importa tant com la temperatura del barril.
El control de la temperatura de fusió és la part que examino més en qualsevol cita. Els barrils multizona solen combinar calefacció elèctrica amb refrigeració d'aigua de circuit tancat per mantenir cada zona dins d'una banda estreta (Especificació de l'equip Aaron). Si un barril no es pot refredar amb la mateixa precisió que s'escalfa, perds la capacitat d'executar resines sensibles a la calor de manera neta.
Formes de matèries primeres que podeu executar
El material que alimenteu dóna forma a la màquina que compreu. A la pràctica veig quatre formes de matèries primeres comunes:
- Pellets — el valor predeterminat per a la resina verge, fàcil de dosificar i fondre
- Grànuls - una mica més gruixut, comú a les línies de composició
- Pols — típic per a mescles secs de PVC i treballs a escala de laboratori
- Escama reciclada — material recuperat amb densitat aparent variable
Amade-Tech assenyala que les màquines d'extrusió de plàstic de laboratori processen la matèria primera en pols, pellet, o en forma de grànuls per produir productes polimèrics continus amb secció transversal uniforme (Amade-Tech, 2024). A continuació, un cargol d'alimentació muntat a la tremuja lliura aquesta matèria primera de manera uniforme al barril (ThoYu, 2024). Fins i tot l'alimentació no és un detall menor; El lliurament inconsistent de la tremuja apareix com a línies de sobretensió i deriva dimensional al perfil acabat.
Com la matriu dóna forma a la sortida
La matriu d'extrusió és l'eina final per la qual passa la fosa, i defineix la secció transversal del producte. Tubs, tubs, pel·lícules, taules, i les ampolles provenen totes del mateix barril amb diferents matrius (Amade-Tech, 2024). Perquè la matriu produeix un perfil de secció transversal contínua, una màquina pot servir diverses línies de productes si inverteix en eines de matriu personalitzades. Aquesta flexibilitat d'eines és una de les raons per les quals tracte l'inventari de matrius com a part de la decisió de compra total en lloc d'una idea posterior..
Components bàsics que inspecciono a cada màquina
Tant si estic revisant una extrusora industrial a la venda o una unitat usada, Passo per la mateixa llista de verificació de components:
- Barril - el cilindre escalfat, idealment multizona amb refrigeració de circuit tancat
- Cargol — el cor de fondre i transmetre; La configuració del cargol determina la qualitat de la sortida
- Motor — La potència del motor de l'extrusora estableix el vostre sostre de rendiment
- Caixa de canvis — la relació de reducció i el factor de servei defineixen el parell útil
- Controls — Control de temperatura de fusió i gestió de zones
- Morir — l'eina de conformació de perfils
Dues especificacions ancorgen aquesta avaluació. Primer, la relació L/D, la longitud del canó dividida pel diàmetre del cargol, em diu quant temps de residència té la fusió; una extrusora Davis Standard de 9 polzades usada (Model 80IN80HT) incorporat 2001 parelles a 32:1 Relació L/D amb un barril de 7 zones i a 900 Motor de corrent continu HP (Llista d'equips d'Aaron). Segon, la relació de reducció de la caixa de canvis i el factor de servei defineixen el lliurament del parell; les unitats industrials solen enumerar ràtios com ara 10.15:1 amb un factor de servei de 1.5 (Equips Aaron). Aquests números es tradueixen directament en la força que podeu empènyer materials viscosos com HDPE o compostos farcits sense aturar-vos..
Per què comprar màquines d'extrusió de plàstic a l'engròs?
La ruta a l'engròs és on es guanya l'estratègia d'adquisició. En la meva experiència, la diferència entre la compra al detall i la compra directa de fàbrica rarament és un petit percentatge; remodela l'economia de tota una línia de producció d'extrusió. A continuació, detallo les quatre raons per les quals recomano constantment comprar equips d'extrusió a granel a través dels canals a l'engròs.
Estalvi de costos en comandes a granel i directes de fàbrica
El preu directe de fàbrica elimina les capes de marcatge del distribuïdor que inflen el preu d'una màquina extrusora de plàstic. Fabricants amb seu a la Xina, per exemple, ofereixen preus a l'engròs directes de fàbrica en extrusores de plàstic (ThoYu, 2024), és per això que tanta intenció de cerca relacionada amb el preu apunta cap a proveïdors estrangers. Quan comparo una única unitat minorista amb una comanda a granel d'un proveïdor de maquinària a l'engròs, el cost per màquina sol baixar prou per canviar el càlcul d'amortització de tot el projecte. Dit això, els preus directes de fàbrica només tenen beneficis quan compteu amb el cost total de propietat, un buit que abordo més endavant en aquesta guia.
Accés a personalització OEM i ODM
Les relacions de venda a l'engròs obren la porta a la personalització OEM i ODM que els canals minoristes poques vegades ofereixen. En lloc d'acceptar una configuració d'estoc, Puc especificar la longitud del cargol, zones de barrils, paquets de control, i eines de matriu personalitzades adaptades al meu producte. Per a qualsevol persona que tingui un perfil de secció transversal contínua especialitzat, aquest és l'únic argument més fort per comprar directament a un fabricant de màquines d'extrusió en lloc d'un revenedor.
Millors condicions sobre eines i peces de recanvi
La conversa de matrius i peces de recanvi és on els termes a l'engròs es combinen tranquil·lament al vostre favor. Negociar eines i un paquet de peces de recanvi a l'ordre original gairebé sempre supera l'obtenció d'ells a poc a poc més tard. Tracto peces de vestir, cargols, bandes de calefacció, i revestiments de bóta, com a part del contracte inicial, i impulso per escrit els compromisos de suport postvenda. Un fort suport postvenda és el que manté una línia en funcionament; sense ell, una màquina barata es converteix en un coll d'ampolla car.
Escala la capacitat de producció de manera eficient
Finalment, La compra a l'engròs em permet escalar la capacitat de l'extrusora sense repetir el cicle complet d'adquisició cada vegada. L'estandardització a la plataforma d'un proveïdor significa peces de recanvi coherents, controls familiars, i formació d'operadors repetible en múltiples màquines. Quan la demanda creix, afegir una segona o tercera unitat idèntica és molt més fàcil que integrar equips no coincidents de diferents proveïdors.
Tipus d'extrusores de plàstic: Cargol simple vs cargol doble
Escollir entre una extrusora d'un sol cargol i una extrusora de dos cargols és la decisió tècnica més conseqüent en una compra a l'engròs.. L'emmarc senzillament: Les màquines d'un sol cargol transmeten i fonen de manera eficient, mentre que les màquines de doble cargol es barregen i es combinen. Fes aquesta coincidència correcta i la resta de l'especificació s'ajustarà al seu lloc.
Extrusores d'un sol cargol
L'extrusora d'un sol cargol és el cavall de batalla per als perfils estàndard a un cost més baix. Sobresurt en fondre resina verge i empènyer-la a través d'una matriu amb una sortida constant, que el fa ideal per a canonades, tubs, i perfils continus senzills. També és la categoria d'equips utilitzats més comú, amb llistes de revenda específiques de marca àmpliament disponibles (Equips Aaron). Si la vostra línia de productes utilitza materials consistents com HDPE o polipropilè a través d'una matriu fixa, una màquina d'un sol cargol sol oferir el millor valor per unitat de sortida.
Extrusores de doble cargol
L'extrusora de doble cargol guanya el seu cost més elevat gràcies a la capacitat de barreja. Dos cargols entrellaçats generen la mescla distributiva i dispersiva necessària per a la barreja, afegint farcits, colorants, i estabilitzadors, i per processar materials reciclats amb propietats variables. Quan treballo amb escates de plàstic reciclat o polímers d'enginyeria sensibles a la calor com el PEEK, el control superior del doble cargol sobre el cisallament i el temps de residència és decisiu. Val la pena assenyalar que les extrusores de reciclatge són una classe de màquina diferent construïda específicament per a la matèria primera recuperada. (ThoYu, 2024), i moltes d'aquestes línies es basen en dissenys de dos cargols exactament per aquest motiu.
Velocitat de sortida i compatibilitat de materials
Els dos tipus divergeixen fortament en el comportament de la sortida i l'ajust del material. La sortida d'un sol cargol és en gran mesura una funció de la velocitat del cargol i la potència del motor, fent-ho previsible per a una sola resina. La sortida de doble cargol és més flexible en totes les formulacions, però sovint s'optimitza per combinar la qualitat en lloc de la producció en brut. Materials com les mescles seques de PVC i escates reciclades es beneficien de la manipulació de dos cargols, mentre que una sola resina neta funciona econòmicament amb un sol cargol.
Cargol simple vs cargol doble: Taula de comparació
|
Factor |
Extrusora d'un sol cargol |
Extrusora de doble cargol |
|---|---|---|
|
Força primària |
Fusió i transport de perfils estàndard |
Mescla, compostatge, i desvolatilització |
|
Cost relatiu |
Abaix |
Més alt |
|
Els millors materials |
HDPE, polipropilè, resines verges simples |
Mescles secs de PVC, escates reciclades, compostos farcits o PEEK |
|
Qualitat de mescla |
Limitat |
Excel·lent (distributius i dispersius) |
|
Productes típics |
Tubs, tubs, perfils senzills |
Compostos, masterbatch, pellet reciclat |
|
Disponibilitat de mercat d'ocasió |
Ampli, llistes específiques de marca habituals |
Més estret, més especialitzats |
|
Comprador ideal |
Línia de productes fixa, centrat en els costos |
Reciclatge, formulacions personalitzades, R&D |
|
Factor |
Extrusora d'un sol cargol |
Extrusora de doble cargol |
|---|---|---|
|
Força primària |
Fusió i transport de perfils estàndard |
Mescla, compostatge, i desvolatilització |
|
Cost relatiu |
Abaix |
Més alt |
|
Els millors materials |
HDPE, polipropilè, resines verges simples |
Mescles secs de PVC, escates reciclades, compostos farcits o PEEK |
|
Qualitat de mescla |
Limitat |
Excel·lent (distributius i dispersius) |
|
Productes típics |
Tubs, tubs, perfils senzills |
Compostos, masterbatch, pellet reciclat |
|
Disponibilitat de mercat d'ocasió |
Ampli, llistes específiques de marca habituals |
Més estret, més especialitzats |
|
Comprador ideal |
Línia de productes fixa, centrat en els costos |
Reciclatge, formulacions personalitzades, R&D |
Coincidència del tipus amb la vostra línia de productes
La meva regla de decisió és senzilla. Si estic extruint un material consistent en un perfil estable, Trio una màquina d'un sol cargol i poso l'estalvi en eines de matriu personalitzades i peces de recanvi. Si el meu procés implica la composició, canvis de color, o una extrusora de reciclatge de plàstic que maneja matèries primeres recuperades, Especifico una plataforma de doble cargol i accepto el preu més alt com a cost del control del procés. Per a compradors que pesin una extrusora a escala de laboratori per al desenvolupament de productes, la mateixa lògica s'aplica a una sortida més petita: coincideix amb el tipus de cargol amb si estàs demostrant una formulació (bessó) o un perfil (solter). Ancoratge de la decisió del cargol a la vostra línia de productes real, en lloc de només al preu del titular, és el que fa que una compra a l'engròs pagui durant tota la seva vida útil. Podeu revisar les configuracions del món real a les llistes de proveïdors i revendes, com ara Inventari d'un sol cargol utilitzat d'Aaron Equipment i Pàgines d'extrusora a l'engròs de ThoYu per veure com apareixen aquestes especificacions a la pràctica.
Quant costa una màquina d'extrusió de plàstic?
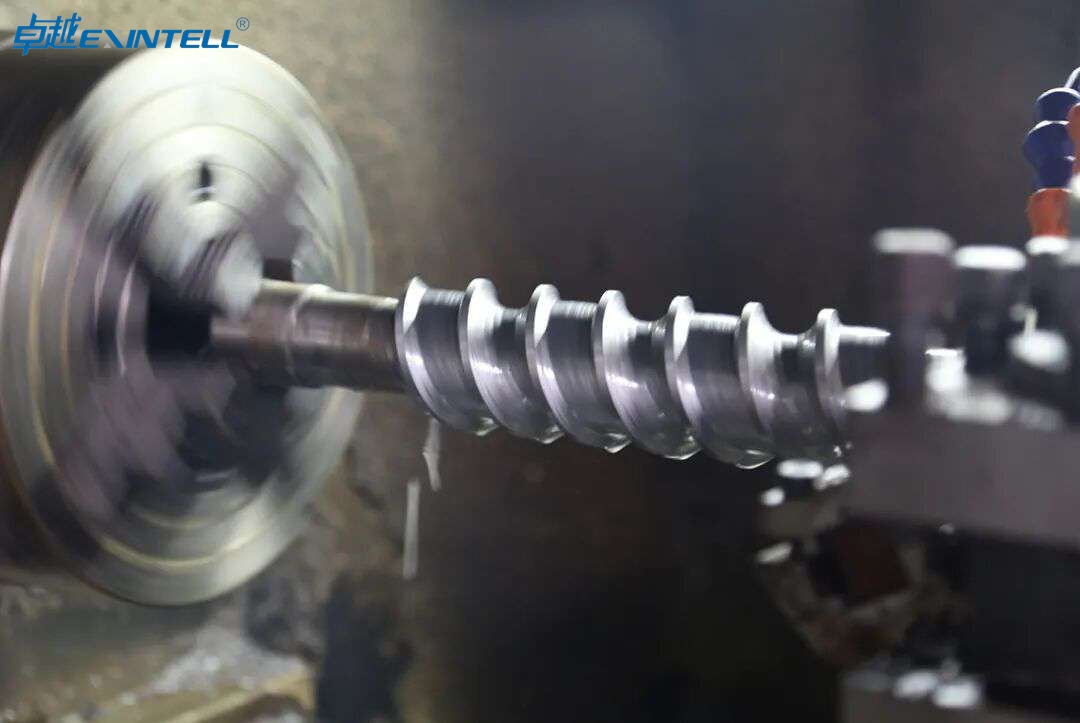
Quan els clients em demanen un sol número, Els dic la resposta honesta: una màquina d'extrusió de plàstic costa des d'uns quants milers de dòlars fins a més d'un milió, i la propagació és totalment a escala. Segons la meva experiència, obtenint equips en tres nivells, les bandes de preus es trenquen clarament al llarg de la capacitat de producció, configuració del cargol, i el nivell d'automatització que necessiteu. Abans de demanar pressupost, ajuda a saber a quin nivell pertanys realment, perquè una extrusora a escala de laboratori i una línia de producció d'extrusió industrial no són la mateixa compra amb un preu diferent. Són màquines diferents. Embalatge lleuger de plàstic reciclable
Intervals de preus per escala: Laboratori, Petit, i Industrial
Agrupo els compradors en tres categories pràctiques. Les extrusores a escala de laboratori són compactes, unitats de sobretaula o de terra construïdes per a R&D, assaigs combinats, i caracterització del material. Processen la matèria primera en pols, pellet, o en forma de grànuls per produir productes polimèrics continus amb una secció transversal uniforme (Amade-Tech). Les petites unitats comercials gestionen la producció de baix volum, execucions de prototipatge, i treball de perfil de nínxol. Les màquines industrials condueixen línies de producció d'extrusió completa per a canonades, pel·lícula, tauler, i sortida d'ampolles durant tot el dia.
A continuació, es mostra com els números aterren normalment en funció de les cotitzacions que he recopilat i de les llistes públiques. Tracteu-los com a intervals de planificació, preus no fixos, ja que la configuració del cargol i les eines els canvien significativament.
| Nivell | Sortida típica | Tipus de cargol | Nou rang de preus (USD) | Interval de preus usats (USD) |
|---|---|---|---|---|
| Extrusora a escala de laboratori | Fins a ~5 kg/h | Cargol simple o doble | $8,000 – $45,000 | $4,000 – $25,000 |
| Petit comercial | ~20 – 150 kg/h | Extrusora d'un sol cargol | $30,000 – $120,000 | $12,000 – $60,000 |
| Línia industrial | 300 kg/h i més | Extrusora de cargol simple o doble | $150,000 – $1,000,000+ | $50,000 – $400,000 |
L'extrem superior de la banda industrial reflecteix línies completes amb equips aigües avall com ara transports, tancs de refrigeració, i bobinadores, a més de control avançat de temperatura de fusió. Un capçal d'extrusora nu costa molt menys que una línia clau en mà, així que sempre confirmeu què inclou realment la cotització abans de comparar els proveïdors.
Què hi ha darrere del preu de l'adhesiu
Quatre variables mouen el nombre més que qualsevol altra cosa. La capacitat és la més evident: bàscules de rendiment amb diàmetre de canó i potència del motor, i tots dos afegeixen cost. La marca importa, perquè una màquina d'un fabricant de màquines d'extrusió establerta comporta una prima lligada a la fiabilitat i la disponibilitat de peces. La condició divideix tot el mercat en nous i usats, que cobreixo amb detall a continuació. I les eines són el silenciós que destrueix el pressupost. Una matriu personalitzada per a un perfil de secció transversal contínua específic pot afegir desenes de milers de dòlars, i sovint es cita per separat de la pròpia màquina.
Costos ocults més enllà del pressupost
El preu de compra poques vegades és el cost total de propietat, and this is where I see first-time buyers get burned. Beyond the machine, budget for these line items:
- Custom die tooling for each product profile you plan to run.
- Installation and rigging for heavy industrial units, which often require crane service and reinforced flooring.
- Electrical and utility upgrades to supply high-horsepower motors and closed-loop barrel cooling systems.
- Freight and, for imports, deures which I break down in the logistics section of this guide.
- Spare wear parts such as replacement screws, barrils, and heater bands.
- Commissioning and operator training, especially for automated control systems.
La meva regla general: afegir 15 a 30 per cent al preu de la màquina per estimar la instal·lació total, cost llest per a la producció. Skipping this math is the single most common planning mistake I encounter.
Plastic Extrusion Machine Wholesale Price: What Drives It?
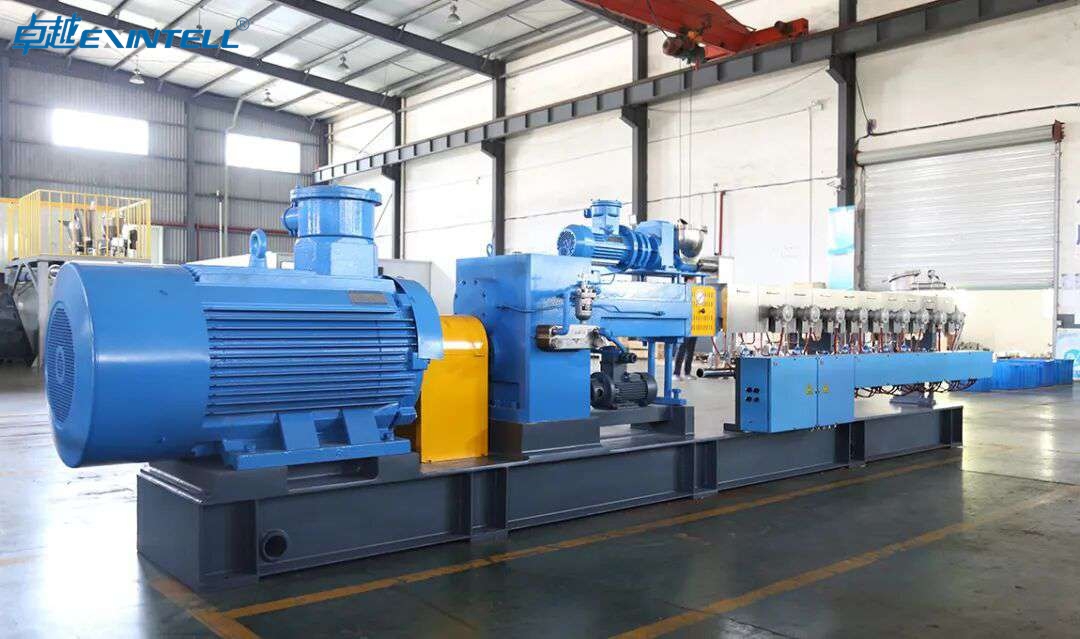
Wholesale pricing follows the same logic as retail, but with more room to negotiate and more variables to scrutinize. When I evaluate a factory-direct extruder price, whether from a domestic dealer or a China-based supplier offering wholesale rates (ThoYu), I work through a consistent checklist of specifications. Each one has a direct line to cost, and understanding them lets you compare quotes on equal terms instead of guessing.
Screw and Barrel Specifications
The screw and barrel are the heart of the machine, and they define both capability and price. The most important spec is the L/D ratio, the length-to-diameter ratio of the screw. A higher L/D ratio delivers better mixing and melt uniformity, which matters for demanding polymers. Per referència, una extrusora Davis Standard de 9 polzades usada (Model 80IN80HT) runs a 32:1 L/D ratio with a 7-zone barrel (Llista d'equips d'Aaron). More zones mean finer melt temperature control, since plastic is melted by electric heating tubes and converted to a uniform melt through screw shearing (ThoYu).
Screw configuration also decides the machine class. A single screw extruder is the workhorse for straightforward profiles and is the most common used-equipment category (Equips Aaron). A twin screw extruder costs more but excels at compounding, mixing additives, and processing recycled plastic flake. If you are running PVC, HDPE, or polypropylene at volume, screw geometry should match the resin; PEEK and other high-performance polymers push you toward specialized, higher-cost configurations. Fabricant d'extrusores de doble cargol
Motor and Gearbox Horsepower
Extruder motor horsepower is a direct proxy for throughput and, therefore, preu. That same Davis Standard unit pairs its barrel with a 900 Motor de corrent continu HP (Llista d'equips d'Aaron), which tells you it was built for heavy industrial output. The gearbox translates motor power into usable torque at the screw. Reduction ratios such as 10.15:1 combined with a service factor around 1.5 define how much torque the machine can safely deliver under load (Equips Aaron). When I compare two similarly priced machines, a higher service factor signals more durability headroom, which is worth paying for on equipment you plan to run hard.
Automation and Control Systems
Control systems separate a basic machine from a modern one. Manual temperature dials and simple relays keep the price down but demand skilled operators and produce more scrap. PLC-driven systems with closed-loop barrel cooling, emmagatzematge de receptes, and data logging cost more upfront but pay back through consistency and lower waste. A hopper feeder with a hopper-mounted feeding screw that delivers raw material evenly into the barrel (ThoYu) is standard, but gravimetric feeding and automated blending add cost and precision. For high-volume operations, I consider automation a value driver rather than a luxury.
Certificacions i origen
L'origen i la certificació configuren tant el preu com el risc. Domestic and European machines command higher prices, partly for build quality and partly for support proximity. Preus directes de fàbrica dels fabricants amb seu a la Xina (ThoYu) pot reduir substancialment el cost de la màquina, but you should verify CE marking, UL compliance for the US market, and documented electrical safety before committing. I always ask for certification documents in writing, perquè la readaptació d'una màquina no certificada per complir amb el codi elèctric dels EUA elimina els estalvis que van fer que la importació fos atractiva en primer lloc.
Màquines d'extrusió de plàstic noves i usades
Aquesta és la decisió que més em pregunten, i la meva resposta sempre és la mateixa: depèn de la vostra tolerància al risc i de la vostra cronologia. L'equip d'extrusió usat pot reduir els costos de capital a la meitat o més, però els estalvis vénen amb una exposició real. Les màquines noves costen més i sovint porten terminis de lliurament més llargs, però arriben amb garanties, controls actuals, i un rendiment previsible. Permeteu-me exposar els dos costats com ho faria per a un client.
Estalvi de capital vs risc en unitats usades
El cas financer per a equips usats és fort. Com mostra la taula de preus anterior, pot funcionar una unitat industrial usada 40 a 60 per cent per sota del nou, freeing capital for tooling and downstream equipment. For a startup or a shop testing a new product line, that difference can be the whole business case. The risk is that a polymer processing machine has wear components, screws and barrels degrade, heater bands fail, and motors lose efficiency, and those problems are not always visible in a listing photo. The savings are real, and so is the possibility of buying someone else’s problem.
Inspecting Condition, Hours, and Build Year
I never buy used equipment sight unseen, and I recommend you do not either. My inspection priorities, in order:
- Desgast del cargol i del canó: measure clearances if possible. Excessive clearance kills output and melt quality, and a replacement screw and barrel set is expensive.
- Build year and operating hours: a machine built in 2001, like the Davis Standard example, can still be excellent if maintained, but you need service records to judge.
- Sistemes de calefacció i refrigeració: confirm all barrel zones heat correctly and that closed-loop water cooling holds temperature.
- Motor and gearbox condition: listen for bearing noise and check for oil leaks and gearbox play.
- Control panel function: verify every zone reads and controls accurately, since older controls may lack replacement parts.
When feasible, insist on a powered demonstration running actual Plastic Pellet Manufacturers material. A cold machine hides most of its problems.
Warranty and Support Gaps on Used Equipment
The support gap is the cost that does not show on the invoice. New machines from an extrusion machine manufacturer typically include warranty coverage, commissioning help, and access to after-sales support. Used units are usually sold as-is, so you own every failure from day one. Before I buy used, I confirm two things: that spare parts remain available for that model, and that a service technician familiar with the brand can be reached. A cheap machine with no parts pipeline is a liability, not a bargain.
Resale Value Considerations
Finalment, think about the exit before you enter. Machines from recognized brands hold their value far better on the secondary market, which is exactly why brand-specific resale listings command steady demand (Equips Aaron). If there is any chance you will resize or exit within a few years, buying a well-known single screw extruder, even at a premium, protects your capital on the way out. En la meva experiència, resale strength is the most overlooked factor in the new versus used debate, and it often tips a borderline decision toward the established brand.
My bottom line: buy new when uptime is critical, support matters, and you plan to run the machine for a decade. Buy used when capital is tight, you have the technical capacity to inspect and maintain the equipment, and you stick to reputable brands with living parts supply. Sigui com sigui, do the total cost of ownership math first, because the quote is only the beginning of the spend.
Fonts: Equips Aaron, Used Single Screw Extruders; ThoYu, Wholesale Price China Plastic Extruder; Amade-Tech, Lab Plastic Extrusion Machine.
Where to Find Used Plastic Extrusion Machines Wholesale
When I source equipment on a tight capital budget, the used market is usually my first stop. A well-maintained secondhand extruder can deliver 80 a 90 percent of the service life of a new unit at a fraction of the cost, provided you know how to read a listing and verify condition before wiring any funds. The challenge is not finding machines. It is separating a genuine bargain from a decommissioned liability.
Marketplaces and Dealers Worth Knowing
Most of my used purchases have come through established dealer networks rather than open classified listings. Specialized resellers such as Aaron Equipment maintain rotating inventories of single screw and twin screw extruders, and they photograph, tag, and often power-test each unit before listing it. That vetting matters. A dealer with a physical yard and a reputation to protect gives me recourse that an anonymous marketplace posting never will. I still cross-check auction houses and industry-specific listing boards, but I treat a reputable dealer as the baseline for used extrusion equipment.
Reading a Listing Like an Engineer
A used listing is a spec sheet in disguise, and three numbers tell me most of what I need to know before I ever call. Consider a real example: una extrusora Davis Standard de 9 polzades usada (Model 80IN80HT) incorporat 2001, advertised with a 32:1 Relació L/D, a 7-zone barrel, i a 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron).
- Relació L/D. The barrel length-to-diameter ratio governs residence time and mixing. A 32:1 ratio suits demanding melt homogeneity work; shorter ratios around 24:1 handle simpler profiles. If your polymer needs thorough melting, do not buy short.
- Barrel zones. Seven independently controlled heating zones give me granular melt temperature control across the barrel length. More zones mean finer thermal tuning, which is critical for heat-sensitive resins.
- Motor horsepower. A 900 HP drive signals a high-throughput production machine, not a lab tool. Motor HP scales roughly with output capacity, so match it to your target line speed rather than buying more drive than your die can use.
Listings also disclose the gearbox reduction ratio and service factor, which together define usable torque. A 10.15:1 reduction with a 1.5 factor de servei, per exemple, tells me the drivetrain has headroom for sustained duty (font: Equips Aaron). I read those figures as a durability signal, not a footnote.
Brands That Hold Value on the Resale Market
Brand reputation follows a machine into its second life. Davis Standard, en la meva experiència, commands a premium on the resale market precisely because parts, cargols, and service documentation remain available years after manufacture. That liquidity cuts both ways: I pay more up front, but I recover more when I resell, and I spend less time hunting for a replacement extruder screw configuration or barrel liner. When I compare two similar used units, a supported brand almost always wins on total cost of ownership even at a higher sticker price.
Verifying Condition Before You Commit
I never buy a used extruder on photographs alone. My pre-purchase checklist runs through the wear points that quietly drain performance:
- Desgast del cargol i del canó. Request bore measurements. Worn clearances degrade output and pressure stability, and reconditioning a barrel is expensive.
- Heater and thermocouple health. Confirm every zone reaches and holds setpoint. Dead zones on a multi-zone barrel are a red flag.
- Drive and gearbox. Listen for bearing noise and check for oil leaks. A failing gearbox can cost as much as the machine.
- Sistema de refrigeració. Many industrial units use electric heating with closed-loop water cooling (font: Especificacions de l'equip Aaron). Verify the cooling circuit is intact and free of scale.
- Run test. Whenever possible, I insist on a powered demonstration under load, not just a cold spin.
If a seller resists an inspection or a run test, I walk. The savings on a used polymer processing machine evaporate the moment you have to rebuild a drivetrain.
Small and Lab-Scale Plastic Extrusion Machines
Not every buyer needs a 900 HP monster. A large share of the search interest around this keyword points toward small and near-me machines, and that tracks with what I see in practice: R&equips D, universitats, and startups need compact extruders that fit a lab bench and run on standard power. These machines trade throughput for flexibility, and for the right use case that is exactly the trade you want.
What Lab-Scale Machines Actually Do
A lab-scale extruder processes feedstock in powder, pellet, o en forma de grànuls per produir productes polimèrics continus amb una secció transversal uniforme (font: Amade-Tech). The core physics is identical to production equipment: a hopper feeder delivers raw material evenly into the barrel, electric heating tubes melt the polymer, and the screw shears and homogenizes it into a uniform melt before the extrusion die shapes the output (font: ThoYu). The difference is scale, not principle, which is what makes lab machines so useful for process development. What you learn at bench scale transfers to production.
Typical Products and Use Cases
I reach for a lab-scale unit in three situations:
- R&D and formulation. Testing new resin blends, additius, or recycled plastic flake without committing a production line.
- Prototipatge. Producing sample films, tubs, and small profiles for customer approval or tooling validation.
- Low-volume production. Serving niche markets where demand does not justify a full extrusion production line.
These machines readily handle common thermoplastics like PVC, HDPE, i polipropilè, and higher-spec units extend to engineering polymers such as PEEK when the barrel and screw are rated for the elevated melt temperatures.
Footprint and Power Requirements
The practical appeal of a lab extruder is that it lives in an ordinary room. Many bench units draw single-phase or light three-phase power and occupy a footprint measured in a few square feet, versus the dedicated bay and heavy three-phase service a production extruder demands. Before buying, I confirm two things: the electrical service my facility can supply, and whether the cooling requirement is air or water. Getting the utilities wrong is the most common reason a small machine sits idle after delivery.
Knowing When to Upgrade to Production Scale
A lab machine has a ceiling, and recognizing it early saves money. I plan the jump to production scale when sustained order volume outpaces the machine’s extruder capacity output, when I am running multiple shifts just to keep up, or when per-unit cost on the small line exceeds what a production extruder would deliver. The signal is economic, not emotional: once the lab unit becomes the bottleneck rather than the tool, it is time to scale. I typically keep the lab machine anyway, redeployed for the R&D work it does best.
Lab-Scale vs Production Extruders at a Glance
| Atribut | Laboratori / Small-Scale Extruder | Production Extruder |
|---|---|---|
| Primary use | R&D, prototipatge, low-volume runs | Continuous commercial production |
| Typical motor | Fractional to ~20 HP | 50 a 900+ HP (p. ex., 900 HP Davis Standard) |
| Relació L/D | ~20:1 a 25:1 | 24:1 a 32:1 |
| Barrel zones | 2 a 4 | 5 a 7+ |
| Power service | Single-phase / light 3-phase | Heavy 3-phase |
| Petjada | Benchtop to compact floor unit | Dedicated production bay |
| Sortida | Grams to low kg/hr | Hundreds of kg/hr |
Figures for the production column reflect the specification range seen in listings such as the Davis Standard 80IN80HT (font: Equips Aaron); lab-scale ranges reflect typical bench-unit configurations.
Buying Plastic Extrusion Machines Wholesale in the USA
Search intent around this keyword leans heavily toward USA and near-me queries, and that reflects a real procurement decision every US buyer faces: buy domestic or import. Factory-direct pricing from overseas manufacturers is genuinely attractive, and I have bought imported equipment when the numbers justified it. But the sticker price is only one line in the ledger. Here is how I weigh the domestic option.
The Case for Domestic Dealers
Buying from a US-based dealer or manufacturer gives me three advantages that rarely show up on a spec sheet but always show up in operations:
- Faster lead times. A machine in a domestic yard ships in days, not the weeks of ocean transit and customs clearance an import requires. When a line is down, that speed is worth real money.
- Easier service and parts. Domestic support means same-timezone technicians, stocked spare parts, and no international freight on a replacement gearbox or barrel. After-sales support is the single most underrated factor in extruder ownership.
- Standards compliance. US machines are typically built or certified to UL and NEC electrical requirements. That compliance simplifies installation, satisfies insurers, and passes inspection without the retrofit an uncertified import may need.
Compliance Is Not Optional
I want to be direct about this because it trips up first-time importers. An extruder that is not UL-listed or NEC-compliant can fail a facility electrical inspection, void insurance coverage, and create OSHA exposure. Retrofitting an imported machine to meet US standards, rewiring controls, replacing heaters, adding certified safety interlocks, can consume much of the money you saved on purchase price. Before I import, I confirm exactly what certification the unit carries and what it will cost to close any gap.
Cost Tradeoffs: Domestic vs Imported
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (font: ThoYu), and for high-volume standardized equipment that pricing can be compelling. But the landed cost of an import includes freight, assegurança, drets d'importació, corretatge duaner, i el transport interior, none of which appear in the quoted machine price. Layer on longer lead times, potential language and timezone friction on support, and any compliance retrofit, and the gap narrows considerably. La meva regla general: I model total cost of ownership over the first three years, not the purchase price, before deciding. On that basis, domestic often wins for equipment I need serviced quickly, while imports can win for planned capacity additions where lead time is not urgent.
How I Vet a Wholesale Supplier
Whether domestic or overseas, I run every wholesale machinery supplier through the same gate before committing capital. I confirm the minimum order quantity and whether it fits my actual need, request references from buyers running the same machine class, verify certifications in writing rather than taking a catalog claim at face value, and structure payment with protection, staged milestone payments or an escrow arrangement rather than a full wire against a promise. For imports specifically, I clarify Incoterms so I know exactly where the seller’s responsibility ends and mine begins. A supplier who answers these questions clearly is one I can build a relationship with; one who deflects is one I pass on.
Finding Wholesale Suppliers Near You
When I start a sourcing project for bulk extrusion equipment, I map suppliers in concentric circles: local, regional, then global. Proximity carries real value that rarely shows up on a quote, and I have learned to weigh it deliberately before chasing the lowest number.
Local vs Regional Sourcing Benefits
A supplier within a few hours’ drive lets me tour the floor, watch a machine run my resin, and shake hands with the service manager who will pick up the phone at 2 a.m. during a line-down event. Regional suppliers widen the pool of available inventory and specialization while keeping domestic warranty terms and familiar payment protections intact. En la meva experiència, the closer the vendor, the shorter the mean-time-to-repair, and for a single screw extruder running continuous cross-section profile work, downtime is the expense that quietly dwarfs the purchase price.
Installation and Service Proximity
Rigging, leveling, wiring a 900 HP DC drive, and commissioning a 7-zone barrel with closed-loop cooling all go smoother when the technician is local. A used Davis Standard 9-inch extruder (Model 80IN80HT) amb a 32:1 L/D ratio and 900 HP motor, incorporat 2001, is a serious piece of iron to install and dial in (font: Llista d'equips d'Aaron). I want the people who know that machine within reach for melt temperature control tuning and screw configuration adjustments during the first production weeks.
Trade Shows and Industry Directories
Two channels consistently surface credible vendors for me. Trade shows such as NPE: The Plastics Show and Fakuma put dozens of extrusion machine manufacturers in one hall, where I can compare a twin screw extruder against a single screw side by side and collect real spec sheets. For structured search, I lean on Thomasnet and the used-equipment marketplaces like Aaron Equipment, which maintains brand-specific resale listings for single screw extruders (font: Equips Aaron). Directories are a starting shortlist, not a verdict, so I always follow up with a plant visit or video walkthrough.
China vs US Suppliers: Weighing the Tradeoffs
The decision I face most often is factory-direct pricing from overseas versus the service density of a domestic partner. Neither wins outright. The right call depends on your volume, your in-house maintenance capability, and how much lead-time risk your production schedule can absorb.
Balancing Local Price with Global Options
China-based manufacturers offer factory-direct wholesale pricing on plastic extruders, and that gap can be substantial on comparable specifications (font: ThoYu). US suppliers, and used domestic equipment, close part of that gap when you factor in freight, deures, and the cost of coordinating support across time zones. I treat the sticker price as one input into total cost of ownership, not the deciding figure.
Lead Time and Shipping Considerations
Domestic used equipment can ship in days; a new overseas extrusion production line typically runs on a build-plus-ocean-freight timeline measured in months. Ocean transit, manipulació del port, and inland drayage all add weeks and variability. If your project has a hard launch date, that schedule risk deserves a line in your model alongside the price advantage.
Suport, Parts, and Language Logistics
This is where I have seen buyers underestimate the friction. Time-zone offsets stretch troubleshooting cycles, spare gearbox and screw components may ship internationally, and technical documentation quality varies. Before committing overseas, I confirm English-language manuals, a named support contact, and a stocked or expedited parts channel for wear items like screws, barrils, and heater bands.
China vs US Sourcing at a Glance
| Factor | Ultramar (p. ex., Xina) factory-direct | US supplier / domestic used |
|---|---|---|
| Unit price | El més baix, factory-direct wholesale (font: ThoYu) | Higher new; competitive on used inventory (font: Equips Aaron) |
| Temps d'execució | Build plus ocean freight, typically months | Days to weeks for in-stock units |
| Landed cost | Add freight, deures, drenatge | Add domestic freight and rigging |
| Service proximity | Remote, depenent de la zona horària | On-site or regional |
| Parts availability | Enviament internacional, plan ahead | Domestic stock, gir més ràpid |
| Documentació & language | Verify English manuals and support | Native-language support |
La meva regla general: high volume with a capable maintenance team favors overseas factory-direct; tight timelines or lean staffing favor domestic. Note that SERP demand for this keyword splits evenly across manufacturer, ecommerce, and informational content at roughly 33.3% cadascun (font: SERP analysis, 2025), and buyer searches cluster around price, “prop meu,” “EUA,” i “utilitzat” intents (font: SERP/PAA data, 2025) — a fair reflection of how mixed real purchasing behavior is.
How to Choose a Plastic Extrusion Machine Manufacturer
Once I have a shortlist, I run every candidate through the same vetting sequence. The goal is to separate a genuine polymer processing machine partner from a broker who will disappear after the wire transfer clears.
Quality Assurance and Factory Verification
I verify the factory before I verify the price. For overseas vendors that means a live video walkthrough or a third-party inspection of the production floor, weld quality on the extruder barrel, and evidence they actually build rather than resell. I ask to see a machine running feedstock in powder, pellet, or granule form to confirm they handle continuous polymer output the way their marketing claims (font: Amade-Tech). Seeing the heating tubes and screw shearing melt real resin into a uniform stream tells me more than any brochure (font: ThoYu).
Track Record and Reference Customers
I request three reference customers running similar materials, whether that is PVC pipe, HDPE profile, polypropylene sheet, o un polímer d'enginyeria exigent com el PEEK. A manufacturer with a documented history in your specific application has already solved the problems you are about to encounter. If a vendor cannot produce references, I treat that as a signal, not an oversight.
Customization and Application Expertise
The best manufacturers speak fluently about screw configuration, L/D ratio selection, and custom die tooling for your exact profile. Extruders produce a wide range of continuous products, including pipes, tubs, pel·lícules, taules, i ampolles (font: Amade-Tech), and each demands different tooling and thermal setup. I probe how they size the gearbox reduction ratio and service factor to my torque needs, drawing on published industrial examples such as a 10.15:1 ratio at a 1.5 factor de servei (font: Equips Aaron). A vendor who can discuss whether a single screw or twin screw extruder fits my recycled plastic flake feedstock, and how the hopper feeder delivers material evenly, has earned a closer look.
After-Sales Support and Parts Availability
I put the support terms in writing before purchase: response-time commitments, commissioning assistance, formació d'operadors, and guaranteed availability of wear parts like screws, barrils, and heater elements. For a plastic recycling extruder or any line running abrasive reclaimed material, wear-part supply is not optional, it is the difference between a productive asset and expensive scrap. I confirm lead times on those parts specifically, since that is what governs real-world uptime.
Certifications and Quality Systems
Finalment, I check the paperwork that signals a disciplined operation. ISO 9001 indicates a functioning quality management system, and CE marking matters if the equipment enters or transits European jurisdictions. For a US install I confirm the electrical build can meet UL and NFPA 79 expectatives, since a 900 HP DC drive with multi-zone electric heating and closed-loop water cooling (font: Especificacions de l'equip Aaron) has to satisfy my local inspector and my insurer. Certifications do not guarantee quality on their own, but their absence usually correlates with corners cut elsewhere.
Vetting sources I return to include ThoYu for factory-direct wholesale context (ThoYu wholesale listing) and Aaron Equipment for used single screw extruder benchmarks (Aaron Equipment used extruders).
Decoding Key Specifications Before You Buy
Every wholesale quote I review lists a wall of specifications, and most buyers I coach fixate on price before they understand what those numbers actually deliver. En la meva experiència, four figures tell you more about a machine’s real capability than the headline output rate does: la relació L/D, the number of heating and cooling zones, the screw diameter, and the motor-to-gearbox pairing. Read those correctly and you can predict melt quality, energy draw, and output ceiling before the machine ever ships.
L/D Ratio and Its Impact on Melting and Mixing
The L/D ratio expresses the screw’s effective length divided by its diameter, and it governs how much residence time the polymer gets inside the barrel. A longer L/D gives the melt more distance to homogenize, which matters when you run temperature-sensitive or highly filled compounds. Per referència, una extrusora Davis Standard de 9 polzades usada (Model 80IN80HT) I analyzed lists a 32:1 Relació L/D (font: Llista d'equips d'Aaron), which sits at the higher end for single-screw machines and signals strong melting and mixing headroom.
As a rough guide, I treat 24:1 a 26:1 as adequate for straightforward commodity resins, 28:1 a 32:1 as the sweet spot for consistent mixing and venting, and anything longer as specialty territory for demanding compounds. A single screw extruder built for basic profile work rarely needs the same length as one processing recycled plastic flake with variable bulk density. If a supplier can’t tell you the L/D ratio, that’s a signal the listing is thin on engineering detail.
Number of Heating and Cooling Zones
Multi-zone barrels let you stage the temperature profile from feed throat to die, and more zones mean finer control over melt temperature. The Davis Standard unit referenced above uses a 7-zone barrel (font: Especificacions de l'equip Aaron), which gives an operator granular control across the length of the screw. Plastic in an extruder is melted by electric heating tubes and converted into a uniform melt through screw shearing (font: ThoYu), so the zone count directly shapes how evenly that transition happens.
Cooling is the other half of the equation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (font: Especificacions de l'equip Aaron), which pulls heat back out when shear or process feedback pushes a zone above setpoint. When I vet a machine, I confirm both the heating zone count and whether cooling is air or closed-loop water. Water cooling responds faster and holds tighter melt temperature control, which pays off on precision products.
Screw Diameter and Output Rate
Screw diameter is the single strongest predictor of throughput. Output scales roughly with the cube of the diameter, so a modest jump in screw size produces a large jump in kilograms per hour. That relationship is why a 9-inch machine like the Davis Standard example carries a 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron) — the mass of material moving through a large-diameter screw demands proportionally more drive power.
When comparing wholesale offers, always normalize output against diameter and resin type. A quoted output of, dir, 300 kg/hr means little without knowing whether it was measured on low-density film resin or a stiff PVC compound. I ask suppliers to state the resin, melt temperature, and screw speed used for their rated output, then compare like with like.
Motor HP and Gearbox Reduction Ratio
The motor and gearbox work as a matched pair. Motor horsepower sets the available power, while the gearbox reduction ratio converts high-speed, low-torque motor output into the low-speed, high-torque rotation the screw needs. Industrial extruders publish both the ratio and a service factor — for example, a 10.15:1 reduction with a 1.5 factor de servei (font: Equips Aaron) — and that service factor tells you how much margin the drivetrain carries above nominal load.
I treat the service factor as a durability indicator. A gearbox rated 1.5 is designed to absorb shock loads and continuous duty without premature wear, which is exactly what you want on a machine running multiple shifts. A hopper-mounted feeding screw delivers raw material evenly into the barrel (font: ThoYu), and that steady feed keeps torque demand predictable so the gearbox operates within its rated envelope.
Matching Machine Capacity to Your Production Volume
Specifications only matter once you tie them to your actual demand. The most expensive mistakes I see in wholesale procurement come from sizing decisions, not from picking a bad brand. Online Plastics Recycling Marketplace Buy too small and you’ll run the line flat out with no cushion for growth; buy too large and you’ll carry idle capital, higher energy bills, and startup scrap on every short run.
Estimating Throughput Needs
Start with your target finished-product volume, then work backward. I calculate required output in kilograms per hour by taking monthly demand, dividing by realistic operating hours, and adding an allowance for scrap and changeover. A useful sanity check: if you need 40,000 kg per month and run a single shift of about 160 productive hours, you need roughly 250 kg/hr of sustained output, and I’d size for 300 kg/hr to leave headroom.
Feedstock form affects this math too. Lab and production extruders process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section (font: Amade-Tech), and bulk density varies enough between those forms that the same screw can deliver noticeably different mass throughput. Confirm your rated output against the feedstock you’ll actually run.
Avoiding Under- and Over-Sizing
Undersizing forces the machine to run at maximum screw speed constantly, which raises melt temperature, accelerates wear, and leaves zero margin for demand spikes. Oversizing is subtler but real: an oversized extruder run at low speed can produce poor mixing and unstable output, and you pay for motor and heating capacity you never use. My rule is to target a machine that hits your peak demand at roughly 75 a 85 percent of its rated capacity, which keeps it in an efficient, controllable band.
Planning for Future Growth
Wholesale machinery is a multi-year commitment, so I plan sizing against a two-to-three-year demand forecast, not today’s orders. Dit això, buying far ahead of demand ties up capital you could deploy elsewhere. A middle path I often recommend: size the extruder for near-term growth, but confirm the extrusion production line’s downstream equipment and the supplier’s screw and die options can scale, so you upgrade tooling rather than replacing the whole line.
Batch vs Continuous Production
Extrusion is inherently a continuous process — extruders produce continuous profiles including pipes, tubs, pel·lícules, taules, i ampolles (font: Amade-Tech) — so the batch-versus-continuous question is really about how your business schedules work. If you run long stable jobs, a larger continuous line maximizes efficiency. Si feu molts treballs curts amb canvis freqüents de material i color, prioritzeu el canvi ràpid i la resposta tèrmica ràpida sobre la mida bruta, perquè les vostres pèrdues vindran de les transicions, no de la velocitat de la línia superior.
| Perfil de producció | Diàmetre típic del cargol | Sortida indicativa | L/D suggerit | El millor ajust |
|---|---|---|---|---|
| Laboratori / R&D i petites tirades | 20–45 mm | Fins a ~50 kg/h | 24:1–28:1 | Mostreig, lot petit, Proves PEEK |
| Petit comercial | 50-75 mm | ~80–250 kg/h | 26:1–30:1 | Perfils, tub petit, pel·lícula especialitzada |
| Producció de volum mitjà | 90–120 mm | ~300-600 kg/h | 28:1–32:1 | Tub de HDPE, fulla, perfil continu |
| Gran volum / industrial pesada | 150 mm i més | 600 kg/h i més | 30:1–32:1+ | Conduccions grans, palet, escates reciclades |
Tracto aquests rangs com un marc inicial per a les converses amb els proveïdors, normes no fixes. La producció real sempre depèn de la resina, control de la temperatura de fusió, i configuració de cargols, so I verify each figure against a supplier’s tested data for my specific material.
Extruders for Specific Products: Pipa, Pel·lícula, Full, Pallet
The extruder is only the melt engine. What defines your finished product is the extrusion die and the downstream line built around it. When I evaluate a wholesale package, I look at the die and tooling as closely as the machine itself, because that’s where product quality and application fit are actually determined.
Pipe and Tube Extrusion Lines
Pipe and tube lines pair the extruder with an annular die, a vacuum calibration and cooling tank, a haul-off, and a cutter or coiler. For PVC and HDPE pipe, dimensional stability and wall concentricity are everything, so tight melt temperature control and steady output matter more than peak speed. I confirm the die is matched to my target diameter range and that the calibration tooling is included or clearly quoted, since retooling for a new pipe size is a recurring cost buyers often overlook.
Film and Sheet Die Configurations
Film and sheet share extrusion fundamentals but diverge at the die. Blown film uses an annular die with an air ring and tower; cast film and sheet use a flat T-die or coat-hanger die feeding a chill-roll or three-roll stack. Polypropylene and polyethylene dominate here, and die width plus lip adjustment set your thickness tolerance. When comparing offers, I ask specifically which die configuration is included and whether the lip is manually or automatically adjustable, because that determines how tightly you can hold gauge across the web.
Pallet and Profile Applications
Pallet and heavy-profile production is where large machines and recycled feedstock meet. Chinese manufacturers offer factory-direct wholesale pricing on plastic extruders built for pallet production (font: ThoYu, ThoYu pallet extruder), and these lines frequently run reclaimed material. Recycling extruders are a distinct machine class designed for reclaimed plastic feedstock (font: ThoYu), so if you plan to process recycled plastic flake, I strongly advise sourcing a machine engineered for it rather than adapting a virgin-resin extruder — the feed section, ventilació, and wear surfaces are built differently.
Custom Die and Tooling Options
Custom die tooling is what turns a general-purpose extruder into a machine that makes your exact product. Whether you need a bespoke profile cross section, a specific pipe wall structure, or a particular sheet width, I confirm three things with the supplier upfront: lead time for custom tooling, whether tooling design is in-house or subcontracted, and the cost of future die changes. A capable extrusion machine manufacturer will quote tooling as a clear line item and stand behind dimensional performance, which also tells you something about the after-sales support you’ll receive once the line is running.
For buyers exploring the used market, single screw extruders are a well-established resale category with brand-specific listings (font: Equips Aaron). When I consider used equipment for a specific product, I always verify that compatible dies and calibration tooling exist for my application, since a bargain machine with no path to the right tooling isn’t a bargain at all.
Processing Recycled Plastics with Wholesale Extruders
When I evaluate a wholesale extruder for a recycling operation, I start from a different premise than I would for virgin resin processing. Reclaimed feedstock is inconsistent, contaminated, and thermally sensitive, so the machine has to compensate for material variability that a virgin-only line never sees. Recycling extruders are a distinct machine class built for reclaimed plastic feedstock (font: ThoYu, 2025), and treating them as interchangeable with standard profile extruders is one of the more expensive mistakes I have watched buyers make.
Recycling Extruders and Material Preparation
The extruder itself is only one stage in a longer chain. Before recycled plastic flake reaches the hopper feeder, it typically passes through washing, assecat, and size reduction. A hopper-mounted feeding screw delivers raw material evenly into the barrel (font: ThoYu, 2025), and even that step becomes harder when the input is irregular flake rather than uniform pellets. En la meva experiència, the quality of upstream preparation determines whether the extruder runs stably or surges. If you are quoting a wholesale line and the supplier only prices the extruder, ask specifically about the material prep equipment, because the melt quality you get downstream depends on it.
The core melting mechanism is unchanged: plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (font: ThoYu, 2025). What changes with reclaim is how much shear and residence time the material can tolerate before it degrades. HDPE and polypropylene reclaim are relatively forgiving; PVC regrind is far less so and punishes overheating quickly.
Why Twin Screw Extruders Excel with Reclaim
For consistent recycled output, I lean toward a twin screw extruder over a single screw extruder in most reclaim applications. The reason is mechanical. Twin screw configurations provide better mixing, more controllable shear, and stronger devolatilization, which matters when the feedstock carries moisture and volatiles picked up during its first life. A single screw extruder remains a common and cost-effective used-equipment category with brand-specific resale listings (font: Equips Aaron, 2025), and it can handle clean, well-prepared regrind. But when feedstock quality is uneven, the extruder screw configuration in a twin screw machine gives me the process latitude to keep melt temperature control tight across batches.
The tradeoff is cost. Twin screw machines carry higher purchase and tooling prices, and the gearbox is more complex. That is a real budget line, not a rounding error, so I weigh it against the value of the finished product. High-value recycled compounds justify the investment; commodity reclaim often does not.
Contamination and Filtration Considerations
Contamination is the defining challenge of recycled feedstock, and filtration is how you manage it. A melt filtration system, usually a screen changer with a fine mesh pack, removes particulate before the melt reaches the extrusion die. Without adequate filtration, contaminants cause surface defects, weak spots, and clogged dies. I always confirm two things with a wholesale supplier: the screen changer type (manual, hydraulic, o continu) and the finest mesh the system supports without excessive pressure buildup. For heavily contaminated post-consumer streams, a continuous screen changer avoids the production stoppages that manual changes force.
Multi-zone barrels commonly use electric heating with closed-loop water cooling (font: Especificacions de l'equip Aaron, 2025), and precise zone control becomes even more important with reclaim because you are trying to melt inconsistent material without scorching the fraction that heats fastest.
Circular Manufacturing Opportunities
The commercial case for recycling extruders keeps strengthening. Brand commitments to recycled content and tightening regulation on single-use plastics are pushing demand for in-house reprocessing. I see two viable models. The first is closed-loop: reprocessing your own production scrap back into the same line, which improves yield and reduces raw material spend. The second is a dedicated recycling line that converts purchased post-industrial or post-consumer feedstock into salable pellets or profiles. Both turn a waste stream into either cost savings or revenue, and the extruder is the pivot point of that conversion.
Certifications and Standards to Look For
Certification is where wholesale procurement, especialment de proveïdors estrangers, gets serious. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (font: ThoYu, 2025), and that pricing is genuinely attractive. But a low quote means nothing if the machine cannot be legally installed, insured, or operated in your jurisdiction. I treat certification as a gating requirement, not a nice-to-have.
CE Marking for European Compliance
If you operate in or export to the European Economic Area, El marcatge CE és obligatori. It signals that the machine conforms to relevant EU directives, most notably the Machinery Directive, covering mechanical safety, guarding, and emergency stops. For a US buyer this may seem irrelevant, but I raise it because many buyers plan to resell finished goods into Europe or operate multinational facilities. Confirm the CE marking is backed by an actual Declaration of Conformity and a technical file, not just a sticker on the frame. A legitimate manufacturer produces the paperwork on request.
ISO 9001 Gestió de la qualitat
ISO 9001 certifies that the manufacturer runs a documented quality management system. It does not certify any individual machine, and I want to be precise about that distinction because suppliers sometimes blur it. What ISO 9001 tells me is that the factory has repeatable processes for design, producció, and inspection, which correlates with more consistent build quality across units. For wholesale buyers ordering multiple machines or planning repeat purchases, that process consistency is exactly what protects you from unit-to-unit variation.
UL for US Electrical Safety
Per al mercat dels EUA, UL certification on electrical components is the one I refuse to compromise on. Extruders draw significant power through motors, bandes de calefacció, i armaris de control. A used Davis Standard 9-inch extruder, per exemple, runs a 900 HP DC motor across a 7-zone barrel (font: Llista d'equips d'Aaron, 2025), and that scale of electrical load makes safety certification a genuine risk-management issue, not a formality. UL or an equivalent NRTL listing affects your ability to pass local electrical inspection, secure insurance, and satisfy OSHA expectations. Imported machines frequently ship with control systems that are not UL-listed, so budget for potential panel rework or re-certification in the US.
Documentation and Compliance Verification
Certificates are only as good as your ability to verify them. My verification routine is straightforward:
- Request certificate numbers and check them against the issuing body’s public database rather than trusting a PDF.
- Confirm the certificate covers the specific model, not a different machine in the product family.
- Ask for the Declaration of Conformity, wiring diagrams, and the operation and maintenance manual before you release final payment.
- Where feasible, commission a third-party pre-shipment inspection to confirm the physical machine matches the documentation.
Tying compliance verification to your payment milestones is the single most effective piece of leverage you have as a wholesale buyer. Once the machine ships, that leverage is gone.
Understanding Total Cost of Ownership
The purchase price is the number everyone fixates on, and it is the one that matters least over the life of the machine. When I model total cost of ownership, I fold in energy, manteniment, temps d'inactivitat, i instal·lació, and the ranking of suppliers frequently reverses once those costs are included. This is the analysis that most wholesale buying guides skip, and it is where a slightly cheaper machine can quietly become the expensive one.
Energy Consumption and Operating Cost
Energy is the largest recurring cost for most extrusion operations, and it is driven by motor horsepower and heater load. A 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron, 2025) running multiple shifts represents a substantial electricity bill, and small efficiency differences compound over thousands of operating hours. Multi-zone barrels using electric heating with closed-loop water cooling (font: Especificacions de l'equip Aaron, 2025) are more efficient at holding temperature than older uninsulated designs. I ask suppliers for the connected load and, sempre que sigui possible, the specific energy consumption per kilogram of throughput, because that figure lets me compare machines on an operating-cost basis rather than a sticker basis.
Maintenance and Spare Parts
Wear is unavoidable. The screw and barrel are the primary wear components, and processing abrasive or filled materials accelerates it. Recycled plastic flake with residual contamination wears tooling faster than clean virgin resin. Gearbox maintenance also matters: industrial extruders define torque through gearbox reduction ratios such as 10.15:1 amb un factor de servei de 1.5 (font: Equips Aaron, 2025), and that gearbox needs scheduled lubrication and periodic inspection. My practical concern with wholesale and imported machines is spare parts lead time. A cheap machine whose screw takes three months to replace from overseas is not cheap when the line sits idle waiting.
Downtime and Reliability
Downtime is the cost that does not appear on any invoice, which is exactly why it gets underestimated. Every hour a line is down is lost production plus fixed overhead still accruing. Reliability is where established brands and ISO 9001 manufacturers tend to justify their premium. When I assess reliability, I look at build quality on the components that fail expensively, the availability of local service technicians, and the supplier’s after-sales support commitments. A responsive supplier that ships parts quickly is worth more than a marginally lower purchase price.
Installation and Commissioning Expenses
The final and most frequently forgotten category is getting the machine running. Installation and commissioning cover rigging and placement of heavy equipment, electrical and cooling-water hookups, control integration, and the trial runs needed to dial in melt temperature control and output. For imported machines I also budget for potential electrical re-certification and any adaptation to US voltage and plant infrastructure. Commissioning support from the manufacturer, whether on-site or remote, has real value here, and I confirm whether it is included in the quote or billed separately.
Total Cost of Ownership Comparison
The table below illustrates how the cost picture shifts across three common procurement paths. The figures are representative ranges for planning purposes, not fixed quotes, and actual costs vary with capacity, especificació, and supplier.
| Factor de cost | New Domestic (EUA) | Imported Factory-Direct | Used / Refurbished |
|---|---|---|---|
| Purchase price | El més alt | El més baix | De baix a moderat |
| Certification readiness | UL/CE typically included | Often needs verification or rework | Varia; verify by age and origin |
| Eficiència energètica | Current-generation controls | Varies by build quality | Older units may run less efficiently |
| Spare parts lead time | Curt | Llarg (overseas shipping) | Depends on brand support |
| Instal·lació / posada en marxa | Vendor support common | May require added budget | Often buyer-managed |
| Downtime risk | El més baix | Moderat a alt | Moderat; condition-dependent |
My takeaway from running this comparison repeatedly is that the imported factory-direct route wins on purchase price but requires you to budget deliberately for certification, spare parts logistics, i posada en marxa. The used route can be excellent value when the machine comes from a reputable brand with parts still available, which is why brand-specific resale listings (font: Equips Aaron, 2025) are worth studying carefully. New domestic equipment costs the most up front and often justifies it through lower downtime and simpler compliance. Decide by modeling your own numbers across the full ownership horizon, not by the quote alone.
Enviament, Import Duties, i Logística
When I buy a plastic extrusion machine wholesale from an overseas source, the quoted machine price is only the beginning of the conversation. The moment I move from a domestic used unit to factory-direct extruder pricing out of China, logistics becomes a project in its own right. A single screw extruder with a long barrel, a heavy gearbox, and a full extrusion production line footprint does not travel like a pallet of parts. I plan the freight and customs path before I sign, because a surprise here erases the savings that made the import attractive in the first place.
Càrrega, Crating, and Incoterms
The first term I nail down is the Incoterm, because it defines exactly where the seller’s responsibility ends and mine begins. In my experience three matter most for extrusion equipment:
- EXW (Ex Works) — I take ownership at the factory gate and pay for everything after, including inland transport in the origin country. Cheapest on paper, most work for me.
- FOB (Free On Board) — the supplier delivers to the origin port and loads the vessel. This is my default for a first deal with a new wholesale machinery supplier because it splits responsibility at a clean point.
- CIF (Cost, Assegurança, Càrrega) — the seller arranges ocean freight and insurance to my destination port. Convenient, but I always ask for the itemized breakdown so I can compare it against an independent forwarder quote.
Crating is not a line item I skip. An industrial extruder for sale overseas ships as a heavy, oddly balanced load, and the extruder barrel, matriu d'extrusió, and hopper feeder each need to be secured against vibration and moisture during a five- to eight-week ocean transit. I insist on a fumigated hardwood or steel-reinforced crate, desiccant packs inside sealed control cabinets, and a packing list that itemizes every component. For anything over roughly two meters wide or 10 tones, I confirm whether the load qualifies as out-of-gauge, because that changes the container type and the price.
US Import Duties and Customs
US import duty on plastics processing machinery generally falls under Harmonized Tariff Schedule heading 8477, que cobreix maquinària per treballar cautxú o plàstics. Base most-favored-nation duty rates in this heading are frequently low or zero, but I never assume the rate — I confirm the exact HTS subheading for my specific machine with a licensed customs broker before purchase (font: Comissió de Comerç Internacional dels EUA, Tarifa Harmonitzada, 2025, hts.usitc.gov). Beyond the base duty, I check for any additional Section 301 tariffs that apply to goods of Chinese origin, since those have been adjusted repeatedly and can add a meaningful percentage to landed cost.
On top of duty I budget for the standard federal fees: the Merchandise Processing Fee and, for ocean shipments, the Harbor Maintenance Fee. I also file the ISF (Arxiu de seguretat de l'importador, el “10+2”) at least 24 hours before the goods load overseas, because a late filing draws a penalty that has nothing to do with the machine’s value. A customs broker handles these filings for me, and their fee is small relative to the risk of getting them wrong.
Lead Time Planning
I build my schedule backward from the date I need the polymer processing machine running. A realistic timeline for a made-to-order extrusion production line from Asia looks like this:
- Manufacturing and assembly: 6 a 12 weeks depending on custom die tooling and screw configuration
- Factory acceptance and third-party inspection: 1 a 2 setmanes
- Ocean transit to a US West Coast port: 3 a 5 setmanes (longer to East Coast)
- Customs clearance and drayage: 1 a 2 setmanes
- Inland freight, aparell, i instal·lació: 1 a 3 setmanes
That puts a typical door-to-commissioning window at three to six months. I treat any supplier who promises dramatically less with healthy skepticism.
Rigging and Site Delivery
The final hundred meters are the ones people underestimate. A loaded extruder does not roll off a truck on its own. I arrange a rigging crew with the right forklift or crane capacity, verify that my facility’s dock, doorways, and floor loading can accept the machine’s footprint and weight, and confirm the power drop matches the extruder motor horsepower — a 900 HP DC motor draws very differently than a modest lab-scale extruder. On one project I nearly missed that the closed-loop barrel cooling system needed a dedicated water supply already plumbed before the rigging crew arrived. Now that check is on my pre-delivery list every time.
Payment Terms and Buyer Protections
Sending a large deposit to a factory I have never visited on another continent is the moment where a wholesale extruder deal feels riskiest. I manage that risk with payment structure, not just trust. The goal is simple: I want money to move only as the supplier hits verifiable milestones, and I want a neutral mechanism holding the leverage until I confirm the machine is what I paid for.
Letters of Credit and Escrow
For larger orders I favor a documentary carta de crèdit (LC). My bank commits to pay the supplier only when the supplier presents the exact documents my LC specifies — bill of lading, llista d'embalatge, inspection certificate, and so on. The paperwork discipline of an LC protects both sides, and it signals to a serious extrusion machine manufacturer that I am a professional counterparty. The tradeoff is bank fees and rigidity: any document discrepancy can hold up release, so I draft the required-documents list carefully.
For mid-sized deals, a third-party escrow service or a marketplace with built-in trade assurance offers similar protection with less overhead. The escrow agent holds my funds and releases them on agreed conditions. I read the release triggers closely, because an escrow that releases on shipment rather than on acceptance does far less for me.
Deposit and Milestone Structures
The structure I return to most often for a factory-direct order is a 30/40/30 split, and I have found it balances the supplier’s cash-flow needs against my protection:
- 30% dipòsit to begin production
- 40% on completion, paid after a successful factory acceptance test and third-party inspection, before the machine ships
- 30% balance after delivery, instal·lació, and successful commissioning at my site
I resist any pressure toward a 50% or larger upfront deposit from a supplier I do not have history with. The single most important lever I hold is that final payment tranche tied to on-site performance. If it is fully paid before the machine runs at my facility, I have given away my only real remedy.
Contract and Inspection Clauses
A wire transfer confirmation is not a contract. I insist on a purchase agreement that spells out, com a mínim:
- Detailed technical specifications: diàmetre del cargol, Relació L/D, extruder screw configuration, gearbox reduction ratio and service factor, zones de barrils, heating and cooling method, and rated capacity output
- Acceptance criteria tied to measurable output — for example, a specified throughput in kilograms per hour on a named resin such as HDPE or PVC, at a stated melt temperature control tolerance
- Right to third-party inspection before shipment, at my discretion
- Penalty and remedy clauses for late delivery or failed acceptance
- Governing law, dispute resolution venue, i termes de garantia
I tie the acceptance clause to a real production condition rather than a vague “machine works” statement. “Produces continuous cross-section profile at 300 kg/hr on virgin polypropylene within spec” is enforceable. “Functional” is not.
Reducing Overseas Transaction Risk
Beyond structure, a few habits reduce my exposure. I pay to the company’s registered corporate bank account, never to a personal account or a sudden last-minute change of banking details — that redirection is a common fraud pattern. I keep all commitments in writing. And I match my payment protection to deal size: an LC for a full extrusion production line, escrow or trade assurance for a single mid-range machine, and even for a modest used unit I still hold a meaningful balance until commissioning.
Vetting Suppliers and Verifying Quality
Payment protection limits my downside, but it does not put a working machine on my floor. That comes from vetting the supplier well and verifying the equipment before it ships. Since the SERP for this category splits evenly across manufacturers, ecommerce platforms, and other content (font: SERP analysis, 2025), buyers land in front of very different seller types, and the diligence I apply has to flex accordingly. A factory-direct manufacturer, a marketplace reseller, and a used-equipment dealer each deserve a different set of questions.
Factory Audits and References
Before I commit to a new extrusion machine manufacturer, I verify they actually build what they sell. I ask for their business license and registration, confirm how long they have operated, and request references from prior US or export customers — then I actually call those references. When the order justifies it, I commission an on-site factory audit, either through a sourcing agent or an inspection firm. The auditor confirms the factory exists, has real production capacity, and is not simply a trading company drop-shipping another workshop’s output. Trading companies are not automatically a problem, but I want to know which one I am dealing with, because it changes who is accountable for after-sales support.
Third-Party Inspection Services
I treat pre-shipment inspection as non-negotiable on any significant purchase. An independent inspector — from a global firm like SGS, TÜV, Bureau Veritas, or a specialist machinery inspector — visits the factory before the balance-triggering milestone. They verify that the build matches the contracted specifications: the correct extruder barrel construction, screw and die tooling, gearbox rating, motor horsepower, i sistema de control. A pre-shipment inspection report is one of the documents I list in my letter of credit, which links the money release directly to verified quality. The inspection fee is trivial next to the cost of receiving a machine that does not meet spec after it has cleared customs.
Sample Runs and Acceptance Testing
Specifications on paper are a promise; a sample run is proof. I ask the supplier to run the machine on my actual feedstock — whether that is virgin resin, recycled plastic flake, or a specific grade of PEEK or polypropylene — and produce the profile I intend to make. I want to see documented throughput, dimensional tolerance on the continuous cross-section, surface quality, and stable melt temperature control across the barrel zones. For a recycling extruder in particular, testing on real reclaimed material rather than clean pellets tells me whether the screw configuration and feeding system will actually handle my input. Where possible, I have this run witnessed by my third-party inspector or captured on video with live instrument readings.
Warranty and Service Commitments
The last thing I verify is what happens after the machine is running. I get the warranty in writing — typical coverage runs 12 mesos, sometimes longer on the mechanical structure — and I read what it excludes. Then I look past the warranty to practical serviceability: whether spare parts for the gearbox, escalfadors, and screw are stocked or reasonably available, what the lead time is for a critical replacement, whether the supplier provides commissioning support and operator training, and whether remote technical support is available in a time zone and language I can work with. A cheaper machine from a supplier with no realistic service path is not the bargain it looks like.
Supplier Vetting Comparison
To make the tradeoffs concrete, here is how I weigh the three seller types I most often evaluate when buying extrusion equipment. This maps to the new-versus-used-versus-imported procurement decision that runs through the whole purchase.
| Vetting factor | Factory-direct manufacturer (ultramar) | Online marketplace / reseller | Domestic used-equipment dealer |
|---|---|---|---|
| Typical price position | Lowest per-spec; factory-direct extruder pricing | Mitjana; platform markup added | Variable; strong value on legacy brands |
| Personalització (cargol, morir, Relació L/D) | High — built to order | De baix a moderat | None — as-is condition |
| Lead time to running | 3–6 months incl. logística | Varies with stock and origin | Fastest — often weeks |
| Inspection method | Auditoria de fàbrica + pre-shipment inspection | Platform assurance + independent check | In-person condition assessment |
| Payment protection | Letter of credit / milestone escrow | Trade assurance / escrow | Standard domestic terms |
| Garantia & servei | New warranty; verify parts pipeline | Depends on seller | Limited or none; dealer-dependent |
| El millor ajust | Custom production line, cost-driven | Standard machines, moderate volume | Proven brands like a used single screw extruder, fast need |
Both ends of that table are legitimate paths. China-based manufacturers offer genuine factory-direct wholesale pricing on plastic extruders (font: ThoYu, ThoYu), while the domestic used market lists brand-specific machines such as a Davis-Standard 9-inch single screw extruder with a 32:1 Relació L/D, seven-zone barrel, i 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron, Equips Aaron). The right choice depends on how much customization, velocitat, and service I need, and the vetting discipline above is what turns any of these into a purchase I can stand behind.
Instal·lació, Posada en marxa, and Training
Buying the machine is only half the transaction. En la meva experiència, the gap between a signed purchase order and a line running at rated output is where most first-time buyers lose weeks and margin. I treat installation, posada en marxa, and training as a single project with its own timeline, not an afterthought bundled into shipping. What follows is the sequence I use to bring a new or used extruder from crate to steady-state production.
Site and Utility Requirements
Before the freight arrives, I confirm the site can actually support the equipment. Industrial extruders draw serious power and generate real heat, així que la planificació dels serveis públics és el primer. A used Davis Standard 9-inch extruder, per exemple, vaixells amb a 900 Motor de corrent continu HP i un barril de 7 zones (font: Llista d'equips d'Aaron, 2024), que em diu immediatament que una alimentació de botiga estàndard de 240 V no la tallarà. Mapejo quatre requisits abans del lliurament:
- Servei elèctric: Confirmeu la tensió, fase, i amperatge contra la càrrega del motor i de l'escalfador. La potència del motor de l'extrusora condueix el màxim d'aspiració, i els barrils multizona afegeixen càrregues de calefacció elèctrica a sobre.
- Refrigeració: Els barrils multizona solen combinar calefacció elèctrica amb refrigeració de circuit tancat a base d'aigua (font: Especificacions de l'equip Aaron, 2024). Verifico la capacitat del refrigerador, cabal, i la qualitat de l'aigua abans del primer dia.
- Pis i accés: Una línia de producció d'extrusió amb transport aigües avall, tancs de refrigeració, i els talladors necessiten un espai lineal i un nivell, llosa amb càrrega nominal. Mesuro la línia completa, no només la petjada de l'extrusora.
- Ventilació i seguretat: El control de la temperatura de fusió significa calor i, amb alguns polímers, fume management. Local exhaust and clearances matter for both compliance and operator comfort.
Setup and Calibration Steps
Once the machine is positioned and services are connected, I run commissioning as a checklist rather than a feel. The core polymer processing machine converts feedstock in powder, pellet, or granule form into a continuous cross-section profile (font: Amade-Tech, 2024), and every stage of that conversion needs to be dialed in:
- Mechanical alignment: Confirm the gearbox, cargol, and barrel are aligned and torqued. Gearbox reduction ratios and service factors define torque delivery (font: Equips Aaron, 2024), so I verify the drivetrain before applying load.
- Heater and thermocouple verification: Plastic is melted by electric heating tubes and homogenized through screw shearing (font: ThoYu, 2024). I check each zone independently and confirm every thermocouple reads accurately.
- Feed system check: Hopper-mounted feeding screws deliver raw material evenly into the barrel (font: ThoYu, 2024). I confirm consistent feed with the actual resin, si això és PVC, HDPE, polipropilè, or recycled plastic flake.
- Die and tooling fit-up: Install the extrusion die, confirm the screw configuration suits the resin, and set the melt temperature profile for a stable, uniform cross section.
- Dry run then wet run: Cycle the line empty, then purge and run production resin, adjusting zone temperatures and screw speed until dimensions hold to spec.
Operator Training Needs
A calibrated machine still fails without trained operators. I schedule training to overlap with commissioning so the team learns on the exact line they will run. My minimum curriculum covers startup and shutdown sequencing, purge procedures between resin changes, reading and adjusting melt temperature control, recognizing off-spec output, and routine maintenance of screw, barril, i morir. For used equipment where the manufacturer is not on site, I budget for a third-party commissioning engineer or negotiate remote support into the deal. After-sales support is a spec worth confirming before purchase, no després.
Ramp-Up to Full Production
I never assume rated output on day one. Published extruder capacity output is a ceiling under ideal conditions, and real ramp-up follows resin behavior, eines, and operator familiarity. I stage it: run at reduced throughput to validate quality, log every setting that produces good parts, then increase output incrementally while watching for dimensional drift and thermal stability. En els meus projectes, a well-commissioned single screw extruder reaches stable full production within one to three weeks; a twin screw extruder or a compounding line can take longer because there are more variables to tune.
Wholesale Buyer’s Checklist and Next Steps
When I run a procurement cycle for bulk extrusion equipment, I work through the same five stages every time. This is the unified framework I wish more buyers had when comparing new, utilitzat, and imported options, because each channel carries different risks and each stage removes a category of avoidable loss.
1. Define Application, Volum, and Budget
I start with the product, not the machine. What continuous cross-section profile am I making, in what polymer, at what daily volume? Pipa, pel·lícula, tauler, and profile lines have different die tooling, Relació L/D, and screw configuration requirements (font: Amade-Tech, 2024). A lab-scale extruder suits R&D and short runs; an industrial extruder for sale suits committed volume. I set a budget that accounts for total cost of ownership, no només el preu de l'adhesiu.
2. Shortlist Suppliers Across Channels
The market for this keyword splits evenly across manufacturer, ecommerce, and other content types, roughly a third each (font: SERP analysis, 2024). I mirror that in sourcing by building three shortlists: OEM manufacturers, used-equipment dealers, and factory-direct import suppliers. China-based manufacturers offer factory-direct wholesale pricing on plastic extruders (font: ThoYu, 2024), while dealers like Aaron Equipment list brand-specific used single screw extruders with full specs. Casting across all three channels is the only way to know what a fair price actually is.
3. Compare Specs and Total Cost
I compare specifications on a single sheet so nothing hides in a footnote. The table below shows how I frame the three channels for a mid-range single screw extruder.
| Factor | New (OEM) | Used (Dealer) | Imported (Factory-Direct) |
|---|---|---|---|
| Upfront price | El més alt | Lowest for equivalent size | Low to mid, before landed costs |
| Temps d'execució | Moderate to long (build to order) | El més curt (en estoc) | El més llarg (build plus ocean freight) |
| Garantia / suport | Full OEM warranty and support | Limited or as-is | Varia; confirm in writing |
| Spec certainty | Exact to order | Fixed by the listed unit | Configurable, verify against quote |
| Hidden costs | Instal·lació, eines | Reforma, unknown wear | Import duties, enviament, posada en marxa |
| El millor ajust | Long-term critical production | Fast start, tight capital | Volume buyers comfortable with logistics |
Total cost of ownership is where imported equipment surprises people. The quoted extruder machine price is not the landed cost. I add ocean freight, US import duties, transport interior, aparell, instal·lació, and commissioning before I compare across channels. A low factory-direct number can equal or exceed a domestic used price once everything lands.
4. Negotiate Terms and Finalize Protections
Once I have a preferred supplier, I negotiate the terms that protect the money, not just the price. My payment-protection playbook is consistent:
- Staged payments tied to milestones: dipòsit, pre-shipment inspection, and balance on acceptance rather than 100% upfront.
- Inspecció de tercers before shipment for imported or used units, confirming the machine matches the quoted specifications.
- Written performance criteria: rated output, tolerància dimensional, and acceptance test conditions defined in the contract.
- After-sales terms in writing: disponibilitat de peces de recanvi, warranty scope, and remote or on-site support.
- Clear minimum order quantity and Incoterms so responsibility for freight, assegurança, and duties is unambiguous.
Següents passos
My recommended path from here: write a one-page spec sheet for your application, request quotes from at least two suppliers in each channel, build the comparison table above with your real numbers, i la llista final a dos finalistes abans de negociar. Aquesta seqüència manté el palanquejament del vostre costat i converteix una gran compra de capital en una decisió controlada.
Preguntes freqüents
Quant costa una màquina d'extrusió de plàstic?
El preu depèn molt més de la mida, tipus de cargol, i condició que en qualsevol figura de llista única. En la meva experiència, una extrusora compacta a escala de laboratori o un sol cargol es troba a l'extrem inferior, mentre que una gran línia industrial amb una alta relació L/D, un barril d'extrusora multizona, i l'equip aigües avall costa moltes vegades més. Unitats usades, com ara les extrusores d'un sol cargol de marca venudes a través de distribuïdors, generalment, redueix el preu del nou OEM per a una mida equivalent (font: Equips Aaron, 2024). Compareu sempre el preu de la màquina extrusora de plàstic com a terra, total cost of ownership number rather than the headline quote.
Where can I find a plastic extrusion machine near me or in the USA?
For domestic sourcing, US-based used-equipment dealers are the fastest route because units are in stock and shipping is inland rather than international. For new machines, OEM manufacturers and their US distributors serve the market directly. If you are open to factory-direct wholesale pricing, China-based manufacturers ship internationally (font: ThoYu, 2024), but you take on import duties, mercaderies marítimes, and commissioning logistics. La meva regla és senzilla: buy near you when speed and support matter, and import when volume justifies the added logistics.
Should I buy a new or used extruder?
Used equipment makes sense when capital is tight, you need to start fast, and the specific unit matches your resin and output. A used single screw extruder with documented specs, such as a Davis Standard unit with a 32:1 L/D ratio and 7-zone barrel (font: Llista d'equips d'Aaron, 2024), can be an excellent value. New OEM equipment makes sense for long-term critical production where warranty, exact-to-spec configuration, and factory support outweigh the higher upfront cost. I steer buyers toward used for a first line or a proven process, and new for mission-critical or novel applications.
How do I choose a reliable manufacturer or wholesale supplier?
I vet suppliers on four things: verifiable references for the exact machine class I need, clear written specifications, defined after-sales support and spare-parts availability, and willingness to accept staged payments with pre-shipment inspection. A credible extrusion machine manufacturer will document gearbox reduction ratios, service factors, and torque delivery rather than quoting output alone (font: Equips Aaron, 2024). If a supplier resists third-party inspection or written performance criteria, I treat that as a red flag.
What is the difference between a single screw and a twin screw extruder?
A single screw extruder is the workhorse for straightforward profiles, canonada, and film in resins like PVC, HDPE, i polipropilè. A twin screw extruder provides stronger mixing and better control for compounding, high-fill formulations, and demanding materials such as PEEK. Twin screw lines cost more and take longer to tune, so I only recommend them when the application genuinely needs the mixing performance. Match the screw configuration to the polymer and product, not to a general preference.
Can I use an extruder for recycled plastic?
Sí, but often on a purpose-built machine. Recycling extruders are a distinct machine class designed for reclaimed feedstock (font: ThoYu, 2024). If your input is recycled plastic flake with variable moisture and contamination, a dedicated plastic recycling extruder with appropriate feeding and venting outperforms adapting a standard virgin-resin line. Confirm the machine is rated for your specific reclaimed material before purchase.
What ongoing costs should I budget beyond the purchase price?
Total cost of ownership includes electricity for the motor and heaters, closed-loop cooling water, wear parts for the screw and barrel, custom die tooling for new products, formació d'operadors, and periodic maintenance. For imported machines, add duties, mercaderies, i posada en marxa. Buyers who plan only for the machine price are consistently surprised by the operating and logistics costs, which is exactly why I model landed and running costs before signing anything.
What Is Plastic Extrusion Machine Wholesale and Why It Matters for B2B Buyers
When I talk with procurement teams about buying extrusion equipment in volume, the first thing I clarify is what “a l'engròs” actually means in this category. It is not a discount aisle. It is a procurement channel where you buy directly from manufacturers, distribuïdors autoritzats, or used-equipment dealers at factory-direct or bulk-negotiated pricing, usually bypassing the retail markup that comes with single-unit retail sales. En la meva experiència, understanding that distinction changes how you negotiate, how you vet, and how you budget.
Definició: What a Plastic Extrusion Machine Actually Does
A plastic extrusion machine converts raw polymer feedstock into a continuous product with a uniform cross section. Lab and production units process feedstock in powder, pellet, or granule form to produce continuous polymer products (font: Amade-Tech, 2024). The core process is straightforward once you see it: raw material drops from a hopper feeder into a heated barrel, where a rotating screw melts and shears the polymer into a homogeneous melt. As ThoYu describes it, the plastic is melted by electric heating tubes and transformed into a uniform melt through screw extrusion and shearing (font: ThoYu, 2024). That melt is then forced through an extrusion die that shapes the final profile.
The machine architecture matters when you compare quotes. A single screw extruder is the workhorse for many standard profiles and is the most common category on the used market, amb llistes de revenda específiques de marca àmpliament disponibles (font: Equips Aaron, 2024). A twin screw extruder delivers better mixing and is typical for compounding, polímers farcits, i el reciclatge. Two specifications define capacity more than any marketing claim:
- Relació L/D — the length-to-diameter ratio of the screw and barrel. A used Davis Standard 9-inch extruder (Model 80IN80HT), per exemple, features a 32:1 Relació L/D, a 7-zone barrel, i a 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron). Higher L/D generally means more melting and mixing capacity.
- Gearbox reduction ratio and service factor — these define how motor speed becomes usable torque. Industrial units commonly quote figures such as a 10.15:1 reduction ratio with a 1.5 factor de servei (font: Equips Aaron). If a supplier cannot give you these, treat that as a data gap.
Supporting systems round out the package: the hopper-mounted feeding screw delivers raw material evenly into the barrel (font: ThoYu), and multi-zone barrels commonly pair electric heating with closed-loop water cooling for melt temperature control (font: Especificacions de l'equip Aaron).
Context del mercat: Where Wholesale Buyers Actually Source Equipment
The sourcing landscape is more fragmented than most first-time buyers expect. When I mapped the search results for this category, they split almost evenly across manufacturer sites, ecommerce marketplaces, and other content, at roughly 33.3% cadascun (font: SERP analysis). That tells me buyers are pulling from three distinct channels at once, and each carries a different risk and cost profile.
China-based manufacturers openly advertise factory-direct wholesale pricing on plastic extruders (font: ThoYu), which is why imported equipment dominates a large share of price-sensitive inquiries. Al mateix temps, buyer search behavior clusters heavily around price, “prop meu,” “EUA,” “utilitzat,” and small-machine intents (font: SERP/PAA data). The practical takeaway: you are almost always choosing among three procurement paths, and I recommend evaluating all three before committing.
New vs. Used vs. Imported: A Procurement Framework
| Factor | New (domestic OEM) | Used (dealer/resale) | Imported (factory-direct) |
|---|---|---|---|
| Upfront cost | El més alt | El més baix per unitat | De baix a moderat |
| Temps d'execució | Weeks to months (build to order) | El més curt (en estoc) | El més llarg (producció + mercaderies marítimes) |
| Garantia / suport postvenda | Strongest | Limited or as-is | Varies widely; verify carefully |
| Spec transparency | Alt | Alt (documented history) | Requires diligence |
| Hidden costs | Instal·lació, eines | Refurb, peces de desgast | Import duties, enviament, logística |
| El millor ajust | Long-run production, critical tolerances | Budget projects, proven models | Cost-driven scale-up with in-house maintenance |
I built this framework because it is the piece most buyers are missing. Comparing a used single screw extruder listing against an imported quote on price alone ignores the total cost of ownership, and that gap is where budgets get blown.
Aplicacions clau: Matching the Machine to Your Output
Extruders produce continuous profiles including pipes, tubs, pel·lícules, taules, i ampolles (font: Amade-Tech). The polymer you run dictates screw configuration, barrel design, i control de temperatura. In my experience the most common wholesale buyers fall into a few groups:
- Rigid profile and pipe producers running PVC and HDPE, who need robust torque and stable melt temperature control.
- Packaging and film converters running polypropylene and HDPE for continuous cross-section profiles.
- Recyclers, where a plastic recycling extruder is a distinct machine class purpose-built for reclaimed feedstock and recycled plastic flake (font: ThoYu). Do not repurpose a virgin-resin single screw for heavy recycling duty.
- R&D and specialty labs running lab-scale extruders, sometimes with high-performance polymers like PEEK, where a small, precise machine beats a large production line.
Per què és important per als compradors B2B
Wholesale procurement of a polymer processing machine is a capital decision with a multi-year payback. Getting the L/D ratio, extruder motor horsepower, and extruder capacity output right the first time is the difference between a line that runs profitably and one that bottlenecks your throughput. That is exactly why the supplier you choose matters as much as the machine.
How to Choose the Right Plastic Extrusion Machine Wholesale Supplier
Once buyers accept that the supplier decision drives the outcome, the next question is how to actually evaluate one. I use a repeatable process built around evidence, not sales pitches. Below is the vendor evaluation approach I apply before I recommend committing capital.
Vendor Evaluation: What Separates a Real Supplier From a Broker
A credible extrusion machine manufacturer or wholesale machinery supplier should be able to answer technical questions without deflecting. I evaluate on four dimensions:
- Specification transparency. They should provide the L/D ratio, relació de reducció de la caixa de canvis, factor de servei, motor horsepower, recompte de zones de barrils, and cooling method in writing. Recall the benchmarks: a documented industrial unit lists a 32:1 L/D ratio and a 900 HP motor (font: Llista d'equips d'Aaron). If a quote omits these, the supplier either does not know the equipment or does not want you to.
- Technical fit to your polymer. A serious supplier asks what you are running (PVC, HDPE, polipropilè, PEEK, or recycled flake) before quoting. The right extruder screw configuration depends on the answer.
- Suport postvenda. Ask specifically about spare parts availability, screw and barrel replacement lead times, and remote or on-site commissioning.
- Verifiable track record. Documented resale history, reference customers, and real installation photos. Factory-direct sellers advertising wholesale pricing (font: ThoYu) still need to clear this bar.
Red Flags: When to Walk Away
These are the warning signs that have saved me from bad purchases:
- Refusal or inability to share core specifications (Relació L/D, gearbox ratio, motor HP).
- Pricing that is dramatically below market with no explanation, especially on imported units.
- Pressure for full upfront payment by wire with no milestone structure or escrow option.
- No written warranty terms and no clear after-sales support contact.
- Vague answers on import duties, enviament, and logistics for cross-border deals, leaving those costs entirely on you.
- Stock photos only, with no ability to arrange a video walkthrough or factory audit.
Llista de verificació de Due Diligence
I run every serious quote through this list before signing:
- Confirm full specifications in writing and match them to your production requirements.
- Verify business registration, export licensing (for imports), and years in operation.
- Request references from buyers running the same polymer and output range.
- For used equipment, obtain maintenance records and, sempre que sigui possible, arrange an inspection or test run. Single screw extruders are a well-documented resale category, so history should be available (font: Equips Aaron).
- Get a landed-cost breakdown: preu unitari, custom die tooling, embalatge, ocean or freight cost, drets d'importació, i instal·lació.
- Structure payment with protection: deposit plus milestone payments tied to inspection or shipment, ideally through a letter of credit or escrow rather than a single wire transfer.
- Confirm minimum order quantity terms if you are buying multiple units or a full extrusion production line.
- Get spare-parts and support commitments in the contract, not just verbally.
Consideracions clau: Cost total de propietat
The plastic extruder machine price on the quote is the smallest part of the story. Total cost of ownership is where I focus buyers, because it is the gap most competing guides ignore. For an imported unit, the sticker price can be misleading once you add:
- Logistics and duties — ocean freight, assegurança, corretatge duaner, and import duties on cross-border purchases.
- Eines — custom die tooling for your specific profile, which is rarely bundled.
- Energia — electric heating tubes and motor horsepower drive a meaningful ongoing utility cost.
- Wear parts and maintenance — screws, barrils, and gearbox service over the machine’s life.
- Downtime risk — a cheaper machine with no local support can cost more per year in lost production than a pricier one with strong after-sales coverage.
Practical Tips From Experience
A few habits that consistently pay off:
- Get at least three quotes across the new, utilitzat, and imported channels so you can compare on landed cost, no el preu de l'adhesiu.
- Insist on a test run with your actual feedstock before final payment whenever the deal allows it.
- Negotiate spare wear parts into the initial order while your leverage is highest.
- For imports, budget a realistic timeline; factory-direct pricing (font: ThoYu) comes with longer lead times and shipping risk you should plan around.
- Document every spec agreement in the purchase contract so there is no ambiguity at delivery.
Industry Context
Because search behavior in this category skews toward price, “prop meu,” utilitzat, and USA intents (font: SERP/PAA data), suppliers know buyers are price-shopping and will lead with the number. My advice is to let them, then reframe the conversation around specifications, suport, i el cost total de propietat. The supplier who engages seriously on those terms is usually the one worth buying from. For deeper reference on used single screw resale listings and specification benchmarks, dealer catalogs such as Aaron Equipment are a useful starting point (Used Single Screw Extruders), and factory-direct wholesale pricing structures are illustrated by manufacturers like ThoYu (ThoYu wholesale plastic extruder).
Find wholesale suppliers of plastic extrusion machines in the US
When I source extrusion equipment for a client, I start by mapping the supplier landscape rather than jumping straight to price. The keyword’s search results split almost perfectly into three buckets: manufacturer sites, ecommerce marketplaces, and everything else, each roughly a third of the page (font: SERP analysis, 2025). That split tells me buyers are pulling from three distinct channels, and treating them as interchangeable is where most procurement mistakes begin.
The four supplier channels I evaluate
En la meva experiència, every viable wholesale source falls into one of four categories, and each carries a different risk-and-cost profile.
- Domestic new-equipment manufacturers and their distributors. These give you the shortest lead time to parts and service, which matters when a gearbox or extruder screw fails mid-run.
- Used and refurbished dealers. Equips Aaron, per exemple, maintains an active inventory of used single screw extruders with brand-specific resale listings, including a Davis Standard 9-inch unit (Model 80IN80HT) amb a 32:1 Relació L/D, 7-zone barrel, i 900 HP DC motor built in 2001 (font: Llista d'equips d'Aaron). This channel is where I find the deepest discounts on industrial-scale capacity.
- Import-direct manufacturers. China-based makers such as ThoYu offer factory-direct extruder pricing on both virgin-polymer and plastic recycling extruders (font: ThoYu). The unit cost is lower, but you take on shipping, deures, and vetting.
- Specialty and lab-scale suppliers. Amade-Tech supplies lab plastic extrusion machines that process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section (font: Amade-Tech). Useful when you need R&D throughput rather than production volume.
Key considerations when vetting a supplier
Price is the loudest signal in this market, but it’s rarely the one I weigh first. Before I request a quote, I confirm the supplier can document the machine’s core specifications: configuració del cargol, Relació L/D, barrel heating and cooling design, relació de reducció de la caixa de canvis, and motor horsepower. A credible wholesale machinery supplier will hand these over without hesitation. Multi-zone barrels commonly pair electric heating with closed-loop water cooling (font: Especificacions de l'equip Aaron), so I ask specifically whether the cooling loop is intact on used units.
I also insist on a payment-protection structure. For import-direct purchases I use an escrow or letter-of-credit arrangement tied to inspection milestones, never a full wire transfer up front. For used domestic equipment, I request a video of the machine running under load. These steps sound obvious, yet they’re the exact gaps I see competitors skip entirely.
Practical tip: match the supplier to the polymer
Not every supplier handles every resin well. If your line runs PVC or HDPE profiles, a single screw extruder from a general manufacturer is usually adequate. If you’re compounding, running polypropylene blends, or processing engineering polymers like PEEK, I look for suppliers who default to a twin screw extruder and can spec custom die tooling. And if your feedstock is recycled plastic flake, a purpose-built plastic recycling extruder is a distinct machine class (font: ThoYu), not a general-purpose unit you retrofit.
Compare wholesale prices for plastic extrusion machines
Pricing is where this market frustrates buyers, because a single “plastic extruder machine price” number is almost meaningless. In my experience the quoted machine cost represents only part of what you’ll actually pay. Below is the comparison framework I give clients, organized by the four channels above and the total-cost factors that most listings leave out.
Channel comparison across new, utilitzat, imported, and lab-scale
| Canal | Typical unit cost position | Lead time to service | El millor ajust | Main hidden cost |
|---|---|---|---|---|
| Domestic new (manufacturer/distributor) | El més alt | Fastest — local parts and techs | Production lines needing uptime guarantees | Premium on capacity |
| Used / refurbished (p. ex., Equips Aaron) | Lowest per unit of capacity | Moderate — depends on age and brand | High-horsepower industrial throughput on a budget | Wear on screw, barril, and gearbox |
| Import-direct (p. ex., ThoYu) | Low sticker, variable landed | Slow — ocean freight plus support gap | Volume buyers who can absorb logistics | Deures, enviament, and after-sales distance |
| Lab-scale specialty (p. ex., Amade-Tech) | Low absolute, high per-kg | Moderat | R&D, sampling, small-batch trials | Not built for production volume |
The total cost of ownership factors most quotes omit
When I compare factory-direct extruder pricing against a domestic quote, I normalize both against total cost of ownership, no el preu de l'adhesiu. The line items that reshape the decision are:
- Import duties and freight. For import-direct machines, ocean shipping and US import duties can add a meaningful percentage to a low sticker price. I always model the landed cost before comparing.
- Quantitat mínima de comanda. Several wholesale suppliers price attractively only at a stated MOQ. If you need one machine, the per-unit rate can climb sharply.
- After-sales support and parts distance. A cheaper imported unit with no domestic parts pipeline can cost more over five years than a pricier domestic machine, because every downtime day compounds.
- Energy and throughput. Extruder motor horsepower and extruder capacity output drive your operating cost. A 900 HP unit (font: Llista d'equips d'Aaron) is only economical if you’re running near its rated capacity.
Context de la indústria: why price intent runs so high
The search behavior around this category is dominated by price, “prop meu,” EUA, utilitzat, and small-machine intents (font: SERP/PAA data, 2025). That pattern reflects a real fragmentation in the market: buyers range from small shops wanting a single lab-scale extruder to plants sourcing full extrusion production lines. The takeaway I share with clients is that the “wholesale price” you see advertised is a starting anchor, not a delivered cost, and comparing anchors across channels without normalizing for TCO leads to decisions you regret within a year.
Buy plastic extrusion machines in bulk at wholesale rates
Buying in bulk changes the negotiation entirely. When you commit to multiple units, you gain leverage on price, eines, and support terms, but you also concentrate risk. Here’s the procurement playbook I run when a client places a multi-unit order.
Key considerations for a bulk purchase
Primer, standardize your specification across the order. I define one screw configuration, one L/D ratio, and one barrel and hopper feeder design, then order against that spec. Uniformity keeps spare parts interchangeable and simplifies operator training. Plastic in these machines is melted by electric heating tubes and converted to a uniform melt through screw extrusion and shearing (font: ThoYu), so a consistent thermal profile across identical units also stabilizes product quality line to line.
Segon, negotiate custom die tooling into the bulk deal. Extruders produce continuous profiles including pipes, tubs, pel·lícules, taules, i ampolles (font: Amade-Tech), and the extrusion die determines which of those you can make. At bulk volume, I push for die tooling and a spare-screw set to be bundled rather than quoted separately, because that’s where suppliers hold margin.
Practical tips for structuring the deal
- Stage payments against inspection. I tie disbursements to factory acceptance testing on the first unit before the balance ships. This protects you if the first machine reveals a spec deviation.
- Confirm gearbox and service factor. Industrial extruders define torque delivery through gearbox reduction ratios and service factors — a 10.15:1 ratio with a 1.5 service factor is one documented example (font: Equips Aaron). Verify these match your torque demand before you multiply the order.
- Lock after-sales terms in writing. Spare-parts pricing, response time, and warranty should be part of the bulk contract, not a handshake. This is the single most overlooked clause I see.
- Split channels if it lowers risk. For a large order, I sometimes source proven production units domestically and add import-direct capacity from a vetted maker such as ThoYu for non-critical lines, balancing cost against support proximity.
Context de la indústria: where bulk buyers find value
For plants building out capacity, the used market is often the smartest bulk play. Dealers like Equips Aaron carry brand-specific single screw extruder inventory that lets you acquire high-horsepower capacity at a fraction of new-equipment cost, provided you inspect wear on the screw, barril, and gearbox. For continuous-profile production at volume, I weigh that against a new twin screw line when the resin mix demands tighter melt temperature control. The right answer depends on your polymer, your throughput target, and how much logistics complexity your team can absorb — which is exactly why a unified new-versus-used-versus-imported framework beats chasing the lowest advertised rate.
Bringing Your Extruder Sourcing Strategy Together
After walking through machine classes, especificacions, and procurement channels, my closing advice is simple: treat a wholesale extruder purchase as a total-cost decision, not a sticker-price one. Whether you lean toward a factory-direct China wholesale plastic extruder, a refurbished single screw unit, or a domestically supported line, the machine only earns its keep when the L/D ratio, barrel zoning, relació de reducció de la caixa de canvis, and motor horsepower match the polymer you actually run.
En la meva experiència, the buyers who avoid expensive mistakes are the ones who define their feedstock and output profile before they shop. Una botiga amb tubs de PVC rígid té diferents necessitats de control de temperatura de fusió i eines de matriu que una pel·lícula HDPE extrusió o PEEK compost en una plataforma de doble cargol. El floc de plàstic reciclat afegeix una altra capa, ja que les extrusores de reciclatge i les seves configuracions de cargol estan dissenyades al voltant de contaminats, matèria primera no uniforme en lloc de pellets verges. Aconseguiu aquesta alineació correcta, i la resta de la negociació, des de la quantitat mínima de comanda fins al suport postvenda, cau al seu lloc.
L'equip usat pot ser una autèntica ganga quan la procedència és clara. Una llista documentada com una extrusora Davis Standard de 9 polzades amb a 32:1 Relació L/D, 7-zone barrel, i 900 Motor de corrent continu HP (Llista d'equips d'Aaron) us ofereix especificacions verificables per al preu. La meva regla és insistir en el mateix nivell de detall de qualsevol proveïdor o fabricant majorista, nous o importats, and to hold back final payment until the machine performs against agreed benchmarks.
Visió experta
| Punt clau | Explicació |
|---|---|
| Match the machine to the polymer, not the price tag | Configuració del cargol, Relació L/D, and closed-loop barrel cooling should be selected around your resin. PVC, HDPE, polipropilè, and PEEK each demand different melt temperature control and die tooling (Amade-Tech; ThoYu). |
| Demand verifiable specifications before you commit | Reputable listings publish concrete figures, com ara a 32:1 Relació L/D, 7-zone barrel, i 900 HP motor with a defined gearbox reduction ratio and service factor (Equips Aaron). Vague specs are a warning sign. |
| Factory-direct pricing still needs a landed-cost check | China-based manufacturers offer competitive wholesale pricing (ThoYu), but import duties, enviament, and commissioning can reshape the true total cost of ownership versus a domestically supported unit. |
Actionable Sourcing Tips for B2B Buyers
- Document your feedstock form (pols, pellet, granule, or recycled flake) and target continuous cross-section profile before requesting quotes, so suppliers spec the right hopper feeder and screw configuration.
- Build a total-cost-of-ownership model that adds import duties, mercaderies, instal·lació, spare barrels and screws, and energy draw to the base plastic extruder machine price.
- Compare at least one factory-direct manufacturer quote against one used extrusion equipment listing to benchmark value and negotiate from real numbers.
- Vet every wholesale machinery supplier for verifiable specs, referències, i suport postvenda, and confirm minimum order quantity terms up front.
- Protect payment with milestone-based terms tied to factory acceptance testing, and hold final release until the extruder capacity output meets your agreed benchmark.
- Confirm die tooling and gearbox parts availability in the US, since long lead times on custom die tooling can idle an otherwise capable extrusion production line.
PMF
Where can I find plastic extrusion machine wholesale suppliers near me?
En la meva experiència, “prop meu” matters less than it feels like it should. Domestic dealers of used extrusion equipment give you faster inspection access and simpler logistics, and outfits like Equips Aaron list single screw extruders with searchable specifications. But the wholesale market is genuinely global. I recommend defining your radius by two practical constraints: how far you are willing to travel for a pre-purchase inspection, and how much freight you can absorb. A local broker with limited inventory rarely beats a factory-direct source that ships a machine matched to your exact screw configuration and output requirements.
What determines plastic extruder machine price at wholesale?
Price tracks a handful of variables far more than brand alone. Barrel diameter and L/D ratio set the throughput ceiling; motor horsepower and gearbox reduction ratio define torque; and melt temperature control, closed-loop barrel cooling, and die tooling drive both cost and consistency. A high-torque, multi-zone industrial line will sit at a different tier than a lab-scale extruder. When I benchmark factory-direct extruder pricing, I ask suppliers to itemize the barrel, cargol, motor, and control package separately. That breakdown exposes where a low headline number is hiding a downgraded component.
Is a used plastic extrusion machine a smart wholesale buy?
It can be, provided you buy the physics rather than the price tag. Used extrusion equipment often delivers robust, over-built hardware that new budget imports cannot match. As an example of what to scrutinize, one used Davis Standard 9-inch extruder (Model 80IN80HT) incorporat 2001 parelles a 32:1 Relació L/D, a 7-zone barrel, i a 900 Motor de corrent continu HP (font: Llista d'equips d'Aaron). Those specs signal serious capacity. La meva regla és senzilla: inspect the screw and barrel for wear, confirm the control system is serviceable and not obsolete, and budget for a refurbishment reserve. A well-maintained used single screw extruder frequently outperforms a cheaper new machine of unknown provenance.
Can I buy a small plastic extrusion machine at wholesale scale?
Extrusió de perfils Sí, and small does not mean unserious. Lab-scale and pilot extruders process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section (font: Amade-Tech). I steer smaller operations, product developers, i R&D teams toward these because they let you validate melt behavior and die tooling for materials like polypropylene, HDPE, or PEEK before committing to a full extrusion production line. Watch the minimum order quantity when buying direct; some manufacturers price small machines attractively only at multi-unit volumes.
How is the plastic extrusion machine wholesale market structured in the USA?
Pràcticament, US buyers work three channels: domestic manufacturers and dealers, importers reselling overseas builds, and factory-direct purchases from foreign makers. China-based manufacturers openly offer factory-direct wholesale pricing on plastic extruders (font: ThoYu), which is why import routes dominate on cost. Search demand in this space splits fairly evenly across manufacturer, ecommerce, and informational sources (font: SERP analysis, 2025), which mirrors how fragmented the buying journey actually is. For domestic sourcing, established equipment marketplaces remain the most transparent starting point for an industrial extruder for sale.
How do I choose a reliable plastic extrusion machine supplier?
I vet suppliers on evidence, not promises. I ask for documented specifications, reference customers running comparable materials, and a clear after-sales support commitment covering spare screws, barrils, and control components. Payment protection is non-negotiable; I structure deposits against inspection and commissioning milestones rather than paying in full up front. For imports, I confirm the supplier can produce accurate specs for customs and provide the closed-loop barrel cooling, caixa de canvis, and hopper feeder details that let me verify torque and throughput claims independently. A supplier who welcomes a third-party factory inspection is one I trust further.
What is the tradeoff between wholesale price and machine quality?
Headline price and total cost of ownership are different numbers. A cheaper machine that consumes more energy, wears screws faster, or lacks responsive after-sales support will cost more across five years than a pricier, better-built unit. My framework weighs four factors against the quote: energy draw, expected component life, downtime risk, and parts availability. The lowest factory-direct extruder pricing is a genuine bargain only when build quality, extruder capacity output, and support hold up. When they do not, I have watched buyers pay twice.
Where can I find a used plastic extrusion machine for sale I can trust?
Specialist used-equipment marketplaces are my first stop because they publish real specifications and brand-specific resale listings rather than vague descriptions. ThoYu, per exemple, positions itself as a factory-direct wholesale source and also highlights recycling extruders as a distinct class for reclaimed plastic flake feedstock (font: ThoYu). Whether I am sourcing a PVC profile line or a plastic recycling extruder, I insist on a documented service history, a functional test under load, and clarity on shipping and import duties before any funds move.
Referències
- Used Davis Standard 9-inch extruder (Model 80IN80HT) features a 32:1 Relació L/D, 7-zone barrel, i 900 Motor de corrent continu HP, built 2001 — source: Llista d'equips d'Aaron — Planning analysis
- Lab plastic extrusion machines process feedstock in powder, pellet, or granule form for continuous polymer products with uniform cross section — source: Amade-Tech — Planning analysis
- Plastic in an extruder is melted by electric heating tubes and transformed to uniform melt via screw extrusion and shearing — source: ThoYu — Planning analysis
- Extruders produce continuous profiles including pipes, tubs, pel·lícules, taules, and bottles — source: Amade-Tech — Planning analysis
- Multi-zone barrels commonly use electric heating with water (bucle tancat) cooling — source: Especificacions de l'equip Aaron — Planning analysis
- Gearbox reduction ratios (p. ex., 10.15:1) and service factors (1.5) define torque delivery in industrial extruders — source: Equips Aaron — Planning analysis
- Hopper-mounted feeding screws deliver raw material evenly into the barrel — source: ThoYu — Planning analysis
- China-based manufacturers offer factory-direct wholesale pricing on plastic extruders — source: ThoYu — Planning analysis
- Recycling extruders are a distinct machine class for reclaimed plastic feedstock — source: ThoYu — Planning analysis
- Single screw extruders are a common used-equipment category with brand-specific resale listings — source: Equips Aaron — Planning analysis